WO2020021644A1 - Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure et automobile - Google Patents
Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure et automobile Download PDFInfo
- Publication number
- WO2020021644A1 WO2020021644A1 PCT/JP2018/027770 JP2018027770W WO2020021644A1 WO 2020021644 A1 WO2020021644 A1 WO 2020021644A1 JP 2018027770 W JP2018027770 W JP 2018027770W WO 2020021644 A1 WO2020021644 A1 WO 2020021644A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- friction
- underlining
- mass
- material composition
- heat
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16D—COUPLINGS FOR TRANSMITTING ROTATION; CLUTCHES; BRAKES
- F16D69/00—Friction linings; Attachment thereof; Selection of coacting friction substances or surfaces
- F16D69/02—Composition of linings ; Methods of manufacturing
- F16D69/025—Compositions based on an organic binder
- F16D69/026—Compositions based on an organic binder containing fibres
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16D—COUPLINGS FOR TRANSMITTING ROTATION; CLUTCHES; BRAKES
- F16D65/00—Parts or details
- F16D65/02—Braking members; Mounting thereof
- F16D65/04—Bands, shoes or pads; Pivots or supporting members therefor
- F16D65/092—Bands, shoes or pads; Pivots or supporting members therefor for axially-engaging brakes, e.g. disc brakes
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16D—COUPLINGS FOR TRANSMITTING ROTATION; CLUTCHES; BRAKES
- F16D2200/00—Materials; Production methods therefor
- F16D2200/0004—Materials; Production methods therefor metallic
- F16D2200/0026—Non-ferro
- F16D2200/003—Light metals, e.g. aluminium
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16D—COUPLINGS FOR TRANSMITTING ROTATION; CLUTCHES; BRAKES
- F16D2200/00—Materials; Production methods therefor
- F16D2200/0034—Materials; Production methods therefor non-metallic
- F16D2200/0056—Elastomers
Definitions
- the present invention relates to a friction member, a friction material composition for an underlining material, an underlining material, and a vehicle.
- the specific gravity of steel sheet is about 7.8 mg / m 3
- the specific gravity of aluminum is about 2.7 Mg / m 3 as compared to
- lighter specific gravity of the resin is from about 1 Mg / m 3, such as aluminum and resin
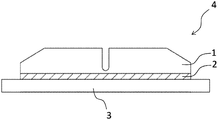
- FIGS. 1 and 2 show an example of a disc brake pad as a friction member for braking attached to a motorcycle or a four-wheeled automobile.
- FIG. 1 is a top view of the disc brake pad 4
- FIG. 2 is an example of a cross-sectional view taken along line AA of FIG.
- the disc brake pad 4 has the upper lining 1 fixed to one surface of the back plate 3 via the lower lining 2.
- a back plate made of a steel plate material has been used for a disc brake pad.
- a back plate using a lighter material has been proposed.
- a back plate having a weight of about 0.1 to 10 mm has been proposed.
- the present inventors have been studying to change the back plate from a conventional steel-made one to a resin-made one or a light-weighted one made of aluminum or the like in order to reduce the weight of the disc brake pad. It has been found that the lightweight material has insufficient durability as compared with the conventional steel back plate. This is thought to be because the frictional heat at the time of braking raises the temperature of the friction material surface, and the heat increases the temperature of the back plate, thereby reducing the mechanical strength of the lightweight material.
- the present invention has been made in order to solve such problems, and a friction material composition for an underlining material capable of improving the durability of a back plate while maintaining good productivity and mechanical strength of the underlining material. It is an object of the present invention to provide an article, an underlining material, a friction member, and a vehicle using the friction material composition for an underlining material.
- the present invention relates to the following [1] to [19].
- a friction member having an upper material, a lower material, and a back plate in this order, The underlining material is formed by molding a friction material composition for an underlining material,
- the friction material composition for underlining material contains an organic filler and a binder,
- the friction material composition for underlining materials which can improve the durability of a backplate, maintaining the productivity and mechanical strength of underlining material favorable, and the friction material composition for underlining materials were used.
- An underlay, a friction member and a vehicle can be provided.
- FIG. 2 is a schematic diagram of an AA cross section in FIG. 1.
- the components are not essential unless otherwise specified.
- the upper limit or the lower limit of the numerical range may be replaced with the value shown in the embodiment.
- the content of each component in the underlining material or the friction material composition for the underlining material when there are a plurality of substances corresponding to each component, unless otherwise specified, the underlining material or the underlining It means the total content of the plurality of types of substances present in the material friction material composition.
- embodiments in which the items described in this specification are arbitrarily combined are also included in the present invention.
- the friction material composition for underlining material of the present embodiment A friction material composition for a subbing material, comprising an organic filler and a binder, and containing, as the organic filler, a heat-insoluble phenol resin.
- a friction material composition for a subbing material comprising an organic filler and a binder, and containing, as the organic filler, a heat-insoluble phenol resin.
- the organic filler can exhibit a function as a friction modifier for improving vibration damping properties, abrasion resistance and the like.
- the organic filler does not include a fibrous material (for example, an organic fiber described later).
- One kind of the organic filler may be used alone, or two or more kinds may be used in combination.
- the friction material composition for underlining material of the present embodiment contains a heat-infusible phenol resin as an organic filler.
- the “heat-unmelting type” refers to a press machine in which 5 g of a particulate phenol resin is inserted between two stainless steel plates having a thickness of 0.2 mm and heated to 100 ° C. Is defined as a property that the particulate phenolic resins do not fuse with each other when pressed at a total load of 2 minutes.
- the heat-infusible phenol resin may be used alone or in combination of two or more.
- the friction material composition for underlining material of the present embodiment contains a heat-infusible phenolic resin as an organic filler, thereby maintaining the productivity and mechanical strength of the underlining material while maintaining the durability of the back plate. Can be improved.
- a heat-infusible phenolic resin as an organic filler, thereby maintaining the productivity and mechanical strength of the underlining material while maintaining the durability of the back plate. Can be improved.
- the present inventors as a method, reduce the content of the organic component having a low thermal conductivity.
- the amount of the binder used conventionally is increased in order to increase the content of the organic component, burrs are generated at the time of molding and productivity is deteriorated, and cashew particles as an organic filler are generated.
- the boiling methanol solubility of the heat-insoluble phenol resin is preferably 20% or less, more preferably 10% or less. Further, the heat-insoluble phenol resin may be one that does not dissolve in boiling methanol.
- the term “solubility of boiling methanol” in the present specification means the content of a boiling methanol-soluble component in the heat-insoluble phenol resin, and specifically, was calculated by the following test. Defined as a value. About 10 g (initial mass) of the heat-infusible phenol resin was precisely weighed and heated under reflux in substantially 500 mL of substantially anhydrous methanol for 30 minutes. Filter through a glass filter of No.
- Boiled methanol solubility (difference between initial mass of heat-insoluble phenolic resin and mass of residue after drying) ⁇ 100 / (initial mass of heat-insoluble phenolic resin) (1)
- the heat-infusible phenol resin is obtained as a reaction product of a phenol and an aldehyde.
- phenols include phenol, naphthol, hydroquinone, resorcinol, xylenol, pyrogallol, and the like. Of these, phenol is preferred.
- Aldehydes include formaldehyde, paraformaldehyde, dalioxal, benzaldehyde and the like. Among these, formaldehyde and paraformaldehyde are preferred.
- one type may be used alone, or two or more types may be used in combination.
- the average particle size of the heat-infusible phenol resin is preferably 1 to 50 ⁇ m, more preferably 5 to 40 ⁇ m, and still more preferably 10 to 30 ⁇ m.
- the average particle diameter means a value of D50 (median diameter of volume distribution, cumulative median value) measured by a method of measuring a laser diffraction particle size distribution, and the same applies hereinafter.
- D50 median diameter of volume distribution, cumulative median value
- LA-920 manufactured by Horiba Ltd.
- the shape of the heat-insoluble phenol resin is not particularly limited, but is preferably spherical.
- the sphericity of the heat-infusible phenol resin is preferably 0.5 or more.
- “sphericity” in this specification refers to the observation of the shape of 50 heat-infusible phenolic resins using a scanning electron microscope, and using the ratio of the shortest diameter / longest diameter of each particle. The calculated arithmetic mean.
- the method for producing the heat-infusible phenolic resin is not particularly limited.
- a particulate phenolic resin is formed by reacting an aldehyde with a phenol in an aqueous medium, and a reaction solution containing the particulate phenolic resin is prepared. After heating to make the granular phenol resin thermally infusible, a method of isolating the heat infusible phenol resin may be mentioned. More specific methods for producing the heat-infusible phenolic resin are as described in, for example, JP-A-57-1770011, WO 2008/047700, and the like.
- the heat-insoluble phenol resin preferably has a methylol group.
- the methylol group is a functional group that can be a reaction point with a phenolic resin or the like of the binder, and the reaction strengthens the bonding interface between the organic filler and the binder, thereby further improving the mechanical strength of the underlay material.
- Becomes The presence of the methylol group can be confirmed by the presence of an absorption peak at 990 to 1015 cm ⁇ 1 attributed to the methylol group in an infrared absorption spectrum by a KBr tablet method.
- the amount of the methylol group is not particularly limited, the infrared absorption peak intensity D 990 to 1015 at 990 to 1015 cm ⁇ 1 attributed to the methylol group and the infrared absorption peak intensity D 1600 at 1600 cm ⁇ 1 derived from the benzene nucleus are obtained.
- the ratio [D 990 to 1015 / D 1600 ] is preferably in the range of 0.2 to 9.0.
- the content of the heat-insoluble phenolic resin in the friction material composition for underlining material of the present embodiment is preferably 3 to 40 parts by mass, more preferably 5 to 30 parts by mass, based on 100 parts by mass of the friction material composition for underlining material. Part by mass, more preferably 7 to 25 parts by mass, still more preferably 10 to 20 parts by mass, and particularly preferably 13 to 18 parts by mass.
- the content of the heat-infusible phenolic resin is within the above range, the durability of the back plate can be further improved while the productivity and mechanical strength of the underlay material are kept good.
- the friction material composition for underlining material of the present embodiment may further contain an organic filler such as cashew particles, rubber, and melamine dust.
- an organic filler such as cashew particles, rubber, and melamine dust.
- cashew particles and rubber are preferred from the viewpoints of improving the stability of friction coefficient and wear resistance and suppressing squeal.
- Cashew particles and rubber may be used in combination, or cashew particles coated with rubber may be used.
- the other organic fillers one type may be used alone, or two or more types may be used in combination.
- Cashew particles are obtained by pulverizing hardened cashew nut shell oil and may be generally referred to as cashew dust.
- Cashew particles are generally classified into brown, brown-black, black, and the like, depending on the type of curing agent used in the curing reaction.
- the average particle size of the cashew particles is preferably 850 ⁇ m or less, more preferably 750 ⁇ m or less, and even more preferably 600 ⁇ m or less, from the viewpoint of dispersibility.
- the lower limit of the average particle size of the cashew particles is not particularly limited, and may be 200 ⁇ m or more, 300 ⁇ m or more, or 400 ⁇ m or more.
- the content is preferably 0.5 to 10 parts by mass with respect to 100 parts by mass of the friction material composition for underlining material. 7 parts by mass is more preferable, and 2 to 5 parts by mass is further preferable.
- the content of the cashew particles is equal to or more than the lower limit, appropriate flexibility can be imparted to the underlay material, so that there is a tendency that sound vibration can be improved, and when the content is equal to or less than the upper limit, heat resistance and There is a tendency that a decrease in crack resistance can be suppressed.
- a rubber commonly used for an underlay material can be used, and examples thereof include natural rubber and synthetic rubber.
- the synthetic rubber include acrylonitrile-butadiene rubber (NBR), acrylic rubber, isoprene rubber, polybutadiene rubber (BR), styrene butadiene rubber (SBR), silicone rubber, and ground powder of tire tread rubber.
- NBR acrylonitrile-butadiene rubber
- BR polybutadiene rubber
- SBR styrene butadiene rubber
- silicone rubber and ground powder of tire tread rubber.
- acrylonitrile-butadiene rubber (NBR) and pulverized powder of tire tread rubber are preferable from the viewpoint of balance between heat resistance, flexibility and production cost.
- the content is preferably 1 to 35 parts by mass, and more preferably 10 to 30 parts by mass with respect to 100 parts by mass of the friction material composition for underlining material. Is more preferable, and 15 to 25 parts by mass is further preferable.
- the rubber content is in the above range, the elastic modulus of the underlining material tends to be high, and it is possible to avoid deterioration of vibration damping properties such as squealing, and also deterioration of heat resistance and heat history. This tends to prevent the strength from being reduced.
- the total content of the organic filler in the friction material composition for underlining material of the present embodiment is preferably 5 to 60 parts by mass, and more preferably 10 to 50 parts by mass with respect to 100 parts by mass of the friction material composition for underlining material.
- the content is more preferably 15 to 45 parts by mass, and particularly preferably 20 to 40 parts by mass.
- the binder has a function of binding and integrating an organic filler, an inorganic filler used as necessary, a fiber base material, and the like, and giving a predetermined shape and strength.
- a binder commonly used for an underlay material can be used.
- the thermosetting resin include a phenol resin, an epoxy resin, a polyimide resin, and a melamine resin.
- the phenolic resin may be an unmodified phenolic resin, a modified phenolic resin, an elastomer-dispersed phenolic resin, or the like.
- the modified phenolic resin acrylic-modified phenolic resin, silicone-modified phenolic resin, cashew-modified phenolic resin, Epoxy-modified phenolic resins, alkylbenzene-modified phenolic resins, and the like.
- the elastomer-dispersed phenolic resin include an acrylic elastomer-dispersed phenolic resin and a silicone elastomer-dispersed phenolic resin.
- unmodified phenolic resin acrylic-modified phenolic resin, silicone-modified phenolic resin, and alkylbenzene-modified phenolic resin are preferable from the viewpoint of providing good heat resistance, moldability and friction coefficient.
- One kind of the binder may be used alone, or two or more kinds may be used in combination.
- the phenolic resin used as the binder is preferably a hot-melt phenolic resin from the viewpoint of the moldability of the friction material composition for underlining materials.
- the “hot-melt type” means that 5 g of a particulate phenol resin is inserted between two 0.2 mm-thick stainless steel plates and heated at 100 ° C. with a total load of 50 kg for 2 minutes. When pressed, it is defined as the property that particulate phenolic resins fuse together.
- the total content of the heat-infusible phenol resin and the hot-melt phenol resin is preferably from 10 to 60 parts by mass, more preferably from 15 to 55 parts by mass, based on 100 parts by mass of the friction material composition for underlining material. 20 to 50 parts by mass are more preferred. When the total content is within the above range, the durability of the back plate can be further improved while maintaining the productivity and mechanical strength of the underlay material.
- the content of the binder in the friction material composition for underlining material of the present embodiment is preferably 5 to 45 parts by mass, more preferably 8 to 40 parts by mass, based on 100 parts by mass of the friction material composition for underlining material. Is more preferably 10 to 35 parts by mass, particularly preferably 12 to 30 parts by mass.
- the friction material composition for underlining material of the present embodiment further contains an inorganic filler.
- the inorganic filler can exhibit a function as a friction adjusting material for avoiding deterioration of the heat resistance, abrasion resistance, stability of friction coefficient and the like of the underlining material.
- the inorganic filler does not include a fibrous material (for example, an inorganic fiber described later).
- the inorganic filler one type may be used alone, or two or more types may be used in combination.
- the inorganic filler there is no particular limitation on the inorganic filler, and an inorganic filler generally used for an underlay material can be used.
- the inorganic filler include metal sulfides such as antimony trisulfide, tin sulfide, molybdenum disulfide, bismuth sulfide, and zinc sulfide; and titanium such as potassium titanate, lithium potassium titanate, sodium titanate, and potassium magnesium titanate.
- Acid salts mica, graphite, coke, calcium hydroxide, calcium oxide, sodium carbonate, calcium carbonate, magnesium carbonate, barium sulfate, dolomite, coke, mica, vermiculite, calcium sulfate, granular potassium titanate, plate-like potassium titanate, Talc, clay, zeolite, chromite, zirconium oxide, titanium oxide, magnesium oxide, triiron tetroxide, zinc oxide, ⁇ -alumina; iron powder, cast iron powder, aluminum powder, nickel powder, tin powder, zinc powder, and the above metals Small of A metal powder of an alloy powder and the like containing Kutomo one metal. Among these, barium sulfate is preferred.
- the content is preferably 1 to 60 parts by mass, and more preferably 3 to 50 parts by mass, per 100 parts by mass of the friction material composition for underlining material.
- the parts by mass are more preferably 5 to 40 parts by mass, and particularly preferably 8 to 35 parts by mass.
- the friction material composition for underlining material of the present embodiment further contains a fiber base material.
- the fibrous base material has a reinforcing effect on the underlay material.
- Examples of the fiber base include organic fibers and inorganic fibers.
- One type of fiber base material may be used alone, or two or more types may be used in combination.
- the organic fiber is a fibrous material containing an organic substance as a main component.
- the organic fiber include hemp, cotton, aramid fiber, cellulose fiber, and acrylic fiber. Among these, aramid fibers are preferred from the viewpoint of heat resistance.
- the content is preferably 1 to 20 parts by mass, and more preferably 3 to 15 parts by mass with respect to 100 parts by mass of the friction material composition for underlining material. Part by mass, more preferably 7 to 12 parts by mass.
- the inorganic fiber is a fibrous material mainly composed of an inorganic substance other than a metal and a metal alloy, and can exert an effect of improving the mechanical strength and abrasion resistance of the underlining material.
- the inorganic fiber include mineral fiber, glass fiber, fibrous wollastonite, metal fiber, carbon fiber, ceramic fiber, biodegradable ceramic fiber, rock wool, potassium titanate fiber, silica alumina fiber, flame-resistant fiber, and the like.
- mineral fibers are preferred.
- the mineral fibers are artificial inorganic fibers melt-spun with blast furnace slag such as slag wool, basalt such as basalt fiber, and other natural rocks as main components.
- the mineral fiber examples include a mineral fiber containing SiO 2 , Al 2 O 3 , CaO, MgO, FeO, Na 2 O, etc., or a mineral fiber containing one or more of these compounds.
- a mineral fiber containing an aluminum element is preferred, a mineral fiber containing Al 2 O 3 is more preferred, and a mineral fiber containing Al 2 O 3 and SiO 2 is even more preferred.
- the average fiber length of the mineral fibers is preferably 500 ⁇ m or less, more preferably 400 ⁇ m or less, and even more preferably 340 ⁇ m or less, from the viewpoint of suppressing a decrease in shear strength.
- the lower limit of the mineral fiber may be, for example, 100 ⁇ m or more, or 120 ⁇ m or more.
- the average fiber diameter (diameter) of the mineral fibers is not particularly limited, but is usually 1 to 20 ⁇ m, and may be 2 to 15 ⁇ m.
- the mineral fibers are preferably biosoluble from the viewpoint of harmful effects on the human body.
- biosoluble mineral fiber refers to a mineral fiber that has the characteristic of being partially decomposed in a short time and discharged out of the body even when taken into the human body.
- the chemical composition is such that the total amount of alkali oxides and alkaline earth oxides (total amount of sodium, potassium, calcium, magnesium and barium oxides) is 18% by mass or more, and (a) short-term inhalation
- the half-life of a fiber having a length of more than 20 ⁇ m is less than 10 days in an in vivo durability test by exposure, and (b) a half-life of a fiber having a length of more than 20 ⁇ m in an in vivo durability test by short-term intratracheal injection. Less than 40 days, (c) no significant carcinogenicity in the intraperitoneal administration test, or (d) no pathological findings or tumor formation associated with carcinogenicity in the long-term inhalation exposure test.
- Such biodegradable mineral fibers include SiO 2 —Al 2 O 3 —CaO—MgO. -F O (-K 2 O-Na 2 O) fibers and the like, SiO 2, Al 2 O 3 , CaO, MgO, FeO, the optional at least two selected from K 2 O and Na 2 O, etc. Mineral fibers contained in combination.
- the content is preferably 5 to 40 parts by mass, more preferably 10 to 30 parts by mass, based on 100 parts by mass of the friction material composition for underlining material. Part by mass, more preferably 15 to 25 parts by mass.
- the content of the inorganic fiber is within the above range, the mechanical strength and the wear resistance of the underlay material can be further improved.
- the friction material composition for underlining material of the present embodiment may be composed only of the above-mentioned components, and may contain other components other than the above-described components as necessary.
- the friction material composition for underlining material of the present embodiment preferably does not contain copper.
- the content of copper in the friction material composition for underlining material is 0.1% as a copper element. It is preferably less than 5% by mass, more preferably 0.2% by mass or less, even more preferably 0.05% by mass or less.
- the content of copper indicates the content of copper element (Cu) contained in copper, copper alloy, and copper compound in fibrous or powdery form in the entire friction material composition for underlining material.
- the friction material composition for underlining material of the present embodiment does not contain an iron-based metal, but when an iron-based metal is contained, the content of the iron-based metal in the friction material composition for underlining material is preferably , Iron element is preferably less than 0.5% by mass, more preferably 0.2% by mass or less, further preferably 0.05% by mass or less.
- Iron element is preferably less than 0.5% by mass, more preferably 0.2% by mass or less, further preferably 0.05% by mass or less.
- the friction material composition for underlining material of the present embodiment is classified as NAO (Non-Asbestos-Organic) material, and is a so-called non-asbestos friction material composition (a friction material composition containing no asbestos or containing it). Even in this case, the friction material composition has a very small amount of asbestos. It is preferable that the friction material composition for underlining material of the present embodiment does not contain asbestos. However, when asbestos is contained, the content is 0.1 to 100 parts by mass of the friction material composition for underlining material. It is preferably at most 2% by mass.
- the total content of the organic components in the underlining material friction material composition of the present embodiment is preferably 20 parts by mass or more, more preferably 40 parts by mass or more, based on 100 parts by mass of the underlining material friction material composition. It is more preferably at least 50 parts by mass, particularly preferably at least 60 parts by mass. When the total content is within the above range, the durability of the back plate can be further improved while maintaining the productivity and mechanical strength of the underlay material.
- the total content of the organic components may be not more than 80 parts by mass, or may be not more than 75 parts by mass with respect to 100 parts by mass of the friction material composition for underlining materials.
- the friction member according to the present embodiment includes: A friction member having an upper material, a lower material, and a back plate in this order,
- the underlining material is formed by molding a friction material composition for an underlining material,
- the friction material composition for underlining material contains an organic filler and a binder,
- the organic filler contains a heat-insoluble phenol resin.
- the underlining material of the present embodiment is obtained by molding the friction material composition for an underlining material of the present embodiment.
- the preferable aspect of the friction material composition for an underlining material used for forming the underlining material provided in the friction member of the present embodiment is the same as the preferable aspect of the above-described friction material composition for an underlining material of the present embodiment.
- FIG. 1 and 2 show a disc brake pad 4 which is one mode of the friction member of the present embodiment.
- the disc brake pad 4 has a back plate 3, a lower lining material 2, and an upper lining material 1 in this order.
- the overlay material 1 is formed by molding a friction material composition for an overlay material, and is a friction material that becomes a friction surface of a friction member.
- a friction material composition for an overlay there is no particular limitation on the friction material composition for an overlay, and a known friction material composition for an overlay can be used. Specifically, it contains an organic filler, an inorganic filler, a fiber base material, and a binder, and does not contain copper, or even if it contains copper, the content of copper is 0.5% by mass as a copper element. It is preferable to use a friction material composition for an upholstery material that is less than.
- the organic filler, the inorganic filler, the fiber base material, and the binder the same ones as described in the friction material composition for the underlay material can be used.
- the lower lining material 2 is formed by molding the friction material composition for the lower lining material of the present embodiment, and is a layer interposed between the upper lining material 1 serving as a friction surface of the friction member and the back plate 3. is there.
- the thickness of the underlining material 2 is preferably 1 mm or more, more preferably 1 to 5 mm, and still more preferably 2 to 4 mm. When the thickness of the underlining material is 1 mm or more, the heat insulating effect between the overlining material and the back plate increases, and cracks and cracks in the back plate can be effectively suppressed.
- the thermal conductivity of the underlining material 2 in the thickness direction is preferably 0.50 W / m ⁇ K or less, more preferably 0.40 W / m ⁇ K or less, further preferably 0.35 W / m ⁇ K or less, and 0.30 W / m ⁇ K. / MK or less is particularly preferred.
- the lower limit of the thermal conductivity in the thickness direction of the underlining material 2 is not particularly limited, and may be 0.05 W / m ⁇ K or more, or 0.1 W / m ⁇ K or more.
- the back plate 3 is not particularly limited, but preferably contains a material having a lower specific gravity than steel from the viewpoint of weight reduction.
- the back plate contains a material having a lighter specific gravity than steel, preferably 50% by volume or more, more preferably 80% by volume or more, and still more preferably 90% by volume or more. preferable.
- the specific gravity of the light material than steel specific gravity is preferably from 5 mg / m 3 or less, more preferably 3Mg / m 3 or less, more preferably 2Mg / m 3 or less.
- the specific gravity of the back plate is preferably 5 mg / m 3 or less, more preferably 3Mg / m 3 or less, more preferably 2Mg / m 3 or less.
- the material having a lower specific gravity than steel examples include (1) fiber-reinforced resin, (2-1) aluminum alloy, (2-2) aluminum or an aluminum composite material in which ceramic particles are dispersed in aluminum or an aluminum alloy, (3-1) And (3-2) magnesium or a magnesium composite material in which ceramic particles are dispersed in a magnesium alloy. That is, the back plate contains at least one selected from the group consisting of the above materials (1), (2-1), (2-2), (3-1) and (3-2). And may consist of at least one selected from the group consisting of the above materials (1), (2-1), (2-2), (3-1) and (3-2). You may.
- the fiber-reinforced resin refers to a composite of fiber and resin, that is, a composite of fiber and resin. Since the specific gravity of the fiber reinforced resin is about 1 Mg / m 3, it is suitable as a lightweight material.
- the fiber used for the fiber reinforced resin examples include glass fiber, alumina fiber such as ⁇ -alumina type and ⁇ -alumina type, and inorganic fiber such as boron fiber; aramid fiber such as para-aramid fiber and meta-aramid fiber; At least one selected from the group consisting of cellulose fibers, nanocellulose fibers, PBO (polyparaphenylenebenzoxazole) fibers, or oxidized fibers, pitch-based fibers, and carbon-based fibers such as PAN (polyacrylonitrile) -based carbon fibers; Can be used. Particularly when used as a back plate, glass fibers and carbon fibers are preferable from the viewpoint of strength and rigidity, and carbon fibers are more preferable from the viewpoint of high thermal conductivity.
- the thermal conductivity of the back plate can be further improved, and when the braking temperature is increased by frictional heat due to repeated braking, the temperature distribution in the back plate can be made uniform. In addition, there is a tendency that a local temperature rise is prevented, and cracks and cracks due to thermal decomposition and a decrease in strength of the resin are easily prevented.
- the phenol resin examples include a resol-type phenol resin, a straight novolak-type phenol resin, an aralkyl-modified phenol resin, and an elastomer-modified phenol resin modified with an acrylic elastomer, a silicone elastomer, or the like.
- a straight novolak type phenol resin and a resol type phenol resin are preferable from the viewpoint of heat resistance.
- the epoxy resin a commercially available product can be used, and the epoxy resin can be synthesized by a conventional method.
- the epoxy resin is preferably an epoxy resin having an aromatic ring from the viewpoint of strength and heat resistance.
- a phenol novolak type epoxy resin a cresol novolak type epoxy resin, a naphthalene type epoxy resin, or the like can be suitably used.
- epoxy resin modified with silicone, acrylonitrile, butadiene, isopropyl rubber, polyamide resin, or the like can also be used.
- additives can be added in addition to the fibers and the resin.
- Other additives include inorganic fillers, organic fillers, metal powders and the like.
- the other additives one kind may be used alone, and two kinds or more may be used in combination.
- the other additives are preferably an inorganic filler, an organic filler, and a metal powder in the form of particles.
- the particle diameter is preferably small. Specifically, from the viewpoint of improving slidability, graphite, molybdenum disulfide, tungsten sulfide, fluororesin, coke, and the like are mentioned.
- magnesium hydroxide and aluminum hydroxide are used.
- antimony compounds, etc. from the viewpoint of weight reduction, hollow inorganic particles, etc., from the viewpoint of improving the curing speed of the resin, calcium oxide, calcium hydroxide, etc., to improve the thermal conductivity
- metal powder, graphite, magnesium oxide, zinc oxide and the like can be mentioned.
- Aluminum has a small specific gravity of about 2.7 Mg / m 3 and is suitable as a lightweight material. However, from the viewpoint of strength, it is preferable to use an aluminum alloy as the back plate.
- Aluminum alloys include 2XXX (Al-Cu), 3XXX (Al-Mn), 4XXX (Al-Si), 5XXX (Al-Mg), and 6XXX (Al-Mg-Si).
- AC1C Al-Cu-based
- AC1B Al-Cu-based
- AC2A Al-Cu-Si-based
- AC2B Al-Cu-) Si-based
- AC3A Al-Si-based
- AC4A AC4C
- AC4C Al-Si-Mg-based
- AC4B Al-Si-Cu-based
- AC4D Al-Si-Cu-Mg-based
- AC5A Al- Cu-Ni-Mg
- AC7A Al-Mg
- AC8A Al-Si-Cu-Ni-Mg
- AC8B Al-Si-Cu-Ni-Mg
- AC9A Al-Si-) Cu-Mg type , AC9B (Al-Si-Cu-Mg) and other casting aluminum alloys
- ADC1 Al-Si
- ADC3 Al-Si
- Aluminum composite materials (ceramic particle reinforced aluminum-based composite materials) in which ceramic particles are dispersed in aluminum or the above aluminum alloy have a higher Young's modulus than aluminum alloys. The rigidity can be increased, which is preferable.
- oxide-based ceramics such as Al 2 O 3 , TiO 2 , SiO 2 , and ZrO 2 ; carbide-based ceramics such as SiC and TiC; and nitride-based ceramics such as TiN can be used.
- magnesium alloy Since magnesium has a small specific gravity of 1.74 Mg / m 3 , it is suitable as a lightweight material, but from the viewpoint of strength, it is preferable to use a magnesium alloy as the back plate.
- the magnesium alloy include M1 (Mg—Mn alloy); AZ series such as AZ61 and AZ91 (Mg—Al—Zn alloy); ZK series such as ZK51 and ZK60 (Mg—Zn—Zr alloy); ZH series such as ZH62.
- Mg-Zn-Zr alloy EK-based (Mg-Rare-earth alloy) such as EK30; HK-based (Mg-Th-based alloy) such as HK31; K1 (Mg-Zr alloy);
- a magnesium alloy for processing can be used.
- a flame-retardant magnesium alloy to which calcium is added by several% can be used.
- Ceramic particle reinforced magnesium-based composite material in which ceramic particles are dispersed in magnesium or the above magnesium alloy has a higher Young's modulus than a magnesium alloy.
- the rigidity can be increased, which is preferable.
- oxide ceramics such as Al 2 O 3 , TiO 2 , SiO 2 , ZrO 2 , carbide ceramics such as SiC and TiC, and nitride ceramics such as TiN can be used.
- the thermal conductivity of the back plate in the thickness direction is preferably 0.4 W / m ⁇ K or more, more preferably 0.45 W / m ⁇ K or more, and still more preferably 1.0 W / m ⁇ K or more.
- the upper limit of the thermal conductivity in the thickness direction of the back plate is not particularly limited, but may be 400 W / m ⁇ K or less, or 250 W / m ⁇ K or less.
- the friction member of the present embodiment may be, for example, a friction material composition for an overlay material and a friction material composition for an underlay material of the present embodiment, respectively, separately prepared by a Reidige mixer (“Redige” is a registered trademark), Mixing using a mixer such as a kneader or an Eirich mixer (“Eirich” is a registered trademark), and then mixing the friction material composition for an upper material and the friction material composition for a lower material with a molding die after mixing. And a preform for underlaying material and a preform for uppering material are superimposed on one surface of the back plate, for example, under the conditions of a molding temperature of 130 to 160 ° C. and a molding pressure of 20 to 50 MPa.
- the mixture may be directly thermoformed without the preforming step.
- the friction member of the present embodiment is suitable for a disc brake pad or a drum brake lining. Further, the friction material composition for the overlay material and the friction material composition for the underlay material of the present embodiment are formed into a target shape, processed, pasted, and the like, so that clutch facing, an electromagnetic brake, a holding brake, etc. It can also be used as a friction material.
- the embodiment also provides a vehicle equipped with the friction member of the embodiment.
- the vehicle include large vehicles, medium vehicles, ordinary vehicles, large special vehicles, small special vehicles, large motorcycles, and ordinary motorcycles.
- Thermal conductivity in the thickness direction of the underlining material is measured by shaping the friction material composition for the underlining material at 150 ° C. for 5 minutes at 30 MPa, and then cutting out into a columnar shape having a diameter of 50 mm and a thickness of 2 mm.
- a sample is prepared, the bottom surface of the sample for measurement is sandwiched between two metal cylinders, and a temperature gradient method at room temperature (25 ° C.) under atmospheric pressure (Arc Technology Co., Ltd. thermal conductivity measurement device “ARC -TC-1 ”).
- the temperature difference between the two metal cylinders in contact with the sample was 13 to 20 ° C., and the average temperature was 25 ° C. Nominal values are shown in Table 2 for the thermal conductivity of the back plate.
- the temperature of the back plate at the 50th braking was measured by a thermocouple embedded in the back plate.
- b There was no breakage of the back plate portion and no deformation exceeding 1 mm, but cracks occurred.
- NBR acrylonitrile-butadiene rubber powder
- NBR acrylonitrile-butadiene rubber powder
- -Potassium titanate-Zirconia-Mica-Graphite artificial graphite, sphere, average particle size 15 m ⁇ Tin sulfide ⁇ Barium sulfate ⁇ Calcium hydroxide (fiber base material)
- Aramid fiber fibrillated aramid fiber
- Mineral fiber average fiber length 230 ⁇ 50 ⁇ m
- Aluminum alloy A5083 GFRP: phenolic resin composited with 25 mm glass fiber (glass fiber 50% by mass)
- CFRP phenolic resin composited with 25 mm carbon fiber (50% by mass of carbon fiber)
- Examples 1 to 6 and Comparative Examples 1 to 5 (Production of disc brake pad) According to the blending amounts shown in Tables 1 and 2, each component was blended for each of the friction material composition for the overlay material and the friction material composition for the underlay material. The mixture was mixed with a digue mixer M20) to obtain a friction material composition for an upper material and a friction material composition for a lower material. The friction material composition for an upper covering material and the friction material composition for a lower covering material were integrally preformed by a molding press (manufactured by Oji Machine Industry Co., Ltd.).
- the obtained preformed product was heated and pressed together with the back plate shown in Table 2 using a molding press (manufactured by Sanki Seiko Co., Ltd.) under the conditions of a molding temperature of 140 to 160 ° C., a molding pressure of 30 MPa, and a molding time of 5 minutes. Molded.
- the obtained molded article was heat-treated at 200 ° C. for 4.5 hours, polished using a rotary polisher, and scorched at 500 ° C. to obtain a disc brake pad.
- the disc brake pads obtained in Examples and Comparative Examples had a back plate thickness of 6 mm, an upper material thickness of 4 mm, a lower material thickness of 3 mm, and a friction material projected area of 52 cm 2 . Using the obtained disc brake pads, each measurement and evaluation were performed according to the above-described methods. Table 2 shows the results.
Landscapes
- Engineering & Computer Science (AREA)
- General Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Compositions Of Macromolecular Compounds (AREA)
- Braking Arrangements (AREA)
- Manufacture Of Macromolecular Shaped Articles (AREA)
Abstract
La présente invention concerne : une composition de matériau de frottement pour matériaux de couche inférieure, qui contient une charge organique et un liant, et qui contient une résine phénolique non thermofusible en tant que charge organique ; un matériau de couche inférieure qui utilise cette composition de matériau de frottement pour des matériaux de couche inférieure ; un élément de frottement; et une automobile.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/JP2018/027770 WO2020021644A1 (fr) | 2018-07-24 | 2018-07-24 | Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure et automobile |
| JP2020531884A JP7226447B2 (ja) | 2018-07-24 | 2018-07-24 | 摩擦部材、下張り材用摩擦材組成物、下張り材及び車 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/JP2018/027770 WO2020021644A1 (fr) | 2018-07-24 | 2018-07-24 | Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure et automobile |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020021644A1 true WO2020021644A1 (fr) | 2020-01-30 |
Family
ID=69182297
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2018/027770 Ceased WO2020021644A1 (fr) | 2018-07-24 | 2018-07-24 | Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure et automobile |
Country Status (2)
| Country | Link |
|---|---|
| JP (1) | JP7226447B2 (fr) |
| WO (1) | WO2020021644A1 (fr) |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0276935A (ja) * | 1988-09-12 | 1990-03-16 | Honda Motor Co Ltd | 摩擦材 |
| JPH04338107A (ja) * | 1991-05-15 | 1992-11-25 | Kuraray Chem Corp | 球状活性炭の製法 |
| JP2000046078A (ja) * | 1998-07-29 | 2000-02-15 | Taiheiyo Cement Corp | ブレーキパッド用バッキングプレート及びその製造方 法 |
| JP2017057312A (ja) * | 2015-09-17 | 2017-03-23 | 曙ブレーキ工業株式会社 | 摩擦材組成物及び摩擦材 |
| WO2017183155A1 (fr) * | 2016-04-21 | 2017-10-26 | 日立化成株式会社 | Composition de matériau de friction, matériau de friction et élément de friction obtenus à partir de ladite composition |
-
2018
- 2018-07-24 WO PCT/JP2018/027770 patent/WO2020021644A1/fr not_active Ceased
- 2018-07-24 JP JP2020531884A patent/JP7226447B2/ja active Active
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0276935A (ja) * | 1988-09-12 | 1990-03-16 | Honda Motor Co Ltd | 摩擦材 |
| JPH04338107A (ja) * | 1991-05-15 | 1992-11-25 | Kuraray Chem Corp | 球状活性炭の製法 |
| JP2000046078A (ja) * | 1998-07-29 | 2000-02-15 | Taiheiyo Cement Corp | ブレーキパッド用バッキングプレート及びその製造方 法 |
| JP2017057312A (ja) * | 2015-09-17 | 2017-03-23 | 曙ブレーキ工業株式会社 | 摩擦材組成物及び摩擦材 |
| WO2017183155A1 (fr) * | 2016-04-21 | 2017-10-26 | 日立化成株式会社 | Composition de matériau de friction, matériau de friction et élément de friction obtenus à partir de ladite composition |
Also Published As
| Publication number | Publication date |
|---|---|
| JPWO2020021644A1 (ja) | 2021-08-12 |
| JP7226447B2 (ja) | 2023-02-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6281755B1 (ja) | 摩擦材組成物、およびこれを用いた摩擦材および摩擦部材 | |
| WO2020021646A1 (fr) | Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure, plaquette de frein à disque et automobile | |
| JP5790175B2 (ja) | ノンアスベスト摩擦材組成物 | |
| US11155733B2 (en) | Friction material composition, and friction material and friction member each obtained using friction material composition | |
| JP6425894B2 (ja) | 摩擦材組成物、摩擦材組成物を用いた摩擦材及び摩擦部材 | |
| JPWO2012066963A1 (ja) | ノンアスベスト摩擦材組成物、これを用いた摩擦材及び摩擦部材 | |
| JPWO2016060129A1 (ja) | 摩擦材組成物、摩擦材および摩擦部材 | |
| JP5987539B2 (ja) | 摩擦材組成物、これを用いた摩擦材及び摩擦部材 | |
| US20200332851A1 (en) | Frictional member, and frictional material composition and frictional material for lower-layer material | |
| WO2020021647A1 (fr) | Élément de frottement, composition de matériau de frottement pour matériaux de couche inférieure, matériau de couche inférieure, plaquette de frein à disque et automobile | |
| WO2017130332A1 (fr) | Composition de matériau de frottement, matériau de frottement et élément de frottement | |
| JPWO2018230672A1 (ja) | 摩擦部材、ディスクブレーキパッド及び車 | |
| JP6493956B2 (ja) | 摩擦材組成物、摩擦材及び摩擦部材 | |
| JP6440947B2 (ja) | 摩擦材組成物、摩擦材組成物を用いた摩擦材及び摩擦部材 | |
| JP2016145274A (ja) | 摩擦材および摩擦部材 | |
| JP6596956B2 (ja) | 摩擦材組成物、およびこれを用いた摩擦材および摩擦部材 | |
| JP7226447B2 (ja) | 摩擦部材、下張り材用摩擦材組成物、下張り材及び車 | |
| JP2022094170A (ja) | ディスクブレーキパッド | |
| JP6570167B2 (ja) | 摩擦材組成物、およびこれを用いた摩擦材および摩擦部材 | |
| JP7226448B2 (ja) | バックプレート、ディスクブレーキパッド及びキャリパーアッセンブリ | |
| JP7702251B2 (ja) | 摩擦部材、摩擦材組成物、摩擦材及び車 | |
| JP6553355B2 (ja) | 摩擦材組成物、摩擦材組成物を用いた摩擦材および摩擦部材 | |
| WO2020255279A1 (fr) | Élément de frottement, composition de matériau de frottement, matériau de frottement et véhicule | |
| JP2020073635A (ja) | 摩擦材組成物、摩擦材および摩擦部材 | |
| JP2019059941A (ja) | 摩擦材組成物、摩擦材組成物を用いた摩擦材及び摩擦部材 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 18927270 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2020531884 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 18927270 Country of ref document: EP Kind code of ref document: A1 |