WO2020196149A1 - Tôle d'acier plaquée de zn-al-mg en fusion et son procédé de fabrication - Google Patents
Tôle d'acier plaquée de zn-al-mg en fusion et son procédé de fabrication Download PDFInfo
- Publication number
- WO2020196149A1 WO2020196149A1 PCT/JP2020/011959 JP2020011959W WO2020196149A1 WO 2020196149 A1 WO2020196149 A1 WO 2020196149A1 JP 2020011959 W JP2020011959 W JP 2020011959W WO 2020196149 A1 WO2020196149 A1 WO 2020196149A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- steel sheet
- molten
- less
- hot
- plated steel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
- C23C2/022—Pretreatment of the material to be coated, e.g. for coating on selected surface areas by heating
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/38—Ferrous alloys, e.g. steel alloys containing chromium with more than 1.5% by weight of manganese
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/01—Layered products comprising a layer of metal all layers being exclusively metallic
- B32B15/012—Layered products comprising a layer of metal all layers being exclusively metallic one layer being formed of an iron alloy or steel, another layer being formed of aluminium or an aluminium alloy
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/01—Layered products comprising a layer of metal all layers being exclusively metallic
- B32B15/013—Layered products comprising a layer of metal all layers being exclusively metallic one layer being formed of an iron alloy or steel, another layer being formed of a metal other than iron or aluminium
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/04—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/04—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material
- B32B15/043—Layered products comprising a layer of metal comprising metal as the main or only constituent of a layer, which is next to another layer of the same or of a different material of metal
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/18—Layered products comprising a layer of metal comprising iron or steel
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/20—Layered products comprising a layer of metal comprising aluminium or copper
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0226—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/06—Ferrous alloys, e.g. steel alloys containing aluminium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/14—Ferrous alloys, e.g. steel alloys containing titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/22—Ferrous alloys, e.g. steel alloys containing chromium with molybdenum or tungsten
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/24—Ferrous alloys, e.g. steel alloys containing chromium with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/26—Ferrous alloys, e.g. steel alloys containing chromium with niobium or tantalum
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/28—Ferrous alloys, e.g. steel alloys containing chromium with titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/32—Ferrous alloys, e.g. steel alloys containing chromium with boron
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/44—Ferrous alloys, e.g. steel alloys containing chromium with nickel with molybdenum or tungsten
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/46—Ferrous alloys, e.g. steel alloys containing chromium with nickel with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/50—Ferrous alloys, e.g. steel alloys containing chromium with nickel with titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/54—Ferrous alloys, e.g. steel alloys containing chromium with nickel with boron
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
- C23C2/022—Pretreatment of the material to be coated, e.g. for coating on selected surface areas by heating
- C23C2/0224—Two or more thermal pretreatments
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
- C23C2/024—Pretreatment of the material to be coated, e.g. for coating on selected surface areas by cleaning or etching
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/04—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor characterised by the coating material
- C23C2/06—Zinc or cadmium or alloys based thereon
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/04—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor characterised by the coating material
- C23C2/12—Aluminium or alloys based thereon
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/26—After-treatment
- C23C2/261—After-treatment in a gas atmosphere, e.g. inert or reducing atmosphere
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/26—After-treatment
- C23C2/28—Thermal after-treatment, e.g. treatment in oil bath
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/26—After-treatment
- C23C2/28—Thermal after-treatment, e.g. treatment in oil bath
- C23C2/29—Cooling or quenching
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/34—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor characterised by the shape of the material to be treated
- C23C2/36—Elongated material
- C23C2/40—Plates; Strips
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/02—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings only including layers of metallic material
- C23C28/023—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings only including layers of metallic material only coatings of metal elements only
- C23C28/025—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings only including layers of metallic material only coatings of metal elements only with at least one zinc-based layer
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/30—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer
- C23C28/32—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one pure metallic layer
- C23C28/321—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one pure metallic layer with at least one metal alloy layer
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/30—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer
- C23C28/32—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one pure metallic layer
- C23C28/322—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one pure metallic layer only coatings of metal elements only
- C23C28/3225—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one pure metallic layer only coatings of metal elements only with at least one zinc-based layer
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/30—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer
- C23C28/34—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one inorganic non-metallic material layer, e.g. metal carbide, nitride, boride, silicide layer and their mixtures, enamels, phosphates and sulphates
- C23C28/345—Coatings combining at least one metallic layer and at least one inorganic non-metallic layer including at least one inorganic non-metallic material layer, e.g. metal carbide, nitride, boride, silicide layer and their mixtures, enamels, phosphates and sulphates with at least one oxide layer
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C30/00—Coating with metallic material characterised only by the composition of the metallic material, i.e. not characterised by the coating process
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C30/00—Coating with metallic material characterised only by the composition of the metallic material, i.e. not characterised by the coating process
- C23C30/005—Coating with metallic material characterised only by the composition of the metallic material, i.e. not characterised by the coating process on hard metal substrates
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C8/00—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C8/06—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using gases
- C23C8/08—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using gases only one element being applied
- C23C8/10—Oxidising
- C23C8/16—Oxidising using oxygen-containing compounds, e.g. water, carbon dioxide
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/003—Cementite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/005—Ferrite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/008—Martensite
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12535—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.] with additional, spatially distinct nonmetal component
- Y10T428/12611—Oxide-containing component
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/1266—O, S, or organic compound in metal component
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/1266—O, S, or organic compound in metal component
- Y10T428/12667—Oxide of transition metal or Al
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12736—Al-base component
- Y10T428/1275—Next to Group VIII or IB metal-base component
- Y10T428/12757—Fe
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12785—Group IIB metal-base component
- Y10T428/12792—Zn-base component
- Y10T428/12799—Next to Fe-base component [e.g., galvanized]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12861—Group VIII or IB metal-base component
- Y10T428/12951—Fe-base component
- Y10T428/12972—Containing 0.01-1.7% carbon [i.e., steel]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/26—Web or sheet containing structurally defined element or component, the element or component having a specified physical dimension
Definitions
- the present invention relates to a molten Zn-Al-Mg-based plated steel sheet and a method for producing the same.
- Patent Document 1 by adding Si, Nb and Ti to a steel sheet, the hardness difference between a hard phase such as martensite and bainite structure and a ferrite phase is reduced, so that a high tensile strength of 780 MPa or more is obtained. And a technique for achieving both workability and workability are disclosed.
- Patent Document 2 discloses a hot-dip Zn—Al—Mg-based galvanized steel sheet having a high tensile strength of 780 MPa or more and excellent bending workability.
- Japanese Patent Publication Japanese Patent Laid-Open No. 2006-283156
- Japanese Patent Publication Japanese Patent Laid-Open No. 2014-189812
- Patent Document 1 the technique described in Patent Document 1 is not suitable for plated steel sheets. Further, according to the manufacturing method described in Patent Document 2, the amount of martensite after plating may decrease depending on the hot rolling conditions, so that the strength of 780 MPa or more may not be stably obtained. ..
- One aspect of the present invention is to realize a molten Zn-Al-Mg-based galvanized steel sheet that stably achieves both a tensile strength of 780 MPa or more and high workability.
- the molten Zn-Al-Mg-based plated steel sheet according to one aspect of the present invention has a fused Zn-Al-Mg based plated layer on the surface of the steel base material.
- the steel base material is C: 0.050 to 0.180%, Si: 0.001 to 0.50%, Mn: 1.00 to 2.80%, Ti: in mass%. It contains 0.01 to 0.10% and B: 0.005 to 0.0100%, the balance contains Fe and unavoidable impurities, and the average grain size of cementite after winding in the hot rolling process is 2 ⁇ m.
- the metal structure after the continuous hot-dip zinc plating step has a ferrite phase and a second phase having an area ratio of 15% or more and less than 45%, and the second phase is made of martensite or martensite and bainite. It is composed and has an average crystal grain size of 8 ⁇ m or less.
- the method for producing a molten Zn—Al—Mg-based plated steel sheet includes a hot rolling step, a cold rolling step, annealing and molten Zn—Al—Mg.
- the hot rolling step the average cooling rate after hot rolling is 20 ° C./sec or more and less than 80 ° C./sec, and the winding temperature is 400 ° C. or more and less than 600 ° C.
- molten Zn-Al-Mg-based galvanized steel sheet that stably achieves both a tensile strength of 780 MPa or more and high workability.
- (C) C is an element necessary for increasing the strength of steel.
- a C content of 0.050% or more is required.
- the C content is limited to 0.180% or less, and may be controlled to 0.160% or less.
- Si Si
- Si silicon
- Mn Mn manganese Mn (manganese) is effective for increasing the strength.
- a Mn content of 1.00% or more is secured in order to stably obtain a strength level of 780 MPa or more in tensile strength.
- the Mn content is set to 2.80% or less.
- Ti titanium
- Ti titanium
- S sulfur
- N nitrogen
- B which is necessary for suppressing the austenite-ferrite transformation, easily binds to N
- the addition of Ti is effective in ensuring the content of solid-solved B.
- the Ti content is 0.01% by mass or more, the content of solid-solved B necessary for suppressing the austenite-ferrite transformation is secured, and the effect of finely precipitating the precipitate appears remarkably. Further, when the Ti content is 0.1% by mass or less, the Ti content in the base steel sheet does not become excessive, and the manufacturing cost of the base steel sheet can be suppressed.
- B B (boron) suppresses austenite-ferrite transformation of steel and contributes to strengthening the transformed structure. By suppressing the austenite-ferrite transformation, it has the effect of lowering the precipitation start temperature of Ti-based carbides and the like and refining those carbides. In order to obtain the above effect sufficiently, a B content of 0.0005% or more is secured. It is more effective to set it to 0.0010% or more. However, a large amount of B is a factor that causes a decrease in workability due to the formation of boride. When B is added, it is necessary to carry out in the range of 0.0100% or less, and it may be controlled to 0.0050% or less.
- P phosphorus
- P (phosphorus) is effective in strengthening the solid solution, it is preferable to secure a P content of 0.005% or more. It may be managed to 0.010% or more. However, if the P content is excessive, segregation is likely to occur and the workability is lowered. The P content is limited to 0.050% or less.
- S sulfur
- S sulfur
- the S content is allowed up to 0.020%. However, since excessive reduction in S causes an increase in the steelmaking load, the S content may usually be 0.001% or more.
- Al Al (aluminum) has a deoxidizing action. In order to fully exert its action, it is desirable to add Al so that the Al content in the steel is 0.005% or more. However, excessive Al content causes a decrease in workability. Therefore, the Al content is limited to 0.10% or less, and may be controlled to 0.050% or less.
- Nb, V Similar to Ti, Nb (niobium) and V (vanadium) improve the uniformity of the structure by miniaturizing the structure, and improve the strength without deteriorating the workability such as bendability by strengthening the dispersion of carbide particles. Contribute to. Therefore, one or two types of Nb and V may be contained as required. In order to sufficiently obtain the above effects, it is more effective to secure a content of 0.01% or more for Nb and 0.03% or more for V. However, if a large amount of these elements is contained, the workability is deteriorated. Therefore, when one or two of these are added, the Nb content is in the range of 0.10% or less, and the V content is also in the range of 0.10% or less.
- Mo, Cr Since both Mo (molybdenum) and Cr (chromium) have an effect of improving the strength by strengthening the solid solution, one or two types of Mo and Cr may be contained as needed. In order to fully exert the above action, it is more effective to secure a content of 0.01% or more for Mo and 0.01% or more for Cr. However, if a large amount of these elements is contained, the ductility will be lowered. Therefore, when one or two of these are added, the Mo content is set to the range of 1.00% or less, and the Cr content is also set to the range of 1.00% or less.
- the steel sheet according to the present embodiment contains C, Si, Mn, Ti, and B, and may further contain each of the above-mentioned components as other components.
- a preferred embodiment further comprises one or more of P, S, and Al. In a more preferred embodiment, all of these are included.
- one or more, preferably all, of P, S, and Al are included, and Nb, V, Cr, and Examples include those further containing one or more types of Mo.
- the balance contains Fe and unavoidable impurities.
- the steel base material is applied to a DP (dual phase) steel sheet having martensite or a composite structure in which martensite and bainite are dispersed as the second phase in the main phase ferrite.
- the total area ratio of martensite dispersed in the main phase ferrite or the second phase composed of martensite and bainite is 15% or more and less than 45%. If the area ratio of the second phase is less than 15%, it becomes difficult to stably obtain a tensile strength of 780 MPa or more. On the contrary, when it becomes 45% or more, it becomes too hard and the workability deteriorates.
- the second phase is most preferably martensite only, but bainite may be partially dispersed.
- the ratio of the volume of bainite to the total volume of martensite and bainite is more preferably in the range of 0 to 5%. All of the examples of the present invention in the examples described later satisfy this condition.
- the average crystal grain size of the second phase is refined to 8 ⁇ m or less. It was found that sufficient workability was ensured and it was useful for expanding the degree of freedom in design. It is preferable that ferrite, which is the main phase, is also miniaturized, but the average crystal grain size of the second phase is particularly important for processability.
- the ferrite phase is also sufficiently refined.
- the average crystal grain size of the ferrite phase is 10 ⁇ m or less.
- the average crystal grain size of the ferrite phase is 10 ⁇ m or less.
- the above-mentioned hot-dip Zn-Al-Mg-based plated steel sheet is a general hot-dip galvanized steel sheet in which each step of hot rolling, pickling, cold rolling, annealing, and hot-dip galvanizing is performed on a steel slab in this order. It can be manufactured using the line.
- the average cooling rate is 20 ° C./sec or more and less than 80 ° C./sec
- the winding temperature is 400 ° C. or more and less than 600 ° C.
- hot rolling was performed at a finish rolling temperature of 830 to 940 ° C.
- the cold rolling ratio was set to 40 to 70%
- annealing was performed at 740 to 880 ° C.
- the average cooling rate up to at least 450 ° C. is 5 ° C./sec or more in the cooling process until the film is immersed in the plating bath.
- the finish rolling temperature in hot rolling is 830 to 940 ° C.
- the finish rolling temperature is 830 ° C. or higher, the deformation resistance of the steel sheet does not increase, and it is possible to prevent a decrease in the manufacturability of the steel sheet due to hot rolling.
- the finish rolling temperature is 940 ° C. or lower, it is possible to prevent the occurrence of scale defects on the coil surface and suppress the deterioration of the surface quality.
- the finished rolled steel sheet (hot-rolled steel sheet) is cooled to a winding temperature of 400 ° C. or higher and lower than 600 ° C. at an average cooling rate of 20 ° C./sec or more and less than 80 ° C./sec.
- the average cooling rate is 20 ° C./sec or less, or when the winding temperature is 600 ° C. or more
- the cementite of the hot-dip steel sheet structure becomes coarse, and some of the coarse cementite is not present in the reduction heating in the hot-dip galvanizing process. It remains as a dissolved carbide.
- the amount of martensite after hot-dip galvanizing is reduced, and a tensile strength of 780 MPa or more cannot be obtained.
- the average cooling rate is 80 ° C./sec or more, or when the winding temperature is less than 400 ° C.
- the hardness of the hot-rolled steel sheet increases due to the high dislocation density, and the load in the cold rolling process increases. Not only is it increased, but it also causes a decrease in workability after the hot dip galvanizing process.
- the cementite particle size after winding by hot rolling is 2 ⁇ m or less.
- the residual undissolved carbide can be suppressed in the reduction heating in the hot-dip galvanizing step, so that the amount of martensite after hot-dip galvanizing increases. Therefore, it is possible to stably produce a plated steel sheet having both strength and workability at a high level of 780 MPa or more.
- the cold rolling ratio is preferably 40 to 70%. If the cold rolling ratio is less than 40%, the structure after annealing becomes coarse and the bendability deteriorates. On the other hand, when the cold rolling rate exceeds 70%, the structure miniaturization effect of cold rolling is saturated. Further, it is not preferable to give an excessively high cold rolling rate because it increases the load in the cold rolling process.
- the plate thickness after hot rolling is adjusted according to the final target plate thickness so that the cold rolling ratio in this cold rolling step is within the above range. In some cases, after hot rolling, an intermediate cold rolling + intermediate annealing step may be inserted before the cold rolling step.
- Continuous hot dip galvanizing process In the continuous hot-dip galvanizing step, annealing and hot-dip Zn-Al-Mg plating are sequentially performed.
- the material temperature (maximum temperature reached) may be heated to 740 to 880 ° C. in a reducing atmosphere. If the material temperature does not reach 740 ° C., recrystallization is insufficient and an unrecrystallized structure tends to remain, so that it is difficult to stably obtain good processability. If the temperature exceeds 880 ° C., the crystal grains of the austenite matrix become coarse, and the miniaturization of the second phase necessary for imparting good processability becomes insufficient.
- the time for holding the material temperature in the range of 740 to 880 ° C. may be set in the range of, for example, 60 seconds or less.
- the average cooling rate up to at least 450 ° C is 5 ° C / sec or more. If the cooling rate in this temperature range is slower than this, pearlite is likely to be partially generated, and it becomes difficult to stably obtain a high intensity of 780 MPa or more. Further, from the viewpoint of miniaturization of the ferrite particle size and the second phase particle size, it is effective to set the cooling rate to 5 ° C./sec or more. Since the steel targeted in the present invention contains a predetermined Ti and, if necessary, Nb as described above, the average crystal grain size of ferrite is 10 ⁇ m or less by selecting the cooling rate after heating in this way. In addition, a fine structure having an average crystal grain size of 8 ⁇ m or less in the second phase can be obtained.
- this annealing be performed on a continuous plating line where annealing and molten Zn-Al-Mg-based plating can be performed with a single line through plate.
- the steel sheet is directly immersed in the hot-dip galvanizing bath after being cooled to the appropriate material temperature for immersion in the hot-dip galvanizing bath.
- the annealing atmosphere is a reducing atmosphere, and the steel sheet is controlled so as not to come into contact with the atmosphere until it is immersed in the plating bath.
- the plating bath composition is, for example, by mass%, Al: 3.0 to 22.0%, Mg: 0.05 to 10.0%, Ti: 0 to 0.10%, B: 0 to 0.05%. , Si: 0 to 2.0%, Fe: 0 to 2.0%, and the balance is Zn and unavoidable impurities.
- the plating layer composition of the obtained plated steel sheet substantially reflects the plating bath composition.
- the obtained plated steel sheet is brought into contact with water vapor in a closed container to blacken the plated layer.
- the brightness (L * value) of the surface of the plating layer can be reduced to 60 or less (preferably 40 or less, more preferably 35 or less).
- a steel sheet in which a black oxide of Zn is present on the surface layer of the molten Zn—Al—Mg-based plating layer and the surface brightness L * is 60 or less can be obtained. If the surface layer of the plated steel sheet has such brightness, a black plated steel sheet having excellent design can be obtained.
- the contact time with water vapor and the like are appropriately set according to the required brightness L * .
- the brightness (L * value) of the surface of the plating layer is measured using a spectroscopic color difference meter.
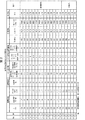
- a slab having the chemical composition shown in FIG. 1 is hot-rolled at a heating temperature of 1250 ° C., a finish rolling temperature of 880 ° C., an average cooling rate from finish rolling to winding at 15 to 70 ° C./sec, and a winding temperature of 420 to 630 ° C. Then, a hot-rolled steel sheet having a plate thickness of 1.8 to 2.8 mm was obtained.
- the hot-rolled steel sheet After pickling the hot-rolled steel sheet, it is cold-rolled at a rolling rate of 45 to 65% to obtain a plating base plate (steel base material) with a plate thickness of 1.0 mm, which is passed through a continuous hot-dip galvanizing line to hydrogen- It was annealed at various temperatures of 750 to 850 ° C. in a nitrogen mixed gas atmosphere, and cooled to about 420 ° C. at a cooling rate of 8 to 12 ° C./sec.
- a plating base plate steel base material
- a plate thickness of 1.0 mm which is passed through a continuous hot-dip galvanizing line to hydrogen- It was annealed at various temperatures of 750 to 850 ° C. in a nitrogen mixed gas atmosphere, and cooled to about 420 ° C. at a cooling rate of 8 to 12 ° C./sec.
- molten Zn-Al-Mg-based plating bath having the following bath composition, then pulled up, and the amount of plating adhered to each side is about 90 g / m 2 by the gas wiping method.
- a molten Zn-Al-Mg-based plated steel sheet was produced by adjusting to, and this was used as a test material.
- the plating bath temperature was about 410 ° C.
- the plating bath composition is as follows; By mass%, Al: 6%, Mg: 3%, Ti: 0.002%, B: 0.0005%, Si: 0.01%, Fe: 0.1%, the balance: Zn.
- each steel (example of the present invention: steels A to G, comparative example: steel a)
- CT indicates the winding temperature
- cooling rate indicates the average cooling rate from finish rolling to winding in hot rolling
- annealing temperature indicates reduction heating in a continuous hot-dip galvanizing line. Indicates the temperature.
- Tensile strength TS and total elongation T.El were determined according to JIS Z2241 using JIS No. 5 test pieces collected so that the longitudinal direction of the test pieces was perpendicular to the rolling direction of the plating base plate (steel base material).
- Metal structure The metal structures of the hot-rolled material and the plating material were observed with a scanning electron microscope in a cross section (L cross section) parallel to the rolling direction.
- the hot-rolled material was etched with Piclar's reagent and then image-analyzed in 10 fields to determine the average grain size of cementite.
- the plating materials all had a metal structure in which ferrite was the main phase and martensite or martensite and bainite were present as the second phase.
- Image analysis of 10 fields of view was performed to determine the area ratio of the second phase and the average crystal grain size (diameter equivalent to a circle).
- the cementite particle size of the hot-rolled material is 2 ⁇ m or less, and the area ratio of the second phase composed of martensite or martensite and bainite of the plating material is 15% or more and less than 45%.
- the average crystal grain size of the second phase is 8 ⁇ m or less, the tensile strength TS is 780 MPa or more, and the tensile strength TS ⁇ total elongation T.I. El was 14000 MPa ⁇ % or more, and the bendability index R / t was 1.5 or less. That is, in the example of the present invention, a plated steel sheet having both strength and workability at a high level was stably obtained.
- CT take-up temperature
- the area ratio of the second phase was less than 15%, and the tensile strength TS was 780 MPa or less. That is, a plated steel sheet satisfying the strength required in the present invention could not be obtained.
- the molten Zn-Al-Mg-based plated steel sheet according to one aspect of the present invention is a molten Zn-Al-Mg-based plated steel sheet having a molten Zn-Al-Mg-based plating layer on the surface of the steel substrate.
- B containing 0.0005 to 0.0100%, the balance containing Fe and unavoidable impurities, the average particle size of cementite after winding in the hot rolling step is 2 ⁇ m or less, and the continuous hot-dip zinc plating step.
- the later metallographic structure has a ferrite phase and a second phase having an area ratio of 15% or more and less than 45%.
- the second phase is composed of martensite or martensite and baynite, and has an average crystal grain size of 8 ⁇ m. It is as follows.
- the molten Zn—Al—Mg-based galvanized steel sheet according to one aspect of the present invention has P: 0.005 to 0.050%, S: 0.001 to 0.020%, and Al: 0.005 in mass%. It may further contain one or more of ⁇ 0.10%.
- the molten Zn—Al—Mg-based galvanized steel sheet according to one aspect of the present invention has Nb: 0 to 0.10%, V: 0 to 0.10%, Cr: 0 to 1.00%, and Cr: 0 to 1.00% in mass%. Mo: One or more of 0 to 1.00% may be further contained.
- the surface layer of the molten Zn-Al-Mg-based plating layer contains a black oxide of Zn, and the surface brightness L * is 60 or less. There may be.
- the method for producing a molten Zn-Al-Mg-based plated steel sheet according to one aspect of the present invention is continuous melting in which a hot rolling step, a cold rolling step, and annealing and molten Zn-Al-Mg-based plating are performed in this order.
- the average cooling rate after hot rolling is 20 ° C./sec or more and less than 80 ° C./sec, and the winding temperature is 400 ° C. or more and less than 600 ° C.
- the steel base material has a mass% of C: 0.050 to 0.180% and Si: 0.001 to 0. 50%, Mn: 1.00 to 2.80%, Ti: 0.01 to 0.10%, and B: 0.005 to 0.0100%, the balance containing Fe and unavoidable impurities, as described above.
- the average particle size of cementite after winding in the hot rolling step is 2 ⁇ m or less
- the metal structure after the continuous hot-dip galvanizing step has a ferrite phase and a second phase having an area ratio of 15% or more and less than 45%.
- the second phase may be composed of martensite or martensite and bainite, and the average crystal grain size may be 8 ⁇ m or less.
- the steel base material is mass%, P: 0.005 to 0.050%, S: 0.001 to 0. It may further contain one or more of 020% and Al: 0.005 to 0.10%.
- the steel base material is mass%, Nb: 0 to 0.10%, V: 0 to 0.10%, Cr. It may further contain one or more of: 0 to 1.00% and Mo: 0 to 1.00%.
- the surface layer of the molten Zn—Al—Mg-based plating layer contains a black oxide of Zn, and the surface brightness L * is high. It may be 60 or less.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Thermal Sciences (AREA)
- Physics & Mathematics (AREA)
- Inorganic Chemistry (AREA)
- Crystallography & Structural Chemistry (AREA)
- Oil, Petroleum & Natural Gas (AREA)
- Heat Treatment Of Sheet Steel (AREA)
- Coating With Molten Metal (AREA)
Abstract
La présente invention concerne une tôle d'acier plaquée qui est à la fois résistante et apte au façonnage. Dans cette tôle d'acier plaquée de Zn-Al-Mg en fusion, un matériau de base d'acier contient, en termes de % massiques, 0,050-0,180% massique de C, 0,001-0,50% massique de Si, 1,00-2,80% massiques de Mn, 0,01-0,10% massique de Ti et 0,0005-0,0100% massique de B. Le diamètre moyen des particules de cémentite après enroulement dans une étape de laminage à chaud est de 2 µm ou moins. Après une étape de placage en continu de zinc en fusion, la structure métallique présente une phase de ferrite et une deuxième phase dans un rapport de surface non inférieur à 15 % et inférieur à 45 %. La deuxième phase est constituée de martensite ou de martensite et de bainite, et présente un diamètre de grain cristallin moyen inférieur ou égal à 8 µm.
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US17/438,440 US20220154320A1 (en) | 2019-03-22 | 2020-03-18 | MOLTEN Zn-Al-Mg-PLATED STEEL SHEET AND METHOD FOR PRODUCING SAME |
| KR1020217032242A KR20210135577A (ko) | 2019-03-22 | 2020-03-18 | 용융 Zn-Al-Mg계 도금 강판 및 그 제조 방법 |
| MX2021010939A MX2021010939A (es) | 2019-03-22 | 2020-03-18 | Lamina de acero enchapada con zn-al-mg fundida y metodo para producir la misma. |
| CN202080020996.6A CN113631736A (zh) | 2019-03-22 | 2020-03-18 | 热浸镀Zn-Al-Mg系钢板及其制造方法 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019-055044 | 2019-03-22 | ||
| JP2019055044A JP7288184B2 (ja) | 2019-03-22 | 2019-03-22 | 溶融Zn-Al-Mg系めっき鋼板の製造方法 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2020196149A1 true WO2020196149A1 (fr) | 2020-10-01 |
Family
ID=72557979
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2020/011959 Ceased WO2020196149A1 (fr) | 2019-03-22 | 2020-03-18 | Tôle d'acier plaquée de zn-al-mg en fusion et son procédé de fabrication |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20220154320A1 (fr) |
| JP (1) | JP7288184B2 (fr) |
| KR (1) | KR20210135577A (fr) |
| CN (1) | CN113631736A (fr) |
| MX (1) | MX2021010939A (fr) |
| TW (1) | TW202102696A (fr) |
| WO (1) | WO2020196149A1 (fr) |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2011153361A (ja) * | 2010-01-28 | 2011-08-11 | Nisshin Steel Co Ltd | 曲げ性および耐溶融金属脆化特性に優れた高強度Zn−Al−Mg系めっき鋼板 |
| JP2014189812A (ja) * | 2013-03-26 | 2014-10-06 | Nisshin Steel Co Ltd | 溶接構造部材用高強度めっき鋼板およびその製造法 |
| CN104419867A (zh) * | 2013-09-05 | 2015-03-18 | 鞍钢股份有限公司 | 1250MPa级超高强锌铝镁镀层钢板及其生产方法 |
| JP2017145441A (ja) * | 2016-02-16 | 2017-08-24 | 日新製鋼株式会社 | 黒色表面被覆高強度鋼板およびその製造方法 |
| WO2017169561A1 (fr) * | 2016-03-31 | 2017-10-05 | Jfeスチール株式会社 | Plaque d'acier mince, plaque d'acier galvanisée, procédé de production de plaque d'acier laminée à chaud, procédé de production de plaque d'acier entièrement dure laminée à froid, procédé de production de plaque traitée thermiquement, procédé de production de plaque d'acier mince et procédé de production de plaque d'acier galvanisée |
| JP2019031728A (ja) * | 2017-08-10 | 2019-02-28 | 日新製鋼株式会社 | 建築部材用高強度Zn−Al−Mg系表面被覆鋼板およびそれを用いた建築部材 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP4500197B2 (ja) | 2005-04-01 | 2010-07-14 | 新日本製鐵株式会社 | 成形性と溶接性に優れた高強度冷延鋼板、高強度溶融亜鉛めっき鋼板及び高強度合金化溶融亜鉛めっき鋼板の製造方法 |
| JP4903915B2 (ja) * | 2010-01-26 | 2012-03-28 | 新日本製鐵株式会社 | 高強度冷延鋼板及びその製造方法 |
| JP5867444B2 (ja) * | 2013-04-15 | 2016-02-24 | Jfeスチール株式会社 | 靭性に優れた高強度熱延鋼板およびその製造方法 |
| CN103556048B (zh) * | 2013-10-24 | 2015-04-29 | 钢铁研究总院 | 一种低屈强比、高强度汽车用双相钢板的生产方法 |
| SG11201604578TA (en) * | 2013-12-19 | 2016-07-28 | Nisshin Steel Co Ltd | Steel sheet hot-dip-coated with zn-al-mg-based system having excellent workability and method for manufacturing same |
-
2019
- 2019-03-22 JP JP2019055044A patent/JP7288184B2/ja active Active
-
2020
- 2020-03-18 US US17/438,440 patent/US20220154320A1/en not_active Abandoned
- 2020-03-18 CN CN202080020996.6A patent/CN113631736A/zh active Pending
- 2020-03-18 WO PCT/JP2020/011959 patent/WO2020196149A1/fr not_active Ceased
- 2020-03-18 KR KR1020217032242A patent/KR20210135577A/ko not_active Ceased
- 2020-03-18 MX MX2021010939A patent/MX2021010939A/es unknown
- 2020-03-19 TW TW109109208A patent/TW202102696A/zh unknown
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2011153361A (ja) * | 2010-01-28 | 2011-08-11 | Nisshin Steel Co Ltd | 曲げ性および耐溶融金属脆化特性に優れた高強度Zn−Al−Mg系めっき鋼板 |
| JP2014189812A (ja) * | 2013-03-26 | 2014-10-06 | Nisshin Steel Co Ltd | 溶接構造部材用高強度めっき鋼板およびその製造法 |
| CN104419867A (zh) * | 2013-09-05 | 2015-03-18 | 鞍钢股份有限公司 | 1250MPa级超高强锌铝镁镀层钢板及其生产方法 |
| JP2017145441A (ja) * | 2016-02-16 | 2017-08-24 | 日新製鋼株式会社 | 黒色表面被覆高強度鋼板およびその製造方法 |
| WO2017169561A1 (fr) * | 2016-03-31 | 2017-10-05 | Jfeスチール株式会社 | Plaque d'acier mince, plaque d'acier galvanisée, procédé de production de plaque d'acier laminée à chaud, procédé de production de plaque d'acier entièrement dure laminée à froid, procédé de production de plaque traitée thermiquement, procédé de production de plaque d'acier mince et procédé de production de plaque d'acier galvanisée |
| JP2019031728A (ja) * | 2017-08-10 | 2019-02-28 | 日新製鋼株式会社 | 建築部材用高強度Zn−Al−Mg系表面被覆鋼板およびそれを用いた建築部材 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7288184B2 (ja) | 2023-06-07 |
| TW202102696A (zh) | 2021-01-16 |
| US20220154320A1 (en) | 2022-05-19 |
| KR20210135577A (ko) | 2021-11-15 |
| JP2020152993A (ja) | 2020-09-24 |
| CN113631736A (zh) | 2021-11-09 |
| MX2021010939A (es) | 2021-10-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6525114B1 (ja) | 高強度亜鉛めっき鋼板およびその製造方法 | |
| US7919194B2 (en) | High strength steel sheet having superior ductility | |
| JP5858199B2 (ja) | 高強度溶融亜鉛めっき鋼板及びその製造方法 | |
| JP4635525B2 (ja) | 深絞り性に優れた高強度鋼板およびその製造方法 | |
| JP5332355B2 (ja) | 高強度溶融亜鉛めっき鋼板およびその製造方法 | |
| US7780799B2 (en) | Cold-rolled steel sheet having a tensile strength of 780 MPA or more, an excellent local formability and a suppressed increase in weld hardness | |
| US6692584B2 (en) | High tensile cold-rolled steel sheet excellent in ductility and in strain aging hardening properties, and method for producing the same | |
| US11008632B2 (en) | Steel sheet, coated steel sheet, method for producing hot-rolled steel sheet, method for producing cold-rolled full hard steel sheet, method for producing heat-treated sheet, method for producing steel sheet, and method for producing coated steel sheet | |
| US10889873B2 (en) | Complex-phase steel sheet having excellent formability and method of manufacturing the same | |
| KR20110105404A (ko) | 고강도 용융 아연 도금 강판 및 그 제조 방법 | |
| EP2762581A1 (fr) | Tôle en acier laminée à chaud, et procédé de fabrication de celle-ci | |
| CN101999007A (zh) | 扩孔性和延展性的平衡极良好、疲劳耐久性也优异的高强度钢板和镀锌钢板以及这些钢板的制造方法 | |
| KR20190076307A (ko) | 가공성이 우수한 고강도 강판 및 이의 제조방법 | |
| CN102822359A (zh) | 深拉深性优良的高强度钢板的制造方法 | |
| WO2021153746A1 (fr) | Tôle d'acier laminée à chaud et procédé de production correspondant | |
| WO2017131056A1 (fr) | Tôle d'acier galvanisé à rapport d'élasticité élevé, résistance élevée, et son procédé de production | |
| JP4211520B2 (ja) | 耐時効性に優れた高強度高延性亜鉛めっき鋼板およびその製造方法 | |
| JP4407449B2 (ja) | 高強度鋼板およびその製造方法 | |
| JP5703632B2 (ja) | 温間プレス成形用素材及びパネル用部材の製造方法 | |
| JP4333352B2 (ja) | 延性および伸びフランジ性に優れる高強度冷延鋼板の製造方法 | |
| JP4500197B2 (ja) | 成形性と溶接性に優れた高強度冷延鋼板、高強度溶融亜鉛めっき鋼板及び高強度合金化溶融亜鉛めっき鋼板の製造方法 | |
| JP2007077510A (ja) | 耐時効性に優れた高強度高延性亜鉛めっき鋼板およびその製造方法 | |
| JP7288184B2 (ja) | 溶融Zn-Al-Mg系めっき鋼板の製造方法 | |
| JP5034296B2 (ja) | 歪時効硬化特性に優れた熱延鋼板およびその製造方法 | |
| KR20240090135A (ko) | 하이브리드 고강도 저합금 냉간압연 및 어닐링 강 스트립 및 그 제조방법 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 20778683 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 20217032242 Country of ref document: KR Kind code of ref document: A |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 20778683 Country of ref document: EP Kind code of ref document: A1 |