WO2023007902A1 - 鉄基軟磁性粉末、それを用いた磁性部品及び圧粉磁芯 - Google Patents
鉄基軟磁性粉末、それを用いた磁性部品及び圧粉磁芯 Download PDFInfo
- Publication number
- WO2023007902A1 WO2023007902A1 PCT/JP2022/019735 JP2022019735W WO2023007902A1 WO 2023007902 A1 WO2023007902 A1 WO 2023007902A1 JP 2022019735 W JP2022019735 W JP 2022019735W WO 2023007902 A1 WO2023007902 A1 WO 2023007902A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- iron
- soft magnetic
- magnetic powder
- based soft
- powder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C33/00—Making ferrous alloys
- C22C33/02—Making ferrous alloys by powder metallurgy
- C22C33/0257—Making ferrous alloys by powder metallurgy characterised by the range of the alloying elements
- C22C33/0264—Making ferrous alloys by powder metallurgy characterised by the range of the alloying elements the maximum content of each alloying element not exceeding 5%
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/153—Amorphous metallic alloys, e.g. glassy metals
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F1/00—Metallic powder; Treatment of metallic powder, e.g. to facilitate working or to improve properties
- B22F1/10—Metallic powder containing lubricating or binding agents; Metallic powder containing organic material
- B22F1/102—Metallic powder coated with organic material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F1/00—Metallic powder; Treatment of metallic powder, e.g. to facilitate working or to improve properties
- B22F1/16—Metallic particles coated with a non-metal
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F5/00—Manufacture of workpieces or articles from metallic powder characterised by the special shape of the product
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C33/00—Making ferrous alloys
- C22C33/02—Making ferrous alloys by powder metallurgy
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/153—Amorphous metallic alloys, e.g. glassy metals
- H01F1/15308—Amorphous metallic alloys, e.g. glassy metals based on Fe/Ni
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/153—Amorphous metallic alloys, e.g. glassy metals
- H01F1/15333—Amorphous metallic alloys, e.g. glassy metals containing nanocrystallites, e.g. obtained by annealing
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/153—Amorphous metallic alloys, e.g. glassy metals
- H01F1/15358—Making agglomerates therefrom, e.g. by pressing
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/20—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of particles, e.g. powder
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/20—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of particles, e.g. powder
- H01F1/22—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of particles, e.g. powder pressed, sintered, or bound together
- H01F1/24—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of particles, e.g. powder pressed, sintered, or bound together the particles being insulated
- H01F1/26—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of particles, e.g. powder pressed, sintered, or bound together the particles being insulated by macromolecular organic substances
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F27/00—Details of transformers or inductances, in general
- H01F27/24—Magnetic cores
- H01F27/255—Magnetic cores made from particles
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F3/00—Cores, Yokes, or armatures
- H01F3/08—Cores, Yokes, or armatures made from powder
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F41/00—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties
- H01F41/02—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties for manufacturing cores, coils, or magnets
- H01F41/0206—Manufacturing of magnetic cores by mechanical means
- H01F41/0246—Manufacturing of magnetic circuits by moulding or by pressing powder
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F1/00—Metallic powder; Treatment of metallic powder, e.g. to facilitate working or to improve properties
- B22F1/06—Metallic powder characterised by the shape of the particles
- B22F1/065—Spherical particles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F1/00—Metallic powder; Treatment of metallic powder, e.g. to facilitate working or to improve properties
- B22F1/06—Metallic powder characterised by the shape of the particles
- B22F1/068—Flake-like particles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F9/00—Making metallic powder or suspensions thereof
- B22F9/02—Making metallic powder or suspensions thereof using physical processes
- B22F9/06—Making metallic powder or suspensions thereof using physical processes starting from liquid material
- B22F9/08—Making metallic powder or suspensions thereof using physical processes starting from liquid material by casting, e.g. through sieves or in water, by atomising or spraying
- B22F9/082—Making metallic powder or suspensions thereof using physical processes starting from liquid material by casting, e.g. through sieves or in water, by atomising or spraying atomising using a fluid
- B22F2009/0824—Making metallic powder or suspensions thereof using physical processes starting from liquid material by casting, e.g. through sieves or in water, by atomising or spraying atomising using a fluid with a specific atomising fluid
- B22F2009/0828—Making metallic powder or suspensions thereof using physical processes starting from liquid material by casting, e.g. through sieves or in water, by atomising or spraying atomising using a fluid with a specific atomising fluid with water
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2201/00—Treatment under specific atmosphere
- B22F2201/02—Nitrogen
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2203/00—Controlling
- B22F2203/11—Controlling temperature, temperature profile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2301/00—Metallic composition of the powder or its coating
- B22F2301/35—Iron
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2302/00—Metal Compound, non-Metallic compound or non-metal composition of the powder or its coating
- B22F2302/45—Others, including non-metals
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2998/00—Supplementary information concerning processes or compositions relating to powder metallurgy
- B22F2998/10—Processes characterised by the sequence of their steps
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F9/00—Making metallic powder or suspensions thereof
- B22F9/002—Making metallic powder or suspensions thereof amorphous or microcrystalline
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F9/00—Making metallic powder or suspensions thereof
- B22F9/02—Making metallic powder or suspensions thereof using physical processes
- B22F9/06—Making metallic powder or suspensions thereof using physical processes starting from liquid material
- B22F9/08—Making metallic powder or suspensions thereof using physical processes starting from liquid material by casting, e.g. through sieves or in water, by atomising or spraying
- B22F9/082—Making metallic powder or suspensions thereof using physical processes starting from liquid material by casting, e.g. through sieves or in water, by atomising or spraying atomising using a fluid
Definitions
- the present invention relates to an iron-based soft magnetic powder, a magnetic part using the same, and a dust core.
- Magnetic cores used in electric motors, transformers, reactors, etc. are required to have high magnetic flux density and low core loss.
- magnetic cores formed by laminating electromagnetic steel sheets have mainly been used.
- magnetic steel sheets with insulated surfaces are used, The magnetic properties were different, and there was a problem that the magnetic properties in the direction perpendicular to the steel sheet surface were poor.
- iron core materials used for power conversion parts using inverters, such as reactor iron cores the increase in high-frequency iron loss caused by switching harmonics has become a problem, and there is a demand to reduce this. rice field.
- Dust cores are manufactured by inserting insulating-coated soft magnetic particles (iron powder) into a mold and press-molding them. Compared to molding the core, the degree of freedom in shape is high, and it is possible to form a three-dimensional magnetic circuit.
- iron-based soft magnetic particles can be used for manufacturing the dust core, the manufacturing process is short, and there is an advantage in terms of cost.
- the iron-based soft magnetic particles used in the dust core have the advantage that each particle is covered with an insulating coating material, and the magnetic properties are uniform in all directions. Suitable for circuit formation.
- eddy current loss which is the main component of high-frequency iron loss, is small compared to laminated electromagnetic steel sheets. From this point of view, recently, the development of reactors and the like using dust cores is nowadays.
- Nanocrystalline materials have traditionally attracted attention mainly in the field of thin ribbons as materials that achieve both low coercive force and high magnetic flux density. , the nanocrystalline phase is responsible for the high magnetic flux density. In order to suppress the coercive force increase due to the crystalline phase, the average diameter of the crystallites of the nanocrystalline phase is less than 50 nm. In recent years, various developments have been made in order to obtain this nanocrystalline structure in dust cores.
- Patent Document 1 discloses an alloy composition consisting of Fe, B, Si, P, C and Cu.
- the alloy composition of Patent Document 1 has a continuous ribbon shape or a powder shape.
- a powder-shaped alloy composition (soft magnetic powder) is produced, for example, by an atomizing method, and has an amorphous phase as a main phase.
- nanocrystals of Fe (bccFe) are precipitated, whereby an Fe-based nanocrystal alloy powder is obtained.
- Patent Literature 2 discloses that a powder having a maximum circularity value of a certain value or more and an average value of the circularity of particles of a certain value or more is used to improve fluidity when the powder is filled into a mold.
- JP 2010-070852 A Japanese Patent Application Laid-Open No. 2019-21906
- Patent Document 1 the magnetic properties of the Fe-based nanocrystalline alloy powder proposed in Patent Document 1 and the dust core using this Fe-based nanocrystalline alloy powder are not sufficient, and the magnetic flux density is further improved and the iron loss is reduced. Reduction is required.
- Patent document 2 only specifies the particle circularity. However, in order to obtain a soft magnetic powder having good magnetic properties, it is not enough to control the circularity to make the particles spherical, and it is difficult to stably secure sufficient soft magnetic properties. be.
- An object of the present invention is to solve the above-mentioned problems and to provide an iron-based soft magnetic powder that can produce a dust core with low iron loss.
- the gist and configuration of the present invention are as follows. [1] An iron-based soft magnetic powder, Crystallinity is 10% or less, The median value of volume-based circularity (C 50 ) is 0.85 or more, In a nitrogen atmosphere, the temperature was raised to 400°C at a heating rate of 3 °C/min, held at that temperature for 20 minutes, and then allowed to cool naturally to room temperature.
- the iron-based soft magnetic powder of [1], represented by [3] P in the composition formula is replaced with at least one element selected from C, Mn, Cr, Mo, Nb, Sn, Zr, Ta, W, Hf and V in an amount of 4.0 at% or
- [4] The iron-based soft magnetic powder according to any one of [1] to [3], wherein the content of O contained as unavoidable impurities is 0.3% by mass or less.
- [5] The iron-based soft magnetic powder according to any one of [1] to [4], wherein the surfaces of the particles constituting the iron-based soft magnetic powder have insulating coatings.
- [6] Magnetic parts using the iron-based soft magnetic powder of [5].
- an iron-based soft magnetic powder that can produce a powder magnetic core with low iron loss. More specifically, by insulating the iron-based soft magnetic powder of the present invention, it is possible to produce an insulation-coated iron-based powder having good magnetic properties (saturation magnetic flux density, coercive force). By using the base powder, it is possible to produce a dust core with low iron loss.
- An iron-based soft magnetic powder (hereinafter also referred to as "soft magnetic powder"), which is one embodiment of the present invention, has a crystallinity of 10% or less, and a median volume-based particle circularity (C 50 ) is 0.85 or more, in a nitrogen atmosphere, the temperature is raised to 400 ° C. at a heating rate of 3 ° C./min, held at this temperature for 20 minutes, and then naturally cooled to room temperature.
- the number density of Cu clusters in the powder is 1.00 ⁇ 10 3 pieces/ ⁇ m 3 or more and 1.00 ⁇ 10 6 pieces/ ⁇ m 3 or less, and the average value of the Cu concentration of Cu clusters is 30.0 at % or more.
- iron-based means containing 50% by mass or more of Fe.
- Room temperature means 0°C or higher and 40°C or lower.
- Natural cooling refers to natural cooling while being left in the air at room temperature without using any special cooling means.
- crystallinity It is assumed that the soft magnetic powder of the present invention is subjected to heat treatment after powder compaction to precipitate nanocrystals and then used as a magnetic core. Therefore, the crystallinity in the powder state is preferably as low as 10% or less. The degree of crystallinity is preferably 5% or less, and may be 0%. If the degree of crystallinity exceeds 10%, the nanocrystals are coarsened during the heat treatment process after compaction, resulting in a significant deterioration in magnetic properties.
- the degree of crystallinity can be evaluated using powder X-ray diffractometry as the ratio of the area of the crystalline peak to the sum of the area of the amorphous region and the crystalline peak in the profile obtained by X-ray diffraction. can be calculated.
- the circularity in the present invention is a value defined by the formula (1). (here, C is the degree of circularity, A is the projected area of 1 particle, the unit is m 2 , P is the particle circumference length of one particle, and the unit is m. )
- Circularity is measured as follows.
- the powder to be measured is dispersed, for example with compressed air, onto a flat surface (eg, the surface of a glass plate) and an image of each particle is taken with a microscope.
- the total number of particles in the powder to be measured shall be 1000 or more.
- the photographed image is analyzed by a computer, and the projected area and particle perimeter of each particle are measured.
- the circularity of each particle is calculated by substituting the measurement result into the above formula (1).
- the diameter of a circle having the same area as the projected area of each particle (equivalent circle diameter) is calculated, and the volume of a sphere having the same diameter as that diameter is calculated.
- the circularity and volume of each particle can be obtained, and the volume frequency at each circularity can be calculated.
- the circularity of all particles in the powder to be measured is arranged in ascending order, and the circularity of particles corresponding to 50% of the total volume of all particles is taken as the median value (C 50 ). Since the upper limit of circularity is 1 according to the definition, the median value of circularity is 1 or less. Since the average value of circularity is greatly influenced by the value of particles with high circularity, the median value of circularity (C 50 ) is used in the present invention as an indicator of the circularity of the powder as a whole.
- the soft magnetic powder of the present invention has a volume-based median circularity (C 50 ) of 0.85 or more, preferably 0.90 or more, and more preferably 0.95 or more. Within this range, the shape magnetic anisotropy of the particles is reduced, and the coercive force is sufficiently reduced.
- C 50 volume-based median circularity
- the soft magnetic powder of the present invention was heated in a nitrogen atmosphere to 400°C at a heating rate of 3°C/min, held at that temperature for 20 minutes, and then naturally cooled to room temperature. is 1.00 ⁇ 10 3 pieces/ ⁇ m 3 or more and 1.00 ⁇ 10 6 pieces/ ⁇ m 3 or less, and the average value of the Cu concentration of Cu clusters is 30 at % or more.
- the number density and Cu concentration of Cu clusters in the present invention are values measured under predetermined conditions.
- the temperature is raised to 400° C. at , the temperature is maintained for 20 minutes, and then the powder is allowed to cool naturally to room temperature.
- the spontaneously cooled powder is a powder that has not been subjected to further heat treatment after reaching room temperature by spontaneous cooling, and the Cu class measurement is performed on the powder immediately after reaching room temperature by spontaneous cooling.
- the powder may be allowed to stand at room temperature after reaching room temperature by natural cooling.
- the atom detection efficiency by the three-dimensional atom probe electric field ion microscope is assumed to be about 30%.
- the values measured by the three-dimensional atom probe field ion microscope are calculated back to the values when the detection efficiency is 30%, and the number density and Cu concentration of Cu clusters are calculated. may be used.
- Cu clusters can be analyzed by the Maximum Separation Method with parameters of 0.5 nm as the maximum spacing dmax between Cu atoms and 13 Cu atoms as the minimum index Nmin constituting the cluster.
- a sample is taken from the central part of the particles that constitute the powder to be measured, and FIB (Focused Ion Beam) processing is used to make a needle-like sample into a needle shape.
- the tip of the needle-like sample is preferably 100 nm ⁇ or less.
- the measurement volume is 8 ⁇ 10 ⁇ 24 m 3 or more and can be 1 ⁇ 10 ⁇ 20 m 3 or less.
- the ionization of the needle-shaped sample may be electrolytic evaporation by voltage load or laser-assisted field evaporation.
- the number density of Cu clusters in the present invention is 1.00 ⁇ 10 3 / ⁇ m 3 or more and 1.00 ⁇ 10 6 / ⁇ m 3 or less. If the number density of Cu clusters is less than the above lower limit, the amount of nanocrystal nuclei produced is insufficient, and a sufficient magnetic flux density cannot be obtained. In addition, if it is larger than the above upper limit, coarsening of nanocrystals of bccFe generated with clusters as nuclei is promoted, so heat treatment in a shorter time is required, and nanocrystallization after dust core formation is required. In heat treatment, it becomes difficult to ensure stable properties.
- the average Cu concentration of Cu clusters in the present invention is 30.0 atomic % or more. If the Cu concentration of the Cu clusters is less than the above lower limit, it becomes difficult to grow bccFe using the clusters as nuclei.
- the Cu concentration of Cu clusters is preferably 35.0 at % or higher, more preferably 40.0 at % or higher.
- the upper limit of Cu concentration is not particularly limited, and may be 100 at %.
- the soft magnetic powder may contain unavoidable impurities that are inevitably mixed during the manufacturing process or the like, but the above composition formula excludes unavoid
- M in the composition formula is at least one element selected from Ni and Co.
- Fe, Ni and Co are elements responsible for developing soft magnetic properties.
- a+b is preferably 79.0 at % or more.
- b is preferably 10.0 atomic % or less.
- b may be 0 atomic %. If the amount of Fe, Ni, and Co added is excessive, it becomes difficult to make the material completely amorphous during the manufacturing process, so a+b is preferably 84.5 at % or less.
- a+b is more preferably 84.0 at % or less, still more preferably 83.0 at % or less.
- Si has the effect of suppressing the generation of Fe—P-based precipitates that adversely affect magnetic properties during heat treatment after compaction.
- the Si content may be 0 atomic %, addition of 2.0 atomic % or more is preferable in order to stably obtain a nanocrystalline structure.
- excessive addition causes a decrease in the magnetic flux density of the powder after nanocrystallization, so it is preferably less than 6.0 at %.
- c is more preferably 5.0 at % or less, still more preferably 4.0 at % or less.
- B is an element responsible for stable amorphous formation. However, excessive addition causes a decrease in the magnetic flux density of the powder after nanocrystallization, so it is preferably 11.0 at % or less. d is more preferably 10 at % or less, still more preferably 9.5 at % or less. d is preferably 1 atomic % or more.
- Cu is an essential element for forming Cu clusters, and is preferably added in an amount of 0.2 at % or more.
- f is more preferably 0.3 at % or more, and more preferably 0.8 at % or less.
- P in the composition formula of the present invention can be replaced with at least one of C, Mn, Cr, Mo, Nb, Sn, Zr, Ta, W, Hf and V in an amount up to 4.0 at%. .
- P in the composition formula of the present invention can be replaced with at least one of C, Mn, Cr, Mo, Nb, Sn, Zr, Ta, W, Hf and V in an amount up to 4.0 at%. .
- O is an unavoidable impurity. Excessive inclusion of O causes a decrease in magnetic flux density and an increase in coercive force, so it is preferable to suppress the O content to 0.3% by mass or less. The O content is more preferably suppressed to 0.2% by mass or less, and may be 0% by mass.
- the soft magnetic powder of the present invention can be produced using a water atomization method or a gas atomization method in which water or gas is sprayed onto a molten metal, atomized, and cooled to solidify. Alternatively, it can be obtained by processing a powder obtained by a pulverization method or an oxide reduction method.
- the degree of crystallinity can be adjusted by controlling the water pressure, water amount, etc. during water atomization, and in the case of the gas atomization method, it can be adjusted by controlling the gas pressure, gas flow rate, etc. during gas atomization. can.
- the obtained powder may be classified by various methods and adjusted to a predetermined degree of circularity and particle size.
- the degree of circularity can be set within a predetermined range by adjusting the pressure of the gas for spraying water or gas to a low pressure.
- the circularity can be adjusted by smoothing the particle surface or classifying with a sieve to remove particles with low circularity.
- the surface of the powder obtained by a pulverization method, an oxide reduction method, or a normal high-pressure water atomization method or gas atomization method is smoothed, and/or particles with low circularity are removed by classifying with a sieve. may be removed.
- the number density and concentration of Cu clusters can be adjusted by heat-treating the powder obtained using the atomization method in an inert or reduced pressure atmosphere.
- the heat treatment may also serve as a drying treatment after dehydration.
- the heat treatment temperature is preferably 100° C. or higher and 300° C. or lower. If the temperature is within this range, a sufficient effect can be obtained, excessive generation of clusters can be suppressed, and deterioration of the magnetic properties after nanocrystallization can be avoided.
- the heat treatment time can be changed arbitrarily, but is preferably 12 hours or less in consideration of productivity.
- the iron-based soft magnetic powder of the present invention can have an apparent density of 3.70 Mg/m 3 or more, preferably 4.00 Mg/m 3 or more.
- the industrially achievable apparent density is 5.00 Mg/m 3 or less.
- the average particle diameter (D 50 ) can be 100 ⁇ m or less, preferably 20 ⁇ m or more and 40 ⁇ m or less. Apparent density can be measured by the method specified in JIS Z 2504.
- the average particle size (D 50 ) is the particle size at which the volume-based cumulative particle size distribution measured by the laser diffraction/scattering method is 50%.
- the iron-based soft magnetic powder of the present invention can be provided with an insulating coating on the surfaces of particles constituting the powder.
- the insulating coating is not particularly limited, and may be an inorganic insulating coating or an organic insulating coating. Either one of these may be used, or both may be used.
- As the inorganic insulating coating a coating containing an aluminum compound is preferable, and a coating containing aluminum phosphate is more preferable.
- the inorganic insulating coating may be a chemical conversion coating.
- As the organic insulating coating an organic resin coating is preferable. Examples of organic resins include silicone resins, phenol resins, epoxy resins, polyamide resins, and polyimide resins. These may be contained singly or two or more may be contained in an arbitrary ratio. Among them, a film containing a silicone resin is more preferable.
- the insulating coating may be a single-layer coating or a multi-layer coating consisting of two or more layers.
- the multi-layer coating may be a multi-layer coating composed of the same type of coating, or may be a multi-layer coating composed of different types of coatings.
- silicone resins examples include SH805, SH806A, SH840, SH997, SR620, SR2306, SR2309, SR2310, SR2316, DC12577, SR2400, SR2402, SR2404, SR2405, SR2406, SR2410, SR2410, manufactured by Dow Corning Toray Co., Ltd.
- the coating containing an aluminum compound may be a coating mainly composed of an aluminum compound or a coating composed of an aluminum compound.
- the coating may further contain a metal compound containing a metal other than aluminum. Examples of metals other than aluminum include Mg, Mn, Zn, Co, Ti, Sn, Ni, Fe, Zr, Sr, Y, Cu, Ca, V, and Ba. These may be used alone, or two or more may be used in an arbitrary ratio.
- metal compounds containing metals other than aluminum include phosphates, carbonates, nitrates, acetates, and hydroxides. These may be used alone, or two or more may be used in an arbitrary ratio.
- the metal compound is preferably soluble in a solvent such as water, and more preferably a water-soluble metal salt.
- the amount of the insulating coating is not particularly limited, it is preferably 0.1% by mass or more and 5% by mass or less with respect to the iron-based soft magnetic powder.
- the iron-based soft magnetic powder of the present invention may contain a substance different from the insulating coating in at least one of the insulating coating, under the insulating coating, and on the insulating coating.
- substances include surfactants for improving wettability, binders for binding between particles, additives for pH control, and the like. It is preferable that the total amount of the above substances in the entire insulating coating be 10% by mass or less.
- the method for forming the insulating coating is not particularly limited, it is preferably formed by wet processing.
- the wet treatment for example, there is a method of mixing an insulation coating forming treatment liquid and soft magnetic powder.
- the mixing method is not particularly limited, but for example, a method of stirring and mixing the soft magnetic powder and the treatment solution in a tank such as an attritor or a Henschel mixer, or a method of making the soft magnetic powder into a fluid state by a rolling fluid type coating device or the like.
- a method of supplying and mixing treatment solutions is preferred.
- the solution may be supplied to the soft magnetic powder in its entirety before or immediately after the start of mixing, or may be supplied in several portions during mixing.
- the treatment liquid may be supplied continuously during mixing using a droplet supply device, spray, or the like.
- a dust core which is another embodiment of the present invention, is a dust core using the iron-based soft magnetic powder.
- a method for manufacturing the dust core is not particularly limited, and any method can be used.
- a powder magnetic core can be obtained by charging the iron-based soft magnetic powder of the present invention into a mold and subjecting it to pressure molding so as to obtain desired dimensions and shape.
- the iron-based soft magnetic powder preferably has an insulating coating.
- Pressure molding is not particularly limited, and any method can be used, and examples thereof include cold molding, mold lubrication molding, and the like.
- the molding pressure can be appropriately determined according to the application, but if the molding pressure is increased, the green density increases and the magnetic properties are improved, so it is preferably 490 MPa or more, more preferably 686 MPa or more. .
- a lubricant can be used in pressure molding.
- the lubricant may be applied to the mold wall surface or added to the iron-based soft magnetic powder.
- a lubricant By using a lubricant, it is possible to reduce the friction between the mold and the powder during pressure molding, further suppressing the reduction in the density of the molded product, and reduce the friction when extracting from the mold. can also be reduced, and cracking of the compact (powder magnetic core) during removal can be prevented.
- Lubricants are not particularly limited, and include metallic soaps such as lithium stearate, zinc stearate and calcium stearate, and waxes such as fatty acid amides.
- a heat treatment may be applied to the obtained dust core.
- the heat treatment conditions can be appropriately determined according to the appropriate nano-crystallization temperature of the powder, but in general, the heat treatment is preferably performed at 200° C. or higher and 700° C. or lower for a time period of about 5 minutes or longer and 300 minutes or shorter.
- the heat treatment can be performed in any atmosphere such as air, inert atmosphere, reducing atmosphere, and vacuum.
- the heating rate is preferably 10°C/min or less, more preferably 5°C. / minute or less. From the viewpoint of productivity, the heating rate is preferably 1° C./min or more, more preferably 2° C./min or more.
- the iron-based soft magnetic powder of the present invention is particularly preferable as a starting material for manufacturing magnetic parts such as transformers, inductors, and magnetic cores of motors.
- the Morphologi G3 is a device that has a function of imaging particles with a microscope and analyzing the obtained image.
- the dried iron-based soft magnetic powder was dispersed on glass with air of 500 kPa so that the shape of individual particles could be distinguished.
- the powder dispersed on the glass was observed with a microscope attached to Morphologi G3, and the magnification was automatically adjusted so that the number of particles included in the field of view was 5,000.
- image analysis was performed on 5000 particles contained in the field of view, and the circularity ⁇ of each particle was automatically calculated.
- the median circularity (C 50 ) was obtained when the circularities of the obtained individual particles were arranged in ascending order.
- the target iron-based soft magnetic powder was heated to 400° C. at 3° C./min in a nitrogen atmosphere and held at 400° C. for 20 minutes in a nitrogen atmosphere. and then naturally cooled to room temperature.
- a needle-shaped sample was prepared by the method described above, and Cu clusters were evaluated by a three-dimensional atom probe electric field ion microscope (3DAP) by the method described above.
- 3DAP three-dimensional atom probe electric field ion microscope
- the atom detection efficiency of 3DAP was set to about 30%.
- Two needle-like samples were prepared, one sample was ionized by electric field evaporation by voltage load, and the other was ionized by laser-assisted electric field evaporation and measured. The number density and Cu concentration are their average values.
- the insulation coating solution is a silicone resin (SR2400 manufactured by Dow Corning Toray Co., Ltd.) with a resin content of 60% by mass, further diluted with xylene. It was coated so as to be After mixing, the mixture was allowed to stand in the air at room temperature for 10 hours for drying. After drying, heat treatment was performed at 150° C. for 60 minutes to harden the resin.
- the insulating-coated iron-based soft magnetic powder was filled in a mold coated with lithium stearate and pressure-molded to form a dust core (outer diameter: 38 mm, inner diameter: 25 mm, height: 6 mm).
- the molding pressure was 1470 MPa, and molding was performed in one step.
- the temperature was raised from room temperature at a rate of 3°C/min in a furnace under an N2 atmosphere, and then held at 400°C for 20 minutes. After the heat treatment, the sample was removed from the furnace in an N2 atmosphere and air-cooled to room temperature.
- the above test piece was wound (100 turns on the primary side, 20 turns on the secondary side), and the iron loss (0.1 T, 20 kHz) was measured using a high-frequency iron loss measuring instrument (manufactured by Metron Giken Co., Ltd.).
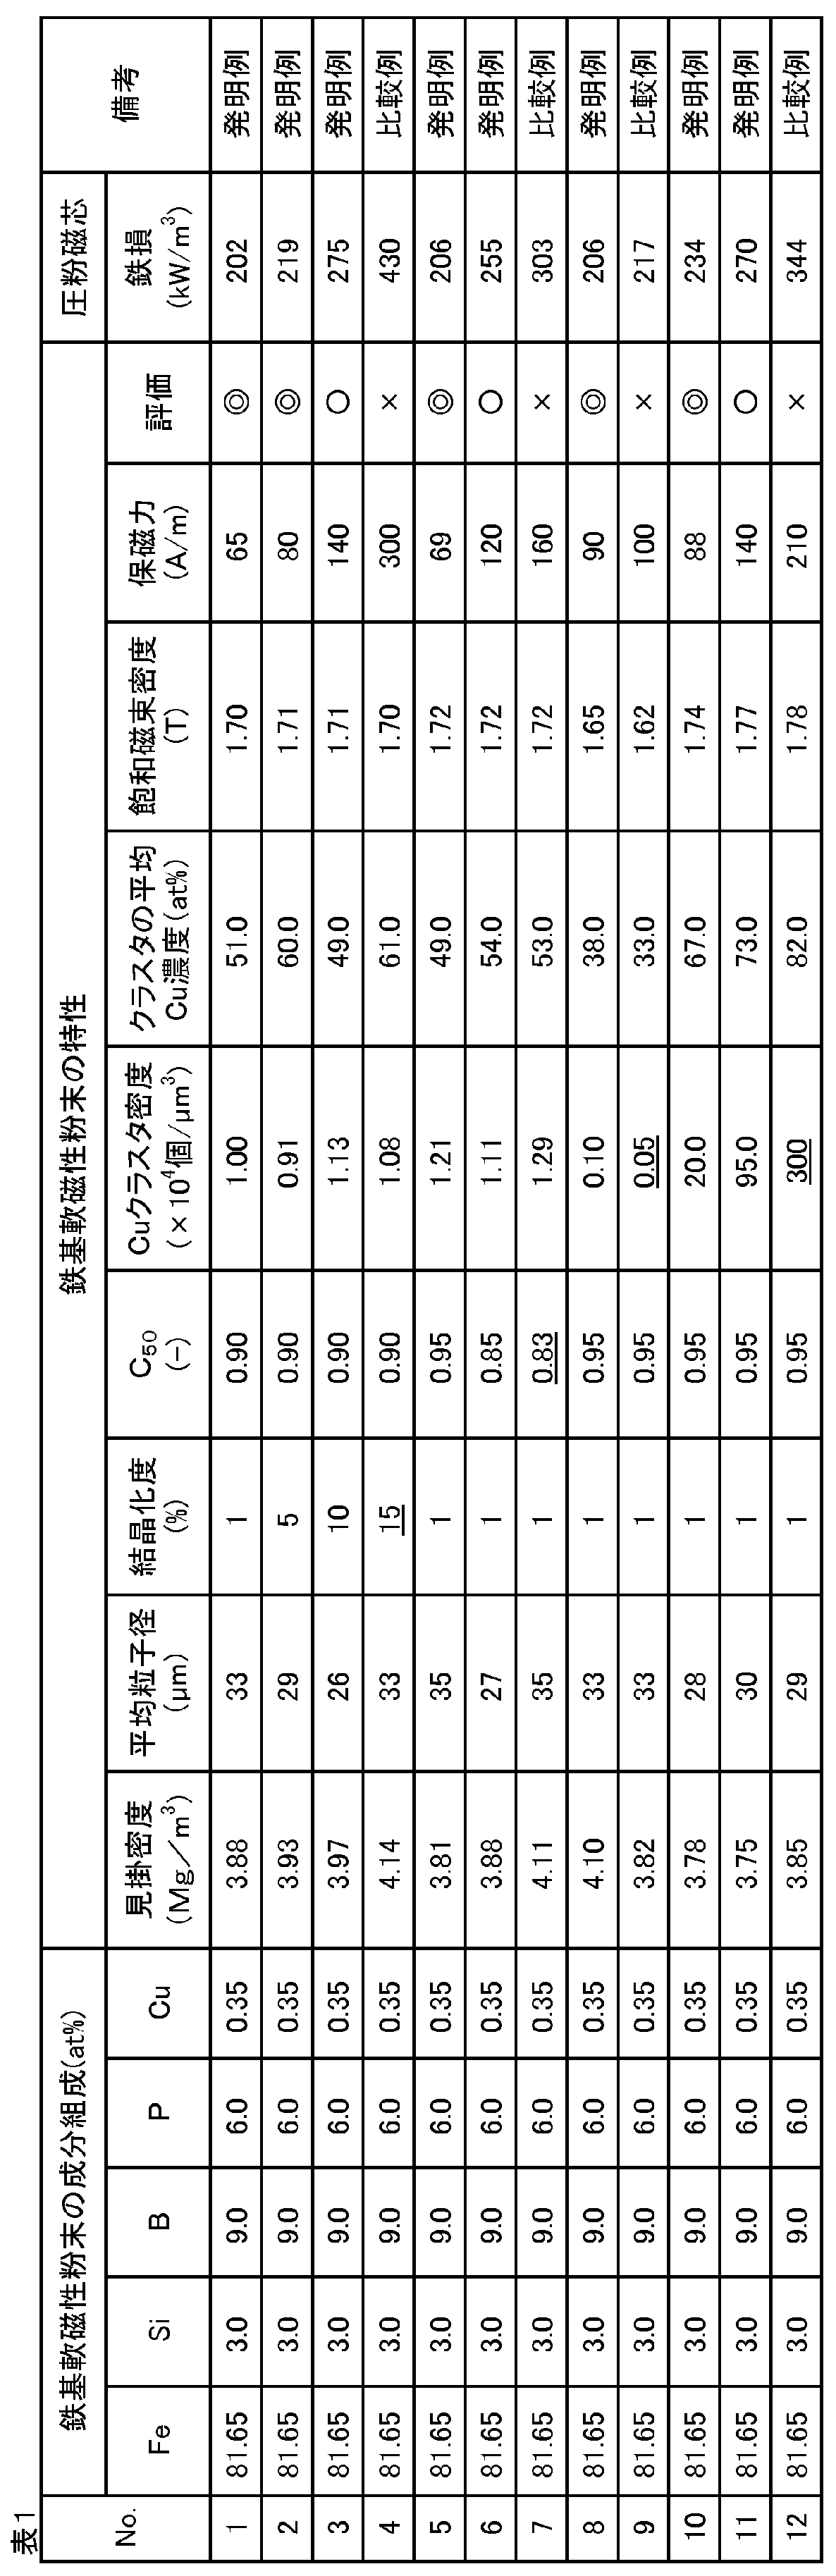
- Example 1 Molten steel having the chemical composition shown in Table 1 was rapidly solidified by a water atomization method to produce an iron-based soft magnetic powder.
- No. 5 is in descending order of water pressure.
- No. 6 and no. 7 No. 5 has the lowest water pressure, and No. 7 has the highest water pressure).
- No. 6 and no. 7 No. 5 is the slowest and No. 7 is the fastest).
- No. 8 to 12 are No. Water atomization was performed under the same conditions as in 1.
- the drying treatment is No. For Nos. 1 to 7, the furnace temperature was set to 180° C., and the treatment was carried out for 6 hours in an air atmosphere and further for 6 hours under a reduced pressure of 10 Pa relative to the atmospheric pressure.
- No. No. 8 at 120° C. for 6 hours; No. 9 at 80° C. for 6 hours; 10 at 220° C. for 6 hours; 11 at 290° C. for 6 hours; 12 was 360° C. for 6 hours.
- Table 1 shows the measurement results of the properties of the obtained soft magnetic powder. Acceptance judgment of the soft magnetic powder is as follows. Magnetic flux density of 1.65 T or more and coercive force of 100 A/m or less ⁇ A magnetic flux density of 1.65 T or more and a coercive force of more than 100 A/m to 150 A/m or less: ⁇ A magnetic flux density of less than 1.65 T and/or a coercive force of more than 150 A/m: ⁇ " ⁇ " and " ⁇ " are acceptable, and " ⁇ " is unacceptable.
- the invention examples corresponding to the iron-based soft magnetic powder of the present invention were judged to be good or bad, and had excellent magnetic properties.
- the dust cores produced using the iron-based soft magnetic powders of the invention examples all had iron losses below 300 kW/m 3 and had excellent magnetic properties.
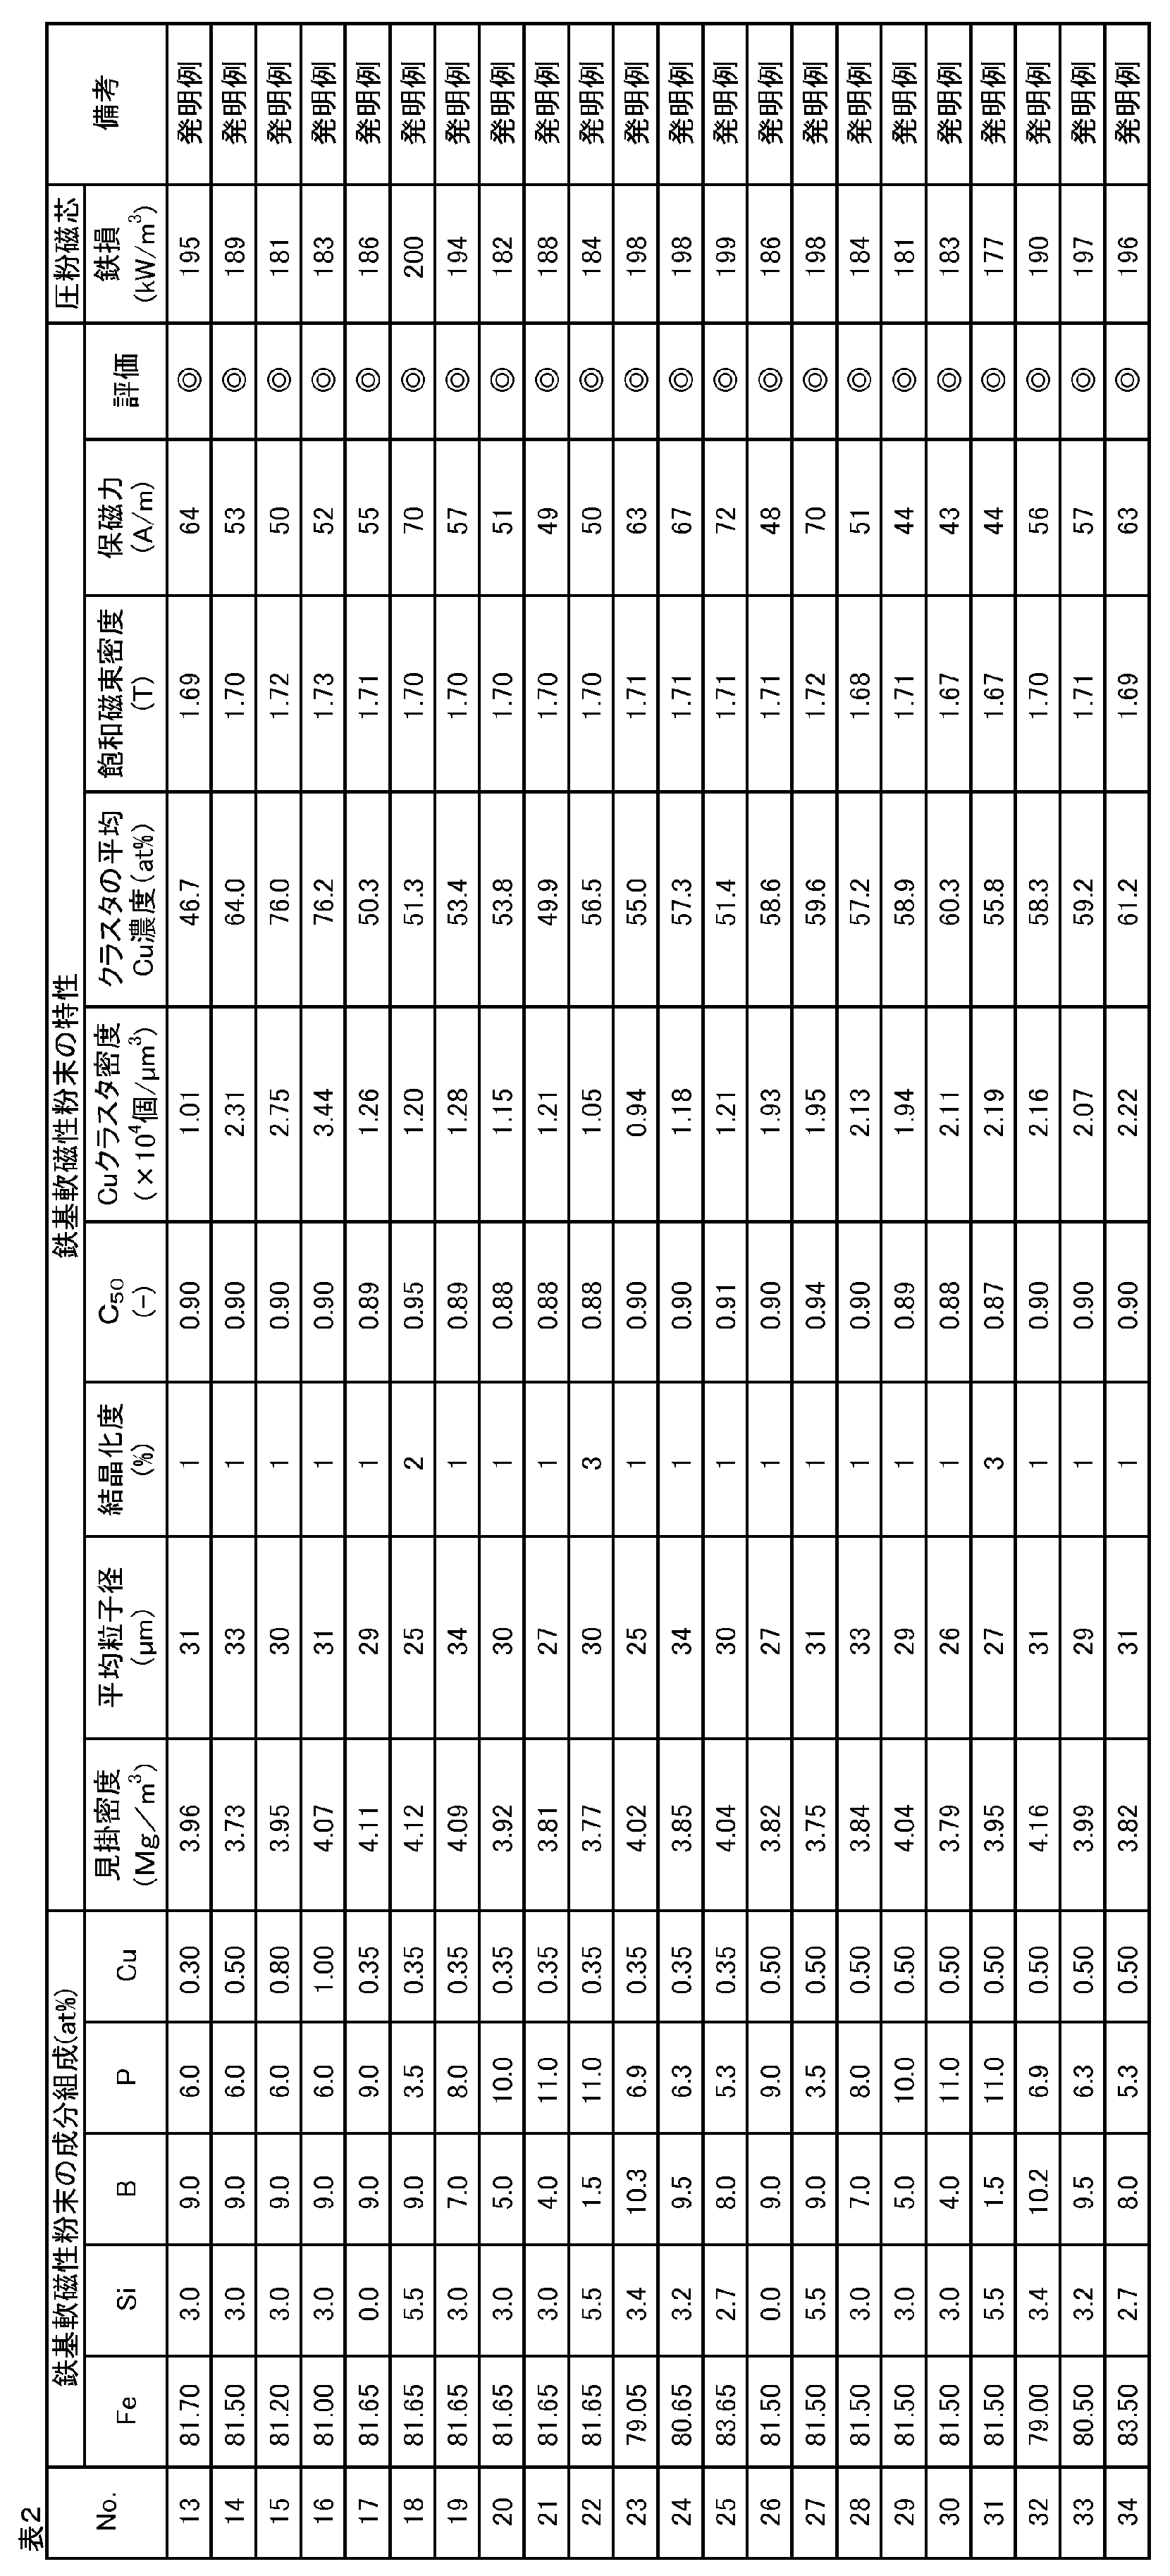
- Example 2 In order to examine the effects of the amounts of Si, B, P, and Cu added, an iron-based soft magnetic powder having the component composition shown in Table 2 was produced. The manufacturing method was the same as No. 1 of Example 1, except that the chemical composition of the molten steel used was changed. Same as 1.
- Nos. 13 to 34 are invention examples that satisfy the predetermined composition formula, but all the pass/fail judgments are " ⁇ ", and the iron loss of the dust core is all 200 kW / m 3 or less, and has excellent magnetic properties.
- Table 2 Nos. 13 to 34 are invention examples that satisfy the predetermined composition formula, but all the pass/fail judgments are " ⁇ ", and the iron loss of the dust core is all 200 kW / m 3 or less, and has excellent magnetic properties.
- Example 3 In order to examine the effect of substituting a portion of Fe with Ni and Co, iron-based soft magnetic powders having the compositions shown in Table 3 were produced. The manufacturing method was the same as No. 1 of Example 1, except that the chemical composition of the molten steel used was changed. Same as 1.
- Example 4 In order to examine the effect of substituting a portion of P with Mn, Cr, Mo, Nb, Sn, Zr, Tr, W, Hf, and V, powders having the composition shown in Table 4 were prepared. The manufacturing method was the same as No. 1 of Example 1, except that the chemical composition of the molten steel used was changed. Same as 1.
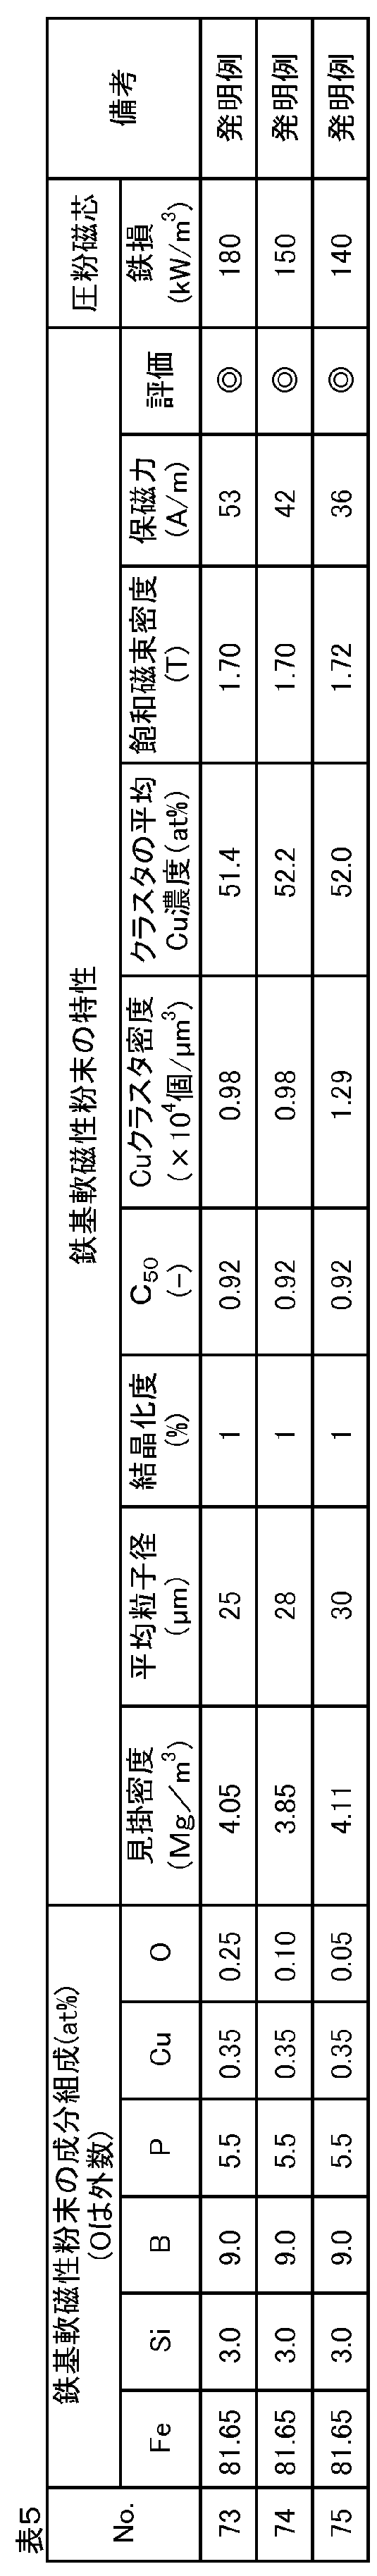
- Example 5 In order to examine the effect of the O content contained as an unavoidable impurity in the soft magnetic powder, No. Powders having the compositions shown in 73-75 were prepared. The manufacturing method was the same as No. 1 of Example 1, except that the chemical composition of the molten steel used was changed. Similar to 1, but the difference in O content is due to the adjustment of the atmospheric oxygen concentration during spraying.
- 73 to 75 are invention examples in which the content of O, which is an unavoidable impurity, is suppressed to 0.3% by mass or less.
- the iron loss of all of them was 200 kW/m 3 or less, and they had excellent magnetic properties.
Landscapes
- Engineering & Computer Science (AREA)
- Power Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Dispersion Chemistry (AREA)
- Physics & Mathematics (AREA)
- Electromagnetism (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Manufacturing & Machinery (AREA)
- Spectroscopy & Molecular Physics (AREA)
- Inorganic Chemistry (AREA)
- Crystallography & Structural Chemistry (AREA)
- Powder Metallurgy (AREA)
- Soft Magnetic Materials (AREA)
- Manufacture Of Metal Powder And Suspensions Thereof (AREA)
Abstract
Description
特許文献2には、粒子の円形度の最大値が一定値以上かつ平均値が一定値以上である粉末を使用し、粉末を金型へ充填する際の流動性を向上させることが開示されている。
特許文献2で規定されているのは粒子円形度のみである。しかしながら、良好な磁気特性を有する軟磁性粉末を得るには円形度を制御して粒子形状を球状にするのみでは不十分であって、十分な軟磁気特性を安定して確保するのが困難である。
[1]鉄基軟磁性粉末であって、
結晶化度が10%以下であり、
体積基準の円形度の中央値(C50)が0.85以上であり、
窒素雰囲気中、昇温速度3℃/分で400℃まで昇温し、該温度で20分間保持し、次いで室温まで自然放冷した粉末中のCuクラスタの数密度が1.00×103個/μm3以上1.00×106個/μm3以下であり、かつCuクラスタのCu濃度の平均値が30.0at%以上である、鉄基軟磁性粉末。
[2]不可避的不純物を除く成分組成が、組成式:FeaMbSicBdPeCuf
(式中、
79.0at%≦a+b≦84.5at%
0at%≦b≦10.0at%
0at%≦c<6.0at%
0at%<d≦11.0at%
3.0at%<e≦11.0at%
0.2at%≦f≦1.0at%、かつ
a+b+c+d+e+f=100at%であり、
Mは、Ni及びCoから選ばれる少なくとも1種の元素である)
で示される、[1]の鉄基軟磁性粉末。
[3]前記組成式におけるPが、4.0at%以下の量で、C、Mn、Cr、Mo、Nb、Sn、Zr、Ta、W、Hf及びVから選ばれる少なくとも1種の元素で置換されている、[2]の鉄基軟磁性粉末。
[4]前記不可避的不純物として含まれるO含有量が0.3質量%以下である、[1]~[3]のいずれかの鉄基軟磁性粉末。
[5]前記鉄基軟磁性粉末を構成する粒子の表面に絶縁被覆を有する、[1]~[4]のいずれかの鉄基軟磁性粉末。
[6][5]の鉄基軟磁性粉末を用いてなる磁性部品。
[7][5]の鉄基軟磁性粉末を用いてなる圧粉磁芯。
本発明の一実施形態である鉄基軟磁性粉末(以下、「軟磁性粉末」ともいう。)は、結晶化度が10%以下であり、体積基準の粒子円形度の中央値(C50)が0.85以上であり、窒素雰囲気中、昇温速度3℃/分で400℃まで昇温し、該温度で20分間保持し、次いで室温まで自然放冷した粉末中のCuクラスタの数密度が1.00×103個/μm3以上1.00×106個/μm3以下であり、かつCuクラスタのCu濃度の平均値が30.0at%以上である。
ここで、「鉄基」とは、50質量%以上のFeを含むことをいう。「室温」は、0℃以上40℃以下をいう。「自然放冷」とは、特別の冷却手段を使用することなく、室温の大気中に放置したまま自然冷却させることをいう。
本発明の軟磁性粉末は、圧粉成形後に熱処理を施し、ナノ結晶を析出させてから磁芯として用いることを想定している。そのため、粉末の状態での結晶化度は低いほうが望ましく、10%以下とする。結晶化度は、好ましくは5%以下であり、0%であってもよい。結晶化度が10%超であると、圧粉成形後の熱処理過程でのナノ結晶粗大化が進み、磁気特性が大幅に低下する。
本発明における円形度は、(1)式で定義される値とする。

Cは、円形度であり、
Aは、1粒子の投影面積であって、単位はm2であり、
Pは、1粒子の粒子周囲長さであって、単位はmである。)
測定対象とする粉末を、例えば圧縮空気で、平坦な表面(例えば、ガラス板の表面)上に分散させて、各粒子の画像を顕微鏡で撮影する。測定対象の粉末における全粒子数は1000個以上とする。
撮影画像をコンピュータで解析し、各粒子の投影面積と粒子周囲長さを測定する。測定結果を上記(1)式に代入して、各粒子の円形度を算出する。
各粒子の投影面積と同じ面積を持つ円の直径(円相当径)を算出し、その直径と同じ直径を有する球の体積を算出する。これにより、各粒子の円形度と体積が得られ、各円形度における体積頻度を算出することができる。
本発明の軟磁性粉末は、窒素雰囲気中、昇温速度3℃/分で400℃まで昇温し、該温度で20分間保持し、次いで室温まで自然放冷した粉末中のCuクラスタの数密度が1.00×103個/μm3以上1.00×106個/μm3以下であり、かつCuクラスタのCu濃度の平均値が30at%以上である。
また、CuクラスタのCu濃度は、以下の式で算出した数値である。
Cu濃度(at%)=クラスタ領域内のCu原子数/クラスタ領域の全原子数×100
Cuクラスタの解析は、Maximum Separation Methodにより、Cu原子間の最大間隔dmaxとして0.5nm、クラスタを構成する最低限指数NminとしてCu原子13個をパラメータとして行うことができる。
3次元アトムプローブ電界イオン顕微鏡の測定には、測定対象の粉末を構成する粒子中央部から試料を採取し、FIB(Focused Ion Beam)加工により、針状にした針状試料を使用することができる。針状試料の先端は、100nmφ以下とすることが好ましい。測定体積は、8×10-24m3以上であり、1×10-20m3以下とすることができる。
針状試料のイオン化は、電圧負荷による電解蒸発でも、レーザーアシストによる電界蒸発でもよい。
本発明の鉄基軟磁性粉末は、不可避的不純物を除く成分組成が、
組成式:FeaMbSicBdPeCuf
(式中、
79.0at%≦a+b≦84.5at%、
0at%≦b≦10.0at%、
0at%≦c<6.0at%、
0at%<d≦11.0at%、
3.0at%<e≦11.0at%、
0.2at%≦f≦1.0at%、
a+b+c+d+e+f=100at%であり、
Mは、Ni及びCoから選ばれる少なくとも1種の元素である)
であることが好ましい。このような組成とすることにより、粉末の結晶化度を10%以下に抑えることができ、熱処理後によって、bccFeのナノ結晶を析出させて磁性特性を一層改善することができる。
軟磁性粉末には、製造工程等から不可避的に混入される不可避的不純物が含まれ得るが、上記組成式は、不可避的不純物を除いたものである。
組成式におけるMは、Ni及びCoから選ばれる少なくとも1種の元素である。Fe、Ni及びCoは軟磁気特性の発現を担う元素である。粉末の磁束密度を高いレベルに維持するために、a+bは79.0at%以上とするのが好ましい。
Ni及びCoの過度の添加は飽和磁束密度の低下や原料コストの増加を招くため、bは10.0at%以下とするのが好ましい。bは0at%であってもよい。
Fe、Ni、Coの添加量が過剰な場合、製造過程で完全な非晶質とするのが難しくなるため、a+bは84.5at%以下とするのが好ましい。
a+bは、より好ましくは84.0at%以下であり、さらに好ましくは83.0at%以下である。
Siは、圧粉成形後の熱処理中に、磁気特性に悪影響を及ぼすFe-P系析出物の発生を抑制する効果がある。Si含有量は0at%であってもよいが、安定してナノ結晶組織を得るためには、2.0at%以上の添加が好ましい。一方、過度の添加はナノ結晶化後の粉末の磁束密度低下を招くため、6.0at%未満とするのが好ましい。cは、より好ましくは5.0at%以下であり、さらに好ましくは4.0at%以下である。
Bは、安定した非晶質の形成を担う元素である。ただし、過度の添加は、ナノ結晶化後の粉末の磁束密度低下を招くため、11.0at%以下とするのが好ましい。dは、より好ましくは10at%以下であり、さらに好ましくは9.5at%以下である。dは、1at%以上であることが好ましい。
Pを添加することで、さらに非晶質が形成され易くなるため、3.0at%超で添加することが好ましい。Pは粉末の保磁力を低減する効果もある。一方、過度の添加は成形後のナノ結晶化を目的とする熱処理の最中に保磁力を大幅に増加させるFe-P系析出物の形成を容易にし、ナノ結晶化後の粉末の磁束密度低下を招くため、11.0at%以下とするのが好ましい。eは、より好ましくは10.0at%以下であり、さらに好ましくは9.0at%以下である。
CuはCuクラスタを生成するのに必須の元素であり、0.2at%以上で添加することが好ましい。一方、過度の添加は、Cuクラスタが過多となる状況を生み出し、ナノ結晶化後の磁気特性を劣化させるため、1.0at%以下とすることが好ましい。fは、より好ましくは0.3at%以上であり、また、より好ましくは0.8at%以下である。
本発明の組成式におけるPは、4.0at%以下までの量で、C、Mn、Cr、Mo、Nb、Sn、Zr、Ta、W、Hf及びVの少なくとも1種で置換することができる。Pの一部をこれらの元素で置換することで、サイズの大きく異なる原子が混入し、非晶質が形成され易くなる。また、非晶質組織中の元素分布の均質化にも寄与するため、保磁力を低下させることができる。置換する場合、好ましくは0.3at%以上であり、より好ましくは1.0at%以上である。
不可避的不純物としてOが挙げられるが、Oが過度に混入すると磁束密度の低下や保磁力の増加を招くため、O含有量を0.3質量%以下に抑制することが好ましい。O含有量は、0.2質量%以下に抑制することがより好ましく、0質量%であってもよい。
本発明の軟磁性粉末は、金属溶湯に水やガスを吹き付け、噴霧状にして冷却凝固させる水アトマイズ法やガスアトマイズ法を用いて製造することができる。あるいは、粉砕法や酸化物還元法で得られた粉末を加工することによって得ることもできる。
見掛密度は、JIS Z 2504に規定された方法で測定することができる。
平均粒子径(D50)は、レーザー回折・散乱法で測定した体積基準積算粒度分布が50%となる粒径である。
本発明の鉄基軟磁性粉末は、該粉末を構成する粒子の表面に絶縁被覆を備えることができる。
無機絶縁被覆としては、アルミニウム化合物を含有する被膜が好ましく、リン酸アルミニウムを含有する被膜がより好ましい。無機絶縁被覆は、化成皮膜であってもよい。
有機絶縁被覆としては、有機樹脂被膜が好ましい。有機樹脂としては、例えば、シリコーン樹脂、フェノール樹脂、エポキシ樹脂、ポリアミド樹脂、ポリイミド樹脂などが挙げられる。これらを単独で含んでいても、2種以上を任意の比率で含んでいてもよい。中でも、シリコーン樹脂を含有する被膜がより好ましい。
絶縁被覆は、1層の被膜であっても、2層以上からなる多層被膜であってもよい。多層被膜は、同種の被膜からなる多層被膜であってもよく、異なる種類の被膜からなる多層被膜であってもよい。
アルミニウム化合物を含有する被覆は、アルミニウム化合物を主体とする被膜であってよく、アルミニウム化合物からなる被膜であってもよい。被膜は、さらにアルミニウム以外の金属を含む金属化合物を含有してもよい。アルミニウム以外の金属としては、例えば、Mg、Mn、Zn、Co、Ti、Sn、Ni、Fe、Zr、Sr、Y、Cu、Ca、V、Baなどが挙げられる。これらは単独で用いても、2種以上を任意の比率で用いてもよい。アルミニウム以外の金属を含む金属化合物としては、例えば、リン酸塩、炭酸塩、硝酸塩、酢酸塩、水酸化物などが挙げられる。これらは単独で用いても、2種以上を任意の比率で用いてもよい。金属化合物は、水などの溶媒に可溶であることが好ましく、水溶性金属塩であることがより好ましい。
混合方法は、特に限定されないが、例えば、アトライター又はヘンシェルミキサーなどの槽内で軟磁性粉末と処理溶液とを撹拌混合する方法や、転動流動型被覆装置などにより軟磁性粉末を流動状態として処理溶液を供給して混合する方法などが好ましい。
軟磁性粉末への溶液の供給は、混合開始前又は開始直後に全量を供給してもよく、混合中に数回に分けて供給してもよい。あるいは、液滴供給装置、スプレーなどを用いて、混合中に継続して処理液を供給してもよい。
本発明の他の実施形態である圧粉磁芯は、上記鉄基軟磁性粉末を用いてなる圧粉磁芯である。
圧粉磁芯の製造方法は、特に限定されず、任意の方法を用いることができる。例えば、本発明の鉄基軟磁性粉末を金型に装入し、所望の寸法及び形状となるように加圧成形することによって圧粉磁芯を得ることができる。鉄基軟磁性粉末は絶縁被膜を備えたものであることが好ましい。
成形圧力は、用途に応じて適宜決定することができるが、成形圧力を増加すれば、圧粉密度が高くなり、磁気特性が向上する点から、490MPa以上が好ましく、より好ましくは686MPa以上である。
潤滑剤は、特に限定されず、ステアリン酸リチウム、ステアリン酸亜鉛、ステアリン酸カルシウム等の金属石鹸、脂肪酸アミドなどのワックスが挙げられる。
本発明の鉄基軟磁性粉末を出発原料として用いることにより、鉄損の低い圧粉磁芯を製造することができる。本発明の鉄基軟磁性粉末は、特にトランス、インダクタ、モータの磁芯等の磁性部品等を製造する際の出発原料として好ましい。
実施例における鉄基軟磁性粉末の評価は、以下のようにして行った。
対象となる鉄基軟磁性粉末を乾燥した後、粒子画像イメージング分析装置(スペクトリス株式会社製 モフォロギG3)に装入した。モフォロギG3は、顕微鏡により粒子を撮像し、得られた画像を解析する機能を有する装置である。
乾燥させた鉄基軟磁性粉末を、個々の粒子の形状が判別可能となるように、500kPaの空気によりガラス上に分散させた。次いで、ガラス上に分散させた粉末をモフォロギG3付属の顕微鏡で観察し、視野に含まれる粒子の個数が5000個になるよう自動で倍率を調整した。その後、視野内に含まれる5000個の粒子について画像解析を行い、自動的に各粒子の円形度φを算出した。得られた個々の粒子の円形度を昇順に並べた際の、円形度の中央値(C50)を求めた。
鉄基軟磁性粉末の結晶化度の評価は、先に述べた粉末X線回折を用いる方法によって実施した。
対象の鉄基軟磁性粉末を、窒素雰囲気中で、3℃/分で400℃に昇温し、400℃で20分間、窒素雰囲気中で保持し、次いで室温まで自然冷却した。冷却後の鉄基軟磁性粉末について、先に述べた方法で、針状試料を作成し、先に述べた方法で、3次元アトムプローブ電界イオン顕微鏡(3DAP)によるCuクラスタの評価を実施した。
3DAPの原子の検出効率は30%程度とした。針状試料は2個用意し、1個は、電圧負荷による電界蒸発でイオン化し、もう1個は、レーザーアシストによる電界蒸発でイオン化し、測定を行った。数密度及びCu濃度は、これらの平均値である。
上記(3)の熱処理後の鉄基軟磁性粉末について磁気特性を評価した。振動試料型磁力計(VSM:Vibrating Sample Magnetometer)を使用して飽和磁気モーメントを測定し、保磁力と飽和磁束密度測定を算出した。最大磁場は1300kA/mとした。
実施例で得られた鉄基軟磁性粉末((3)の熱処理をしていないもの)に絶縁被覆用溶液を添加し、混合することにより絶縁被覆を施した。絶縁被覆用溶液は、樹脂分60質量%のシリコーン樹脂(東レ・ダウコーニング株式会社製 SR2400)をさらにキシレンにより希釈したものであり、この溶液を用いて鉄基軟磁性粉末に対する樹脂が3質量%となるように被覆した。混合後、乾燥のため室温の大気中で10時間静置した。乾燥後、樹脂硬化のため150℃で60分間の熱処理を行った。次に、絶縁被覆した鉄基軟磁性粉末を、ステアリン酸リチウムを塗布した金型に充填し、加圧成形して圧粉磁芯(外径38mm、内径25mm、高さ6mm)とした。成形圧力は1470MPaとし、1回で成形した。成形体の強度向上のためN2雰囲気下の炉で室温から3℃/分で昇温後に400℃で20分間保持した。熱処理後はN2雰囲気下で炉から取り出してから室温まで空冷し、得られた試料を圧粉磁芯の試験片とした。
表1に示す成分組成の溶鋼を水アトマイズ法により急冷凝固させて、鉄基軟磁性粉末を作製した。表1のNo.1~7は、水圧や溶鋼の注入速度を適宜調整することにより結晶化度と円形度を調整した。具体的には、No.1~4では、水アトマイズ時の水圧を変化させており、水圧が高い順にNo.1、No.2、No.3及びNo.4であり(No.1がもっとも水圧が高く、No.4がもっとも水圧が小さい。)、水圧の小さいもの程、結晶化度が高い。No.5~7は、水アトマイズ時の噴霧水の水圧及び溶鋼の注入速度を変化させており、水圧が小さい順にNo.5、No.6及びNo.7であり(No.5がもっとも水圧が低く、No.7がもっとも水圧が高い)、溶鋼注入速度が小さい順にNo.5、No.6及びNo.7である(No.5がもっとも遅く、No.7がもっとも速い)。No.8~12は、No.1と同等の条件で水アトマイズを行った。
次に、水アトマイズ法により製造した粉末に対して、Cuクラスタの密度調整を兼ねた乾燥処理を行った。乾燥処理は、No.1~7は炉温を180℃とし、6時間の大気雰囲気で、さらに大気圧に対し10Paの減圧下で6時間の処理を実施した。
乾燥処理における大気雰囲気での処理について、No.8は、120℃で6時間、No.9は80℃で6時間、No.10は220℃で6時間、No.11は290℃で6時間、No.12は360℃で6時間とした。
磁束密度が1.65T以上かつ保磁力が100A/m以下 ・・・◎
磁束密度が1.65T以上かつ保磁力が100A/m超150A/m以下・・・〇
磁束密度が1.65T未満かつ/又は保磁力が150A/m超 ・・・×
「〇」と「◎」が合格であり、「×」は不合格である。
Si、B、P、Cuの添加量の影響を検討するために、表2に示す成分組成の鉄基軟磁性粉末を作製した。作製方法は、使用した溶鋼の成分組成を変更したこと以外は、実施例1のNo.1と同様である。
Feの一部をNi、Coと置換した際の影響を検討するために、表3に示す成分組成の鉄基軟磁性粉末を作製した。作製方法は、使用した溶鋼の成分組成を変更したこと以外は、実施例1のNo.1と同様である。

Pの一部をMn、Cr、Mo、Nb、Sn、Zr、Tr、W、Hf、Vと置換した際の影響を検討するために、表4に示す成分組成の粉末を作製した。作製方法は、使用した溶鋼の成分組成を変更したこと以外は、実施例1のNo.1と同様である。

軟磁性粉末の不可避的不純物として含まれるO含有量の影響を検討するために、表5のNo.73~75に示す組成の粉末を作製した。作製方法は、使用した溶鋼の成分組成を変更したこと以外は、実施例1のNo.1と同様であるが、O含有量の相違は噴霧中の雰囲気酸素濃度を調整したことによる。
Claims (7)
- 鉄基軟磁性粉末であって、
結晶化度が10%以下であり、
体積基準の円形度の中央値(C50)が0.85以上であり、
窒素雰囲気中、昇温速度3℃/分で400℃まで昇温し、該温度で20分間保持し、次いで室温まで自然放冷した粉末中のCuクラスタの数密度が1.00×103個/μm3以上1.00×106個/μm3以下であり、かつCuクラスタのCu濃度の平均値が30.0at%以上である、鉄基軟磁性粉末。 - 不可避的不純物を除く成分組成が、組成式:FeaMbSicBdPeCuf
(式中、
79.0at%≦a+b≦84.5at%
0at%≦b≦10.0at%
0at%≦c<6.0at%
0at%<d≦11.0at%
3.0at%<e≦11.0at%
0.2at%≦f≦1.0at%、かつ
a+b+c+d+e+f=100at%であり、
Mは、Ni及びCoから選ばれる少なくとも1種の元素である)
で示される、請求項1に記載の鉄基軟磁性粉末。 - 前記組成式におけるPが、4.0at%以下の量で、C、Mn、Cr、Mo、Nb、Sn、Zr、Ta、W、Hf及びVから選ばれる少なくとも1種の元素で置換されている、請求項2に記載の鉄基軟磁性粉末。
- 前記不可避的不純物として含まれるO含有量が0.3質量%以下である、請求項1~3のいずれか一項に記載の鉄基軟磁性粉末。
- 前記鉄基軟磁性粉末を構成する粒子の表面に絶縁被覆を有する、請求項1~4のいずれかに一項に記載の鉄基軟磁性粉末。
- 請求項5に記載の鉄基軟磁性粉末を用いてなる磁性部品。
- 請求項5に記載の鉄基軟磁性粉末を用いてなる圧粉磁芯。
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CA3223549A CA3223549C (en) | 2021-07-26 | 2022-05-09 | Iron-based soft magnetic powder, magnetic component using same and dust core |
| EP22848984.5A EP4372769A4 (en) | 2021-07-26 | 2022-05-09 | IRON-BASED SOFT MAGNETIC POWDER, MAGNETIC COMPONENT USING SAME AND DUST CORE |
| JP2022555883A JP7304498B2 (ja) | 2021-07-26 | 2022-05-09 | 鉄基軟磁性粉末、それを用いた磁性部品及び圧粉磁芯 |
| US18/579,400 US20240342792A1 (en) | 2021-07-26 | 2022-05-09 | Iron-based soft magnetic powder, magnetic component using same and dust core |
| CN202280046505.4A CN117581315A (zh) | 2021-07-26 | 2022-05-09 | 铁基软磁性粉末、使用该粉末的磁性部件和压粉磁芯 |
| KR1020237044361A KR102826320B1 (ko) | 2021-07-26 | 2022-05-09 | 철기 연자성 분말, 그것을 이용한 자성 부품 및 압분 자심 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2021122053 | 2021-07-26 | ||
| JP2021-122053 | 2021-07-26 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2023007902A1 true WO2023007902A1 (ja) | 2023-02-02 |
Family
ID=85086589
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2022/019735 Ceased WO2023007902A1 (ja) | 2021-07-26 | 2022-05-09 | 鉄基軟磁性粉末、それを用いた磁性部品及び圧粉磁芯 |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20240342792A1 (ja) |
| EP (1) | EP4372769A4 (ja) |
| JP (1) | JP7304498B2 (ja) |
| KR (1) | KR102826320B1 (ja) |
| CN (1) | CN117581315A (ja) |
| WO (1) | WO2023007902A1 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2025192081A1 (ja) * | 2024-03-15 | 2025-09-18 | 戸田工業株式会社 | 軟磁性金属粉末 |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017034091A (ja) * | 2015-07-31 | 2017-02-09 | Jfeスチール株式会社 | 軟磁性圧粉磁芯の製造方法および軟磁性圧粉磁芯 |
| JP2019203150A (ja) * | 2018-05-21 | 2019-11-28 | Tdk株式会社 | 軟磁性粉末、圧粉体および磁性部品 |
| WO2021132254A1 (ja) * | 2019-12-25 | 2021-07-01 | 株式会社東北マグネットインスティテュート | ナノ結晶軟磁性合金 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| BRPI0906063B1 (pt) | 2008-08-22 | 2019-12-10 | Tohoku Magnet Institute Co., Ltd. | composição de liga e método para formar uma liga nanocristalina baseada em ferro |
| WO2018152309A1 (en) * | 2017-02-15 | 2018-08-23 | Crs Holdings, Inc. | Fe-based, soft magnetic alloy |
| JP6998552B2 (ja) | 2017-07-06 | 2022-02-04 | パナソニックIpマネジメント株式会社 | 圧粉磁心 |
| CN112534076B (zh) * | 2018-07-31 | 2022-06-03 | 杰富意钢铁株式会社 | 软磁性粉末、Fe基纳米晶合金粉末、磁性部件以及压粉磁芯 |
| CN112750589B (zh) * | 2019-10-31 | 2024-08-30 | Tdk株式会社 | 磁性体芯和线圈部件 |
-
2022
- 2022-05-09 WO PCT/JP2022/019735 patent/WO2023007902A1/ja not_active Ceased
- 2022-05-09 KR KR1020237044361A patent/KR102826320B1/ko active Active
- 2022-05-09 EP EP22848984.5A patent/EP4372769A4/en active Pending
- 2022-05-09 JP JP2022555883A patent/JP7304498B2/ja active Active
- 2022-05-09 CN CN202280046505.4A patent/CN117581315A/zh active Pending
- 2022-05-09 US US18/579,400 patent/US20240342792A1/en active Pending
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017034091A (ja) * | 2015-07-31 | 2017-02-09 | Jfeスチール株式会社 | 軟磁性圧粉磁芯の製造方法および軟磁性圧粉磁芯 |
| JP2019203150A (ja) * | 2018-05-21 | 2019-11-28 | Tdk株式会社 | 軟磁性粉末、圧粉体および磁性部品 |
| WO2021132254A1 (ja) * | 2019-12-25 | 2021-07-01 | 株式会社東北マグネットインスティテュート | ナノ結晶軟磁性合金 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4372769A4 * |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2025192081A1 (ja) * | 2024-03-15 | 2025-09-18 | 戸田工業株式会社 | 軟磁性金属粉末 |
Also Published As
| Publication number | Publication date |
|---|---|
| KR102826320B1 (ko) | 2025-06-26 |
| US20240342792A1 (en) | 2024-10-17 |
| KR20240010503A (ko) | 2024-01-23 |
| EP4372769A4 (en) | 2024-11-13 |
| JP7304498B2 (ja) | 2023-07-06 |
| CN117581315A (zh) | 2024-02-20 |
| EP4372769A1 (en) | 2024-05-22 |
| JPWO2023007902A1 (ja) | 2023-02-02 |
| CA3223549A1 (en) | 2023-02-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN112534076B (zh) | 软磁性粉末、Fe基纳米晶合金粉末、磁性部件以及压粉磁芯 | |
| Liu et al. | Microstructure and magnetic properties of soft magnetic powder cores of amorphous and nanocrystalline alloys | |
| CN110225801B (zh) | 软磁性粉末、Fe基纳米晶合金粉末、磁性部件及压粉磁芯 | |
| JP4630251B2 (ja) | 圧粉磁心および圧粉磁心用の鉄基粉末 | |
| JP6669304B2 (ja) | 結晶質Fe基合金粉末及びその製造方法 | |
| CN111093860B (zh) | Fe基纳米晶合金粉末及其制造方法、Fe基非晶合金粉末及磁芯 | |
| KR102423591B1 (ko) | 연자성 합금 및 자성 부품 | |
| US11783974B2 (en) | Soft magnetic alloy and magnetic device | |
| KR20210002498A (ko) | 합금 분말, Fe기 나노 결정 합금 분말 및 자심 | |
| WO2014034616A1 (ja) | 圧粉磁心用鉄粉および圧粉磁心の製造方法 | |
| JP7304498B2 (ja) | 鉄基軟磁性粉末、それを用いた磁性部品及び圧粉磁芯 | |
| JP2018073947A (ja) | 軟磁性合金、軟磁性合金粉末及び磁性部品 | |
| JP6260667B1 (ja) | 軟磁性合金 | |
| CA3223549C (en) | Iron-based soft magnetic powder, magnetic component using same and dust core | |
| JP2025058542A (ja) | 軟磁性金属粉末、磁気コアおよび磁性部品 | |
| JP6969677B2 (ja) | 圧粉磁芯用鉄基粉末および圧粉磁芯 | |
| JP2022001659A (ja) | 圧粉磁芯用鉄基粉末およびそれを用いた圧粉磁芯 | |
| JP7207551B2 (ja) | 圧粉磁芯用鉄基粉末、圧粉磁芯および圧粉磁芯の製造方法 | |
| JP2018073945A (ja) | 複合磁性粒及び磁性部品 | |
| WO2023007900A1 (ja) | Fe基非晶質合金粉末、磁性部品、および圧粉磁芯 | |
| WO2023007901A1 (ja) | Fe基非晶質合金粉末、磁性部品、および圧粉磁芯 | |
| JP2025167784A (ja) | 軟磁性合金粒子、軟磁性粉末、圧粉磁芯および電子部品 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 2022555883 Country of ref document: JP Kind code of ref document: A |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 22848984 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 3223549 Country of ref document: CA |
|
| ENP | Entry into the national phase |
Ref document number: 20237044361 Country of ref document: KR Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1020237044361 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202280046505.4 Country of ref document: CN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 18579400 Country of ref document: US |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2022848984 Country of ref document: EP |
|
| ENP | Entry into the national phase |
Ref document number: 2022848984 Country of ref document: EP Effective date: 20240212 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |