WO2023026819A1 - 高強度鋼板およびその製造方法 - Google Patents
高強度鋼板およびその製造方法 Download PDFInfo
- Publication number
- WO2023026819A1 WO2023026819A1 PCT/JP2022/030044 JP2022030044W WO2023026819A1 WO 2023026819 A1 WO2023026819 A1 WO 2023026819A1 JP 2022030044 W JP2022030044 W JP 2022030044W WO 2023026819 A1 WO2023026819 A1 WO 2023026819A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- less
- steel sheet
- layer
- cold
- martensite
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/01—Layered products comprising a layer of metal all layers being exclusively metallic
- B32B15/012—Layered products comprising a layer of metal all layers being exclusively metallic one layer being formed of an iron alloy or steel, another layer being formed of aluminium or an aluminium alloy
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/01—Layered products comprising a layer of metal all layers being exclusively metallic
- B32B15/013—Layered products comprising a layer of metal all layers being exclusively metallic one layer being formed of an iron alloy or steel, another layer being formed of a metal other than iron or aluminium
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/004—Heat treatment of ferrous alloys containing Cr and Ni
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/005—Heat treatment of ferrous alloys containing Mn
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/008—Heat treatment of ferrous alloys containing Si
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0226—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0236—Cold rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0247—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment
- C21D8/0263—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment following hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0247—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the heat treatment
- C21D8/0273—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0278—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips involving a particular surface treatment
- C21D8/0284—Application of a separating or insulating coating
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/001—Ferrous alloys, e.g. steel alloys containing N
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/005—Ferrous alloys, e.g. steel alloys containing rare earths, i.e. Sc, Y, Lanthanides
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/008—Ferrous alloys, e.g. steel alloys containing tin
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/06—Ferrous alloys, e.g. steel alloys containing aluminium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/08—Ferrous alloys, e.g. steel alloys containing nickel
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/10—Ferrous alloys, e.g. steel alloys containing cobalt
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/14—Ferrous alloys, e.g. steel alloys containing titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/16—Ferrous alloys, e.g. steel alloys containing copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/32—Ferrous alloys, e.g. steel alloys containing chromium with boron
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/34—Ferrous alloys, e.g. steel alloys containing chromium with more than 1.5% by weight of silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/38—Ferrous alloys, e.g. steel alloys containing chromium with more than 1.5% by weight of manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/58—Ferrous alloys, e.g. steel alloys containing chromium with nickel with more than 1.5% by weight of manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/60—Ferrous alloys, e.g. steel alloys containing lead, selenium, tellurium, or antimony, or more than 0.04% by weight of sulfur
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
- C23C2/022—Pretreatment of the material to be coated, e.g. for coating on selected surface areas by heating
- C23C2/0224—Two or more thermal pretreatments
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/04—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor characterised by the coating material
- C23C2/06—Zinc or cadmium or alloys based thereon
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/04—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor characterised by the coating material
- C23C2/12—Aluminium or alloys based thereon
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/26—After-treatment
- C23C2/28—Thermal after-treatment, e.g. treatment in oil bath
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D3/00—Electroplating: Baths therefor
- C25D3/02—Electroplating: Baths therefor from solutions
- C25D3/22—Electroplating: Baths therefor from solutions of zinc
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/001—Austenite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/004—Dispersions; Precipitations
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/005—Ferrite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2211/00—Microstructure comprising significant phases
- C21D2211/008—Martensite
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2241/00—Treatments in a special environment
Definitions
- the present invention relates to a high-strength steel sheet and its manufacturing method.
- Parts such as crash boxes have punched end faces and bent parts. Therefore, steel sheets used for these parts are required to have good stretch flangeability and bendability.
- a part using a high-strength steel sheet having a tensile strength of 1180 MPa or more may suffer so-called delayed fracture due to penetration of hydrogen therein.
- Steel sheets for automobiles are required to have good delayed fracture resistance because stress is applied during pressing and assembly, and there is a risk of hydrogen intrusion from the environment after that.
- the present invention has been made in view of the above points, and provides a high-strength steel sheet having a tensile strength of 1180 MPa or more and excellent part strength, stretch flangeability, bendability and delayed fracture resistance. With the goal.
- the present invention provides the following [1] to [14].
- [1] A steel sheet is provided, and the steel sheet contains, in mass %, C: 0.090% or more and 0.390% or less, Si: 0.01% or more and 2.00% or less, Mn: 2.00% or more and 4.
- the balance has a component composition consisting of Fe and inevitable impurities and a microstructure, and in the microstructure, the area ratio of martensite is 70% or more and the area ratio of ferrite is 10% or less, A high-strength steel sheet, wherein the area ratio of retained austenite is 10% or less, and the ratio of the number of martensite blocks in which metastable carbides are present to the number of martensite blocks is 2% or more.
- the high-strength steel sheet according to [1] above, wherein the number density of the metastable carbides in the martensite block in which the metastable carbides are present is 1 ⁇ 10 6 /mm 2 or more.
- the above component composition further includes Ti: 0.200% or less, Nb: 0.200% or less, V: 0.200% or less, Ta: 0.10% or less, W: 0.10% or less, in terms of % by mass.
- B 0.0100% or less
- Cr 1.00% or less
- Mo 1.00% or less
- Ni 1.00% or less
- Co 0.010% or less
- Cu 1.00% below
- Sn 0.200% or less
- Sb 0.200% or less
- Ca 0.0100% or less
- Mg 0.0100% or less
- REM 0.0100% or less
- Zr 0.100% or less
- the above [1] or [2] containing at least one element selected from the group consisting of Te: 0.100% or less, Hf: 0.10% or less, and Bi: 0.200% or less high-strength steel plate.
- the steel sheet has a soft layer as a surface layer, the surface layer is a portion from the surface of the steel sheet to 200 ⁇ m in the thickness direction, and the soft layer is the 1 ⁇ 4 position of the thickness of the steel sheet.
- the high-strength steel sheet according to any one of [1] to [3] above, wherein the portion has a Vickers hardness of 85% or less with respect to the Vickers hardness of .
- the nano-hardness is measured at 300 points or more in the range of 50 ⁇ m ⁇ 50 ⁇ m at the 1/4 position in the plate thickness direction of the soft layer, the nano-hardness is 7.0 GPa with respect to the total number of measurement points.
- the standard deviation ⁇ A of the nano-hardness at the thickness direction depth 1 ⁇ 4 position of the soft layer is 1.8 GPa or less, and the nano-hardness at the thickness direction depth 1 ⁇ 2 position of the soft layer.
- the residence time t1 in the temperature range T1 above Ms ° C. and 700 ° C. or less is 1000 s or less, and Ms -80 ° C. or more and Ms ° C. or less.
- the first average cooling rate v1 in the temperature range T2 is 1.0 ° C./s or more and 40.0 ° C./s or less, and the second average cooling rate v2 in the temperature range T3 of 150 ° C. or more and less than Ms-80 ° C.
- Formula 2 100 ⁇ X ⁇ 400 [12]
- heating at the heating temperature is performed in an atmosphere with a dew point of ⁇ 30° C. or higher to form a soft layer on the surface layer of the cold-rolled sheet. It is a portion from the surface of the rolled sheet to 200 ⁇ m in the sheet thickness direction, and the soft layer is a portion where the Vickers hardness is 85% or less with respect to the Vickers hardness at the 1/4 position of the sheet thickness of the cold-rolled sheet.
- a high-strength steel sheet that has a tensile strength of 1180 MPa or more and is excellent in part strength, stretch flange formability, bendability and delayed fracture resistance.
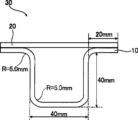
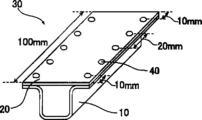
- FIG. 4 is a perspective view showing a state in which a test piece is subjected to orthogonal bending; It is a front view of a test body. It is a perspective view of a test body. FIG. 4 is a perspective view showing a state in which an axial crush test is being performed on a specimen;
- the high-strength steel sheet of the present invention has a steel sheet (base steel sheet), and this steel sheet has a composition and a microstructure described below.
- the high-strength steel sheet of the present invention has a tensile strength of 1180 MPa or more and is excellent in part strength, stretch flange formability, bendability and delayed fracture resistance.
- High strength means that the tensile strength (TS) determined by a tensile test described later is 1180 MPa or more.
- Excellent part strength means that the yield ratio (YR) determined by a tensile test described later is 65% or more.
- Excellent stretch flangeability means that the hole expansion ratio ( ⁇ ) determined by the hole expansion test described later is 30% or more.
- Excellent bendability means that no cracks occur in any of the five test pieces in the bending test described below.
- Excellent delayed fracture resistance means that in the delayed fracture test described later, when TS is 1180 MPa or more and less than 1700 MPa, after 48 hours, when TS is 1700 MPa or more, cracks are confirmed after 24 hours. means not
- the steel sheet (base steel sheet) constituting the high-strength steel sheet of the present invention will be described.
- the steel sheet is, for example, a cold-rolled sheet after undergoing post-heating, which will be described later.
- the plate thickness of the steel plate is not particularly limited, and is usually 0.3 mm or more and 2.8 mm or less.
- composition of the steel sheet (hereinafter also referred to as “chemical composition of the present invention” for convenience) will be described.
- “%” in the component composition of the present invention means “% by mass” unless otherwise specified.
- C (C: 0.090% or more and 0.390% or less) C is one of the important basic components of steel, and particularly in the present invention, it affects the area ratios of martensite and ferrite. If the C content is too low, the area ratio of martensite decreases, making it difficult to achieve a TS of 1180 MPa or more. Therefore, the C content is 0.090% or more, preferably 0.100% or more, and more preferably 0.110% or more. On the other hand, if the C content is too high, the amount of retained austenite increases excessively, and the hardness of martensite generated from the retained austenite during punching greatly increases.
- the C content is 0.390% or less, preferably 0.360% or less, and more preferably 0.350% or less.
- Si 0.01% or more and 2.00% or less
- Si increases the strength of the steel sheet by suppressing the precipitation of cementite in martensite and solid-solution strengthening.
- the Si content is 0.01% or more, preferably 0.20% or more, and more preferably 0.30% or more.
- the Si content is 2.00% or less, preferably 1.50% or less, and more preferably 1.30% or less.
- Mn is one of the important basic components of steel, and particularly in the present invention, it affects the area ratio of martensite. If the Mn content is too low, the martensite area ratio decreases, making it difficult to achieve a TS of 1180 MPa or more. Therefore, the Mn content is 2.00% or more, preferably 2.20% or more, and more preferably 2.50% or more. On the other hand, if the Mn content is too high, the austenite is stabilized, the retained austenite is excessively increased, and the hardness of the martensite generated from the retained austenite at the time of punching greatly increases.
- the Mn content is 4.00% or less, preferably 3.80% or less, and more preferably 3.60% or less.
- the P content is 0.100% or less, preferably 0.070% or less, more preferably 0.050% or less, and even more preferably 0.020% or less.
- the lower limit of the P content is not particularly limited.
- P is a solid-solution strengthening element and increases the strength of the steel sheet. Therefore, the P content is preferably 0.001% or more, more preferably 0.002% or more.
- the S content is 0.0200% or less, preferably 0.0100% or less, more preferably 0.0050% or less, and even more preferably 0.0020% or less.
- the lower limit of the S content is not particularly limited, it is preferably 0.0001% due to production technology restrictions.
- Al (Al: 1.000% or less) Al performs sufficient deoxidation to reduce inclusions in the steel. However, if the Al content is too high, a large amount of ferrite is generated, the hole expansion ratio is lowered, and the stretch flangeability is lowered. Therefore, the Al content is 1.000% or less, preferably 0.500% or less, and more preferably 0.100% or less. On the other hand, in order to stably deoxidize, the Al content is preferably 0.010% or more, more preferably 0.015% or more, and even more preferably 0.020% or more.
- N (N: 0.0100% or less) N exists as a nitride and lowers the ultimate deformability of the steel sheet. As a result, the hole expansion ratio is lowered and the stretch flangeability is lowered. Also, the bendability is reduced. Therefore, the N content is 0.0100% or less, preferably 0.0070% or less, and more preferably 0.0050% or less. Although the lower limit of the N content is not particularly limited, it is preferably 0.0001% due to production technology restrictions.
- O (O: 0.0100% or less) O exists as an oxide and lowers the ultimate deformability of the steel sheet. As a result, the hole expansion ratio is lowered and the stretch flangeability is lowered. Also, the bendability is reduced. Therefore, the O content is 0.0100% or less, preferably 0.0050% or less, more preferably 0.0030% or less, and even more preferably 0.0020% or less. Although the lower limit of the O content is not particularly limited, it is preferably 0.0001% due to production technology restrictions.
- the component composition of the present invention may further contain at least one element selected from the group consisting of the elements described below in mass %.
- Ti, Nb and V each 0.200% or less
- the contents of Ti, Nb and V are each preferably 0.200% or less, more preferably 0.100% or less, and still more preferably 0.080% or less. If the content of each element is within this range, a large amount of coarse precipitates and inclusions are not generated, and the ultimate deformability of the steel sheet is not lowered, so the stretch flangeability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limits of the contents of Ti, Nb and V are not particularly limited.
- Ti, Nb and V increase the strength of the steel sheet by forming fine carbides, nitrides or carbonitrides during hot rolling or annealing, which will be described later. Therefore, when Ti, Nb and V are added, the content of Ti, Nb and V is preferably 0.001% or more, and preferably 0.005% or more, from the viewpoint of obtaining the effect of adding these elements. More preferably, 0.010% or more is even more preferable.
- Ta and W each 0.10% or less
- the contents of Ta and W are each preferably 0.10% or less, more preferably 0.08% or less, and still more preferably 0.04% or less. If the content of each element is within this range, a large amount of coarse precipitates and inclusions are not generated, and the ultimate deformability of the steel sheet is not lowered, so the stretch flangeability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limits of the Ta and W contents are not particularly limited. However, Ta and W increase the strength of the steel sheet by forming fine carbides, nitrides or carbonitrides during hot rolling or annealing, which will be described later. Therefore, when Ta and W are added, the contents of Ta and W are preferably 0.01% or more, respectively, from the viewpoint of obtaining the effect of adding these elements.
- the B content is preferably 0.0100% or less, more preferably 0.0080% or less, even more preferably 0.0050% or less.
- the lower limit of the B content is not particularly limited. However, B segregates at austenite grain boundaries during annealing, which will be described later, and improves hardenability. Therefore, when B is added, the B content is preferably 0.0003% or more, more preferably 0.0005% or more, and still more preferably 0.0010% or more, from the viewpoint of obtaining the effect of B addition.
- each of Cr, Mo and Ni is preferably 1.00% or less, more preferably 0.90% or less, and still more preferably 0.80% or less. If the content of each element is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, resulting in better stretch flangeability (hole expansion ratio). Moreover, bendability is also more excellent.
- the lower limits of the contents of Cr, Mo and Ni are not particularly limited. However, Cr, Mo and Ni improve hardenability.
- the content of Cr, Mo and Ni is preferably 0.01% or more, and preferably 0.02% or more, from the viewpoint of obtaining the effect of adding these elements. More preferably, 0.03% or more is even more preferable.
- the Co content is preferably 0.010% or less, more preferably 0.008% or less, even more preferably 0.006% or less. If the Co content is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, so the stretch flange formability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limit of Co content is not particularly limited. However, Co improves hardenability. Therefore, when Co is added, the Co content is preferably 0.001% or more, more preferably 0.002% or more, and still more preferably 0.004% or more, from the viewpoint of obtaining the effect of Co addition.
- the Cu content is preferably 1.00% or less, more preferably 0.80% or less, and even more preferably 0.30% or less. If the Cu content is within this range, coarse precipitates and inclusions do not increase and the ultimate deformability of the steel sheet does not decrease, so the stretch flangeability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limit of the Cu content is not particularly limited. However, Cu improves hardenability. Therefore, when Cu is added, the Cu content is preferably 0.01% or more, more preferably 0.03% or more, and still more preferably 0.05% or more, from the viewpoint of obtaining the effect of adding Cu.
- the Sn content is preferably 0.200% or less, more preferably 0.100% or less, and even more preferably 0.050% or less. If the Sn content is within this range, cracks do not form inside the steel sheet during casting or hot rolling described later, and the ultimate deformability of the steel sheet does not decrease, so stretch flangeability (hole expansion ratio) is improved. Better. Moreover, bendability is also more excellent.
- the lower limit of the Sn content is not particularly limited. However, Sn improves hardenability. Therefore, when Sn is added, the Sn content is preferably 0.001% or more, more preferably 0.004% or more, and still more preferably 0.008% or more, from the viewpoint of obtaining the effect of Sn addition.
- the Sb content is preferably 0.200% or less, more preferably 0.100% or less, and even more preferably 0.050% or less. If the Sb content is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, so the stretch flangeability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limit of the Sb content is not particularly limited. However, Sb controls the softening thickness of the surface layer to enable strength adjustment. Therefore, when Sb is added, the Sb content is preferably 0.001% or more, more preferably 0.003% or more, and still more preferably 0.007% or more, from the viewpoint of obtaining the effect of adding Sb.
- the Ca, Mg and REM (rare earth metal) contents are each preferably 0.0100% or less, more preferably 0.0050% or less, and even more preferably 0.0030% or less. If the content of each element is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, resulting in better stretch flangeability (hole expansion ratio). Moreover, bendability is also more excellent.
- the lower limits of the Ca, Mg and REM contents are not particularly limited. However, Ca, Mg and REM spheroidize the shape of nitrides and sulfides and improve the ultimate deformability of the steel sheet.
- the contents of Ca, Mg, and REM are each preferably 0.0002% or more, and 0.0005% or more, from the viewpoint of obtaining the effect of adding these elements. More preferably, 0.0010% or more is even more preferable.
- Zr and Te each 0.100% or less
- the contents of Zr and Te are each preferably 0.100% or less, more preferably 0.080% or less, and still more preferably 0.050% or less. If the content of each element is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, resulting in better stretch flangeability (hole expansion ratio). Moreover, bendability is also more excellent.
- the lower limits of the contents of Zr and Te are not particularly limited. However, Zr and Te spheroidize the shape of nitrides and sulfides and improve the ultimate deformability of the steel sheet. Therefore, when Zr and Te are added, the contents of Zr and Te are preferably 0.001% or more, more preferably 0.003% or more, respectively, from the viewpoint of obtaining the effect of adding these elements. More preferably 0.007% or more.
- the Hf content is preferably 0.10% or less, more preferably 0.08% or less, and even more preferably 0.05% or less. If the Hf content is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, so the stretch flangeability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limit of Hf content is not particularly limited. However, Hf spheroidizes the shape of nitrides and sulfides and improves the ultimate deformability of the steel sheet. Therefore, when Hf is added, the Hf content is preferably 0.01% or more, more preferably 0.02% or more, from the viewpoint of obtaining the effect of adding Hf.
- the Bi content is preferably 0.200% or less, more preferably 0.100% or less, and even more preferably 0.030% or less. If the Bi content is within this range, coarse precipitates and inclusions do not increase, and the ultimate deformability of the steel sheet does not decrease, so the stretch flangeability (hole expansion ratio) is more excellent. Moreover, bendability is also more excellent.
- the lower limit of the Bi content is not particularly limited. However, Bi is an element that reduces segregation. Therefore, when Bi is added, the Bi content is preferably 0.001% or more, more preferably 0.002% or more, and still more preferably 0.004% or more, from the viewpoint of obtaining the effect of Bi addition.
- the balance in the component composition of the present invention consists of Fe and unavoidable impurities.
- Fe for Ti, Nb, V, Ta, W, B, Cr, Mo, Ni, Co, Cu, Sn, Sb, Ca, Mg, REM, Zr, Te, Hf and Bi, the content of each element is If the content is less than the lower limit of the preferred range, the element is treated as an unavoidable impurity because it does not impair the effects of the present invention.
- microstructure of the steel sheet (hereinafter also referred to as "the microstructure of the present invention” for convenience) will be described.
- the area ratio of martensite is 70% or more, preferably 75% or more, more preferably 80% or more, and even more preferably 85% or more.
- the upper limit is not particularly limited, and this effect can be obtained even if the area ratio of martensite is 100%.
- Martensite includes lower bainite, martensite self-tempered during cooling performed in annealing described later, martensite tempered by post-heating described later, and the like. The observation position of martensite is the 1/4 position of the plate thickness of the steel plate, as will be described later.
- the area ratio of ferrite is 10% or less, preferably 8% or less, more preferably 5% or less, and even more preferably 3% or less.
- the lower limit is not particularly limited, and this effect can be obtained even if the area ratio of ferrite is 0%.
- Ferrites include allotriomorph ferrite, idiomorph ferrite, Widmanstetten ferrite, upper bainite, and the like. The observation position of the ferrite is the 1/4 position of the plate thickness of the steel plate, as will be described later.
- the method for measuring the area ratios of martensite and ferrite is as follows. First, a sample is cut out from a steel plate so that the plate thickness cross section (L cross section at the position of 1/4 of the plate thickness) parallel to the rolling direction is the observation surface. The observation surface of the sample is mirror-polished with diamond paste, then finished with colloidal silica, and etched with 1% by volume of nital to expose the structure. Next, the observation surface of the sample is observed at a magnification of 3000 times using a scanning electron microscope (SEM) under the condition of an acceleration voltage of 10 kV to obtain SEM images for 3 fields of view. The area ratio of each tissue is calculated from the obtained SEM image using Adobe Photoshop (manufactured by Adobe Systems).
- Adobe Photoshop manufactured by Adobe Systems
- the area ratio of each tissue is obtained by dividing the area of each tissue by the measured area.
- the area ratio of each tissue is calculated for three fields of view, and the average value thereof is taken as the area ratio of each tissue.
- ferrite has a gray flat structure
- martensite has a hierarchical structure with fine irregularities inside, and both can be distinguished from each other.
- the area ratio of retained austenite is 10% or less, preferably 8% or less, more preferably 5% or less, and even more preferably 4% or less.
- the lower limit is not particularly limited, and this effect can be obtained even if the area ratio of retained austenite is 0%.
- the method for measuring the area ratio of retained austenite is as follows. First, the steel plate is ground so that the 1/4 position of the plate thickness (the position corresponding to 1/4 of the plate thickness in the depth direction from the steel plate surface) is the measurement surface, and then chemical polishing is performed to further 0.1 mm. Grind and get a sample. The (200) plane, (220) plane and (311) plane of fcc iron (austenite) and the (200) plane of bcc iron were measured using an X-ray diffractometer using a Co K ⁇ ray source. The integrated reflection intensities of the (211) and (220) planes are measured.
- the intensity ratio of the integrated reflection intensity of each surface of fcc iron to the integrated reflection intensity of each surface of bcc iron is obtained. Let the average value of nine intensity ratios be the volume fraction of retained austenite. The volume fraction of retained austenite is regarded as the area fraction of retained austenite.
- the ratio of the number of martensite blocks in which metastable carbides are present to the number of martensite blocks is 2% or more, preferably 5% or more, and 10%. 20% or more is more preferable, and 30% or more is particularly preferable.
- the upper limit of the ratio p is not particularly limited, and may be 100%.
- Metastable carbides are metastable carbides that precipitate during the tempering process of martensite.
- Metastable carbides are, for example, Fe carbides (iron-based carbides) other than cementite, and include at least one carbide selected from the group consisting of epsilon ( ⁇ ) carbides, eta ( ⁇ ) carbides and chi ( ⁇ ) carbides. be done.
- the method for measuring the ratio of the number of martensite blocks in which metastable carbides are present (ratio p) to the number of martensite blocks is as follows. First, the steel plate is ground so that the 1/4 position of the plate thickness (the position corresponding to 1/4 of the plate thickness in the depth direction from the steel plate surface) is the observation surface, and then electrolytically polished to obtain a sample. make. Observation surfaces of the prepared samples are observed using a transmission electron microscope (TEM) under the condition of an acceleration voltage of 200 kV. Since the dislocation density of martensite is significantly higher than that of ferrite and retained austenite, martensite can be distinguished from each other and identified within the observation field by observing the strain contrast in the TEM bright-field image.
- TEM transmission electron microscope
- a martensite block is one of the structural units of martensite having a hierarchical structure, and is a group of laths having the same habit plane and the same crystal orientation.
- the diffraction contrast differs for each block in martensite, it can be distinguished from other structural units such as packets and laths, and martensite blocks can be identified.
- an electron beam is incident from the [100] orientation of the martensite block, an electron diffraction pattern of the matrix martensite is obtained.
- Adjacent martensitic blocks have different crystal orientations across the block boundaries, and thus have different contrasts in bright-field images, so that they can be distinguished from each other.
- FIG. 1 is an example of an electron diffraction pattern of martensite in which carbides are present. If carbides are present in the single observed martensite block, the electron diffraction pattern of the carbides is obtained in addition to the electron diffraction pattern of the matrix martensite ( ⁇ ), as shown in FIG.
- the martensite block is: Defined as martensitic blocks in which metastable carbides are present.
- the ratio of the number of martensite blocks in which metastable carbides are present to the number of martensite blocks is "the number of martensite blocks whose ratio d c / dm to the number of martensite blocks is 1.020 or more and 1.150 or less.
- Metastable carbides may exist inside martensite blocks or at boundaries such as block boundaries, but preferably inside martensite blocks.
- the obtained value is defined as the ratio (ratio p) [%] of the number of martensite blocks in which the metastable carbide exists to the number of martensite blocks.
- the number density of metastable carbides in a martensite block in which metastable carbides are present is preferably 1 ⁇ 10 6 /mm 2 or more, and 10 ⁇ 10 6 /mm 2 or more is more preferable, and 100 ⁇ 10 6 /mm 2 or more is even more preferable.
- the upper limit of the number density n is not particularly limited . /mm 2 is more preferred, and 10,000 ⁇ 10 6 /mm 2 is even more preferred.
- the number density of metastable carbides (number density n) in a martensite block in which metastable carbides are present is obtained as follows. In measuring the fraction p using TEM as described above, a selected area electron diffraction pattern was obtained in a single martensite block in which metastable carbides were present, and the electron diffraction spots obtained from the metastable carbides were used to obtain a dark field get the image. In dark field images, metastable carbides exhibit a white contrast. A 300 nm ⁇ 300 nm area is imaged inside a single martensite block and the number of metastable carbides is counted. It should be noted that adjacent martensite blocks may exist in a region of 300 nm ⁇ 300 nm across a block boundary.
- the area of a martensite block in which metastable carbides are present is defined as the area of a single martensite block for which a selected area electron diffraction pattern was obtained. Adjacent martensitic blocks have different crystal orientations across the block boundaries, and thus have different contrasts in bright-field images, so that they can be distinguished from each other.
- the average equivalent circle diameter of the metastable carbides in the martensite block is preferably 20 nm or less, more preferably 5 nm or less.
- the average equivalent circle diameter of the metastable carbides in the martensite block is determined as follows. In measuring the fraction p using TEM as described above, a selected area electron diffraction pattern was obtained in a single martensite block in which metastable carbides were present, and the electron diffraction spots obtained from the metastable carbides were used to obtain a dark field get the image. In dark field images, metastable carbides exhibit a white contrast. A dark-field image of a 300 nm ⁇ 300 nm area is taken inside a single martensite block and image processing is performed to obtain a binarized image so that the metastable carbides can be distinguished. By particle analysis of the binarized image, the equivalent circle diameter is obtained for each metastable carbide particle.
- the binarized image is divided using the Watershed method. Equivalent circle diameters are determined for each of all the metastable carbides present in the area of 300 nm ⁇ 300 nm (for 3 fields of view). The average value of the equivalent circle diameters for the three fields of view is obtained, and this is taken as the average value of the equivalent circle diameters of the metastable carbides in the martensite block.
- the microstructure of the present invention may have a structure (residual structure) other than the martensite, ferrite and retained austenite described above.
- the area ratio of the remaining structure is preferably 3% or less because the effect of the present invention is not impaired.
- residual structures include pearlite; carbides such as cementite precipitated in ferrite; alloy carbonitrides precipitated in ferrite; other structures known as steel plate structures; Metastable carbides precipitated in martensite and iron-based carbides such as cementite precipitated in martensite are not included in the residual structure.
- the steel sheet (base steel sheet) constituting the high-strength steel sheet of the present invention preferably has a soft layer on its surface layer. Since the soft layer contributes to suppressing the progress of bending cracks during press forming and collision, the bendability is more excellent, and the fracture resistance at the time of collision is also excellent.
- the surface layer is a portion extending from the surface of the steel sheet (cold-rolled sheet) to 200 ⁇ m in the sheet thickness direction.
- the soft layer is a decarburized layer, more specifically, a portion having a Vickers hardness of 85% or less with respect to the Vickers hardness at the position of 1/4 thickness of the steel sheet (cold-rolled sheet).
- the Vickers hardness at the 1/4 position of the steel plate thickness is the cross section (parallel to the surface of the steel plate) surface) Vickers hardness.
- the Vickers hardness is measured according to JIS Z 2244-1:2020 with a load of 10 gf.
- the thickness of the soft layer is preferably 3 ⁇ m or more, more preferably 7 ⁇ m or more, and even more preferably 11 ⁇ m or more.
- the thickness of the soft layer is preferably 150 ⁇ m or less, more preferably 100 ⁇ m or less, and even more preferably 80 ⁇ m or less.
- the thickness of the soft layer is obtained as follows. First, using a Vickers hardness tester, the Vickers hardness is measured at intervals of 1 ⁇ m from a position 1 ⁇ m in the plate thickness direction from the surface of the steel sheet to a position 100 ⁇ m in the plate thickness direction with a load of 10 gf. Next, the Vickers hardness is measured at intervals of 20 ⁇ m to the center of the plate thickness. Note that the Vickers hardness is measured after smoothing a cross section (L cross section) of the steel sheet parallel to the rolling direction by wet polishing.
- a portion (region) where the Vickers hardness measured in this way is 85% or less with respect to the Vickers hardness at the 1/4 position of the plate thickness of the steel plate is defined as the soft layer, and the plate thickness of this portion (region) The thickness in the direction is determined as the thickness of the soft layer (unit: ⁇ m).
- ratio r The nano-hardness is measured at 300 points or more (for example, 512 points) within a range of 50 ⁇ m ⁇ 50 ⁇ m at 1/4 position in the plate thickness direction of the soft layer. At this time, the ratio of measurement points with a nano-hardness of 7.0 GPa or more to the total number of measurement points is called "ratio r".
- the ratio r is, for example, 0.20 or less, preferably 0.15 or less, and more preferably 0.10 or less.
- a smaller ratio r means less hard structures (such as martensite) and inclusions in the microstructure. When the microstructure has few hard structures and inclusions, void formation, void connection, and crack propagation can be suppressed more effectively during press forming and collision. That is, the bendability is further excellent, and the breakage resistance at the time of collision is further excellent (the value of SF max , which will be described later, is favorable).
- standard deviation ⁇ A and standard deviation ⁇ B The standard deviation of the nano-hardness at the 1 ⁇ 4 position in the plate thickness direction of the soft layer is called “standard deviation ⁇ A ”.
- standard deviation ⁇ B The standard deviation of the nano-hardness at the half depth position in the thickness direction of the soft layer is called “standard deviation ⁇ B ".
- the standard deviation ⁇ A is, for example, 2.0 GPa or less, preferably 1.8 GPa or less, and more preferably 1.7 GPa or less.
- the standard deviation ⁇ B is, for example, 2.5 GPa or less, preferably 2.2 GPa or less, and more preferably 2.1 GPa or less.
- a small standard deviation ⁇ A and a small standard deviation ⁇ B means that the hardness difference of each structure in the microstructure is small. In this case, formation of voids, connection of voids, and propagation of cracks can be further suppressed during press forming and collision. That is, the bendability is further improved, and the breakage resistance at the
- Nanohardness is hardness measured using the nanoindentation method. More specifically, the nano-hardness at the 1/4 position and 1/2 position in the plate thickness direction depth of the soft layer is obtained as follows. First, when a plated layer and/or a metal plated layer (both of which will be described later) are formed on the surface of the steel sheet, the plated layer and/or the metal plated layer are peeled off. After that, mechanical polishing is performed from the surface of the steel plate to the thickness direction depth 1/4 position (or 1/2 position) of the soft layer, then buffing is performed using diamond and alumina, and colloidal polishing is performed. Polishing with silica is performed.
- an L cross-section at the 1/4 position (or 1/2 position) of the depth in the plate thickness direction of the soft layer is obtained.
- the nano-hardness of the L-section of the soft layer is measured under the conditions of a load of 500 ⁇ N, a measurement area of 50 ⁇ m ⁇ 50 ⁇ m, and a dot interval of 2 ⁇ m.
- the high-strength steel sheet of the present invention may have a metal plating layer (also referred to as "pre-annealing plating layer") on the surface of the steel sheet.
- the metal plating layer is a layer different from the plating layer described later.
- a metal electroplating layer is preferable as the metal plating layer. Since the metal plating layer contributes to suppressing the occurrence of bending cracks during press forming and collision, the bendability is more excellent, and the fracture resistance at the time of collision is also excellent.
- the metal plating layer is preferably a metal plating layer having a component composition composed of Fe and unavoidable impurities (hereinafter also referred to as "Fe-based metal plating layer”).
- the metal plating layer is preferably a metal plating layer having a composition composed of Ni and unavoidable impurities (hereinafter also referred to as "Ni-based metal plating layer").
- the component composition of the Fe-based metal plating layer is at least one selected from the group consisting of B, C, P, N, O, Ni, Mn, Mo, Zn, W, Pb, Sn, Cr, V and Co. elements in a total amount of 10% by mass or less.
- the C content is preferably 0.08% by mass or less.
- the adhesion amount (per side) of the metal plating layer is more than 0 g/m 2 , preferably 2.0 g/m 2 or more, more preferably 5.0 g/m 2 or more, and further preferably 8.0 g/m 2 or more. preferable.
- the upper limit of the adhesion amount (per side) of the metal plating layer is not particularly limited, but from the viewpoint of cost, it is preferably 60.0 g/m 2 or less, more preferably 50.0 g/m 2 or less. /m 2 or less is more preferable, 30.0 g/m 2 or less is particularly preferable, and 20.0 g/m 2 or less is most preferable.
- the adhesion amount of the metal plating layer is obtained as follows. First, a steel plate on which a metal plating layer is formed is cut into a size of 10 mm ⁇ 15 mm and embedded in resin to obtain an embedded sample. Any three points in the cross section of the embedded sample are observed using a scanning electron microscope (SEM) at an acceleration voltage of 15 kV at a magnification of 2000 to 10000 times depending on the thickness of the metal plating layer, and metal plating Measure the layer thickness. By multiplying the average value of the thicknesses at the three locations by the specific gravity of the metal element (for example, Fe) of the metal plating layer, it is converted into the adhesion amount per one side of the metal plating layer.
- SEM scanning electron microscope
- the high-strength steel sheet of the present invention may have a plating layer on the surface of the steel sheet or metal plating layer.
- the plated layer is a layer different from the metal plated layer described above, and is formed by a plating process to be described later.
- the plated layer is not particularly limited, and examples thereof include a hot-dip plated layer and an electroplated layer.
- the plated layer may be an alloyed plated layer (alloyed plated layer).
- the plating layer includes a zinc plating layer (Zn plating layer), an Al plating layer, etc. Among them, a zinc plating layer is preferable.
- the galvanized layer may contain elements such as Al and Mg.
- the composition of the plated layer is not particularly limited, and may be a general composition.
- the plating layer when it is a hot-dip galvanized layer or an alloyed hot-dip galvanized layer, it generally contains Fe: 20% by mass or less, Al: 0.001 to 1.0% by mass, and Pb , Sb, Si, Sn, Mg, Mn, Ni, Cr, Co, Ca, Cu, Li, Ti, Be, Bi and at least one selected from the group consisting of REM in total 0 to 3.5% by mass and the balance being Zn and unavoidable impurities.
- the coating weight per side of the plated layer is preferably 20 to 80 g/m 2 .
- An alloyed hot-dip galvanized layer obtained by alloying a hot-dip galvanized layer with such an adhesion amount is also preferable.
- the Fe content in the plated layer is preferably less than 7% by mass.
- the Fe content in the plated layer is preferably 7 to 20% by mass, more preferably 7 to 15% by mass.
- the adhesion amount of the coating layer is determined as follows. First, 0.6 g of a corrosion inhibitor (IBIT 700BK (registered trademark), manufactured by Asahi Kagaku Kogyo Co., Ltd.) that suppresses the corrosion of Fe is added to 1 L of a 10% by mass hydrochloric acid aqueous solution to obtain a treatment liquid. A steel sheet having a plating layer formed thereon is immersed as a test material in the obtained treatment liquid to dissolve the plating layer. By measuring the mass of the test material before and after dissolving the plating layer, the mass decrease of the test material is obtained. The coating amount (g/m 2 ) of the coating layer is obtained by dividing the obtained mass reduction amount by the surface area of the steel sheet (the area of the portion covered with the coating layer).
- a corrosion inhibitor IBIT 700BK (registered trademark) that suppresses the corrosion of Fe is added to 1 L of a 10% by mass hydrochloric acid aqueous solution to obtain a treatment liquid.
- the manufacturing method of the present invention is also a method of manufacturing the above-described high-strength steel sheet of the present invention.
- ⁇ Hot rolling, pickling and cold rolling> In the manufacturing method of the present invention, first, a steel slab having the chemical composition of the present invention is subjected to hot rolling, pickling, and cold rolling to obtain a cold-rolled sheet.
- a method for melting molten steel to be a steel slab (steel material) is not particularly limited, and a known melting method using a converter, an electric furnace, or the like can be employed.
- Steel slabs are preferably produced by continuous casting to prevent macro segregation, but they can also be produced by other methods such as ingot casting and thin slab casting.
- the manufactured steel slab is once cooled to room temperature, then heated again, subjected to hot rolling (rough rolling and finish rolling), and then coiled.
- hot rolling rough rolling and finish rolling
- a hot-rolled sheet is obtained.
- the produced steel slab may be charged into the heating furnace as a warm piece without being cooled to room temperature, or may be rolled (roughly rolled) immediately after being slightly heated.
- a rough rolled plate is obtained by rough rolling a steel slab.
- the temperature at which the steel slab is roughly rolled (slab heating temperature) is preferably 1100° C. or higher from the viewpoint of dissolving carbides and reducing the rolling load.
- the slab heating temperature is preferably 1300° C. or lower in order to prevent an increase in scale loss.
- the slab heating temperature is the surface temperature of the steel slab. When the slab heating temperature is lowered, it is preferable to heat the rough rolled sheet using a bar heater or the like before finish rolling from the viewpoint of preventing troubles in hot rolling.
- the temperature (finish rolling temperature) at which finish rolling is performed is preferably the Ar3 transformation point or higher. This reduces the rolling load. Furthermore, the rolling reduction in the non-recrystallized state of austenite is reduced, the development of an abnormal structure elongated in the rolling direction is suppressed, and the workability is excellent. Finish rolling may be carried out continuously by joining rough rolled plates. The rough rolled sheet may be wound once before the finish rolling is performed. In order to reduce the rolling load, part or all of the finish rolling may be lubricated rolling. Lubricating rolling is also preferable from the viewpoint of homogenizing the shape and quality of the steel sheet. The coefficient of friction during lubricating rolling is preferably in the range of 0.10 to 0.25.
- the coiling temperature after hot rolling is preferably 300 to 700°C from the viewpoint of improving the threadability during cold rolling and annealing, which will be described later.
- the hot-rolled sheet obtained by hot rolling is pickled.
- oxides on the surface of the hot-rolled sheet are removed, and the high-strength steel sheet, which is the final product, is excellent in chemical conversion treatability and quality of the coating layer.
- the pickling may be performed once, or may be carried out in a plurality of times.
- the hot-rolled sheet after pickling is optionally subjected to softening heat treatment and then cold-rolled.
- a cold-rolled sheet is thus obtained.
- the conditions for cold rolling are not particularly limited, but the cumulative reduction in cold rolling is preferably 20 to 75%.
- the number of rolling passes and the rolling reduction of each pass are not particularly limited.
- the cold-rolled sheet thus obtained is optionally subjected to a metal plating treatment (pre-annealing plating treatment) described below, and then subjected to annealing and post-heating described below.
- a metal plating treatment pre-annealing plating treatment
- the hot-rolled sheet (including the hot-rolled sheet after pickling) and the cold-rolled sheet described above may be subjected to some kind of annealing before the metal plating treatment (pre-annealing plating treatment) is performed.
- the metal plating treatment is a treatment for forming the above-described metal plating layer (pre-annealing plating layer) on the surface (at least one side) of the cold-rolled sheet before annealing, which will be described later.
- metal electroplating treatment metal electroplating treatment is preferable.
- a metal electroplating layer can be formed as a metal plating layer.
- an electroplating bath used for metal electroplating a sulfuric acid bath, a hydrochloric acid bath, a mixed bath of both, or the like can be used.
- the adhesion amount of the formed metal electroplating layer can be adjusted by the energization time of the metal electroplating process.
- Metal elements contained in the electroplating bath include, for example, Cr, Mn, Fe, Co, Ni, Cu, Ga, Ge, As, Ru, Rh, Pd, Ag, Cd, In, Sn, Sb, Os, Ir , Rt, Au, Hg, Ti, Pb and Bi. Of these, Fe or Ni is preferred.
- the electroplating bath can further contain at least one element selected from the group consisting of B, C, P, N, O, Ni, Mn, Mo, Zn, W, Pb, Sn, Cr, V and Co. .
- the total content of these elements in the electroplating bath is preferably such that the total content of these elements in the formed metal plating layer is 10% by mass or less.
- the content of Fe ions (Fe 2+ ) or Ni ions (Ni 2+ ) in the electroplating bath before starting energization is preferably 0.5 to 2.0 mol/L.
- the electroplating bath can contain metallic elements as metal ions and non-metallic elements as part of boric acid, phosphoric acid, nitric acid, organic acids, and the like.
- the electroplating bath may further contain a conductivity aid such as sodium sulfate or potassium sulfate; a chelating agent; a pH buffer;
- the temperature of the electroplating bath is preferably 30 to 85° C. from the viewpoint of constant temperature maintenance.
- the pH of the electroplating bath is preferably 1.0 or more from the viewpoint of preventing a decrease in current efficiency due to hydrogen generation, and is preferably 3.0 or less in consideration of electrical conductivity.
- the current density is preferably 10 A/dm 2 or more from the viewpoint of productivity, and preferably 150 A/dm 2 or less from the viewpoint of facilitating control of the amount of the metal electroplating layer to be formed.
- the speed at which the cold-rolled sheet is passed through the electroplating bath (sheet threading speed) is preferably 5 mpm or more from the viewpoint of productivity, and 150 mpm from the viewpoint of stably controlling the adhesion amount of the metal electroplating layer to be formed. The following are preferred.
- degreasing and water washing for cleaning the surface of the cold-rolled sheet, and pickling and water washing for activating the surface of the cold-rolled sheet may be performed.
- the method of degreasing and washing with water is not particularly limited, and conventional methods can be used.
- Various acid solutions such as sulfuric acid, hydrochloric acid, nitric acid, and mixtures thereof can be used for pickling. Among them, sulfuric acid, hydrochloric acid, or mixtures thereof are preferred.
- the concentration of the acid solution is preferably 1 to 20% by mass in consideration of the ability to remove the oxide film and the prevention of surface defects due to over-acid pickling. Antifoaming agents, pickling accelerators, pickling inhibitors, and the like may be added to the acid solution.
- the obtained cold-rolled sheet is annealed.
- the cold-rolled sheet is heated at a heating temperature described later, and then cooled to a cooling stop temperature described later.
- the heating temperature is 800° C. or higher, preferably 820° C. or higher.
- the upper limit of the heating temperature is not particularly limited, 950° C. is preferable from the viewpoint of workability and the like.
- the time (heating time) for heating the cold-rolled sheet at the heating temperature is not particularly limited, but if it is too short, the reverse transformation to austenite may not proceed sufficiently, so it is preferably 30 seconds or longer, more preferably 60 seconds or longer.
- the upper limit of the heating time is not particularly limited, and is, for example, 6000 s, preferably 3000 s. In addition, "s" means a second.
- the dew point of the atmosphere when the cold-rolled sheet is heated at the above-described heating temperature is preferably ⁇ 30° C. or higher, more preferably ⁇ 20° C. or higher, still more preferably ⁇ 15° C. or higher, and particularly preferably ⁇ 5° C. or higher.
- the dew point is preferably 30° C. or less from the viewpoint of suitably preventing the surface oxidation of the metal plating layer (plating layer before annealing) and improving the adhesion of the plating layer formed by the plating treatment described later. .
- ⁇ Retention time t1 in temperature range T1 above Ms ° C. and 700 °C or less 1000 s or less>>
- the cold-rolled sheet that is cooled to the cooling stop temperature after heating passes through a temperature range T1 of Ms°C or higher and 700°C or lower. If the cold-rolled sheet stays in the temperature region T1 for too long (residence time t1), excessive ferrite transformation occurs and the area ratio of ferrite increases, failing to obtain good stretch flangeability and bendability. Therefore, the residence time t1 is 1000 s or less, preferably 500 s or less, and more preferably 300 s or less.
- the lower limit of the residence time t1 is not particularly limited, it is preferably 1 s, more preferably 5 s, and still more preferably 10 s from the viewpoint of reducing the burden of capital investment.
- Cooling in the temperature range T1 may be either continuous cooling or intermittent cooling.
- intermittent cooling is preferable from the viewpoint of alleviating the stress generated due to structural changes during cooling, achieving a good steel sheet shape, and obtaining better stretch flangeability and bendability.
- the first average cooling rate v1 is 1.0° C./s or higher, preferably 2.0° C./s or higher, and more preferably 3.0° C./s or higher.
- the first average cooling rate v1 is 40.0° C./s or less, preferably 25.0° C./s or less, and more preferably 20.0° C./s or less.
- Continuous cooling is preferable for cooling in the temperature range T2.
- the second average cooling rate v2 is 0.3° C./s or higher, preferably 0.5° C./s or higher, and more preferably 1.0° C./s or higher.
- the second average cooling rate v2 is less than the first average cooling rate v1. If the second average cooling rate v2 is equal to or higher than the first average cooling rate v1, the diffusion of C in martensite will be insufficient, and the precursor stage of metastable carbide will not occur sufficiently. As a result, in the subsequent post-heating, the precipitation of metastable carbides is suppressed, the ratio p becomes low, and the delayed fracture resistance becomes insufficient.
- Continuous cooling is preferable for cooling in the temperature range T3.
- Ms is the temperature (Ms point) at which martensite transformation begins to occur, and the value measured by the Formaster test is used.
- the cold-rolled sheet may be subjected to bending and unbending one or more times. Bending and unbending is preferably performed in a temperature range of 150°C or higher and Ms°C or lower. Bending and unbending are bending performed in a direction perpendicular to the rolling direction and subsequent unbending. Bending and unbending promotes martensite transformation. As a result, metastable carbides are efficiently precipitated in post-heating, which will be described later, and the ratio (ratio p) of the number of martensite blocks in which metastable carbides are present to the number of martensite blocks is increased.
- the number of times of bending and unbending is preferably 1 or more, more preferably 2 or more, and even more preferably 3 or more.
- the number of bending and unbending processes is preferably 10 times or less, more preferably 8 times or less, and even more preferably 5 times or less.
- the method of bending and unbending is not particularly limited, but generally includes a method using rolls.
- the diameter of the roll used for bending and unbending is not particularly limited, but is preferably 300 to 2000 mm.
- ⁇ Cooling stop temperature 150°C or less>>
- the cooling stop temperature is 150° C. or lower. This fully completes the martensite transformation. If the cooling stop temperature is higher than 150°C, the untransformed austenite does not transform into martensite, the amount of retained austenite becomes excessive, and good part strength and stretch flangeability cannot be obtained.
- the cold-rolled sheet cooled to the cooling stop temperature may be further cooled to room temperature.
- the cooling rate from the cooling stop temperature to room temperature is not particularly limited.
- the cooling method is also not particularly limited, and any method can be adopted, such as gas jet cooling, mist cooling, water cooling, air cooling, and the like.
- ⁇ Post-heating> The annealed (heated and cooled) cold-rolled sheet is then post-heated.
- metastable carbides that improve the delayed fracture resistance are precipitated in the martensite blocks generated during the cooling in the annealing described above.
- a high-strength steel sheet having a TS of 1180 MPa or more which is excellent in delayed fracture resistance while having good part strength, stretch-flangeability and bendability, can be obtained.
- the annealed cold-rolled sheet is subjected to post-heating at a temperature X (unit: ° C.), which is the highest temperature reached, and a holding time Y (unit: s) at temperature X-10 ° C. or higher. It is carried out under the conditions satisfying the following formula 1.
- a temperature X unit: ° C.
- Y unit: s
- ratio p the ratio of the number of martensite blocks in which metastable carbides are present
- Formula 1 8000 ⁇ (273+X) ⁇ (20+Log(Y/3600)) ⁇ 12000
- variable part Z (273+X) ⁇ (20+Log(Y/3600))" in Equation 1 above is hereinafter referred to as "variable part Z" for convenience.
- the value of the variable part Z is 8000 or more, preferably 8500 or more, and more preferably 9000 or more, because the ratio p is high.
- the value of the variable part Z is 12,000 or less, preferably 11,500 or less, and more preferably 11,000 or less, because the ratio p is high.
- the temperature X (unit: °C) preferably satisfies Formula 2 below. This increases the metastable carbide number density (number density n) in the martensite block where metastable carbides are present.
- Formula 2 100 ⁇ X ⁇ 400
- the temperature X is preferably 100° C. or higher, more preferably 120° C. or higher, and even more preferably 150° C. or higher, because the number density n increases.
- the temperature X is preferably 400° C. or lower, more preferably 380° C. or lower, and even more preferably 350° C. or lower.
- the high-strength steel sheet of the present invention is obtained by the production method of the present invention.
- the obtained high-strength steel sheet of the present invention is a plated steel sheet having a plated layer.
- the cold-rolled sheet may be plated.
- the plating treatment for example, hot dip galvanizing treatment (treatment for forming a hot dip galvanized layer), alloying hot dip galvanizing treatment (alloying hot dip galvanizing by performing alloying treatment after hot dip galvanizing treatment processing to form a layer) and the like.
- An electroplating layer may be formed by an electroplating process. The plating treatment is performed, for example, on the cold-rolled sheet staying in the temperature range T1 (Ms° C. or higher and 700° C. or lower).
- the hot-dip galvanizing treatment When the hot-dip galvanizing treatment is performed, it is preferable to immerse the cold-rolled sheet in a galvanizing bath at 440 to 500° C., and then adjust the coating amount of the coating layer by gas wiping or the like.
- the amount of Al in the zinc plating bath is preferably 0.10-0.23% by mass.
- the hot-dip galvanizing treatment is preferably carried out during residence in the above-described temperature range T1 (Ms° C. or higher and 700° C. or lower) during annealing.
- the temperature of the alloying treatment is too low, the Zn—Fe alloying rate becomes excessively slow, which may impair the productivity.
- the temperature of the alloying treatment is too high, untransformed austenite may transform into pearlite and the TS may decrease.
- Skin pass rolling may be performed after the plating treatment.
- the rolling reduction in skin pass rolling is preferably 0.05% or more from the viewpoint of increasing the yield strength.
- the upper limit of the rolling reduction is not particularly limited, it is preferably 1.50% from the viewpoint of productivity.
- Skin-pass rolling may be performed online or offline.
- the skin pass with the target rolling reduction may be performed at once, or may be performed in several steps.
- the obtained cold-rolled sheets were subjected to annealing and post-heating under the conditions shown in Table 3 below to obtain steel sheets.
- the heating time at the heating temperature was 200 seconds.
- the bending and unbending processing was performed in the temperature range T2 and the temperature range T3.
- ⁇ Plating treatment Some of the cold-rolled sheets were subjected to hot-dip galvanizing treatment during retention in the temperature range T1 (Ms°C or higher and 700°C or lower) to form a coating layer (hot-dip galvanizing layer) on both sides. . That is, a hot-dip galvanized steel sheet (GI) was obtained. A hot-dip galvanizing bath (bath temperature: 470° C.) containing 0.20% by mass of Al and the balance being Zn and unavoidable impurities was used for the hot-dip galvanizing treatment. The adhesion amount per side of the hot-dip galvanized layer was about 45 g/m 2 . The composition of the formed hot-dip galvanized layer contained 0.1 to 1.0% by mass of Fe and 0.2 to 1.0% by mass of Al, with the balance being Fe and unavoidable impurities. .
- Another part of the cold-rolled sheet is subjected to alloying hot-dip galvanizing treatment while staying in the temperature range T1 (Ms ° C. or higher and 700 ° C. or lower) to obtain a coating layer (alloyed hot-dip zinc plating layer) was formed. That is, an alloyed hot-dip galvanized steel sheet (GA) was obtained.
- a hot dip galvanizing bath bath temperature: 470° C.
- the alloying treatment was performed at 550°C.
- the amount of the alloyed hot-dip galvanized layer deposited on one side was about 45 g/m 2 .
- the composition of the galvannealed layer thus formed contained 7 to 15% by mass of Fe and 0.1 to 1.0% by mass of Al, with the balance being Fe and unavoidable impurities.
- GI when a hot-dip galvanized layer is formed
- GA when an alloyed hot-dip galvanized layer is formed
- CR when a galvannealed layer is not formed
- Type in Table 3 below. described in the column.
- hot-dip galvanized steel sheets (GI) and alloyed hot-dip galvanized steel sheets (GA) are also simply referred to as “steel sheets”.
- a bending test was performed in accordance with JIS Z 2248. Specifically, a strip-shaped test piece having a width of 30 mm and a length of 100 mm was taken from the obtained steel sheet so that the direction parallel to the rolling direction of the steel sheet was the axial direction of the bending test. A 90° V bending test was performed using the sampled test piece under the conditions of an indentation load of 100 kN and a pressing holding time of 5 seconds. The maximum bending radius R at which the value (R/t) obtained by dividing the bending radius R by the plate thickness t is 5 or less (for example, when the plate thickness t is 1.4 mm, the bending radius R is 7.0 mm). A bending test was performed on two specimens.
- ⁇ Delayed fracture test A strip-shaped test piece having a width of 70 mm and a length of 16 mm was taken from the obtained steel sheet so that the direction perpendicular to the rolling direction of the steel sheet was the mechanically ground end face. Bending deformation was applied to the sampled test piece so that a stress equivalent to 800 MPa was applied to the central portion by four-point bending. Next, the bending-deformed test piece was immersed in a 0.1% by mass ammonium thiocyanate solution at 25° C. whose pH was adjusted to 5.0 using a McIlvain buffer. After that, the test piece in this solution was observed to confirm the presence or absence of cracks.
- the evaluation results of delayed fracture resistance were good in the order of (i), (ii), (iii) and (iv) below.
- the proportion p is 2% or more and less than 20% and the number density n is less than 1 ⁇ 10 6 /mm
- the proportion p is 2% or more and less than 20% and the number density n is 1 ⁇ 10 6 pcs/mm or more
- Proportion p is 20% or more and less than 30%
- Proportion p is 30% or more
- the steel sheets of 2-6, 8-10 and 17-20 were insufficient in at least one of tensile strength, part strength, stretch flange formability, bendability and delayed fracture resistance.
- the obtained cold-rolled steel was subjected to annealing and post-heating under the conditions shown in Table 5 below to obtain steel sheets.
- the heating time at the heating temperature was 200 seconds.
- the bending and unbending processing was performed in the temperature range T2 and the temperature range T3.
- a metal electroplating treatment was performed as a metal plating treatment (pre-annealing plating treatment) to form an Fe-based metal plating layer or a Ni-based metal plating layer.
- a metal plating treatment pre-annealing plating treatment
- Fe when the Fe-based metal plating layer is formed
- Ni when the Ni-based metal plating layer is formed
- - when the metal plating treatment is not performed
- - in Table 5 below. described in the column of "metal plating treatment”.
- a sulfuric acid bath bath temperature: 50° C., pH: 2.0
- a sulfuric acid bath bath temperature: 50° C., pH: 2.0
- Electrolytic treatment was carried out in an electroplating bath with the cold-rolled sheet as the cathode and the iridium oxide electrode as the anode at a current density of 45 A/dm 2 .
- the adhesion amount of the formed metal plating layer was controlled by adjusting the energization time.
- ⁇ Plating treatment Some of the cold-rolled sheets were subjected to hot-dip galvanizing treatment during retention in the temperature range T1 (Ms°C or higher and 700°C or lower) to form a coating layer (hot-dip galvanizing layer) on both sides. . That is, a hot-dip galvanized steel sheet (GI) was obtained. A hot-dip galvanizing bath (bath temperature: 470° C.) containing 0.20% by mass of Al and the balance being Zn and unavoidable impurities was used for the hot-dip galvanizing treatment. The adhesion amount per side of the hot-dip galvanized layer was about 45 g/m 2 . The composition of the formed hot-dip galvanized layer contained 0.1 to 1.0% by mass of Fe and 0.2 to 1.0% by mass of Al, with the balance being Fe and unavoidable impurities. .
- Another part of the cold-rolled sheet is subjected to alloying hot-dip galvanizing treatment while staying in the temperature range T1 (Ms ° C. or higher and 700 ° C. or lower) to obtain a coating layer (alloyed hot-dip zinc plating layer) was formed. That is, an alloyed hot-dip galvanized steel sheet (GA) was obtained.
- a hot dip galvanizing bath bath temperature: 470° C.
- the alloying treatment was performed at 550°C.
- the amount of the alloyed hot-dip galvanized layer deposited on one side was about 45 g/m 2 .
- the composition of the galvannealed layer thus formed contained 7 to 15% by mass of Fe and 0.1 to 1.0% by mass of Al, with the balance being Fe and unavoidable impurities.
- GI when a hot-dip galvanized layer is formed
- GA when an alloyed hot-dip galvanized layer is formed
- CR when a galvannealed layer is not formed. described in the column.
- hot-dip galvanized steel sheets (GI) and alloyed hot-dip galvanized steel sheets (GA) are also simply referred to as “steel sheets”.
- the obtained steel plate was subjected to a tensile test and a hole expansion test in the same manner as in Test Example 1, and the yield strength (YS), tensile strength (TS), yield ratio (YR), and total elongation (El) were measured. and the hole expansion ratio ( ⁇ ) were determined.
- the obtained steel plate was subjected to a bending test and a delayed fracture test in the same manner as in Test Example 1 to evaluate bendability and delayed fracture resistance. All the results are shown in Table 6 below.
- FIG. 2A is a perspective view showing a state in which the test piece T1 is subjected to 90° bending.
- FIG. 2B is a perspective view showing a state in which the test piece T1 is subjected to orthogonal bending.
- D1 indicates the width direction (C direction) and D2 indicates the rolling direction (L direction).
- the test piece T1 was subjected to 90° bending (primary bending) with a radius of curvature/plate thickness of 4.2. More specifically, as shown in FIG. 2A, a punch B1 was pressed under the following conditions into a test piece T1 placed on a die A1 having a V-groove. Next, the test piece T1 was subjected to orthogonal bending (secondary bending). More specifically, as shown in FIG. 2B, a punch B2 was pressed into the test piece T1 placed on the support roll A2 under the following conditions.
- the stroke at the maximum load was obtained from the stroke-load curve obtained when orthogonal bending was applied. 90° bending and orthogonal bending were performed three times, and the average value of three strokes at maximum load was obtained as SF max (unit: mm). When the obtained SF max satisfies the following condition A, it was determined that the fracture resistance (resistance to bending fracture) at the time of collision is excellent.
- An axial crush test was performed as follows. First, a test piece of 150 mm ⁇ 100 mm was cut from the obtained steel plate by shearing. The 150 mm side of the test piece is a side parallel to the rolling direction (L direction) of the steel plate. Next, the test piece is molded (bent) to a depth of 40 mm using a mold with a punch shoulder radius of 5.0 mm and a die shoulder radius of 5.0 mm. A hat-shaped member 10 was fabricated as shown in FIGS. 3A and 3B. A test piece having a size of 80 mm ⁇ 100 mm was cut out from the obtained steel plate, separately from the test piece for the hat-shaped member 10 , and used as the flat plate 20 .
- FIGS. 3A and 3B The hat-shaped member 10 and the flat plate 20 were spot-welded to produce a specimen 30 as shown in FIGS. 3A and 3B.
- 3A is a front view of test body 30, and
- FIG. 3B is a perspective view of test body 30.
- FIG. 3B the spot-welded portions 40 were positioned such that the distance between the end portion of the specimen 30 and the spot-welded portions 40 was 10 mm, and the distance between adjacent spot-welded portions 40 was 20 mm.
- FIG. 3C is a perspective view showing a state in which the specimen 30 is subjected to an axial crush test. As shown in FIG. 3C, one end of the specimen 30 was joined to the base plate 50 by TIG welding.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Mechanical Engineering (AREA)
- Thermal Sciences (AREA)
- Physics & Mathematics (AREA)
- Crystallography & Structural Chemistry (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- Oil, Petroleum & Natural Gas (AREA)
- Heat Treatment Of Sheet Steel (AREA)
- Coating With Molten Metal (AREA)
Abstract
Description
そのため、車体強度の増加を目的として、自動車キャビンの骨格を形成する主要な構造部品については、引張強さ(TS)が1180MPa以上の高強度鋼板(例えば、特許文献1)を適用する事例が増加している。
自動車用鋼板については、プレス時や組付け時に応力が負荷され、その後、環境から水素が侵入するリスクがあるため、良好な耐遅れ破壊特性が要求される。
[1]鋼板を備え、上記鋼板が、質量%で、C:0.090%以上0.390%以下、Si:0.01%以上2.00%以下、Mn:2.00%以上4.00%以下、P:0.100%以下、S:0.0200%以下、Al:1.000%以下、N:0.0100%以下、および、O:0.0100%以下を含有し、残部がFeおよび不可避的不純物からなる成分組成と、ミクロ組織と、を有し、上記ミクロ組織において、マルテンサイトの面積率が、70%以上であり、フェライトの面積率が、10%以下であり、残留オーステナイトの面積率が、10%以下であり、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合が、2%以上である、高強度鋼板。
[2]上記準安定炭化物が存在するマルテンサイトブロックにおける上記準安定炭化物の数密度が、1×10⁶個/mm2以上である、上記[1]に記載の高強度鋼板。
[3]上記成分組成は、更に、質量%で、Ti:0.200%以下、Nb:0.200%以下、V:0.200%以下、Ta:0.10%以下、W:0.10%以下、B:0.0100%以下、Cr:1.00%以下、Mo:1.00%以下、Ni:1.00%以下、Co:0.010%以下、Cu:1.00%以下、Sn:0.200%以下、Sb:0.200%以下、Ca:0.0100%以下、Mg:0.0100%以下、REM:0.0100%以下、Zr:0.100%以下、Te:0.100%以下、Hf:0.10%以下、および、Bi:0.200%以下からなる群から選ばれる少なくとも1種の元素を含有する、上記[1]または[2]に記載の高強度鋼板。
[4]上記鋼板は、表層として、軟質層を有し、上記表層は、上記鋼板の表面から板厚方向に200μmまでの部分であり、上記軟質層は、上記鋼板の板厚1/4位置のビッカース硬さに対して、ビッカース硬さが85%以下の部分である、上記[1]~[3]のいずれかに記載の高強度鋼板。
[5]上記軟質層の板厚方向深さ1/4位置におけるナノ硬さを、50μm×50μmの範囲内の300点以上で測定するとき、測定点の総数に対する、ナノ硬さが7.0GPa以上である測定点の割合rが、0.10以下である、上記[4]に記載の高強度鋼板。
[6]上記軟質層の板厚方向深さ1/4位置におけるナノ硬さの標準偏差σAが、1.8GPa以下であり、上記軟質層の板厚方向深さ1/2位置におけるナノ硬さの標準偏差σBが、2.2GPa以下である、上記[4]または[5]に記載の高強度鋼板。
[7]上記鋼板の表面に、更に、焼鈍前めっき層としての金属めっき層を有する、上記[1]~[6]のいずれかに記載の高強度鋼板。
[8]上記鋼板の表面に、更に、めっき層を有する、上記[1]~[6]のいずれかに記載の高強度鋼板。
[9]上記金属めっき層の表面に、更に、めっき層を有する、上記[7]に記載の高強度鋼板。
[10]上記[1]~[3]のいずれかに記載の高強度鋼板を製造する方法であって、上記[1]または[3]に記載の成分組成を有する鋼スラブに、熱間圧延、酸洗および冷間圧延を施すことにより冷延板を得て、上記冷延板に、焼鈍および後加熱を施し、上記焼鈍では、上記冷延板を、800℃以上の加熱温度で加熱し、次いで、150℃以下の冷却停止温度まで冷却し、ただし、上記冷却において、Ms℃超700℃以下の温度域T1における滞留時間t1が、1000s以下であり、Ms-80℃以上Ms℃以下の温度域T2における第1平均冷却速度v1が、1.0℃/s以上40.0℃/s以下であり、150℃以上Ms-80℃未満の温度域T3における第2平均冷却速度v2が、0.3℃/s以上上記第1平均冷却速度v1未満であり、上記後加熱を、最高到達温度である温度Xと、上記温度X-10℃以上での保持時間Yとが下記式1を満たす条件で実施する、高強度鋼板の製造方法。
式1:8000≦(273+X)×(20+Log(Y/3600))≦12000
ただし、上記温度Xの単位は℃であり、上記保持時間Yの単位はsである。
[11]上記温度Xが、下記式2を満たす、上記[10]に記載の高強度鋼板の製造方法。
式2:100≦X≦400
[12]上記焼鈍では、上記加熱温度での加熱を、露点が-30℃以上の雰囲気下で実施することにより、上記冷延板の表層に、軟質層を形成し、上記表層は、上記冷延板の表面から板厚方向に200μmまでの部分であり、上記軟質層は、上記冷延板の板厚1/4位置のビッカース硬さに対して、ビッカース硬さが85%以下の部分である、上記[10]または[11]に記載の高強度鋼板の製造方法。
[13]上記冷延板に、上記焼鈍を施す前に、金属めっき処理を実施して、上記冷延板の表面に、焼鈍前めっき層としての金属めっき層を形成する、上記[10]~[12]のいずれかに記載の高強度鋼板の製造方法。
[14]上記焼鈍において、上記冷延板に、めっき処理を施して、めっき層を形成する、上記[10]~[13]のいずれかに記載の高強度鋼板の製造方法。
本発明の高強度鋼板は、鋼板(下地鋼板)を有し、この鋼板が後述する成分組成およびミクロ組織を有する。
本発明の高強度鋼板を、例えば、自動車の構造部材に適用することにより、車体の軽量化による燃費向上を図ることができ、産業上の利用価値は極めて大きい。
部品強度に優れるとは、後述する引張試験により求める降伏比(YR)が65%以上であることを意味する。
伸びフランジ性に優れるとは、後述する穴広げ試験により求める穴広げ率(λ)が30%以上であることを意味する。
曲げ性に優れるとは、後述する曲げ試験において、5つの試験片のいずれにも亀裂が発生しない場合を意味する。
耐遅れ破壊特性に優れるとは、後述する遅れ破壊試験において、TSが1180MPa以上1700MPa未満の場合は48時間が経過した時点、TSが1700MPa以上の場合は24時間が経過した時点で、割れが確認されないことを意味する。
まず、本発明の高強度鋼板を構成する鋼板(下地鋼板)について説明する。
鋼板は、例えば、後述する後加熱を経た後の冷延板である。
鋼板の板厚は、特に限定されず、通常、0.3mm以上2.8mm以下である。
鋼板の成分組成(以下、便宜的に、「本発明の成分組成」ともいう)を説明する。
本発明の成分組成における「%」は、特に明記しない限り「質量%」を意味する。
Cは、鋼の重要な基本成分の1つであり、特に本発明においては、マルテンサイトおよびフェライトの面積率に影響する。
C含有量が少なすぎると、マルテンサイトの面積率が減少し、1180MPa以上のTSを実現することが困難になる。このため、C含有量は、0.090%以上であり、0.100%以上が好ましく、0.110%以上がより好ましい。
一方、C含有量が多すぎると、残留オーステナイトが過度に増加し、打ち抜き時に残留オーステナイトから生成するマルテンサイトの硬度が大きく上昇する。その結果、穴広げ時の亀裂進展が促進され、穴広げ率が低下して、伸びフランジ性が低下する。また、曲げ性も低下する。このため、C含有量は、0.390%以下であり、0.360%以下が好ましく、0.350%以下はより好ましい。
Siは、マルテンサイト中のセメンタイトの析出抑制や固溶強化によって、鋼板の強度を上昇させる。この効果を得るため、Si含有量は、0.01%以上であり、0.20%以上が好ましく、0.30%以上がより好ましい。
一方、Si含有量が多すぎると、フェライトの面積率が過剰となり、フェライトとマルテンサイトとの界面での打ち抜き時および穴広げ時のボイドの生成が増加する。その結果、穴広げ率が低下して、伸びフランジ性が低下する。また、部品強度および曲げ性が劣化する。このため、Si含有量は、2.00%以下であり、1.50%以下が好ましく、1.30%以下がより好ましい。
Mnは、鋼の重要な基本成分の1つであり、特に本発明においては、マルテンサイトの面積率に影響する。
Mn含有量が少なすぎると、マルテンサイトの面積率が減少し、1180MPa以上のTSを実現することが困難になる。このため、Mn含有量は、2.00%以上であり、2.20%以上が好ましく、2.50%以上がより好ましい。
一方、Mn含有量が多すぎると、オーステナイトが安定化し、残留オーステナイトが過度に増加し、打ち抜き時に残留オーステナイトから生成するマルテンサイトの硬度が大きく上昇する。その結果、穴広げ時の亀裂進展が促進され、穴広げ率が低下して、伸びフランジ性が低下する。このため、Mn含有量は、4.00%以下であり、3.80%以下が好ましく、3.60%以下がより好ましい。
Pは、旧オーステナイト粒界に偏析して粒界を脆化させるため、鋼板の極限変形能を低下させる。これにより、穴広げ率が低下して、伸びフランジ性が低下する。また、曲げ性も低下する。このため、P含有量は、0.100%以下であり、0.070%以下が好ましく、0.050%以下がより好ましく、0.020%以下が更に好ましい。
P含有量の下限は、特に限定されない。もっとも、Pは、固溶強化元素であり、鋼板の強度を上昇させる。このため、P含有量は、0.001%以上が好ましく、0.002%以上がより好ましい。
Sは、硫化物として存在し、鋼板の極限変形能を低下させる。これにより、穴広げ率が低下して、伸びフランジ性が低下する。また、曲げ性も低下する。このため、S含有量は、0.0200%以下であり、0.0100%以下が好ましく、0.0050%以下がより好ましく、0.0020%以下が更に好ましい。
S含有量の下限は、特に限定されないが、生産技術上の制約から、0.0001%が好ましい。
Alは、十分な脱酸を行ない、鋼中介在物を低減する。
もっとも、Al含有量が多すぎると、フェライトが多量に生成し、穴広げ率が低下して、伸びフランジ性が低下する。このため、Al含有量は、1.000%以下であり、0.500%以下が好ましく、0.100%以下がより好ましい。
一方、安定して脱酸を行なうためには、Al含有量は、0.010%以上が好ましく、0.015%以上がより好ましく、0.020%以上が更に好ましい。
Nは、窒化物として存在し、鋼板の極限変形能を低下させる。これにより、穴広げ率が低下して、伸びフランジ性が低下する。また、曲げ性も低下する。このため、N含有量は、0.0100%以下であり、0.0070%以下が好ましく、0.0050%以下がより好ましい。
N含有量の下限は、特に限定されないが、生産技術上の制約から、0.0001%が好ましい。
Oは、酸化物として存在し、鋼板の極限変形能を低下させる。これにより、穴広げ率が低下して、伸びフランジ性が低下する。また、曲げ性も低下する。このため、O含有量は、0.0100%以下であり、0.0050%以下が好ましく、0.0030%以下がより好ましく、0.0020%以下が更に好ましい。
O含有量の下限は、特に限定されないが、生産技術上の制約から、0.0001%が好ましい。
本発明の成分組成は、更に、質量%で、以下に記載する元素からなる群から選ばれる少なくとも1種の元素を含有してもよい。
Ti、NbおよびVの含有量は、それぞれ、0.200%以下が好ましく、0.100%以下がより好ましく、0.080%以下が更に好ましい。各元素の含有量がこの範囲であれば、粗大な析出物や介在物が多量に生成せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Ti、NbおよびVの含有量の下限は、特に限定されない。もっとも、Ti、NbおよびVは、後述する熱間圧延または焼鈍の際に、微細な炭化物、窒化物または炭窒化物を形成することによって、鋼板の強度を上昇させる。このため、Ti、NbおよびVを添加する場合、これらの元素の添加効果を得る観点から、Ti、NbおよびVの含有量は、それぞれ、0.001%以上が好ましく、0.005%以上がより好ましく、0.010%以上が更に好ましい。
TaおよびWの含有量は、それぞれ、0.10%以下が好ましく、0.08%以下がより好ましく、0.04%以下が更に好ましい。各元素の含有量がこの範囲であれば、粗大な析出物や介在物が多量に生成せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、TaおよびWの含有量の下限は、特に限定されない。もっとも、TaおよびWは、後述する熱間圧延または焼鈍の際に、微細な炭化物、窒化物または炭窒化物を形成することによって、鋼板の強度を上昇させる。このため、TaおよびWを添加する場合、これらの元素の添加効果を得る観点から、TaおよびWの含有量は、それぞれ、0.01%以上が好ましい。
B含有量は、0.0100%以下が好ましく、0.0080%以下がより好ましく、0.0050%以下が更に好ましい。B含有量がこの範囲であれば、後述する熱間圧延の際に鋼板の内部に割れが生成せず、鋼板の極限変形能が低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、B含有量の下限は、特に限定されない。もっとも、Bは、後述する焼鈍の際に、オーステナイト粒界に偏析し、焼入れ性を向上させる。このため、Bを添加する場合、Bの添加効果を得る観点から、B含有量は、0.0003%以上が好ましく、0.0005%以上がより好ましく、0.0010%以上が更に好ましい。
Cr、MoおよびNiは、それぞれ、1.00%以下が好ましく、0.90%以下がより好ましく、0.80%以下が更に好ましい。各元素の含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Cr、MoおよびNiの含有量の下限は、特に限定されない。もっとも、Cr、MoおよびNiは、焼入れ性を向上させる。このため、Cr、MoおよびNiを添加する場合、これらの元素の添加効果を得る観点から、Cr、MoおよびNiの含有量は、それぞれ、0.01%以上が好ましく、0.02%以上がより好ましく、0.03%以上が更に好ましい。
Co含有量は、0.010%以下が好ましく、0.008%以下がより好ましく、0.006%以下が更に好ましい。Co含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Co含有量の下限は、特に限定されない。もっとも、Coは、焼入れ性を向上させる。このため、Coを添加する場合、Coの添加効果を得る観点から、Co含有量は、0.001%以上が好ましく、0.002%以上がより好ましく、0.004%以上が更に好ましい。
Cu含有量は、1.00%以下が好ましく、0.80%以下がより好ましく、0.30%以下が更に好ましい。Cu含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Cuの含有量の下限は、特に限定されない。もっとも、Cuは、焼入れ性を向上させる。このため、Cuを添加する場合、Cuの添加効果を得る観点から、Cu含有量は、0.01%以上が好ましく、0.03%以上がより好ましく、0.05%以上が更に好ましい。
Sn含有量は、0.200%以下が好ましく、0.100%以下がより好ましく、0.050%以下が更に好ましい。Sn含有量がこの範囲であれば、鋳造または後述する熱間圧延の際に、鋼板の内部に割れが生成せず、鋼板の極限変形能が低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Sn含有量の下限は、特に限定されない。もっとも、Snは、焼入れ性を向上させる。このため、Snを添加する場合、Snの添加効果を得る観点から、Sn含有量は、0.001%以上が好ましく、0.004%以上がより好ましく、0.008%以上が更に好ましい。
Sb含有量は、0.200%以下が好ましく、0.100%以下がより好ましく、0.050%以下が更に好ましい。Sb含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Sb含有量の下限は、特に限定されない。もっとも、Sbは、表層軟化厚みを制御して、強度調整を可能にする。このため、Sbを添加する場合、Sbの添加効果を得る観点から、Sb含有量は、0.001%以上が好ましく、0.003%以上がより好ましく、0.007%以上が更に好ましい。
Ca、MgおよびREM(希土類金属)の含有量は、それぞれ、0.0100%以下が好ましく、0.0050%以下がより好ましく、0.0030%以下が更に好ましい。各元素の含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Ca、MgおよびREMの含有量の下限は、特に限定されない。もっとも、Ca、MgおよびREMは、窒化物や硫化物の形状を球状化し、鋼板の極限変形能を向上させる。このため、Ca、MgおよびREMを添加する場合、これらの元素の添加効果を得る観点から、Ca、MgおよびREMの含有量は、それぞれ、0.0002%以上が好ましく、0.0005%以上がより好ましく、0.0010%以上が更に好ましい。
ZrおよびTeの含有量は、それぞれ、0.100%以下が好ましく、0.080%以下がより好ましく、0.050%以下が更に好ましい。各元素の含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、ZrおよびTeの含有量の下限は、特に限定されない。もっとも、ZrおよびTeは、窒化物や硫化物の形状を球状化し、鋼板の極限変形能を向上させる。このため、ZrおよびTeを添加する場合、これらの元素の添加効果を得る観点から、ZrおよびTeの含有量は、それぞれ、0.001%以上が好ましく、0.003%以上がより好ましく、0.007%以上が更に好ましい。
Hf含有量は、0.10%以下が好ましく、0.08%以下がより好ましく、0.05%以下が更に好ましい。Hf含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Hf含有量の下限は、特に限定されない。もっとも、Hfは、窒化物や硫化物の形状を球状化し、鋼板の極限変形能を向上させる。このため、Hfを添加する場合、Hfの添加効果を得る観点から、Hf含有量は、0.01%以上が好ましく、0.02%以上がより好ましい。
Bi含有量は、0.200%以下が好ましく、0.100%以下がより好ましく、0.030%以下が更に好ましい。Bi含有量がこの範囲であれば、粗大な析出物や介在物が増加せず、鋼板の極限変形能は低下しないため、伸びフランジ性(穴広げ率)がより優れる。また、曲げ性もより優れる。
一方、Bi含有量の下限は、特に限定されない。もっとも、Biは、偏析を軽減する元素である。このため、Biを添加する場合、Biの添加効果を得る観点から、Bi含有量は、0.001%以上が好ましく、0.002%以上がより好ましく、0.004%以上が更に好ましい。
本発明の成分組成における残部は、Feおよび不可避的不純物からなる。
上述したTi、Nb、V、Ta、W、B、Cr、Mo、Ni、Co、Cu、Sn、Sb、Ca、Mg、REM、Zr、Te、HfおよびBiについて、各元素の含有量が上述した好適範囲の下限値未満である場合、本発明の効果を害することがないため、その元素は、不可避的不純物として扱う。
次に、鋼板のミクロ組織(以下、便宜的に「本発明のミクロ組織」ともいう)を説明する。
マルテンサイトを主相とすることにより、1180MPa以上のTSを実現できる。このため、マルテンサイトの面積率は、70%以上であり、75%以上が好ましく、80%以上がより好ましく、85%以上が更に好ましい。
上限は特に限定されず、マルテンサイトの面積率が100%であっても、この効果は得られる。
マルテンサイトは、下部ベイナイト、後述する焼鈍において実施する冷却中に自己焼戻しを生じたマルテンサイト、後述する後加熱により焼戻されたマルテンサイト等を含む。
マルテンサイトの観察位置は、後述するように、鋼板の板厚の1/4位置である。
フェライトを少なくすることにより、良好な伸びフランジ性および曲げ性が得られる。このため、フェライトの面積率は、10%以下であり、8%以下が好ましく、5%以下がより好ましく、3%以下が更に好ましい。
下限は特に限定されず、フェライトの面積率が0%であっても、この効果は得られる。
フェライトは、アロトリオモルフフェライト、イディオモルフフェライト、ウィドマンステッテンフェライト、上部ベイナイト等を含む。
フェライトの観察位置は、後述するように、鋼板の板厚の1/4位置である。
まず、鋼板から、その圧延方向に平行な板厚断面(板厚1/4位置のL断面)が観察面となるように、サンプルを切り出す。サンプルの観察面を、ダイヤモンドペーストを用いて鏡面研磨し、その後、コロイダルシリカを用いて仕上げ研磨を施し、更に、1体積%ナイタールを用いてエッチングすることにより、組織を現出させる。
次いで、サンプルの観察面を、加速電圧10kVの条件で、走査型電子顕微鏡(SEM)を用いて3000倍の倍率で観察し、3視野分のSEM画像を得る。
得られたSEM画像から、Adobe Photoshop(Adobe Systems社製)を用いて、各組織の面積率を算出する。具体的には、各組織の面積を測定面積で除して得られる値を、各組織の面積率とする。各組織の面積率を3視野分算出し、それらの平均値を、各組織の面積率とする。
SEM画像において、フェライトは灰色を呈する平坦な組織であり、マルテンサイトは内部に微細な凹凸を有する階層構造を持つ組織であり、両者を互いに識別できる。
残留オーステナイトを少なくすることにより、良好な部品強度および伸びフランジ性が得られる。このため、残留オーステナイトの面積率は、10%以下であり、8%以下が好ましく、5%以下がより好ましく、4%以下が更に好ましい。
下限は特に限定されず、残留オーステナイトの面積率が0%であっても、この効果は得られる。
まず、鋼板を、その板厚1/4位置(鋼板表面から深さ方向で板厚の1/4に相当する位置)が測定面となるように研削し、その後、化学研磨により更に0.1mm研磨し、サンプルを得る。
サンプルの測定面について、X線回折装置により、CoのKα線源を用いて、fcc鉄(オーステナイト)の(200)面、(220)面および(311)面、ならびに、bcc鉄の(200)面、(211)面および(220)面の積分反射強度を測定する。
bcc鉄の各面の積分反射強度に対するfcc鉄の各面の積分反射強度の強度比を求める。9つの強度比の平均値を、残留オーステナイトの体積率とする。
残留オーステナイトの体積率を、残留オーステナイトの面積率とみなす。
マルテンサイトブロック中に析出した準安定炭化物によって、優れた部品強度、曲げ性、伸びフランジ性を保ちつつ、耐遅れ破壊特性が向上する。
この効果を得るためには、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合(「割合p」とも表記する)は、2%以上であり、5%以上が好ましく、10%以上がより好ましく、20%以上が更に好ましく、30%以上が特に好ましい。
割合pの上限は、特に限定されず、100%であってもよい。
準安定炭化物は、例えば、セメンタイト以外のFe炭化物(鉄系炭化物)であり、イプシロン(ε)炭化物、イータ(η)炭化物およびカイ(χ)炭化物からなる群から選ばれる少なくとも1種の炭化物が挙げられる。
まず、鋼板を、その板厚1/4位置(鋼板表面から深さ方向で板厚の1/4に相当する位置)が観察面となるように研削し、その後、電解研磨して、サンプルを作製する。作製したサンプルの観察面を、透過型電子顕微鏡(TEM)を用いて、加速電圧200kVの条件で、観察する。マルテンサイトの転位密度は、フェライトや残留オーステナイトよりも著しく高いので、TEMの明視野像において、ひずみのコントラストを観察することにより、互いに区別され、観察視野内のマルテンサイトを同定できる。
マルテンサイトブロックとは、階層構造をとるマルテンサイトの構成単位の1つであり、晶癖面が同じ、かつ、結晶方位が同じラスの集団である。TEMの明視野像では、マルテンサイト内においてブロック毎に回折コントラストが異なることから、パケットやラスなどの他の構成単位と区別でき、マルテンサイトブロックを同定できる。
マルテンサイトブロックの[100]方位から電子線を入射すると、母相マルテンサイトの電子回折図形が得られる。隣接するマルテンサイトブロックどうしは、ブロック境界を介して結晶方位が異なるので、明視野像でコントラストが異なることから、互いに区別される。
観察した単一のマルテンサイトブロックに炭化物が存在する場合、図1に示すように、母相マルテンサイト(α)の電子回折図形に加えて、炭化物の電子回折図形が得られる。
図1中、黒丸は、電子線が[100]方位から入射した場合における、母相マルテンサイトの電子回折斑点、白丸は、炭化物の電子回折斑点を示す。
図1における母相マルテンサイトの電子回折斑点間の距離D1と、炭化物の電子回折斑点間の距離D2とから、炭化物の面間隔dcと母相マルテンサイトの面間隔dmとの比dc/dmを、下記式3を用いて計算する。
式3:dc/dm=D1/D2
例えば、炭化物がセメンタイトである場合、距離D2は距離D1と等しい。このため、比dc/dmの値は、1である(D1/D2=dc/dm=1)。
一方、準安定炭化物(ε炭化物など)の距離D2は、セメンタイトよりも短いので、比dc/dm(=D1/D2)値は1よりも大きい。このため、準安定炭化物が存在する場合における比dc/dmの下限値を「1.020」とする。
なお、比dc/dmの上限については、ε炭化物の距離D2に基づいて、「1.150」と定める。
耐遅れ破壊特性がより優れるという理由から、マルテンサイトブロックにおける準安定炭化物の数密度が高いことが好ましい。これは、準安定炭化物の数密度が高いと、水素トラップ量がより大きくなるためと考えられる。
具体的には、準安定炭化物が存在するマルテンサイトブロックにおける準安定炭化物の数密度(「数密度n」とも表記する)は、1×10⁶個/mm2以上が好ましく、10×106個/mm2以上がより好ましく、100×106個/mm2以上が更に好ましい。
数密度nの上限は、特に限定されず、例えば10,000,000×106個/mm2であり、1,000,000×106個/mm2が好ましく、100,000×106個/mm2がより好ましく、10,000×106個/mm2が更に好ましい。
上述したTEMを用いた割合pの測定に際して、準安定炭化物が存在する単一のマルテンサイトブロックにおいて制限視野電子回折図形を取得し、準安定炭化物から得られた電子回折斑点を用いて、暗視野像を得る。暗視野像において、準安定炭化物は、白いコントラストを呈する。
単一のマルテンサイトブロック内部で300nm×300nmの領域を撮影し、準安定炭化物の個数を数える。なお、300nm×300nmの領域に、ブロック境界を介した隣接するマルテンサイトブロックが存在していても構わない。
準安定炭化物が存在するマルテンサイトブロックの面積を、制限視野電子回折図形を得た単一のマルテンサイトブロックの面積と定義する。隣接するマルテンサイトブロックどうしは、ブロック境界を介して結晶方位が異なるので、明視野像でコントラストが異なることから、互いに区別される。
上記の測定を3視野で行ない、準安定炭化物の個数を、準安定炭化物が存在するマルテンサイトブロックの面積で除した値(=準安定炭化物の個数/準安定炭化物が存在するマルテンサイトブロックの面積)を3視野分求める。それらの平均値を、準安定炭化物が存在するマルテンサイトブロックにおける準安定炭化物の数密度(数密度n)とする。
マルテンサイトブロックにおける準安定炭化物の円相当径の平均値が小さいほど、水素トラップ能が高まったり、遅れ破壊に寄与する転位移動を抑制したりするために、耐遅れ破壊特性がより優れる。
このため、マルテンサイトブロックにおける準安定炭化物の円相当径の平均値は、20nm以下が好ましく、5nm以下がより好ましい。
上述したTEMを用いた割合pの測定に際して、準安定炭化物が存在する単一のマルテンサイトブロックにおいて制限視野電子回折図形を取得し、準安定炭化物から得られた電子回折斑点を用いて、暗視野像を得る。暗視野像において、準安定炭化物は、白いコントラストを呈する。
単一のマルテンサイトブロック内部で300nm×300nmの領域の暗視野像を撮影し、画像処理を実施して、準安定炭化物が区別できるように二値化画像を得る。二値化画像を粒子解析することにより、全ての準安定炭化物粒子それぞれについて、円相当径を求める。準安定炭化物どうしが暗視野像において重なっている場合は、二値化画像に対して、Watershed法を用いた分割を実施する。
300nm×300nmの領域に存在する全ての準安定炭化物それぞれについて、円相当径を求める(3視野分)。3視野分の円相当径の平均値を求め、これを、マルテンサイトブロックにおける準安定炭化物の円相当径の平均値とする。
本発明のミクロ組織は、上述したマルテンサイト、フェライトおよび残留オーステナイト以外の組織(残部組織)を有していてもよい。
もっとも、残部組織の面積率は、本発明の効果が損なわれないという理由から、3%以下が好ましい。
残部組織としては、例えば、パーライト;フェライト中に析出したセメンタイトなどの炭化物;フェライト中に析出した合金炭窒化物;その他の鋼板の組織として公知の組織;等が挙げられる。
なお、マルテンサイト中に析出した準安定炭化物、および、マルテンサイト中に析出したセメンタイトなどの鉄系炭化物は、残部組織に含まれない。
本発明の高強度鋼板を構成する鋼板(下地鋼板)は、その表層に、軟質層を有することが好ましい。
プレス成形および衝突の際に、軟質層が曲げ割れ進展の抑制に寄与するため、曲げ性がより優れ、かつ、衝突時の耐破断性にも優れる。
軟質層は、脱炭層であり、より詳細には、鋼板(冷延板)の板厚1/4位置のビッカース硬さに対して、ビッカース硬さが85%以下の部分である。
鋼板の板厚1/4位置のビッカース硬さとは、鋼板の板厚1/4位置(鋼板の表面から深さ方向で板厚の1/4に相当する位置)の断面(鋼板の表面と平行な面)のビッカース硬さを意味する。
ビッカース硬さは、JIS Z 2244-1:2020に準拠して、荷重を10gfとして測定する。
軟質層の厚さは、3μm以上が好ましく、7μm以上がより好ましく、11μm以上が更に好ましい。
一方、軟質層の厚さは、150μm以下が好ましく、100μm以下がより好ましく、80μm以下が更に好ましい。
まず、ビッカース硬さ試験機を用いて、荷重を10gfとして、鋼板の表面から板厚方向に1μmの位置から、板厚方向に100μmの位置まで、1μm間隔で、ビッカース硬さを測定する。次いで、板厚中心まで、20μm間隔で、ビッカース硬さを測定する。
なお、鋼板の圧延方向に平行な断面(L断面)を、湿式研磨により平滑化してから、ビッカース硬さを測定する。
このように測定されるビッカース硬さが、鋼板の板厚1/4位置のビッカース硬さに対して85%以下である部分(領域)を軟質層と定義し、この部分(領域)の板厚方向の厚さを、軟質層の厚さ(単位:μm)として求める。
軟質層の板厚方向深さ1/4位置におけるナノ硬さを、50μm×50μmの範囲内の300点以上(例えば、512点)で測定する。このとき、測定点の総数に対する、ナノ硬さが7.0GPa以上である測定点の割合を「割合r」と呼ぶ。
割合rは、例えば0.20以下であり、0.15以下が好ましく、0.10以下がより好ましい。
割合rが小さいことは、硬質な組織(マルテンサイトなど)および介在物がミクロ組織に少ないことを意味する。ミクロ組織に硬質な組織および介在物が少ない場合、プレス成形および衝突の際に、ボイドの生成、ボイドの連結および亀裂の進展をより抑制できる。すなわち、曲げ性が更に優れ、かつ、衝突時の耐破断性がより優れる(後述するSFmaxの値が良好である)。
軟質層の板厚方向深さ1/4位置のナノ硬さの標準偏差を「標準偏差σA」と呼ぶ。
軟質層の板厚方向深さ1/2位置のナノ硬さの標準偏差を「標準偏差σB」と呼ぶ。
標準偏差σAは、例えば2.0GPa以下であり、1.8GPa以下が好ましく、1.7GPa以下がより好ましい。
標準偏差σBは、例えば2.5GPa以下であり、2.2GPa以下が好ましく、2.1GPa以下がより好ましい。
標準偏差σAおよび標準偏差σBが小さいことは、ミクロ組織における各組織の硬度差が小さいことを意味する。この場合、プレス成形および衝突の際に、ボイドの生成、ボイドの連結および亀裂の進展をより抑制できる。すなわち、曲げ性が更に優れ、かつ、衝突時の耐破断性がより優れる。
より詳細には、軟質層の板厚方向深さ1/4位置および1/2位置におけるナノ硬さは、以下のように求める。
まず、めっき層および/または金属めっき層(いずれも後述する)が鋼板の表面に形成されている場合は、めっき層および/または金属めっき層を剥離する。
その後、鋼板の表面から、軟質層の板厚方向深さ1/4位置(または1/2位置)まで機械研磨を実施し、次いで、ダイヤモンドおよびアルミナを用いたバフ研磨を実施し、更に、コロイダルシリカを用いた研磨を実施する。こうして、軟質層の板厚方向深さ1/4位置(または1/2位置)のL断面を得る。
次いで、Hysitron社のtribo-950を用い、バーコビッチ形状のダイヤモンド圧子により、荷重:500μN、測定領域:50μm×50μm、打点間隔:2μmの条件で、軟質層のL断面のナノ硬さを測定する。
本発明の高強度鋼板は、鋼板の表面上に、金属めっき層(「焼鈍前めっき層」ともいう)を備えてもよい。金属めっき層は、後述するめっき層とは異なる層である。
金属めっき層としては、金属電気めっき層が好ましい。
プレス成形および衝突の際に、金属めっき層が曲げ割れ発生の抑制に寄与するため、曲げ性がより優れ、かつ、衝突時の耐破断性にも優れる。
すなわち、金属めっき層としては、Feおよび不可避的不純物からなる成分組成を有する金属めっき層(以下、「Fe系金属めっき層」ともいう)が好ましい。
または、金属めっき層としては、Niおよび不可避的不純物からなる成分組成を有する金属めっき層(以下、「Ni系金属めっき層」ともいう)が好ましい。
Fe系金属めっき層の成分組成は、更に、B、C、P、N、O、Ni、Mn、Mo、Zn、W、Pb、Sn、Cr、VおよびCoからなる群から選ばれる少なくとも1種の元素を、合計10質量%以下の量で含んでいてもよい。Cを含む場合、C含有量は0.08質量%以下が好ましい。
一方、金属めっき層の付着量(片面あたり)は、上限は特に限定されないが、コストの観点から、60.0g/m2以下が好ましく、50.0g/m2以下がより好ましく、40.0g/m2以下が更に好ましく、30.0g/m2以下が特に好ましく、20.0g/m2以下が最も好ましい。
まず、金属めっき層が形成された鋼板を、10mm×15mmのサイズに切断してから、樹脂に埋め込み、埋め込みサンプルを得る。埋め込みサンプルの断面における任意の3か所を、走査型電子顕微鏡(SEM)を用いて、加速電圧15kVの条件で、金属めっき層の厚さに応じて倍率2000~10000倍で観察し、金属めっき層の厚さを測定する。3か所の厚さの平均値に、金属めっき層の金属元素(例えば、Fe)の比重を乗じることによって、金属めっき層の片面あたりの付着量に換算する。
本発明の高強度鋼板は、鋼板または金属めっき層の表面上に、めっき層を備えてもよい。めっき層は、上述した金属めっき層とは異なる層であり、後述するめっき処理によって形成される。
めっき層としては、特に限定されず、例えば、溶融めっき層、電気めっき層などが挙げられる。めっき層は、合金化されためっき層(合金化めっき層)であってもよい。
例えば、めっき層が溶融亜鉛めっき層または合金化溶融亜鉛めっき層である場合、一般的には、Fe:20質量%以下、Al:0.001~1.0質量%を含有し、更に、Pb、Sb、Si、Sn、Mg、Mn、Ni、Cr、Co、Ca、Cu、Li、Ti、Be、BiおよびREMからなる群から選ばれる少なくとも1種を合計で0~3.5質量%含有し、残部がZnおよび不可避的不純物からなる組成が挙げられる。
めっき層が溶融亜鉛めっき層である場合、めっき層中のFe含有量は、7質量%未満が好ましい。めっき層が合金化溶融亜鉛めっき層である場合、めっき層中のFe含有量は、7~20質量%が好ましく、7~15質量%がより好ましい。
まず、10質量%の塩酸水溶液1Lに、Feの腐食を抑制する腐食抑制剤(イビット700BK」(登録商標)、朝日化学工業社製)0.6gを添加し、処理液を得る。得られた処理液に、めっき層が形成された鋼板を供試材として浸漬し、めっき層を溶解させる。
めっき層の溶解前後で供試材の質量を測定することにより、供試材の質量減少量を求める。求めた質量減少量を、鋼板表面の面積(めっき層で被覆されていた部分の面積)で除することにより、めっき層の付着量(g/m2)を得る。
次に、本発明の高強度鋼板の製造方法(以下、便宜的に「本発明の製造方法」ともいう)を説明する。本発明の製造方法は、上述した本発明の高強度鋼板を製造する方法でもある。
本発明の製造方法においては、まず、上述した本発明の成分組成を有する鋼スラブに、熱間圧延、酸洗および冷間圧延を施すことにより、冷延板を得る。
鋼スラブは、マクロ偏析を防止するため、連続鋳造法で製造することが好ましいが、造塊法、薄スラブ鋳造法などの他の方法によっても製造できる。
なお、製造した鋼スラブを、室温まで冷却しないで温片のまま加熱炉に装入してもよいし、わずかに保熱した後に直ちに圧延(粗圧延)してもよい。
鋼スラブを粗圧延する際の温度(スラブ加熱温度)は、炭化物の溶解や圧延荷重の低減の観点から、1100℃以上が好ましい。一方、スケールロスの増大を防止するため、スラブ加熱温度は、1300℃以下が好ましい。
スラブ加熱温度は、鋼スラブの表面温度である。
スラブ加熱温度を低めにした場合は、熱間圧延におけるトラブルを防止する観点から、仕上げ圧延の前に、バーヒーターなどを用いて粗圧延板を加熱することが好ましい。
仕上げ圧延は、粗圧延板どうしを接合して連続的に実施してもよい。仕上げ圧延を実施する前に、粗圧延板を一旦巻き取ってもよい。
圧延荷重を低減するために、仕上げ圧延の一部または全部を、潤滑圧延としてもよい。潤滑圧延は、鋼板形状および材質を均一化する観点からも好ましい。潤滑圧延する際の摩擦係数は、0.10~0.25の範囲が好ましい。
なお、金属めっき処理(焼鈍前めっき処理)を実施する前に、上述した熱延板(酸洗後の熱延板を含む)および冷延板に、何らかの焼鈍が施されていてもよい。
金属めっき処理(焼鈍前めっき処理)は、後述する焼鈍を施す前の冷延板の表面(少なくとも片面)に、上述した金属めっき層(焼鈍前めっき層)を形成する処理である。
金属電気めっき処理に用いる電気めっき浴としては、硫酸浴、塩酸浴、両者の混合浴などを使用できる。形成される金属電気めっき層の付着量は、金属電気めっき処理の通電時間などによって調整できる。
電気めっき浴が含有する金属元素としては、例えば、Cr、Mn、Fe、Co、Ni、Cu、Ga、Ge、As、Ru、Rh、Pd、Ag、Cd、In、Sn、Sb、Os、Ir、Rt、Au、Hg、Ti、PbおよびBiからなる群から選ばれる少なくとも1種の元素が挙げられる。これらのうち、FeまたはNiが好ましい。
電気めっき浴中、これらの元素の合計含有量は、形成される金属めっき層中のこれらの元素の合計含有量が10質量%以下になる量が好ましい。
通電開始前の電気めっき浴中、Feイオン(Fe2+)またはNiイオン(Ni2+)の含有量は、0.5~2.0mol/Lが好ましい。
電気めっき浴は、更に、硫酸ナトリウム、硫酸カリウムなどの伝導度補助剤;キレート剤;pH緩衝剤;等を含有していてもよい。
電気めっき浴のpHは、水素発生による電流効率の低下を防ぐ観点から、1.0以上が好ましく、電気伝導度を考慮すると、3.0以下が好ましい。
電流密度は、生産性の観点から、10A/dm2以上が好ましく、形成される金属電気めっき層の付着量の制御を容易にする観点から、150A/dm2以下が好ましい。
冷延板を電気めっき浴に通板させる速度(通板速度)は、生産性の観点から、5mpm以上が好ましく、形成される金属電気めっき層の付着量を安定的に制御する観点から、150mpm以下が好ましい。
脱脂および水洗の方法としては、特に限定されず、通常の方法を使用できる。
酸洗には、硫酸、塩酸、硝酸、および、これらの混合物などの各種の酸液を使用できる。なかでも、硫酸、塩酸、または、これらの混合物が好ましい。酸液の濃度は、酸化皮膜の除去能力、過酸洗による表面欠陥の防止などを考慮すると、1~20質量%が好ましい。酸液には、消泡剤、酸洗促進剤、酸洗抑制剤などを添加してもよい。
次いで、得られた冷延板に、焼鈍を施す。
焼鈍では、概略的には、冷延板を、後述する加熱温度で加熱し、次いで、後述する冷却停止温度まで冷却する。
加熱温度が低すぎると、フェライトおよびオーステナイトの二相域での加熱になるため、マルテンサイトの面積率が低くなり、所望のTSが得られない。このため、加熱温度は、800℃以上であり、820℃以上が好ましい。
加熱温度の上限は、特に限定されないが、操業性等の観点から、950℃が好ましい。
加熱時間の上限は、特に限定されず、例えば、6000sであり、3000sが好ましい。
なお、「s」は、秒を意味する。
上述した加熱温度で冷延板を加熱する際の雰囲気の露点は、-30℃以上が好ましく、-20℃以上がより好ましく、-15℃以上が更に好ましく、-5℃以上が特に好ましい。これにより、冷延板の脱炭反応が促進され、上述した軟質層が形成されやすい。
一方、金属めっき層(焼鈍前めっき層)の表面酸化を好適に防ぎ、かつ、後述するめっき処理によって形成されるめっき層の密着性を良好にする観点から、この露点は、30℃以下が好ましい。
加熱後に冷却停止温度まで冷却される冷延板は、Ms℃以上700℃以下の温度域T1を経る。冷延板が温度域T1に滞留する時間(滞留時間t1)が長すぎると、フェライト変態が過度に生じ、フェライトの面積率が高くなり、良好な伸びフランジ性および曲げ性が得られない。
このため、滞留時間t1は、1000s以下であり、500s以下が好ましく、300s以下がより好ましい。
滞留時間t1の下限は、特に限定されないが、設備投資負担の軽減の観点から、1sが好ましく、5sがより好ましく、10sが更に好ましい。
温度域T1(Ms℃以上700℃以下)を経た冷延板は、次いで、Ms-80℃以上Ms℃未満の温度域T2を経る。冷延板を、温度域T2において、以下に説明する第1平均冷却速度v1で冷却することにより、Ms℃以下で生成したマルテンサイトからCが未変態オーステナイト中に分配される。
このため、第1平均冷却速度v1は、1.0℃/s以上であり、2.0℃/s以上が好ましく、3.0℃/s以上がより好ましい。
このため、第1平均冷却速度v1は、40.0℃/s以下であり、25.0℃/s以下が好ましく、20.0℃/s以下がより好ましい。
温度域T2を経た冷延板は、次いで、150℃以上Ms-80℃未満の温度域T3を経る。冷延板を、温度域T3において、以下に説明する第2平均冷却速度v2で冷却する。
これにより、最終的に得られるミクロ組織において、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合(割合p)が高くなる。
その理由は、以下のように推測される。
温度域T3では、Cが濃化した未変態オーステナイトにおいて、マルテンサイト変態が進行する。このとき、マルテンサイトブロック中をCが部分的に拡散し、準安定炭化物の前駆段階が生じる。その結果、続く後加熱において、準安定炭化物の析出が著しく促進される。
このため、第2平均冷却速度v2は、0.3℃/s以上であり、0.5℃/s以上が好ましく、1.0℃/s以上がより好ましい。
第2平均冷却速度v2が第1平均冷却速度v1以上であると、マルテンサイト中のCの拡散が不十分となり、準安定炭化物の前駆段階が十分に生じない。その結果、続く後加熱において、準安定炭化物の析出が抑制され、割合pが低くなり、耐遅れ破壊特性が不十分となる。
焼鈍の途中で、冷延板に対して、1回以上の曲げ曲げ戻し加工を実施してもよい。
曲げ曲げ戻し加工は、150℃以上Ms℃以下の温度域で実施することが好ましい。
曲げ曲げ戻し加工とは、圧延方向に対して垂直方向に実施する曲げ加工、および、それに続く曲げ戻し加工である。曲げ曲げ戻し加工によって、マルテンサイト変態が促進される。これにより、後述する後加熱において、準安定炭化物が効率よく析出し、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合(割合p)が上昇する。
一方、曲げ曲げ戻し加工の回数が多すぎると、著しい加工硬化により、Elが低下する場合がある。このため、曲げ曲げ戻し加工の回数は、10回以下が好ましく、8回以下がより好ましく、5回以下が更に好ましい。
冷却停止温度は、150℃以下である。これにより、マルテンサイト変態が十分に完了する。冷却停止温度が150℃超である場合、未変態オーステナイトがマルテンサイト変態せずに、残留オーステナイト量が過大となり、良好な部品強度および伸びフランジ性が得られない。
冷却停止温度から室温までの冷却速度は、特に限定されない。冷却方法も、特に限定されず、任意の方法を採用でき、例えば、ガスジェット冷却、ミスト冷却、水冷、空冷などの方法を採用できる。
焼鈍(加熱および冷却)を施した冷延板に、次いで、後加熱を施す。
後加熱を実施することにより、上述した焼鈍における冷却中に生成したマルテンサイトブロックにおいて、耐遅れ破壊特性を向上させる準安定炭化物が析出する。これにより、良好な部品強度、伸びフランジ性および曲げ性を有しつつ、耐遅れ破壊特性に優れる、TSが1180MPa以上の高強度鋼板が得られる。
より詳細には、焼鈍を施した冷延板に、後加熱を、最高到達温度である温度X(単位:℃)と、温度X-10℃以上での保持時間Y(単位:s)とが下記式1を満たす条件で実施する。これにより、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合(割合p)が高くなり、耐遅れ破壊特性が優れる。
式1:8000≦(273+X)×(20+Log(Y/3600))≦12000
このため、割合pが高くなるという理由から、変数部Zの値は、8000以上であり、8500以上が好ましく、9000以上がより好ましい。
このため、割合pが高くなるという理由から、変数部Zの値は、12000以下であり、11500以下が好ましく、11000以下がより好ましい。
後加熱において、温度X(単位:℃)は、下記式2を満たすことが好ましい。これにより、準安定炭化物が存在するマルテンサイトブロックにおける準安定炭化物の数密度(数密度n)が高くなる。
式2:100≦X≦400
同様の理由から、温度Xは、400℃以下が好ましく、380℃以下がより好ましく、350℃以下が更に好ましい。
こうして、本発明の製造方法により、本発明の高強度鋼板が得られる。
本発明の製造方法において、後述するめっき処理を施す場合、得られる本発明の高強度鋼板は、めっき層を有するめっき鋼板である。
本発明の製造方法においては、冷延板にめっき処理を施してもよい。
めっき処理としては、例えば、溶融亜鉛めっき処理(溶融亜鉛めっき層を形成する処理)、合金化溶融亜鉛めっき処理(溶融亜鉛めっき処理の後に、合金化処理を実施することにより、合金化溶融亜鉛めっき層を形成する処理)などが挙げられる。電気めっき処理により、電気めっき層を形成してもよい。
めっき処理は、例えば、温度域T1(Ms℃以上700℃以下)に滞留中の冷延板に対して、実施する。
亜鉛めっき浴のAl量は、0.10~0.23質量%が好ましい。
溶融亜鉛めっき処理は、上述した焼鈍中の温度域T1(Ms℃以上700℃以下)における滞留中に実施することが好ましい。
一方、合金化処理の温度は、高すぎると、未変態オーステナイトがパーライトへ変態し、TSが低下する場合があることから、600℃以下が好ましく、560℃以下がより好ましい。
スキンパス圧延での圧下率は、降伏強さを上昇させる観点から、0.05%以上が好ましい。圧下率の上限は、特に限定されないが、生産性の観点から1.50%が好ましい。
スキンパス圧延は、オンラインで実施してもよいし、オフラインで実施してもよい。
一度に目的の圧下率のスキンパスを実施してもよいし、数回に分けて実施してもよい。
〈鋼板の製造〉
下記表1~表2に示す成分組成(残部はFeおよび不可避的不純物からなる)を有する溶鋼を転炉において溶製し、連続鋳造法にて鋼スラブを得た。
得られた鋼スラブに熱間圧延を施して、熱延板を得た。具体的には、鋼スラブを、1250℃に加熱して粗圧延し、次いで、仕上げ圧延温度900℃で仕上げ圧延を施してから、500℃の条件で巻き取り、その後、室温まで冷却して、熱延板を得た。
得られた熱延板に、酸洗を施した後、500℃の条件で軟質化熱処理を施し、次いで、圧延率50%の条件で冷間圧延を施した。こうして、板厚1.4mmの冷延板を得た。
加熱温度での加熱時間は、200sとした。
曲げ曲げ戻し加工は、温度域T2および温度域T3において実施した。
一部の冷延板に対しては、温度域T1(Ms℃以上700℃以下)での滞留中に、溶融亜鉛めっき処理を実施して、両面にめっき層(溶融亜鉛めっき層)を形成した。すなわち、溶融亜鉛めっき鋼板(GI)を得た。
溶融亜鉛めっき処理には、Al:0.20質量%を含有し、残部がZnおよび不可避的不純物からなる溶融亜鉛めっき浴(浴温:470℃)を使用した。
溶融亜鉛めっき層の片面あたりの付着量は、45g/m2程度とした。
形成した溶融亜鉛めっき層の組成は、Fe:0.1~1.0質量%およびAl:0.2~1.0質量%を含有し、残部がFeおよび不可避的不純物からなる組成であった。
溶融亜鉛めっき処理には、Al:0.14質量%を含有し、残部がZnおよび不可避的不純物からなる溶融亜鉛めっき浴(浴温:470℃)を使用した。
合金化処理は、550℃とした。
合金化溶融亜鉛めっき層の片面あたりの付着量は、45g/m2程度とした。
形成した合金化溶融亜鉛めっき層の組成は、Fe:7~15質量%およびAl:0.1~1.0質量%を含有し、残部がFeおよび不可避的不純物からなる組成であった。
以下、溶融亜鉛めっき鋼板(GI)および合金化溶融亜鉛めっき鋼板(GA)も、単に、「鋼板」と呼ぶ。
得られた鋼板について、上述した方法にしたがって、マルテンサイト、フェライトおよび残留オーステナイトの面積率、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合(割合p)、ならびに、準安定炭化物が存在するマルテンサイトブロックにおける準安定炭化物の数密度(数密度n)を測定した。結果を下記表4に示す。
得られた鋼板について、以下に説明する試験を実施して、各種特性を評価した。結果を下記表4に示す。
引張試験は、JIS Z 2241に準拠して実施した。
具体的には、得られた鋼板から、鋼板の圧延方向に対して直角方向が長手方向となるように、JIS5号試験片を採取した。採取した試験片を用いて、クロスヘッド速度が1.67×10⁻¹mm/sの条件で、引張試験を実施して、降伏強さ(YS)[MPa]、引張強さ(TS)[MPa]および全伸び(El)[%]を測定した。更に、降伏比(YR)(=100×YS/TS)[%]を算出した。
引張強さ(TS)が1180MPa以上である場合、高強度であると判断した。
降伏比(YR)が65%以上である場合、部品強度に優れると判断した。
穴広げ試験は、JIS Z 2256に準拠して実施した。
具体的には、得られた鋼板を剪断して、100mm×100mmのサイズの試験片を採取した。採取した試験片に、クリアランス12.5%で直径10mmの穴を打ち抜いた。その後、内径75mmのダイスを用いて、しわ押さえ力9ton(88.26kN)で抑えた状態で、頂角60°の円錐ポンチを穴に押し込み、亀裂発生限界における穴直径Df[mm]を測定した。初期の穴直径をD0[mm]として、下記の式から、穴広げ率λ[%]を求めた。
λ={(Df-D0)/D0}×100
穴広げ率(λ)が30%以上である場合、伸びフランジ性に優れると判断した。
曲げ試験は、JIS Z 2248に準拠して実施した。
具体的には、得られた鋼板から、鋼板の圧延方向に対して平行方向が曲げ試験の軸方向となるように、幅30mm、長さ100mmの短冊状の試験片を採取した。採取した試験片を用いて、押込み荷重100kN、押付け保持時間5秒の条件で、90°V曲げ試験を実施した。
曲げ半径Rを板厚tで除した値(R/t)が5以下となる最大の曲げ半径R(例えば、板厚tが1.4mmの場合、曲げ半径Rは7.0mm)で、5つの試験片について、曲げ試験を実施した。次いで、曲げ頂点の稜線部における亀裂発生の有無を確認した。
亀裂発生の有無は、曲げ頂点の稜線部を、デジタルマイクロスコープ(RH-2000、ハイロックス社製)を用いて、40倍の倍率で観察することにより、確認した。
5つの試験片のいずれにも亀裂が発生しなかった場合のみ、曲げ性に優れると判断し、下記表4には「優」を記載した。
一方、5つの試験片のいずれかに亀裂が発生した場合は、曲げ性が不十分であると判断し、下記表4には「劣」を記載した。
得られた鋼板から、鋼板の圧延方向に対して直角方向が機械研削端面となるように、幅70mm、長さ16mmの短冊状の試験片を採取した。採取した試験片に、四点曲げによって中央部に800MPa相当の応力が付加されるように、曲げ変形を加えた。
次いで、曲げ変形を加えた試験片を、マッキルベイン緩衝液を用いてpHを5.0に調整した25℃の0.1質量%チオシアン酸アンモニウム溶液中に浸漬した。
その後、この溶液中の試験片を観察し、割れの発生の有無を確認した。
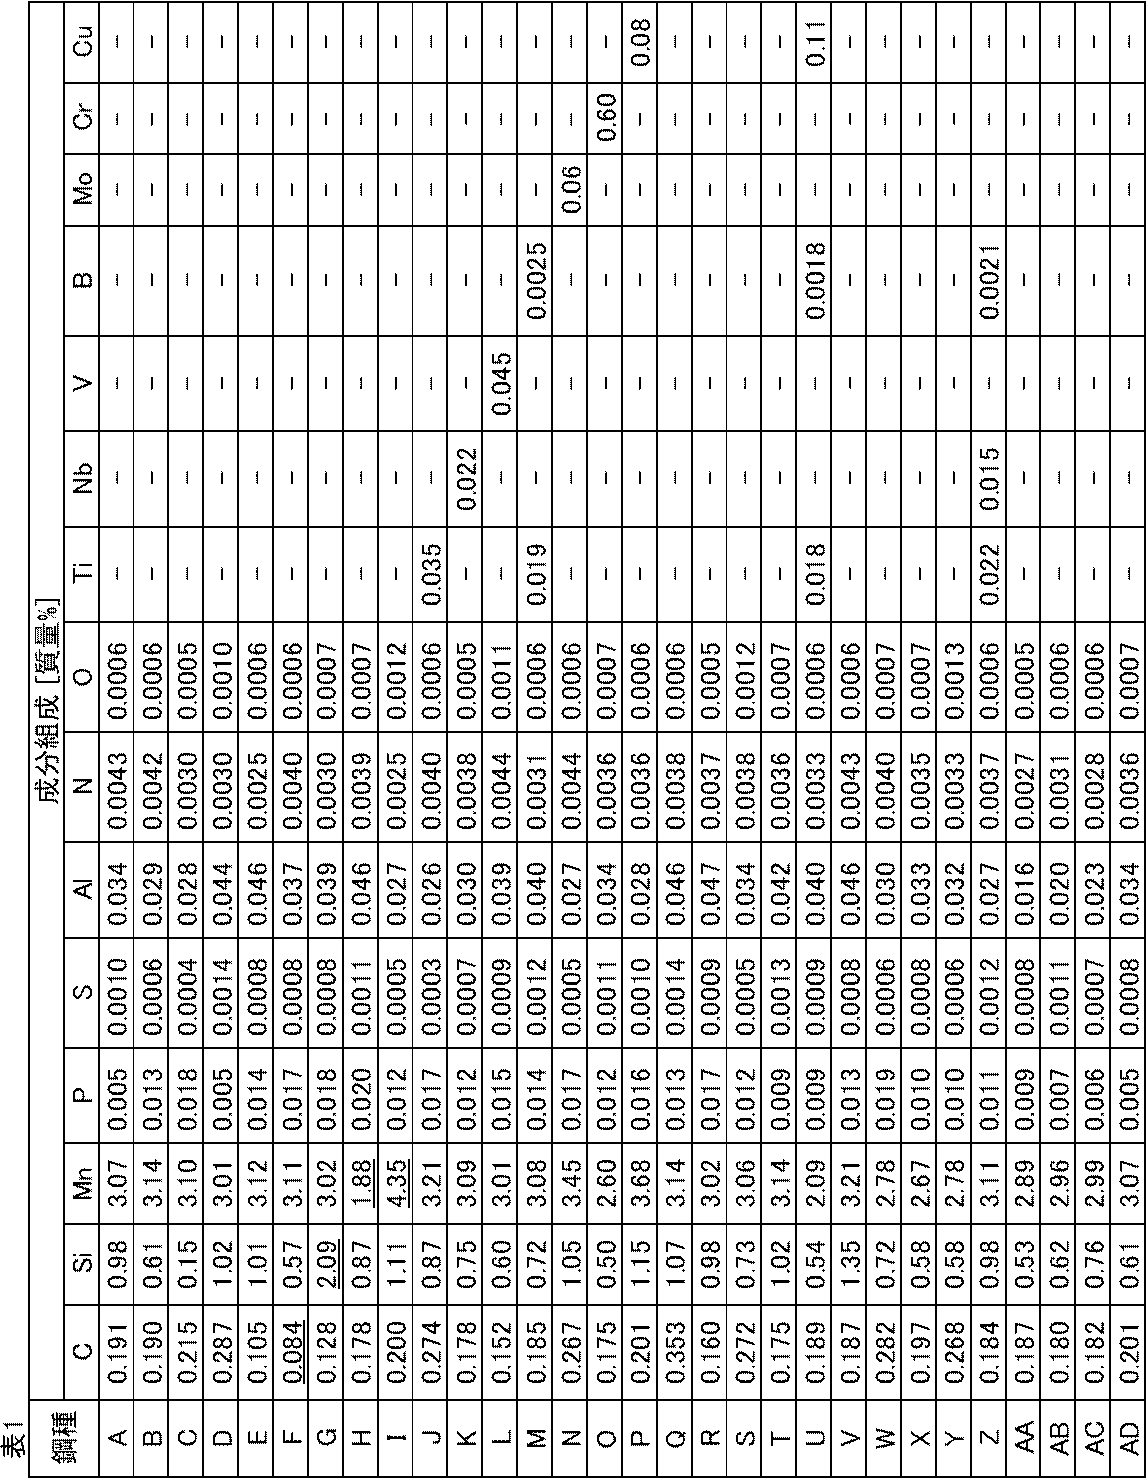
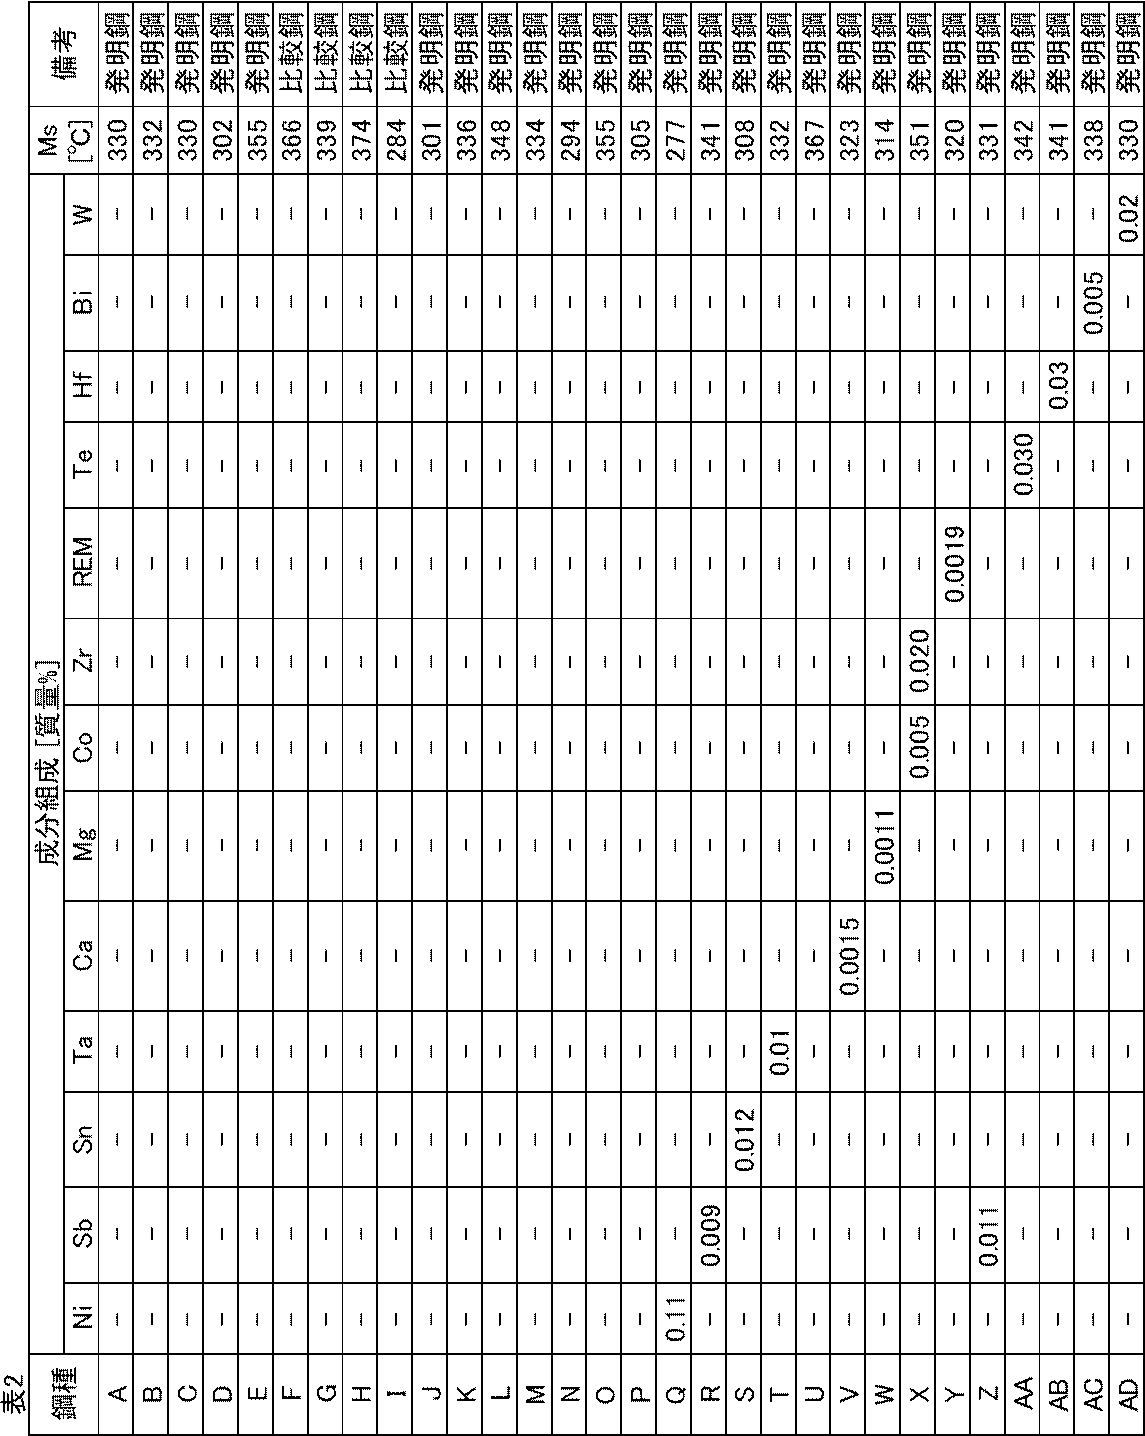
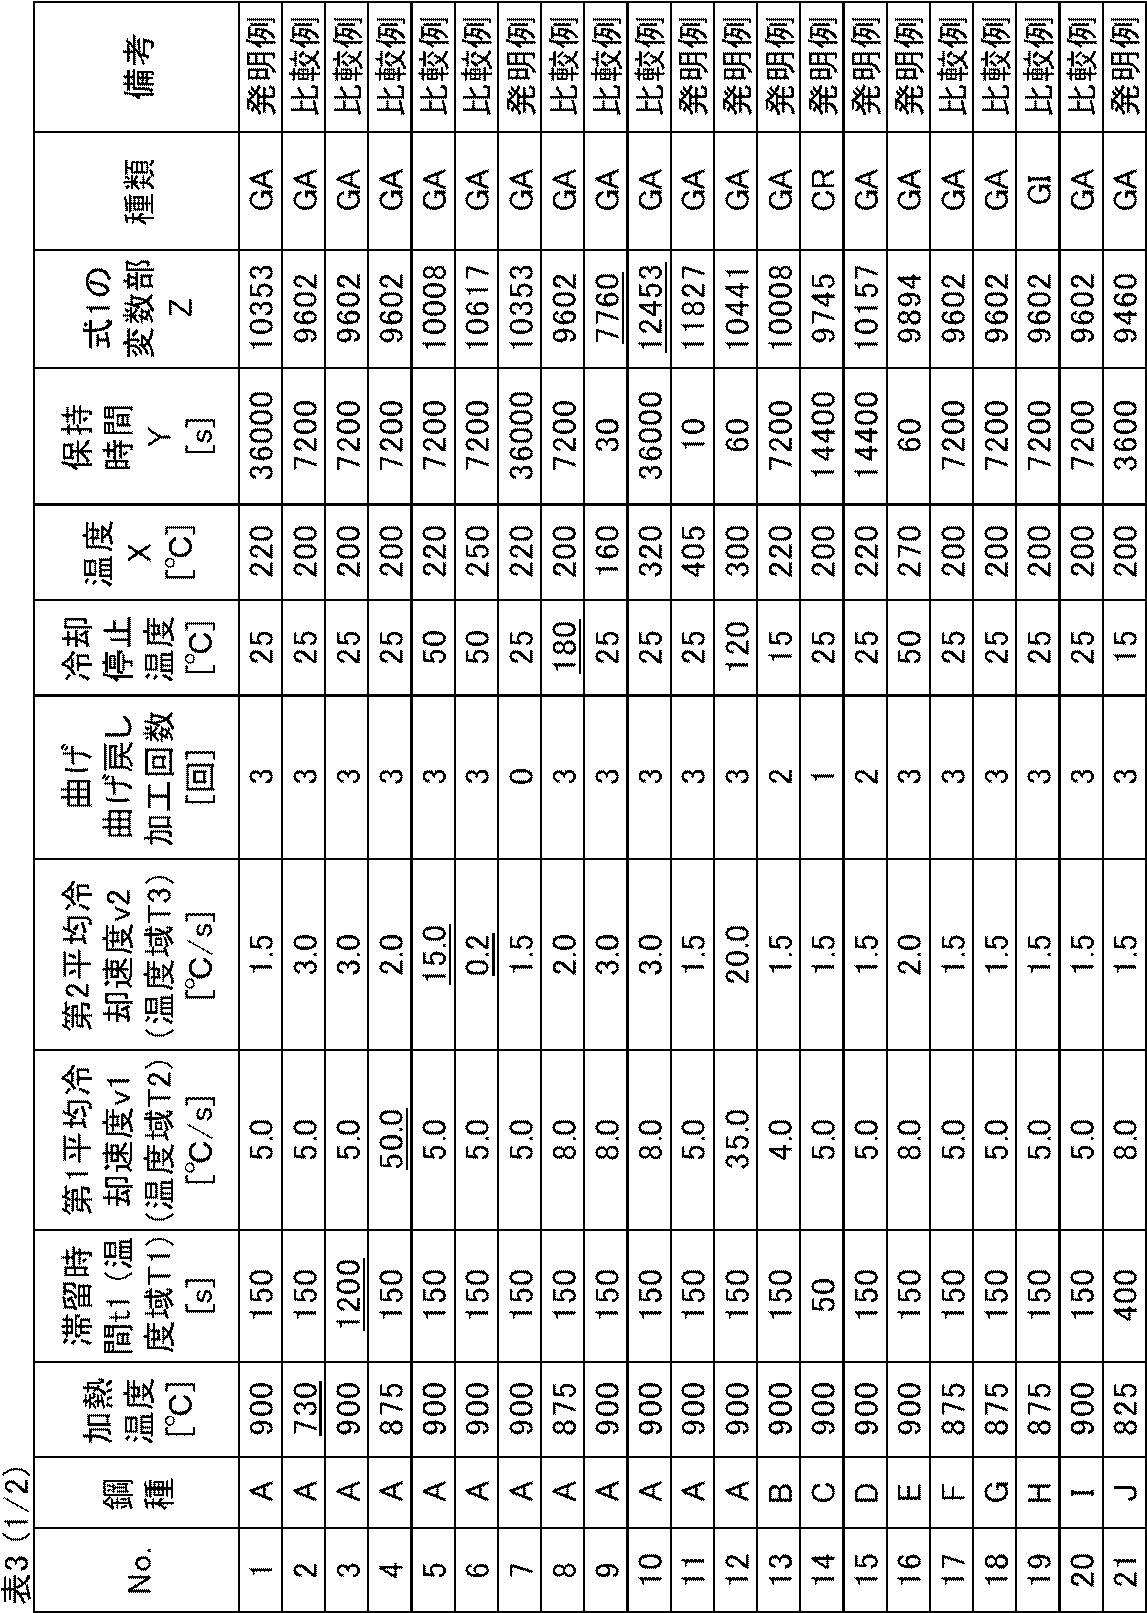
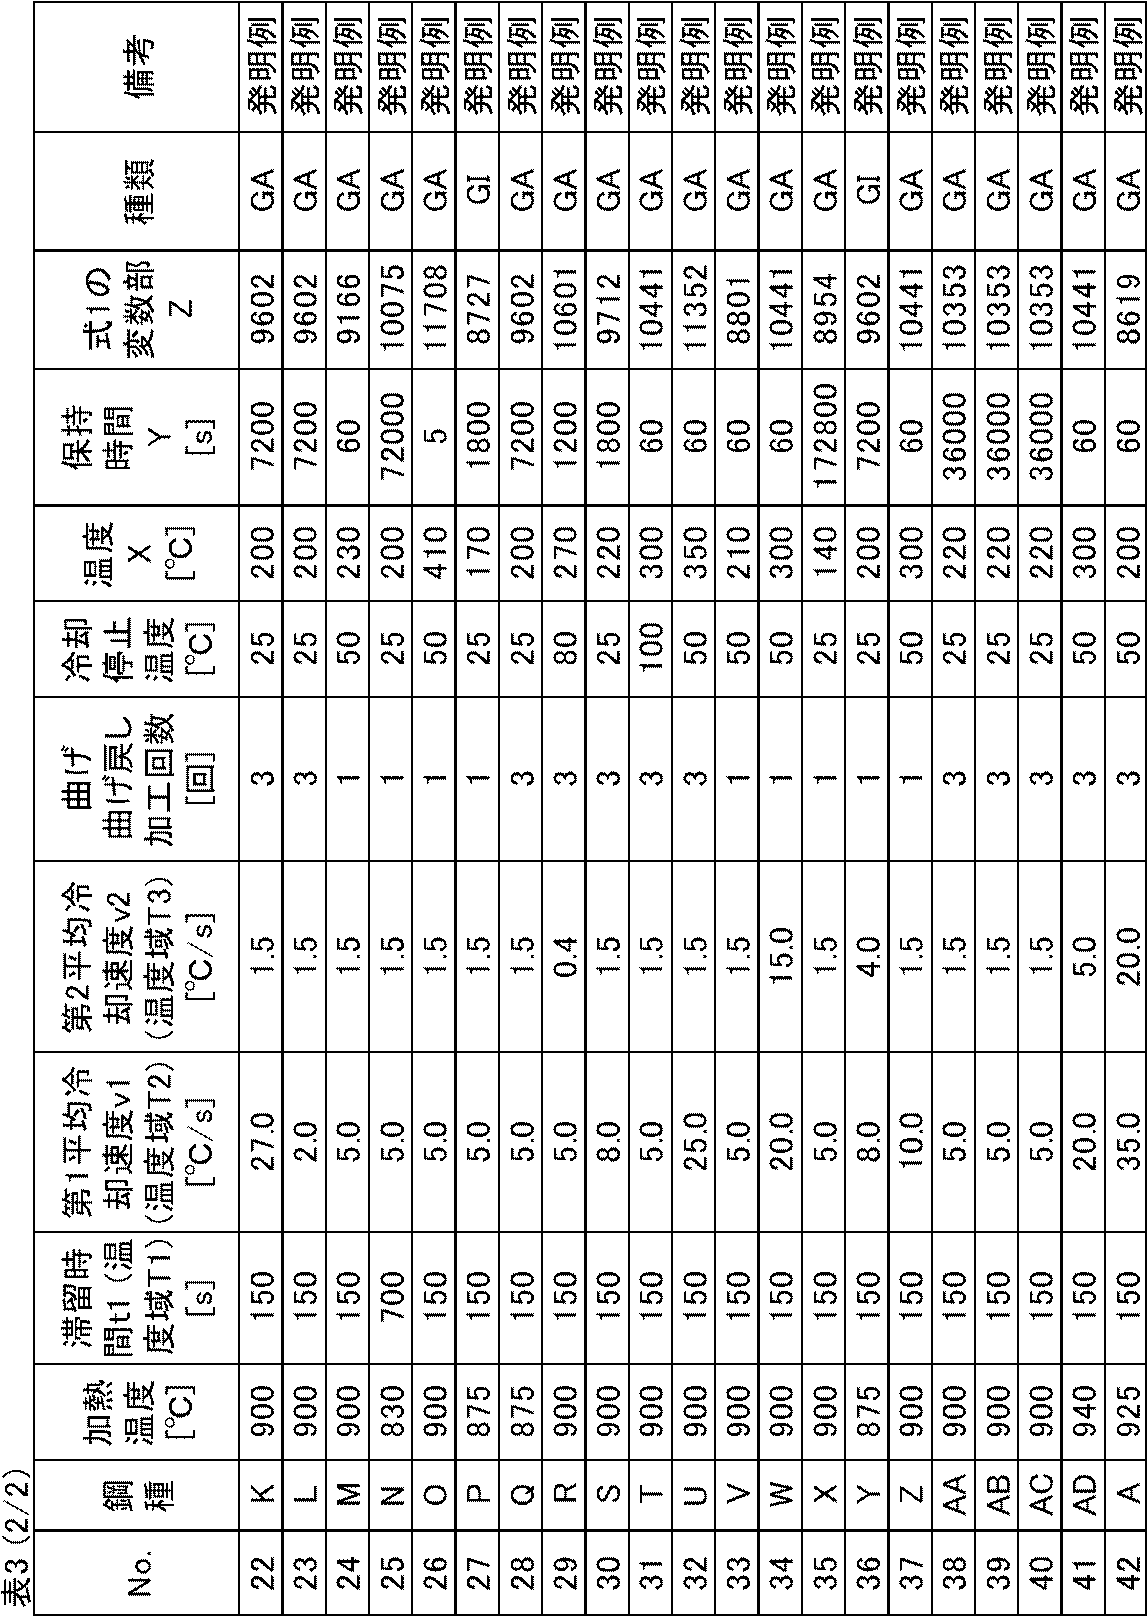
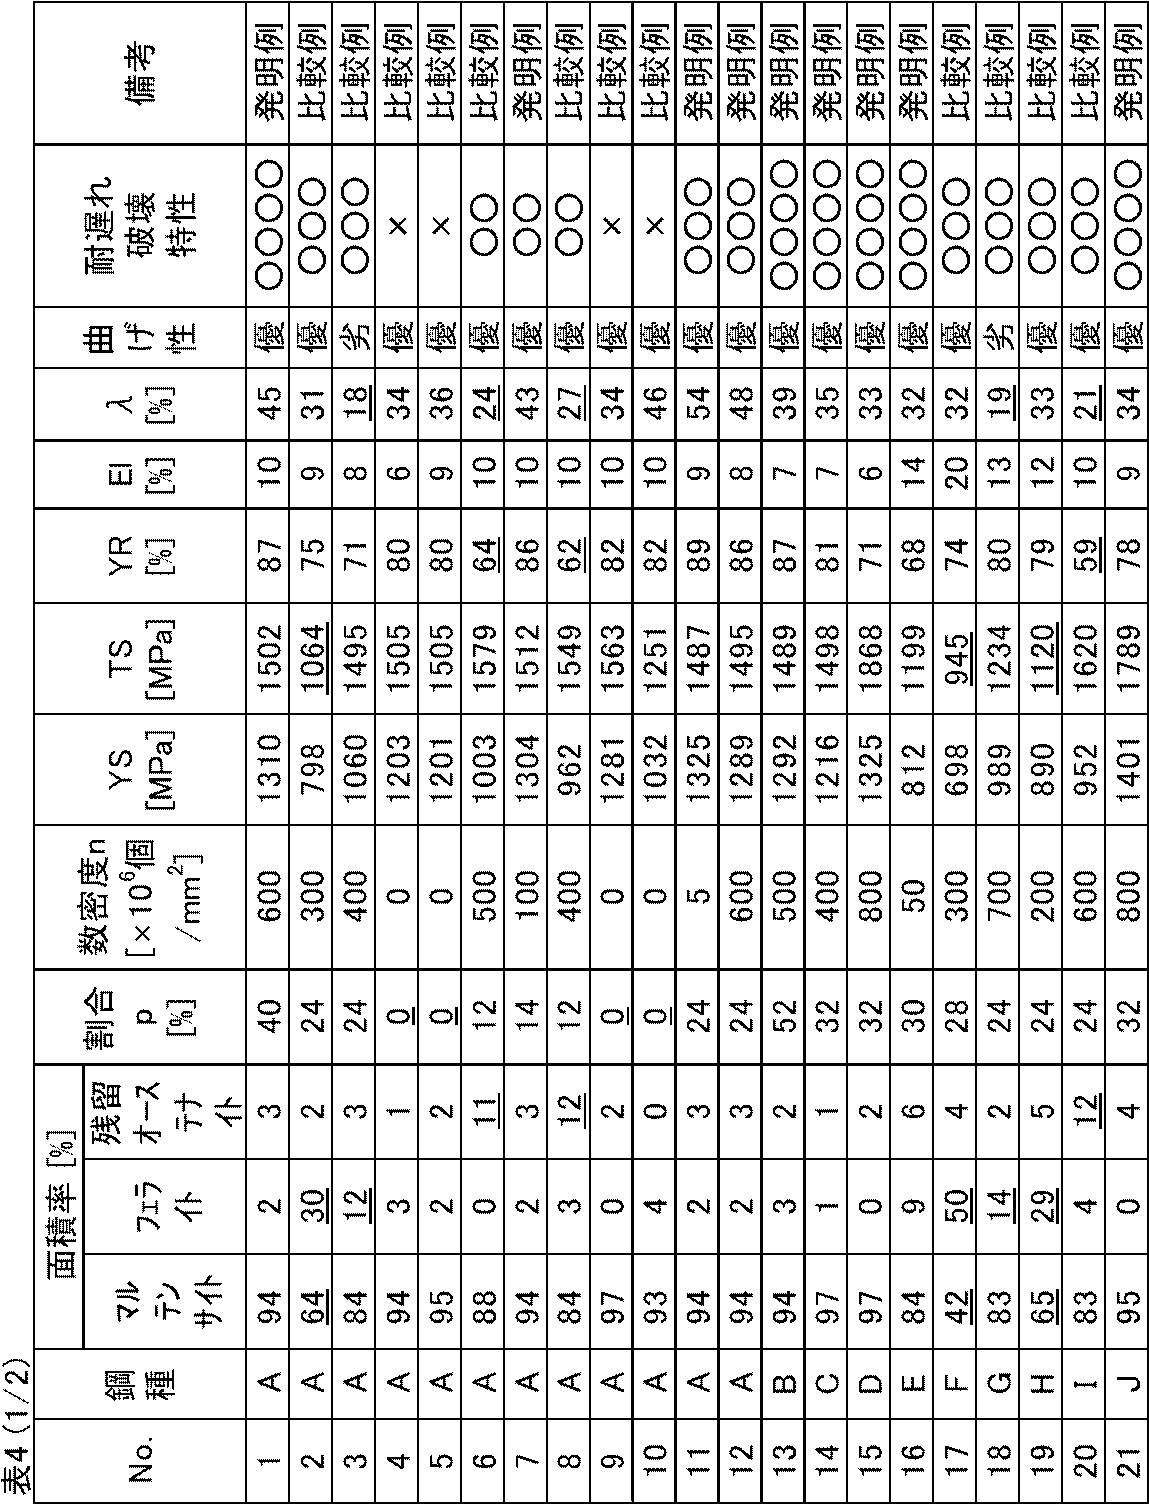
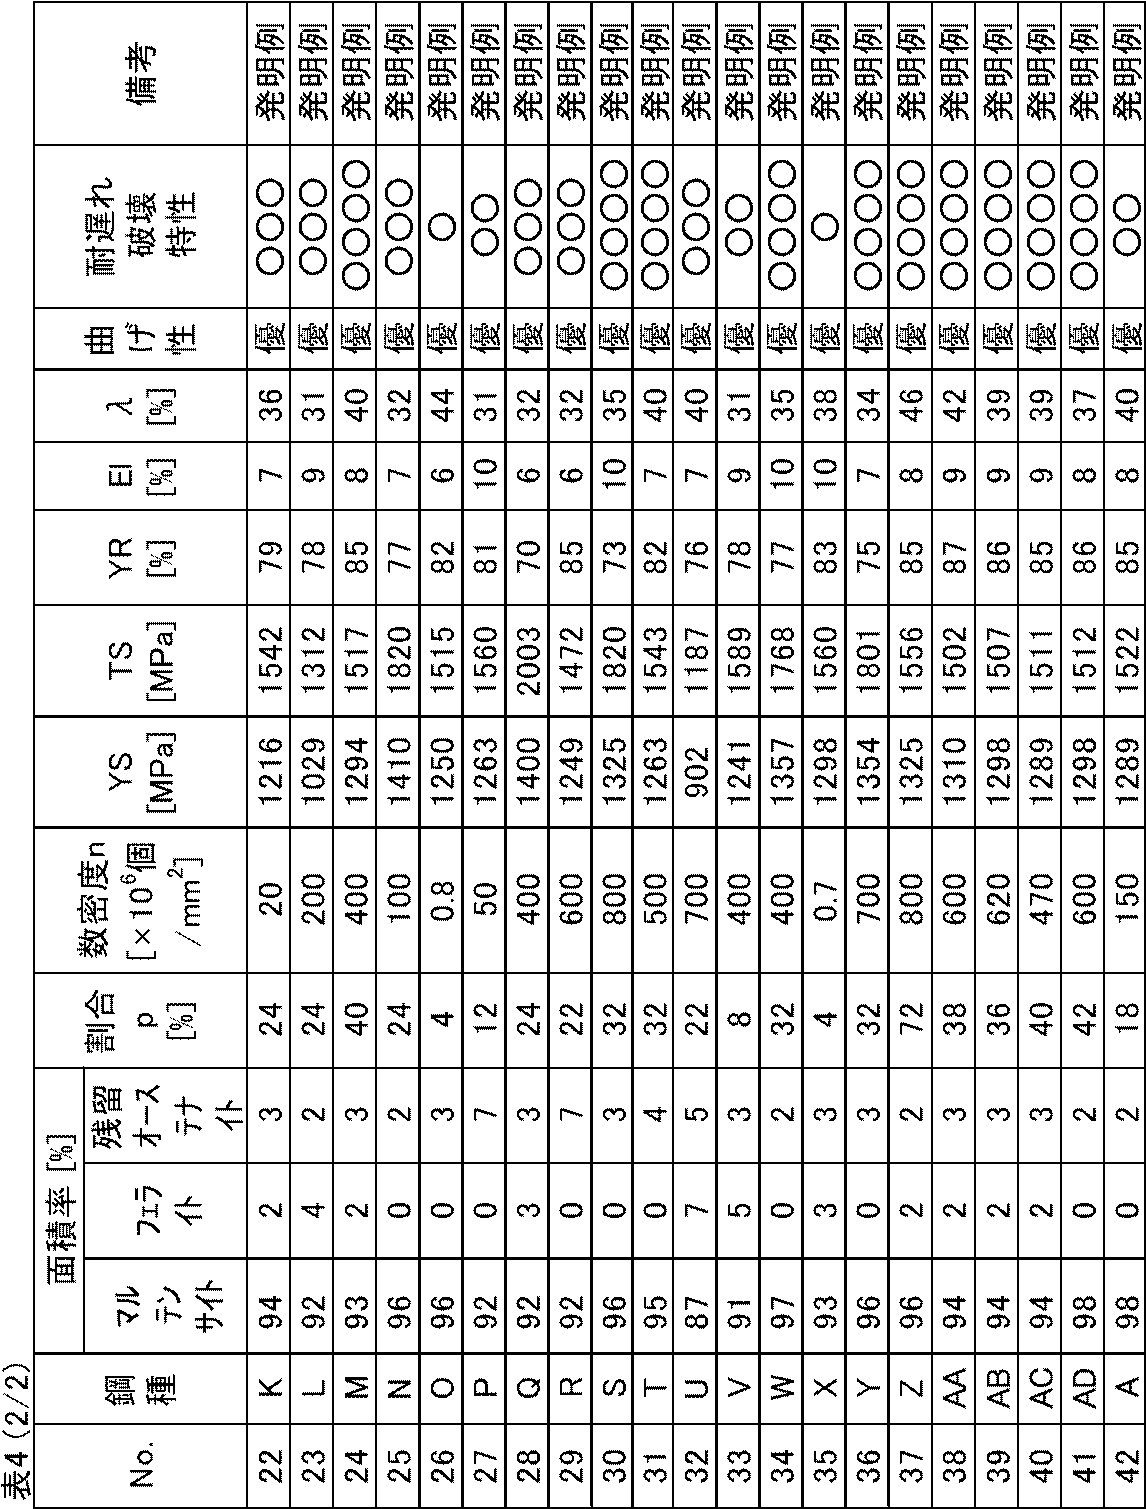
上記表4に示すように、No.1、7、11~16および21~42の鋼板は、いずれも、引張強さが1180MPa以上であり、かつ、部品強度、伸びフランジ性、曲げ性および耐遅れ破壊特性に優れていた。
(i)割合pが2%以上20%未満、かつ、数密度nが1×10⁶個/mm未満
(ii)割合pが2%以上20%未満、かつ、数密度nが1×10⁶個/mm以上
(iii)割合pが20%以上30%未満
(iv)割合pが30%以上
〈鋼板の製造〉
上記表1~表2に示す成分組成(残部はFeおよび不可避的不純物からなる)を有する溶鋼を転炉において溶製し、連続鋳造法にて鋼スラブを得た。
得られた鋼スラブに熱間圧延を施して、熱延板を得た。具体的には、鋼スラブを、1250℃に加熱して粗圧延し、次いで、仕上げ圧延温度900℃で仕上げ圧延を施してから、500℃の条件で巻き取り、その後、室温まで冷却して、熱延板を得た。
得られた熱延板に、酸洗を施した後、500℃の条件で軟質化熱処理を施し、次いで、圧延率50%の条件で冷間圧延を施した。こうして、板厚1.2mmの冷延板を得た。
加熱温度での加熱時間は、200sとした。
曲げ曲げ戻し加工は、温度域T2および温度域T3において実施した。
Fe系金属めっき層を形成した場合は「Fe」を、Ni系金属めっき層を形成した場合は「Ni」を、金属めっき処理を実施しなかった場合は「-」を、下記表5の「金属めっき処理」の欄に記載した。
電気めっき浴としては、1.5mol/LのFe2+イオンまたはNi2+イオンを含有する硫酸浴(浴温:50℃、pH:2.0)を用いた。
電気めっき浴中で、冷延板を陰極とし、酸化イリジウム電極を陽極として、45A/dm2の電流密度で、電解処理を実施した。形成される金属めっき層の付着量は、通電時間を調整することによって制御した。
一部の冷延板に対しては、温度域T1(Ms℃以上700℃以下)での滞留中に、溶融亜鉛めっき処理を実施して、両面にめっき層(溶融亜鉛めっき層)を形成した。すなわち、溶融亜鉛めっき鋼板(GI)を得た。
溶融亜鉛めっき処理には、Al:0.20質量%を含有し、残部がZnおよび不可避的不純物からなる溶融亜鉛めっき浴(浴温:470℃)を使用した。
溶融亜鉛めっき層の片面あたりの付着量は、45g/m2程度とした。
形成した溶融亜鉛めっき層の組成は、Fe:0.1~1.0質量%およびAl:0.2~1.0質量%を含有し、残部がFeおよび不可避的不純物からなる組成であった。
溶融亜鉛めっき処理には、Al:0.14質量%を含有し、残部がZnおよび不可避的不純物からなる溶融亜鉛めっき浴(浴温:470℃)を使用した。
合金化処理は、550℃とした。
合金化溶融亜鉛めっき層の片面あたりの付着量は、45g/m2程度とした。
形成した合金化溶融亜鉛めっき層の組成は、Fe:7~15質量%およびAl:0.1~1.0質量%を含有し、残部がFeおよび不可避的不純物からなる組成であった。
以下、溶融亜鉛めっき鋼板(GI)および合金化溶融亜鉛めっき鋼板(GA)も、単に、「鋼板」と呼ぶ。
得られた鋼板について、上述した方法にしたがって、マルテンサイト、フェライトおよび残留オーステナイトの面積率、マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合(割合p)、ならびに、準安定炭化物が存在するマルテンサイトブロックにおける準安定炭化物の数密度(数密度n)を測定した。結果を下記表6に示す。
得られた鋼板について、マルテンサイト、フェライトおよび残留オーステナイト以外の残部組織は、全てθ(フェライト中に析出したセメンタイト)であった。
上述した方法に従って、金属めっき層(Fe系金属めっき層またはNi系金属めっき層)の付着量を求めた。結果を下記表6に示す。
金属めっき処理を実施しなかった(つまり、金属めっき層を形成しなかった)場合は、下記表6の「金属めっき層の付着量」の欄に「-」を記載した。
上述した方法に従って、軟質層の厚さ、割合r(測定点の総数:512点)、標準偏差σAおよび標準偏差σBを求めた。結果を下記表6に示す。
得られた鋼板について、試験例1と同様にして、引張試験および穴広げ試験を実施して、降伏強さ(YS)、引張強さ(TS)、降伏比(YR)、全伸び(El)および穴広げ率(λ)を求めた。
また、得られた鋼板について、試験例1と同様にして、曲げ試験および遅れ破壊試験を実施して、曲げ性および耐遅れ破壊特性を評価した。
いずれも結果を下記表6に示す。
得られた鋼板から、60mm×65mmの試験片T1を、剪断加工および端面研削加工により採取した。試験片T1の60mmの辺は、鋼板の圧延方向(L方向)に平行な辺であり、試験片T1の65mmの辺は、鋼板の幅方向(C方向)に平行な辺である。
採取した試験片T1に、後述する90°曲げ加工および直交曲げ加工を実施した。
図2Aは、試験片T1に90°曲げ加工を実施している状態を示す斜視図である。
図2Bは、試験片T1に直交曲げ加工を実施している状態を示す斜視図である。
図2Aおよび図2Bにおいて、D1は幅方向(C方向)を示し、D2は圧延方向(L方向)を示す。
具体的には、まず、試験片T1に、曲率半径/板厚:4.2で、90°曲げ加工(一次曲げ加工)を施した。より詳細には、図2Aに示すように、V溝を有するダイA1の上に載せた試験片T1に対して、下記条件で、パンチB1を押し込んだ。
次に、試験片T1に、直交曲げ加工(二次曲げ加工)を施した。より詳細には、図2Bに示すように、支持ロールA2の上に載せた試験片T1に対して、下記条件で、パンチB2を押し込んだ。
試験方法:ダイ支持、パンチ押し込み
成形荷重:10ton
試験速度:30mm/min
保持時間:5s
曲げ方向:圧延方向(L方向)
試験方法:ロール支持、パンチ押し込み
ロール径:φ30mm
パンチ先端R:0.4mm
ロール間距離:(板厚×2)+0.5mm
ストローク速度:20mm/min
曲げ方向:幅方向(C方向)
求めたSFmaxが、下記条件Aを満たす場合、衝突時の耐破断性(曲げ破断に対する耐性)に優れると判断した。
TSが1180MPa以上1320MPa未満であるときは、SFmaxが24.5mm以上であり、TSが1320MPa以上であるときは、SFmaxが24.0mm以上である。
以下のようにして、軸圧壊試験を実施した。
まず、得られた鋼板から、150mm×100mmの試験片を、剪断加工により採取した。試験片の150mmの辺は、鋼板の圧延方向(L方向)に平行な辺である。
次いで、試験片を、パンチ肩半径が5.0mmであり、かつ、ダイ肩半径が5.0mmである金型を用いて、深さ40mmとなるように成形加工(曲げ加工)して、図3Aおよび図3Bに示すように、ハット形部材10を作製した。
また、得られた鋼板から、ハット形部材10となる試験片とは別に、80mm×100mmのサイズの試験片を切り出し、これを、平板20とした。
ハット形部材10と平板20とをスポット溶接して、図3Aおよび図3Bに示すように、試験体30を作製した。
図3Aは、試験体30の正面図であり、図3Bは、試験体30の斜視図である。
スポット溶接部40の位置は、図3Bに示すように、試験体30の端部とスポット溶接部40との間隔が10mm、隣り合うスポット溶接部40どうしの間隔が20mmとなる位置にした。
図3Cは、試験体30に軸圧壊試験を実施している状態を示す斜視図である。
図3Cに示すように、試験体30の一方の端部を、地板50とTIG溶接により接合した。次に、試験体30の他方の端部に、インパクタ60を衝突速度10mm/minで等速衝突させる試験(軸圧壊試験)を実施し、試験体30を70mm圧壊した。図3Cにおいて、D3は、インパクタ60を試験体30に衝突させる方向(圧壊方向)を示す。
試験後の試験体30の外観を観察し、軸圧壊破断(外観割れ)の有無を確認した。
外観割れが認められなかった場合は「◎」を、外観割れが1箇所以下で認められた場合は「○」を、外観割れが2箇所以上で認められた場合は「×」を、下記表6に記載した。「◎」または「○」の場合、衝突時の耐破断性(軸圧壊破断に対する耐性)に優れると判断した。


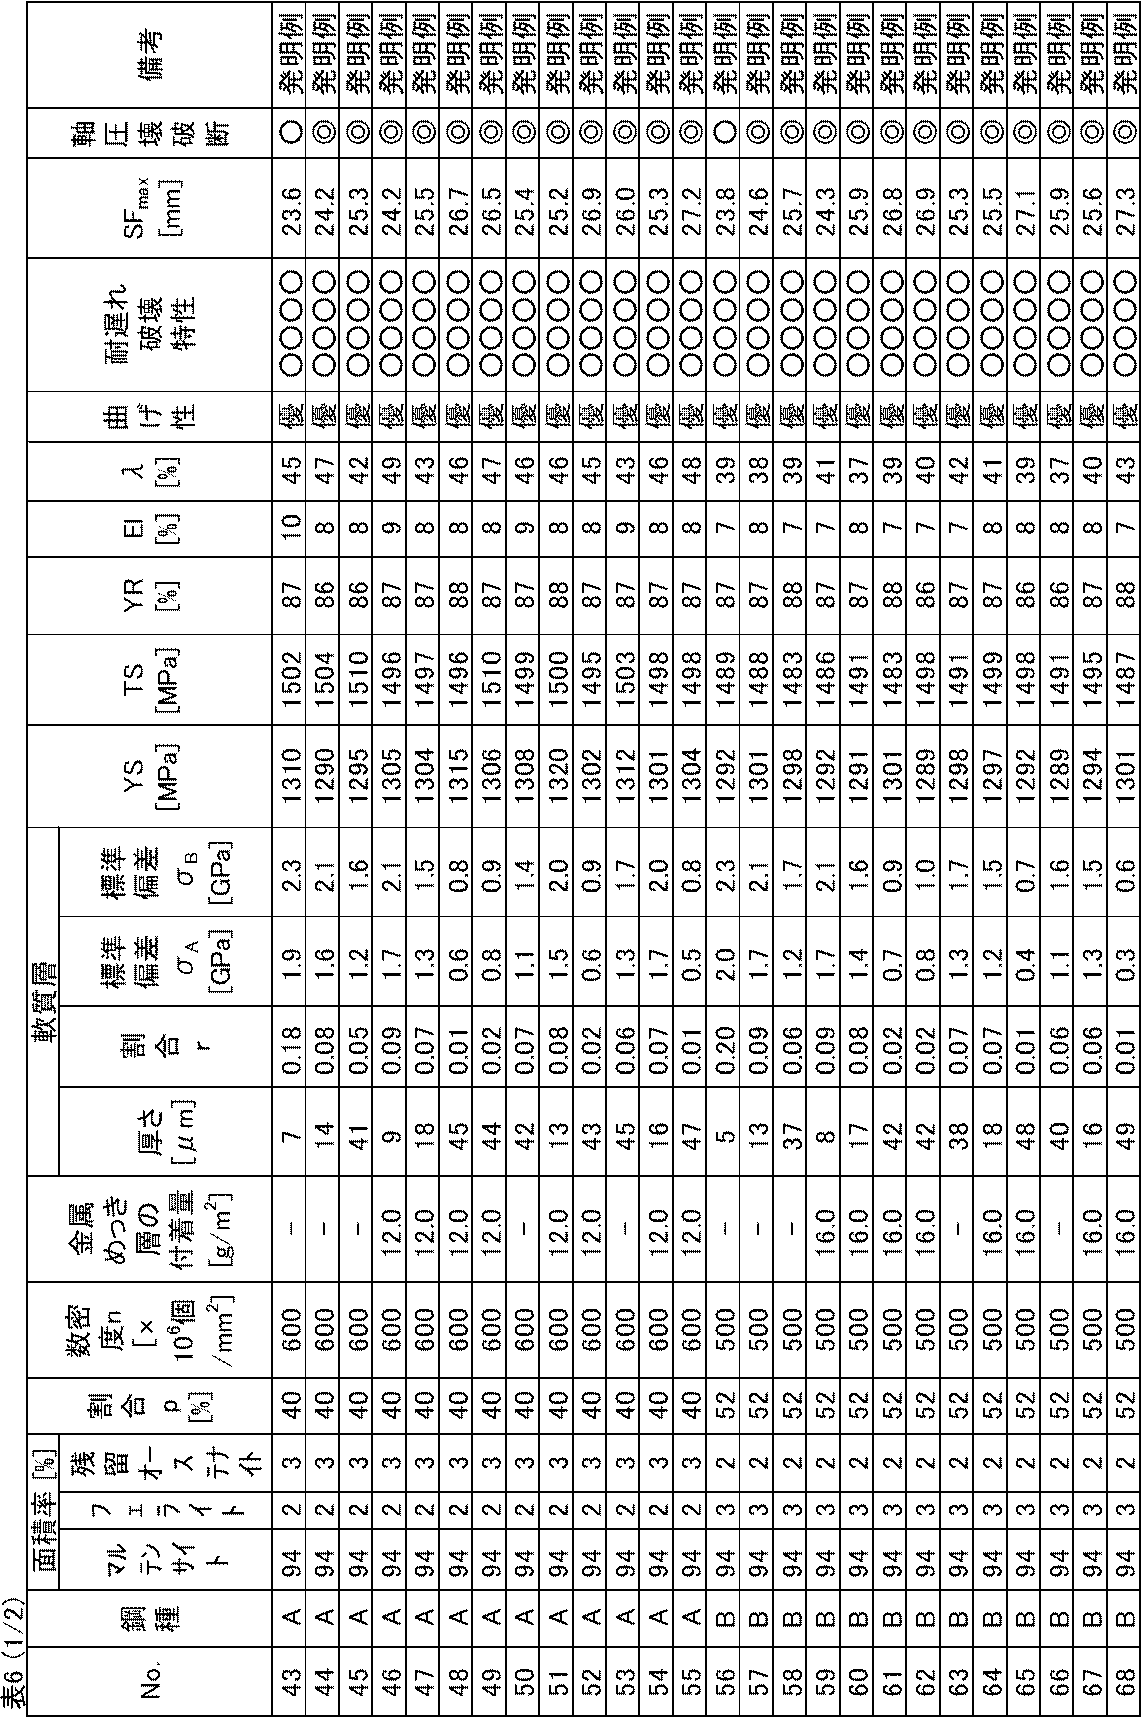

上記表6に示すように、No.43~94の鋼板は、いずれも、引張強さが1180MPa以上であり、かつ、部品強度、伸びフランジ性、曲げ性および耐遅れ破壊特性に優れていた。更に、衝突時の耐破断性(軸圧壊破断に対する耐性)にも優れていた。
露点が-30℃以上-20℃未満の場合、軟質層の厚さは10μm以下であった。この場合、軸圧壊試験による衝突時の耐破断性(軸圧壊破断に対する耐性)の評価結果は「○」であったが、金属めっき層を有する場合は「◎」に向上した。
A2:支持ロール
B1:パンチ
B2:パンチ
T1:試験片
D1:幅方向(C方向)
D2:圧延方向(L方向)
D3:圧壊方向
10:ハット形部材
20:平板
30:試験体
40:スポット溶接部
50:地板
60:インパクタ
Claims (14)
- 鋼板を備え、
前記鋼板が、
質量%で、
C:0.090%以上0.390%以下、
Si:0.01%以上2.00%以下、
Mn:2.00%以上4.00%以下、
P:0.100%以下、
S:0.0200%以下、
Al:1.000%以下、
N:0.0100%以下、および、
O:0.0100%以下を含有し、残部がFeおよび不可避的不純物からなる成分組成と、ミクロ組織と、を有し、
前記ミクロ組織において、
マルテンサイトの面積率が、70%以上であり、
フェライトの面積率が、10%以下であり、
残留オーステナイトの面積率が、10%以下であり、
マルテンサイトブロック数に対する準安定炭化物が存在するマルテンサイトブロック数の割合が、2%以上である、高強度鋼板。 - 前記準安定炭化物が存在するマルテンサイトブロックにおける前記準安定炭化物の数密度が、1×10⁶個/mm2以上である、請求項1に記載の高強度鋼板。
- 前記成分組成は、更に、質量%で、
Ti:0.200%以下、
Nb:0.200%以下、
V:0.200%以下、
Ta:0.10%以下、
W:0.10%以下、
B:0.0100%以下、
Cr:1.00%以下、
Mo:1.00%以下、
Ni:1.00%以下、
Co:0.010%以下、
Cu:1.00%以下、
Sn:0.200%以下、
Sb:0.200%以下、
Ca:0.0100%以下、
Mg:0.0100%以下、
REM:0.0100%以下、
Zr:0.100%以下、
Te:0.100%以下、
Hf:0.10%以下、および、
Bi:0.200%以下からなる群から選ばれる少なくとも1種の元素を含有する、請求項1または2に記載の高強度鋼板。 - 前記鋼板は、表層として、軟質層を有し、
前記表層は、前記鋼板の表面から板厚方向に200μmまでの部分であり、
前記軟質層は、前記鋼板の板厚1/4位置のビッカース硬さに対して、ビッカース硬さが85%以下の部分である、請求項1~3のいずれか1項に記載の高強度鋼板。 - 前記軟質層の板厚方向深さ1/4位置におけるナノ硬さを、50μm×50μmの範囲内の300点以上で測定するとき、測定点の総数に対する、ナノ硬さが7.0GPa以上である測定点の割合rが、0.10以下である、請求項4に記載の高強度鋼板。
- 前記軟質層の板厚方向深さ1/4位置におけるナノ硬さの標準偏差σAが、1.8GPa以下であり、
前記軟質層の板厚方向深さ1/2位置におけるナノ硬さの標準偏差σBが、2.2GPa以下である、請求項4または5に記載の高強度鋼板。 - 前記鋼板の表面に、更に、焼鈍前めっき層としての金属めっき層を有する、請求項1~6のいずれか1項に記載の高強度鋼板。
- 前記鋼板の表面に、更に、めっき層を有する、請求項1~6のいずれか1項に記載の高強度鋼板。
- 前記金属めっき層の表面に、更に、めっき層を有する、請求項7に記載の高強度鋼板。
- 請求項1~3のいずれか1項に記載の高強度鋼板を製造する方法であって、
請求項1または3に記載の成分組成を有する鋼スラブに、熱間圧延、酸洗および冷間圧延を施すことにより冷延板を得て、
前記冷延板に、焼鈍および後加熱を施し、
前記焼鈍では、前記冷延板を、800℃以上の加熱温度で加熱し、次いで、150℃以下の冷却停止温度まで冷却し、
ただし、前記冷却において、
Ms℃超700℃以下の温度域T1における滞留時間t1が、1000s以下であり、
Ms-80℃以上Ms℃以下の温度域T2における第1平均冷却速度v1が、1.0℃/s以上40.0℃/s以下であり、
150℃以上Ms-80℃未満の温度域T3における第2平均冷却速度v2が、0.3℃/s以上前記第1平均冷却速度v1未満であり、
前記後加熱を、最高到達温度である温度Xと、前記温度X-10℃以上での保持時間Yとが下記式1を満たす条件で実施する、高強度鋼板の製造方法。
式1:8000≦(273+X)×(20+Log(Y/3600))≦12000
ただし、前記温度Xの単位は℃であり、前記保持時間Yの単位はsである。 - 前記温度Xが、下記式2を満たす、請求項10に記載の高強度鋼板の製造方法。
式2:100≦X≦400 - 前記焼鈍では、前記加熱温度での加熱を、露点が-30℃以上の雰囲気下で実施することにより、前記冷延板の表層に、軟質層を形成し、
前記表層は、前記冷延板の表面から板厚方向に200μmまでの部分であり、
前記軟質層は、前記冷延板の板厚1/4位置のビッカース硬さに対して、ビッカース硬さが85%以下の部分である、請求項10または11に記載の高強度鋼板の製造方法。 - 前記冷延板に、前記焼鈍を施す前に、金属めっき処理を実施して、前記冷延板の表面に、焼鈍前めっき層としての金属めっき層を形成する、請求項10~12のいずれか1項に記載の高強度鋼板の製造方法。
- 前記焼鈍において、前記冷延板に、めっき処理を施して、めっき層を形成する、請求項10~13のいずれか1項に記載の高強度鋼板の製造方法。
Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202280054470.9A CN117795113A (zh) | 2021-08-24 | 2022-08-05 | 高强度钢板及其制造方法 |
| US18/683,349 US20250137084A1 (en) | 2021-08-24 | 2022-08-05 | High-strength steel sheet and method for manufacturing same |
| EP22861109.1A EP4375384A4 (en) | 2021-08-24 | 2022-08-05 | HIGH STRENGTH STEEL SHEET AND ITS MANUFACTURING METHOD |
| MX2024002348A MX2024002348A (es) | 2021-08-24 | 2022-08-05 | Lamina de acero de alta resistencia y metodo de fabricacion de la misma. |
| JP2022576110A JP7294549B1 (ja) | 2021-08-24 | 2022-08-05 | 高強度鋼板およびその製造方法 |
| KR1020247004226A KR20240032937A (ko) | 2021-08-24 | 2022-08-05 | 고강도 강판 및 그 제조 방법 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2021-136566 | 2021-08-24 | ||
| JP2021136566 | 2021-08-24 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2023026819A1 true WO2023026819A1 (ja) | 2023-03-02 |
Family
ID=85323095
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2022/030044 Ceased WO2023026819A1 (ja) | 2021-08-24 | 2022-08-05 | 高強度鋼板およびその製造方法 |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20250137084A1 (ja) |
| EP (1) | EP4375384A4 (ja) |
| JP (1) | JP7294549B1 (ja) |
| KR (1) | KR20240032937A (ja) |
| CN (1) | CN117795113A (ja) |
| MX (1) | MX2024002348A (ja) |
| WO (1) | WO2023026819A1 (ja) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2024029145A1 (ja) * | 2022-08-03 | 2024-02-08 | 日本製鉄株式会社 | 鋼板 |
| WO2025013460A1 (ja) * | 2023-07-12 | 2025-01-16 | Jfeスチール株式会社 | 鋼板、部材および部品並びにそれらの製造方法 |
| JPWO2025075096A1 (ja) * | 2023-10-04 | 2025-04-10 | ||
| JPWO2025150337A1 (ja) * | 2024-01-09 | 2025-07-17 | ||
| JPWO2025150338A1 (ja) * | 2024-01-09 | 2025-07-17 |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR20250094763A (ko) * | 2023-12-18 | 2025-06-26 | 주식회사 포스코 | 냉연강판 및 그 제조방법 |
| WO2026070623A1 (ja) * | 2024-09-30 | 2026-04-02 | Jfeスチール株式会社 | 鋼板 |
| CN120082813B (zh) * | 2025-05-06 | 2025-08-01 | 北京科技大学 | 一种低成本高强韧低密度耐腐蚀的桥梁钢及其制备方法 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2016050343A (ja) | 2014-08-29 | 2016-04-11 | 新日鐵住金株式会社 | 耐水素脆化特性に優れた超高強度冷延鋼板およびその製造方法 |
| JP2020059881A (ja) * | 2018-10-09 | 2020-04-16 | 日本製鉄株式会社 | 鋼材およびその製造方法 |
| WO2021153393A1 (ja) * | 2020-01-31 | 2021-08-05 | Jfeスチール株式会社 | 鋼板、部材及びそれらの製造方法 |
| WO2021193057A1 (ja) * | 2020-03-27 | 2021-09-30 | Motp合同会社 | 鋼材及びその製造方法 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP6237364B2 (ja) * | 2014-03-17 | 2017-11-29 | 新日鐵住金株式会社 | 衝突特性に優れた高強度鋼板及びその製造方法 |
| JP6460238B2 (ja) * | 2015-07-13 | 2019-01-30 | 新日鐵住金株式会社 | 鋼板、溶融亜鉛めっき鋼板、及び合金化溶融亜鉛めっき鋼板、並びにそれらの製造方法 |
| JP6402830B2 (ja) * | 2015-08-24 | 2018-10-10 | 新日鐵住金株式会社 | 合金化溶融亜鉛めっき鋼板及びその製造方法 |
| KR102312464B1 (ko) * | 2017-02-10 | 2021-10-13 | 제이에프이 스틸 가부시키가이샤 | 고강도 아연 도금 강판 및 그 제조 방법 |
| JP2018188675A (ja) * | 2017-04-28 | 2018-11-29 | Jfeスチール株式会社 | 高強度熱延鋼板およびその製造方法 |
-
2022
- 2022-08-05 CN CN202280054470.9A patent/CN117795113A/zh active Pending
- 2022-08-05 MX MX2024002348A patent/MX2024002348A/es unknown
- 2022-08-05 KR KR1020247004226A patent/KR20240032937A/ko active Pending
- 2022-08-05 EP EP22861109.1A patent/EP4375384A4/en active Pending
- 2022-08-05 WO PCT/JP2022/030044 patent/WO2023026819A1/ja not_active Ceased
- 2022-08-05 US US18/683,349 patent/US20250137084A1/en active Pending
- 2022-08-05 JP JP2022576110A patent/JP7294549B1/ja active Active
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2016050343A (ja) | 2014-08-29 | 2016-04-11 | 新日鐵住金株式会社 | 耐水素脆化特性に優れた超高強度冷延鋼板およびその製造方法 |
| JP2020059881A (ja) * | 2018-10-09 | 2020-04-16 | 日本製鉄株式会社 | 鋼材およびその製造方法 |
| WO2021153393A1 (ja) * | 2020-01-31 | 2021-08-05 | Jfeスチール株式会社 | 鋼板、部材及びそれらの製造方法 |
| WO2021193057A1 (ja) * | 2020-03-27 | 2021-09-30 | Motp合同会社 | 鋼材及びその製造方法 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4375384A4 |
Cited By (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2024029145A1 (ja) * | 2022-08-03 | 2024-02-08 | 日本製鉄株式会社 | 鋼板 |
| JPWO2024029145A1 (ja) * | 2022-08-03 | 2024-02-08 | ||
| WO2025013460A1 (ja) * | 2023-07-12 | 2025-01-16 | Jfeスチール株式会社 | 鋼板、部材および部品並びにそれらの製造方法 |
| JP7652346B1 (ja) * | 2023-07-12 | 2025-03-27 | Jfeスチール株式会社 | 鋼板、部材および部品並びにそれらの製造方法 |
| JPWO2025075096A1 (ja) * | 2023-10-04 | 2025-04-10 | ||
| WO2025075096A1 (ja) * | 2023-10-04 | 2025-04-10 | Jfeスチール株式会社 | 骨格部材 |
| JPWO2025150337A1 (ja) * | 2024-01-09 | 2025-07-17 | ||
| WO2025150337A1 (ja) * | 2024-01-09 | 2025-07-17 | Jfeスチール株式会社 | 亜鉛系めっき鋼板及びその製造方法 |
| JPWO2025150338A1 (ja) * | 2024-01-09 | 2025-07-17 | ||
| WO2025150338A1 (ja) * | 2024-01-09 | 2025-07-17 | Jfeスチール株式会社 | 亜鉛系めっき鋼板及びその製造方法 |
| JP7786646B2 (ja) | 2024-01-09 | 2025-12-16 | Jfeスチール株式会社 | 亜鉛系めっき鋼板及びその製造方法 |
| JP7786644B2 (ja) | 2024-01-09 | 2025-12-16 | Jfeスチール株式会社 | 亜鉛系めっき鋼板及びその製造方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| JPWO2023026819A1 (ja) | 2023-03-02 |
| MX2024002348A (es) | 2024-03-13 |
| CN117795113A (zh) | 2024-03-29 |
| US20250137084A1 (en) | 2025-05-01 |
| KR20240032937A (ko) | 2024-03-12 |
| JP7294549B1 (ja) | 2023-06-20 |
| EP4375384A1 (en) | 2024-05-29 |
| EP4375384A4 (en) | 2024-11-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7294549B1 (ja) | 高強度鋼板およびその製造方法 | |
| JP7367893B1 (ja) | 高強度鋼板、高強度鋼板を用いてなる部材、部材からなる自動車の骨格構造部品用又は自動車の補強部品、ならびに高強度鋼板及び部材の製造方法 | |
| CN117062928B (zh) | 镀锌钢板、部件以及它们的制造方法 | |
| JP7601257B2 (ja) | 鋼板、部材およびそれらの製造方法 | |
| US20250313912A1 (en) | Steel sheet, member, and methods for producing same | |
| JP7537634B2 (ja) | 鋼板、部材およびそれらの製造方法 | |
| JP7619483B2 (ja) | 亜鉛めっき鋼板、部材およびそれらの製造方法 | |
| WO2023007833A1 (ja) | 亜鉛めっき鋼板および部材、ならびに、それらの製造方法 | |
| JP7197062B1 (ja) | 亜鉛めっき鋼板および部材、ならびに、それらの製造方法 | |
| JP7364119B1 (ja) | 溶融亜鉛めっき鋼板、溶融亜鉛めっき鋼板を用いてなる部材、部材からなる自動車の骨格構造部品用又は自動車の補強部品、ならびに溶融亜鉛めっき鋼板及び部材の製造方法 | |
| JP7601256B2 (ja) | 鋼板、部材およびそれらの製造方法 | |
| JP7820407B2 (ja) | 鋼板、部材およびそれらの製造方法 | |
| JP7613635B2 (ja) | 亜鉛めっき鋼板、部材及びそれらの製造方法 | |
| JP7473860B1 (ja) | 高強度鋼板、その製造方法、部材及び自動車部品 | |
| JP7711775B2 (ja) | 溶融亜鉛めっき鋼板、溶融亜鉛めっき鋼板を用いてなる部材、部材からなる自動車の骨格構造部品又は自動車の補強部品、ならびに溶融亜鉛めっき鋼板及び部材の製造方法 | |
| EP4663784A1 (en) | Zinc-plated steel sheet, member, and methods for producing same |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 2022576110 Country of ref document: JP Kind code of ref document: A |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 22861109 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202280054470.9 Country of ref document: CN |
|
| ENP | Entry into the national phase |
Ref document number: 20247004226 Country of ref document: KR Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1020247004226 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 18683349 Country of ref document: US |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202417010192 Country of ref document: IN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2022861109 Country of ref document: EP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2401001110 Country of ref document: TH |
|
| ENP | Entry into the national phase |
Ref document number: 2022861109 Country of ref document: EP Effective date: 20240220 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWP | Wipo information: published in national office |
Ref document number: 18683349 Country of ref document: US |