CN202491331U - Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive - Google Patents

Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive Download PDF

Info

Publication number
CN202491331U
CN202491331U CN2012200736295U CN201220073629U CN202491331U CN 202491331 U CN202491331 U CN 202491331U CN 2012200736295 U CN2012200736295 U CN 2012200736295U CN 201220073629 U CN201220073629 U CN 201220073629U CN 202491331 U CN202491331 U CN 202491331U
Authority
CN
China
Prior art keywords
screw extruder
bopp
foreign matter
double screw
twin
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Expired - Fee Related
Application number
CN2012200736295U
Other languages
Chinese (zh)
Inventor
杨思班
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
ZHEJIANG HIASIA TECHNOLOGY Co Ltd
Original Assignee
ZHEJIANG HIASIA TECHNOLOGY Co Ltd
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by ZHEJIANG HIASIA TECHNOLOGY Co Ltd filed Critical ZHEJIANG HIASIA TECHNOLOGY Co Ltd
Priority to CN2012200736295U priority Critical patent/CN202491331U/en
Application granted granted Critical
Publication of CN202491331U publication Critical patent/CN202491331U/en
Anticipated expiration legal-status Critical
Expired - Fee Related legal-status Critical Current

Links

Images

Classifications

    • B—PERFORMING OPERATIONS; TRANSPORTING
    • B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
    • B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
    • B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
    • B29C48/25—Component parts, details or accessories; Auxiliary operations
    • B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
    • B29C48/375—Plasticisers, homogenisers or feeders comprising two or more stages
    • B29C48/39—Plasticisers, homogenisers or feeders comprising two or more stages a first extruder feeding the melt into an intermediate location of a second extruder
    • B—PERFORMING OPERATIONS; TRANSPORTING
    • B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
    • B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
    • B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
    • B29C48/25—Component parts, details or accessories; Auxiliary operations
    • B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
    • B29C48/395—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die using screws surrounded by a cooperating barrel, e.g. single screw extruders
    • B29C48/40—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die using screws surrounded by a cooperating barrel, e.g. single screw extruders using two or more parallel screws or at least two parallel non-intermeshing screws, e.g. twin screw extruders

Landscapes

  • Engineering & Computer Science (AREA)
  • Mechanical Engineering (AREA)
  • Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
  • Processes Of Treating Macromolecular Substances (AREA)

Abstract

本实用新型公开了一种用于BOPP母料添加剂的生产装置,主要包括喂料斗、螺旋喂料器、双螺杆挤出机、冷却水槽、切粒机和振动筛,所述的喂料斗与螺旋喂料器之间设置有一除铁装置,可将原料中的金属异物进行清除,防止金属异物进入双螺杆挤出机内造成机械性破坏;所述的螺旋喂料器的传动电机采用调速电机,可根据生产工艺的不同方便地调节原料的喂入量,保证了原料的融熔和共聚反应效果;所述的双螺杆挤出机的加热区设有8组,并采用热电阻传导加热方式,尾端还设有一过滤网,可防止未经完全融熔的原料或异物挤出。

Figure 201220073629

The utility model discloses a production device for BOPP masterbatch additives, which mainly includes a feeding hopper, a screw feeder, a twin-screw extruder, a cooling water tank, a pelletizer and a vibrating screen. The feeding hopper and the screw There is an iron removal device between the feeders, which can remove the metal foreign matter in the raw material, and prevent the metal foreign matter from entering the twin-screw extruder and causing mechanical damage; the transmission motor of the screw feeder adopts a speed-regulating motor , the feeding amount of raw materials can be adjusted conveniently according to different production processes, ensuring the melting and copolymerization effect of raw materials; the heating zone of the twin-screw extruder is equipped with 8 groups, and thermal resistance conduction heating is adopted , There is also a filter screen at the end to prevent the raw material or foreign matter from being completely melted from being squeezed out.

Figure 201220073629

Description

The process units that is used for BOPP masterbatch additive
(1) technical field
The utility model relates to field of plastics processing, is specifically related to a kind of production and processing device of BOPP masterbatch additive.
(2) background technology
Along with the continuous development of flexible package industry, ordinary packing has satisfied not the people's life requirement, and the paper class Soft Roll market demand is growing.The BOPP film is wherein a kind of functional plastic packaging material with superperformance; Kind of series of products surplus the antifogging film that development forms, heat-sealing film, ultra-thin high matt film, torsion film, the label film etc. ten have been widely used in the packaging industries such as food, clothes and handicraft.BOPP masterbatch additive is in process, and is generally all composite through flowing freely particle by polyphosphazene polymer alkene alpha-olefin, finally makes mixing polymer, is the top layer additive of producing the BOPP function film.Because the difference of the raw material of types of functionality sexupara feed additives is bigger; And it is all variant to the melting temperature in the process of manufacture, copolyreaction duration etc.; Particularly the production technology of masterbatch additive and masterbatch has bigger difference, and general masterbatch process units can not adapt to the production and the processing of some special masterbatch additives.
(3) summary of the invention
The utility model provides a kind of processing unit (plant) of suitable BOPP film masterbatch Additive Production, and its main technical schemes is following:
A kind of process units that is used for BOPP masterbatch additive; Mainly comprise feeding hopper, scroll feeder, double screw extruder, bosh, pelleter and vibratory sieve; Be provided with a deironing apparatus between said feeding hopper and the scroll feeder; Scroll feeder can feed the raw making materials of masterbatch additive to the head chamber of double screw extruder through feed opening by the stability of flow ground of setting, and raw material is extruded and passed through to draw tie rod from the afterbody of double screw extruder after the melting and copolyreaction of double screw extruder; Make many group strip material get into immersion cooling in the bosh; The strip material gets into the pelleter pelletizing after cooling and drying, be discharged in the vibratory sieve by pelleter subsequently and sieve; The finished particle material that granularity meets directly packs through feed opening, and the powder-material that screens out out then carries out recycling through the discharging opening of vibratory sieve bottom.
As preferably, the thermal treatment zone of the described double screw extruder of the utility model is provided with 8 groups, and adopts thermal resistance conduction mode of heating.
As preferably, the utility model also is provided with a screen pack at the tail end of double screw extruder, can prevent to extrude without the raw material or the foreign matter of melting fully.
As preferably, the driving motor of the described scroll feeder of the utility model adopts buncher, can carry out speed regulation according to the flow size of feeding material.
The beneficial effect of the utility model is embodied in: be provided with a deironing apparatus between feeding hopper and the scroll feeder, can the metallic foreign body in the raw material be removed, prevent to cause mechanical destruction in the metallic foreign body entering double screw extruder; Adopt the feeding manner of adjustable-speed, can regulate the feed quantity of raw material easily, guarantee the melting and the copolyreaction effect of raw material according to the difference of production technology; The screen pack that the double screw extruder tail end is provided with can prevent to extrude without the raw material or the foreign matter of melting fully, guarantees the reliability of melting material traction and tie rod.
(4) description of drawings
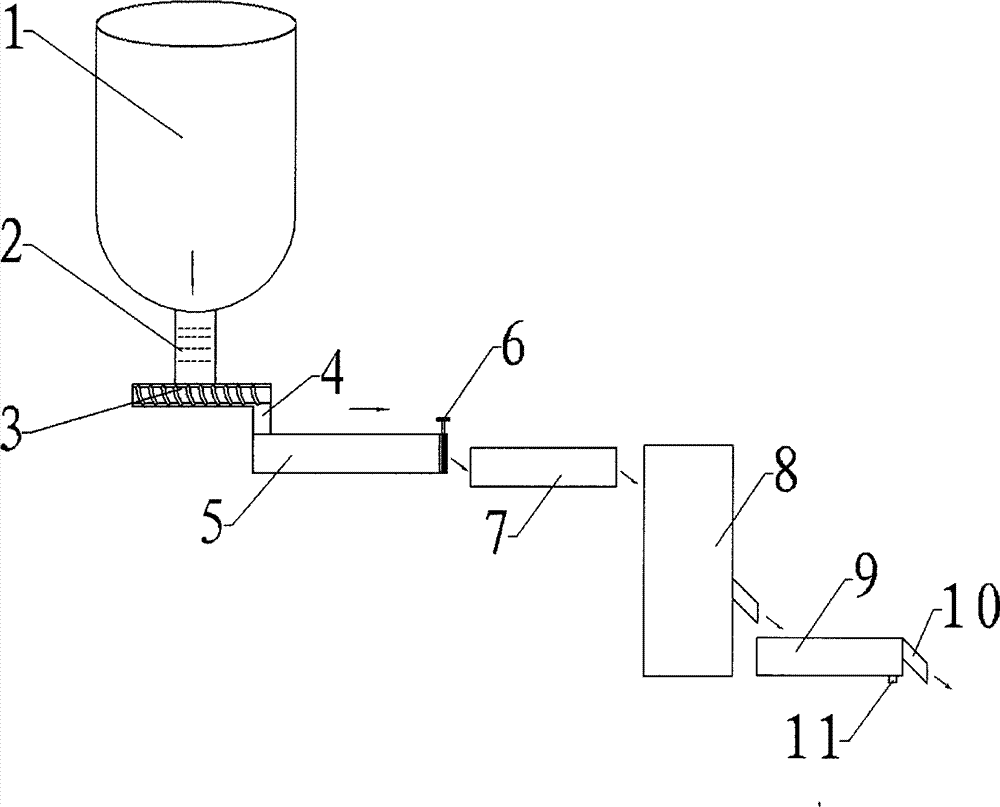
Fig. 1 is the structural representation of the utility model
(5) specific embodiment
Shown in accompanying drawing; The process units of a kind of BOPP of being used for masterbatch additive that the utility model relates to; Mainly comprise feeding hopper 1, scroll feeder 3, double screw extruder 5, bosh 7, pelleter 8 and vibratory sieve 9; Be provided with a deironing apparatus 2 between feeding hopper 1 and the scroll feeder 3, deironing apparatus 2 can be removed the metallic foreign body in the raw material, prevents to cause mechanical destruction in the metallic foreign body entering double screw extruder 5; The driving motor of scroll feeder 3 adopts buncher, can the raw making materials of masterbatch additive be fed to the head chamber of double screw extruder 5 through feed opening 4 by the stability of flow ground of setting; The thermal treatment zone of double screw extruder 5 is provided with 8 groups; And adopt thermal resistance to conduct mode of heating; Raw material is after the melting and copolyreaction of double screw extruder 5; Extrude and through the traction tie rod, the tail end of double screw extruder 5 also is provided with a screen pack 6 from the afterbody of double screw extruder 5, can prevent to extrude without the raw material or the foreign matter of fully melting; Many groups strip material through double screw extruder 5 is extruded carries out the immersion water-cooled but through drawing to get in the bosh 7; The strip material is after cooling and drying; Get into pelleter 8 pelletizings; Be discharged in the vibratory sieve 9 by pelleter 8 subsequently and sieve, the finished particle material that granularity meets directly packs through feed opening 10, and the powder-material that screens out out then carries out recycling through the discharging opening 11 of vibratory sieve 9 bottoms.

Claims (2)

1. process units that is used for BOPP masterbatch additive; Comprise feeding hopper, scroll feeder, double screw extruder, bosh, pelleter and vibratory sieve; It is characterized in that: be provided with a deironing apparatus between said feeding hopper and the scroll feeder; The driving motor of scroll feeder adopts buncher, and the thermal treatment zone of said double screw extruder is provided with 8 groups, and adopts thermal resistance conduction mode of heating.
2. a kind of process units that is used for BOPP masterbatch additive according to claim 1, it is characterized in that: the tail end of said double screw extruder also is provided with a screen pack.
CN2012200736295U 2012-02-29 2012-02-29 Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive Expired - Fee Related CN202491331U (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN2012200736295U CN202491331U (en) 2012-02-29 2012-02-29 Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN2012200736295U CN202491331U (en) 2012-02-29 2012-02-29 Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive

Publications (1)

Publication Number Publication Date
CN202491331U true CN202491331U (en) 2012-10-17

Family

ID=46997570

Family Applications (1)

Application Number Title Priority Date Filing Date
CN2012200736295U Expired - Fee Related CN202491331U (en) 2012-02-29 2012-02-29 Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive

Country Status (1)

Country Link
CN (1) CN202491331U (en)

Similar Documents

Publication Publication Date Title
CN204546994U (en) A kind of plastic extruder with feed arrangement
CN204249209U (en) A kind of blanking device of plunger-type injection molding machine
CN204869587U (en) A twin-screw extruder for molding plastic pellets
CN102205655B (en) Continuous production process of polyethylene (PE) breathable film
CN204546993U (en) A kind of feed arrangement of plastic extruder
CN102205654A (en) One-step production process of polyethylene (PE) breathable film
CN102363333B (en) Equipment for producing inorganic matter fine particle-coated plastic particles
CN202491332U (en) Energy-saving type processing device for biaxially-oriented polypropylene (BOPP) master batch production
CN105906904A (en) Energy-saving environment-friendly process for preparing high-pressure polyethylene with waste packaging films
CN203282696U (en) Dedicated device for producing massive hot-melt pressure-sensitive adhesive
CN206326764U (en) Impurity removal device for plastic granule production
JP2019015497A (en) Method of drying resin, method of producing resin composition, and method of producing film
CN206085393U (en) Extrusion molding machine for plastic pellet production
CN103587092B (en) EVA film extruder with feed adjustment function
CN205467222U (en) Novel extruder
CN105619749B (en) There is the method for work for the EVA film extruder for being fed hydraulic regulation
CN207207170U (en) Packaging film production line
CN103286874A (en) Special device for producing block-shaped hot melt pressure sensitive adhesive
WO2016059572A2 (en) A plant and method for making a plastic film
CN207077739U (en) A kind of extrusion device of bidirectional stretching polypropylene film
CN216329945U (en) Feeding barrel for plastic machinery
CN205167502U (en) New extruder die for granulation
CN202764190U (en) Feeding film blowing device for chemical industry
JP4707377B2 (en) Molding method for thermoplastic resin film
CN203141824U (en) Plastic extrusion film-pressing apparatus for production of regenerated plastics

Legal Events

Date Code Title Description
C14 Grant of patent or utility model
GR01 Patent grant
C17 Cessation of patent right
CF01 Termination of patent right due to non-payment of annual fee

Granted publication date: 20121017

Termination date: 20130229

CF01 Termination of patent right due to non-payment of annual fee