CN202491332U - Energy-saving type processing device for biaxially-oriented polypropylene (BOPP) master batch production - Google Patents
Energy-saving type processing device for biaxially-oriented polypropylene (BOPP) master batch production Download PDFInfo
- Publication number
- CN202491332U CN202491332U CN2012200736384U CN201220073638U CN202491332U CN 202491332 U CN202491332 U CN 202491332U CN 2012200736384 U CN2012200736384 U CN 2012200736384U CN 201220073638 U CN201220073638 U CN 201220073638U CN 202491332 U CN202491332 U CN 202491332U
- Authority
- CN
- China
- Prior art keywords
- screw extruder
- twin
- bopp
- energy
- masterbatch
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/375—Plasticisers, homogenisers or feeders comprising two or more stages
- B29C48/39—Plasticisers, homogenisers or feeders comprising two or more stages a first extruder feeding the melt into an intermediate location of a second extruder
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/36—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die
- B29C48/395—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die using screws surrounded by a cooperating barrel, e.g. single screw extruders
- B29C48/40—Means for plasticising or homogenising the moulding material or forcing it through the nozzle or die using screws surrounded by a cooperating barrel, e.g. single screw extruders using two or more parallel screws or at least two parallel non-intermeshing screws, e.g. twin screw extruders
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C48/00—Extrusion moulding, i.e. expressing the moulding material through a die or nozzle which imparts the desired form; Apparatus therefor
- B29C48/25—Component parts, details or accessories; Auxiliary operations
- B29C48/78—Thermal treatment of the extrusion moulding material or of preformed parts or layers, e.g. by heating or cooling
- B29C48/875—Thermal treatment of the extrusion moulding material or of preformed parts or layers, e.g. by heating or cooling for achieving a non-uniform temperature distribution, e.g. using barrels having both cooling and heating zones
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
Abstract
本实用新型公开了一种用于BOPP母料生产的节能型加工装置,主要包括喂料斗、螺旋喂料器、双螺杆挤出机、冷却水槽、切粒机和振动筛,所述的喂料斗与螺旋喂料器之间设置有一除铁装置,可将原料中的金属异物进行清除,防止金属异物进入双螺杆挤出机内造成机械性破坏;所述的螺旋喂料器的传动电机采用调速电机,可根据生产工艺的不同方便地调节原料的喂入量,保证了原料的融熔和共聚反应效果;所述的双螺杆挤出机的加热方式采用电磁感应加热器,共设有10组加热区,并采用分组单独控制方式,可根据母料生产工艺的要求方便地调节双螺杆挤出机各区域的控制温度。
The utility model discloses an energy-saving processing device for the production of BOPP masterbatch, which mainly includes a feeding hopper, a screw feeder, a twin-screw extruder, a cooling water tank, a pelletizer and a vibrating screen. The feeding hopper There is an iron removal device between the screw feeder, which can remove the metal foreign matter in the raw material, and prevent the metal foreign matter from entering the twin-screw extruder and causing mechanical damage; the transmission motor of the screw feeder adopts an adjustable The high-speed motor can easily adjust the feeding amount of raw materials according to different production processes, ensuring the melting and copolymerization reaction effect of raw materials; the heating method of the twin-screw extruder adopts electromagnetic induction heaters, and a total of 10 Group heating zones, and adopt grouping and individual control, the control temperature of each zone of the twin-screw extruder can be conveniently adjusted according to the requirements of the masterbatch production process.
Description
(一)技术领域 (1) Technical field
本实用新型涉及塑料加工领域,具体涉及一种新型的BOPP母料生产加工装置。The utility model relates to the field of plastic processing, in particular to a novel production and processing device for BOPP masterbatch.
(二)背景技术 (2) Background technology
随着软包装工业的不断发展,普通包装已经满足不了人民的生活需求,纸塑类软包市场需求日益增长。BOPP薄膜是其中一种具有良好性能的功能性塑性包装材料,发展形成的防雾滴膜、热封膜、超薄高消光膜、扭结膜、标签膜等十余种系列产品,已广泛应用于食品、服装及工艺品等包装行业中。BOPP母料及母料添加剂等产品在加工过程中,一般都通过由高分子聚烯烃α-烯烃自由流动粒子复配,最终制得混炼聚合物。由于各类功能性母料及添加剂的原料区别较大,且对生产加工过程中的融熔温度、共聚反应时长等都有差异,特别是螺杆挤出机冷态开机的预热时间较长,因此该类加工设备的电费支出占生产成本的比例较大,另外,螺杆挤出机采用热电阻传导加热的方式在生产过程中控制各加热区的融熔温度不十分精确,是制约BOPP母料产品最终理化特性的主要因素。With the continuous development of the flexible packaging industry, ordinary packaging can no longer meet the needs of people's lives, and the market demand for paper-plastic soft packaging is increasing day by day. BOPP film is one of the functional plastic packaging materials with good performance. It has developed more than ten series of products such as anti-fogging film, heat-sealing film, ultra-thin high-matt film, twist film, label film, etc., which have been widely used in Food, clothing and handicrafts and other packaging industries. In the process of processing BOPP masterbatch and masterbatch additives, etc., they are generally compounded with high molecular polyolefin α-olefin free-flowing particles to finally obtain a mixed polymer. Since the raw materials of various functional masterbatches and additives are quite different, and there are differences in the melting temperature and copolymerization reaction time in the production and processing process, especially the preheating time for the cold start of the screw extruder is long, so The electricity expense of this type of processing equipment accounts for a large proportion of the production cost. In addition, the screw extruder adopts thermal resistance conduction heating to control the melting temperature of each heating zone during the production process, which is not very accurate, which restricts BOPP master batch products. The main factor of the final physical and chemical properties.
(三)发明内容 (3) Contents of the invention
本实用新型提供了一种适合BOPP薄膜母料生产的新型加工装置,其主要技术方案如下:The utility model provides a novel processing device suitable for the production of BOPP film masterbatch, and its main technical scheme is as follows:
一种用于BOPP母料生产的节能型加工装置,主要包括喂料斗、螺旋喂料器、双螺杆挤出机、冷却水槽、切粒机和振动筛,所述喂料斗与螺旋喂料器之间设置有一除铁装置,螺旋喂料器可将母料的制作原料按设定的流量稳定地通过下料口喂入至双螺杆挤出机的机头腔内,原料经双螺杆挤出机的融熔和共聚反应后,从双螺杆挤出机的尾部挤出并通过牵引拉条,使多组条状料进入冷却水槽内浸入式冷却,冷却水槽设有进水口和出水口,进水口设置在冷却水槽前端的底部,出水口设置在冷却水槽后端的上部,条状料经冷却并干燥后,进入切粒机切粒,随后由切粒机卸入振动筛内筛分,粒度符合的成品颗粒料通过下料口直接装袋,筛除出的粉状料则通过振动筛底部的出料口进行回收再利用。An energy-saving processing device for the production of BOPP masterbatch, mainly including a feeding hopper, a screw feeder, a twin-screw extruder, a cooling water tank, a pelletizer and a vibrating screen. There is an iron removal device in between. The screw feeder can stably feed the raw materials of the masterbatch into the head cavity of the twin-screw extruder through the discharge port according to the set flow rate, and the raw materials pass through the twin-screw extruder. After the melting and copolymerization reaction, it is extruded from the tail of the twin-screw extruder and passed through the pulling rod, so that multiple groups of strip materials enter the cooling water tank for immersion cooling. The cooling water tank is equipped with a water inlet and a water outlet. It is set at the bottom of the front end of the cooling water tank, and the water outlet is set at the upper part of the rear end of the cooling water tank. After the strip material is cooled and dried, it enters the granulator for cutting, and then the granulator is discharged into the vibrating screen for screening. The finished granular material is directly bagged through the discharge port, and the powdery material screened out is recycled and reused through the discharge port at the bottom of the vibrating screen.
作为优选,本实用新型所述的螺旋喂料器的传动电机采用调速电机,可根据喂入物料的流量大小进行速度调节。As a preference, the transmission motor of the screw feeder described in the utility model adopts a speed-regulating motor, and the speed can be adjusted according to the flow rate of the fed material.
作为优选,本实用新型所述的双螺杆挤出机的加热方式采用电磁感应加热器,共设有10组加热区,并采用分组单独控制方式,可根据母料生产工艺的要求方便地调节双螺杆挤出机各区域的控制温度。As a preference, the heating method of the twin-screw extruder described in the utility model adopts an electromagnetic induction heater, and there are 10 groups of heating zones in total, and adopts a grouping and individual control mode, which can conveniently adjust the twin-screw extruder according to the requirements of the masterbatch production process. Control temperature in each zone of the screw extruder.
作为优选,本实用新型在双螺杆挤出机的尾端还设有一过滤网,可防止未经完全融熔的原料或异物挤出。As a preference, the utility model is also equipped with a filter screen at the tail end of the twin-screw extruder, which can prevent raw materials or foreign matter not completely melted from being extruded.
本实用新型的有益效果有:The beneficial effects of the utility model have:
1、喂料斗与螺旋喂料器之间设置有一除铁装置,可将原料中的金属异物进行清除,防止金属异物进入双螺杆挤出机内造成机械性破坏。1. There is an iron removal device between the feeding hopper and the screw feeder, which can remove the metal foreign matter in the raw material and prevent the metal foreign matter from entering the twin-screw extruder and causing mechanical damage.
2、采用速度可调的喂料方式,可根据生产工艺的不同方便地调节原料的喂入量,保证原料的融熔和共聚反应效果。2. The feeding method with adjustable speed can be used to conveniently adjust the feeding amount of raw materials according to different production processes, so as to ensure the melting and copolymerization reaction effect of raw materials.
3、双螺杆挤出机尾端设置的过滤网,可防止未经完全融熔的原料或异物挤出,保证融熔料牵引与拉条的可靠性。3. The filter screen installed at the end of the twin-screw extruder can prevent the extrusion of raw materials or foreign objects that have not been completely melted, and ensure the reliability of the pulling of the molten material and the pulling of the rod.
4、双螺杆挤出机的加热方式采用电磁感应加热器,通过高频脉冲电流加到套在双螺杆挤出机金属融熔筒上的感应圈上,从而产生高速变化的交变磁场,由磁场的磁力穿过金属融熔筒产生涡流使金属材料自身快速发热,从而使金属融熔筒内的原料得到快速加热和融熔。该种加热方式加热迅速,预热时间短,热量损失小,热利用率可高达80%以上,节能效果明显。4. The heating method of the twin-screw extruder adopts an electromagnetic induction heater, and the high-frequency pulse current is applied to the induction coil set on the metal melting cylinder of the twin-screw extruder, thereby generating a high-speed changing alternating magnetic field, which is controlled by The magnetic force of the magnetic field passes through the metal melting cylinder to generate eddy current, which makes the metal material itself heat rapidly, so that the raw materials in the metal melting cylinder are rapidly heated and melted. This kind of heating method heats up quickly, the warm-up time is short, the heat loss is small, the heat utilization rate can be as high as more than 80%, and the energy-saving effect is obvious.
(四)附图说明 (4) Description of drawings
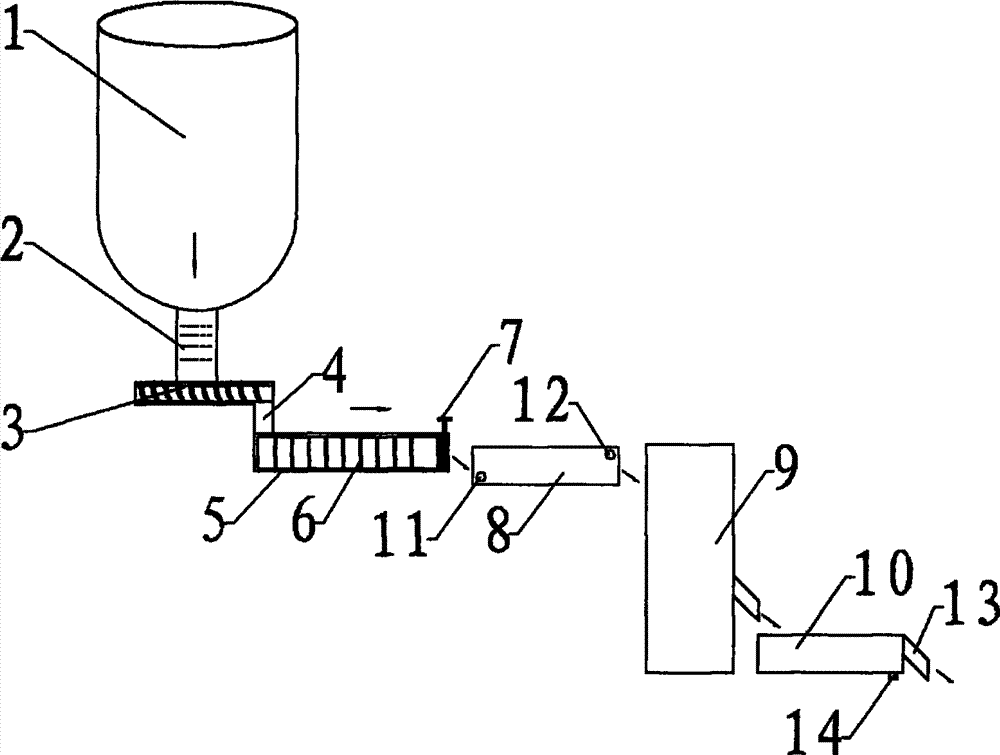
图1为本实用新型的结构示意图Fig. 1 is the structural representation of the utility model
(五)具体实施方式 (5) Specific implementation methods
如附图所示,本实用新型涉及的一种用于BOPP母料生产的节能型加工装置,主要包括喂料斗1、螺旋喂料器3、双螺杆挤出机5、冷却水槽8、切粒机9和振动筛10,所述喂料斗1与螺旋喂料器3之间设置有一除铁装置2,可将原料中的金属异物进行清除,防止金属异物进入双螺杆挤出机内造成机械性破坏;螺旋喂料器3的传动电机采用调速电机,可将母料的制作原料按设定的流量稳定地通过下料口4喂入至双螺杆挤出机5的机头腔内,双螺杆挤出机5的加热方式采用电磁感应加热器,共设有10组加热区6,并采用分组单独控制方式,可根据母料的加工特性方便地调节双螺杆挤出机各区域的控制温度;原料经双螺杆挤出机5的融熔和共聚反应后,从双螺杆挤出机5的尾部挤出并通过牵引拉条,双螺杆挤出机5的尾端还设有一过滤网7,可防止未经完全融熔的原料或异物挤出;经牵引拉条的多组条状料进入冷却水槽8内进行浸入式冷却,冷却水槽8设有进水口11和出水口12,进水口11设置在冷却水槽8前端的底部,出水口12设置在冷却水槽8后端的上部,条状料经冷却并干燥后,进入切粒机9切粒,随后由切粒机9卸入振动筛10内筛分,粒度符合的成品颗粒料通过下料口13直接装袋,筛除出的粉状料则通过振动筛10底部的出料口14进行回收再利用。As shown in the drawings, the utility model relates to an energy-saving processing device for the production of BOPP masterbatch, mainly including a feeding hopper 1, a screw feeder 3, a twin-screw extruder 5, a cooling water tank 8, a pelletizer extruder 9 and vibrating screen 10, and an iron removal device 2 is arranged between the feeding hopper 1 and the screw feeder 3, which can remove the metal foreign matter in the raw material and prevent the metal foreign matter from entering the twin-screw extruder and causing mechanical damage. Destruction; the transmission motor of the screw feeder 3 adopts a speed-regulating motor, which can stably feed the raw materials of the masterbatch into the head cavity of the twin-screw extruder 5 through the discharge port 4 according to the set flow rate. The heating method of the screw extruder 5 adopts an electromagnetic induction heater, and there are 10 groups of heating zones 6 in total, and adopts a separate control method in groups, which can conveniently adjust the control temperature of each area of the twin-screw extruder according to the processing characteristics of the masterbatch The raw material is extruded from the afterbody of the twin-screw extruder 5 after the melting and copolymerization reaction of the twin-screw extruder 5 and passed through the pulling rod, and the tail end of the twin-screw extruder 5 is also provided with a filter screen 7, It can prevent the extrusion of raw materials or foreign objects that have not been completely melted; multiple groups of strip materials that have been drawn into the cooling water tank 8 for immersion cooling, the cooling water tank 8 is equipped with a water inlet 11 and a water outlet 12, and the water inlet 11 Set at the bottom of the front end of the cooling water tank 8, and the water outlet 12 is set at the upper part of the rear end of the cooling water tank 8. After the strip material is cooled and dried, it enters the pelletizer 9 for pelletizing, and then the pelletizer 9 is discharged into the vibrating screen 10. After sieving, the finished granular material with a consistent particle size is directly bagged through the discharge port 13, and the powdered material screened out is recycled through the discharge port 14 at the bottom of the vibrating screen 10.
Claims (2)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012200736384U CN202491332U (en) | 2012-02-29 | 2012-02-29 | Energy-saving type processing device for biaxially-oriented polypropylene (BOPP) master batch production |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012200736384U CN202491332U (en) | 2012-02-29 | 2012-02-29 | Energy-saving type processing device for biaxially-oriented polypropylene (BOPP) master batch production |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202491332U true CN202491332U (en) | 2012-10-17 |
Family
ID=46997571
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012200736384U Expired - Fee Related CN202491332U (en) | 2012-02-29 | 2012-02-29 | Energy-saving type processing device for biaxially-oriented polypropylene (BOPP) master batch production |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202491332U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104787597A (en) * | 2015-02-09 | 2015-07-22 | 江苏中立方实业有限公司 | Polypropylene capacitor film feeding method |
| CN105946196A (en) * | 2016-05-20 | 2016-09-21 | 成都科力夫科技有限公司 | Screw extruder with prepressing function |
-
2012
- 2012-02-29 CN CN2012200736384U patent/CN202491332U/en not_active Expired - Fee Related
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104787597A (en) * | 2015-02-09 | 2015-07-22 | 江苏中立方实业有限公司 | Polypropylene capacitor film feeding method |
| CN105946196A (en) * | 2016-05-20 | 2016-09-21 | 成都科力夫科技有限公司 | Screw extruder with prepressing function |
| CN105946196B (en) * | 2016-05-20 | 2018-07-17 | 佛山市南海慷德家居制品有限公司 | A kind of screw rod banded extruder with pre-pressing function |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204546994U (en) | A kind of plastic extruder with feed arrangement | |
| CN209006681U (en) | A kind of metal powder extrusion molding apparatus | |
| CN102294767A (en) | Method for recovering and granulating waste plastic | |
| CN205167511U (en) | Cooling air drying device for granulation | |
| CN102205655B (en) | Continuous production process of polyethylene (PE) breathable film | |
| CN104890234A (en) | In-situ polymerization extrusion three-dimensional printer based on ring-opening polymerization of glycolide | |
| CN204547020U (en) | The anti-clogging plastic extruder that a kind of high-frequency electromagnetic with measuring pump heats | |
| CN102205654A (en) | One-step production process of polyethylene (PE) breathable film | |
| CN206201451U (en) | Cooling device for plastic pellet production | |
| CN102363333B (en) | Equipment for producing inorganic matter fine particle-coated plastic particles | |
| CN104943130A (en) | Heating component for plastic extruding machine | |
| CN105906904A (en) | Energy-saving environment-friendly process for preparing high-pressure polyethylene with waste packaging films | |
| CN104760250A (en) | PPS plastic rod production device and production method | |
| CN207359403U (en) | A kind of plastic granulating device | |
| CN202607875U (en) | Device for producing superfine talcum powder polypropylene filling masterbatches | |
| CN202964969U (en) | Novel plastic granulator | |
| CN202491331U (en) | Production device for BOPP (Biaxially-Oriented Polypropylene) master batch additive | |
| CN105034195A (en) | Thermoplastic elastomer prilling process | |
| CN109049769A (en) | A kind of plastic film processing unit (plant) | |
| CN204054570U (en) | A kind of high-efficient energy-saving environment friendly with electromagnetic induction heating moulds volume wire drawing machine | |
| CN202527138U (en) | A granulation device for a mixture of rosin, paraffin and potassium chloride with low softening point | |
| CN207359589U (en) | A kind of twin-screw EVA is plasticized extrusion device | |
| CN207481180U (en) | Extruder head | |
| CN205344025U (en) | Production facility of hollow plate in two -sided tectorial membrane | |
| CN204955363U (en) | Screw extruder |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20121017 Termination date: 20130229 |