CN202492598U - On-line device for electrolyzing and phosphatizing steel wire at normal temperature - Google Patents
On-line device for electrolyzing and phosphatizing steel wire at normal temperature Download PDFInfo
- Publication number
- CN202492598U CN202492598U CN2012201161666U CN201220116166U CN202492598U CN 202492598 U CN202492598 U CN 202492598U CN 2012201161666 U CN2012201161666 U CN 2012201161666U CN 201220116166 U CN201220116166 U CN 201220116166U CN 202492598 U CN202492598 U CN 202492598U
- Authority
- CN
- China
- Prior art keywords
- control device
- current control
- electrolyzer
- electrolyzing
- steel wire
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 229910000831 Steel Inorganic materials 0.000 title claims abstract description 18
- 239000010959 steel Substances 0.000 title claims abstract description 18
- 239000007788 liquid Substances 0.000 claims abstract description 12
- 210000002421 cell wall Anatomy 0.000 claims abstract description 4
- 239000002893 slag Substances 0.000 abstract description 7
- 238000005265 energy consumption Methods 0.000 abstract description 4
- 230000007613 environmental effect Effects 0.000 abstract description 4
- 210000004027 cell Anatomy 0.000 abstract 6
- BHEPBYXIRTUNPN-UHFFFAOYSA-N hydridophosphorus(.) (triplet) Chemical compound [PH] BHEPBYXIRTUNPN-UHFFFAOYSA-N 0.000 abstract 1
- OAICVXFJPJFONN-UHFFFAOYSA-N Phosphorus Chemical compound [P] OAICVXFJPJFONN-UHFFFAOYSA-N 0.000 description 6
- 238000010438 heat treatment Methods 0.000 description 6
- 229910052698 phosphorus Inorganic materials 0.000 description 6
- 239000011574 phosphorus Substances 0.000 description 6
- 238000005516 engineering process Methods 0.000 description 4
- 238000007669 thermal treatment Methods 0.000 description 4
- 238000004519 manufacturing process Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 229910019142 PO4 Inorganic materials 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000005868 electrolysis reaction Methods 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- NBIIXXVUZAFLBC-UHFFFAOYSA-K phosphate Chemical compound [O-]P([O-])([O-])=O NBIIXXVUZAFLBC-UHFFFAOYSA-K 0.000 description 1
- 239000010452 phosphate Substances 0.000 description 1
- 230000001105 regulatory effect Effects 0.000 description 1
- 229910001220 stainless steel Inorganic materials 0.000 description 1
- 239000010935 stainless steel Substances 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
Images

Landscapes
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
Abstract
The utility model discloses an on-line device for electrolyzing and phosphatizing steel wire at normal temperature, and the device comprises an electrolyzing cell, a low bath and a liquid pump, wherein the low bath is arranged below the electrolyzing cell, the liquid pump is arranged in the low bath, a plurality of overflow control devices are arranged between the electrolyzing cell and the low bath, two cathode guide wheels are symmetrically arranged at two ends of the electrolyzing cell, a cathode conductive wheel is arranged outside each cathode guide wheel, a plurality of main anodes and auxiliary anodes are arranged on the cell wall of the electrolyzing cell, and the main anodes and the auxiliary anodes are arranged at intervals, a pulse rectifier system and a current control device are connected outside the electrolyzing cell, the current control device is connected with the main anodes and the auxiliary anodes, the pulse rectifier system is connected with the current control device, and the current control device is controlled to produce impulse current. The device has the advantages of simple structure, convenience in operation, no phosphorous slag, low energy consumption, small occupied space, easiness for popularization of continuous processing, and health and environmental friendliness.
Description
Technical field
The utility model relates to the device of steel wire electrolysis normal temperature phosphating technology on the thermal treatment continuous lines, the device of the online normal temperature electrolytic phosphating of particularly a kind of steel wire.
Background technology
Current, what steel wire phosphatization on the thermal treatment continuous lines adopted is middle temperature phosphating equipment, and mostly this device fabrication material is that anticorrosive stainless-steel sheet is welded; Type of heating generally adopts steam, directly squeezes into steam to the heating tube that places the phosphatization groove, or through the chuck indirect heating; The former heating tube surface is prone to the deposition phosphorus slag, hinders thermal energy transfer, along with long use phosphorus slag accumulates over a long period on the heating tube surface; Energy loss increases gradually, and clearing up phosphorus slag simultaneously wastes time and energy, though latter's cleaning phosphorus slag is comparatively convenient; But equipment manufacturing operation is complicated, cost an arm and a leg, and increased the apparatus maintenance expense, adopts indirect heating to increase energy consumption.
Summary of the invention
The purpose of the utility model is in order to overcome above deficiency, a kind of design science, economy to be provided, and material is easy to get and environmental protection, operates the device of the online normal temperature electrolytic phosphating of easy steel wire.
The device of the online normal temperature electrolytic phosphating of a kind of steel wire of the utility model comprises electrolyzer, Lower tank and liquid pump, below electrolyzer, is provided with Lower tank; In Lower tank, be provided with liquid pump; Between electrolyzer and Lower tank, be provided with a plurality of overflow controls, be arranged with the negative electrode guide wheel, be provided with the negative electrode conductive casters in the outside of each negative electrode guide deflection sheave at the two ends of electrolyzer; On the cell wall of electrolyzer, be provided with a plurality of main anodes and auxilliary anode; And the alternate setting with auxilliary anode of main anode is externally connected with impulse commutation system and current control device at electrolyzer, and current control device is connected with auxilliary anode with main anode; The impulse commutation system is connected with current control device, and the control current gear produces pulsed current.
The steel wire that the utility model can satisfy many group different sizes simultaneously carries out online normal temperature phosphating, changes along with the requirement of thermal treatment process, does not produce phosphorus slag, and energy consumption is low, and it is little to take the place, helps continuous lines technology and promotes the green health environmental protection.
Description of drawings
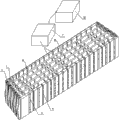
Fig. 1 is the structural representation of the utility model;
Fig. 2 is the electrolytic reaction groove synoptic diagram of the utility model;
Label among the figure: 1-negative electrode guide wheel, 2-negative electrode conductive casters, 3-main anode, the auxilliary anode of 4-, 5-overflow control, 6-liquid pump, 7-current control device, 8-electrolyzer, 9-Lower tank, 10-impulse commutation system.
Embodiment
A kind of embodiment of device of the online normal temperature electrolytic phosphating of a kind of steel wire of the utility model is shown in conjunction with Fig. 1-2, comprises electrolyzer 8, Lower tank 9 and liquid pump 6, below electrolyzer 8, be provided with Lower tank 9; In Lower tank 9, be provided with liquid pump 6; Between electrolyzer 8 and Lower tank 9, be provided with a plurality of overflow controls 5, be arranged with negative electrode guide wheel 1, be provided with negative electrode conductive casters 2 in the outside of each negative electrode guide deflection sheave 1 at the two ends of electrolyzer 8; On the cell wall of electrolyzer 8, be provided with a plurality of main anodes 3 and auxilliary anode 4; And main anode 3 and auxilliary anode 4 alternate settings are externally connected with impulse commutation system 10 and current control device 7 at electrolyzer 8, and current control device 7 is connected with auxilliary anode 4 with main anode 3; Impulse commutation system 10 is connected with current control device 7, and controls said current control device 7 generation pulsed current.
The main anode 3 of bottom, auxilliary anode 4 are connected with the anode of impulse commutation system 10, current control system 11 in the electrolyzer 8, and normal temperature electrolytic phosphating liquid injects electrolytic phosphating groove 8 rapidly under the startup of liquid pump 6, guarantees that the steel wire that is imported into all is immersed in below liquid level 2cm; Regulating surplus valve control 5 flows in Lower tank 9 the phosphatization hydrorrhea; Then steel wire is passed through negative electrode conductive casters 2, divide into groups to depress, get into electrolyzer 8 at negative electrode guide wheel 1; Make between steel wire and separate; Steel wire does not contact with main anode 3 auxilliary anodes 4, opens current control device 7, and steel wire is applied pulsed current; Regulate current control device 7 according to heat treated LV, make steel wire obtain thickness >=8g/ ㎡ phosphatize phosphate coat at the normal temperature electrolytic phosphating.
In sum, the utlity model has following advantage: the steel wire that can satisfy many group different sizes simultaneously carries out online normal temperature phosphating, can change along with the requirement of thermal treatment process; Do not produce phosphorus slag, energy consumption is low, and it is little to take the place; Help continuous lines technology and promote the green health environmental protection.
Claims (1)
1. the device of the online normal temperature electrolytic phosphating of steel wire; It is characterized in that: comprise electrolyzer (8), Lower tank (9) and liquid pump (6); Be provided with Lower tank (9) in said electrolyzer (8) below; In said Lower tank (9), be provided with liquid pump (6), between said electrolyzer (8) and Lower tank (9), be provided with a plurality of overflow controls (5), be arranged with negative electrode guide wheel (1) at the two ends of said electrolyzer (8); Be provided with negative electrode conductive casters (2) in the outside of each said negative electrode guide deflection sheave (1); On the cell wall of said electrolyzer (8), be provided with a plurality of main anodes (3) and auxilliary anode (4), and said main anode (3) and the alternate setting of auxilliary anode (4); Be externally connected with impulse commutation system (10) and current control device (7) at said electrolyzer (8); Said current control device (7) is connected with auxilliary anode (4) with main anode (3), and said impulse commutation system (10) is connected with current control device (7), and controls said current control device (7) generation pulsed current.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012201161666U CN202492598U (en) | 2012-03-26 | 2012-03-26 | On-line device for electrolyzing and phosphatizing steel wire at normal temperature |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012201161666U CN202492598U (en) | 2012-03-26 | 2012-03-26 | On-line device for electrolyzing and phosphatizing steel wire at normal temperature |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202492598U true CN202492598U (en) | 2012-10-17 |
Family
ID=46998834
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012201161666U Expired - Fee Related CN202492598U (en) | 2012-03-26 | 2012-03-26 | On-line device for electrolyzing and phosphatizing steel wire at normal temperature |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202492598U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103603022A (en) * | 2013-11-18 | 2014-02-26 | 贵州钢绳股份有限公司 | Steel wire heat treatment-electrolysis-phosphorization continuous production line equipment and process |
-
2012
- 2012-03-26 CN CN2012201161666U patent/CN202492598U/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103603022A (en) * | 2013-11-18 | 2014-02-26 | 贵州钢绳股份有限公司 | Steel wire heat treatment-electrolysis-phosphorization continuous production line equipment and process |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102703959B (en) | Copper bar continuous travelling tinning method and equipment | |
| CN105951155B (en) | A kind of steel wire double method for bonderizing and its continuous producing apparatus online | |
| CN202705472U (en) | Online phosphating device for metal wires | |
| CN202705545U (en) | Copper bar continuous movement tinning device | |
| CN101165221A (en) | Method and equipment for continuous moving jet tinning of long copper bars | |
| CN103132122B (en) | Steel wire on-line normal-temperature electrolytic phosphatization method | |
| CN102732867B (en) | Online phosphatization apparatus of metal wire rods | |
| CN103397364A (en) | Aluminum-silicon alloy surface ceramic treatment method and apparatus | |
| CN203112938U (en) | Multi-voltage variable-electrode electrolyzer | |
| CN201864609U (en) | Device for removing phosphorous by electrolysis | |
| CN202766645U (en) | Electrolysis phosphorization equipment | |
| CN202090057U (en) | Phosphating device for steel wire surfaces | |
| CN206680548U (en) | A kind of electroxidation leaches and the U-type groove of reduction deposition | |
| CN203429271U (en) | Ceramic treatment device for surface of aluminum-silicon alloy | |
| CN204752848U (en) | Bonderizing production line | |
| CN202492599U (en) | Folding cogging online phosphating device | |
| CN203668535U (en) | Needle spraying reverse flow washing device for electrolytic zinc electrolysis follow-up section cathode plate | |
| CN207391587U (en) | A kind of electrolytic phosphating device for electrolytic phosphating of steel wires | |
| CN203866076U (en) | Complex-breaking and chromium-removing device for tanning dyeing wastewater | |
| CN203546144U (en) | Metal anti-corrosion device | |
| CN204022946U (en) | A kind of heating unit for pickling tank | |
| CN201777923U (en) | Water tank capable of controlling water level and water temperature for treating landfill leachate | |
| CN101709502A (en) | Method for removing copper sheet from surface of titanium and titanium alloy extruded tube | |
| CN103741195B (en) | Electrolytic phosphating of steel wires processes device | |
| CN105040075A (en) | Electroplating equipment |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20121017 Termination date: 20150326 |
|
| EXPY | Termination of patent right or utility model |