EP0140511A1 - Procédé et dispositif pour enlever du matériau en excès des noyaux en sable - Google Patents
Procédé et dispositif pour enlever du matériau en excès des noyaux en sable Download PDFInfo
- Publication number
- EP0140511A1 EP0140511A1 EP84305627A EP84305627A EP0140511A1 EP 0140511 A1 EP0140511 A1 EP 0140511A1 EP 84305627 A EP84305627 A EP 84305627A EP 84305627 A EP84305627 A EP 84305627A EP 0140511 A1 EP0140511 A1 EP 0140511A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- particles
- cores
- stream
- conduit
- impact
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000000463 material Substances 0.000 title claims abstract description 17
- 238000000034 method Methods 0.000 title claims abstract description 13
- 239000002245 particle Substances 0.000 claims abstract description 42
- 239000004033 plastic Substances 0.000 claims description 6
- 229920003023 plastic Polymers 0.000 claims description 6
- -1 polyethylene Polymers 0.000 claims description 4
- 238000005422 blasting Methods 0.000 claims description 3
- CWYNVVGOOAEACU-UHFFFAOYSA-N Fe2+ Chemical compound [Fe+2] CWYNVVGOOAEACU-UHFFFAOYSA-N 0.000 claims description 2
- 239000004698 Polyethylene Substances 0.000 claims description 2
- 239000004743 Polypropylene Substances 0.000 claims description 2
- 229920000573 polyethylene Polymers 0.000 claims description 2
- 229920001155 polypropylene Polymers 0.000 claims description 2
- 230000003628 erosive effect Effects 0.000 abstract description 3
- 239000007779 soft material Substances 0.000 abstract 1
- 238000004140 cleaning Methods 0.000 description 9
- 230000000712 assembly Effects 0.000 description 3
- 238000000429 assembly Methods 0.000 description 3
- 238000000465 moulding Methods 0.000 description 3
- 239000004576 sand Substances 0.000 description 3
- 239000011230 binding agent Substances 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 239000000203 mixture Substances 0.000 description 2
- 240000007049 Juglans regia Species 0.000 description 1
- 235000009496 Juglans regia Nutrition 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 240000008042 Zea mays Species 0.000 description 1
- 235000005824 Zea mays ssp. parviglumis Nutrition 0.000 description 1
- 235000002017 Zea mays subsp mays Nutrition 0.000 description 1
- 238000009825 accumulation Methods 0.000 description 1
- 230000003749 cleanliness Effects 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 235000005822 corn Nutrition 0.000 description 1
- 239000002923 metal particle Substances 0.000 description 1
- 239000011236 particulate material Substances 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 235000020234 walnut Nutrition 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/18—Finishing
Definitions
- This invention relates generally to the art of finishing and cleaning molded articles by directing particulate material against the rough molded article. Impeller systems for directing metal shot against cast metal articles for cleaning the articles is well known.
- the present invention relates more specifically to the finish cleaning of molded sand cores which are made by molding a mixture of sand and a binder, to form a core that may be of complex shape having holes, projections, notches, and other irregularly shaped areas.
- Such articles are far more delicate than the articles which have heretofore been finished by blasting with an impact media, often metal particles moving at high velocities. Accordingly, prior art blasting apparatus and methods have not been adaptable to the problem of automated cleaning of molded sand cores, and the present rubbing by hand methods for cleaning cores are unacceptable because they are time consuming and expensive.
- the present invention provides an apparatus and method in which relatively soft impact particles are showered against the cores in a relatively gentle manner so as to remove flash and other excess material without damaging the cores.
- the apparatus consists of a conveyor on which the relatively light-weight sand cores are supported so that the opposite sides of the cores can be reached by streams of impact particles.
- a plurality of nozzles are positioned both above and below the conveyor and relatively low pressure air is directed through the nozzles in the direction of the sand cores on the conveyors. Large volumes of relatively soft impact particles without any sharp points or edges, such as small pieces of plastic, are entrained in the air so that they will be directed against the sand cores.
- the flash and other excess material is relatively loosely adhered or attached to the main body of the core and as a result, when these loosely adhered pieces are impacted by the moving particles, they are dislodged from the main body of the core. However, when these relatively soft slow moving particles engage the sand core, the particles do not damage or disrupt the surface of the main body of the core.
- the apparatus can be operated continuously to automatically clean and finish a large number of sand cores in a short time.
- the method and apparatus of this invention is advantageous in that it provides for the rapid and thorough cleaning of complex parts by subjecting these parts to showers of particles moving against the parts from different directions so as to finish both internal and external surfaces in the part.
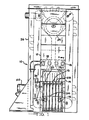
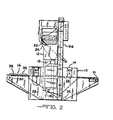
- the apparatus of this invention is shown in Figs. 1 and 2 as including a main frame 12 on which is mounted a housing 14 and a conveyor assembly 16 which is operable to move aand cores to be cleaned through the housing 14.
- a plurality of nozzles 18 are mounted in the housing l4•at positions above the conveyor assembly 16 and a plurality of the same nozzles 18 mounted below the conveyor 16.
- the nozzles 18 are supplied with air by a blower or turbine 20 and a particalized media 22 is fed to the nozzles 18 from a supply hopper 24 located above the nozzles 18.
- An elevator assembly 26, of conventional type, operates to transfer used particles 22 from the bottom of the apparatus and deliver these particles to the hopper 24 for re-use.
- the conveyor assembly 16 is illustrated as including a plurality of endless strands 28 (Fig. 1), similar to ropes or cables, trained about pulley or sheave assemblies 30, 31 and 32 mounted on the main frame 12.
- the pully assembly 30 includes a shaft 34 which is driven by a motor drive assembly 36 so as to move the strands 28 that extend horizontally between the pulley assemblies 30 and 31 from left to right in Fig. 1.
- a plurality of sand cores to be finished, indicated diagrammatically at 38 in Fig. 2, are laid on the horizontal strands 28 and are moved by the strands into the housing 14 to positions between the upwardly and downwardly directed nozzles assemblies 18.
- each of the nozzles 18 consists of a nozzle head 42 rotatably mounted on an injector body 44 which is connected to a conduit 46 through which air is supplied from the blower 20 and a conduit 48 through which the particles 22 are supplied.
- An inclined septum 47 directs the particles in conduit 48 toward the air stream emanating from conduit 46 at the lower edge 49 of the septum 47. Since the air stream in conduit 46 is created by the blower 20, in contrast to a compressor, it is at a low pressure, namely, below 2 psi. As a result, the stream entrains large volumes of the particles 22 falling off the edge 49 in the form of a curtain. This forms a low pressure stream issuing from nozzle head 42 that contains a dense accumulation of particles 22 directed toward sand cores to be cleaned. It is to be understood that the nozzle head 42 can be remote from the injector body 44 and be connected thereto by a suitable passage.
- the result is a relatively soft flow of particles 22 from each nozzle head 42 that provides for a shower of the particles 22 on both the top and bottom sides of the cores 38 supported on the strands 28 in the housing 14.
- a variety of different relatively soft particles 22 that do not have sharp edges or corners, such as walnut shells, corn. cobs and similar non-ferrous media, can be used in apparatus 10. Particles that are as hard as conventional steel shot used for blast cleaning are too hard and cause erosion of a sand core. However, particles 22 formed of plastic and generally cylindrical in shape and processed so as to have rounded edges, as illustrated in Fig. 6, are preferred from the standpoints of effectivness, cost, cleanliness and lack of surface erosion on the core.
- the particles 22 are preferably formed of an easily obtained plastic, such as polyethylene or polypropylene, and are relatively small in size, having a diameter of about 0.07 inches and a length of about 0.10 inches or less.
- a rough molded sand core 38 is shown in Fig. 4.
- the core is of a relatively complex shape having notches 50, openings 52, projections 54, and other irregularly shaped surfaces on which excess material, a mixture of sand and the binder, adhere as indicated at 56.
- These excess adhering portions 56 are sometimes referred to as "flash" and must be removed from the main body 58 of the sand core 38 in order to make the core 38 useable for its intended purpose in a molding process.
- the cores 38 are placed on the conveyor 16 as shown in Fig. 2 so that they travel on the conveyor 16 through the enclosure 14 and are subjected to the fluidized media 22 that is directed from both above and below onto the surfaces of the sand core 38.
- the open construction of the conveyor 16 enables thorough showering of the core 38 from both above and below. After the sand cores 38 emerge from : the housing 14, they are readily useable in molding operations.
- the method and apparatus of this invention provides for the relatively gentle application of soft impact particles against the somewhat vulnerable body 58 of the sand core 38 so as to provide for the complete removal of all of the excess materials 56 on the body 58 without danger of damage to the body 58.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Cleaning In General (AREA)
- Casting Devices For Molds (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US52926083A | 1983-09-06 | 1983-09-06 | |
| US529260 | 1983-09-06 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0140511A1 true EP0140511A1 (fr) | 1985-05-08 |
| EP0140511B1 EP0140511B1 (fr) | 1987-11-04 |
Family
ID=24109161
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19840305627 Expired EP0140511B1 (fr) | 1983-09-06 | 1984-08-17 | Procédé et dispositif pour enlever du matériau en excès des noyaux en sable |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0140511B1 (fr) |
| JP (1) | JPS6072638A (fr) |
| AU (1) | AU574382B2 (fr) |
| CA (1) | CA1214916A (fr) |
| DE (1) | DE3467105D1 (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2019051521A1 (fr) * | 2017-09-18 | 2019-03-21 | Fill Gesellschaft M.B.H. | Procédé pour ébavurer des noyaux de coulée et des moules de coulée |
| US20190170202A1 (en) * | 2016-08-10 | 2019-06-06 | Knorr-Bremse Systeme Fuer Nutzfahrzeuge Gmbh | Brake Carrier |
| WO2021062456A1 (fr) * | 2019-10-03 | 2021-04-08 | Fill Gesellschaft M.B.H. | Procédé de traitement de surface |
| US20220271359A1 (en) * | 2021-02-12 | 2022-08-25 | Bayerische Motoren Werke Aktiengesellschaft | Traction Battery Having a Degassing Collector, and Motor Vehicle |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6533020B2 (en) * | 2001-06-11 | 2003-03-18 | General Motors Corporation | Casting of engine blocks |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2929120A (en) * | 1957-12-04 | 1960-03-22 | Gen Motors Corp | Method of definning sand cores |
| EP0086321A1 (fr) * | 1982-01-18 | 1983-08-24 | Carl Kurt Walther GmbH & Co. KG | Procédé pour l'ébarbage de noyaux fabriquées à partir de matériel granuleux |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS49108692A (fr) * | 1973-02-19 | 1974-10-16 | ||
| JPS5630057A (en) * | 1979-08-15 | 1981-03-26 | Mazda Motor Corp | Deburring method for core |
| JPS58205646A (ja) * | 1982-05-24 | 1983-11-30 | Sintokogio Ltd | 中子のバリ取り方法 |
-
1984
- 1984-08-17 CA CA000461283A patent/CA1214916A/fr not_active Expired
- 1984-08-17 EP EP19840305627 patent/EP0140511B1/fr not_active Expired
- 1984-08-17 DE DE8484305627T patent/DE3467105D1/de not_active Expired
- 1984-08-31 AU AU32632/84A patent/AU574382B2/en not_active Ceased
- 1984-09-04 JP JP18526884A patent/JPS6072638A/ja active Pending
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2929120A (en) * | 1957-12-04 | 1960-03-22 | Gen Motors Corp | Method of definning sand cores |
| EP0086321A1 (fr) * | 1982-01-18 | 1983-08-24 | Carl Kurt Walther GmbH & Co. KG | Procédé pour l'ébarbage de noyaux fabriquées à partir de matériel granuleux |
Non-Patent Citations (1)
| Title |
|---|
| MODERN CASTING, vol. 73, no. 12, December 1983, page 46, Des Plaines, Illinois, US; "Core finisher" "machine eliminates core fins" * |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20190170202A1 (en) * | 2016-08-10 | 2019-06-06 | Knorr-Bremse Systeme Fuer Nutzfahrzeuge Gmbh | Brake Carrier |
| US10837508B2 (en) * | 2016-08-10 | 2020-11-17 | Knorr-Bremse Systeme Fuer Nutzfahrzeuge Gmbh | Brake carrier |
| WO2019051521A1 (fr) * | 2017-09-18 | 2019-03-21 | Fill Gesellschaft M.B.H. | Procédé pour ébavurer des noyaux de coulée et des moules de coulée |
| WO2021062456A1 (fr) * | 2019-10-03 | 2021-04-08 | Fill Gesellschaft M.B.H. | Procédé de traitement de surface |
| US20220271359A1 (en) * | 2021-02-12 | 2022-08-25 | Bayerische Motoren Werke Aktiengesellschaft | Traction Battery Having a Degassing Collector, and Motor Vehicle |
Also Published As
| Publication number | Publication date |
|---|---|
| DE3467105D1 (en) | 1987-12-10 |
| CA1214916A (fr) | 1986-12-09 |
| AU574382B2 (en) | 1988-07-07 |
| AU3263284A (en) | 1985-03-14 |
| EP0140511B1 (fr) | 1987-11-04 |
| JPS6072638A (ja) | 1985-04-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US2996846A (en) | Method and means for deflashing or trimming molded rubber parts | |
| CN105451939B (zh) | 研磨装置以及研磨方法 | |
| EP1427545B1 (fr) | Appareil de depoussierage de materiau particulaire | |
| KR101928700B1 (ko) | 연속 벨트 컨베이어 방식의 쇼트 블라스트 시스템 | |
| CN210678349U (zh) | 一种钢结构通过式抛丸机 | |
| KR930003042B1 (ko) | 샌드 블라스트를 이용한 피가공물의 가공방법 및 장치 | |
| EP0140511B1 (fr) | Procédé et dispositif pour enlever du matériau en excès des noyaux en sable | |
| CN207509047U (zh) | 一种吊钩式抛丸机 | |
| US4659391A (en) | Method and apparatus for removing excess material from sand cores | |
| JP3758919B2 (ja) | 選別コンベヤ | |
| JP3013053B2 (ja) | ブラスト装置 | |
| US10518385B2 (en) | Apparatus and process for surface treating interior of a workpiece | |
| JPH01289666A (ja) | ブラスト装置 | |
| JP3179338B2 (ja) | ブラスト加工装置 | |
| USRE25554E (en) | Method and means for deflashinc or trimming molder rubber parts | |
| JPH0677898B2 (ja) | 被研掃物に連続的に研掃および空気吹付けを行なう装置 | |
| CN112192452B (zh) | 可同时上下抛丸的振动输送槽通过式连续落砂抛丸清理机 | |
| US4780993A (en) | Method and apparatus for surface treating a workpiece | |
| JPH0582570A (ja) | Icモールドのクリーニング装置 | |
| JP2004181580A (ja) | 成形品のバリ取り装置 | |
| EP0095829A1 (fr) | Procédé et appareil pour l'ébarbage de pièces moulées métalliques | |
| JPH0144304Y2 (fr) | ||
| JP4500143B2 (ja) | アイスブラストによる氷粒搬送装置 | |
| JPH03256673A (ja) | 成形品仕上装置 | |
| JPS5973275A (ja) | プラスチツクス製品用シヨツトブラスト機 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB IT |
|
| 17P | Request for examination filed |
Effective date: 19851107 |
|
| 17Q | First examination report despatched |
Effective date: 19860530 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: B & U CORPORATION |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| REF | Corresponds to: |
Ref document number: 3467105 Country of ref document: DE Date of ref document: 19871210 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| ITTA | It: last paid annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19960715 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19960716 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19960724 Year of fee payment: 13 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19970817 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19970817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980501 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |