EP0150226A1 - Verfahren und Vorrichtung zur Vermeidung von Schaumformung beim freifallenden Giessstrahl in Giessformen, Giessrinnen oder andere Gefässe - Google Patents
Verfahren und Vorrichtung zur Vermeidung von Schaumformung beim freifallenden Giessstrahl in Giessformen, Giessrinnen oder andere Gefässe Download PDFInfo
- Publication number
- EP0150226A1 EP0150226A1 EP83113078A EP83113078A EP0150226A1 EP 0150226 A1 EP0150226 A1 EP 0150226A1 EP 83113078 A EP83113078 A EP 83113078A EP 83113078 A EP83113078 A EP 83113078A EP 0150226 A1 EP0150226 A1 EP 0150226A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- molten metal
- containers
- aperture
- cover plate
- atmosphere
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D5/00—Machines or plants for pig or like casting
- B22D5/04—Machines or plants for pig or like casting with endless casting conveyors
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D1/00—Treatment of fused masses in the ladle or the supply runners before casting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D21/00—Casting non-ferrous metals or metallic compounds so far as their metallurgical properties are of importance for the casting procedure; Selection of compositions therefor
- B22D21/02—Casting exceedingly oxidisable non-ferrous metals, e.g. in inert atmosphere
- B22D21/027—Casting heavy metals with low melting point, i.e. less than 1000 degrees C, e.g. Zn 419 degrees C, Pb 327 degrees C, Sn 232 degrees C
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D27/00—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting
- B22D27/003—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting by using inert gases
Definitions
- This invention relates to a process for minimizing foam formation on the top surface of molten metal during pouring of the metal into moulds or similar containers, or during free falling of molten metal from a furnace to a launder, or cascading of the metal from launder to launder.
- molten metal such as zinc
- foamed metal is formed on the top surface of the molten metal. This foam is normally skimmed off the surface of the molten metal manually. The task is arduous, requires workers to be in close proximity to molten metal and produces significant amounts of foamed metal which must be reclaimed.
- foam formation may be minimized by maintaining the molten metal, during filling of the mould, or free falling of the molten metal into launders or other containers, under an essentially non-oxidizing atmosphere so as to prevent entrainment of sufficient oxygen into the molten metal by the falling stream to form an excessive amount of bubbles having a tenacious oxidized film and which do not collapse when they float to the surface of the molten metal but rather produce undesirable foam on such surface.
- the non-oxidizing atmosphere is preferably provided by an inert gas, such as nitrogen, and it can contain a small quantity of oxygen, e.g. up to 2% without producing excessive quantities of bubbles.
- the above disclosed method may be carried out by placing a cover on the top of the molten metal container, and by providing an aperture therein for passage of the molten metal and means for introducing a non-oxidizing gas under the cover.
- the invention could also be carried out on a continuous slab casting machine comprising a train of closely spaced open top ingot moulds mounted on an endless conveyor chain by providing a hood over the casting machine at the filling station and introducing a non-oxidizing gas under the hood. Seals would be required at the hood entrance and exit as well as on the sides to prevent excessive loss of non-oxidizing gas.
- the hood would of course require a sealed opening for introducing the molten metal through one of the walls thereof.
- the process is preferably carried out on a continuous casting machine by an apparatus which does not require the use of any seals.
- Such apparatus comprises a cover plate located at a predetermined distance above a number of containers or ingot moulds and having an aperture therein for casting molten metal in each container as they pass under the aperture.
- the cover plate extends a predetermined distance before and after such aperture and has a predetermined number of ports therein for feeding a non-oxidizing gas through the cover plate to progressively develop a non-oxidizing atmosphere in the containers as they approach the aperture in the cover plate and to maintain such atmosphere in the containers as they pass such aperture.
- the entrance length of the cover plate before the mould filling aperture is necessary to progressively develop the required non-oxidizing atmosphere while the exit length of the cover plate is needed to maintain the required non-oxidizing atmosphere.
- the entrance length is determined by the conveyor line speed, the container volume, the container to cover gap and the influence of these factors on the volume of purging gas required to obtain the desired atmosphere.
- the exit length is determined by the pneumatic resistance required to prevent back flow of air into the container being filled.
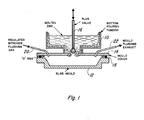
- the laboratory apparatus comprises a bottom-pouring tundish 10 which is used to feed molten zinc into a slab mould 12 through a cover 14 closing the top of the mould.
- the bottom of the tundish 'is provided with an opening registering with a corresponding opening in the cover 14 and is sealed to the cover by any suitable means such as by welding.
- the opening in the bottom of the tundish is closed by a plug valve 16 which may be opened when it is desired to pour molten metal into the mould.
- the cover is sealed to the mould by '0' ring 18.
- a metered nitrogen inlet 20 and exhaust vent 22 are provided through the cover to maintain a suitable non-oxidizing atmosphere on the top surface of the mould.
- a preliminary experimental procedure was carried out involving filling the tundish with molten zinc and then opening the valve to fill the mould. A fair amount of foam was formed on the top of the molten metal. The same procedure was repeated except that the covered mould was purged with nitrogen before opening the valve to fill the mould. The mould was uncovered soon after filling, before solidification to allow freezing of metal in air. No foam appeared on top of the molten metal.
- the invention may also be carried out on a continuous slab casting machine, such as the Sheppard casting machine which has a number of moulds mounted on an endless conveyor chain.
- the non-oxidizing atmosphere may be provided by means of a hood surrounding the casting machine at the filling station. Molten metal would be fed from a furnace to a pouring ladle located inside the hood and from the pouring ladle into the moulds as they move past the filling station.
- a metered nitrogen inlet and exhaust vent would be provided through the hood to provide a non-oxidizing atmosphere in the hood.
- the nitrogen atmosphere within the hood must be maintained at a slight positive pressure such that the ambient oxidizing atmosphere outside the hood cannot enter the hood through the mould entrance and exit ports. However, seals would be required at the hood entrance and exit to prevent excessive loss of nitrogen gas.
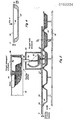
- FIG. 2 there is shown a train of closely spaced open top ingot moulds 30 mounted on an endless conveyor chain 32 moving at a line speed of about 2 in/sec. in the direction indicated by arrow A.
- the ingot moulds all have flat top surfaces.
- a stationary cover plate 34 is mounted adjacent to but spaced by a predetermined distance D from the top surface of the moulds and covers a predetermined number of moulds before and after a metal pouring station which is mounted on the top of the cover plate.
- the metal pouring station is a conventional design comprising a launder 36 which ends with a downspout 38 used to feed molten metal into a ladle 40.
- the ladle 40 is intermittently pivoted to successively pour metal into each mould through a pouring slot 42 in the cover plate.
- a trap 44 is positioned at the end of the launder to capture dross which may be floating on the surface of the molten metal.
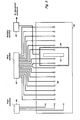
- the cover plate 34 is provided with a predetermined number of gas inlet ports 46 and an inert gas is fed into such ports through a front manifold 48 and a main manifold 50.
- Inert gas is fed to the front mould entering under the plate through three gas inlet ports to rapidly purge the moulds, and to the remaining moulds under the plate through a single row of ports to progressively lower and maintain the oxygen level at the pouring station below a predetermined value.
- An auxiliary manifold 52 is also provided for feeding inert gas to the ladle enclosure 54 and the downspout enclosure 56. Cover strips 58 are placed on the gaps between the moulds so as to prevent excessive leakage of gas through such gaps.
- the width of the plate 34 is equal to that of moulds 30. Inert gas enters the moulds at gas ports 46 and flows out through the gaps at the sides and the ends of the cover plate.
- the width of the cover as well as the width of the container with respect to the container cavity are dependent on the pneumatic resistance required to prevent back flow of air into the moulds.
- the tests were carried out by establishing a predetermined nitrogen flow rate through the cover plate and then traversing the moulds past the cover plate at the same speed as a conventional casting machine conveyor (2 in/sec.). Each mould was progressively purged as it entered under the cover plate. The mould atmosphere was sampled in the centre of the mould by pumping a sample to an oxygen analyser as the mould approached the pouring slot.
- Atmosphere tests were initially carried out with the machine in operation but without pouring liquid metal. These tests indicated that oxygen levels could be maintained at the pouring station in the range of 0.3-0.5% and that no gain could be achieved by increasing the nitrogen flow rate above 2000 SCFH.
- Liquid zinc was then started up with preheating flames on the launder and ladle. Nitrogen was first delivered at 250 SCFH to the front manifold and at 1500 SCFH to the main manifold of the cover plate and successively to the ladle and downspout enclosures at 250 SCFH. The oxygen level maintained at the pouring station was in the range of 0.35-0.45%.
- the slab ingot surfaces were seen to be bright and dross-free.
- Transparent oxide films identical to those obtained in the laboratory tests using oxygen levels in the range of 0.2-0.5% were observed on the slabs.
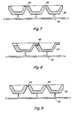
- Figures 7, 8 and 9 show refinements to reduce loss of gas in between the moulds and so reduce the gas flow requirements.
- the edges of the moulds are thicker than that shown in Figure 2 and this increases the resistance to gas flow in the gap 60 between the moulds.
- the edges of the moulds are designed so that the gap 62 is horizontal in order to prevent direct flow of the gas from the cover ports. This design is in a way equivalent to the cover strips 58 of Figure 2 but is much more resistant to wear and tear.
- Figure 9 shows another method of reducing gas flow which involves the use of a seal 64 in between the moulds. This alternative is possible since this seal is non rubbing.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Continuous Casting (AREA)
- Silicon Compounds (AREA)
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AU22592/83A AU560253B2 (en) | 1983-12-23 | 1983-12-20 | Process and apparatus for minimizing foam formation during free falling of molten metal into moulds, launders or other containers |
| EP19830113078 EP0150226B1 (de) | 1983-12-23 | 1983-12-23 | Verfahren und Vorrichtung zur Vermeidung von Schaumformung beim freifallenden Giessstrahl in Giessformen, Giessrinnen oder andere Gefässe |
| DE8383113078T DE3374279D1 (en) | 1983-12-23 | 1983-12-23 | Process and apparatus for minimizing foam formation during free falling of molten metal into moulds, launders or other containers |
| JP25250083A JPS60145262A (ja) | 1983-12-23 | 1983-12-29 | 連続鋳造で発泡を最少にするための装置 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP19830113078 EP0150226B1 (de) | 1983-12-23 | 1983-12-23 | Verfahren und Vorrichtung zur Vermeidung von Schaumformung beim freifallenden Giessstrahl in Giessformen, Giessrinnen oder andere Gefässe |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0150226A1 true EP0150226A1 (de) | 1985-08-07 |
| EP0150226B1 EP0150226B1 (de) | 1987-11-04 |
Family
ID=8190905
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19830113078 Expired EP0150226B1 (de) | 1983-12-23 | 1983-12-23 | Verfahren und Vorrichtung zur Vermeidung von Schaumformung beim freifallenden Giessstrahl in Giessformen, Giessrinnen oder andere Gefässe |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0150226B1 (de) |
| JP (1) | JPS60145262A (de) |
| AU (1) | AU560253B2 (de) |
| DE (1) | DE3374279D1 (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2781395A1 (fr) * | 1998-07-27 | 2000-01-28 | Brochot Sa | Dispositif pour couler des lingots d'un metal liquide non ferreux, notamment du magnesium liquide, selon de grandes cadences de production sans diminution de la qualite |
| WO2001091948A1 (fr) * | 2000-05-31 | 2001-12-06 | Brochot Sa | Procede et dispositif pour proteger un metal fondu non ferreux |
| CN113492208A (zh) * | 2020-04-01 | 2021-10-12 | 青海北辰科技有限公司 | 一种新型镁锭铸造气体保护装置 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR101159949B1 (ko) | 2010-02-26 | 2012-06-25 | 현대제철 주식회사 | 주선기의 몰드 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2099208A (en) * | 1936-03-02 | 1937-11-16 | William H D Horsfall | Apparatus for preventing the oxidation of metals |
| EP0088701A1 (de) * | 1982-03-08 | 1983-09-14 | Noranda Inc. | Verfahren und Vorrichtung zum Giessen eines flüssigen Nichteisenmetalles |
-
1983
- 1983-12-20 AU AU22592/83A patent/AU560253B2/en not_active Ceased
- 1983-12-23 EP EP19830113078 patent/EP0150226B1/de not_active Expired
- 1983-12-23 DE DE8383113078T patent/DE3374279D1/de not_active Expired
- 1983-12-29 JP JP25250083A patent/JPS60145262A/ja active Granted
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2099208A (en) * | 1936-03-02 | 1937-11-16 | William H D Horsfall | Apparatus for preventing the oxidation of metals |
| EP0088701A1 (de) * | 1982-03-08 | 1983-09-14 | Noranda Inc. | Verfahren und Vorrichtung zum Giessen eines flüssigen Nichteisenmetalles |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2781395A1 (fr) * | 1998-07-27 | 2000-01-28 | Brochot Sa | Dispositif pour couler des lingots d'un metal liquide non ferreux, notamment du magnesium liquide, selon de grandes cadences de production sans diminution de la qualite |
| WO2000006321A1 (fr) * | 1998-07-27 | 2000-02-10 | Brochot S.A. | Dispositif pour couler des lingots d'un metal liquide non ferreux |
| WO2001091948A1 (fr) * | 2000-05-31 | 2001-12-06 | Brochot Sa | Procede et dispositif pour proteger un metal fondu non ferreux |
| FR2809643A1 (fr) * | 2000-05-31 | 2001-12-07 | Brochot Sa | Procede et dispositif pour proteger un metal fondu non ferreux |
| CN113492208A (zh) * | 2020-04-01 | 2021-10-12 | 青海北辰科技有限公司 | 一种新型镁锭铸造气体保护装置 |
| CN113492208B (zh) * | 2020-04-01 | 2025-03-04 | 青海北辰科技有限公司 | 一种新型镁锭铸造气体保护装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| AU560253B2 (en) | 1987-04-02 |
| AU2259283A (en) | 1985-06-27 |
| DE3374279D1 (en) | 1987-12-10 |
| EP0150226B1 (de) | 1987-11-04 |
| JPS60145262A (ja) | 1985-07-31 |
| JPH0431781B2 (de) | 1992-05-27 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4565234A (en) | Casting process and installation for a non-ferrous metal in the molten state | |
| JPS571544A (en) | Method and device for horizontal strand casting of molten metal, particularly steel | |
| SK283020B6 (sk) | Spôsob výroby pásu z tvárnej ocele a zariadenie na jeho vykonávanie | |
| US3552478A (en) | Method for starting and maintaining the supply of metal to a downward operating continuous casting mold | |
| EP0150226B1 (de) | Verfahren und Vorrichtung zur Vermeidung von Schaumformung beim freifallenden Giessstrahl in Giessformen, Giessrinnen oder andere Gefässe | |
| MXPA97001757A (es) | Dispositivo de control de flujo para la boquilla externa de un recipiente metalurgico | |
| US4549598A (en) | Process for minimizing foam formation during free falling of molten metal into moulds, launders or other containers | |
| US3845809A (en) | Means for the continuous casting of steel | |
| US3174200A (en) | Method of purging mold and pouring metal therein | |
| US3794218A (en) | Method and apparatus for opening a sealing element, which cannot be actuated, of the bottom nozzle of a casting vessel | |
| US4576220A (en) | Method and apparatus for maintaining an atmosphere around a predetermined portion of an endless discrete object conveyor | |
| US4711429A (en) | Tundish for mixing alloying elements with molten metal | |
| US1690750A (en) | Method of pouring steel | |
| CA1160017A (en) | Process for minimizing foam formation during free falling of molten metal into moulds, launders or other containers | |
| JP3484820B2 (ja) | 快削鋼の連続鋳造方法 | |
| US4658881A (en) | Casting apparatus for providing controlled ambient during production casting | |
| US20080173423A1 (en) | Sequence Casting Process for Producing a High-Purity Cast Metal Strand | |
| US5915459A (en) | Method and equipment for the integral casting of metal strip close to its final dimensions | |
| FI73373B (fi) | Foerfarande och anordning foer minimering av skumbildning vid smaelt metalls fria fall in i formar, traog och motsvarande kaerl. | |
| US3700026A (en) | Ingot casting apparatus | |
| JPS5514132A (en) | Preventing method for oxygen entry of cast ingot in continuous casting and device thereof | |
| US4723763A (en) | Device for continuous injection under low pressure of a powdered additive into a stream of molten metal | |
| RU2031758C1 (ru) | Способ разливки легкоокисляющихся сплавов | |
| NO160691B (no) | Fremgangsm te fo minske skumdannelse p ovemeltet metall. | |
| JPS5797847A (en) | Method for feeding molten metal into mold in continuous casting |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): BE DE FR IT NL |
|
| 17P | Request for examination filed |
Effective date: 19850912 |
|
| 17Q | First examination report despatched |
Effective date: 19860915 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE DE FR IT NL |
|
| REF | Corresponds to: |
Ref document number: 3374279 Country of ref document: DE Date of ref document: 19871210 |
|
| ITF | It: translation for a ep patent filed | ||
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| ITTA | It: last paid annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 19921013 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19921120 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19921231 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19930226 Year of fee payment: 10 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Effective date: 19931231 |
|
| BERE | Be: lapsed |
Owner name: NORANDA INC. Effective date: 19931231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19940701 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19940831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19940901 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |