EP0217548A1 - Versteifungsbügel für Büstenhalter und Verfahren zu seiner Herstellung - Google Patents
Versteifungsbügel für Büstenhalter und Verfahren zu seiner Herstellung Download PDFInfo
- Publication number
- EP0217548A1 EP0217548A1 EP86306748A EP86306748A EP0217548A1 EP 0217548 A1 EP0217548 A1 EP 0217548A1 EP 86306748 A EP86306748 A EP 86306748A EP 86306748 A EP86306748 A EP 86306748A EP 0217548 A1 EP0217548 A1 EP 0217548A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- wire
- brassiere
- legs
- annealed
- stiffening member
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- A—HUMAN NECESSITIES
- A41—WEARING APPAREL
- A41C—CORSETS; BRASSIERES
- A41C3/00—Brassieres
- A41C3/12—Component parts
- A41C3/122—Stay means
- A41C3/126—Stay means with additional means provided at the ends, e.g. for protection
Definitions
- the present invention relates generally to brassieres and more particularly, relates to improvements in wire members for use in brassieres.
- the use of metallic wires or frames as stiffening members or frames in the manufacture of brassieres is well known in the art.
- the wires have a generally U-shaped configuration extending along the side peripheral portions of the brassiere cups and are generally of a rectangular cross sectional configuration with the longer dimension extending radially with respect to the curvature of the wire.
- the wires are secured to the brassiere by enclosing the wires within the fabric along the perimeter of the brassiere cups.
- the wires may be retained by means of stitching about the ends of the wires.
- the brassiere wires or frames may be formed of a spring steel and in particular, a high carbon spring steel which is well known for its suitability.
- end caps or tips wherein the plastic material forming the cap extends beyond the end of the wire for a substantial distance.
- the end cap is of a flexible material and thus renders the end of the wire more resilient than would otherwise be the case. While such a construction provides substantial advantages over the bare metallic stiffening member, it has been found that these members which are slipped on the wire may become disengaged therefrom after repeated washing of the garment. Furthermore, these end caps are frequently secured to the wire after the same has been inserted in the garment and the manual operation of so doing is an expensive one.
- stiffening member suitable for use in a brassiere wherein the stiffening member has one or more portions which are softer and more flexible than the remaining portions.
- a stiffening member for a brassiere wherein the member is formed of a metallic spring wire material having a generally U-shaped configuration
- the improvement wherein a portion of the stiffening member is subjected to an annealing operation to thereby soften said portion.
- a method for treating a stiffening member suitable for use in a brassiere comprising the step of annealing a portion of the member which is formed of a metallic spring wire material.
- the preferred improved stiffening member of the present invention comprises a conventional U-shaped wire having a generally rectangular cross-sectional configuration with the longer dimension extending radially with respect to the curvature of the wire.
- the wire is formed of a spring wire material. At least a portion of the spring wire is subjected to an annealing step to soften the portion treated and thereby render the same more flexible or bendable and to provide greater comfort to the wearer.
- the stiffening member may be subjected to the aforesaid annealing operation at one or more places.
- the stiffening member is annealed at two different places, each place being adjacent the end of one of the legs of the member.
- the location of the annealed portion of the wire may vary depending upon the size of the wire and the particular garment in which it is to be utilized.
- the wire would be annealed at a position ranging from the end of each leg to a distance of 4 inches from the end of the leg.
- the stiffening member or frame would be annealed at a position ranging between 1/4" to 1 inch from the end of the leg and a distance of 1/2" has been found to be very suitable.
- the length of the annealed portion can also vary according to the requirements of the designer. Thus, a very small portion, typically 1/8" to 3/4" in length, may be subjected to the annealing or alternatively, again depending on the ultimate end use of the member, a larger length may be annealed.
- the annealed portion is desirably provided with a protective coating or subjected to a further treatment to prevent oxidation of the metallic member.
- the means of annealing the member may be chosen from among many well known to those knowledgeable in the art. Thus, one may use various types of flames to anneal or alternatively, an induction type of annealing could be utilized.
- One attractive alternative is to utilize high intensity infrared line heaters. These heaters generate highly concentrated radiant heat flux density along a thin • line at the external focal axis of an elliptical reflector. Such heaters produce rapid heating rates and high temperatures which can be focused very precisely at the desired location.
- the specifics time and temperature will again be a choice which can be made by those knowledgeable in the art; typically, the spring wire to be used in a brassiere wire would be heated to a temperature of above 1600°F and air cooled.
- the specific temperature and time of treatment can be varied as is well known by those skilled in the art.in order to achieve the desired result.
- This annealing treatment will substantially reduce the hardness of the material; again, it is well within the knowledge of those skilled in the art to vary the hardness to achieve the results desired for a particular required design of brassiere wire.
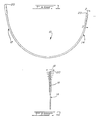
- FIG. 1 a typical stiffening member 10 which is suitable for use in a brassiere.
- Member 10 has a generally U-shaped configuration with two leg portions which are designated by reference numerals 12 and 14. Adjacent the free end of legs 12 and 14, the material is subjected to an annealing operation as designated by reference numeral 16. This annealing operation at the point 16 renders this point "softer" and permits movement of the free ends as shown by arrow 18. Subsequent to the annealing operation, a protective coating 20 is provided; protective coating 20 may be of a suitable material, typically a latex material.
- the method for forming the stiffening member is well understood by those knowledgeable in the art.
- a roll of a suitable continuous spring wire material is supplied.
- This material has normally been subjected to annealing and tempering treatments as is conventional in the art.
- the wire material is cut to a suitable length and formed into the U-shaped members such as shown in Figure 1.
- the legs are subjected to the annealing treatment to soften the desired portion.
- the protective coating is applied to the ends of the stiffening members or wires.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Corsets Or Brassieres (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT86306748T ATE55676T1 (de) | 1985-09-04 | 1986-09-02 | Versteifungsbuegel fuer buestenhalter und verfahren zu seiner herstellung. |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CA000489992A CA1261551A (en) | 1985-09-04 | 1985-09-04 | Brassiere wires and method for forming same |
| CA489992 | 1985-09-04 | ||
| US887903 | 1986-07-18 | ||
| US06/887,903 US4770650A (en) | 1985-09-04 | 1986-07-18 | Brassiere wires and method of forming same |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0217548A1 true EP0217548A1 (de) | 1987-04-08 |
| EP0217548B1 EP0217548B1 (de) | 1990-08-22 |
Family
ID=25670778
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19860306748 Expired EP0217548B1 (de) | 1985-09-04 | 1986-09-02 | Versteifungsbügel für Büstenhalter und Verfahren zu seiner Herstellung |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0217548B1 (de) |
| DE (1) | DE3673595D1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2023280151A1 (zh) * | 2021-07-05 | 2023-01-12 | 肇庆市鼎湖兴文塑胶五金制品有限公司 | 一种具有软端部的内衣钢圈 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2746052A (en) * | 1955-04-04 | 1956-05-22 | S & S Ind Inc | Brassiere frame |
| US4285113A (en) * | 1978-04-19 | 1981-08-25 | Rowell Ross F | Method of forming brassiere wires |
-
1986
- 1986-09-02 EP EP19860306748 patent/EP0217548B1/de not_active Expired
- 1986-09-02 DE DE8686306748T patent/DE3673595D1/de not_active Expired - Lifetime
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2746052A (en) * | 1955-04-04 | 1956-05-22 | S & S Ind Inc | Brassiere frame |
| US4285113A (en) * | 1978-04-19 | 1981-08-25 | Rowell Ross F | Method of forming brassiere wires |
Non-Patent Citations (1)
| Title |
|---|
| L.E.ALBAN et al.: "METALS HANDBOOK NINTH EDITION", vol. 4, Heat Treating, pages 18-21, American Society for Metals, Metals Park, Ohio, US; * |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2023280151A1 (zh) * | 2021-07-05 | 2023-01-12 | 肇庆市鼎湖兴文塑胶五金制品有限公司 | 一种具有软端部的内衣钢圈 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE3673595D1 (de) | 1990-09-27 |
| EP0217548B1 (de) | 1990-08-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4770650A (en) | Brassiere wires and method of forming same | |
| JPH0335945B2 (de) | ||
| WO1999037235A3 (en) | Superelastic endodontic instrument, method of manufacture, and apparatus therefor | |
| RU94014241A (ru) | Способ и печь для гибки и отпуска стеклянных листов, опирающихся на кольцевую форму | |
| EP0217548B1 (de) | Versteifungsbügel für Büstenhalter und Verfahren zu seiner Herstellung | |
| KR100941257B1 (ko) | 유도 전류를 이용한 히티드 스티어링 휠 | |
| AR025347A1 (es) | Aparato y procedimiento para fabricar alambre fino | |
| US4201220A (en) | Brassiere wires | |
| US5078485A (en) | Temples for eyeglasses | |
| US4285113A (en) | Method of forming brassiere wires | |
| US2666202A (en) | Foundation garment | |
| US3923561A (en) | Method of heat treating saw | |
| US2500566A (en) | Method for the manufacture of piston ring elements | |
| JPS57198211A (en) | Manufacture of heat treat pc steel rod | |
| KR100391780B1 (ko) | 장갑 셋팅장치 | |
| US2012335A (en) | Machine for applying intense heat | |
| JPS63127225A (ja) | 眼鏡部品 | |
| JP2013204092A (ja) | 加熱装置及び加熱方法 | |
| RU97103386A (ru) | Способ производства буровых штанг | |
| JPH0360909B2 (de) | ||
| CN208532876U (zh) | 一种新型退火镍环 | |
| JPS6480391A (en) | Method of manufacturing hair for doll | |
| JPH04303556A (ja) | フィラメントの成形方法 | |
| JPS6341822A (ja) | 眼鏡フレ−ム | |
| KR20150124130A (ko) | 형상기억합금을 이용한 안경 코받침대 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19871002 |
|
| 17Q | First examination report despatched |
Effective date: 19890113 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19900822 Ref country code: CH Effective date: 19900822 Ref country code: AT Effective date: 19900822 |
|
| REF | Corresponds to: |
Ref document number: 55676 Country of ref document: AT Date of ref document: 19900915 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3673595 Country of ref document: DE Date of ref document: 19900927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19900930 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 19901002 Year of fee payment: 5 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| ITTA | It: last paid annual fee | ||
| NLS | Nl: assignments of ep-patents |
Owner name: SARA LEE INTERNATIONAL CORPORATION TE WINSTON-SALE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP |
|
| ITPR | It: changes in ownership of a european patent |
Owner name: CESSIONE;SARA LEE INTERNATIONAL CORPORATION |
|
| EAL | Se: european patent in force in sweden |
Ref document number: 86306748.4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19970829 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19970905 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19970909 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19970918 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19970929 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 19971104 Year of fee payment: 12 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980902 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980903 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980930 |
|
| BERE | Be: lapsed |
Owner name: SARA LEE INTERNATIONAL CORP. (UNE SOCIETE DE L'ET Effective date: 19980930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990401 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19980902 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 86306748.4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990531 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 19990401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990701 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050902 |