EP0247209A1 - Vorrichtung und Verfahren zum elektrochemischen Polieren der Innenflächen von Rohren - Google Patents
Vorrichtung und Verfahren zum elektrochemischen Polieren der Innenflächen von Rohren Download PDFInfo
- Publication number
- EP0247209A1 EP0247209A1 EP86106812A EP86106812A EP0247209A1 EP 0247209 A1 EP0247209 A1 EP 0247209A1 EP 86106812 A EP86106812 A EP 86106812A EP 86106812 A EP86106812 A EP 86106812A EP 0247209 A1 EP0247209 A1 EP 0247209A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- electrolyte
- polishing head
- tube
- dielectric
- cathode
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25F—PROCESSES FOR THE ELECTROLYTIC REMOVAL OF MATERIALS FROM OBJECTS; APPARATUS THEREFOR
- C25F7/00—Constructional parts, or assemblies thereof, of cells for electrolytic removal of material from objects; Servicing or operating
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25F—PROCESSES FOR THE ELECTROLYTIC REMOVAL OF MATERIALS FROM OBJECTS; APPARATUS THEREFOR
- C25F3/00—Electrolytic etching or polishing
- C25F3/16—Polishing
Definitions
- the invention relates to a device for electrochemical polishing and / or pickling the inner surfaces of pipes with a flowing electrolyte which at least partially passes through a cathode arranged inside the anodically connected pipe, and to a corresponding method for electrochemical polishing and / or pickling pipe inner surfaces .
- a method and a device for electrochemically polishing the inner walls of pipes are also known from European patent application 82 104 946.7, in which an electrode acting as a cathode can be moved through the pipe. The electrolyte is filled into the entire pipe section to be electropolished.
- a device for electropolishing the inner walls of pipes in which a pipe lance is introduced into the pipe, which has a cathodic area between its tip and a retaining ring, the pipe lance with bores for the passage of the electrolyte liquid is provided.
- the known methods and devices for electrochemical polishing and / or pickling of inner tube surfaces have the disadvantage that a very high consumption of electrolyte is required for complete filling, flushing and cooling of the tube.
- the gases (hydrogen and oxygen) generated during electrolytic polishing also have to be removed, which likewise results in a very high electrolyte throughput through the tube.
- the invention has for its object to provide a device and a method for electrochemical polishing and / or pickling the inner surfaces of pipes, which enables both a reduction in the amount of electrolyte used and an improvement in the polishing and pickling quality. It is also intended by the invention that a considerably greater variety of electrolyte compositions can be used compared to conventional processes.
- the device according to the invention for solving this problem is characterized by a polishing head which is movable through the tube and has feed lines for the electrolyte and for electric current, a cathode arranged in the interior of the polishing head and a dielectric which at least partially forms the outer wall of the polishing head, the passes the electrolyte stream and leaves a working gap for the electrolyte stream between itself and the pipe inner surface to be polished or to be etched.
- the method according to the invention for solving the problem is characterized in that the electrolyte stream is pumped into a polishing head provided with a cathode and out of it by a dielectric into a working gap formed between the dielectric and the inner surface of the tube.
- a polishing head is thus moved through the tube. It is essential that a so-called working gap is formed between a wall of the polishing head formed from a dielectric and the inner surface of the tube, into which the electrolyte is pressed by the dielectric.
- the inventive design of a working gap between the dielectric and the inner surface of the tube significantly reduces the consumption of electrolyte compared to the prior art.
- Electrolytes that can be regenerated via ion exchangers or electrolytic separation cells can be used. It is possible to keep the metal content of the electrolyte so low that the cathode surfaces cannot be passivated by deposited metal sludge.
- the stream of electrolyte flowing into the polishing head into one anodic partial flow and a cathodic partial flow is divided, the anodic partial flow passing through the dielectric and the tube inner surface, but not the cathode, while the cathodic partial flow passes the cathode but not the tube inner surface.
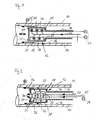
- the polishing head (12) is slowly moved through the tube 10.
- the polishing head 12 is sometimes also referred to as a "tampon".
- the polishing head 12 is moved through the tube 10 by means of a guide 14, which is designed as a tube with a much smaller diameter than the tube 10 to be cleaned.
- the polishing head 12 is approximately cylindrical and lies concentrically in the pipe 10 to be cleaned.
- the jacket of the cylindrical polishing head 12 is formed by a dielectric 18 which is uniformly spaced from the inner surface 16 of the tube 10.
- the polishing head 12 can be moved in the direction of the arrow 20, that is to say in both directions, through the tube 10.
- the electrolyte flow 22 in FIGS. 1 and 2 enters the polishing head 12 from the right through the guide 14 and in the exemplary embodiment according to FIG. 1 is pressed radially outwards by the dielectric 18 according to the arrows.
- the guide 14 receives the electrical supply lines 25 for the cathodes 26.
- a uniform, narrow working gap 28 is formed between the cylindrical jacket-shaped dielectric outer walls of the polishing head 12 and the inner surface 16 of the tube 10.
- the electrolyte stream 22 ⁇ passes through the working gap 28 and causes the electrochemical removal and polishing in a known manner on the inner surface 16.
- the electrolyte stream 22 entering the polishing head 12 is divided into a cathodic and an anodic partial stream 30 or 32.
- the cathodic partial stream 30 only passes through the cathodes 26, but not through the dielectric 18 and the working gap 28.
- the hydrogen gas formed on the cathodes 26 does not reach the dielectric 18 or the inner surface 16 to be polished, which on the one hand prevents the dielectric 18 from being loaded with hydrogen gas and on the other hand also avoids harmful effects of the hydrogen on the inner surface 16.
- the anodic partial stream 32 passes through the dielectric wall 18 and the working gap 28, so that the electrochemical polishing of the inner surface 16 can take place.
- the cathodic partial stream 30 exits through an opening 34 in the front wall of the polishing head 12 and, like the anodic partial stream 32, is collected and, if necessary, returned after regeneration.
- Textile Teflon fabrics are preferably used as the dielectric 18. Glass fiber fabrics and acid-resistant plastic fabrics and nonwovens can also be used.
- the dimensions of the polishing head 12 and, in particular, of the dielectric 18 are adapted or selected for a given tube inner diameter in such a way that a working gap with optimal thickness is created.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Electrical Discharge Machining, Electrochemical Machining, And Combined Machining (AREA)
- Cleaning And De-Greasing Of Metallic Materials By Chemical Methods (AREA)
Abstract
Description
- Die Erfindung betrifft eine Vorrichtung zum elektrochemischen Polieren und/oder Beizen der Innenflächen von Rohren mit einem strömenden Elektrolyt, der zumindest teilweise eine im Inneren des anodisch geschalteten Rohres angeordnete Kathode passiert, sowie ein entsprechendes Verfahren zum elektrochemischen Polieren und/oder Beizen von Rohr-Innenflächen.
- Aus der europäischen Patentanmeldung 82 104 945.9 sind ein Verfahren und eine Vorrichtung zum sogenannten Elektropolieren der Innenwände von metallischen Rohren bekannt, bei denen der Elektrolyt mittels Hochdruck von ca. 50 Bar auf ein Teilstück der Wandung des Rohres aufgebracht wird. Die Kathode wird mit Hilfe des Hochdruckstrahls im Rohr bewegt, so daß nacheinander unterschiedliche Abschnitte der Rohr-Innenwand poliert werden können.
- Aus der europäischen Patentanmeldung 82 104 946.7 sind ebenfalls ein Verfahren und eine Vorrichtung zum elektrochemischen Polieren der Innenwände von Rohren bekannt, bei denen eine als Kathode wirkende Elektrode durch das Rohr bewegbar ist. Der Elektrolyt wird in den gesamten zu elektropolierenden Rohrabschnitt eingefüllt.
- Aus dem DE-GM 80 11 918 ist eine Vorrichtung zum Elektropolieren der Innenwände von Rohren bekannt, bei der eine Rohrlanze in das Rohr eingebracht wird, die zwischen ihrer Spitze und einem Stauring einen kathodischen Bereich aufweist, wobei die Rohrlanze mit Bohrungen zum Durchtritt der Elektrolytflüssigkeit versehen ist.
- Der vorstehend beispielhaft angedeutete Stand der Technik für das elektrochemische Polieren von Rohr-Innenwänden läßt sich grob in zwei Klassen aufteilen:
- 1) In das innenseitig zu polierende Rohr wird eine durchgehende Kathode eingesetzt und der Elektrolyt wird durch das anodisch geschaltete Rohr gepumpt. Während des Elektropolierens liegt das Rohr entweder waagerecht oder leicht schräg und wird um seine Längsachse gedreht. Es ist dabei auch möglich, das Rohr vertikal zu stellen.
- 2) Es wird eine nur partiell auf jeweils einen bestimmten Abschnitt der Rohr-Innenwand einwirkende Kathode (die also wesentlich kürzer ist als das zu elektropolierende Rohr) durch das Rohr bewegt. Dabei wird der Elektrolyt durch das Rohr gepumpt.
- Die bekannten Verfahren und Vorrichtungen zum elektrochemischen Polieren und/oder Beizen von Rohr-Innenflächen haben den Nachteil, daß zur vollständigen Füllung, Durchspülung und Kühlung des Rohres ein sehr hoher Elektrolytverbrauch erforderlich ist. Auch müssen die bei der elektrolytischen Polierung entstehenden Gase (Wasserstoff und Sauerstoff) abgeführt werden, was ebenfalls einen sehr hohen Elektrolyt-Durchsatz durch das Rohr bedingt.
- Auch können bei den bekannten Vorrichtungen und Verfahren nur Elektrolyte eingesetzt werden, deren Metallgehalt erheblichen Einschränkungen unterworfen ist. Ein erhöhter Metallgehalt in den Elektrolyten führt bei den bekannten Vorrichtungen nämlich zur Passivierung der Kathodenoberflächen durch Belegung mit kathodisch abgeschiedenem Metallschlamm, was eine erhebliche Reduzierung der Polierqualität zur Folge hat. Um den Metallgehalt der Elektrolyte gering zu halten, ist es deshalb erforderlich, den Elektrolyte in erheblichen Mengen umzuwälzen.
- Auch ist zu berücksichtigen, daß die Beseitigung des mit Metallen angereicherten Elektrolyts zur Vermeidung von Umweltbelastungen sehr große Kosten verursacht. Beim Stand der Technik werden zum Elektropolieren der Innenflächen von Rohren aus austenitischen Chromnickelstählen Gemische aus Phosphorsäure, Schwefelsäure und Wasser verwendet. Diese Säuren stellen schon als solche eine erhebliche Umweltbelastung und ein Gefährdungspotential dar, das besondere Sicherheitsmaßnahmen erforderlich macht.
- Der Erfindung liegt die Aufgabe zugrunde, eine Vorrichtung und ein Verfahren zum elektrochemischen Polieren und/oder Beizen der Innenflächen von Rohren zu schaffen, die bzw. das sowohl eine Reduzierung der verwendeten Elektrolytmenge als auch eine Verbesserung der Polier- und Beizqualität ermöglicht. Auch soll durch die Erfindung erreicht werden, daß gegenüber herkömmlichen Verfahren eine wesentlich größere Vielfalt von Elektrolyt-Zusammensetzungen verwendet werden kann.
- Die erfindungsgemäße Vorrichtung zur Lösung dieser Aufgabe zeichnet sich aus durch einen Polierkopf, der durch das Rohr bewegbar ist und Zuleitungen für den Elektrolyt und für elektrischen Strom aufweist, eine im Inneren des Polierkopfes angeordnete Kathode und ein zumindest teilweise die Außenwand des Polierkopfes bildendes Dielektrikum, das den Elektrolytstrom durchläßt und zwischen sich und der zu polierenden bzw. zu beizenden Rohr-Innenfläche einen Arbeitsspalt für den Elektrolytstrom freiläßt.
- Das erfindungsgemäße Verfahren zur Lösung der gestellten Aufgabe zeichnet sich dadurch aus, daß der Elektrolytstrom in einen mit einer Kathode versehenen Polierkopf und aus diesem durch ein Dielektrikum in einen zwischen dem Dielektrikum und der Rohr-Innenfläche gebildeten Arbeitsspalt gepumpt wird.
- Gemäß der Erfindung wird also ein Polierkopf durch das Rohr bewegt. Wesentlich ist, daß zwischen einer aus einem Dielektrikum gebildeten Wand des Polierkopfes und der Innenfläche des Rohres ein sogenannter Arbeitsspalt gebildet wird, in welchen der Elektrolyt durch das Dielektrikum eingepreßt wird.
- Durch die erfindungsgemäß vorgesehene Ausbildung eines Arbeitsspalts zwischen dem Dielektrikum und der Innenfläche des Rohres wird der Elektrolytverbrauch im Vergleich zum Stand der Technik erheblich gesenkt.
- Es hat sich auch gezeigt, daß durch die Kombination von elektrochemischem Polieren mit dem Wischeffekt des Dielektrikums die Wirksamkeit des Elektropoliervorgangs in einer nach herkömmlichen Verfahren nicht zu erzielende Weise die Polierqualität erheblich verbessert werden kann. Auch können mit Erfolg sehr unterschiedliche Elektrolyte verwendet werden, die im Vergleich zum Stand der Technik insbesondere eine wesentlich geringere Umweltbelastung darstellen. Es können Elektrolyte eingesetzt werden, die über Ionenaustauscher oder elektrolytische Abscheidezellen regenerierbar sind. Dabei ist es möglich, den Metallgehalt des Elektrolyten so niedrig zu halten, daß die Kathodenoberflächen nicht durch abgeschiedene Metallschlämme passiviert werden können.
- In einer bevorzugten Variante der Erfindung ist vorgesehen, daß der in den Polierkopf einströmende Elektrolytstrom in einen anodischen Teilstrom und einen kathodischen Teilstrom aufgeteilt ist, wobei der anodische Teilstrom das Dielektrikum und die Rohr-Innenfläche, aber nicht die Kathode passiert, während der kathodische Teilstrom die Kathode, aber nicht die Rohr-Innenfläche passiert.
- Eine derartige Auftrennung des Elektrolytstromes in anodische und kathodische Teilströme ist aus der nicht vorveröffentlichten europäischen Patentanmeldung 86 105 747 der Anmelderin beim partiellen elektrochemischen Polieren von freien Oberflächen bekannt. Alle dort erwähnten Vorteile gelten auch für das Innenpolieren von Rohren.
- Weitere Vorteile der Erfindung ergeben sich aus den Unteransprüchen.
- Nachfolgend werden Ausführungsbeispiele der Erfindung anhand der Zeichnung näher erläutert. Es zeigt:
- Fig. 1 einen Schnitt durch den Teil eines Rohres, dessen Innenfläche poliert werden soll, sowie einen im Rohr bewegbaren Polierkopf und
- Fig. 2 einen Schnitt gemäß Fig. 1 mit einem Polierkopf, in dem der Elektrolytstrom in einen anodischen und einen kathodischen Teilstrom getrennt wird.
- Ein Rohr 10 aus Stahl, beispielsweise Chromnickelstahl, soll innenseitig gereinigt und poliert werden. Hierzu wird der Polierkopf (12) langsam durch das Rohr 10 bewegt. Der Polierkopf 12 wird mitunter auch als "Tampon" bezeichnet. Mittels einer Führung 14, die als Rohr mit wesentlich geringerem Durchmesser als das zu reinigende Rohr 10 ausgebildet ist, wird der Polierkopf 12 durch das Rohr 10 bewegt.
- Wie den Fig. 1 und 2 zu entnehmen ist, ist der Polierkopf 12 etwa zylinderförmig ausgebildet und liegt konzentrisch in dem zu reinigenden Rohr 10.
- Der Mantel des zylinderförmigen Polierkopfes 12 wird durch ein Dielektrikum 18 gebildet, das durchgehend einen gleichmäßigen Abstand zur Innenfläche 16 des Rohres 10 aufweist.
- Der Polierkopf 12 ist in Richtung des Pfeiles 20, also in beiden Richtungen durch das Rohr 10 bewegbar.
- Der Elektrolytstrom 22 tritt in den Fig. 1 und 2 durch die Führung 14 von rechts in den Polierkopf 12 ein und wird beim Ausführungsbeispiel gemäß Fig. 1 durch das Dielektrikum 18 gemäß den Pfeilen radial nach außen gepreßt.
- Die Führung 14 nimmt bei beiden Ausführungsbeispielen gemäß den Fig. 1 und 2 jeweils die elektrischen Versorgungsleitungen 25 für die Kathoden 26 auf.
- Zwischen den zylindermantelförmigen dielektrischen Außenwänden des Polierkopfes 12 und der Innenfläche 16 des Rohres 10 wird ein gleichförmiger enger Arbeitsspalt 28 gebildet. Der Elektrolytstrom 22ʹ passiert den Arbeitsspalt 28 und bewirkt in bekannter Weise an der Innenfläche 16 die elektrochemische Abtragung und Politur.
- Beim in Fig. 2 gezeigten Ausführungsbeispiel wird der in den Polierkopf 12 eintretende Elektrolytstrom 22 in einen kathodischen und einen anodischen Teilstrom 30 bzw. 32 aufgeteilt. Der kathodische Teilstrom 30 passiert nur die Kathoden 26, nicht aber das Dielektrikum 18 und den Arbeitsspalt 28. Somit gelangt das an den Kathoden 26 gebildete Wasserstoffgas nicht zum Dielektrikum 18 und auch nicht zur zu polierenden Innenfläche 16, wodurch zum einen verhindert ist, daß das Dielektrikum 18 mit Wasserstoffgas belastet wird und zum anderen auch schädliche Wirkungen des Wasserstoffs an der Innenfläche 16 vermieden sind.
- Der anodische Teilstrom 32 passiert gemäß Fig. 2 die dielektrische Wand 18 und den Arbeitsspalt 28, so daß die elektrochemische Politur der Innenfläche 16 erfolgen kann.
- Der kathodische Teilstrom 30 tritt durch eine Öffnugn 34 in der Vorderwand des Polierkopfes 12 aus und wird ebenso wie der anodische Teilstrom 32 aufgefangen und nach einer Regenerierung gegebenenfalls zurückgeführt.
- Als Dielektrikum 18 werden bevorzugt textile Teflongewebe verwendet. Auch können Glasfasergewebe und säurebeständige Kunststoffgewebe und -vliese eingesetzt werden.
- Die Abmessungen des Polierkopfes 12 und insbesondere des Dielektrikums 18 werden bei einem gegebenen Rohr-Innendurchmesser so angepaßt oder gewählt, daß ein Arbeitsspalt mit optimaler Stärke entsteht.
Claims (9)
gekennzeichnet durch
- einen Polierkopf (12), der durch das Rohr (10) bewegbar ist und Zuleitungen (14; 25) für den Elektrolyt und für elektrischen Strom aufweist,
- eine im Inneren des Polierkopfes (12) angeordnete Kathode (26) und
- ein zumindest teilweise die Außenwand des Polierkopfes (12) bildendes Dielektrikum (18), das Elektrolyt durchläßt und zwischen sich und der zu polierenden bzw. zu beizenden Rohr-Innenfläche (16) einen Arbeitsspalt (28) für den Elektrolytstrom (22ʹ, 32) freiläßt.
dadurch gekennzeichnet,
daß der Polierkopf (12) zumindest annähernd zylinderförmig ist, wobei das Dielektrikum (18) zumindest teilweise den Mantel des Zylinders bildet.
dadurch gekennzeichnet,
daß der in den Polierkopf (12) einströmende Elektrolytstrom (22) in einen anodischen Teilstrom (32) und einen kathodischen Teilstrom (30) aufgeteilt wird, wobei der anodische Teilstrom das Dielektrikum (18) und die Rohr-Innenfläche (16), aber nicht die Kathode (26) passiert, während der kathodische Teilstrom (30) die Kathode (26), aber nicht die Rohr-Innenfläche (16) passiert.
dadurch gekennzeichnet,
daß eine Führung (14) für den Polierkopf (12) als Rohr ausgeformt ist, in dem die elektrischen Leitungen (25) für den Polierkopf verlaufen und durch das der Elektrolyt zum Polierkopf gepumpt wird.
dadurch gekennzeichnet,
daß der Polierkopf (12) mittels einer elastischen Schlauchleitung mit Elektrolyt sowie Strom versorgt und mittels einer Stange oder eines Seiles durch das Rohr (10) gezogen wird.
dadurch gekennzeichnet,
daß der Druck, mit dem der Elektrolyt durch das Dielektrikum (18) gedrückt wird, steuerbar ist.
dadurch gekennzeichnet,
daß der Elektrolytstrom (22) in einen mit einer Kathode (26) versehenen Polierkopf (12) und aus diesem durch ein Dielektrikum (18) in einen zwischen dem Dielektrikum und der Rohr-Innenfläche (16) gebildeten Arbeitsspalt (28) gepumpt wird.
dadurch gekennzeichnet,
daß der Elektrolytstrom (22) im Polierkopf (12) in einen anodischen Teilstrom (32) und in einen kathodischen Teilstrom (30) aufgeteilt wird, wobei der anodische Teilstrom das Dielektrikum (18) und die Rohr-Innenfläche (16), aber nicht die Kathode (26) passiert, während der kathodische Teilstrom (30) die Kathode (26), aber nicht das Dielektrikum und die Rohr-Innenfläche (16) passiert.
dadurch gekennzeichnet,
daß der Polierkopf (12) durch das Rohr (10) bewegt wird.
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT86106812T ATE54681T1 (de) | 1986-05-20 | 1986-05-20 | Vorrichtung und verfahren zum elektrochemischen polieren der innenflaechen von rohren. |
| EP86106812A EP0247209B1 (de) | 1986-05-20 | 1986-05-20 | Vorrichtung und Verfahren zum elektrochemischen Polieren der Innenflächen von Rohren |
| DE8686106812T DE3672831D1 (de) | 1986-05-20 | 1986-05-20 | Vorrichtung und verfahren zum elektrochemischen polieren der innenflaechen von rohren. |
| US07/047,653 US4772367A (en) | 1986-05-20 | 1987-05-08 | Apparatus for and a method of electrochemically polishing pipe inside surfaces |
| JP62120323A JPH0765240B2 (ja) | 1986-05-20 | 1987-05-19 | 管の内面を電気化学的に研摩および/または酸洗する方法および装置 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP86106812A EP0247209B1 (de) | 1986-05-20 | 1986-05-20 | Vorrichtung und Verfahren zum elektrochemischen Polieren der Innenflächen von Rohren |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0247209A1 true EP0247209A1 (de) | 1987-12-02 |
| EP0247209B1 EP0247209B1 (de) | 1990-07-18 |
Family
ID=8195133
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP86106812A Expired - Lifetime EP0247209B1 (de) | 1986-05-20 | 1986-05-20 | Vorrichtung und Verfahren zum elektrochemischen Polieren der Innenflächen von Rohren |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US4772367A (de) |
| EP (1) | EP0247209B1 (de) |
| JP (1) | JPH0765240B2 (de) |
| AT (1) | ATE54681T1 (de) |
| DE (1) | DE3672831D1 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0607894A1 (de) * | 1993-01-19 | 1994-07-27 | Corning Incorporated | Verfahren zum elektrolytischen Polieren mit einer STEM-Elektrode |
| WO2017220633A1 (de) * | 2016-06-21 | 2017-12-28 | Extrude Hone Gmbh | Verfahren und vorrichtung zum elektrolytischen polieren und verfahren zum herstellen einer kathode |
Families Citing this family (32)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0730692Y2 (ja) * | 1988-11-14 | 1995-07-12 | 石川島播磨重工業株式会社 | 小口径管内面の電解腐食装置 |
| JPH0794090B2 (ja) * | 1989-11-01 | 1995-10-11 | 工業技術院長 | 小径管内面の電解砥粒超鏡面仕上げ方法 |
| JPH06959B2 (ja) * | 1989-11-22 | 1994-01-05 | 工業技術院長 | 高速電解粗仕上げ法 |
| US5413463A (en) * | 1991-12-30 | 1995-05-09 | General Electric Company | Turbulated cooling passages in gas turbine buckets |
| US5507923A (en) * | 1993-11-09 | 1996-04-16 | Stouse; Henry J. | Method and apparatus for electrolytic polishing of tubular products |
| US5819400A (en) * | 1996-06-25 | 1998-10-13 | Smith & Wesson Corp. | Method of manufacturing an electrode assembly for electrochemically etching rifling in gun barrels |
| US6168691B1 (en) * | 1996-08-09 | 2001-01-02 | Atotech Deutschland Gmbh | Device for electrochemical treatment of elongate articles |
| US5958195A (en) * | 1997-05-22 | 1999-09-28 | Therma Corporation, Inc. | Tube inner surface electropolishing device |
| US6217726B1 (en) * | 1997-05-22 | 2001-04-17 | Therma Corporation, Inc. | Tube inner surface electropolishing device with electrolyte dam |
| JPH11138350A (ja) * | 1997-11-10 | 1999-05-25 | Kobe Steel Ltd | アルミ中空押出形材の円筒部内面の研磨方法及び装置並びにアルミ中空押出形材 |
| IT1311147B1 (it) * | 1999-11-04 | 2002-03-04 | Edk Res Ag | Macchina per pulizia localizzata con cella, elettrolitica e/o adultrasuoni, di decapaggio e/o lucidatura |
| US6402908B1 (en) | 2000-02-02 | 2002-06-11 | Therma Corporation, Inc. | Pipe electropolishing apparatus using an electrolyte heater and cooler |
| US6277264B1 (en) | 2000-02-02 | 2001-08-21 | Therma Corporation, Inc. | System and method for using multiple lead connections in an electropolishing process |
| US6547950B1 (en) | 2000-02-02 | 2003-04-15 | Therma Corporation, Inc. | Cathode rinsing station and method |
| US6523615B2 (en) | 2000-03-31 | 2003-02-25 | John Gandy Corporation | Electropolishing method for oil field tubular goods and drill pipe |
| RU2193607C2 (ru) * | 2000-08-02 | 2002-11-27 | Курский государственный технический университет | Устройство для электрохимической обработки внутренней поверхности труб с криволинейной осью |
| JP2002173799A (ja) * | 2000-12-04 | 2002-06-21 | Zenken:Kk | 水酸化ラジカルを用いた有機物質の酸化分解方法及び酸化分解装置 |
| US6712668B2 (en) | 2000-12-06 | 2004-03-30 | Therma Corporation, Inc. | System and method for electropolishing nonuniform pipes |
| US6428681B1 (en) | 2000-12-06 | 2002-08-06 | Therma Corporation, Inc. | System and method for reversing electrolyte flow during an electropolishing operation |
| TW572063U (en) * | 2001-11-28 | 2004-01-11 | Ind Tech Res Inst | An electropolishing process means for an inner surface of a long tube |
| TW530717U (en) * | 2001-12-13 | 2003-05-01 | Ind Tech Res Inst | An apparatus for electrolyzing polishing/grinding internal surface of long tube |
| US8492489B2 (en) | 2004-02-13 | 2013-07-23 | Total Petrochemicals Research Feluy | Double loop technology |
| WO2007075634A2 (en) | 2005-12-21 | 2007-07-05 | Exxonmobil Research And Engineering Company | Corrosion resistant material for reduced fouling, heat transfer component with improved corrosion and fouling resistance, and method for reducing fouling |
| US8201619B2 (en) | 2005-12-21 | 2012-06-19 | Exxonmobil Research & Engineering Company | Corrosion resistant material for reduced fouling, a heat transfer component having reduced fouling and a method for reducing fouling in a refinery |
| WO2010142550A1 (en) * | 2009-06-08 | 2010-12-16 | Novo Nordisk A/S | A method for manufacturing a needle cannula having improved flow properties |
| DE102016100558B4 (de) * | 2016-01-14 | 2023-08-10 | Plasotec Gmbh | Polierkopf und Verfahren zum Plasmapolieren einer Innenfläche eines Werkstücks |
| US10864567B2 (en) | 2018-04-17 | 2020-12-15 | Government Of The United States As Represented By The Secretary Of The Army | Systems and methods for electroprocessing a gun barrel using a moving electrode |
| CN115122227B (zh) * | 2022-06-20 | 2023-06-27 | 沈阳理工大学 | 一种金属管类零件异形截面螺旋深孔内表面移动式等离子电化学抛光装置 |
| EP4309811B1 (de) * | 2022-07-18 | 2024-09-25 | Hammann GmbH | Verfahren zur elektromechanischen entfernung von ablagerungen in rohrleitungen oder apparaten |
| CN116288637A (zh) * | 2023-02-01 | 2023-06-23 | 中科艾尔(北京)科技有限公司 | 一种电解抛光过程中表面光滑度的控制系统及方法 |
| TW202513905A (zh) * | 2023-05-23 | 2025-04-01 | 美商蘭姆研究公司 | 歧管之內部幾何形狀的表面加工 |
| CN117655436B (zh) * | 2023-12-29 | 2026-03-27 | 上海交通大学 | 一种零件内通道光整装置及方法 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3202598A (en) * | 1963-03-22 | 1965-08-24 | Titanium Metals Corp | Electrolytic polishing tool |
| FR2561672A1 (fr) * | 1984-03-21 | 1985-09-27 | Travaux Milieu Ionisant | Dispositif d'electrolyse, utilisable notamment pour la decontamination radioactive de surfaces metalliques |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2764540A (en) * | 1952-09-10 | 1956-09-25 | William G Farin | Method and means for electropolishing inner surfaces |
| DE1202607B (de) * | 1961-01-20 | 1965-10-07 | Nyby Bruk Ab | Verfahren zur anodischen Oberflaechenbehandlung von Metallgegenstaenden |
| DE1496727B2 (de) * | 1963-06-18 | 1972-03-02 | Benteler Werke AG, Werk Neuhaus, 4794 Schloß Neuhaus | Verfahren zur elektrolytischen behandlung der innen und aussenflaeche von rohren |
| JPS5691380U (de) * | 1979-12-14 | 1981-07-21 | ||
| US4369101A (en) * | 1980-05-02 | 1983-01-18 | Nukem Gmbh | Apparatus for electropolishing tubes |
| JPS6050878A (ja) * | 1983-08-30 | 1985-03-20 | 日本電気株式会社 | コネクタ |
| DE3343396A1 (de) * | 1983-11-30 | 1985-06-05 | Kraftwerk Union AG, 4330 Mülheim | Verfahren zum dekontaminieren metallischer komponenten einer kerntechnischen anlage |
| US4601802A (en) * | 1984-07-31 | 1986-07-22 | The Upjohn Company | Apparatus for internally electropolishing tubes |
-
1986
- 1986-05-20 AT AT86106812T patent/ATE54681T1/de active
- 1986-05-20 EP EP86106812A patent/EP0247209B1/de not_active Expired - Lifetime
- 1986-05-20 DE DE8686106812T patent/DE3672831D1/de not_active Expired - Lifetime
-
1987
- 1987-05-08 US US07/047,653 patent/US4772367A/en not_active Expired - Fee Related
- 1987-05-19 JP JP62120323A patent/JPH0765240B2/ja not_active Expired - Lifetime
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3202598A (en) * | 1963-03-22 | 1965-08-24 | Titanium Metals Corp | Electrolytic polishing tool |
| FR2561672A1 (fr) * | 1984-03-21 | 1985-09-27 | Travaux Milieu Ionisant | Dispositif d'electrolyse, utilisable notamment pour la decontamination radioactive de surfaces metalliques |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0607894A1 (de) * | 1993-01-19 | 1994-07-27 | Corning Incorporated | Verfahren zum elektrolytischen Polieren mit einer STEM-Elektrode |
| WO2017220633A1 (de) * | 2016-06-21 | 2017-12-28 | Extrude Hone Gmbh | Verfahren und vorrichtung zum elektrolytischen polieren und verfahren zum herstellen einer kathode |
Also Published As
| Publication number | Publication date |
|---|---|
| JPS62290899A (ja) | 1987-12-17 |
| JPH0765240B2 (ja) | 1995-07-12 |
| EP0247209B1 (de) | 1990-07-18 |
| ATE54681T1 (de) | 1990-08-15 |
| US4772367A (en) | 1988-09-20 |
| DE3672831D1 (de) | 1990-08-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0247209B1 (de) | Vorrichtung und Verfahren zum elektrochemischen Polieren der Innenflächen von Rohren | |
| EP0098468A1 (de) | Verfahren zum Schweissplattieren von senkrechten Wänden | |
| DE2634282B1 (de) | Verfahren zum kontinuierlichen einbringen von zusatzmitteln in ein mit fluessigem metall gefuelltes gefaess | |
| DE1440263A1 (de) | Vorrichtung zum Herstellen von Bohrungen geringen Durchmessers mittels Elektroerosion | |
| EP0335277A1 (de) | Verfahren und Vorrichtung zum selektiven Elektroplattieren | |
| DE68925145T2 (de) | Durch Ziehen eines Bündels erhaltene Metallfaser | |
| DE3136187C2 (de) | Verfahren und Vorrichtung zur Reinigung der Innenwände von metallischen Leitungssystemen durch Elektropolieren mit Hilfe bewegter Elektroden | |
| DE1298388B (de) | Verfahren und Vorrichtung zur elektrolytischen Bearbeitung eines metallenen Werkstoffes | |
| EP0053719B1 (de) | Verfahren zum Ätzen von Metalloberflächen | |
| DE1807481C3 (de) | Verfahren zum partiellen Galvanisieren | |
| DE3123645C2 (de) | ||
| DE2544305A1 (de) | Verfahren und vorrichtung zum aetzen der inneren oberflaeche von rohren oder hohlzylindern | |
| EP0038447A1 (de) | Vorrichtung zum partiellen Galvanisieren von leitenden oder leitend gemachten Oberflächen | |
| DE8613637U1 (de) | Vorrichtung zum elektrochemischen Polieren der Innenflächen von Rohren | |
| DE2449735A1 (de) | Verfahren zur elektrolytischen abscheidung von metallen auf zylinderfoermigen gegenstaenden und vorrichtung zur durchfuehrung des verfahrens | |
| DE202019001138U1 (de) | Anlage zum Plasmapolieren durch Elektrolytstrahl | |
| DE2356985A1 (de) | Verfahren zur herstellung nahtloser metallischer rohre | |
| EP1902161B1 (de) | Elektrodenanordnung und verfahren zum elektrochemischen beschichten einer werkstückoberfläche | |
| DE2842201C2 (de) | Vorrichtung zum Herstellen verzinnter Kupferdrähte | |
| EP0074464B1 (de) | Vorrichtung zur Reinigung der Innenwände von metallischen Leitungssystemen durch Elektropolieren mit Hilfe bewegter Elektroden | |
| EP0020318A1 (de) | Vorrichtung zum Herstellen geschweisster Gitter aus einander kreuzenden Metalldrähten mit Hilfe der elektrischen Widerstandsschweissmethode | |
| EP1060827B1 (de) | Verfahren und Vorrichtung zur Innenoberflächenbehandlung von metallischen Rohren | |
| DE19635404C2 (de) | Verfahren und Elektrode zum Entgraten und/oder Einrunden von scharfkantigen Übergängen in Rauchabzugsbohrungen in Waffenrohren | |
| DE2301391A1 (de) | Ausbildung, anordnung und verwendung eines mit einer metallflaeche zu verschweissenden metallstifts | |
| DE3323060C2 (de) | Verfahren zur Fixierung von radioaktivem Krypton sowie Vorrichtung zur Durchführung des Verfahrens |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19880211 |
|
| 17Q | First examination report despatched |
Effective date: 19890328 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRE;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED.SCRIBED TIME-LIMIT Effective date: 19900718 Ref country code: SE Effective date: 19900718 Ref country code: NL Effective date: 19900718 Ref country code: BE Effective date: 19900718 Ref country code: FR Effective date: 19900718 |
|
| REF | Corresponds to: |
Ref document number: 54681 Country of ref document: AT Date of ref document: 19900815 Kind code of ref document: T |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| REF | Corresponds to: |
Ref document number: 3672831 Country of ref document: DE Date of ref document: 19900823 |
|
| EN | Fr: translation not filed | ||
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19910520 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19910531 Ref country code: CH Effective date: 19910531 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19910531 |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19980507 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19980625 Year of fee payment: 13 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990520 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19990520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000301 |