EP0341457A2 - Procédé pour produire une bande de papier lisse et brillant, et calandre pour l'application du procédé - Google Patents
Procédé pour produire une bande de papier lisse et brillant, et calandre pour l'application du procédé Download PDFInfo
- Publication number
- EP0341457A2 EP0341457A2 EP89106932A EP89106932A EP0341457A2 EP 0341457 A2 EP0341457 A2 EP 0341457A2 EP 89106932 A EP89106932 A EP 89106932A EP 89106932 A EP89106932 A EP 89106932A EP 0341457 A2 EP0341457 A2 EP 0341457A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- paper web
- roller
- nip
- rollers
- calender arrangement
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21G—CALENDERS; ACCESSORIES FOR PAPER-MAKING MACHINES
- D21G1/00—Calenders; Smoothing apparatus
- D21G1/0073—Accessories for calenders
- D21G1/0093—Web conditioning devices
Definitions
- the invention relates to a method of the type corresponding to the preamble of claims 1 and 2 and a calender arrangement for carrying out this method.
- a generic method and such a calender arrangement are known from DE-OS 36 00 033.
- the known embodiment comprises two pairs of rollers passed one after the other by the paper web, the rollers of which are arranged in reverse, ie in the first pair of rollers the hard roller engages on the paper web on one side and in the second pair of rollers on the other side. This results in the same treatment and surface formation of the paper web on both sides.
- the hard roller ie the steel roller, is heated to a temperature in the two pairs of rollers which corresponds at least to the temperature at which the fibers of the paper web begin to deform. In the case of paper, this temperature is approximately 175 ° C.
- the high temperature results in a paper web with improved gloss without a substantial loss of specific volume, ie volume per gram of paper mass, which corresponds to the reciprocal of the density.
- the surface should have the best possible gloss without the paper web as a whole being compressed by a continuous plasticization to form a compact mass with a low specific volume and poor opacity.
- the invention has for its object to increase this effect of the generation of gloss on the surface without lowering the "bulk”, ie the specific volume inside.
- the heat can be removed from cooling on one side or on both sides. However, it must be so thorough that noticeable heat is also removed from the inner areas of the paper web.
- the surface heating increases the gloss effect of the hard roller by increasing the surface temperature beforehand.
- the additional surface heating should of course be carried out so that it is limited to the surface, so that the effect of the cooling is not negated. It is particularly suitable at high working speeds, at which it can be difficult to achieve the required heating in the short contact period of the paper web in the highly heated hard roller.
- the invention also relates to the calender arrangements corresponding to claims 1 and 2, which are reproduced in claims 4 and 5.
- two pairs of rollers are therefore present, which form two nips which are traversed successively by the paper web, as is shown in DE-OS 36 00 033.
- At least the second roll nip should be preceded by a cooling device for the continuous paper web in order to counteract the increase in temperature inside, which is caused by the treatment of the paper web in the first roll nip and the subsequent penetration of the heat into the paper web.
- the cooling device can be designed according to claim 8 or 9 in detail.
- the smoothing effect of the highly heated hard roll can be supported by applying a certain amount of heat to the paper web on the side to be smoothed before it enters the roll gap in question (claim 10).
- the corresponding heating device can be designed in detail according to claims 11 to 13.
- the change in the wrap angle according to claims 14 and 15 is a relatively simple method to implement, to adapt the contact time of the web to the roller in question and thus to adapt the amount of heat transferred.
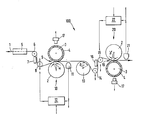
- the designated as a whole with 100 Calender arrangement includes two roller pairs 10 and 20, which are traversed by the paper web 1 one after the other and each having a high heated steel roller 2 with surface temperatures in the range of 150 to 250 o C and a "soft", ie with a paper or Plastic cover 4 provided roller 3 include.
- the highly heated steel roller 2 engages the paper web 1 from below, and in the case of the pair of rollers 20 the corresponding highly heated steel roller 2 from above.
- At least one of the cooperating rollers 2, 3 of each roller pair 10, 20 is controlled by deflection.
- the paper web 1 runs with the usual moisture content of 5 to 15% initially according to the drawing from the left through a cooling field 5, in which, for example, cold air is blown onto the web surface and thereby its temperature is lowered, for example below the ambient temperature, if the paper web 1 previously Ambient temperature.
- the cooled paper web 1 is then deflected vertically downwards via a deflection roller 6 and passes through a heating device 7, which can be designed, for example, as radiant heating and by means of which the paper web superficially on the side facing the highly heated hard roller 2 when passing through the roller pair 10 Experiences temperature increase.
- a heating device 7 can be designed, for example, as radiant heating and by means of which the paper web superficially on the side facing the highly heated hard roller 2 when passing through the roller pair 10 Experiences temperature increase.
- the paper web 1 is guided over a vertically movable deflection roller 8.
- the paper web 1 then runs into the nip 9 of the first pair of rollers 10.
- the vertical mobility of the deflection roller 8 has the purpose of changing the wrap angle ⁇ of the highly heated hard roller 2 in order to change and adapt the heat transfer from the roller 2 to the lower side of the paper web 1 to be smoothed in the roller gap 9 by a correspondingly changed contact time to be able to.
- the effect of the treatment in the nip 9 on the lower side of the paper web 1 to be smoothed is detected by a smoothing measuring device 11, the signals of which are processed in a control device 12 and used to control the position of the deflection roller 8 and thus the wrap angle ⁇ .
- the paper web 1 After leaving the nip 9, the paper web 1 has a considerable temperature on the underside, which would normally spread into the interior of the paper web 1. To prevent this, the paper web 1 is passed over a cooling roller 13 which is connected upstream of the next pair of rollers 20. As a result, the previously highly heated side of the paper web 1 is cooled and heat is removed from it as a whole.
- the degree of cooling effect can be controlled by changing the wrap angle ⁇ of the cooling roller 13 by means of the deflecting roller 14 which can be raised and lowered.
- the deflecting roller 14 is followed in the web running direction by a deflecting roller 15 which can be raised and lowered in such a way that a vertical web section is present between the deflecting rollers 14 and 15, the position of which does not change when the position of the deflecting rollers 14, 15 changes, and that of the highly heated roller 2 of the second pair of rollers 20 facing the upper side of the paper web 1 is opposed by a heating device 16 which heats up the web 1 on the surface. With the superficial additional heat, the material web 1 reaches the nip 19 of the second pair of rollers 20, the wrap angle ⁇ of the highly heated roller 2 and thus its effect on the paper web 1 being determined by the position of the deflection roller 15.
- the effect of the treatment in the roll gap 19 is controlled by the measuring device 21 and input to a control device 22 which controls the position of the deflection roller 15.
- temperature measuring devices 17 are provided.
- the soft rollers 3 are cooled, so that the paper web 1 bears on one side against the highly heated hard roller 2 and on the other side against the cooled roller 3 .
- the cooling effect of the soft roller 3 can be influenced by changing the wrap angle. It goes without saying that the wrap angle on the hard roller 2 cannot be changed at the same time.
- cooling can also take place at this point by means of a cooled roller.
- a cooling field can also be present instead of the cooled roller 13, although the cooled roller 13 has advantages in that it acts specifically on the side of the paper web 1 heated by the highly heated hard roller 2 of the nip 9.
- the heaters 7, 16 are only optional. There may be only one or no additional heating device at all.
Landscapes
- Paper (AREA)
- Treatment Of Fiber Materials (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3815463A DE3815463A1 (de) | 1988-05-06 | 1988-05-06 | Verfahren zur erzeugung von glaette und glanz auf einer papierbahn und entsprechende kalanderanordnung |
| DE3815463 | 1988-05-06 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0341457A2 true EP0341457A2 (fr) | 1989-11-15 |
| EP0341457A3 EP0341457A3 (fr) | 1990-01-17 |
Family
ID=6353785
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89106932A Withdrawn EP0341457A3 (fr) | 1988-05-06 | 1989-04-18 | Procédé pour produire une bande de papier lisse et brillant, et calandre pour l'application du procédé |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US5033373A (fr) |
| EP (1) | EP0341457A3 (fr) |
| JP (1) | JPH01321999A (fr) |
| BR (1) | BR8902056A (fr) |
| DE (1) | DE3815463A1 (fr) |
| FI (1) | FI892162L (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO1992003614A1 (fr) * | 1990-08-22 | 1992-03-05 | Beloit Corporation | Procede de reduction du pluchage |
| EP0529385A1 (fr) * | 1991-08-08 | 1993-03-03 | Sulzer-Escher Wyss Gmbh | Procédé et dispositif pour produire une bande lisse et brillante |
| US5387782A (en) * | 1991-04-17 | 1995-02-07 | Sulzer-Escher Wyss Gmbh | Apparatus for smoothing paper webs |
| EP0957202B1 (fr) * | 1998-05-08 | 2004-03-31 | V.I.B. Systems GmbH | Procédé et dispositif pour la fabrication de papier SC-A online |
Families Citing this family (34)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4011394C1 (fr) * | 1990-04-09 | 1991-11-28 | Sulzer-Escher Wyss Gmbh, 7980 Ravensburg, De | |
| DE4121381C1 (fr) * | 1991-06-28 | 1992-06-04 | Sulzer-Escher Wyss Gmbh, 7980 Ravensburg, De | |
| US5215008A (en) * | 1991-10-24 | 1993-06-01 | Kartovaara Ilkka K | Calendering machine for testing paper |
| ATE176508T1 (de) | 1992-11-03 | 1999-02-15 | Valmet Corp | Verfahren und vorrichtung zum beideseitigen streichen einer dünnen druckpapierbahn |
| DE9320455U1 (de) * | 1993-01-16 | 1994-08-25 | V.I.B. Apparatebau Gmbh, 63477 Maintal | Vorrichtung zum Erhöhen von Glanz und/oder Glätte einer Materialbahn |
| FI95061C (fi) * | 1993-03-08 | 1995-12-11 | Valmet Paper Machinery Inc | Menetelmä paperiradan kalanteroinnissa ja menetelmää soveltava kalanteri |
| DE9306448U1 (de) * | 1993-04-29 | 1993-06-09 | Sulzer-Escher Wyss GmbH, 7980 Ravensburg | Glättwerksanordnung |
| IT1271756B (it) * | 1994-03-17 | 1997-06-09 | Interplastica S A | Procedimento ed apparato atti ad assicurare un ottimo ancoraggio fra un tessuto e il relativo rivestimento di materiale plastico, direttamente mediante calandratura |
| US5524532A (en) * | 1994-12-28 | 1996-06-11 | Valmet Corporation | Method and apparatus for calendering a paper or board web |
| JPH10128946A (ja) * | 1996-10-30 | 1998-05-19 | Riso Kagaku Corp | 製版装置 |
| DE69919538T2 (de) | 1998-01-20 | 2005-09-08 | Metso Paper, Inc. | Verfahren ung vorrichtung zur konditionierung einer walze, insbesondere von einer walze in einer papierherstellungs- oder veredelungsvorrichtung |
| DE19826899B4 (de) * | 1998-05-08 | 2005-05-19 | V.I.B. Systems Gmbh | Verfahren und Vorrichtung zur Online-Kalandrierung von SC-A-Papier |
| DE19821820A1 (de) * | 1998-05-15 | 1999-11-18 | Voith Sulzer Papiertech Patent | Vorrichtung zur Oberflächenbehandlung einer laufenden Materialbahn, insbesondere aus Karton |
| US6085646A (en) * | 1998-08-04 | 2000-07-11 | Beloit Technologies, Inc. | Multiple nip calender for a paper making machine |
| US6287424B1 (en) | 1998-09-22 | 2001-09-11 | International Paper Company | Method for finishing paperboard to achieve improved smoothness |
| US6190500B1 (en) | 1998-10-02 | 2001-02-20 | International Paper Company | Multilayer linerboard having improved printing properties and related method of manufacture |
| FI115235B (fi) | 2000-02-11 | 2005-03-31 | Metso Paper Inc | Menetelmä ja laite kalanteroinnissa |
| EP1162045B1 (fr) * | 2000-05-30 | 2007-03-14 | Andritz Küsters GmbH & Co. KG | Dispositif à rouleau |
| FI20002782L (fi) * | 2000-12-19 | 2002-06-20 | Keskuslaboratorio | Menetelmä ja laite paperin kalanteroimiseksi |
| US6893693B2 (en) * | 2000-12-21 | 2005-05-17 | Georgia-Pacific Corporation | High gloss disposable pressware |
| US6715630B2 (en) | 2002-01-23 | 2004-04-06 | Fort James Corporation | Disposable food container with a linear sidewall profile and an arcuate outer flange |
| US7337943B2 (en) * | 2002-06-27 | 2008-03-04 | Dixie Consumer Products Llc | Disposable servingware containers with flange tabs |
| US8584929B2 (en) | 2003-10-20 | 2013-11-19 | Dixie Consumer Products Llc | Pressed paperboard servingware with improved rigidity and rim stiffness |
| US7819790B2 (en) | 2004-02-20 | 2010-10-26 | Dixie Consumer Products Llc | Apparatus for making paperboard pressware with controlled blank feed |
| DE102004032507A1 (de) * | 2004-07-06 | 2006-02-16 | Voith Paper Patent Gmbh | Verfahren und Vorrichtung zum Behandeln einer Bahn aus Papier oder Karton |
| DE102005039991A1 (de) * | 2005-08-23 | 2007-03-08 | Voith Patent Gmbh | Kalander |
| US20080230001A1 (en) * | 2006-02-23 | 2008-09-25 | Meadwestvaco Corporation | Method for treating a substrate |
| DE102009024912B4 (de) * | 2009-06-15 | 2011-11-17 | OCé PRINTING SYSTEMS GMBH | Verfahren zum Ändern der Temperatur einer Bedruckstoffbahn in einem Drucker oder Kopierer |
| US8684260B2 (en) | 2011-04-01 | 2014-04-01 | Reynolds Consumer Products Inc. | Paperboard plate with corner walls |
| EP2682520B1 (fr) | 2012-07-03 | 2016-06-22 | Valmet Technologies, Inc. | Procédé de production d'une bande fibreuse et ligne de production d'une bande fibreuse |
| EP2765237B1 (fr) | 2013-02-06 | 2016-11-23 | Valmet Technologies, Inc. | Procédé de production d'une bande de fibres et ligne de fabrication d'une bande de fibres |
| EP2876206B2 (fr) | 2013-11-21 | 2023-03-01 | Valmet Technologies, Inc. | Procédé de produktion de bandes de fibres et ligne de fabrication de bandes de fibres |
| DE102018127037B4 (de) | 2018-10-30 | 2021-03-18 | Andritz Küsters Gmbh | Kalander |
| DE102021113813A1 (de) | 2021-05-28 | 2022-12-01 | Voith Patent Gmbh | Verfahren und Vorrichtung |
Family Cites Families (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1291626A (en) * | 1914-03-09 | 1919-01-14 | Int Paper Co | Surfacing paper. |
| US1714261A (en) * | 1927-11-11 | 1929-05-21 | J O Ross Engineering Corp | Paper-converting machinery |
| US2251890A (en) * | 1937-06-25 | 1941-08-05 | Champion Paper & Fibre Co | Supercalendering process |
| US2554663A (en) * | 1949-12-15 | 1951-05-29 | Us Rubber Co | Method of glossing paper |
| GB953713A (en) * | 1960-04-04 | 1964-04-02 | Beloit Iron Works | Improvements in or relating to the finishing of coated paper web materials |
| US3124504A (en) * | 1960-04-04 | 1964-03-10 | Gloss finishing of uncoated paper | |
| US3254593A (en) * | 1963-10-03 | 1966-06-07 | Beloit Corp | Gloss calender drive system and method |
| DE1804515B2 (de) * | 1968-10-23 | 1974-05-30 | Kleinewefers Industrie Co Gmbh, 4150 Krefeld | Kalander zum Mattsatinieren von Papierbahnen |
| US3841963A (en) * | 1971-07-06 | 1974-10-15 | Kleinewefers Ind Co Gmbh | Apparatus for satinizing fibrous webs |
| DE2543228C3 (de) * | 1975-09-27 | 1979-02-22 | J.M. Voith Gmbh, 7920 Heidenheim | Kalander für Papier- und Kartonbahnen |
| JPS5588878A (en) * | 1978-12-27 | 1980-07-04 | Mitsubishi Paper Mills Ltd | Method and apparatus for finishing coated paper |
| CH662837A5 (de) * | 1983-02-10 | 1987-10-30 | Escher Wyss Ag | Kalander zur druck- und waermebehandlung von warenbahnen. |
| US4624744A (en) * | 1984-05-18 | 1986-11-25 | S. D. Warren Company | Method of finishing paper utilizing substrata thermal molding |
| FI72768B (fi) * | 1984-11-30 | 1987-03-31 | Waertsilae Oy Ab | Nerkylning av pappersbana i superkalander. |
| FI71374C (fi) * | 1984-12-31 | 1986-12-19 | Valmet Oy | Foerfarande och anordning vid kalandrering av en bana |
| US4606264A (en) * | 1985-01-04 | 1986-08-19 | Wartsila-Appleton, Incorporated | Method and apparatus for temperature gradient calendering |
| US4689895A (en) * | 1986-02-28 | 1987-09-01 | Thermo Electron-Web Systems, Inc. | Evaporative-cooling apparatus and method for the control of web or web-production machine component surface temperatures |
| US4786529A (en) * | 1987-06-15 | 1988-11-22 | Measurex Corporation | Cross directional gloss controller |
-
1988
- 1988-05-06 DE DE3815463A patent/DE3815463A1/de active Granted
-
1989
- 1989-04-18 EP EP89106932A patent/EP0341457A3/fr not_active Withdrawn
- 1989-05-02 JP JP1113590A patent/JPH01321999A/ja active Pending
- 1989-05-02 BR BR898902056A patent/BR8902056A/pt not_active Application Discontinuation
- 1989-05-03 US US07/347,253 patent/US5033373A/en not_active Expired - Fee Related
- 1989-05-05 FI FI892162A patent/FI892162L/fi not_active Application Discontinuation
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO1992003614A1 (fr) * | 1990-08-22 | 1992-03-05 | Beloit Corporation | Procede de reduction du pluchage |
| US5387782A (en) * | 1991-04-17 | 1995-02-07 | Sulzer-Escher Wyss Gmbh | Apparatus for smoothing paper webs |
| EP0529385A1 (fr) * | 1991-08-08 | 1993-03-03 | Sulzer-Escher Wyss Gmbh | Procédé et dispositif pour produire une bande lisse et brillante |
| US5318670A (en) * | 1991-08-08 | 1994-06-07 | Sulzer-Escher Wyss Gmbh | Method for the generation of smoothness and gloss of a paper web |
| EP0957202B1 (fr) * | 1998-05-08 | 2004-03-31 | V.I.B. Systems GmbH | Procédé et dispositif pour la fabrication de papier SC-A online |
Also Published As
| Publication number | Publication date |
|---|---|
| FI892162A0 (fi) | 1989-05-05 |
| FI892162A7 (fi) | 1989-11-07 |
| FI892162L (fi) | 1989-11-07 |
| EP0341457A3 (fr) | 1990-01-17 |
| US5033373A (en) | 1991-07-23 |
| JPH01321999A (ja) | 1989-12-27 |
| BR8902056A (pt) | 1989-12-05 |
| DE3815463A1 (de) | 1989-11-16 |
| DE3815463C2 (fr) | 1990-02-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3815463C2 (fr) | ||
| DE69405621T2 (de) | Verfahren zum Kalandern einer Papierbahn und ein Kalander zur Durchführung des Verfahrens | |
| DE3305429C2 (de) | Kalander zur Druck- und Wärmebehandlung von Warenbahnen | |
| DE69803049T2 (de) | Verfahren zum kalandrieren und ein kalander zur durchführung des verfahrens | |
| DE69517193T2 (de) | Vorrichtung zum trocknen und glätten einer faserbahn | |
| DE69802672T2 (de) | Verfahren zum kalandrieren und kalander zur anwendung des verfahrens | |
| EP0529385B1 (fr) | Procédé et dispositif pour produire une bande lisse et brillante | |
| DE3542342A1 (de) | Verfahren und anordnung zum kalandern von papier- oder pappebahnen | |
| DE29813663U1 (de) | Vorrichtung zur Online-Herstellung von SC-A-Papier | |
| DE19835989C5 (de) | Verfahren und Vorrichtung zur Online-Kalandrierung von Papier | |
| DE4035986C2 (de) | Kalander für den On-line-Anschluß an eine Papiermaschine | |
| EP0989233B1 (fr) | Section de séchage et sécheur à convection pour une telle section de séchage | |
| DE19901400A1 (de) | Trocknungs- und Glättungseinheit für Faserstoffbahnen | |
| DE69922041T2 (de) | Verfahren und vorrichtung zur behandlung von papier oder pappebahnen | |
| EP0957202B1 (fr) | Procédé et dispositif pour la fabrication de papier SC-A online | |
| EP2295632B1 (fr) | Calendre | |
| DE4037166C1 (en) | Regulation of web width in paper machine - with calendering rolls comprising flexible roll and heating roll, and edge catches at sides in wire section | |
| DE9306448U1 (de) | Glättwerksanordnung | |
| DE102021113813A1 (de) | Verfahren und Vorrichtung | |
| EP1314818B1 (fr) | Appareil et procédé pour lisser une bande de papier ou de carton | |
| EP1614802B1 (fr) | Procédé et appareil pour le traitement d' une bande de papier ou carton | |
| AT506010B1 (de) | Verfahren und anordnung zur einflussnahme auf die eigenschaften einer faserbahn | |
| DE112004000707T5 (de) | Vorrichtung und Verfahren zur Herstellung von Papier oder Karton, und damit hergestelltes Papier oder Karton | |
| DE1303066C2 (de) | Verfahren und vorrichtung zum kaschieren von folienbahnen | |
| DE2456767A1 (de) | Verfahren und vorrichtung zur oberflaechenbearbeitung von bahnmaterial |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): CH FR GB IT LI SE |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): CH FR GB IT LI SE |
|
| 17P | Request for examination filed |
Effective date: 19900706 |
|
| 17Q | First examination report despatched |
Effective date: 19911022 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19920303 |