EP0377478A1 - Appareil pour inspecter des matières en vrac - Google Patents
Appareil pour inspecter des matières en vrac Download PDFInfo
- Publication number
- EP0377478A1 EP0377478A1 EP90200013A EP90200013A EP0377478A1 EP 0377478 A1 EP0377478 A1 EP 0377478A1 EP 90200013 A EP90200013 A EP 90200013A EP 90200013 A EP90200013 A EP 90200013A EP 0377478 A1 EP0377478 A1 EP 0377478A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- colour
- bulk goods
- conveyor means
- video signals
- video camera
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000002356 single layer Substances 0.000 claims abstract description 3
- 239000003086 colorant Substances 0.000 claims description 7
- 241000208125 Nicotiana Species 0.000 claims description 3
- 235000002637 Nicotiana tabacum Nutrition 0.000 claims description 3
- 239000011159 matrix material Substances 0.000 claims description 3
- 239000008187 granular material Substances 0.000 claims description 2
- 235000013311 vegetables Nutrition 0.000 claims description 2
- 238000001514 detection method Methods 0.000 abstract description 6
- 238000007689 inspection Methods 0.000 abstract description 6
- 230000007704 transition Effects 0.000 abstract description 5
- 238000001914 filtration Methods 0.000 abstract description 2
- 238000010276 construction Methods 0.000 description 4
- 239000010410 layer Substances 0.000 description 4
- 239000013590 bulk material Substances 0.000 description 2
- 230000007547 defect Effects 0.000 description 2
- 230000001419 dependent effect Effects 0.000 description 2
- 238000005286 illumination Methods 0.000 description 2
- 244000000626 Daucus carota Species 0.000 description 1
- 235000002767 Daucus carota Nutrition 0.000 description 1
- 235000007688 Lycopersicon esculentum Nutrition 0.000 description 1
- 240000003768 Solanum lycopersicum Species 0.000 description 1
- 238000004364 calculation method Methods 0.000 description 1
- 239000002131 composite material Substances 0.000 description 1
- 238000009795 derivation Methods 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 239000011888 foil Substances 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 238000012544 monitoring process Methods 0.000 description 1
- 239000011022 opal Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/34—Sorting according to other particular properties
- B07C5/342—Sorting according to other particular properties according to optical properties, e.g. colour
- B07C5/3422—Sorting according to other particular properties according to optical properties, e.g. colour using video scanning devices, e.g. TV-cameras
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/36—Sorting apparatus characterised by the means used for distribution
- B07C5/363—Sorting apparatus characterised by the means used for distribution by means of air
- B07C5/365—Sorting apparatus characterised by the means used for distribution by means of air using a single separation means
- B07C5/366—Sorting apparatus characterised by the means used for distribution by means of air using a single separation means during free fall of the articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/36—Sorting apparatus characterised by the means used for distribution
- B07C5/363—Sorting apparatus characterised by the means used for distribution by means of air
- B07C5/367—Sorting apparatus characterised by the means used for distribution by means of air using a plurality of separation means
- B07C5/368—Sorting apparatus characterised by the means used for distribution by means of air using a plurality of separation means actuated independently
Definitions
- the invention relates to an apparatus for inspecting bulk goods, such as vegetables, tobacco, granulates and the like, having an average colour within certain tolerance limits, said apparatus comprising:
- Such an apparatus is e.g. known from EP-A-104 369 and US-A-4 235 342.
- the invention provides an inspection apparatus of the type mentioned above, characterized in that the background observed by the video camera has substantially the same colour as correct bulk goods.
- the apparatus may be characterized in that the background is the upper surface of the conveyor means supporting the bulk goods.
- a very simple embodiment is that in which characterized in that the upper surface of said conveyor means has substantially the same colour as correct bulk goods.
- a conveyor belt can be designed in total in the same colour as the bulk goods to be transported, e.g. an orange conveyor belt for inspecting carrots, a red one for tomatoes, a brown one for tobacco, etcetera.
- the apparatus is characterized in that the conveyor means are translucent; a second light source is positioned under the conveyor means; diffusor means are provided for diffusing light passing said conveyor means; and colour means are provided; in such a way that the background is formed by diffuse light having substantially the same colour as correct bulk goods.
- the diffusor means may be designed as the conveyor means themselves, that e.g. can be provided with a diffusing lower or upper surface or be opal, whilst also use may be made of a diffusor plate between the conveyor means and the second light source.
- the colour means in question may be engineered in different ways. E.g. use may be made of a light source emitting itself light of the desired colour, whilst also use may be made of a colour filter, that is only transparent for the desired colours. This filter may form part of the conveyor means themselves, e.g. be designed as a coloured transparent foil.
- the apparatus is characterized in that the memory is designed as a table (LOOK UP TABLE: LUT) having discrete contents; the second video signals are transferred into digital format by means of an analog/digital convertor; and the digitized second video signals are supplied to the table as an address therefore.
- LOOK UP TABLE: LUT LOOK UP TABLE: LUT
- the apparatus may be characterized by means for forming colour signals, e.g. corresponding with the three basic colours red, green and blue, each having a chrominance component and a luminance component: and a light source emitting light containing the relevant colour(s).
- colour signals e.g. corresponding with the three basic colours red, green and blue, each having a chrominance component and a luminance component: and a light source emitting light containing the relevant colour(s).
- the transfer into digital format can take place in this case such that characterized in that the analog/digital convertor transfers the luminance component of each of the colour signals into digital format of at most eight bits.
- the camera can be of the matrix type or the linear type.
- a matrix camera one can use e.g. mutually partially overlapping pictures, if desired, with intermittent illumination in which case the light source is adapted thereto.
- intermittent illumination in which case the light source is adapted thereto.
- use may be made of a continuous illumination.
- the camera can also be of the linear-array type, in which case the light sensitive elements extend in a direction having a component transverse relative to the conveyor means.
- the apparatus is characterized by selective means for amplifying or attenuating parts of the video signals. This can be engineered e.g. as offset-means for bringing the video signals in a desired band.
- the three components from the basis of a six-dimensional space.
- the reflections of the product and the picture of the conveyor means, particularly a conveyor belt observed by the video camera give picture elements, generally indicated as pixels. These pixels form clusters in the six-dimensional space. These clusters can mutually contain each other in total or in part. Also reflections from the undesired elements to be detected form clusters in this more dimensional space.
- the signal processing apparatus can distinguish between these clusters.
- the contents of the address determines whether the pixel in question is a picture of a product element, of the background (e.g. the conveyor means) or an undesired element to be detected.
- the address is supplied to a processing element that on basis of the frequency of occurrence and/or the values of pixels in the vicinity takes a decision relative to the classification of the pixel in question.
- These data are supplied to a control unit that on basis of the pixel in the picture takes a decision on basis of which the mentioned report signal can or can not energize an ejection station.
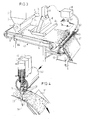
- Fig. 1 shows an apparatus 1 for cleansing of bulk good present in a bulk container 2.
- a funnel 3 is connected for supplying through a dispensing device 4 engineered as a turnstile-lock a thin layer 6 of the bulk goods.
- the turnstile-lock 4 is driven by a motor 7 in order to achieve the desired dispensing.
- the conveyor belt 5 is driven at a speed such that in combination with the speed determined by the adjustment of motor 7 the desired thickness of the layer of bulk goods is obtained.
- an inspection device 8 is arranged comprising in this embodiment to tubular flash lamps 9, 10 and a video camera 11.
- This video camera 11 can supply its output signals to a signal processing unit 12 that can supply control signals to a pneumatic control unit 13 that can energize a pneumatic cylinder 14 on basis thereof.
- This pneumatic cylinder 14 serves the purpose of causing a swinging movement of a strip 16 around a shaft 15 parallel to the width of the conveyor belt 15, said strip 16 extending over the whole length of transport belt 5.
- the strip 16 is in its upper position in which it does not disturb the free path of the bulk goods 6 thrown away by conveyor belt 5 in such a way that this bulk goods can be caught in a bulk container 18 over a screen 17.
- the apparatus 1 also comprises two tubular flash lamps 81, 82 controlled in synchronism with tube lamps 9 and 10 by the signal processing unit 12 for emitting a light flash.
- the conveyor belt 5 is transparent and between the conveyor belt 5 and flash lamps 81, 82 a diffusor plate 83 is arranged for diffusing the light emitted by lamps 81, 82 and besides being coloured in correspondence with the colour of the transported bulk goods 6.
- the video camera sees a background having the same colour as the colour of correct bulk goods.
- the intensities of the respective light sources 9, 10 and 81, 82, 83, 5 are mutually adapted, as a result of which the respective gray values of the background and the products or the bulk goods to be inspected differ only little.
- Fig. 2 shows a different embodiment 20, in which no use is made of only one strip 16, but rather eight aligned plates 21 - 28. All plates are up and down swingable under control by pneumatic cylinders of which those added to plates 23 - 28 are indicated with reference numerals 29 - 34. In the situation shown in fig. 2 the pneumatic cylinders 29 and 30 are activated, as a result of which the plates 23 and 24 are brought into the free path of the bulk goods 6 due to which the corresponding part thereof is deflected in downward direction. The free path is indicated with 35 and the deflected path is indicated with 36.
- a screen indicated with 37 is present in order to avoid undesired straying of the loose bulk goods.
- the displacement of the plates 21 - 28 is controlled by video cameras 38 - 45 that observe in the manner indicated schematically with interrupted lines 46 a zone of the layer 6 bulk material for generating their output signals and supplying them to a not-shown signal processing unit that in accordance with the construction of the apparatus according to fig. 1 uses the output signals of the video camera 38 for the control of plate 21, those of camera 39 for plate 22, etcetera.
- Fig. 3 shows an apparatus 47 corresponding in several aspects with the apparatus according to fig. 1. Corresponding parts are indicated therefore in fig. 3 with the same reference numerals as they are in fig. 1.
- the apparatus 47 according to fig. 3 comprises only the light source 9, 10.
- the conveyor belt 84 is, different from the conveyor belt 5 according to fig. 1 not transparent, but opaque and has an upper surface having the same colour as the bulk goods 6 to be inspected. In accordance with fig. 1 by this measure it is achieved that the gray values of the products or the bulk goods to be inspected and background observed by the video camera differ only little.
- the video camera supplies its output signals to a signal processing unit 48 that different from the embodiment according to fig. 1 controls not only one element, but rather a plurality of aligned and each individually energizable electromagnetic valves 49, arranged on nozzles 50 in the manner shown in fig. 4 in a pressure conduit 52 connected with a source 51 for pressurized air, in such a way that by opening a valve by corresponding energizing from the signal processing unit 48 an airflow indicated with reference numeral 53 is directed to the layer 6 of bulk material in its free path in such way that this free path is interrupted and is changed into a path having a greater downward speed, as indicated with reference numeral 54.
- the signal processing unit 48 according to fig. 3 differs from the signal processing unit 12 according to fig. 1 in that it has to be adapted for deriving from only one video signal a plurality of signals for the selective control of valves 49.
- Fig. 5 shows schematically the construction of an embodiment of a part of the inspection apparatus according to the invention.
- the video signals supplied by a video camera, in this example video camera 11 comprise the colour components red (R), green (G), blue (B). These colour components supplied by camera 11 or a preprocessor making RGB from composite video are each supplied to a respective digitizer 61, 62, 63. These digitizers are mutually identical. In fig. 6 the block schematic construction of unit 61 is shown and explained with reference thereto.
- Each digitizer 61, 62, 63 supplies in this embodiment six-bits information that is related to the strength of the related input signal.
- the three times six bits are simultaneously supplied to a look up table or LUT 64 having a width of eighteen bits. These eighteen bits determine unambiguously an address location in the LUT 64.
- the contents of the LUT 64 is determined in a learning phase to be herein described in more detail and comprises one- to eight-bits information or the colour combination which is determinative whether or not a certain signal composition indicates a product, the transport conveyor, or defects.
- This one to eight bits information is then supplied to an post-processor 65 that determines the relation of each pixel relative to its neighbours.
- This unit may e.g.
- the unit 65 can also be a so-called SNAP (Systolic Neighbourhood Array Processor) in combination with a so-called feature-max, such as e.g. sold by the firm Datacube, United States of America.
- the SNAP is capable of classifying a pixel in combination with its eight most close neighbours. This classification can be stored in the feature-max.
- a central control unit 66 eventually controls the reading-out of the post-processor 65 and, on basis of previously determined criteria takes a decision relative to the energizing, if necessary, of an ejector (see figures 1, 2 3 and 4). This central control unit also controls the initializing of each part and the control of the whole signal processing.
- Monitoring of the process can take place by means of a monitor 73 receiving signals from the output of LUT 64 through a DA-converter 74.
- Fig. 6 shows as an example the block schematic form of digitizer 61.
- the video information at the input 67 hereof is supplied to a sync-stripper 68 that removes the video control signals from the input video signal.
- the signal is amplified by a controllable amplifier 69 and provided with a controllable offset in an offset unit 70.
- the signal supplied thereby is digitized by a six-bits analog/digital-converter 71.
- the output signal thereof is supplied to a LUT 72 for further processing, e.g. inversion.
- control takes place from the central control unit 66.
- the eighteen-bits colour information of product and background is determined. This information results in a histogram in the three-dimensional colour space. From this histogram it is deduced which combination of the eighteen bits can be classified unambiguously as product, which as background, which as reflections, and which as transition phenomena. These last can be picture edges or shadows. This classification offers the opportunity to substantially fill-in the LUT 64. This filling-in determines whether or not a certain combination is desired. The exact filling-in is dependent upon the nature and the construction of the post-processor 65 and can have a width of one to eight bits.
- central control unit 66 controls the energizing of an ejector on basis of the information signals supplied thereto.
Landscapes
- Engineering & Computer Science (AREA)
- Multimedia (AREA)
- Sorting Of Articles (AREA)
- Length Measuring Devices By Optical Means (AREA)
- Investigating Materials By The Use Of Optical Means Adapted For Particular Applications (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| NL8900037A NL8900037A (nl) | 1989-01-06 | 1989-01-06 | Inrichting voor het inspecteren van massagoed. |
| NL8900037 | 1989-05-19 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0377478A1 true EP0377478A1 (fr) | 1990-07-11 |
| EP0377478B1 EP0377478B1 (fr) | 1995-05-03 |
Family
ID=19853915
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19900200013 Expired - Lifetime EP0377478B1 (fr) | 1989-01-06 | 1990-01-03 | Appareil pour inspecter des matières en vrac |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0377478B1 (fr) |
| DE (1) | DE69019001T2 (fr) |
| ES (1) | ES2075131T3 (fr) |
| NL (1) | NL8900037A (fr) |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO1992008322A1 (fr) * | 1990-10-30 | 1992-05-14 | Simco/Ramic Corporation | Camera video de balayage lineaire en couleurs pour un systeme de controle |
| EP0865833A3 (fr) * | 1997-03-19 | 1999-02-03 | Satake Usa Inc. | Arrière-plan réflecteur pour machine de tri |
| NL1024619C2 (nl) * | 2003-10-24 | 2005-04-27 | Staalkat Internat B V | Inrichting voor het inspecteren van objecten. |
| CN101968346A (zh) * | 2010-09-29 | 2011-02-09 | 中国烟草总公司郑州烟草研究院 | 一种烟叶叶片结构的表征方法 |
| CN102615047A (zh) * | 2012-04-26 | 2012-08-01 | 大树智能科技(南京)有限公司 | 烟把在线检测剔除装置 |
| CN103752532A (zh) * | 2014-01-14 | 2014-04-30 | 河南科技大学 | 一种由plc控制系统控制的转盘气吹式烟叶分拣系统 |
| CN104001677A (zh) * | 2014-05-06 | 2014-08-27 | 中国农业大学 | 一种采用电控自动分料的色选机 |
| US9492849B2 (en) | 2005-05-17 | 2016-11-15 | Visys Nv | Method for sorting products moving in a continuous stream on a chute |
| WO2023198664A1 (fr) * | 2022-04-12 | 2023-10-19 | Omya International Ag | Échantillonneur de courroie automatisé permettant de trier des impuretés, procédé et utilisation |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102009032404A1 (de) * | 2009-07-08 | 2011-01-13 | Claas Selbstfahrende Erntemaschinen Gmbh | Mähdrescher |
| CN101650316B (zh) * | 2009-09-15 | 2011-06-29 | 合肥安大电子检测技术有限公司 | 片烟结构在线检测方法 |
| WO2011066267A2 (fr) * | 2009-11-25 | 2011-06-03 | Jing-Yau Chung | Rejet de végétal défectueux par diffraction et réfraction de la lumière |
| DE102019114033A1 (de) * | 2019-05-26 | 2020-11-26 | Dieffenbacher GmbH Maschinen- und Anlagenbau | Überwachungsvorrichtung zur Erfassung wenigstens einer Stoffkomponente in zerkleinerten Werkstoffen, Förderanlage für zerkleinerte Werkstoffe und Verfahren zur Überwachung von zerkleinerten Werkstoffen |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2645343A (en) * | 1949-04-27 | 1953-07-14 | Kelling Nut Co | Photoelectric inspecting and sorting apparatus |
| GB1283902A (en) * | 1970-01-05 | 1972-08-02 | Gunsons Sortex Ltd | Optical unit for use in a light-sensitive sorting machine |
| FR2430272A1 (fr) * | 1978-07-06 | 1980-02-01 | Blitz Electricite | Procede et dispositif pour la detection de corps etrangers dans un produit divise |
| US4235342A (en) * | 1978-05-05 | 1980-11-25 | Geosource Inc. | Sorting apparatus using programmable classifier |
| EP0104369A2 (fr) * | 1982-08-30 | 1984-04-04 | Pietzsch Aktiengesellschaft | Dispositif et méthode pour la reconnaissance optique de graphismes plats sur les objets |
| EP0194148A2 (fr) * | 1985-03-06 | 1986-09-10 | Lockwood Graders (U.K.) Limited | Procédé et dispositif pour la détection de régions colorées et procédé et dispositif pour trier des objets de cette manière |
-
1989
- 1989-01-06 NL NL8900037A patent/NL8900037A/nl unknown
-
1990
- 1990-01-03 DE DE1990619001 patent/DE69019001T2/de not_active Expired - Lifetime
- 1990-01-03 ES ES90200013T patent/ES2075131T3/es not_active Expired - Lifetime
- 1990-01-03 EP EP19900200013 patent/EP0377478B1/fr not_active Expired - Lifetime
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2645343A (en) * | 1949-04-27 | 1953-07-14 | Kelling Nut Co | Photoelectric inspecting and sorting apparatus |
| GB1283902A (en) * | 1970-01-05 | 1972-08-02 | Gunsons Sortex Ltd | Optical unit for use in a light-sensitive sorting machine |
| US4235342A (en) * | 1978-05-05 | 1980-11-25 | Geosource Inc. | Sorting apparatus using programmable classifier |
| FR2430272A1 (fr) * | 1978-07-06 | 1980-02-01 | Blitz Electricite | Procede et dispositif pour la detection de corps etrangers dans un produit divise |
| EP0104369A2 (fr) * | 1982-08-30 | 1984-04-04 | Pietzsch Aktiengesellschaft | Dispositif et méthode pour la reconnaissance optique de graphismes plats sur les objets |
| EP0194148A2 (fr) * | 1985-03-06 | 1986-09-10 | Lockwood Graders (U.K.) Limited | Procédé et dispositif pour la détection de régions colorées et procédé et dispositif pour trier des objets de cette manière |
Cited By (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5315384A (en) * | 1990-10-30 | 1994-05-24 | Simco/Ramic Corporation | Color line scan video camera for inspection system |
| WO1992008322A1 (fr) * | 1990-10-30 | 1992-05-14 | Simco/Ramic Corporation | Camera video de balayage lineaire en couleurs pour un systeme de controle |
| EP0865833A3 (fr) * | 1997-03-19 | 1999-02-03 | Satake Usa Inc. | Arrière-plan réflecteur pour machine de tri |
| NL1024619C2 (nl) * | 2003-10-24 | 2005-04-27 | Staalkat Internat B V | Inrichting voor het inspecteren van objecten. |
| WO2005045406A1 (fr) * | 2003-10-24 | 2005-05-19 | Staalkat International B.V. | Dispositif de controle pour des objets presentant une surface spherique |
| US7474392B2 (en) | 2003-10-24 | 2009-01-06 | Staalkat International B.V. | Inspection device for objects with a spherical surface |
| US9492849B2 (en) | 2005-05-17 | 2016-11-15 | Visys Nv | Method for sorting products moving in a continuous stream on a chute |
| CN101968346A (zh) * | 2010-09-29 | 2011-02-09 | 中国烟草总公司郑州烟草研究院 | 一种烟叶叶片结构的表征方法 |
| CN102615047A (zh) * | 2012-04-26 | 2012-08-01 | 大树智能科技(南京)有限公司 | 烟把在线检测剔除装置 |
| CN103752532A (zh) * | 2014-01-14 | 2014-04-30 | 河南科技大学 | 一种由plc控制系统控制的转盘气吹式烟叶分拣系统 |
| CN103752532B (zh) * | 2014-01-14 | 2015-12-09 | 河南科技大学 | 一种由plc控制系统控制的转盘气吹式烟叶分拣系统 |
| CN104001677A (zh) * | 2014-05-06 | 2014-08-27 | 中国农业大学 | 一种采用电控自动分料的色选机 |
| WO2023198664A1 (fr) * | 2022-04-12 | 2023-10-19 | Omya International Ag | Échantillonneur de courroie automatisé permettant de trier des impuretés, procédé et utilisation |
Also Published As
| Publication number | Publication date |
|---|---|
| NL8900037A (nl) | 1990-08-01 |
| DE69019001T2 (de) | 1995-12-07 |
| ES2075131T3 (es) | 1995-10-01 |
| DE69019001D1 (de) | 1995-06-08 |
| EP0377478B1 (fr) | 1995-05-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0377478B1 (fr) | Appareil pour inspecter des matières en vrac | |
| EP0789633B1 (fr) | Appareil de tri | |
| US5318173A (en) | Hole sorting system and method | |
| US6078018A (en) | Sorting apparatus | |
| US4281933A (en) | Apparatus for sorting fruit according to color | |
| ES3004941T3 (en) | Apparatus for detecting matter | |
| Njoroge et al. | Automated fruit grading system using image processing | |
| JPH0321235B2 (fr) | ||
| JP2008541007A (ja) | 食品の異物検出装置 | |
| US4271967A (en) | System for sorting elongated members | |
| EP1676124A1 (fr) | Dispositif de controle pour des objets presentant une surface spherique | |
| JP7511225B2 (ja) | 農産物の選別装置 | |
| JP6346105B2 (ja) | 選別装置 | |
| EP0707192B1 (fr) | Procédé et dispositif pour mesurer des paramètres de forme d'objets | |
| JPH09178430A (ja) | カメラ式選品装置 | |
| US3917069A (en) | Article sorting equipment | |
| JP2006038751A (ja) | 容器充填口端縁の検査方法及び検査装置並びに充填装置 | |
| JP3184137B2 (ja) | 青果物の選別方法 | |
| KR101206964B1 (ko) | 농산물 검사장치 | |
| JP2019107611A (ja) | 枝豆選別機 | |
| JP2642107B2 (ja) | 青果物の自動等級判定方法と装置 | |
| JP7016160B2 (ja) | X線検査装置 | |
| JPH10160676A (ja) | 米粒検査装置 | |
| JPS6378013A (ja) | 農産物等の形状識別装置 | |
| CN218691647U (zh) | 三伤外观检测机 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB IT NL |
|
| 17P | Request for examination filed |
Effective date: 19910109 |
|
| 17Q | First examination report despatched |
Effective date: 19930303 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: HEUFT SYSTEMTECHNIK GMBH |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT NL |
|
| REF | Corresponds to: |
Ref document number: 69019001 Country of ref document: DE Date of ref document: 19950608 |
|
| ET | Fr: translation filed | ||
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2075131 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20090126 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20090129 Year of fee payment: 20 Ref country code: NL Payment date: 20090122 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20090123 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20090126 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20090120 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20100102 |
|
| NLV7 | Nl: ceased due to reaching the maximum lifetime of a patent |
Effective date: 20100103 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20100104 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20100104 Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20100102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20100103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20100103 |