EP0401124B1 - Verfahren und Vorrichtung zum Verbessern des Verleimens von Holzbrettern zum Herstellen von sogenannten "verleimten Schichthölzern" - Google Patents
Verfahren und Vorrichtung zum Verbessern des Verleimens von Holzbrettern zum Herstellen von sogenannten "verleimten Schichthölzern" Download PDFInfo
- Publication number
- EP0401124B1 EP0401124B1 EP19900401477 EP90401477A EP0401124B1 EP 0401124 B1 EP0401124 B1 EP 0401124B1 EP 19900401477 EP19900401477 EP 19900401477 EP 90401477 A EP90401477 A EP 90401477A EP 0401124 B1 EP0401124 B1 EP 0401124B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- plank
- adhesive
- edge
- board
- glue
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 10
- 238000004026 adhesive bonding Methods 0.000 title claims description 5
- 238000004519 manufacturing process Methods 0.000 title claims description 4
- 239000000853 adhesive Substances 0.000 claims description 12
- 230000001070 adhesive effect Effects 0.000 claims description 12
- 238000011084 recovery Methods 0.000 claims description 4
- 238000006073 displacement reaction Methods 0.000 claims description 2
- 238000010276 construction Methods 0.000 claims 1
- 239000003292 glue Substances 0.000 description 25
- 230000007547 defect Effects 0.000 description 7
- 239000011324 bead Substances 0.000 description 4
- 238000009434 installation Methods 0.000 description 4
- 230000000712 assembly Effects 0.000 description 3
- 238000000429 assembly Methods 0.000 description 3
- 238000000151 deposition Methods 0.000 description 2
- 239000000047 product Substances 0.000 description 2
- 238000003860 storage Methods 0.000 description 2
- 238000007796 conventional method Methods 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 238000001035 drying Methods 0.000 description 1
- 239000012467 final product Substances 0.000 description 1
- 235000000396 iron Nutrition 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27G—ACCESSORY MACHINES OR APPARATUS FOR WORKING WOOD OR SIMILAR MATERIALS; TOOLS FOR WORKING WOOD OR SIMILAR MATERIALS; SAFETY DEVICES FOR WOOD WORKING MACHINES OR TOOLS
- B27G11/00—Applying adhesives or glue to surfaces of wood to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27G—ACCESSORY MACHINES OR APPARATUS FOR WORKING WOOD OR SIMILAR MATERIALS; TOOLS FOR WORKING WOOD OR SIMILAR MATERIALS; SAFETY DEVICES FOR WOOD WORKING MACHINES OR TOOLS
- B27G1/00—Machines or devices for removing knots or other irregularities or for filling-up holes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27M—WORKING OF WOOD NOT PROVIDED FOR IN SUBCLASSES B27B - B27L; MANUFACTURE OF SPECIFIC WOODEN ARTICLES
- B27M3/00—Manufacture or reconditioning of specific semi-finished or finished articles
- B27M3/0013—Manufacture or reconditioning of specific semi-finished or finished articles of composite or compound articles
- B27M3/0026—Manufacture or reconditioning of specific semi-finished or finished articles of composite or compound articles characterised by oblong elements connected laterally
- B27M3/0053—Manufacture or reconditioning of specific semi-finished or finished articles of composite or compound articles characterised by oblong elements connected laterally using glue
Definitions
- the present invention relates to an improvement to the methods and devices for gluing wooden planks for the manufacture of assemblies called glulam.
- glue is deposited on the contact face of at least one of the two boards, preferably in the form of equidistant parallel threads, which are produced by jets which flow onto a board that scrolls below.
- the jets form a curtain of great width, greater than the width of the boards in movement, so that all the boards passing through the installation receive glue over their entire width, whatever it is.
- the glue which is poured outside the width of a moving board falls into a collecting tank placed below, from where it is returned to the installation pump.
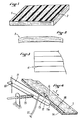
- FIG. 1 A board thus treated is then presented as shown in FIG. 1 where we see a board 1 furnished with glue threads 2. All this is fine as long as the boards are as expected, that is to say with a constant thickness and flat. However, it may happen that as a result of transport and storage time, the board has a defect and is deformed. It can curve and / or shrink at the edges as a result of dryness, as shown in section in 3 in FIG. 2. We then obtain glue-laminated assemblies whose edge has defects like defect 4 in Figure 3. When noticed, the entire assembly may be discarded.
- the present invention aims to avoid these drawbacks.
- the subject of the present invention is a method of gluing wooden planks for the manufacture of assemblies called glulam, in which the surface of the plank receives a layer of glue, characterized in that a a net of additional glue is placed on each side, a short distance from the side edge of the board.
- the glue layer can be deposited in the form of regularly spaced glue threads.
- the additional net may be larger than the others.
- the invention also relates to a device for the implementation of this method, comprising means for scrolling flat on a wooden board above a recovery tank and means for pouring onto the board, during its displacement, a layer of glue, in the form of a series of equidistant nets, said means being provided for pouring the glue over a width greater than that of the board so that the glue spilled outside the width of the board falls in the recovery tank, characterized in that it further comprises means adapted to follow at least one edge of the board for depositing glue in the region of said at least one edge.
- said means adapted to follow at least one edge of the board comprise a follower elastically urged against the edge of the board, so as to remain in contact with the edge whatever the width and the position of the board, pouring means being fixed to said follower for pouring a thread of glue at a determined distance from the end of said follower which is kept in contact with the edge of the board.
- the board 1 has been lined with glue threads 2.
- the installation comprises, in a known manner, a ramp discharging a curtain of glue threads, under which the flat board passes. It is thus furnished with a series of parallel longitudinal threads or cords, which allow gluing for assembly.
- the length of the ramp is at least equal to the largest planks to be treated. So in general, glue is poured on either side of the board and falls into a collecting container from where it is recycled.
- the boards can deform and have defects as in 3 in Figure 2: by drying, the marginal areas of the board can be thinner or deformed. It was found according to the invention that by putting an extra thickness of glue on the edges of the boards, the final product was correct and did not have the defect of small crevices as in 4 in FIG. 3.
- a bead of adhesive is deposited in the vicinity of the edge of the board, which may be thicker than the others.
- the device shown in Figure 4 allows to deposit a bead of glue near an edge of the board, at the distance you want, whatever the width of the board.
- a board 1 runs flat in the direction of arrow f in a machine not shown, to receive on its upper face a layer of glue, possibly in the form of equidistant parallel cords.
- a follower 11 comprising, in the vicinity of its other end 11a, a flat or rounded face 12 biased by a spring 13 against the lateral face 14 of the edge of the board 1.
- a tab or any support 15 is fixed to which is fixed a tube 16 of appropriate diameter and length, supplied with glue by a flexible 17, for depositing a net or bead of glue 18 on the edge of the board 1.
- the distance from the cord 18 to the edge 14 of the board does not depend on the width of the board, nor on its position in the machine. This distance is determined by the position of the tube 16 on the support 15. It can be fixed or adjustable.
- the hole of the tube 16 or the pressure of the adhesive can be adjustable to determine the thickness of the bead of adhesive.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Wood Science & Technology (AREA)
- Forests & Forestry (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
- Veneer Processing And Manufacture Of Plywood (AREA)
Claims (5)
- Verfahren zum Verleimen von Holzbrettern (1) zur Herstellung von sogenannten verleimten Schichthölzern, bei dem die Oberfläche des Bretts eine Leimschicht (2) erhält, dadurch gekennzeichnet, daß ein zusätzlicher Leimfaden (18) auf jeder Seite in einem geringen Abstand zum Seitenrand (14) des Bretts aufgebracht wird.
- Verfahren nach Anspruch 1, bei dem die Leimschicht in Form von gleichmäßig voneinander entfernten Leimfäden (2) aufgebracht wird.
- Verfahren nach Anspruch 2, bei dem der zusätzliche Leimfaden dicker ist als die anderen.
- Vorrichtung zur Anwendung des Verfahrens nach einem der Ansprüche 1 und 2, die Mittel, um ein Holzbrett (1) flach oberhalb eines Auffangbehälters vorbeizuführen, und Mittel aufweist, um auf das Brett während seiner Verschiebung eine Leimschicht in Form einer Reihe von gleich weit voneinander entfernten Fäden (2) zu gießen, wobei die Mittel vorgesehen sind, um den Leim auf eine Breite zu vergießen, die größer ist als die des Bretts, so daß der außerhalb der Breite des Bretts vergossene Leim in den Behälter fällt, dadurch gekennzeichnet, daß daß sie weiter Mittel (11) aufweist, die mindestens einem Rand (14) des Bretts folgen können, um Leim (18) in dem Bereich des mindestens einen Rands aufzubringen.
- Vorrichtung nach Anspruch 4, bei der die Mittel, die mindestens einem Rand des Bretts folgen können, einen Folger (11) aufweisen, der elastisch gegen den Rand (14) des Bretts gezogen wird, um mit dem Rand in Berührung zu bleiben, unabhängig von der Breite und der Stellung des Bretts, wobei Gießmittel (16) an diesem Folger befestigt sind, um einen Leimfaden (18) in einem vorbestimmten Abstand von dem Ende (11a) des Folgers zu vergießen, das mit dem Rand des Bretts in Berührung bleibt.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR8907351 | 1989-06-02 | ||
| FR8907351A FR2647703B1 (fr) | 1989-06-02 | 1989-06-02 | Procede et dispositif pour ameliorer l'encollage de planches de bois pour la fabrication d'assemblages dits lamelle-colle |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0401124A1 EP0401124A1 (de) | 1990-12-05 |
| EP0401124B1 true EP0401124B1 (de) | 1993-03-03 |
Family
ID=9382328
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19900401477 Expired - Lifetime EP0401124B1 (de) | 1989-06-02 | 1990-06-01 | Verfahren und Vorrichtung zum Verbessern des Verleimens von Holzbrettern zum Herstellen von sogenannten "verleimten Schichthölzern" |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0401124B1 (de) |
| DE (1) | DE69000989D1 (de) |
| FR (1) | FR2647703B1 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117428878B (zh) * | 2023-10-24 | 2026-05-01 | 中建八局科技建设有限公司 | 一种建筑垃圾回收利用再生产装置 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3071106A (en) * | 1960-12-13 | 1963-01-01 | Marlin L Burelbach | Plywood edge filler |
| US4056075A (en) * | 1976-01-12 | 1977-11-01 | Abe Seiderman | Automatic hot melt adhesive depositing machine |
| DE3013979A1 (de) * | 1979-07-11 | 1981-01-29 | Hauni Werke Koerber & Co Kg | Verfahren und vorrichtung zum auftragen von leim auf einen bewegten verbindungsstreifen fuer rauchartikel |
| SE442832B (sv) * | 1980-05-23 | 1986-02-03 | Bjorn Von Tell | Sett att fylla ut ytojemnheter i treprodukter med ridabeleggning |
| DE3337878A1 (de) * | 1983-10-18 | 1985-04-25 | Georg Börner Chemisches Werk für Dach- und Bautenschutz GmbH & Co KG, 6430 Bad Hersfeld | Auftragsgeraet fuer klebstoff |
| US4747899A (en) * | 1986-01-31 | 1988-05-31 | Meinan Machinery Works, Inc. | Method for improving the mechanical strength of veneer sheets having lathe checks |
| FR2616702B1 (fr) * | 1987-06-17 | 1992-05-15 | Gauthier Sa Paul | Procede et dispositif pour encoller des lames de bois |
-
1989
- 1989-06-02 FR FR8907351A patent/FR2647703B1/fr not_active Expired - Fee Related
-
1990
- 1990-06-01 EP EP19900401477 patent/EP0401124B1/de not_active Expired - Lifetime
- 1990-06-01 DE DE9090401477T patent/DE69000989D1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| EP0401124A1 (de) | 1990-12-05 |
| FR2647703A1 (fr) | 1990-12-07 |
| DE69000989D1 (de) | 1993-04-08 |
| FR2647703B1 (fr) | 1993-05-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1263666A1 (de) | Kurvenabschnitt eines förderers mit führungsbahnen mit regelbarer breite | |
| WO2019077277A1 (fr) | Bombage de verre par gravite entre squelette et contre-squelette | |
| BE1004127A3 (fr) | Procede et dispositif pour l'amenee de bouteilles ou recipients analogues. | |
| FR2527488A1 (fr) | Appareil de serrage de pieces a souder par un faisceau laser,tablette formee par soudage de pieces,et procede de fabrication d'une telle plaquette | |
| FR2640291A1 (fr) | Toile pour machine a papier | |
| EP1510316B1 (de) | Verfahren zum herstellen von platten aus hydraulischem bindemittel, fertigungsstrasse zur herstellung derartiger platten und vorrichtung zum prägen | |
| EP0401124A1 (de) | Verfahren und Vorrichtung zum Verbessern des Verleimens von Holzbrettern zum Herstellen von sogenannten "verleimten Schichthölzern" | |
| FR2565892A1 (fr) | Appareil pour l'application automatique sous pression de bandes de caoutchouc ou matiere de revetement similaire sur des surfaces etendues de parois | |
| FR2627785A1 (fr) | Dispositif pour le revetement d'une bande avec une composition de revetement | |
| BE1016021A3 (fr) | Plaques a base de liant hydraulique a bords amincis, procede de fabrication de plaques a base de liant hydraulique et ligne de production de telles plaques, et procede de construction de second oeuvre. | |
| FR2760245A1 (fr) | Dispositif sur une carde comportant un cylindre alimenteur et au moins un briseur | |
| EP3529187B1 (de) | Vorrichtung und verfahren zur umlenkung und abtastung von zuschnitten | |
| FR2549809A3 (fr) | Dispositif transporteur angulaire a bandes pour articles de patisserie | |
| WO2004009309A2 (fr) | Procede de fabrication de plaques a bords amincis, a base de liants hydrauliques, ligne et dispositif pour la production de telles plaques | |
| FR2518928A1 (fr) | Dispositif de fabrication de sachets en matiere plastique | |
| EP1361030B1 (de) | Verfahren zum Herstellen von Platten aus hydraulischem Bindemittel sowie Fertigungsstrasse zur Herstellung derartiger Platten | |
| FR2740762A1 (fr) | Dispositif d'empilement de produits en forme de cartes | |
| FR2553074A1 (fr) | Dispositif de pliage multiple et de consolidation de lisieres de nappes continues ou de pieces de tissu decoupees dans celles-ci | |
| FR2534839A1 (fr) | Machine automatique a ebavurer des pieces de petites dimensions | |
| BE883828A (fr) | Procede de fabrication de sacs, machine pour la mise en oeuvre de ce procede et sacs obtenus. | |
| FR2559752A1 (fr) | Procede de fabrication d'une ebauche de matelas, et installation pour la mise en oeuvre de ce procede | |
| FR2734806A1 (fr) | Came de commande pour carrousel de conditionnement, et machine de conditionnement correspondante. | |
| FR2796929A1 (fr) | Procede et installation pour rabouter les extremites de materiaux en bandes, articles textiles notamment | |
| BE1005277A0 (fr) | Dispositif de mise en pile verticale de plaques, notamment de plaques de verre. | |
| EP0052057B1 (de) | Verfahren und Vorrichtung zum Überziehen einer Ladung mit einer Schlauchfolie |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE DE DK IT |
|
| 17P | Request for examination filed |
Effective date: 19910522 |
|
| 17Q | First examination report despatched |
Effective date: 19911223 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE DE DK IT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRE;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED.SCRIBED TIME-LIMIT Effective date: 19930303 Ref country code: DK Effective date: 19930303 Ref country code: DE Effective date: 19930303 |
|
| REF | Corresponds to: |
Ref document number: 69000989 Country of ref document: DE Date of ref document: 19930408 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 19960717 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Effective date: 19970630 |
|
| BERE | Be: lapsed |
Owner name: S.A. PAUL GAUTHIER Effective date: 19970630 |