EP0406249B1 - Installation pour la fabrication de rubans d'acier lamines a chaud - Google Patents
Installation pour la fabrication de rubans d'acier lamines a chaud Download PDFInfo
- Publication number
- EP0406249B1 EP0406249B1 EP89902023A EP89902023A EP0406249B1 EP 0406249 B1 EP0406249 B1 EP 0406249B1 EP 89902023 A EP89902023 A EP 89902023A EP 89902023 A EP89902023 A EP 89902023A EP 0406249 B1 EP0406249 B1 EP 0406249B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- winding
- installation
- rolled steel
- steel strip
- transport means
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/46—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling metal immediately subsequent to continuous casting
- B21B1/466—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling metal immediately subsequent to continuous casting in a non-continuous process, i.e. the cast being cut before rolling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/24—Transferring coils to or from winding apparatus or to or from operative position therein; Preventing uncoiling during transfer
- B21C47/245—Devices for the replacement of full reels by empty reels or vice versa, without considerable loss of time
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/52—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for wires; for strips ; for rods of unlimited length
- C21D9/54—Furnaces for treating strips or wire
- C21D9/68—Furnace coilers; Hot coilers
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F27—FURNACES; KILNS; OVENS; RETORTS
- F27B—FURNACES, KILNS, OVENS OR RETORTS IN GENERAL; OPEN SINTERING OR LIKE APPARATUS
- F27B19/00—Combinations of different kinds of furnaces that are not all covered by any single one of main groups F27B1/00 - F27B17/00
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/22—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length
- B21B1/24—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length in a continuous or semi-continuous process
- B21B1/26—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length in a continuous or semi-continuous process by hot-rolling, e.g. Steckel hot mill
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/22—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length
- B21B1/30—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length in a non-continuous process
- B21B1/32—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length in a non-continuous process in reversing single stand mills, e.g. with intermediate storage reels for accumulating work
- B21B1/34—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling plates, strips, bands or sheets of indefinite length in a non-continuous process in reversing single stand mills, e.g. with intermediate storage reels for accumulating work by hot-rolling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B15/00—Arrangements for performing additional metal-working operations specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B2015/0057—Coiling the rolled product
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/004—Heating the product
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/04—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for de-scaling, e.g. by brushing
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/4998—Combined manufacture including applying or shaping of fluent material
- Y10T29/49988—Metal casting
- Y10T29/49991—Combined with rolling
Definitions
- the invention relates to a system for producing hot-rolled steel strip from a continuously cast starting material, in which the cast strand is wound up into a bundle in a reel station after leaving the continuous casting system and is reeled off in a further coiler station after the bundle has been moved, and the reel stations are fed in are arranged in a common oven.
- Such systems are known. They have the advantage that continuously produced hot-rolled strip from a continuously cast starting material is inexpensive because a considerable saving in energy is made possible solely by the fact that the facilities necessary for reheating the slabs, intermediate transport devices and storage spaces are not required in conventional processes and systems.
- the cast strand which has already been cast in the form of a strip makes it unnecessary to reduce the cross section with a high degree of deformation effort and high deformation energy and permits coils to be wound up immediately behind the continuous casting installation. This winding or reeling is necessary because the maximum casting speed at which the cast strand leaves the continuous caster is much lower than the lowest possible rolling speed of conventional roll stands.
- the object of the present invention is to improve the arrangement of the reel stations within the furnace in such a way that unproblematic reeling and unwinding of the cast strip and, if appropriate, intermediate storage is possible and the implementation of the federal government is simplified.
- winding mandrels circulate in the case of the invention, so that tape can also be wound and converted so that winding cannot be carried out on mandrelless winding devices.
- the winding mandrels are driven independently of one another and the drives which are fixed relative to the orbit of the winding mandrels are detachably coupled to the winding mandrels. This is recommended because the winding mandrels have to work with different drive speeds due to the different speeds for reeling and unwinding. If necessary, the winding mandrels can be brought into the respective winding position step by step and can be coupled there to the drives.
- a further feature of the invention provides that a device for controlled heating of the cast strand to the reel or the rolling temperature is arranged in front of and / or behind the furnace. Such devices can of course be omitted if the temperature of the furnace allows rolling without reheating or the temperature of the greeting line corresponds to the reel temperature.
- cross winding shears and / or devices for descaling be arranged downstream of the winding mandrels in a manner known per se.
- the cross-cut shear is required when the cast strand weight is greater than the coil weight of the coil located in the take-up reel station.
- Descaling equipment is usually required behind the furnace to prevent the scale from rolling into the mill.
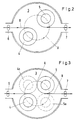
- Fig. 1 the continuous casting system is indicated at 1.
- the cast strand B passes through a pair of scissors at 2 before it is introduced into the furnace 3 with the aid of the driver 6 and wound up on the mandrel 4.
- the winding mandrel 4 can be moved on the circular orbit U shown in dashed lines in the direction of the arrow into a position in which the winding mandrel 5 is drawn in FIG. 2.
- the cast strand B is unwound from the winding mandrel 5 with the aid of the driving apparatus 7 and is fed to the rolling mill 10 through the heating device 8, the cast strand B having previously passed through the descaling device 9.
- a cooling section is indicated at 11, in which the strip is cooled before it is wound up at 12.
- FIG. 3 shows an alternative in which four mandrels 4, 4a, 5, 5b are arranged so as to be movable on the orbit U.
- the winding mandrels have the same spacing from one another and allow intermediate storage of wound bundles in the stations 4a and 5a.
- the device for heating the cast strand can also be located between continuous casting installation 1 and furnace 3; it can also be a special device only for heating the strip edges.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- General Engineering & Computer Science (AREA)
- Metal Rolling (AREA)
- Winding, Rewinding, Material Storage Devices (AREA)
Abstract
Claims (6)
caractérisée en ce que
les moyens de transport (4,5) pour les bobines sont déplaçables pas à pas sur un circuit fermé s'étendant dans un plan vertical,
en ce que, à l'aide des moyens de transport, plus de deux bobines (4,5) sont déplaçables en même temps sur le circuit (U), et en ce que chaque moyen de transport (4,5) est un mandrin de bobinage entraînable au moins dans les positions d'enroulement et de déroulement.
caractérisée en ce que
les moyens de transport (4,5) sont déplaçables sur une trajectoire circulaire.
caractérisée en ce que
les tubes enroulés peuvent être entraînés indépendamment l'un de l'autre par l'intermédiaire d'entraînements fixes par rapport au circuit (U) des dispositifs d'enroulement (4,5), qui sont couplés de façon amovible aux mandrins de bobinage.
caractérisée en ce que,
devant et/ou derrière le four (3), est agencé un dispositif (8) pour réchauffer, de façon commandée, la barre de coulée (B) à la température d'enroulement ou de laminage.
caractérisée en ce que
les moyens de transport (4,5) sont agencés dans le four de bobinage, du côté d'entrée, d'un laminoir Steckel.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT89902023T ATE78727T1 (de) | 1988-03-17 | 1989-02-06 | Anlage zum herstellen von warmgewalztem stahlband. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3809681 | 1988-03-17 | ||
| DE19883809681 DE3809681C1 (en) | 1987-12-31 | 1988-03-17 | Plant for the production of hot-rolled steel |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0406249A1 EP0406249A1 (fr) | 1991-01-09 |
| EP0406249B1 true EP0406249B1 (fr) | 1992-07-29 |
Family
ID=6350414
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89902023A Expired - Lifetime EP0406249B1 (fr) | 1988-03-17 | 1989-02-06 | Installation pour la fabrication de rubans d'acier lamines a chaud |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US5335713A (fr) |
| EP (1) | EP0406249B1 (fr) |
| CA (1) | CA1322480C (fr) |
| DE (1) | DE58901955D1 (fr) |
| ES (1) | ES2015140A6 (fr) |
| WO (1) | WO1989008512A1 (fr) |
Families Citing this family (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3821188A1 (de) * | 1988-06-23 | 1989-12-28 | Schloemann Siemag Ag | Bandgiessanlage mit drehherdofen |
| US5437089A (en) * | 1991-04-17 | 1995-08-01 | Magnitogorsky Metallurgichesky Kombinat Imeni V.I. Lenina | Method and apparatus for continuous production hot-rolled strips |
| IT1260566B (it) * | 1992-06-30 | 1996-04-16 | Danieli Off Mecc | Gruppo avvolgitore-svolgitore per bramme sottili |
| JP3063518B2 (ja) * | 1993-12-27 | 2000-07-12 | 株式会社日立製作所 | 連続鋳造装置及び連続鋳造システム |
| JPH11342402A (ja) * | 1998-05-29 | 1999-12-14 | Kawasaki Steel Corp | 冷間圧延設備 |
| US5956990A (en) * | 1998-08-14 | 1999-09-28 | Danieli United | Apparatus and method for producing and handling superlarge coils of metal strip |
| AT407613B (de) | 1999-03-03 | 2001-05-25 | Voest Alpine Ind Anlagen | Vorrichtung zum endloswickeln von bandmaterial |
| DE10045085C2 (de) * | 2000-09-12 | 2002-07-18 | Siemens Ag | Gießwalzanlage |
| DE10109223C1 (de) | 2001-02-26 | 2002-08-01 | Siemens Ag | Verfahren zum Betreiben einer Gießwalzanlage |
| DE10300362A1 (de) * | 2003-01-06 | 2004-07-22 | Sms Demag Ag | Verfahren und Anlage zum Walzen und anschließendem Haspeln von Metallband, insbesondere von Stahlband |
| US7823431B2 (en) * | 2003-06-13 | 2010-11-02 | Siemens Industry, Inc. | Method and apparatus for temporarily interrupting the passage of long products between upstream and downstream paths in a rolling mill |
| CA2841620C (fr) * | 2004-10-28 | 2016-09-27 | U.S. Manufacturing Corporation | Procede de fabrication d'ensemble trompette tubulaire a paroi d'epaisseur variable |
| IT1397452B1 (it) * | 2009-12-30 | 2013-01-10 | Danieli E C Ohg S P A | Dispositivo e procedimento per avvolgere/svolgere un prodotto metallico in una linea di laminazione |
| KR101726759B1 (ko) * | 2010-11-05 | 2017-04-13 | 주식회사 포스코 | 설비의 교체 및 수리가 용이한 멘드럴 코일박스 |
| CN103894416B (zh) * | 2012-12-26 | 2016-10-19 | Posco公司 | 心轴卷材箱的运行方法、利用其的连续轧制方法和连续轧制装置 |
| DE102013224633A1 (de) * | 2013-01-14 | 2014-07-17 | Sms Siemag Ag | Gieß-Walzanlage sowie Verfahren zum Aus- und Einbau von Walzen in einem Reduziergerüst der Gieß-Walzanlage |
| IT201700028768A1 (it) * | 2017-03-15 | 2018-09-15 | Danieli Off Mecc | Impianto combinato di colata continua e laminazione di nastri metallici a caldo |
| IT201700028732A1 (it) * | 2017-03-15 | 2018-09-15 | Danieli Off Mecc | Impianto combinato di colata continua e laminazione di nastri metallici a caldo |
| CN117358774A (zh) * | 2023-09-19 | 2024-01-09 | 广西北港不锈钢有限公司 | 一种退火酸洗线上料用不锈钢黑皮卷热送热开系统及方法 |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2327906A (en) * | 1941-04-02 | 1943-08-24 | Streine Tool And Mfg Company | Strip coil handling |
| BE482884A (fr) * | 1947-06-05 | |||
| DE972603C (de) * | 1950-08-03 | 1959-09-10 | Kocks Gmbh Friedrich | Kontinuierlich arbeitende Walzenstrasse zum Warmwalzen von Breitband |
| FR1308895A (fr) * | 1961-12-19 | 1962-11-09 | Verwaltungs Ges Moeller & Neum | Laminoir pour tôle épaisse avec train de finissage continu |
| DE1954675C3 (de) * | 1969-10-30 | 1975-07-17 | Josef 4220 Dinslaken Schmitz | Abrollvorrichtung für Wickel aus Bandeisen, Drähten od.dgl |
| US4123011A (en) * | 1975-02-19 | 1978-10-31 | Hitachi, Ltd. | Coil unwind and wind-up method and apparatus therefor |
| JPS57121809A (en) * | 1981-01-22 | 1982-07-29 | Nippon Steel Corp | Production of steel material by direct rolling |
| DE3241745C2 (de) * | 1982-11-11 | 1985-08-08 | Mannesmann AG, 4000 Düsseldorf | Verfahren zum Herstellen von warmgewalztem Stahlband aus stranggegossenem Vormaterial in unmittelbar aufeinanderfolgenden Arbeitsschritten |
| US4630352A (en) * | 1984-09-04 | 1986-12-23 | Tippins Machinery Company, Inc. | Continuous rolling method and apparatus |
| DE3538677A1 (de) * | 1985-10-31 | 1987-05-07 | Schloemann Siemag Ag | Wendehaspel |
| JPS62127145A (ja) * | 1985-11-29 | 1987-06-09 | Kawasaki Steel Corp | 急冷薄帯巻取り方法及び装置 |
| DE3637893C2 (de) * | 1986-11-06 | 1996-02-08 | Schloemann Siemag Ag | Verfahren und Anlage zur Herstellung von warmgewalztem Stahlband und Bandgießanlage |
-
1989
- 1989-02-06 DE DE8989902023T patent/DE58901955D1/de not_active Expired - Fee Related
- 1989-02-06 WO PCT/DE1989/000076 patent/WO1989008512A1/fr not_active Ceased
- 1989-02-06 EP EP89902023A patent/EP0406249B1/fr not_active Expired - Lifetime
- 1989-03-08 ES ES8900830A patent/ES2015140A6/es not_active Expired - Lifetime
- 1989-03-16 CA CA000593959A patent/CA1322480C/fr not_active Expired - Fee Related
-
1990
- 1990-09-14 US US07/582,497 patent/US5335713A/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| WO1989008512A1 (fr) | 1989-09-21 |
| CA1322480C (fr) | 1993-09-28 |
| EP0406249A1 (fr) | 1991-01-09 |
| DE58901955D1 (de) | 1992-09-03 |
| US5335713A (en) | 1994-08-09 |
| ES2015140A6 (es) | 1990-08-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3241745C2 (de) | Verfahren zum Herstellen von warmgewalztem Stahlband aus stranggegossenem Vormaterial in unmittelbar aufeinanderfolgenden Arbeitsschritten | |
| EP1148956B1 (fr) | Procede de travail et installation pour le decapage et le laminage a froid souple et economique de feuillards metalliques | |
| EP0415987B1 (fr) | Procede pour produire en continu du feuillard d'acier ou de la tole d'acier a partir de produits plats fabriques selon le procede de coulee continue en arc | |
| WO1989008512A1 (fr) | Installation pour la fabrication de rubans d'acier lamines a chaud | |
| EP0368048B1 (fr) | Procédé et dispositif de fabrication de bandes d'acier laminées à chaud | |
| DE2256024A1 (de) | Verfahren zum walzen von heissen metallwerkstuecken | |
| EP0595282B2 (fr) | Procédé et installation pour la fabrication de bandes d'acier laminées à chaud, en particulier à partir d'une ébauche de bande coulée en continu | |
| DE69330683T2 (de) | Verfahren zum Entzundern und Kaltwalzen von Metallband | |
| EP2244851B1 (fr) | Installation de laminage pour le laminage de produits à laminer sous forme de feuillard | |
| EP0933147B1 (fr) | Procédé et dispositif de transfert de bobines | |
| DE69909332T2 (de) | Integriertes kontinuierliches stranggiess- und inline warmwalzverfahren sowie entsprechendes verfahren mit zwischenwickeln und abwickeln des vorstreifens | |
| DE3743057C1 (de) | Verfahren und Anlage zum Herstellen von warmgewalztem Band aus stranggegossenem Vormaterial | |
| EP0425715A1 (fr) | Accumulateur de bandes | |
| EP0823294A1 (fr) | Procédé de fabrication d'une bande en acier basse et ultra basse de teneur en carbon | |
| AT511657B1 (de) | Inbetriebnahme einer fertigwalzstrasse in einer giess-walz-verbundanlage | |
| DE3809681C1 (en) | Plant for the production of hot-rolled steel | |
| DE3030382A1 (de) | Verfahren und einrichtung zum heisswalzen von metallwerkstuecken zu baendern oder platten | |
| EP1641573A2 (fr) | Dispositif pour la production de feuillard d'acier lamine a chaud, en particulier a partir d'ebauche en bande coulee en continu | |
| DE2613459A1 (de) | Verfahren und anlage zur vermeidung des schrottanfalles in kontinuierlichen breitbandstrassen | |
| AT511674B1 (de) | Inbetriebnahme einer fertigwalzstrasse in einer giess-walz-verbundanlage | |
| DE3714432C2 (de) | Verfahren und Anlage zur Herstellung von warmgewalztem Stahlband | |
| DE2600784C3 (de) | Verfahren zum Walzen von Warmband und Warmbandwalzwerk zur Durchführung des Verfahrens | |
| EP0701873B1 (fr) | Installation de four comme emmagasinage temporaire, derrière un dispositif de coulée pour brames minces | |
| EP0879100B1 (fr) | Procede et dispositif pour le laminage reversible de feuillards metalliques | |
| DE4344094C1 (de) | Zweistrangige Dünnbrammengießanlage mit Aufwickelvorrichtung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19900816 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| 17Q | First examination report despatched |
Effective date: 19910926 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE FR GB IT LI LU NL SE |
|
| REF | Corresponds to: |
Ref document number: 78727 Country of ref document: AT Date of ref document: 19920815 Kind code of ref document: T |
|
| ET | Fr: translation filed | ||
| REF | Corresponds to: |
Ref document number: 58901955 Country of ref document: DE Date of ref document: 19920903 |
|
| ITF | It: translation for a ep patent filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| EPTA | Lu: last paid annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19950116 Year of fee payment: 7 |
|
| EAL | Se: european patent in force in sweden |
Ref document number: 89902023.4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19950228 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19960228 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19960228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19960901 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 19960901 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20020115 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20020128 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20020129 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20020204 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20020207 Year of fee payment: 14 Ref country code: FR Payment date: 20020207 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20020227 Year of fee payment: 14 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030206 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030206 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030206 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030902 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| EUG | Se: european patent has lapsed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20031031 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050206 |