EP0467807A1 - Verfahren und Vorrichtung zur Dickenkontrolle dünner Stranggussbänder auselektrisch leitendem Material - Google Patents
Verfahren und Vorrichtung zur Dickenkontrolle dünner Stranggussbänder auselektrisch leitendem Material Download PDFInfo
- Publication number
- EP0467807A1 EP0467807A1 EP91420253A EP91420253A EP0467807A1 EP 0467807 A1 EP0467807 A1 EP 0467807A1 EP 91420253 A EP91420253 A EP 91420253A EP 91420253 A EP91420253 A EP 91420253A EP 0467807 A1 EP0467807 A1 EP 0467807A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cylinder
- injector
- inductor
- liquid
- magnetic field
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/16—Controlling or regulating processes or operations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/06—Continuous casting of metals, i.e. casting in indefinite lengths into moulds with travelling walls, e.g. with rolls, plates, belts, caterpillars
- B22D11/0611—Continuous casting of metals, i.e. casting in indefinite lengths into moulds with travelling walls, e.g. with rolls, plates, belts, caterpillars formed by a single casting wheel, e.g. for casting amorphous metal strips or wires
Definitions
- the present invention relates to a method and to a device for controlling the thickness in continuous casting of a thin strip formed by an electrically conductive material such as in particular a metal or a metal alloy.
- the liquid material solidifies in the form of a thin layer which adheres slightly to the substrate formed by the surface of the cylinder and entails via the meniscus an additional fraction of liquid material so that one obtains a continuous strip.
- the thickness of the strip produced in this way depends on the speed of rotation of the cylinder, the height of the molten material in the opening of the injector as well as the heat transfer characteristics of the cylinder.
- the strip produced according to this process has variations in thickness both in the longitudinal direction and in the transverse direction, which makes it difficult to use either directly or after having undergone mechanical treatments and / or thermal.
- the fact that the thickness of the cast strip is not uniform longitudinally can be attributed to two causes.
- this introduction is not continuous due to the response time of the measurement and regulation systems.
- disturbances which are reflected on the one hand by a variation in the height of the material in the injector and on the other hand by the formation of waves at the surface and coming from the place where the liquid material is introduced into the injector.
- the second cause is attributed to the rotation of the cylinder and the extraction of the solidified strip which also cause disturbances in the free surface of the material leading to the formation of waves at the meniscus.
- any temporal or spatial variation in the level of the liquid will cause defects in the morphology of the strip and in particular in its thickness; a temporal perturbation leading rather to longitudinal defects and a spatial perturbation to transverse defects.
- the invention consisting of a method for controlling the thickness in continuous casting of thin strip of electroconductive material obtained by bringing said material in liquid state into contact with the cooled side wall of a rotating cylinder on which it solidifies, the said material being supplied via an injector, the end of which opens along the generatrix of the cylinder so that its free surface touches the said wall, characterized in that the surface of the material placed in the injector by the action of a magnetic field alternating current created by a single-phase electric current.
- R ⁇ ⁇ L2
- ⁇ the electrical conductivity
- ⁇ the pulsation of the magnetic field
- L the height of liquid in the injector.
- the optimum stirring is obtained for a value of R ⁇ close to 40 and the optimum heating for a value close to 20. Stabilization and control of the shape of the surface are obtained for an R ⁇ value greater than 200.
- This process applies to any electroconductive material and especially ferrous or non-ferrous metals and their alloys.
- the invention also relates to a device for implementing the method according to the invention.
- This device consists of a circuit comprising a single-phase alternating current generator, at least one capacitor and at least one inductor characterized in that the said inductor is formed from at least one hollow metallic element, cooled, placed above the surface liquid material contained in the injector and extending parallel to the generator of the cylinder and over at least its entire length.
- the device according to the invention consists of a circuit in which are electrically connected a generator which creates a single-phase alternating current; at least one capacitor and one inductor so as to form an oscillating circuit.
- the frequency is fixed by the choice of the capacity of the capacitor (s). This frequency is determined according to the desired effects: pressure, mixing and heating.
- the inductor is formed from at least one hollow and cooled element, such as, for example, a copper tube inside which circulates cooling water.
- the internal diameter of this tube is chosen so that the water temperature does not exceed 70 ° C whatever the Joule effect resulting from the flow of current.
- the thickness of the tube is greater than the thickness of the electromagnetic skin, that is to say the thickness along which the current is distributed in the tube.
- This inductor is placed above the surface of the liquid metal contained in the injector and parallel to the generator of the cylinder and at a short distance, that is to say, for example, less than 1 cm so that the magnetic field created by the inductor is exerted with maximum efficiency depending on the desired shape and the desired suppression of ripples.
- the inductor preferably has a length greater than that of the width of the opening of the injector.
- the inductor is formed either of one or more elements linked together.
- said elements can be located either in the same plane or in different planes, at least one of which is placed above the surface of the liquid material placed in the injector; these planes are either parallel or oblique with respect to said surface, the inclination being chosen as a function of the desired shape and the desired suppression of the undulations.
- these elements are either rectilinear or have a curvature over their entire length or over a portion of said length, this curvature being situated in a plane parallel to the generator of the cylinder and directed upwards and / or downwards.
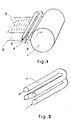
- FIG. 1 there is a casting cylinder 1, the free surface 2 of a bath of liquid metal contained in an injector 3 and an inductor 4 formed of two tubular elements assembled in a U and at l inside of which water circulates in the direction of arrows 5 and 6.
- the inductor is composed of three elements 8 which are parallel to each other, located in the same plane and connected together at a point 9.
- An inductor having the configuration of FIG. 1 was constructed from a copper tube with an outside diameter of 6 mm and an inside diameter of 4 mm. These elements, the distance between axes of which is 9 mm, are placed at a distance of 5 mm above the surface of an aluminum alloy bath and parallel to the axis of the cylinder, the nearest element having its axis located at a distance of 4.5mm from the surface of the cylinder along a radius. As soon as a single-phase electric current of intensity 250 A and frequency 170 kHz was passed through the inductor, the free surface of the metal presented during casting a hollow of maximum amplitude 6 mm, ie a reduction in the 3.5mm liquid height at the meniscus and was free of any disturbance.
- the same inductor was used under the same conditions for the casting of an austenitic stainless steel containing by weight: chromium 18%, nickel 10%, carbon ⁇ 0.08%. Under these conditions, there was a reduction in the height of liquid by 2.5 mm at the meniscus and the surface was free of any disturbance.
- Example 2 An inductor identical to that of Example 1 is positioned along a plane inclined at 40 degrees relative to the horizontal plane and placed above the surface of liquid metal constituted by an aluminum alloy and contained in the injector of a casting machine so that the axis of the lowest element is 4 mm from the surface and that of the highest element is 4.5 mm from the surface of the cylinder.
- a single-phase current of frequency 80 kHz and intensity 250 A was passed through this inductor, it was also noted the presence of a trough of amplitude 6 mm on the surface of the metal and the absence of any disturbance.
- An inductor with a configuration similar to that of FIG. 4 was implemented, made from copper tube of the same dimensions as that of Example 1.
- the plane 11 was placed parallel to the surface of liquid metal constituted by an aluminum alloy and contained in the injector of a casting machine and at a distance of 5 mm while the axis of the element arranged most high in plane 10 was 4.5 mm from the surface of the cylinder.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Continuous Casting (AREA)
- Coils Or Transformers For Communication (AREA)
- Acyclic And Carbocyclic Compounds In Medicinal Compositions (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9009708 | 1990-07-16 | ||
| FR9009708A FR2664513A1 (fr) | 1990-07-16 | 1990-07-16 | Procede et dispositif de controle de l'epaisseur en coulee continue de bande mince de materiau electroconducteur. |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0467807A1 true EP0467807A1 (de) | 1992-01-22 |
Family
ID=9399232
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP91420253A Ceased EP0467807A1 (de) | 1990-07-16 | 1991-07-15 | Verfahren und Vorrichtung zur Dickenkontrolle dünner Stranggussbänder auselektrisch leitendem Material |
Country Status (13)
| Country | Link |
|---|---|
| US (1) | US5184666A (de) |
| EP (1) | EP0467807A1 (de) |
| JP (1) | JPH04231148A (de) |
| KR (1) | KR920002255A (de) |
| AU (1) | AU639808B2 (de) |
| CA (1) | CA2047060A1 (de) |
| FI (1) | FI913401A7 (de) |
| FR (1) | FR2664513A1 (de) |
| IE (1) | IE912460A1 (de) |
| NO (1) | NO912594L (de) |
| NZ (1) | NZ238947A (de) |
| PT (1) | PT98328A (de) |
| ZA (1) | ZA915552B (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5253699A (en) * | 1991-07-31 | 1993-10-19 | Pechiney Recherche | Process for improving the surface condition and thickness regularity of a cast metal strip |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5535812A (en) * | 1995-01-06 | 1996-07-16 | Singleton Technology, Inc. | Method of and apparatus for continuous casting of metal |
| CH695090A5 (de) * | 2001-09-18 | 2005-12-15 | Main Man Inspiration Ag | Verfahren sowie eine Vorrichtung zur Herstellung eines Metallbandes an einer Rollen-Bandgiessmaschine. |
| CN104646643B (zh) * | 2015-02-15 | 2016-12-07 | 东北大学 | 一种直接约束控制导电金属流体液面波动的电磁控制方法 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0174765A2 (de) * | 1984-09-13 | 1986-03-19 | Allegheny Ludlum Corporation | Verfahren und Einrichtung zum Stranggiessen von kristallinen Bändern |
| WO1987002285A1 (en) * | 1985-10-11 | 1987-04-23 | National Aluminum Corporation | Method of and apparatus for continuous casting of metal strip |
| US4771819A (en) * | 1985-04-12 | 1988-09-20 | Nippon Metal Industry Co., Ltd. | Manufacturing apparatus for sheet metal according to continuous casting |
| US4842042A (en) * | 1988-03-07 | 1989-06-27 | Battelle Development Corporation | Thickness control of direct cast strip |
| WO1989007025A1 (en) * | 1988-02-05 | 1989-08-10 | National Aluminum Corporation | Apparatus for and process of direct casting of metal strip |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS59156558A (ja) * | 1983-02-25 | 1984-09-05 | Sumitomo Metal Ind Ltd | 連続鋳造鋳片の凝固殻厚み測定方法 |
| FR2570304B1 (fr) * | 1984-09-19 | 1986-11-14 | Cegedur | Procede de reglage du niveau de la ligne de contact de la surface libre du metal avec la lingotiere dans une coulee verticale |
| JPS61137658A (ja) * | 1984-12-10 | 1986-06-25 | Kawasaki Steel Corp | 急冷薄帯の板厚推定方法 |
| US4751957A (en) * | 1986-03-11 | 1988-06-21 | National Aluminum Corporation | Method of and apparatus for continuous casting of metal strip |
| USH892H (en) * | 1989-10-12 | 1991-03-05 | The United States Of America As Represented By The United States Department Of Energy | Thin sheet casting with electromagnetic pressurization |
| JP2594010B2 (ja) * | 1992-10-22 | 1997-03-26 | 日本無線株式会社 | カラープロッタ |
-
1990
- 1990-07-16 FR FR9009708A patent/FR2664513A1/fr active Pending
-
1991
- 1991-06-25 US US07/720,707 patent/US5184666A/en not_active Expired - Fee Related
- 1991-07-02 NO NO91912594A patent/NO912594L/no unknown
- 1991-07-04 AU AU80197/91A patent/AU639808B2/en not_active Ceased
- 1991-07-08 JP JP3166872A patent/JPH04231148A/ja active Pending
- 1991-07-12 NZ NZ238947A patent/NZ238947A/xx unknown
- 1991-07-15 FI FI913401A patent/FI913401A7/fi not_active Application Discontinuation
- 1991-07-15 KR KR1019910011997A patent/KR920002255A/ko not_active Ceased
- 1991-07-15 PT PT98328A patent/PT98328A/pt not_active Application Discontinuation
- 1991-07-15 IE IE246091A patent/IE912460A1/en unknown
- 1991-07-15 CA CA002047060A patent/CA2047060A1/fr not_active Abandoned
- 1991-07-15 EP EP91420253A patent/EP0467807A1/de not_active Ceased
- 1991-07-16 ZA ZA915552A patent/ZA915552B/xx unknown
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0174765A2 (de) * | 1984-09-13 | 1986-03-19 | Allegheny Ludlum Corporation | Verfahren und Einrichtung zum Stranggiessen von kristallinen Bändern |
| US4771819A (en) * | 1985-04-12 | 1988-09-20 | Nippon Metal Industry Co., Ltd. | Manufacturing apparatus for sheet metal according to continuous casting |
| WO1987002285A1 (en) * | 1985-10-11 | 1987-04-23 | National Aluminum Corporation | Method of and apparatus for continuous casting of metal strip |
| WO1989007025A1 (en) * | 1988-02-05 | 1989-08-10 | National Aluminum Corporation | Apparatus for and process of direct casting of metal strip |
| US4842042A (en) * | 1988-03-07 | 1989-06-27 | Battelle Development Corporation | Thickness control of direct cast strip |
Non-Patent Citations (3)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 10, no. 261 (M-514)(2317), 5 septembre 1986; & JP - A - 6186058 (KAWASAKI STEEL) 01.05.1986 * |
| PATENT ABSTRACTS OF JAPAN vol. 10, no. 333 (M-534)(2389), 12 novembre 1986; & JP - A - 61137658 (KAWASAKI STEEL) 25.06.1986 * |
| PATENT ABSTRACTS OF JAPAN vol. 9, no. 7 (M-350)(1730), 12 janvier 1985; & JP - A - 59156558 (SUMITOMO) 05.09.1984 * |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5253699A (en) * | 1991-07-31 | 1993-10-19 | Pechiney Recherche | Process for improving the surface condition and thickness regularity of a cast metal strip |
Also Published As
| Publication number | Publication date |
|---|---|
| NO912594D0 (no) | 1991-07-02 |
| FI913401A0 (fi) | 1991-07-15 |
| NZ238947A (en) | 1992-12-23 |
| CA2047060A1 (fr) | 1992-01-17 |
| IE912460A1 (en) | 1992-01-29 |
| US5184666A (en) | 1993-02-09 |
| PT98328A (pt) | 1993-07-30 |
| FI913401L (fi) | 1992-01-17 |
| NO912594L (no) | 1992-01-17 |
| FR2664513A1 (fr) | 1992-01-17 |
| AU639808B2 (en) | 1993-08-05 |
| JPH04231148A (ja) | 1992-08-20 |
| AU8019791A (en) | 1992-01-16 |
| FI913401A7 (fi) | 1992-01-17 |
| KR920002255A (ko) | 1992-02-28 |
| ZA915552B (en) | 1992-04-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| FR2664514A1 (fr) | Procede et dispositif de coulee de feuillards et buse de delivrance du metal utilisee avec ce procede et ce dispositif. | |
| FR2664513A1 (fr) | Procede et dispositif de controle de l'epaisseur en coulee continue de bande mince de materiau electroconducteur. | |
| CA2018288A1 (fr) | Dispositif de traitement par anodisation de pistons en alliage d'aluminium utilises dans les moteurs a combustion interne | |
| FR2750438A1 (fr) | Procede et installation de revetement electrolytique par une couche metallique de la surface d'un cylindre pour coulee continue de bandes metalliques minces | |
| EP0407323B1 (de) | Verfahren und Vorrichtung zum Stranggiessen mit Doppelrollen von dünnen metallischen Produkten, geeignet zum Kaltwalzen | |
| FR2679803A1 (fr) | Procede permettant d'ameliorer l'etat de surface et la regularite d'epaisseur d'une bande mince metallique coulee sur une roue. | |
| EP0031772B1 (de) | Verfahren und Vorrichtung zum Herstellen von Float-Glas | |
| CA2048428A1 (fr) | Procede pour controler l'epaisseur d'une bande metallique en continu sur un cylindre | |
| EP0241387A1 (de) | Giessform, die die Regulierung der Höhe der freien Oberfläche von Metallschmelzen zur Berührung mit der Giessform beim vertikalen Giessen gestattet | |
| EP0083611A1 (de) | Verfahren zum vertikalen stranggiessen von aluminium und dessen legierungen mit hoher geschwindigkeit. | |
| EP0393005A2 (de) | Verfahren und Vorrichtung zur Kühlung eines stranggegossenen Metallerzeugnisses | |
| BE1005137A6 (fr) | Procede et dispositif de decalaminage d'un produit metallique lamine a chaud. | |
| FR2658440A3 (fr) | Lingotiere de coulee continue de metal liquide tel que l'acier. | |
| BE1032289B1 (fr) | Procédé de galvanisation de fils en défilement continu et système de filière d'essuyage | |
| FR2684576A1 (fr) | Dispositif de coulee continue d'une bande mince metallique entre cylindres. | |
| EP0222724A1 (de) | Verfahren und Vorrichtung zur Herstellung einer hauchdünnen Metallfolie durch galvanische Beschichtung | |
| FR2485569A1 (fr) | Appareil de metallisation par immersion a chaud d'une face d'une bande | |
| BE850801A (fr) | Procede et dispositif de refroidissement d'elements continus | |
| WO1996038599A1 (fr) | Procede et dispositif pour revetir une bande metallique d'un metal ou d'un alliage a plus bas point de fusion ou de liquide que celui du materiau constituant la bande | |
| EP0277889A1 (de) | Verfahren zur Steuerung des Pegels der Kontaktlinie der freien Metalloberfläche mit der Stranggiesskokille in einen vertikalen Strangguss | |
| FR2619032A3 (fr) | Procede et dispositif d'alimentation en metal liquide d'une installation de coulee continue de produits minces en lingotiere a parois mobiles | |
| FR2695846A1 (fr) | Paroi d'obturation latérale d'une installation de coulée continue des métaux entre parois mobiles et installation comportant une telle paroi. | |
| FR2618704A3 (fr) | Procede et dispositif d'alimentation d'une lingotiere de coulee continue de produits minces | |
| FR2526689A1 (fr) | Procede et appareil pour la coulee continue ou semi-continue de lingots de metal | |
| BE905588A (fr) | Dispositif de depot electrolytique et procede pour sa mise en oeuvre. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES GB GR IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19920204 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: PECHINEY RECHERCHE (GROUPEMENT D'INTERET ECONOMIQ Owner name: I.R.S.I.D. SNC |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: PECHINEY RECHERCHE (GROUPEMENT D'INTERET ECONOMIQ Owner name: I.R.S.I.D. SNC |
|
| 17Q | First examination report despatched |
Effective date: 19941012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN REFUSED |
|
| 18R | Application refused |
Effective date: 19950417 |