EP0504368B1 - Nontisse lie hydrauliquement et son procede de fabrication - Google Patents
Nontisse lie hydrauliquement et son procede de fabrication Download PDFInfo
- Publication number
- EP0504368B1 EP0504368B1 EP91918188A EP91918188A EP0504368B1 EP 0504368 B1 EP0504368 B1 EP 0504368B1 EP 91918188 A EP91918188 A EP 91918188A EP 91918188 A EP91918188 A EP 91918188A EP 0504368 B1 EP0504368 B1 EP 0504368B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- fibers
- nonwoven
- wood pulp
- synthetic fibers
- pct
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 7
- 229920002994 synthetic fiber Polymers 0.000 claims abstract description 28
- 238000000034 method Methods 0.000 claims abstract description 22
- 229920001131 Pulp (paper) Polymers 0.000 claims abstract description 18
- 239000008240 homogeneous mixture Substances 0.000 claims abstract description 6
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 22
- 230000008569 process Effects 0.000 claims description 13
- 230000002745 absorbent Effects 0.000 claims description 12
- 239000002250 absorbent Substances 0.000 claims description 12
- 238000010438 heat treatment Methods 0.000 claims description 8
- 230000004927 fusion Effects 0.000 claims description 4
- 239000012209 synthetic fiber Substances 0.000 abstract description 23
- 239000000203 mixture Substances 0.000 abstract description 16
- 239000004744 fabric Substances 0.000 abstract description 12
- 238000002844 melting Methods 0.000 abstract description 7
- 230000008018 melting Effects 0.000 abstract description 7
- 239000000835 fiber Substances 0.000 description 54
- 239000004698 Polyethylene Substances 0.000 description 13
- 230000009102 absorption Effects 0.000 description 11
- 238000010521 absorption reaction Methods 0.000 description 11
- -1 polyethylene Polymers 0.000 description 10
- 238000012360 testing method Methods 0.000 description 10
- 239000004743 Polypropylene Substances 0.000 description 9
- 239000011230 binding agent Substances 0.000 description 8
- 239000007788 liquid Substances 0.000 description 8
- 239000004745 nonwoven fabric Substances 0.000 description 8
- 229920000573 polyethylene Polymers 0.000 description 7
- 239000004753 textile Substances 0.000 description 6
- 238000001035 drying Methods 0.000 description 5
- 239000004816 latex Substances 0.000 description 5
- 229920000126 latex Polymers 0.000 description 5
- 229920000728 polyester Polymers 0.000 description 5
- 229920001169 thermoplastic Polymers 0.000 description 5
- 239000004416 thermosoftening plastic Substances 0.000 description 5
- 230000000052 comparative effect Effects 0.000 description 3
- 238000005259 measurement Methods 0.000 description 3
- 239000002184 metal Substances 0.000 description 3
- 229920001155 polypropylene Polymers 0.000 description 3
- 230000000717 retained effect Effects 0.000 description 3
- 239000000126 substance Substances 0.000 description 3
- 230000015572 biosynthetic process Effects 0.000 description 2
- 238000003490 calendering Methods 0.000 description 2
- 229920002678 cellulose Polymers 0.000 description 2
- 239000001913 cellulose Substances 0.000 description 2
- 238000001816 cooling Methods 0.000 description 2
- 238000004049 embossing Methods 0.000 description 2
- 238000009434 installation Methods 0.000 description 2
- 230000014759 maintenance of location Effects 0.000 description 2
- 239000008267 milk Substances 0.000 description 2
- 235000013336 milk Nutrition 0.000 description 2
- 210000004080 milk Anatomy 0.000 description 2
- 238000003756 stirring Methods 0.000 description 2
- 239000000725 suspension Substances 0.000 description 2
- 229920013683 Celanese Polymers 0.000 description 1
- 241000876833 Emberizinae Species 0.000 description 1
- 102220632628 Immunoglobulin heavy variable 1-69_E22A_mutation Human genes 0.000 description 1
- 239000004166 Lanolin Substances 0.000 description 1
- 230000009471 action Effects 0.000 description 1
- 230000004888 barrier function Effects 0.000 description 1
- 238000007664 blowing Methods 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 238000007596 consolidation process Methods 0.000 description 1
- 238000007796 conventional method Methods 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 239000002657 fibrous material Substances 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 239000011521 glass Substances 0.000 description 1
- 239000007970 homogeneous dispersion Substances 0.000 description 1
- 239000012943 hotmelt Substances 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 238000010348 incorporation Methods 0.000 description 1
- 229940039717 lanolin Drugs 0.000 description 1
- 235000019388 lanolin Nutrition 0.000 description 1
- 230000000737 periodic effect Effects 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 230000009103 reabsorption Effects 0.000 description 1
- 102220215119 rs1060503548 Human genes 0.000 description 1
- 102200082881 rs33936254 Human genes 0.000 description 1
- 238000005507 spraying Methods 0.000 description 1
- 238000007725 thermal activation Methods 0.000 description 1
- 238000012549 training Methods 0.000 description 1
- 239000001993 wax Substances 0.000 description 1
- 239000002759 woven fabric Substances 0.000 description 1
Images



Classifications
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/44—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties the fleeces or layers being consolidated by mechanical means, e.g. by rolling
- D04H1/46—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties the fleeces or layers being consolidated by mechanical means, e.g. by rolling by needling or like operations to cause entanglement of fibres
- D04H1/48—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties the fleeces or layers being consolidated by mechanical means, e.g. by rolling by needling or like operations to cause entanglement of fibres in combination with at least one other method of consolidation
- D04H1/49—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties the fleeces or layers being consolidated by mechanical means, e.g. by rolling by needling or like operations to cause entanglement of fibres in combination with at least one other method of consolidation entanglement by fluid jet in combination with another consolidation means
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/54—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by welding together the fibres, e.g. by partially melting or dissolving
- D04H1/541—Composite fibres, e.g. sheath-core, sea-island or side-by-side; Mixed fibres
- D04H1/5412—Composite fibres, e.g. sheath-core, sea-island or side-by-side; Mixed fibres sheath-core
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/54—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by welding together the fibres, e.g. by partially melting or dissolving
- D04H1/541—Composite fibres, e.g. sheath-core, sea-island or side-by-side; Mixed fibres
- D04H1/5414—Composite fibres, e.g. sheath-core, sea-island or side-by-side; Mixed fibres side-by-side
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/54—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by welding together the fibres, e.g. by partially melting or dissolving
- D04H1/541—Composite fibres, e.g. sheath-core, sea-island or side-by-side; Mixed fibres
- D04H1/5418—Mixed fibres, e.g. at least two chemically different fibres or fibre blends
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/54—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by welding together the fibres, e.g. by partially melting or dissolving
- D04H1/542—Adhesive fibres
- D04H1/544—Olefin series
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/70—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres characterised by the method of forming fleeces or layers, e.g. reorientation of fibres
- D04H1/74—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres characterised by the method of forming fleeces or layers, e.g. reorientation of fibres the fibres being orientated, e.g. in parallel (anisotropic fleeces)
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1002—Methods of surface bonding and/or assembly therefor with permanent bending or reshaping or surface deformation of self sustaining lamina
- Y10T156/1007—Running or continuous length work
- Y10T156/1008—Longitudinal bending
- Y10T156/1011—Overedge bending or overedge folding
Definitions
- the invention relates to an absorbent nonwoven product consisting mainly of short absorbent fibers, such as wood pulp fibers, and of longer synthetic fibers, the nonwoven being obtained by hydraulic bonding.
- a suspension of fibers in water is produced from which a sheet is formed.
- various qualities of paper are obtained, including cellulose wadding. This one finds many applications like household paper, for the care of the body, the wiping, etc.
- the cellulose wadding presents a weak mechanical resistance especially in the wet state which does not allow its application in the field of industrial or household wiping for example.
- the fibers are suspended in a gas flow, and they are deposited in a sheet on a permeable fabric.
- a binder generally a latex
- This product has substantially the same applications as the latter.
- the incorporation of a binder such as latex has drawbacks. For example, it increases the rigidity of the product and can react chemically with the fluids with which it is likely to come into contact. This is particularly the case when it is desired to make wipes impregnated with a liquid such as toilet milk or the like.
- thermoplastic synthetic fibers which perform the function of binder by thermal activation.
- CHICOPEE thermoplastic synthetic fibers which perform the function of binder by thermal activation.
- CHICOPEE thermally bonded absorbent nonwoven whose density is low, less than 0.15 g / cm3 (0.06 g / cm3 according to the examples reported), and composed of absorbent fibers of the papermaking type mixed with synthetic fibers conjugated to two components: polyethylene and polyester.
- the manufacturing process consists in preparing a sheet from a homogeneous mixture of absorbent fibers and conjugated fibers; then subjecting it to a heat treatment in the mass, under low pressure, at a temperature sufficient to melt the polyethylene located on the surface of the synthetic fibers but not the polyester. In this way, after cooling, a low density nonwoven is obtained, the synthetic material component of which has retained its fibrous character.
- the fact that synthetic fibers retain their integrity is an important factor according to the patent for obtaining a product of high mass volume, with high absorption capacity.
- the envisaged applications consequently aim to use in particular as an absorbent body in hygiene articles, periodic towel for example.
- a consolidation post-treatment (calendering, embossing), or the association with another more resistant veil, seems necessary if one wishes to use this nonwoven in an application such as wiping where the mechanical stresses are great.
- Patent application EP 0326771 describes an absorbent and resistant nonwoven, composed of wood pulp fibers and textile fibers, free of any binder.
- This nonwoven is produced from one or more veils, previously formed by the wet method using the papermaking technique, and consisting of a homogeneous mixture of fibers containing 50 to 75% by weight of wood pulp and 25 to 50% by weight of synthetic fibers of textile length.
- the veil (s) have also been subjected to a binding treatment by water jets, known per se, with sufficient energy to form a relatively dense, uniform nonwoven fabric, with good cohesion of the fibers between them.
- US Patent 3620903 relates to a light nonwoven of the type bound by water jets, comprising at least 20% of synthetic fibers and up to 80% of paper fibers. It is noted that the grammage of the product is a maximum of 57 g / m 2 and that it is intended for a textile application. This product compares favorably in terms of resistance, appearance and drape with conventional textiles for clothing items.
- Patent EP 171 806 relates to a nonwoven, comprising at least 10% of conjugated fibers, bound by water jets and having undergone heating up to the partial melting temperature thereof.
- the other fibers can be any, synthetic or natural, short or long (6 to 50 mm).
- the invention relates to a method of manufacturing an absorbent nonwoven consisting of wood pulp fibers and synthetic fibers, using a binding treatment using water jets.
- the invention is characterized in that the binding treatment by water jets is carried out on a sheet, consisting of a homogeneous mixture of unbound fibers of wood pulp and synthetic fibers, hot-melt at least in part and of length less than 20 mm, formed by air flow and in that the nonwoven is then subjected to heating at a temperature sufficient to cause at least partial fusion of the synthetic fibers.
- the formation of the web is ensured by any conventional method known to those skilled in the art. It consists in preparing metered quantities, on the one hand of synthetic fibers by opening and individualizing them, on the other hand of paper fibers obtained by dry defibration of paper pulp; then driving them by air, suspended in an air flow in a cyclone type mixer for example. The homogeneous mixture resulting from the latter is then entrained, still in suspension in an air flow, towards a head for forming the sheet from which the fibers are deposited uniformly on a support fabric traveling at a determined continuous speed.
- the mixture produced will preferably comprise at least 70% by weight of wood pulp fibers, the remainder consisting of synthetic fibers.
- An advantageous mixture will be composed of 70 to 90% by weight of wood pulp fibers and 30 to 10% of synthetic fibers. If you introduce too little fiber synthetic in the mass of wood pulp fibers, it is difficult to obtain a homogeneous dispersion, and the grammage of the tablecloth lacks regularity. In addition, the subsequent binding is not carried out satisfactorily.
- Synthetic fibers can be of various natures; they will preferably have a length less than 20 mm and a titer between 1.2 and 3.3 dtex.
- the binding treatment by water jets is also known per se to those skilled in the art.
- An example of a process is described in patents US 3,485,706 (EVANS) or US 3,560,326 (BUNTING). It consists in passing through fine jets of high energy liquid through the fibrous sheet to be treated which is arranged by a support, in horizontal displacement, consisting of a perforated plate or else of a suitably chosen woven fabric. The intertwining of the fibers produced by the action of the water jets, leads to consolidating the sheet and gives it a textile appearance.
- the process allows the production of a nonwoven having a basis weight between 20 and 200 g / m 2 , preferably it will be 40 to 100 g / m 2 .
- the upper limit will depend on the ability of the water jets to cross the sheet and interleave the fibers.
- thermoplastic synthetic fibers and by subjecting the nonwoven, originating from the hydraulic bonding station, to a thermal bonding treatment by which the thermoplastic fibers are melted, partially at least, and ensure, after cooling , the formation of bonding zones between the fibers.
- these fibers are two-component fibers of which the one with the lowest melting point is at the surface. The heating temperature is determined so as to be sufficient to melt that of the two components which is at a lower melting point but not the other. These fibers thus allow a lower thermobonding temperature and the fibrous structure is preserved.
- the process therefore makes it possible to obtain a product having a textile appearance, absorbent, resistant to tearing, and therefore the surface does not tend to fluff. It can be used as a disposable or short-term product, as a household, industrial wiping cloth or in catering. By its absence of any chemical binder, it can serve as a support for impregnating liquids: toilet milk, lanolin, wax, etc., and can be used as an impregnated wipe. It can also be used in the medical, surgical, or hygienic field, if necessary, it is possible to subject the nonwoven to a chemical or mechanical softening post-treatment.
- FIG. 1 represents an installation allowing the implementation of the method of the invention.
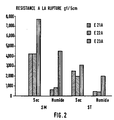
- Figures 2 and 3 are graphs illustrating the tensile strength of nonwovens obtained according to the method of the invention.
- FIG. 4 is a graph illustrating a comparative test with a dry bonded nonwoven by latex and a thermally bonded nonwoven.
- the installation shown in Figure 1 comprises a receiving station for synthetic fibers (2) with a loader to feed a card (4) necessary when the fibers must be opened.
- the card itself feeds a mixer (5) which can be of the cyclone type.
- the mixer is also supplied with wood pulp fibers from a station (3) for dry defibering of paper pulp which is delivered in the form of sheets in a roll.
- the fibers, intimately mixed in the cyclone, are suspended in an air flow which carries them towards a head for forming the sheet (6).
- It may be a device of the type described in patent application EP 032772 (SCANWEB), or an equivalent device.
- This consists of two rotary cylinders (61,62), parallel, perforated wall, and arranged transversely relative to an endless receiving fabric (8), which is itself permeable to air. Inside each cylinder, there is a rod (63) for stirring the fibers provided with fins rubbing against their internal wall when they are rotating.
- the fluidized fibrous material is introduced inside the cylinders (61, 62) by one end, and is sucked through their perforated wall by a depression generated by a vacuum box (10) disposed under the receiving fabric (8 ) opposite the training head (6).
- the stirring rods ensure the progression of the mass of fibers axially inside the cylinders, and help in the division of the aggregates possibly formed as well as in the passage of the fibers to the through walls.
- This station comprises an endless cloth (21) stretched horizontally between rollers (22), at least one of which is driven by suitable means.
- the mesh of the canvas made of metal or plastic threads, is chosen in particular according to the texture, open or not, desired for the nonwoven; a perforated continuous sheet is also suitable.
- the canvas conveys the sheet through a set of ramps of water jets oriented transversely to its direction of movement. The number of ramps depends on the chosen stage of pressures. In the example produced on equipment supplied by the Perfojet Company, there are four.
- the water jets are produced from tubular distributors (24,26,28,30), arranged across the top of the fabric.
- Each distributor feeds a ramp of 40 to 60 injectors consisting of a plate pierced with calibrated orifices.
- the distributors are supplied with pressurized water and deliver high energy water jets on the fibrous web. After having dissipated its energy through the tablecloth, the water is recovered by suction boxes (25,27,29,31) arranged under the fabric opposite each ramp.
- the sheet after having been tied, is wrung by passage over vacuum slots and is then drawn to a drying device (40).
- a drying device (40).
- the one shown in the figure is a through-blowing oven, the temperature of the heating gas of which can be adjusted so as to be able to ensure, in addition to drying, if necessary, the melting of the thermoplastic fibers contained in the sheet.
- the heating conditions in the oven were chosen so as to allow the drying of the nonwoven and the melting of the polyethylene of the synthetic fibers but not that of the polypropylenes In this way, the latter have retained their integrity, while ensuring the bonding of the fibers which are in contact with them.
- the measurements were made according to EDANA standards.
- the test for measuring the breaking strength 20.2-89 consists in subjecting the nonwoven to a tensile force at constant speed (100 mm / min) and in measuring the maximum load before breaking. The elongation corresponds to the extension of the sample measured at this point.
- the absorption capacity measurement test 10.1-72 consists in measuring, on the one hand, the time necessary for a nonwoven to be completely impregnated with a liquid, and on the other hand, the quantity of liquid absorbed during a determined time reduced to the weight of the nonwoven.
- polyethylene / polyester fibers such as those sold under the brand name CELANESE reference K 56 (uncrimped, 10 mm, 2.2 dtex) or else under the SOLSTAR brand (uncrimped, 10 mm, 2.2 dtex) or Polyester / polyester fibers as sold under the brand DUPONT reference 271P (uncrimped, 12 mm, 2.2 dtex) or under the brand UNITIKA reference Melty ( crimped, 10-15 mm, 1.5 / 2 dtex) or polyethylene / polypropylene fibers as sold under the brand DAIWABO reference NBF (uncrimped, 10 mm, 2 dtex).
- CELANESE reference K 56 uncrimped, 10 mm, 2.2 dtex
- SOLSTAR brand uncrimped, 10 mm, 2.2 dtex
- Polyester / polyester fibers as sold under the brand DUPONT reference 271P (uncrimped, 12 mm, 2.2 dtex) or under the brand UNITIKA reference Melty ( crimped
- fibers of the S / S type side / side
- polyethylene fiber sold under the brand STEEN reference Polysteen uncrimped, 12 mm, 2.8 dtex).
- Example 1 In the third case, the conditions of Example 1 were reproduced (tests E23A and E23B).
- the first E31 is a dry type product, the bond between the fibers was obtained by spraying with latex.
- the nonwoven contains 20% by weight of binder.
- the second E32 is a nonwoven, of the dry process type bonded by embossing, with a binder consisting of DANAKLON ESF thermoplastic fibers (see example 1) at a rate of 20%.
- the third E33 is a product produced under the conditions of Example 1 with mixture A.
- Example 1 obtained from mixtures D, E and F according to the process of the invention and a dry nonwoven bonded with latex (15%) as sold under the brand HOMECEL reference P050.
- the test consisted in particular in placing a sample on an absorption plate made of porous sintered glass through which it is moistened.
- the tray is connected by a flexible tube to a tank placed on a scale, and it can be moved along a vertical rail.
- the measurements are taken from the weight indications by the balance, the absorption capacity of the sample of which can be calculated in grams of liquid per gram of sample, after a determined time, and also the speed of initial absorption.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Mechanical Engineering (AREA)
- Nonwoven Fabrics (AREA)
- Adornments (AREA)
- Materials For Medical Uses (AREA)
- Absorbent Articles And Supports Therefor (AREA)
Description
- L'invention se rapporte à un produit nontissé absorbant constitué de fibres absorbantes courtes en majorité, telles que des fibres de pâte de bois, et de fibres synthétiques plus longues, le nontissé étant obtenu par un liage hydraulique.
- Selon une technique courante de fabrication de produits à base de fibres papetières, on réalise une suspension de fibres dans l'eau à partir de laquelle on forme une feuille. Suivant la nature des fibres et le traitement de la feuille on obtient diverses qualités de papiers, dont l'ouate de cellulose. Celle-ci trouve de nombreuses applications comme papier de ménage, pour les soins du corps, l'essuyage, etc.. Toutefois, l'ouate de cellulose présente une faible résistance mécanique surtout à l'état humide qui ne permet pas son application dans le domaine de l'essuyage industriel ou ménager par exemple.
- Selon une autre technique,dite par voie sèche, telle que décrite par exemple dans le brevet GB 2015604 (KROYER), on met les fibres en suspension dans un flux gazeux, et on les dépose en nappe sur une toile perméable. Le faible taux d'humidité ne permettant pas la constitution de liaisons interfibres, il est nécessaire d'ajouter un liant, généralement un latex, pour assurer la cohésion de la nappe. On obtient ainsi un produit présentant une meilleure résistance à la déchirure que le papier traditionnel tout en étant très absorbant. Ce produit trouve sensiblement les mêmes applications que ce dernier. Toutefois, l'incorporation d'un liant tel que le latex présente des inconvénients. Par exemple, il augmente la rigidité du produit et peut réagir chimiquement avec les fluides avec lesquels il est susceptible de venir en contact. C'est le cas notamment quand on souhaite réaliser des lingettes imprégnées avec un liquide tel qu'un lait de toilette ou autre.
- Au lieu d'employer un liant de nature chimique, on a proposé d'incorporer, à la nappe de fibres absorbantes, des fibres synthétiques thermoplastiques qui assurent la fonction de liant par activation thermique. Ainsi par exemple la demande de brevet EP 070164 (CHICOPEE) décrit un nontissé absorbant lié thermiquement dont la masse volumique est faible, inférieure à 0,15 g/cm3 (0,06 g/cm3 selon les exemples rapportés), et composé de fibres absorbantes de type papetier mélangées à des fibres synthétiques conjuguées à deux composants : polyéthylène et polyester. Le procédé de fabrication consiste à préparer une nappe à partir d'un mélange homogène de fibres absorbantes et de fibres conjuguées; puis à lui faire subir un traitement thermique dans la masse, sous faible pression, à une température suffisante pour fondre le polyéthylène localisé en surface des fibres synthétiques mais pas le polyester. De la sorte, on obtient après refroidissement un nontissé de faible densité dont la composante de matière synthétique a conservé son caractère fibreux. Le fait que les fibres synthétiques conservent leur intégrité est un facteur important selon le brevet pour obtenir un produit de volume massique élevé, à grande capacité d'absorption. Les applications envisagées visent en conséquence l'emploi notamment comme corps absorbant dans les articles d'hygiène, serviette périodique par exemple. Cependant un post-traitement de consolidation (calandrage,gaufrage), ou l'association à un autre voile plus résistant, parait nécessaire si l'on souhaite employer ce nontissé dans une application telle que l'essuyage où les contraintes mécaniques sont grandes.
- La demande de brevet EP 0326771 (JAMES RIVER) décrit un nontissé absorbant et résistant, composé de fibres de pâte de bois et de fibres textiles, libre de tout liant. Ce nontissé est réalisé à partir d'un ou de plusieurs voiles, formés préalablement par voie humide selon la technique papetière, et constitués d'un mélange homogène de fibres contenant 50 à 75% en poids de pâte de bois et 25 à 50% en poids de fibres synthétiques de longueur textile. Le ou les voiles ont en outre été soumis à un traitement de liage par jets d'eau, connu en soi, avec une énergie suffisante pour former un tissu nontissé relativement dense, uniforme, avec une bonne cohésion des fibres entre elles.
- On connait également le brevet US 4442161 (KIRAYOGLU) qui se rapporte à un procédé de fabrication d'un nontissé lié par jets d'eau, constitué de fibres synthétiques et de pâte de bois. Le liage est effectué en particulier à partir de fibres synthétiques se présentant sous la forme d'un voile nontissé de filaments continus et de fibres de pâte de bois sous la forme d'une feuille de papier. Le traitement est effectué dans des conditions permettant d'accroître les propriétés de barrière aux liquides du nontissé en vue notamment d'une application comme linge à usage médical ou chirurgical.
- Le brevet US 3620903 porte sur un nontissé léger du type lié par jets d'eau, comprenant au moins 20 % de fibres synthétiques et jusqu'à 80 % de fibres papetières. On note que le grammage du produit est au maximum de 57 g/m2 et qu'il est destiné à une application textile. Ce produit se compare favorablement en termes de résistance, aspect et drapé aux textiles conventionnels pour des articles d'habillement.
- Le brevet EP 171 806 se rapporte à un nontissé, comprenant au moins 10 % de fibres conjuguées, lié par jets d'eau et ayant subi un chauffage jusqu'à la température de fusion partielle de celle-ci. Les autres fibres peuvent être quelconques, synthétiques ou naturelles, courtes ou longues (6 à 50 mm).
- L'invention a pour objet un procédé de fabrication d'un nontissé absorbant constitué de fibres de pâte de bois et de fibres synthétiques, mettant en oeuvre un traitement de liage par jets d'eau. L'invention est caractérisée en ce que le traitement de liage par jets d'eau est effectué sur une nappe, constituée d'un mélange homogène de fibres non liées de pâte de bois et de fibres synthétiques, thermofusibles au moins en partie et de longueur inférieure à 20 mm, formée par voie aéraulique et en ce qu'ensuite le nontissé est soumis à un chauffage à une température suffisante pour entraîner une fusion au moins partielle des fibres synthétiques.
- En effet, contrairement à l'art antérieur qui consiste à partir de voiles nontissés ayant subi un liage préalable, on a constaté que l'on pouvait en appliquant le procédé de l'invention obtenir un produit présentant de bonnes caractéristiques de résistance à la rupture, tant en humide qu'en sec, et de vitesse d'absorption.
- La formation de la nappe est assurée selon un quelconque procédé classique connu de l'homme du métier. Il consiste à préparer des quantités dosées, d'une part de fibres synthétiques en les ouvrant et en les individualisant, d'autre part de fibres papetières obtenues par défibrage à sec de pâte à papier ; puis à les entraîner par voie aéraulique, en suspension dans un flux d'air dans un mélangeur du type cyclone par exemple. Le mélange homogène issu de ce dernier est alors entraîné, toujours en suspension dans un flux d'air, vers une tête de formation de la nappe à partir de laquelle les fibres sont déposées uniformément sur une toile support défilant à une vitesse continue déterminée.
- Le mélange réalisé comportera de préférence au moins 70 % en poids de fibres de pâte de bois, le restant étant constitué de fibres synthétiques. Un mélange avantageux sera composé de 70 à 90 % en poids de fibres de pâte de bois et de 30 à 10 % de fibres synthétiques. Si on introduit une quantité trop faible de fibres synthétiques dans la masse de fibres de pâte de bois, il est difficile d'en obtenir une dispersion homogène, et le grammage de la nappe manque de régularité. En outre le liage ultérieur ne s'effectue pas de façon satisfaisante. Les fibres synthétiques peuvent être de diverses natures ; elles auront de préférence une longueur inférieure à 20 mm et un titre compris entre 1,2 et 3,3 dtex.
- Le traitement de liage par jets d'eau est également en soi connu de l'homme du métier. Un exemple de procédé est décrit dans les brevets US 3485706 (EVANS) ou US 3560326 (BUNTING). Il consiste à faire traverser par de fins jets de liquide à haute énergie la nappe fibreuse à traiter qui est disposée par un support, en déplacement horizontal, constitué d'une plaque perforée ou bien d'une toile tissée convenablement choisie. L'entrelacement des fibres produit par l'a ction des jets d'eau, conduit à consolider la nappe est à lui donner un aspect textile.
- Le procédé permet la production d'un nontissé présentant un grammage compris entre 20 et 200 g/m2, de préférence il sera de 40 à 100 g/m2. En fait, la limite supérieure dépendra de la capacité des jets d'eau à traverser la nappe et effectuer l'entrelacement des fibres.
- On améliore la résistance à la déchirure en choisissant des fibres synthétiques thermoplastiques, et en soumettant le nontissé, issu du poste de liage hydraulique, à un traitement de liage thermique par lequel les fibres thermoplastiques sont fondues, partiellement au moins, et assurent, après refroidissement, la formation de zones de liaison entre les fibres. Avantageusement, ces fibres sont des fibres à deux composants dont celui qui est à plus bas point de fusion est en surface. La température de chauffage est déterminée de façon à être suffisante pour faire fondre celui des deux composants qui est à plus bas point de fusion mais pas l'autre. Ces fibres autorisent ainsi une température de thermoliage plus faible et la structure fibreuse est conservée.
- Le procédé permet donc d'obtenir un produit ayant un aspect textile, absorbant, résistant à la déchirure, et donc la surface n'a pas tendance à pelucher. Il peut être employé, en tant que produit jetable ou à usage court, comme chiffon d'essuyage ménager, industriel, ou dans la restauration. Par son absence de tout liant chimique, il peut servir de support à des liquides d'imprégnation : lait de toilette, lanoline, cire, etc., et peut être employé comme lingette imprégnée. Il peut également être employé dans le domaine médical, chirurgical, ou de l'hygiène, le cas échéant, il est possible de soumettre le nontissé à un post-traitement chimique ou mécanique d'assouplissement.
- D'autres caractéristiques et avantages apparaîtront dans la description qui va suivre d'un mode de réalisation non exhaustif de l'invention en regard des dessins sur lesquels :
- La figure 1 représente une installation permettant la mise en oeuvre du procédé de l'invention.
- Les figures 2 et 3 sont des graphiques illustrant la résistance à la rupture de nontissés obtenus selon le procédé de l'invention.
- La figure 4 est un graphique illustrant un test comparatif avec un nontissé voie sèche lié par latex et un nontissé lié thermiquement.
- L'installation représentée sur la figure 1 comporte un poste de réception des fibres synthétiques (2) avec une chargeuse pour alimenter une carde (4) nécessaire lorsque les fibres doivent être ouvertes. La carde alimente elle-même un mélangeur (5) qui peut être du type cyclone. Le mélangeur est alimenté par ailleurs en fibres de pâte de bois depuis un poste (3) de défibrage à sec de pâte à papier qui est livrée sous forme de feuilles en rouleau. Les fibres, mélangées intimement dans le cyclone, sont en suspension dans un flux d'air qui les entraîne vers une tête de formation de la nappe (6).
- Il peut s'agir d'un dispositif du type décrit dans la demande de brevet EP 032772 (SCANWEB), ou d'un dispositif équivalent. Celui-ci est constitué de deux cylindres (61,62) rotatifs, parallèles, à paroi ajourée, et disposés transversalement par rapport à une toile de réception (8) sans fin, qui est elle-même perméable à l'air. A l'intérieur de chaque cylindre, se trouve une tige (63) de brassage des fibres pourvue d'ailettes frottant contre leur paroi interne quand ils sont en rotation. Le matériau fibreux fluidisé est introduit à l'intérieur des cylindres (61,62) par une extrémité, et est aspiré au travers de leur paroi ajourée par une dépression engendrée par une boite à vide (10) disposée sous la toile de réception (8) en regard de la tête de formation (6). Les tiges de brassage assurent la progression de la masse de fibres axialement à l'intérieur des cylindres, et aident à la division des agrégats éventuellement formés ainsi qu'au passage des fibres au travers des parois. Des tôles (65,66), disposées de part et d'autre des cylindres, canalisent le flux gazeux vers la toile (8). Les fibres sont ainsi réceptionnées sur la toile mobile en une nappe continue qui est entraînée vers le poste de liage par jets d'eau (20).
- Ce poste comprend une toile sans fin (21), tendue horizontalement entre des rouleaux (22), dont l'un au moins est entraîné par des moyens appropriés. Le maillage de la toile, réalisée en fils métalliques ou de matière plastique, est choisi notamment en fonction de la texture, ouverte ou non, désirée pour le nontissé ; une feuille continue ajourée convient également. La toile convoie la nappe au travers d'un jeu de rampes de jets d'eau orientés transversalement par rapport à son sens de déplacement. Le nombre de rampes dépend de l'étagement choisi des pressions. Dans l'exemple réalisé sur un matériel fourni par la Société Perfojet il est de quatre. Les jets d'eau sont produits depuis des distributeurs tubulaires (24,26,28,30), disposés en travers au dessus de la toile. Chaque distributeur alimente une rampe de 40 à 60 injecteurs constituée d'une plaque percée d'orifices calibrés. Les distributeurs sont alimentés en eau sous pression et délivrent des jets d'eau à haute énergie sur la nappe fibreuse. Apres avoir dissipé son énergie au travers de la nappe, l'eau est récupérée par des boites d'aspiration (25,27,29,31) disposées sous la toile en regard de chaque rampe.
- La nappe, après avoir été liée, subit un essorage par passage sur des fentes à vide puis est entraînée vers un dispositif de séchage (40). Celui qui est représenté sur la figure est un four à soufflage traversant dont on peut régler la température du gaz chauffant de manière à pouvoir assurer en plus du séchage, le cas échéant, la fusion des fibres thermoplastiques contenues dans la nappe.
- On a réalisé des nontissés selon le procédé de l'invention avec des mélanges à différents taux de fibres synthétiques (tableau I).
TABLEAU I MELANGES A B C D E F Pâte de bois : "ITT Rayonier JLD"non traitée 80% 70% Vigor 90% 80% 90% 80% Fibres synthétiques : "Danaklon ESF" 12mm 20% 30% "Danaklon ESHF" 6mm 10% 20% "Danaklon ESHF" 12mm 10% 20% - "Danaklon ESF" :
- bicomposants PE/PP, type side/side, frisée longueur 12mm, titre 3,3 dtex
- "Danaklon ESHF" 6mm :
- bicomposants PE/PP, type side/side, frisée longueur 6mm
- "Danaklon ESHF" 12mm :
- bicomposants PE/PP, type side/side frisée longueur 12mm.
- Apres avoir mis les différents mélanges A à F sous forme de nappes, de la façon indiquée plus haut, on a procédé à leur liage par jets d'eau suivi d'un liage thermique. Les conditions de ce liage sont rapportées dans le tableau II qui suit :
Tableau II Toile support : Grille métallique (la contexture et le diamètre des fils métalliques assurent un meilleur entrelacement de la nappe) Vitesse de défilement sous les injecteurs: 25 m/mn Injecteurs: 4 pompes d'injecteurs Diamètre des orifices : 100 - 140 µm Pression des jets d'eau : 30/50/70/90 bars pour le mélange A mesurée au niveau du conduit d'alimentation 30/60/80/100 bars pour les mélanges B 30/40/60/80 bars pour les mélanges C et E Température de l'air dans le four à air chaud traversant 145 à 150°C - Les conditions de chauffage dans le four ont été choisies de façon à permettre le séchage du nontissé et la fusion du polyéthylène des fibres synthétiques mais pas celle du polypropylènes De la sorte, ces dernières ont conservé leur intégrité, tout en assurant la liaison des fibres qui sont à leur contact.
- On a mesuré les caractéristiques de résistance à la rupture et d'absorption des nontissés obtenus selon le procédé. Elles sont rapportées dans le tableau III ci-après :

- Les mesures ont été effectuées selon les normes EDANA. Par exemple, le test de mesure de la résistance à la rupture 20.2-89 consiste à soumettre le nontissé à une force de traction à vitesse constante (100 mm/min) et à mesurer la charge maximale avant rupture. L'allongement correspond à l'extension de l'échantillon mesurée en ce point. Le test de mesure de la capacité d'absorption 10.1-72 consiste à mesurer, d'une part, le temps nécessaire pour qu'un nontissé soit complètement imprégné par un liquide, et d'autre part, la quantité de liquide absorbée pendant un temps déterminé ramenée au poids du nontissé.
- Il est à noter que d'autres fibres, que celles retenues pour l'exemple, sont envisageables. Parmi les fibres à deux composants du type S/C (sheath/core) on peut mentionner des fibres polyéthylène/polyester telles que vendues sous la marque CELANESE référence K 56 (non frisées, 10 mm, 2,2 dtex) ou bien sous la marque SOLSTAR (non frisées, 10 mm, 2,2 dtex) ou bien des fibres Polyester/polyester telles que vendues sous la marque DUPONT référence 271P (non frisées, 12 mm, 2,2 dtex) ou sous la marque UNITIKA référence Melty (frisées, 10-15 mm, 1,5/2 dtex) ou bien des fibres polyethylène/polypropylène telles que vendues sous la marque DAIWABO référence NBF (non frisées, 10 mm, 2 dtex). Parmi les fibres du type S/S (side/side) on peut citer également les fibres polyéthylène/polypropylène vendues sous la marque DAIWABO sous la référence ESF (frisées, 6 mm, 3.3 dtex). Parmi les fibres monocomposantes on peut noter une fibre en polyéthylène vendue sous la marque STEEN référence Polysteen (non frisée, 12 mm, 2,8 dtex).
- A partir de chacun des mélanges A et B de l'exemple précédent on a réalisé trois nontissés, liés hydrauliquement, différents.
- Pour le premier cas on a simplement procédé à un séchage à température modérée de façon à éliminer l'eau sans modifier la structure des fibres (essais E21A et E21B).
- Dans le deuxième cas, on a calandré le nontissé issu du liage par jets d'eau également à température modérée (essais E22A et E22B).
- Dans le troisième cas, on a reproduit les conditions de l'exemple 1 (essais E23A et E23B).
- Les graphiques des figures 2 et 3 représentant la résistance à la rupture d'une éprouvette de 5 cm de large (gf/5cm), sens marche (SM) et sens travers (ST), aussi bien en sec qu'en humide montrent une très nette amélioration par le traitement thermique jusqu'à la température de fusion.
- On a procédé à des essais comparatifs sur trois nontissés de même grammage. Le premier E31 est un produit du type voie sèche dont la liaison entre les fibres a été obtenue par pulvérisation de latex. Le nontissé contient 20 % en poids de liant. Le second E32 est un nontissé, du type voie sèche lié par gaufrage, avec un liant constitué de fibres thermoplastiques DANAKLON ESF (voir exemple 1) à raison de 20 %. Le troisième E33 est un produit réalisé dans les conditions de l'exemple 1 avec le mélange A.
- On constate sur le graphique de la figure 4, représentant la résistance à la rupture sens marche (SM) et sens travers (ST), aussi bien en sec qu'en humide, que le procédé de l'invention conduit à des nontissés nettement plus performants.
- On a effectué un test comparatif d'absorption-rétention-résilience entre des nontissés de l'exemple 1 obtenus à partir des mélanges D, E et F selon le procédé de l'invention et un nontissé voie sèche lié par latex (15 %) tel que vendu sous la marque HOMECEL référence P050.
- Le test a consisté notamment à placer un échantillon sur un plateau d'absorption en verre fritté poreux à travers lequel il est humecté. Le plateau est relié par un tube souple à un réservoir posé sur une balance, et il peut être déplacé le long d'un rail vertical. Les mesures sont effectuées à partir des indications de poids par la balance dont on peut calculer la capacité d'absorption de l'échantillon en gramme de liquide par gramme d'échantillon, au bout d'un temps déterminé, et aussi la vitesse d'absorption initiale.
- Pour la rétention, on déplace le fritté le long du rail de façon que l'échantillon relargue le liquide, du fait de la pression négative créée par la différence de niveau entre le fritté et le réservoir.
Tableau IV PRODUITS MELANGE D MELANGE E MELANGE F HOMECEL Grammage 75,2 72,3 68,4 50,2 Bouffant sec (cc/g) 9,4 9,9 9,3 15,2 Absorption (g/g) 7,3 7,3 7,3 9,4 Vitesse initiale d'absorption (100 x g/g/sec) 186 217 230 175 Rétention (g/g) 4,38 4,44 4,40 5,56 Absorption sous 10 kPa (g/g) 5,1 5,1 5,2 4,9 Réabsorption (g/g) 5,9 6,0 6,0 6,8 Résilience % 17,6 16,1 16,0 30,9 Compression % 31,3 33,5 30,9 54,8 - Cet essai rapporté dans le tableau IV montre notamment que le produit présente une excellente vitesse initiale d'absorption.
Claims (4)
- Procédé pour fabriquer un nontissé absorbant constitué de fibres de pâte de bois et au plus de 30 % de fibres synthétiques mettant en oeuvre un traitement de liage par jets d'eau connu en soi, caractérisé en ce que le traitement de liage par jets d'eau est effectué sur une nappe, constituée d'un mélange homogène de fibres non liées de pâtes de bois et de fibres synthétiques thermofusibles au moins en partie et de longueur inférieure à 20 mm, formée par voie aéraulique et en ce qu'ensuite le nontissé est soumis à un chauffage à une température suffisante pour entraîner une fusion au moins partielle des fibres synthétiques.
- Procédé selon l'une des revendications précédentes caractérisé en ce que les fibres synthétiques comprennent des fibres bicomposantes.
- Procédé selon l'une des revendications précédentes caractérisé en ce que le nontissé présente un grammage compris entre 20 et 200 g/m2, et 40 et 100 g/m2 de préférence.
- Procédé selon la revendication 2 caractérisé en ce que la température est suffisante pour entraîner la fusion du composant dont la température de fusion est la plus basse mais pas la fusion de l'autre composant.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9012348 | 1990-10-08 | ||
| FR9012348A FR2667622B1 (fr) | 1990-10-08 | 1990-10-08 | Montisse lie hydrauliquement et son procede de fabrication. |
| PCT/FR1991/000783 WO1992006237A1 (fr) | 1990-10-08 | 1991-10-04 | Nontisse lie hydrauliquement et son procede de fabrication |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0504368A1 EP0504368A1 (fr) | 1992-09-23 |
| EP0504368B1 true EP0504368B1 (fr) | 1996-08-28 |
Family
ID=9400998
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP91918188A Expired - Lifetime EP0504368B1 (fr) | 1990-10-08 | 1991-10-04 | Nontisse lie hydrauliquement et son procede de fabrication |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US5375306A (fr) |
| EP (1) | EP0504368B1 (fr) |
| AT (1) | ATE141964T1 (fr) |
| CA (1) | CA2070773C (fr) |
| DE (1) | DE69121694T2 (fr) |
| FR (1) | FR2667622B1 (fr) |
| WO (1) | WO1992006237A1 (fr) |
Families Citing this family (37)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4444206A1 (de) * | 1994-12-13 | 1996-06-20 | Fleissner Maschf Gmbh Co | Verfahren und Vorrichtung zum Veredeln von Krempelvliesen |
| FI110326B (fi) * | 1995-06-06 | 2002-12-31 | Bki Holding Corp | Menetelmä kuitukankaan valmistamiseksi |
| US6419789B1 (en) † | 1996-10-11 | 2002-07-16 | Fort James Corporation | Method of making a non compacted paper web containing refined long fiber using a charge controlled headbox and a single ply towel made by the process |
| FR2761901B1 (fr) * | 1997-04-10 | 1999-05-14 | Valeo | Procede de realisation d'un dispositif de filtration et dispositif de filtration en particulier pour l'aeration et/ou la climatisation de locaux ou de vehicules |
| CN1106470C (zh) | 1997-10-13 | 2003-04-23 | M&J纤维技术有限公司 | 一种用于生产塑料纤维和纤维素纤维的纤维网的设备 |
| JP2000034660A (ja) * | 1998-07-17 | 2000-02-02 | Uni Charm Corp | 湿式不織布の製造方法および製造装置 |
| FR2781818B1 (fr) * | 1998-07-31 | 2000-09-01 | Icbt Perfojet Sa | Procede pour la realisation d'un materiau non-tisse complexe et nouveau type de materiau ainsi obtenu |
| US6893522B1 (en) * | 1999-10-05 | 2005-05-17 | Polymer Group, Inc. | High bulk non-woven composite fabric |
| DE10001957A1 (de) * | 2000-01-18 | 2001-07-19 | Fleissner Maschf Gmbh Co | Verfahren und Vorrichtung zur Verfestigung eines nach dem Luftlegeverfahren hergestellten Vlieses |
| DE60144370D1 (de) * | 2000-01-20 | 2011-05-19 | Polymer Group Inc | Vliesstoff mit beständigem bild |
| US6534174B1 (en) * | 2000-08-21 | 2003-03-18 | The Procter & Gamble Company | Surface bonded entangled fibrous web and method of making and using |
| CN1474895A (zh) * | 2000-11-14 | 2004-02-11 | ��Τ����˹ | 由挤出工艺形成的交联纤维素产品 |
| WO2002050354A1 (fr) * | 2000-12-19 | 2002-06-27 | M & J Fibretech A/S | Procede et equipement de production sans bande de base d'une bande de fibres hydro-enchevetrees air-laid |
| US20040260034A1 (en) | 2003-06-19 | 2004-12-23 | Haile William Alston | Water-dispersible fibers and fibrous articles |
| US8513147B2 (en) | 2003-06-19 | 2013-08-20 | Eastman Chemical Company | Nonwovens produced from multicomponent fibers |
| US7892993B2 (en) | 2003-06-19 | 2011-02-22 | Eastman Chemical Company | Water-dispersible and multicomponent fibers from sulfopolyesters |
| WO2006071149A1 (fr) * | 2004-12-29 | 2006-07-06 | Sca Hygiene Products Ab | Moyen d’attache en forme de ceinture pour article absorbant |
| US8921244B2 (en) | 2005-08-22 | 2014-12-30 | The Procter & Gamble Company | Hydroxyl polymer fiber fibrous structures and processes for making same |
| US8852474B2 (en) | 2007-07-17 | 2014-10-07 | The Procter & Gamble Company | Process for making fibrous structures |
| US7972986B2 (en) | 2007-07-17 | 2011-07-05 | The Procter & Gamble Company | Fibrous structures and methods for making same |
| US20090022983A1 (en) | 2007-07-17 | 2009-01-22 | David William Cabell | Fibrous structures |
| US10024000B2 (en) | 2007-07-17 | 2018-07-17 | The Procter & Gamble Company | Fibrous structures and methods for making same |
| US8512519B2 (en) | 2009-04-24 | 2013-08-20 | Eastman Chemical Company | Sulfopolyesters for paper strength and process |
| EP2496768B1 (fr) * | 2009-11-02 | 2015-07-29 | The Procter and Gamble Company | Structures fibreuses à faible peluchage et procédés pour leur fabrications |
| MX343331B (es) * | 2009-11-02 | 2016-11-01 | The Procter & Gamble Company * | Elementos fibrosos de polipropileno y procesos para elaborarlos. |
| BR112012010003A2 (pt) * | 2009-11-02 | 2016-03-01 | Procter & Gamble | elementos fibrosos e estruturas fibrosas que empregam os mesmos |
| MX2012005111A (es) | 2009-11-02 | 2012-05-22 | Procter & Gamble | Estructuras fibrosas y metodos para elaborarlas. |
| JP5770262B2 (ja) | 2010-03-31 | 2015-08-26 | ザ プロクター アンド ギャンブルカンパニー | 繊維性構造体及びその製造方法 |
| US20120183861A1 (en) | 2010-10-21 | 2012-07-19 | Eastman Chemical Company | Sulfopolyester binders |
| US8840757B2 (en) | 2012-01-31 | 2014-09-23 | Eastman Chemical Company | Processes to produce short cut microfibers |
| CN102926131A (zh) * | 2012-10-08 | 2013-02-13 | 稳健实业(深圳)有限公司 | 一种手术巾及其生产方法 |
| TW201420054A (zh) * | 2012-11-21 | 2014-06-01 | Kang Na Hsiung Entpr Co Ltd | 吸濕用不織布及其製法 |
| US9617685B2 (en) | 2013-04-19 | 2017-04-11 | Eastman Chemical Company | Process for making paper and nonwoven articles comprising synthetic microfiber binders |
| US9598802B2 (en) | 2013-12-17 | 2017-03-21 | Eastman Chemical Company | Ultrafiltration process for producing a sulfopolyester concentrate |
| US9605126B2 (en) | 2013-12-17 | 2017-03-28 | Eastman Chemical Company | Ultrafiltration process for the recovery of concentrated sulfopolyester dispersion |
| JP6269181B2 (ja) * | 2014-03-07 | 2018-01-31 | セイコーエプソン株式会社 | シート製造装置 |
| DE102015010105B4 (de) * | 2015-08-03 | 2017-08-24 | Sandler Ag | Dehnbarer Vliesstoff, Verfahren zur Herstellung eines dehnbaren Vliesstoffes und Verwendung desselben |
Family Cites Families (21)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NL70708C (fr) * | 1941-03-01 | |||
| US2464301A (en) * | 1943-12-18 | 1949-03-15 | American Viscose Corp | Textile fibrous product |
| US3620903A (en) * | 1962-07-06 | 1971-11-16 | Du Pont | Lightweight nonpatterned nonwoven fabric |
| US4442161A (en) * | 1982-11-04 | 1984-04-10 | E. I. Du Pont De Nemours And Company | Woodpulp-polyester spunlaced fabrics |
| DE3403670A1 (de) * | 1984-02-03 | 1985-08-08 | Casimir Kast Gmbh & Co Kg, 7562 Gernsbach | Verfahren und anlage zum herstellen von fasermatten als ausgangsmaterial fuer pressformteile |
| JPS6147186A (ja) * | 1984-08-09 | 1986-03-07 | Chemo Sero Therapeut Res Inst | インフルエンザウイルスの精製方法 |
| EP0171806A3 (fr) * | 1984-08-16 | 1987-06-16 | Chicopee | Etoffe non-tissée entremêlée contenant des fibres à deux composants et son procédé de fabrication |
| US4555430A (en) * | 1984-08-16 | 1985-11-26 | Chicopee | Entangled nonwoven fabric made of two fibers having different lengths in which the shorter fiber is a conjugate fiber in which an exposed component thereof has a lower melting temperature than the longer fiber and method of making same |
| US5017312A (en) * | 1984-12-27 | 1991-05-21 | The Coe Manufacturing Company | Oriented chopped fiber mats and method and apparatus for making same |
| US4661132A (en) * | 1985-08-15 | 1987-04-28 | Allied Corporation | Themally formed gradient density filter |
| US4767586A (en) * | 1986-01-13 | 1988-08-30 | Kimberly-Clark Corporation | Apparatus and method for forming a multicomponent integral laid fibrous web with discrete homogeneous compositional zones, and fibrous web produced thereby |
| US4808467A (en) * | 1987-09-15 | 1989-02-28 | James River Corporation Of Virginia | High strength hydroentangled nonwoven fabric |
| US4775579A (en) * | 1987-11-05 | 1988-10-04 | James River Corporation Of Virginia | Hydroentangled elastic and nonelastic filaments |
| US4902564A (en) * | 1988-02-03 | 1990-02-20 | James River Corporation Of Virginia | Highly absorbent nonwoven fabric |
| US4931355A (en) * | 1988-03-18 | 1990-06-05 | Radwanski Fred R | Nonwoven fibrous hydraulically entangled non-elastic coform material and method of formation thereof |
| DE3814996A1 (de) * | 1988-05-03 | 1989-11-16 | Kast Casimir Formteile | Verfahren zur herstellung einer fasermatte |
| JP2577977B2 (ja) * | 1988-10-28 | 1997-02-05 | チッソ株式会社 | 伸縮性不織布及びその製造方法 |
| EP0373974A3 (fr) * | 1988-12-15 | 1990-09-05 | Fiberweb North America, Inc. | Procédé de préparation d'une étoffe non tissée fortement absorbante |
| US5229052A (en) * | 1990-02-23 | 1993-07-20 | Wellman Machinery Of Michigan, Inc. | Apparatus and method for applying multiple type fibers to a foraminous surface |
| US5088910A (en) * | 1990-03-14 | 1992-02-18 | Advanced Environmental Recycling Technologies, Inc. | System for making synthetic wood products from recycled materials |
| US5240764A (en) * | 1992-05-13 | 1993-08-31 | E. I. Du Pont De Nemours And Company | Process for making spunlaced nonwoven fabrics |
-
1990
- 1990-10-08 FR FR9012348A patent/FR2667622B1/fr not_active Expired - Lifetime
-
1991
- 1991-10-04 AT AT91918188T patent/ATE141964T1/de not_active IP Right Cessation
- 1991-10-04 EP EP91918188A patent/EP0504368B1/fr not_active Expired - Lifetime
- 1991-10-04 US US07/852,262 patent/US5375306A/en not_active Expired - Lifetime
- 1991-10-04 CA CA002070773A patent/CA2070773C/fr not_active Expired - Lifetime
- 1991-10-04 DE DE69121694T patent/DE69121694T2/de not_active Expired - Lifetime
- 1991-10-04 WO PCT/FR1991/000783 patent/WO1992006237A1/fr not_active Ceased
Also Published As
| Publication number | Publication date |
|---|---|
| FR2667622B1 (fr) | 1994-10-07 |
| CA2070773A1 (fr) | 1992-04-09 |
| CA2070773C (fr) | 2002-12-10 |
| DE69121694D1 (de) | 1996-10-02 |
| FR2667622A1 (fr) | 1992-04-10 |
| US5375306A (en) | 1994-12-27 |
| ATE141964T1 (de) | 1996-09-15 |
| WO1992006237A1 (fr) | 1992-04-16 |
| EP0504368A1 (fr) | 1992-09-23 |
| DE69121694T2 (de) | 1997-01-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2070773C (fr) | Nontisse absorbant lie hydrauliquement et son procede de fabrication | |
| EP1117860B1 (fr) | Procede pour la realisation d'un materiau non-tissu complexe et materiau ainsi obtenu | |
| EP1246958B1 (fr) | Procede pour la realisation d'un materiau non tisse et materiau ainsi obtenu | |
| EP1192306B1 (fr) | Procede pour la realisation d'un materiau non tisse, installation pour sa mise en oeuvre et non tisse ainsi obtenu | |
| EP1226297B1 (fr) | Procede pour la realisation de nappes non tissees dont la cohesion est obtenue par l'action de jets de fluide | |
| BE897109A (fr) | Etoffe de barrage impermeable et absorbante comportant des films et des nappes fibreuses et procede pour sa fabrication | |
| FR2705698A1 (fr) | Procédé de fabrication d'une nappe de non-tissé constituée de filaments continus liés entre eux et nappe ainsi obtenue. | |
| EP1874991A1 (fr) | Materiau composite non tisse integre et hydroentremele | |
| EP0826811B1 (fr) | Matériau complexe nontisse absorbant comportant une face souple et une face rugueuse, et procédé pour son obtention | |
| CA2061805C (fr) | Textile d'entoilage composite et son procede de fabrication | |
| FR2588285A1 (fr) | Textile non tisse multicouche | |
| WO1978000012A1 (fr) | Materiau de garnissage fibreux et procede pour son obtention | |
| JP2002285466A (ja) | 不織材料の製造方法 | |
| US20030207636A1 (en) | Nonwoven laminate wiping product and proces for its manufacture | |
| CA2080487C (fr) | Procede d'impregnation d'une nappe textile | |
| EP1027499B2 (fr) | Materiau de type voile thermosoude pour infusions et procede de fabrication | |
| FR2588286A1 (fr) | Voile non tisse ayant une douceur amelioree | |
| EP0371847B1 (fr) | Matériau composite à base de fibres minérales, dispositif d'obtention et application du matériau composite | |
| US7290314B2 (en) | Method for producing a complex nonwoven fabric and resulting novel fabric | |
| EP1261768A1 (fr) | Produit d'essuyage lamine non tisse et procede de fabrication | |
| FR2529918A1 (fr) | Procede pour la fabrication de non-tisses aiguilletes en fibres minerales, en particulier refractaires, et non-tisses realises selon ce procede | |
| EP0466563B1 (fr) | Entoilage thermocollant à base de microfibres et procédé pour l'obtenir | |
| WO1996023922A1 (fr) | Procede de traitement d'une nappe de fibres cellulosiques | |
| EP1851372B1 (fr) | Tampon fibreux imprégné | |
| EP1497488B1 (fr) | Non tisse a nappes partiellement liees et ses procede et machine de production. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19920603 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FR GB GR IT LI LU NL SE |
|
| 17Q | First examination report despatched |
Effective date: 19941121 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: KAYSERSBERG |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: KAYSERSBERG |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FR GB GR IT LI LU NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19960828 Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19960828 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19960828 Ref country code: DK Effective date: 19960828 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19960828 |
|
| REF | Corresponds to: |
Ref document number: 141964 Country of ref document: AT Date of ref document: 19960915 Kind code of ref document: T |
|
| ITF | It: translation for a ep patent filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19960906 |
|
| REF | Corresponds to: |
Ref document number: 69121694 Country of ref document: DE Date of ref document: 19961002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19961031 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19961031 Ref country code: BE Effective date: 19961031 Ref country code: CH Effective date: 19961031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19961128 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| BERE | Be: lapsed |
Owner name: KAYSERSBERG Effective date: 19961031 |
|
| PLBQ | Unpublished change to opponent data |
Free format text: ORIGINAL CODE: EPIDOS OPPO |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLBF | Reply of patent proprietor to notice(s) of opposition |
Free format text: ORIGINAL CODE: EPIDOS OBSO |
|
| PLBF | Reply of patent proprietor to notice(s) of opposition |
Free format text: ORIGINAL CODE: EPIDOS OBSO |
|
| 26 | Opposition filed |
Opponent name: THE PROCTER & GAMBLE COMPANY Effective date: 19970528 |
|
| PLBF | Reply of patent proprietor to notice(s) of opposition |
Free format text: ORIGINAL CODE: EPIDOS OBSO |
|
| PLBF | Reply of patent proprietor to notice(s) of opposition |
Free format text: ORIGINAL CODE: EPIDOS OBSO |
|
| PLBQ | Unpublished change to opponent data |
Free format text: ORIGINAL CODE: EPIDOS OPPO |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: FORT JAMES FRANCE |
|
| R26 | Opposition filed (corrected) |
Opponent name: THE PROCTER & GAMBLE COMPANY Effective date: 19970528 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CJ Ref country code: FR Ref legal event code: CD |
|
| PLBO | Opposition rejected |
Free format text: ORIGINAL CODE: EPIDOS REJO |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 19981130 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20090928 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20091118 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20091007 Year of fee payment: 19 Ref country code: FR Payment date: 20091201 Year of fee payment: 19 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20101004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101102 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20110630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101004 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69121694 Country of ref document: DE Effective date: 20110502 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110502 |