EP0672471A1 - Verfahren und Vorrichtung zum Walzen von Bändern - Google Patents
Verfahren und Vorrichtung zum Walzen von Bändern Download PDFInfo
- Publication number
- EP0672471A1 EP0672471A1 EP95103289A EP95103289A EP0672471A1 EP 0672471 A1 EP0672471 A1 EP 0672471A1 EP 95103289 A EP95103289 A EP 95103289A EP 95103289 A EP95103289 A EP 95103289A EP 0672471 A1 EP0672471 A1 EP 0672471A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rollers
- diameter
- radius
- rolls
- end regions
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000005096 rolling process Methods 0.000 title claims abstract description 17
- 238000000034 method Methods 0.000 title claims description 3
- 238000010438 heat treatment Methods 0.000 claims description 3
- 238000006073 displacement reaction Methods 0.000 description 3
- 239000011324 bead Substances 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 238000001816 cooling Methods 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000005489 elastic deformation Effects 0.000 description 1
- 230000002787 reinforcement Effects 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B13/00—Metal-rolling stands, i.e. an assembly composed of a stand frame, rolls, and accessories
- B21B13/14—Metal-rolling stands, i.e. an assembly composed of a stand frame, rolls, and accessories having counter-pressure devices acting on rolls to inhibit deflection of same under load; Back-up rolls
- B21B13/142—Metal-rolling stands, i.e. an assembly composed of a stand frame, rolls, and accessories having counter-pressure devices acting on rolls to inhibit deflection of same under load; Back-up rolls by axially shifting the rolls, e.g. rolls with tapered ends or with a curved contour for continuously-variable crown CVC
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B27/00—Rolls, roll alloys or roll fabrication; Lubricating, cooling or heating rolls while in use
- B21B27/02—Shape or construction of rolls
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B37/00—Control devices or methods specially adapted for metal-rolling mills or the work produced thereby
- B21B37/28—Control of flatness or profile during rolling of strip, sheets or plates
- B21B37/40—Control of flatness or profile during rolling of strip, sheets or plates using axial shifting of the rolls
Definitions
- the invention relates to a method and a device for rolling strips with axially displaceable, in particular low-wear rollers.
- thermal crowning of the rolls which increases with the throughput of the rolling stock through a stand.
- the thermal crowning decreases from the areas of the rolls that lie in the middle of the rolling stock to the edges of the rolling stock. As a result, rolling stock with edge elevation is rolled as the rolling stock throughput increases.
- thermal crowning It is e.g. known to achieve an equalization of both the thermal crowning and especially the wear by cyclical, axial displacement of the rollers.
- the thermal crowning can be counteracted by cooling or heating the rollers, however, these measures cannot prevent thermal crowning.
- the rolling program structure (width, material thickness) is subject to strict rules. However, it is desirable to be able to compile the rolling programs more freely.
- roller materials are used whose wear is negligibly small, then at least one influencing variable which interferes with the rolling programs has been minimized. Since roller wear basically counteracts increasing thermal crowning, this becomes even more noticeable when rolling with low-wear rollers.
- the invention is therefore based on the object of demonstrating an actuator in order to counteract the annoying thermal crowning effect simply and inexpensively in order to be able to design rolling plans more freely.
- rollers in their end regions with enlarged radii are displaced relative to one another in such a way that the width of the rolled strip is in contact with regions of the smaller radius and that with increasing heating and thus thermal crowning by displacing the rollers in opposite directions Areas of their larger radius' are pushed over edge areas of the rolled strip. It is thereby achieved that the edge region elevations of the band, which would occur due to the increasing thermal crowning, are eliminated.
- the amount of displacement can e.g. be determined in a computer which determines the thermal crowning online using a calculation model, values about the contour of the roller, its elastic deformation, etc. being used in order to set an optimal displacement position and thus a desired strip contour.
- the object is achieved in that the rollers of a pair of rollers are each designed in the end regions of their bales with a diameter which is increased compared to their central region.
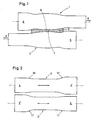
- the strip 3 to be rolled is arranged between the work rolls 1, 2.
- the upper work roll 1 has on its right side a diameter which corresponds to the diameter of the left side of the lower work roll 2. Shown greatly exaggerated, the two work rolls 1, 2 have slightly larger diameters at their other two ends 4, 5. In the contact area of the belt 3 with the work rolls 1, 2, the thermal crowning 6, 7 of the rolls 1, 2 is also shown greatly exaggerated. The work rolls 1, 2 are so opposite in the direction of the arrows 8, 9 shifted against each other that their edge regions 4, 5 of larger diameter are displaced over the edge regions of the rolled strip.
- the band 3 has less strong beads in its edge areas than the beads to be expected would be noticed without the reinforcement of the roller end area.
- FIG. 2 shows an upper work roll 1 'and a lower work roll 2', the bale ends 4, 4 'and 5, 5' have different diameters.
- the slopes 10, 10 ', 11, 11' are also different, so that different thermal crowning can be compensated.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Geometry (AREA)
- Metal Rolling (AREA)
- Reduction Rolling/Reduction Stand/Operation Of Reduction Machine (AREA)
- Control Of Metal Rolling (AREA)
- Manufacturing And Processing Devices For Dough (AREA)
- Laminated Bodies (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
- Rolls And Other Rotary Bodies (AREA)
Abstract
Description
- Die Erfindung betrifft ein Verfahren und eine Vorrichtung zum Walzen von Bändern mit axial verschiebbaren, insbesondere verschleißarmen Walzen.
- Beim Walzen von Band sind mehrere gravierende Einflußgrößen bekannt, die das Bandprofil und die Bandplanheit beeinflussen. Eine dieser Einflußgrößen ist die thermische Bombierung der Walzen, die mit steigendem Walzgutdurchsatz durch ein Gerüst zunimmt. Die thermisch Bombierung nimmt von den Bereichen der Walzen, die in der Walzgutmitte liegen zu den Walzgutkanten hin ab. Damit wird mit zunehmendem Walzgutdurchsatz Walzgut mit Kantenüberhöhung gewalzt.
- Eine weitere Einflußgröße ist der Walzenverschleiß, der vornehmlich dort auftritt, wo das Walzband mit den Walzen in Kontakt kommt, und der den Durchmesser der Walzen abnehmen läßt.
- Es ist z.B. bekannt, durch zyklisches, axiales Verschieben der Walzen eine Vergleichmäßigung sowohl der thermischen Bombierung als vor allem auch des Verschleißes zu erreichen. Durch Kühlung bzw. Heizung der Walzen kann der thermischen Bombierung entgegengewirkt werden, eine Verhinderung der thermischen Bombierung ist mit diesen Maßnahmen jedoch nicht möglich.
- Bedingt durch das Auftreten der thermischen Bombierung und des Arbeitswalzenverschleißes unterliegt der Walzprogrammaufbau (Breite, Materialdicke) strengen Regeln. Wunsch ist es jedoch, die Walzprogramme freier zusammenstellen zu können.
- Werden Walzenwerkstoffe eingesetzt, deren Verschleiß vernachlässigbar klein ist, so ist zumindest eine die Walzprogramme störende Einflußgröße minimiert worden. Da der Walzenverschleiß im Grunde entgegen der zunehmenden thermischen Bombierung wirkt, macht sich diese beim Walzen mit verschleißarmen Walzen noch stärker bemerkbar.
- Der Erfindung liegt daher die Aufgabe zugrunde, ein Stellglied aufzuzeigen, um den störenden, thermischen Bombierungs-Effekt einfach und kostengünstig entgegenzuwirken, um Walzpläne freier gestalten zu können.
- Dazu wird verfahrensmäßig vorgeschlagen, daß jeweils in ihren Endbereichen mit vergrößerten Radien ausgeführte Walzen derart gegeneinander verschoben werden, daß das Walzband in seiner Breite jeweils mit Bereichen des geringeren Radius' in Kontakt stehen und daß mit zunehmender Erwärmung und damit thermischer Bombierung durch gegensinniges Verschieben der Walzen Bereiche ihres größeren Radius' über Randbereiche des Walzbandes geschoben werden. Dadurch wird erreicht, daß die Randbereichüberhöhungen des Bandes, die durch die steigende thermische Bombierung eintreten würden, beseitigt werden.
- Das Maß der Verschiebung kann z.B. in einem Rechner ermittelt werden, der die thermische Bombierung anhand eines Rechenmodells online bestimmt, wobei Werte über die Kontur der Walze, deren elastische Deformation usw. herangezogen werden, um eine optimale Verschiebeposition und damit eine gewünschte Bandkontur einzustellen.
- Vorrichtungsmäßig wird die Aufgabe dadurch gelöst, daß die Walzen eines Walzenpaares jeweils in den Endbereichen ihrer Ballen mit gegenüber deren Mittelbereich erhöhtem Durchmesser ausgeführt sind.
- Von Vorteil ist, wenn der Durchmesserzuwachs nach Anspruch 3 im Bandkantenbereich stetig ist.
- Werden die Merkmale des Anspruchs 4 verwirklicht, so lassen sich unterschiedliche maximale Randbereichüberhöhungen kompensieren.
- Weitere vorteilhafte Ausgestaltungen ergeben sich nach den Ansprüchen 5 bis 7.
- Die beste Kompensation der Randbereichüberhöhungen des Walzbandes ergeben sich, wenn die Arbeitswalzen eines Gerüsts nach den Merkmalen eines der Ansprüche 2 bis 7 ausgebildet sind. Ein Ausführungsbeispiel der Erfindung wird anhand einer Zeichnung näher erläutert. Dabei zeigen
- Figur 1
- die Prinzipdarstellung eines Arbeitswalzenpaares während des Walzvorgangs, wobei die thermische Bombierung und der erfindungsgemäße Walzenschliff zu erkennen ist, die beim Walzvorgang übliche Walzenabplattung und Walzendurchbiegung jedoch nicht berücksichtigt ist, und
- Figur 2
- ein Arbeitswalzenpaar mit beidseitig verstärkten Walzen.
- Der Figur 1 ist eine obere Arbeitswalze 1 und eine untere Arbeitswalze 2 zu entnehmen. Zwischen den Arbeitswalzen 1, 2 ist das zu walzende Band 3 angeordnet.
- Die obere Arbeitswalze 1 weist an ihrer rechten Seite einen Durchmesser auf, der mit dem Durchmesser der linken Seite der unteren Arbeitswalze 2 übereinstimmt. Stark überhöht dargestellt weisen die beiden Arbeitswalzen 1, 2 an ihren beiden anderen Enden 4, 5 geringfügig größere Durchmesser auf. Im Kontaktbereich des Bandes 3 mit den Arbeitswalzen 1, 2 ist ebenfalls stark überhöht dargestellt die thermisch Bombierung 6, 7 der Walzen 1, 2 zu erkennen. Die Arbeitswalzen 1, 2 sind in Richtung der Pfeile 8, 9 so entgegengesetzt gegeneinander verschoben, daß deren Randbereiche 4, 5 größeren Durchmessers über die Randbereiche des Walzbandes verschoben sind.
- Es ist zu erkennen, daß das Band 3 in seinen Kantenbereichen weniger starke Wulste aufweist, als die zu erwartenden Wulste ohne die Verstärkung der Walzenendbereich auffallen würde.
- Die Steilheit des Übergangs vom kleinen zum größeren Durchmesser der Walzen sowie die Differenz zwischen dem kleinen und dem großen Durchmesser ist abhängig von der zu erwartenden thermischen Bombierung 6, 7.
- Figur 2 zeigt eine obere Arbeitswalze 1' sowie eine untere Arbeitswalze 2', deren Ballenenden 4, 4' bzw. 5, 5' unterschiedliche Durchmesser aufweisen. Auch die Steigungen 10, 10', 11, 11' sind unterschiedlich, so daß unterschiedliche thermische Bombierungen kompensierbar sind.
-
- 1
- Obere Arbeitswalze
- 2
- untere Arbeitswalze
- 3
- Walzband
- 4
- verstärktes Walzenende
- 5
- verstärktes Walzenende
- 6
- thermische Bombierung
- 7
- thermische Bombierung
- 8
- Verschiebepfeil
- 9
- Verschiebepfeil
- 10
- Steigung
- 11
- Steigung
Claims (8)
- Verfahren zum Walzen von Bändern (3) mit axial verschiebbaren, insbesondere verschleißarmen Walzen (1, 2),
dadurch gekennzeichnet,
daß jeweils in ihren Endbereichen (4, 5 bzw. 4', 5') mit vergrößerten Radien ausgeführte Walzen (1, 2; 1', 2') derart gegeneinander verschoben werden, daß das Walzband (3) in seiner Breite jeweils mit Bereichen des geringeren Radius' in Kontakt stehen und daß mit zunehmender Erwärmung und mit thermischer Bombierung (6, 7) durch gegensinniges Verschieben (8, 9) der Walzen (1, 2; 1', 2') Bereiche (4, 5 bzw. 4', 5') ihres größeren Radius' über Randbereiche des Walzbandes (3) geschoben werden. - Vorrichtung zum Walzen von Bändern (3) mit axial verschiebbaren, insbesondere verschleißarmen Walzen (1, 2; 1', 2'),
dadurch gekennzeichnet,
daß die Walzen (1, 2; 1', 2') eines Walzpaares jeweils in den Endbereichen (4, 5 bzw. 4', 5') ihrer Ballen mit gegenüber deren Mittelbereich erhöhten Durchmessern ausgeführt sind. - Vorrichtung nach Anspruch 2,
dadurch gekennzeichnet,
daß der Durchmesser der Walzen (1, 2; 1', 2') von deren Mittelbereich mit dem geringsten Durchmesser zum Endbereich (4, 5; 4', 5') der Walzen (1, 2; 1', 2') hin ansteigt. - Vorrichtung nach Anspruch 3,
dadurch gekennzeichnet,
daß die Durchmesser der Endbereiche (4, 4'; 5, 5') einer Walze unterschiedlich sind und daß die Durchmesser der Endbereiche der zweiten Walze des Walzenpaares entsprechend umgekehrte Durchmesserverhältnisse aufweisen. - Vorrichtung nach Anspruch 3,
dadurch gekennzeichnet,
daß nur jeweils eines der Ballenenden (4, 5) mit erhöhtem Durchmesser ausgeführt ist, und daß sie spiegelbildlich so angeordnet sind, daß eines der verstärkten Ballenenden (4, 5) zur Bedienungsseite und das andere zur Antriebsseite des die Walzen aufnehmenden Gerüstes weisen. - Vorrichtung nach einem der Ansprüche 1 bis 5,
dadurch gekennzeichnet,
daß die maximale Differenz der Radien der Durchmesserbereiche in der Größenordnung des im Betrieb als thermische Bombierung (6, 7) zu erwartenden Radius-Anstieges liegt. - Vorrichtung nach Anspruch 6,
dadurch gekennzeichnet,
daß die Radiusdifferenz den maximalen Radiusanstieg der thermischen Bombierung (6, 7) übersteigt. - Vorrichtung nach einem der Ansprüche 2 bis 7,
dadurch gekennzeichnet,
daß die Arbeitswalzen (1, 2; 1', 2') des die Walzen aufnehmenden Gerüsts mit verstärkten Ballenenden (4, 5; 4', 5') ausgeführt sind.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4409299A DE4409299A1 (de) | 1994-03-18 | 1994-03-18 | Verfahren und Vorrichtung zum Walzen von Bändern |
| DE4409299 | 1994-03-18 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0672471A1 true EP0672471A1 (de) | 1995-09-20 |
| EP0672471B1 EP0672471B1 (de) | 1999-12-08 |
Family
ID=6513177
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95103289A Expired - Lifetime EP0672471B1 (de) | 1994-03-18 | 1995-03-08 | Verfahren und Vorrichtung zum Walzen von Bändern |
Country Status (9)
| Country | Link |
|---|---|
| US (1) | US5697244A (de) |
| EP (1) | EP0672471B1 (de) |
| JP (1) | JPH0839120A (de) |
| KR (1) | KR100323469B1 (de) |
| AT (1) | ATE187368T1 (de) |
| DE (2) | DE4409299A1 (de) |
| ES (1) | ES2140572T3 (de) |
| FI (1) | FI109771B (de) |
| TW (1) | TW284714B (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7434435B2 (en) | 2003-09-04 | 2008-10-14 | Sms Demag Ag | Method and device for applying an adjustable tensile-stress distribution, in particular in the edge regions of cold-rolled metal strips |
| RU2413584C1 (ru) * | 2009-10-28 | 2011-03-10 | Открытое акционерное общество Акционерная холдинговая компания "Всероссийский научно-исследовательский и проектно-конструкторский институт металлургического машиностроения имени академика Целикова" (ОАО АХК "ВНИИМЕТМАШ") | Способ и литейно-прокатный комплекс для изготовления фольги из цветных металлов и сплавов |
| CN102744260A (zh) * | 2012-07-09 | 2012-10-24 | 首钢总公司 | 一种兼顾带钢凸度与边降控制的工作辊及其辊形设计方法 |
Families Citing this family (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19719318C2 (de) * | 1997-05-08 | 2003-06-12 | Sms Demag Ag | Verfahren zur Beeinflussung der Bandkontur im Kantenbereich eines Walzenbandes |
| JP2005052864A (ja) * | 2003-08-04 | 2005-03-03 | Ishikawajima Harima Heavy Ind Co Ltd | 帯板製造設備 |
| DE102006051728B4 (de) * | 2006-10-30 | 2013-11-21 | Outokumpu Nirosta Gmbh | Verfahren zum Walzen von Metallbändern, inbesondere von Stahlbändern |
| US8607848B2 (en) * | 2008-08-05 | 2013-12-17 | Nucor Corporation | Method for casting metal strip with dynamic crown control |
| US8607847B2 (en) * | 2008-08-05 | 2013-12-17 | Nucor Corporation | Method for casting metal strip with dynamic crown control |
| US8505611B2 (en) | 2011-06-10 | 2013-08-13 | Castrip, Llc | Twin roll continuous caster |
| CN205659983U (zh) | 2016-06-15 | 2016-10-26 | 日照宝华新材料有限公司 | 一种esp生产线用长公里数轧制辊 |
| KR101868064B1 (ko) * | 2018-02-28 | 2018-07-19 | 보 현 이 | 엠보싱 금속판의 양측면 용접을 용이하게 하는 엠보싱 파이프 제조장치 및 이를 이용한 엠보싱 파이프 제조방법 |
| CN114769325B (zh) * | 2022-04-26 | 2023-07-25 | 马鞍山钢铁股份有限公司 | 一种热连轧cvc工作辊窜辊的控制方法 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS58212802A (ja) * | 1982-06-02 | 1983-12-10 | Kawasaki Steel Corp | 圧延機 |
| JPS6152915A (ja) * | 1984-08-23 | 1986-03-15 | Kawasaki Steel Corp | ワ−クロ−ルシフトミルによる板圧延方法 |
| GB2198981A (en) * | 1986-12-23 | 1988-06-29 | Davy Mckee | Axially-adjustable rolls |
| DE3919285A1 (de) * | 1988-08-29 | 1990-03-01 | Sendzimir Inc T | Vorrichtung und verfahren zum kaltwalzen eines metallbandes |
| JPH06198313A (ja) * | 1992-12-28 | 1994-07-19 | Kawasaki Steel Corp | 熱間仕上げ圧延機用ロール |
Family Cites Families (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3997370A (en) * | 1975-11-17 | 1976-12-14 | Bethlehem Steel Corporation | Method of hot reducing ferrous and ferrous alloy products with composite martensitic nodular cast chill iron rolls |
| JPS5630014A (en) * | 1979-08-17 | 1981-03-26 | Kobe Steel Ltd | Rolling mill |
| DE3038865C1 (de) * | 1980-10-15 | 1982-12-23 | SMS Schloemann-Siemag AG, 4000 Düsseldorf | Walzgeruest mit axial verschiebbaren Walzen |
| JPS61296904A (ja) * | 1985-06-26 | 1986-12-27 | Nippon Steel Corp | 圧延機 |
| US4656859A (en) * | 1985-08-21 | 1987-04-14 | Wean United, Inc. | Rolling mill stand employing variable crown rolls and associated method |
| JPS6293017A (ja) * | 1985-10-21 | 1987-04-28 | Nippon Steel Corp | 圧延における板プロフイル制御方法 |
| JPH0688053B2 (ja) * | 1986-05-30 | 1994-11-09 | 川崎重工業株式会社 | 圧延方法 |
| DE3620197A1 (de) * | 1986-06-16 | 1987-12-17 | Schloemann Siemag Ag | Walzwerk zur herstellung eines walzgutes, insbesondere eines walzbandes |
| JPH0622725B2 (ja) * | 1987-01-12 | 1994-03-30 | 株式会社日立製作所 | 圧延機の制御方法 |
| JP2616917B2 (ja) * | 1987-01-24 | 1997-06-04 | 株式会社日立製作所 | ロールシフト圧延機による圧延方法 |
| DE3712043C2 (de) * | 1987-04-09 | 1995-04-13 | Schloemann Siemag Ag | Walzgerüst mit axial verschiebbaren Walzen |
| JPH0270804U (de) * | 1988-11-21 | 1990-05-30 | ||
| JPH0620562B2 (ja) * | 1988-12-28 | 1994-03-23 | 住友金属工業株式会社 | 熱間圧延時の板クラウン制御方法 |
| JPH06277727A (ja) * | 1993-03-25 | 1994-10-04 | Kobe Steel Ltd | 板クラウン制御方法 |
| JP3317311B2 (ja) * | 1993-06-24 | 2002-08-26 | 石川島播磨重工業株式会社 | ロールシフト式圧延機用ロールとこれを用いた圧延機 |
-
1994
- 1994-03-18 DE DE4409299A patent/DE4409299A1/de not_active Withdrawn
-
1995
- 1995-02-28 TW TW084101826A patent/TW284714B/zh active
- 1995-03-08 AT AT95103289T patent/ATE187368T1/de active
- 1995-03-08 ES ES95103289T patent/ES2140572T3/es not_active Expired - Lifetime
- 1995-03-08 EP EP95103289A patent/EP0672471B1/de not_active Expired - Lifetime
- 1995-03-08 DE DE59507356T patent/DE59507356D1/de not_active Expired - Lifetime
- 1995-03-15 JP JP7056051A patent/JPH0839120A/ja active Pending
- 1995-03-16 FI FI951228A patent/FI109771B/fi not_active IP Right Cessation
- 1995-03-17 US US08/406,032 patent/US5697244A/en not_active Expired - Lifetime
- 1995-03-18 KR KR1019950005711A patent/KR100323469B1/ko not_active Expired - Fee Related
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS58212802A (ja) * | 1982-06-02 | 1983-12-10 | Kawasaki Steel Corp | 圧延機 |
| JPS6152915A (ja) * | 1984-08-23 | 1986-03-15 | Kawasaki Steel Corp | ワ−クロ−ルシフトミルによる板圧延方法 |
| GB2198981A (en) * | 1986-12-23 | 1988-06-29 | Davy Mckee | Axially-adjustable rolls |
| DE3919285A1 (de) * | 1988-08-29 | 1990-03-01 | Sendzimir Inc T | Vorrichtung und verfahren zum kaltwalzen eines metallbandes |
| JPH06198313A (ja) * | 1992-12-28 | 1994-07-19 | Kawasaki Steel Corp | 熱間仕上げ圧延機用ロール |
Non-Patent Citations (3)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 10, no. 211 (M - 501) 24 July 1986 (1986-07-24) * |
| PATENT ABSTRACTS OF JAPAN vol. 18, no. 550 (M - 1690) 20 October 1994 (1994-10-20) * |
| PATENT ABSTRACTS OF JAPAN vol. 8, no. 61 (M - 284) 23 March 1984 (1984-03-23) * |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7434435B2 (en) | 2003-09-04 | 2008-10-14 | Sms Demag Ag | Method and device for applying an adjustable tensile-stress distribution, in particular in the edge regions of cold-rolled metal strips |
| RU2413584C1 (ru) * | 2009-10-28 | 2011-03-10 | Открытое акционерное общество Акционерная холдинговая компания "Всероссийский научно-исследовательский и проектно-конструкторский институт металлургического машиностроения имени академика Целикова" (ОАО АХК "ВНИИМЕТМАШ") | Способ и литейно-прокатный комплекс для изготовления фольги из цветных металлов и сплавов |
| CN102744260A (zh) * | 2012-07-09 | 2012-10-24 | 首钢总公司 | 一种兼顾带钢凸度与边降控制的工作辊及其辊形设计方法 |
| CN102744260B (zh) * | 2012-07-09 | 2014-05-28 | 首钢总公司 | 一种兼顾带钢凸度与边降控制的工作辊及其辊形设计方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| US5697244A (en) | 1997-12-16 |
| ATE187368T1 (de) | 1999-12-15 |
| DE59507356D1 (de) | 2000-01-13 |
| KR100323469B1 (ko) | 2002-06-24 |
| FI109771B (fi) | 2002-10-15 |
| EP0672471B1 (de) | 1999-12-08 |
| FI951228L (fi) | 1995-09-19 |
| DE4409299A1 (de) | 1995-09-21 |
| FI951228A0 (fi) | 1995-03-16 |
| KR950031263A (ko) | 1995-12-18 |
| ES2140572T3 (es) | 2000-03-01 |
| JPH0839120A (ja) | 1996-02-13 |
| TW284714B (de) | 1996-09-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3038865C1 (de) | Walzgeruest mit axial verschiebbaren Walzen | |
| EP0091540B1 (de) | Walzgerüst mit axial verschiebbaren Walzen | |
| DE4309986A1 (de) | Verfahren und Vorrichtung zum Walzen eines Walzbandes | |
| DE2206912A1 (de) | Walzgerüst | |
| EP0560091A1 (de) | Verfahren und Vorrichtung zum Richten von H-förmigen Trägerprofilen | |
| EP1181991A2 (de) | Verfahren und Vorrichtung zum flexiblen Walzen eines Metallbandes | |
| DE3624241C2 (de) | Verfahren zum Betrieb eines Walzwerkes zur Herstellung eines Walzbandes | |
| DE3127190C2 (de) | ||
| EP0672471B1 (de) | Verfahren und Vorrichtung zum Walzen von Bändern | |
| EP0587995B1 (de) | Rollensatz mit zumindest zwei Umlenkrollen für die S-förmige Umlenkung dünner Metallbänder | |
| DE19736767C2 (de) | Walzgerüst zum Walzen von Bändern | |
| DE69702173T3 (de) | Walzwerke | |
| DE102009012929B3 (de) | Richtwalzenanlage zum Planrichten von metallischem Gut, insbesondere von Metallbändern und Blechen | |
| EP0255714B1 (de) | Vielwalzen-Walzgerüst mit paarweise gegensinnig verschiebbaren, verjüngte Enden aufweisenden Zwischenwalzen | |
| DE69209632T2 (de) | Verfahren und Vorrichtung zum Walzen von Metallen zur Herstellung von rundem Stabmaterial oder Walzdraht aus rundem Stab- oder Drahtmaterial mit grösserem Durchmesser | |
| EP1197272B1 (de) | Zweiwalzen-Rundmaschine sowie Verfahren zum Runden von Blechen | |
| DE102010049908B4 (de) | Vielwalzen-Walzwerk vom Cluster-Typ | |
| EP0102014B1 (de) | Walzgerüst zum Auswalzen von Bandmaterial unterschiedlicher Breite | |
| DE69201395T2 (de) | Streckrollen-Richtmaschine. | |
| DE69009102T3 (de) | Vielwalzengerüst. | |
| DE3302333C2 (de) | ||
| EP0534281B1 (de) | Verfahren und Anordnung zur Herstellung von Blechprofilen | |
| EP0173906A1 (de) | Verfahren und Vorrichtung zum Walzen von Flachmaterial | |
| DE102006025751B4 (de) | Verfahren zur Abdichtung einer Vakuumkammer und Schleuseneinrichtung für eine Vakuumkammer | |
| DE3720610C2 (de) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19950322 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE DE ES FR GB IT NL SE |
|
| 17Q | First examination report despatched |
Effective date: 19970204 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE DE ES FR GB IT NL SE |
|
| REF | Corresponds to: |
Ref document number: 187368 Country of ref document: AT Date of ref document: 19991215 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 59507356 Country of ref document: DE Date of ref document: 20000113 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2140572 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20000222 |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: SMS DEMAG AG |
|
| NLT2 | Nl: modifications (of names), taken from the european patent patent bulletin |
Owner name: SMS DEMAG AG |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20110316 Year of fee payment: 17 Ref country code: FR Payment date: 20110404 Year of fee payment: 17 Ref country code: SE Payment date: 20110314 Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20110325 Year of fee payment: 17 Ref country code: GB Payment date: 20110321 Year of fee payment: 17 Ref country code: BE Payment date: 20110311 Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120329 Year of fee payment: 18 |
|
| BERE | Be: lapsed |
Owner name: SCHLOEMANN-SIEMAG A.G. *SMS Effective date: 20120331 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20121001 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120309 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20120308 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20121130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120331 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120402 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120308 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121001 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20130321 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20130313 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20130710 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120309 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59507356 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 187368 Country of ref document: AT Kind code of ref document: T Effective date: 20140308 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59507356 Country of ref document: DE Effective date: 20141001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140308 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140308 |