EP0674971A1 - Verfahren zum Bearbeiten eines Werkstückes - Google Patents
Verfahren zum Bearbeiten eines Werkstückes Download PDFInfo
- Publication number
- EP0674971A1 EP0674971A1 EP95301920A EP95301920A EP0674971A1 EP 0674971 A1 EP0674971 A1 EP 0674971A1 EP 95301920 A EP95301920 A EP 95301920A EP 95301920 A EP95301920 A EP 95301920A EP 0674971 A1 EP0674971 A1 EP 0674971A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- workpiece
- stem
- head
- grinding
- ground
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B5/00—Machines or devices designed for grinding surfaces of revolution on work, including those which also grind adjacent plane surfaces; Accessories therefor
- B24B5/18—Machines or devices designed for grinding surfaces of revolution on work, including those which also grind adjacent plane surfaces; Accessories therefor involving centreless means for supporting, guiding, floating or rotating work
- B24B5/28—Machines or devices designed for grinding surfaces of revolution on work, including those which also grind adjacent plane surfaces; Accessories therefor involving centreless means for supporting, guiding, floating or rotating work for grinding outer surfaces concentrically to bores, involving additional centering means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B15/00—Machines or devices designed for grinding seat surfaces; Accessories therefor
- B24B15/04—Machines or devices designed for grinding seat surfaces; Accessories therefor on valve members
Definitions
- the present invention relates to a method of processing a workpiece to make a poppe-t valve such as an engine valve used in an internal combustion engine.
- Material is molded by forging to make a workpiece which comprises a larger diameter head and a stem, and a poppet valve such as an engine valve is manufactured through various mechanical processing steps, which include cutting the end of the stem; grinding the outer circumferential surface of the stem; chamfering the end of the stem; cutting a cotter groove; and grinding a head.
- a poppet valve such as an engine valve
- the end of the stem is cut to define the total length of the forged workpiece, and then, the outer circumferential surface of the stem is ground.
- the rotary shafts of the rotating grinding and adjusting wheels are not in parallel, so that thrust force is applied to the workpiece in grinding in a direction of retracting direction, while the outer circumferential surface of the stem is ground such that the head is projected between the grinding and adjusting wheels, so that the end of the workpiece is engaged with a stopper between the grinding and adjusting wheels and is thus positioned.
- the ground range is determined between the engaged end and the front end of the grinding wheel.
- the length of the stem is different as forged material (at largest about 5 cm is variable in the total length of 10 cm)
- the ground range is determined from the engaged end, the distance is variable between the head and the ground portion. So, prior to grinding, the stem must be cut to determine the total length of the workpiece.
- forged material is rotatably supported by a plurality of support rollers, and the end face of the head is engaged with a loader head and positioned.
- the workpiece itself is rotated, and the stem of the workpiece is cut by a rotating grindstone.
- black skin of the forged material is sticked on the outer circumferential surface of the support roller, thereby causing unsmooth rotation of the support rollers or workpiece, and increasing wear of the outer circumferential surface of the support roller.
- the black skin is formed by a mold releasing agent which is burnt on the material during hot forging.
- the stem which has bending or warping is supported by the support roller, and a little deviation occurs in the total length, thereby decreasing accuracy in the ground range when the stem is ground.
- a method of processing a workpiece which comprises a larger diameter head and a stem, the method comprising grinding the outer circumferential surface of the stem, followed by cutting the stem at a certain distance from the end of the head.
- the stem of the forged workpiece is ground first to correct bending or warping, and black skin formed in forging is removed. Then, the workpiece is cut at a certain distance from the end of the head, thereby preventing sticking of the black skin to the support roller when the stem is cut, and causing no malfunction owing to bending of the stem in the total length of the workpiece.
- a stem 1a is put between grinding and adjusting wheels 2 and 3 of a centerless grinder as shown in a left portion of Fig. 1 and Fig. 2.
- the workpiece 1 to be processed is put on a workpiece support plate, and the space is reduced, so that the stem la of the workpiece 1 is put between the grinding and adjusting wheels 2 and 3.
- the grinding wheel 2 is rotated at high speed by a first motor 4 via a first rotary shaft 5.
- the adjusting wheel 3 is rotated by a second motor 6 via a second rotary shaft 7 in the same direction as that of the grinding wheel 2 at speed lower than that of the grinding wheel 2, so that the workpiece 1 is rotated in a direction opposite to the grinding wheel 2 on the workpiece support plate, thereby grinding the outer circumferential surface of the stem 1a.
- a head 1b which has diameter larger than the stem 1a is provided at one end of the stem 1a of the workpiece 1 and is projected forward on the grinding and adjusting wheels 2 and 3 as shown in Figs. 1 and 2.
- the end face of the head 1b is engaged with a loader head 8 as a stopper
- the rear end face of the stem 1a is engaged with a pusher 9 which is inserted between the grinding and adjusting wheels 2 and 3
- the loader head 8 comprises a support shaft 8a and a bottom-having cylindrical head 8b which is connected to the end of the shaft 8a by a spherical bearing(not shown) rotatably and somewhat shakably.
- the outer circumferential surface of the stem 1a is thus ground. Even if there is variation in length of the stem 1a or even if rearward thrust force is given to the workpiece 1, the workpiece 1 is ground at backward portion at a certain distance from the end face of the head 1b.
- the rotary shaft 7 of the adjusting wheel 3 is inclined upward in a front direction with respect to the rotary shaft 5 of the grinding wheel 2, so that rearward thrust force is applied to the workpiece 1. Therefore, forward pressing force to the workpiece 1 by the pusher 9 must be larger than the thrust force. But, the rotary shaft 7 is slightly inclined downward in a forward direction, so that forward thrust force is applied to the workpiece, which is pressed towards the loader head 8 by the thrust force, so that pressing force to the workpiece 1 by the pusher 9 may be relatively small.
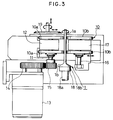
- the workpiece 1 is placed between two driving rollers 10a, 10b and two driven rollers 10b, 10b as support rollers 10.
- a driving shaft 11 through the two driving rollers 10a, 10a is rotatably supported by an intermediate bearing, and is driven by a motor 13 via driving and driven gears 14 and 15.
- the two driven rollers 10b, 10b are arranged against the driving rollers 10a, 10a, and a rotary shaft 11 is rotatably supported by an intermediate bearing 12.
- the axis of the driving shaft 11 of the driving roller 10a is horizontal, while the axis of the rotary shaft 16 of the driven roller 10b is slightly inclined upward in a front direction. (The lower parts in Figs. 1 and 3 are front.)
- the end of the head 1b of the workpiece 1 is engaged on a loader head 18 having a shaft 18a and a head 18b, similar to the loader head 8 in Fig. 2.
- a loader head 18 having a shaft 18a and a head 18b, similar to the loader head 8 in Fig. 2.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Grinding Of Cylindrical And Plane Surfaces (AREA)
Applications Claiming Priority (8)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP6147094 | 1994-03-30 | ||
| JP61470/94 | 1994-03-30 | ||
| JP270840/94 | 1994-11-04 | ||
| JP27084094A JPH07314300A (ja) | 1994-03-30 | 1994-11-04 | 心なし研削盤 |
| JP6300715A JPH08155747A (ja) | 1994-12-05 | 1994-12-05 | 傘形ワークの加工方法 |
| JP300715/94 | 1994-12-05 | ||
| EP95301796 | 1995-03-17 | ||
| EP95301796A EP0674970A1 (de) | 1994-03-30 | 1995-03-17 | Spitzenlose Schleifmaschine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0674971A1 true EP0674971A1 (de) | 1995-10-04 |
| EP0674971B1 EP0674971B1 (de) | 1998-01-14 |
Family
ID=27443091
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19950301920 Expired - Lifetime EP0674971B1 (de) | 1994-03-30 | 1995-03-22 | Verfahren zum Bearbeiten eines Werkstückes |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0674971B1 (de) |
| DE (1) | DE69501414T2 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103624183A (zh) * | 2013-03-22 | 2014-03-12 | 浙江金固股份有限公司 | 一种轮毂气门孔去毛刺专用设备 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2110931A (en) * | 1935-10-23 | 1938-03-15 | Eaton Mfg Co | Machine tool |
| US2151528A (en) * | 1936-02-14 | 1939-03-21 | Black & Decker Mfg Co | Valve stem grinder |
| FR979744A (fr) * | 1948-01-28 | 1951-05-02 | Procédé et machine pour le faconnage d'objets par meulage | |
| EP0456590A1 (de) * | 1990-05-07 | 1991-11-13 | Serdi - Societe D'etudes De Realisation Et De Diffusion Industrielles | Ventilkopf-Schleifgerät, insbesondere für einen Verbrennungsmotor |
-
1995
- 1995-03-22 DE DE1995601414 patent/DE69501414T2/de not_active Expired - Fee Related
- 1995-03-22 EP EP19950301920 patent/EP0674971B1/de not_active Expired - Lifetime
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2110931A (en) * | 1935-10-23 | 1938-03-15 | Eaton Mfg Co | Machine tool |
| US2151528A (en) * | 1936-02-14 | 1939-03-21 | Black & Decker Mfg Co | Valve stem grinder |
| FR979744A (fr) * | 1948-01-28 | 1951-05-02 | Procédé et machine pour le faconnage d'objets par meulage | |
| EP0456590A1 (de) * | 1990-05-07 | 1991-11-13 | Serdi - Societe D'etudes De Realisation Et De Diffusion Industrielles | Ventilkopf-Schleifgerät, insbesondere für einen Verbrennungsmotor |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103624183A (zh) * | 2013-03-22 | 2014-03-12 | 浙江金固股份有限公司 | 一种轮毂气门孔去毛刺专用设备 |
| CN103624183B (zh) * | 2013-03-22 | 2015-06-17 | 浙江金固股份有限公司 | 一种轮毂气门孔去毛刺专用设备 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0674971B1 (de) | 1998-01-14 |
| DE69501414D1 (de) | 1998-02-19 |
| DE69501414T2 (de) | 1998-04-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5674111A (en) | Method of processing a workpiece | |
| US6978546B2 (en) | Method for producing ring members involving use of a rotatably driven mandrel | |
| US5154553A (en) | Apparatus for chamfering and deburring the end edges of a toothed production gear | |
| EP0674971B1 (de) | Verfahren zum Bearbeiten eines Werkstückes | |
| US20010005999A1 (en) | Power transmission member | |
| JP2000304054A (ja) | 円すいころ軸受 | |
| US7468015B2 (en) | Method for manufacturing a variator component of continuously variable transmission, and variator component of continuously variable transmission | |
| JP3849404B2 (ja) | トロイダル型無段変速機のローディングカム板 | |
| JP3835255B2 (ja) | ギア歯面加工方法及び装置 | |
| JPH0378488B2 (de) | ||
| JP3520620B2 (ja) | トロイダル型無段変速機の入力軸の外周面にボールスプライン溝を形成する方法 | |
| JP5323572B2 (ja) | トリポード型等速自在継手およびその製造方法 | |
| JPH0658389A (ja) | プーリー | |
| JP3766764B2 (ja) | バルブステム用研削加工砥石のドレッシング方法およびその装置 | |
| FR2761441A1 (fr) | Carter avant de convertisseur de couple comportant un bossage, et son procede de fabrication | |
| EP0674970A1 (de) | Spitzenlose Schleifmaschine | |
| JPH0753890Y2 (ja) | 平坦面のバニシ仕上げ工具 | |
| JP4434332B2 (ja) | 円板における環状周壁部の成形方法 | |
| JPH0756269Y2 (ja) | シート搬送装置 | |
| EP1170072A1 (de) | Verfahren zum Umformen von Metallstäben | |
| JP2004092902A (ja) | 湿式バンドブレーキ用ブレーキドラムおよびその製造方法 | |
| JPH0217810Y2 (de) | ||
| JP2815267B2 (ja) | 長尺スプラインシャフトの研削方法 | |
| JPS60232868A (ja) | 歯車仕上用砥石の成形方法 | |
| JPH07266203A (ja) | 研削盤におけるワークの回転駆動装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB IT |
|
| 17P | Request for examination filed |
Effective date: 19951017 |
|
| 17Q | First examination report despatched |
Effective date: 19960619 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| ITF | It: translation for a ep patent filed | ||
| REF | Corresponds to: |
Ref document number: 69501414 Country of ref document: DE Date of ref document: 19980219 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19980310 Year of fee payment: 4 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19991130 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20030403 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20040317 Year of fee payment: 10 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050322 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050322 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20050322 |