EP0686438A1 - Vorrichtung zum asymmetrisch Ablegen von Windungen - Google Patents
Vorrichtung zum asymmetrisch Ablegen von Windungen Download PDFInfo
- Publication number
- EP0686438A1 EP0686438A1 EP95107504A EP95107504A EP0686438A1 EP 0686438 A1 EP0686438 A1 EP 0686438A1 EP 95107504 A EP95107504 A EP 95107504A EP 95107504 A EP95107504 A EP 95107504A EP 0686438 A1 EP0686438 A1 EP 0686438A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- coil
- loops
- guide cams
- circumference
- stacking element
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C47/00—Winding-up, coiling or winding-off metal wire, metal band or other flexible metal material characterised by features relevant to metal processing only
- B21C47/02—Winding-up or coiling
- B21C47/10—Winding-up or coiling by means of a moving guide
- B21C47/14—Winding-up or coiling by means of a moving guide by means of a rotating guide, e.g. laying the material around a stationary reel or drum
- B21C47/146—Controlling or influencing the laying pattern of the coils
Definitions
- This invention concerns a device for the asymmetric depositing of loops, as set forth in the main claim.
- the device according to the invention is applied within a rolling plant in the coil-forming station positioned downstream of the rolling train and cooling area.
- This invention is suitable to cooperate with conventional assemblies for the forming and conveying of the loops and enables the method of distributing the loops on the stacking element to be perfected.
- the slabs or billets subjected to the various rolling stages undergo a preliminary cooling before being sent to the loop-forming station.
- This station contains a rotary headstock which forms the loops and generally drops them onto a prearranged removal element consisting of a removal conveyor belt, for instance.
- the loops on this conveyor belt can cooperate further with controlled cooling systems.
- the loops are discharged onto a suitable stacking element to form a coil.
- the coils thus formed then undergo the normal processes of compaction, tying and anything else required for their later use.
- the discharge of the loops onto the relative stacking element entails problems owing to the uneven and disorderly array which the loops may take up in falling from the conveyor belt.
- the loops when they are superimposed on each other in a disorderly manner, form an unbalanced, unstable and incompact coil with a low density of loops.
- the state of the art discloses a plurality of systems to improve the distribution of the loops in the step of forming coils with the purpose of making the formed coil more stable and compact and thus minimising the space taken up by the coil during the subsequent steps of transport and storage.
- Patent US RE 26,052 discloses the employment of a rotary deflector, the arm of which extends radially towards the inside of the coil-forming chamber and defines, together with the opposite side of the coil-forming chamber, a distance which is substantially the same as the diameter of the coil being formed.
- DE-A-1.235.100 too discloses the use of a rotary deflector with an arm directed towards the inside of the coil-forming chamber so as to restrict the possibility of the loops being arranged in an uneven and disorderly manner.
- EP-A-0583099 teaches the use of a rotary deflector having a surface curved in three dimensions and affecting only part of the circumference so as to accompany and displace sideways the loops discharged from the relative conveyors according to a path about a nominal circumference of the coil.
- This document does not make possible the variation and regulation in a desired manner of the eccentric nature of the depositing of the loops, nor does it make possible in any case an axial depositing of the loops according to the axis of the stacking element; it requires an appropriately and three- dimensionally shaped and conformed element for its use, and this situation entails complex and accurate calculations to produce the correct form and yet other drawbacks.
- each discharged loop is displaced by the rotary deflector substantially as soon as it leaves the conveyor belt, that is to say, there is not a first guide segment positioned substantially on the same axis as the stacking element where each loop has the time to take up an orderly and correct position.
- this deflector does not apply a guiding action to the forming loops but exerts only a lateral displacement action, thus causing deformations of the loops.
- the drive system to set the deflector in rotation is complicated and hard to regulate.
- the purpose of the invention is to provide a device which enables the loops to be deposited asymmetrically on the coil being formed.
- the device according to the invention has a very simple concept and embodiment and is very simple to set to work and operate.
- the device according to the invention enables the value of the asymmetric positioning imparted to the loops during their depositing to be regulated very simply in a desired manner even during the progress of work and also makes possible the depositing of coaxial loops or also the depositing of loops coaxial with the axis of the stacking element if that is required by the coil-forming method.
- the device according to the invention ensures in each step a correct and accurate guiding of the loops which are progressively superimposed on each other to form the coil.
- the device according to the invention cooperates with a stacking element having its axis advantageously, but not only, substantially vertical and we shall refer to this in the description that follows.
- the device according to the invention includes a plurality of guide cams able to rotate with a stationary axis of rotation in a synchronized manner about that axis.
- the axes of rotation of the guide cams define between them a circumference coaxial with the axis of the stacking element.
- the axes of rotation of the guide cams are inclined by a desired value in relation to the axis of the stacking element so as to define a cone the vertex of which lies substantially on the axis of the stacking element.
- a substantially cylindrical guide element coaxial with the axis of the stacking element is included above the plane defined by the guide cams and cooperates directly with the zone of release by the means conveying the loops.
- This guide element has the purpose of guiding the descent of the loops along a first segment towards the stacking element so that all those loops arrive in a correct and uniform manner in cooperation with the asymmetric depositing device according to the invention.
- This asymmetric depositing device thus acts on loops which have already been correctly positioned and guided even when the discharge from the conveyor means takes place in a very quick and disorderly manner.
- the lateral surface of these guide cams protrudes at least partly into the annular chamber, or coil-forming chamber, positioned downstream of the guide element, in which the coils pass from the conveyor means to the stacking element.
- the guide cams are installed eccentrically on their respective axes of rotation, and this eccentricity of positioning of the guide cams varies progressively within an arc of 180 from a maximum value to a minimum value along the circumference of positioning of the axes of rotation of the guide cams.
- the guide cams are fitted around the stacking element in such a way that their lateral surface protrudes into the coil-forming chamber in a manner increasing progressively within an arc of 180 and decreasing progressively within the other 180°.
- the guide cams together define between them during their rotation a circumference for the passage of the coils being deposited on the stacking element, this circumference being eccentric in relation to the axis of the stacking element, the value of the eccentricity varying progressively, sequentially and periodically during the depositing of the loops.
- This eccentricity changes from a maximum value in one direction to a maximum value in the other direction and passes through a nil value coinciding with the axis of the stacking element.
- the circumference of the passage being eccentric in relation to the stacking element, enables a depositing to be carried out whereby the loops are offset from each other according to a prearranged and periodical mating sequence.
- the depositing carried out in this manner enables a coil to be produced which is improved in terms of occupation of space in a vertical direction, density, uniformity, stability and balance of the coil and compactness.
- the coil thus produced can cooperate more effectively and uniformly with any cooling systems since the single loops can be lapped more easily and evenly by the action of the cooling systems.
- the device enables a depositing to be also achieved whereby the loops are discharged in an orderly manner on the axis of the stacking element and each of the guide cams is correctly positioned and kept stationary in that position during the whole period of the cycle of formation of the coil.
- a slab or billet is rolled continuously in a rolling train comprising at least one roughing rolling mill stand 11 and a finishing train 12.
- the rolled product is fed into a cooling area generically referenced with 13 and thence to a loop-forming headstock 14.
- Loops 15 formed by the loop-forming headstock 14 are discharged onto a conveyor belt 16 generally associated with cooling means.
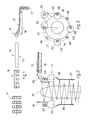
- the loops 15 are discharged from the downstream end of the conveyor belt 16 into a coil-forming station 17, in which the loops 15 are stacked on each other about a stacking element 18 having an axis 27, in this case, substantially vertical so as to form a coil.
- the coil-forming station 17 comprises a first stationary, cylindrical, tubular element 19 which cooperates directly with the downstream end of the conveyor belt 16 and/or with a possible feeder roller 20.
- This first cylindrical, tubular element 19 has the task of guiding the loops 15 discharged from the conveyor 16 along a first segment of their descent into the coil-forming station 17.
- a second cylindrical element 21 is included below the first cylindrical, tubular element 19 and has a diameter greater than the diameter of the stacking element 18 and surrounds that stacking element 18 circumferentially.
- a coil-forming chamber 29 is defined between the stacking element 18 and the second cylindrical element 21.
- a plurality of guide cams 22 are positioned on one single horizontal plane in an intermediate vertical position between the first cylindrical, tubular element 19 and the second cylindrical element 21 which surrounds the stacking element 18.
- All these guide cams 22 rotate in a synchronised manner about stationary axes 23, and the lateral surface of the guide cams 22 extends radially and at least partly into the coil-forming chamber 29.
- the axes 23 of the guide cams 22 together define a circumference which is substantially coaxial with the axis 27 of the stacking element 18.
- the respective axes 23a and 23b of the guide cams 22 are inclined in relation to the axis 27 of the stacking element 18 so as to define a cone having its vertex lying on the axis 27 of the stacking element 18; in the example of Fig.4 the vertex of the cone faces in a downward direction, whereas in the example of Fig.5 the vertex of the cone faces in an upward direction.
- a transmission chain 24 which gets its motion from a motor 25, which is advantageously a variable speed reduction unit, the chain 24 being connected to each specific guide cam 22 by suitable transmission means 26.
- the transmission chain 24 is wound about transmission rollers 28 between one guide cam 22 and the adjacent guide cam 22.
- the guide cams 22 are installed eccentrically in relation to their own axes of rotation 23 and have a substantially cylindrical outline.
- the guide cams 22 have an outline which is at least partly substantially tapered.
- each guide cam 22 is installed progressively offset in relation to the adjacent guide cam 22.
- the surfaces of the guide cams 22 protruding into the coil-forming chamber 29 define with each other a circumference eccentric in relation to the axis 27 of the stacking element 18, this circumference having a diameter smaller than the diameter of the coil-forming chamber 29.
- This progressively variable eccentricity of the downward travel of the loops 15 causes an asymmetric arrangement of the loops 15 about the circumference defined by the stacking element 18, thus achieving a greater filling of space, better stability, greater density and greater compactness of the coil produced.
- the axial positioning of the guide cams 22 can be altered in a desired manner so as to impart to the loops progressively discharged from the conveyor 16 a more or less accentuated asymmetric- ity.
- These guide cams 22 can also be positioned and kept stationary in those positions during the whole coil-forming cycle in such a way that all the loops 15 are discharged on the axis 27 of the stacking element 18 or all the loops 15 are discharged in an orderly manner and are superimposed on each other according to an axis parallel to the axis 27 of the stacking element 18.
Landscapes
- Mechanical Engineering (AREA)
- Engineering & Computer Science (AREA)
- Winding, Rewinding, Material Storage Devices (AREA)
- Collation Of Sheets And Webs (AREA)
- Valve Device For Special Equipments (AREA)
- Physical Vapour Deposition (AREA)
- Discharge Heating (AREA)
- Particle Accelerators (AREA)
- Inductance-Capacitance Distribution Constants And Capacitance-Resistance Oscillators (AREA)
- Valve-Gear Or Valve Arrangements (AREA)
- Transmission Devices (AREA)
- Specific Conveyance Elements (AREA)
- Attitude Control For Articles On Conveyors (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ITUD940099 | 1994-06-07 | ||
| IT94UD000099A IT1267252B1 (it) | 1994-06-07 | 1994-06-07 | Dispositivo per il deposito asimmetrico delle spire |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0686438A1 true EP0686438A1 (de) | 1995-12-13 |
| EP0686438B1 EP0686438B1 (de) | 1998-07-22 |
Family
ID=11421596
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95107504A Expired - Lifetime EP0686438B1 (de) | 1994-06-07 | 1995-05-17 | Vorrichtung zum asymmetrischen Ablegen von Windungen |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP0686438B1 (de) |
| KR (1) | KR960000329A (de) |
| CN (1) | CN1062789C (de) |
| AT (1) | ATE168597T1 (de) |
| DE (1) | DE69503571T2 (de) |
| ES (1) | ES2119270T3 (de) |
| IT (1) | IT1267252B1 (de) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0768126A1 (de) * | 1995-10-16 | 1997-04-16 | Sms Schloemann-Siemag Aktiengesellschaft | Verfahren und Vorrichtung zur Minimierung der Höhe von Drahtbunden |
| US6158683A (en) * | 1998-03-18 | 2000-12-12 | Sms Schloemann-Siemag Ag | Apparatus for forming rolled wire-rod coil |
| DE10026583A1 (de) * | 2000-05-30 | 2001-12-13 | Sket Walzwerkstechnik Gmbh | Vorrichtung zum Ablegen von Walzdrahtwindungen zu einem Drahtbund |
| EP3260212A1 (de) * | 2016-06-20 | 2017-12-27 | Sund Birsta AB | Spulenformmaschine |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| RU2192323C2 (ru) | 2000-05-24 | 2002-11-10 | Некипелов Владимир Станиславович | Способ формирования бунта катанки и устройство для его осуществления |
| US7827841B2 (en) * | 2006-04-13 | 2010-11-09 | Siemens Industry, Inc. | Method of and system for processing different sized long products |
| CN104259351B (zh) * | 2014-07-29 | 2016-08-31 | 安徽省宁国市东波紧固件有限公司 | 一种孔用挡圈自动抖散装置 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2527662A (en) * | 1948-11-30 | 1950-10-31 | Robert L Stevens | Coiling machine |
| USRE26052E (en) | 1966-06-28 | Wire handling apparatus | ||
| DE1235100B (de) | 1965-01-26 | 1967-02-23 | Demag Ag | Vorrichtung zum Sammeln und Unterteilen von Drahtwindungen oder Gruppen derselben |
| EP0583099A1 (de) | 1992-08-03 | 1994-02-16 | Morgan Construction Company | Schleifenleitvorrichtung für Reformingstation |
-
1994
- 1994-06-07 IT IT94UD000099A patent/IT1267252B1/it active IP Right Grant
-
1995
- 1995-05-17 ES ES95107504T patent/ES2119270T3/es not_active Expired - Lifetime
- 1995-05-17 AT AT95107504T patent/ATE168597T1/de not_active IP Right Cessation
- 1995-05-17 DE DE69503571T patent/DE69503571T2/de not_active Expired - Fee Related
- 1995-05-17 EP EP95107504A patent/EP0686438B1/de not_active Expired - Lifetime
- 1995-05-29 KR KR1019950013592A patent/KR960000329A/ko not_active Ceased
- 1995-06-06 CN CN95107192A patent/CN1062789C/zh not_active Expired - Fee Related
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| USRE26052E (en) | 1966-06-28 | Wire handling apparatus | ||
| US2527662A (en) * | 1948-11-30 | 1950-10-31 | Robert L Stevens | Coiling machine |
| DE1235100B (de) | 1965-01-26 | 1967-02-23 | Demag Ag | Vorrichtung zum Sammeln und Unterteilen von Drahtwindungen oder Gruppen derselben |
| EP0583099A1 (de) | 1992-08-03 | 1994-02-16 | Morgan Construction Company | Schleifenleitvorrichtung für Reformingstation |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0768126A1 (de) * | 1995-10-16 | 1997-04-16 | Sms Schloemann-Siemag Aktiengesellschaft | Verfahren und Vorrichtung zur Minimierung der Höhe von Drahtbunden |
| US6158683A (en) * | 1998-03-18 | 2000-12-12 | Sms Schloemann-Siemag Ag | Apparatus for forming rolled wire-rod coil |
| DE10026583A1 (de) * | 2000-05-30 | 2001-12-13 | Sket Walzwerkstechnik Gmbh | Vorrichtung zum Ablegen von Walzdrahtwindungen zu einem Drahtbund |
| EP3260212A1 (de) * | 2016-06-20 | 2017-12-27 | Sund Birsta AB | Spulenformmaschine |
| WO2017220288A1 (en) * | 2016-06-20 | 2017-12-28 | Sund Birsta Ab | Coil-forming machine |
Also Published As
| Publication number | Publication date |
|---|---|
| DE69503571D1 (de) | 1998-08-27 |
| IT1267252B1 (it) | 1997-01-28 |
| KR960000329A (ko) | 1996-01-25 |
| DE69503571T2 (de) | 1999-02-04 |
| CN1123721A (zh) | 1996-06-05 |
| CN1062789C (zh) | 2001-03-07 |
| EP0686438B1 (de) | 1998-07-22 |
| ATE168597T1 (de) | 1998-08-15 |
| ITUD940099A1 (it) | 1995-12-07 |
| ES2119270T3 (es) | 1998-10-01 |
| ITUD940099A0 (it) | 1994-06-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0686439A1 (de) | Vorrichtung zum asymmetrisch Ablegen von Windungen | |
| EP0438066B1 (de) | Anlage zum Auswalzen von Warmbreitband | |
| EP0686438B1 (de) | Vorrichtung zum asymmetrischen Ablegen von Windungen | |
| PL222327B1 (pl) | Sposób i urządzenie do transferowania elementów prętopodobnych w maszynach przemysłu tytoniowego oraz maszyna do wytwarzania sztabek wieloelementowych | |
| RU2412015C2 (ru) | Способ и производственная линия для изготовления горячей ультратонкой стальной полосы с двумя литейными линиями для одной линии бесконечной прокатки | |
| EP1559663B1 (de) | Verfahren und Fördervorrichtung zur Förderung von mit einem Kragen versehenen Gegenständen | |
| US20130112796A1 (en) | Perfected laying head | |
| US4189045A (en) | Device for transferring rod-like objects | |
| EP0815973B1 (de) | Wickelverfahren und Wickelvorrichtung | |
| US6915978B2 (en) | Method of rod coil forming and set of equipment for its realization | |
| EP1844869B1 (de) | Verfahren und System zur Bearbeitung von langen Produkten verschiedener Größen | |
| US6405958B1 (en) | Method and apparatus for minimizing the coil height of wire in a coil forming chamber | |
| US4690267A (en) | Charging-and-conveying means | |
| KR102614518B1 (ko) | 담배 산업의 로드형 제품들의 이송을 위한 이송 장치 및 이송 방법, 및 상기 제품들의 스트림의 구성을 전환하기 위한 장치 | |
| US3711918A (en) | Split level conveyor and collecting means for controlled cooled steel rod | |
| US3460777A (en) | Deposition of a continuous string of turns of wire upon a conveyor | |
| EP1791775A1 (de) | Vorrichtung zum unterbrechungsfreien aufwickeln einer kontinuierlich zugeförderten textilen warenbahn | |
| RU2256519C1 (ru) | Способ намотки тонкой ленты в рулон и устройство для его осуществления | |
| SU1616786A1 (ru) | Способ прокатки тонкой металлической ленты из порошка | |
| US3593836A (en) | Transfer apparatus | |
| DE10103677B4 (de) | Verfahren zur Erzeugung von Drahtbunden niedriger Höhe | |
| RU2275261C2 (ru) | Способ и устройство для замедления движения и временного накапливания изделия горячей прокатки | |
| EP1590112A1 (de) | Vorrichtung zur kontinuierlichen herstellung von draht- oder stabstahl aus der giesshitze und verfahren zu deren betrieb | |
| RU22900U1 (ru) | Линия для продольной резки полосового проката | |
| JPH02133530A (ja) | 熱間圧延線材の捲落し装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE DE ES FR GB IT SE |
|
| 17P | Request for examination filed |
Effective date: 19960606 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19970919 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| ITF | It: translation for a ep patent filed | ||
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE DE ES FR GB IT SE |
|
| REF | Corresponds to: |
Ref document number: 168597 Country of ref document: AT Date of ref document: 19980815 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 69503571 Country of ref document: DE Date of ref document: 19980827 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2119270 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20030526 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20040422 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20040423 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20040426 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20040428 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20040503 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20040514 Year of fee payment: 10 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050131 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050517 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050517 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050517 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050518 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050518 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 |
|
| BERE | Be: lapsed |
Owner name: *DANIELI & C. OFFICINE MECCANICHE S.P.A. Effective date: 20050531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20051201 |
|
| EUG | Se: european patent has lapsed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20050517 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20050518 |
|
| BERE | Be: lapsed |
Owner name: *DANIELI & C. OFFICINE MECCANICHE S.P.A. Effective date: 20050531 |