EP0816101A2 - Verfahren zum Herstellen eines Schaumkörpers für eine Tintenpatrone - Google Patents
Verfahren zum Herstellen eines Schaumkörpers für eine Tintenpatrone Download PDFInfo
- Publication number
- EP0816101A2 EP0816101A2 EP97810401A EP97810401A EP0816101A2 EP 0816101 A2 EP0816101 A2 EP 0816101A2 EP 97810401 A EP97810401 A EP 97810401A EP 97810401 A EP97810401 A EP 97810401A EP 0816101 A2 EP0816101 A2 EP 0816101A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- coating
- press
- plate
- foam body
- foam
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41J—TYPEWRITERS; SELECTIVE PRINTING MECHANISMS, i.e. MECHANISMS PRINTING OTHERWISE THAN FROM A FORME; CORRECTION OF TYPOGRAPHICAL ERRORS
- B41J2/00—Typewriters or selective printing mechanisms characterised by the printing or marking process for which they are designed
- B41J2/005—Typewriters or selective printing mechanisms characterised by the printing or marking process for which they are designed characterised by bringing liquid or particles selectively into contact with a printing material
- B41J2/01—Ink jet
- B41J2/17—Ink jet characterised by ink handling
- B41J2/175—Ink supply systems ; Circuit parts therefor
- B41J2/17503—Ink cartridges
- B41J2/17513—Inner structure
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1052—Methods of surface bonding and/or assembly therefor with cutting, punching, tearing or severing
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1052—Methods of surface bonding and/or assembly therefor with cutting, punching, tearing or severing
- Y10T156/1062—Prior to assembly
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/12—Surface bonding means and/or assembly means with cutting, punching, piercing, severing or tearing
- Y10T156/13—Severing followed by associating with part from same source
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/12—Surface bonding means and/or assembly means with cutting, punching, piercing, severing or tearing
- Y10T156/1317—Means feeding plural workpieces to be joined
- Y10T156/1322—Severing before bonding or assembling of parts
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1702—For plural parts or plural areas of single part
- Y10T156/1744—Means bringing discrete articles into assembled relationship
- Y10T156/1751—At least three articles
Definitions
- the present invention relates to a method for manufacturing a foam body for insertion into an ink cartridge for one Inkjet printer according to the preamble of claim 1.
- One such The method is known from EP-A-709 209.
- This font relates to a three-color inkjet print head.
- the punched out Foam bodies are first compressed and in a heating press warmed up so that they sit down.
- a cover is put around before insertion, which is part of the lower area and the two large areas of the foam body covered.
- the shell consists of Paper. The cover facilitates the insertion of the foam body into the relatively narrow and high middle chamber.
- the object of the present invention is a method indicate by means of which such coated foam body can be produced efficiently. This task will solved by the characterizing features of claim 1.
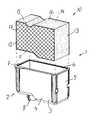
- the ink cartridge 1 has a housing 2 with a bottom 3, side walls 4-7 and a lid, not shown. At the bottom is 3 a nozzle 8 for plugging onto a print head of an inkjet printer molded.
- Foam body 10 used with a base 11 accordingly the inside of the bottom 3, four side surfaces 12-15 and one Top surface 16.
- the two wide side surfaces 12 and 14 are coated with a material that is much less Coefficient of friction against the material of the housing 2 has than the foam body 10.
- the coating 17 can for Example of a thermoplastic film glued on with a hot melt adhesive for example made of PE or PU, a fabric, a fleece or be a paint job.
- the coating can be porous or perforated. It may not need the entire area to be.
- the foam body 10 When the foam body 10 is inserted into the housing 2, it becomes slightly compressed perpendicular to surfaces 12 and 14. Through the Coating 17 is achieved that the foam body easily ins Housing must be inserted without corners or edges on edges, or surfaces of the housing get stuck and therefore close to the ground free spaces and adjoining compressed areas of the Foam body 10 arise with changed capillaryity. Both Phenomena that were previously difficult when inserting the foam body were to be avoided, reduce the usable foam volume of the Foam body 10.
- the coating 17 is applied before the foam body 10 is punched out applied to the foam sheet, from which subsequently with a multiple punching knife (strip steel knife) in a punching press a plurality of foam bodies 10 simultaneously in one stroke be punched out.
- the coating 17 is in a Heating press applied, either simultaneously on both sides or initially only on one side, followed by the foam sheet is turned and the other side is coated. If the coating film (for example made of PU or PE) with a Hot melt adhesive is coated, the temperature of the Press plate (s) of the heating press between the melting temperature of the hot melt adhesive and the higher melting temperature of the Foil selected.
Landscapes
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Ink Jet (AREA)
- Particle Formation And Scattering Control In Inkjet Printers (AREA)
- Laminated Bodies (AREA)
Abstract
Description
Claims (8)
- Verfahren zur Herstellung eines Schaumkörpers (10) zum Einsetzen in eine Tintenpatrone (1) für einen Inkjet-Printer, wobei der Schaumkörper (10) aus einer Platte ausgestanzt und an zwei gegenüberliegenden Seitenflächen (12, 14) mit einer Beschichtung (17) beschichtet wird, dadurch gekennzeichnet, dass die Beschichtung (17) vor dem Ausstanzen des Schaumkörpers (10) auf die beiden Grossflächen der Platte aufgebracht wird.
- Verfahren nach Anspruch 1, wobei die Beschichtung (17) auf der der Platte zugekehrten Seite mit einem Heissschmelzkleber beschichtet und die Beschichtung (17) in einer Presse aufgebracht wird, und wobei die Temperatur einer Pressplatte zwischen der Schmelztemperatur des Klebers und der Schmelztemperatur der Beschichtung eingestellt wird.
- Verfahren nach Anspruch 1, wobei als Beschichtung eine Verbundfolie aus zwei Materialien mit unterschiedlicher Schmelztemperatur verwendet wird und das Material mit der tieferen Schmelztemperatur der Platte zugekehrt wird.
- Verfahren nach Anspruch 1, wobei als Beschichtung eine Kunststoffolie verwendet wird, eine Pressplatte mit einer Antihaftschicht (zum Beispiel mit PTFE) beschichtet ist und die Pressplatte auf eine Temperatur oberhalb der Schmelztemperatur der Folie erwärmt wird.
- Verfahren nach einem der Ansprüche 1 bis 4, wobei in einer Presse beide Grossflächen der Schaumstoffplatte gleichzeitig beschichtet werden.
- Verfahren nach einem der Ansprüche 1 bis 5, wobei die Schaumstoffplatte vor dem Beschichten in einer Presse komprimiert und erwärmt wird, so dass sie sich setzt, und wobei anschliessend in derselben Presse die beiden Folien aufgesiegelt werden.
- Verfahren nach einem der Ansprüche 1 bis 6, wobei nach dem Beschichten mit einem Vielfach-Stanzmesser gleichzeitig eine Vielzahl von Schaumkörpern (10) aus der Platte ausgestanzt wird.
- Nach dem Verfahren gemäss einem der Ansprüche 1 bis 7 hergestellter Schaumkörper (10) mit einer Beschichtung (17) auf zwei gegenüberliegenden Seitenflächen (12, 14), dadurch gekennzeichnet, dass die Beschichtung (17) auf die beiden Seitenflächen (12, 14) aufgesiegelt ist und sich ausschliesslich über diese Seitenflächen (12, 14) erstreckt.
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19626637 | 1996-07-02 | ||
| DE19626637 | 1996-07-02 | ||
| DE19706266A DE19706266A1 (de) | 1996-07-02 | 1997-02-18 | Verfahren zum Herstellen eines Schaumkörpers für eine Tintenpatrone |
| DE19706266 | 1997-02-18 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0816101A2 true EP0816101A2 (de) | 1998-01-07 |
| EP0816101A3 EP0816101A3 (de) | 1999-06-23 |
| EP0816101B1 EP0816101B1 (de) | 2003-07-30 |
Family
ID=26027135
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP97810401A Expired - Lifetime EP0816101B1 (de) | 1996-07-02 | 1997-06-24 | Verfahren zum Herstellen eines Schaumkörpers für eine Tintenpatrone |
Country Status (3)
| Country | Link |
|---|---|
| US (1) | US6059916A (de) |
| EP (1) | EP0816101B1 (de) |
| CA (1) | CA2206977C (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2760405A1 (fr) * | 1997-03-07 | 1998-09-11 | Seiko Epson Corp | Cartouche a encre pour imprimante a jet d'encre |
Families Citing this family (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP3833026B2 (ja) | 1998-10-27 | 2006-10-11 | キヤノン株式会社 | 吸収体の挿入方法、および液体容器の製造装置 |
| USD438241S1 (en) | 1999-05-28 | 2001-02-27 | Seiko Epson Corporation | Ink cartridge for printer |
| USD442219S1 (en) | 2000-03-03 | 2001-05-15 | Wisertek International Corp. | Ink cartridge for a printer |
| USD440600S1 (en) | 2000-04-28 | 2001-04-17 | Seiko Epson Corporation | Ink cartridge for printer |
| US6595711B2 (en) * | 2000-05-26 | 2003-07-22 | Legacy Manufacturing, Llc | Printer cartridge having a foam retention clip |
| USD483403S1 (en) | 2000-12-19 | 2003-12-09 | Océ-Technologies B.V. | Inkball with a hole |
| US6837715B2 (en) * | 2001-03-06 | 2005-01-04 | General Binding Corporation | Dry erase and tack display board having no frame |
| USD457184S1 (en) | 2001-04-30 | 2002-05-14 | Hewlett-Packard Company | Ink jet print cartridge |
| USD464371S1 (en) | 2001-04-30 | 2002-10-15 | Hewlett-Packard Company | Ink jet print cartridge |
| US6698872B2 (en) * | 2001-06-15 | 2004-03-02 | International United Technology Co., Ltd. | Ink cartridge for preventing ink from spilling |
| USD535688S1 (en) * | 2005-04-04 | 2007-01-23 | Canon Kabushiki Kaisha | Ink cartridge for printer |
| USD534582S1 (en) * | 2005-04-04 | 2007-01-02 | Canon Kabushiki Kaisha | Ink cartridge for printer |
| JP5804727B2 (ja) * | 2011-02-25 | 2015-11-04 | キヤノン株式会社 | 液体収納容器の製造方法および製造装置 |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2772196A (en) * | 1954-05-21 | 1956-11-27 | Us Rubber Co | Shoe sole and method of making same |
| US4055699A (en) * | 1976-12-02 | 1977-10-25 | Scholl, Inc. | Cold insulating insole |
| JPS607439B2 (ja) * | 1980-01-31 | 1985-02-25 | 松下電器産業株式会社 | スピ−カ用振動板およびその製造方法 |
| JPS6342816A (ja) * | 1986-08-11 | 1988-02-24 | Buruu Marine:Kk | フインの成型方法 |
| US5199662A (en) * | 1989-11-22 | 1993-04-06 | Klupt Carle D | Limited use combined mailer and video cassette and method of forming same |
| JP3160312B2 (ja) * | 1990-07-10 | 2001-04-25 | キヤノン株式会社 | インクジェットカートリッジ及び該カートリッジを用いた記録装置 |
| JP2543970Y2 (ja) * | 1991-06-24 | 1997-08-13 | 株式会社ブリヂストン | ウレタンフォ−ム充填容器 |
| US5637389A (en) * | 1992-02-18 | 1997-06-10 | Colvin; David P. | Thermally enhanced foam insulation |
| SG72660A1 (en) * | 1993-08-23 | 2000-05-23 | Canon Kk | Exchangeable ink cartridge |
| EP0709209B1 (de) * | 1994-10-31 | 1998-12-30 | Hewlett-Packard Company | Tintenbehälter mit Schutzblatt für porösen Körper |
| US5735453A (en) * | 1995-11-14 | 1998-04-07 | Gick; James W. | Decorative novelty articles |
-
1997
- 1997-06-04 CA CA002206977A patent/CA2206977C/en not_active Expired - Fee Related
- 1997-06-24 EP EP97810401A patent/EP0816101B1/de not_active Expired - Lifetime
- 1997-07-01 US US08/886,332 patent/US6059916A/en not_active Expired - Fee Related
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2760405A1 (fr) * | 1997-03-07 | 1998-09-11 | Seiko Epson Corp | Cartouche a encre pour imprimante a jet d'encre |
| US6170941B1 (en) | 1997-03-07 | 2001-01-09 | Seiko Epson Corporation | Ink cartridge for ink-jet recorder |
| FR2799689A1 (fr) * | 1997-03-07 | 2001-04-20 | Seiko Epson Corp | Cartouche a encre pour imprimante a jet d'encre |
Also Published As
| Publication number | Publication date |
|---|---|
| CA2206977A1 (en) | 1998-01-02 |
| EP0816101B1 (de) | 2003-07-30 |
| EP0816101A3 (de) | 1999-06-23 |
| US6059916A (en) | 2000-05-09 |
| CA2206977C (en) | 2005-11-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0816101B1 (de) | Verfahren zum Herstellen eines Schaumkörpers für eine Tintenpatrone | |
| DE4233558C2 (de) | Elektrische Maschine | |
| DE3801059C2 (de) | Reparaturflicken für Fahrzeugkarosserien | |
| DE69030251T2 (de) | Thermisches verfahren zur herstellung von papierschablone | |
| DE2749620C3 (de) | Verfahren zur Herstellung gedruckter Schaltungen | |
| DE2922568C2 (de) | Verfahren und Vorrichtung zum Herstellen eines plattenförmigen Formkörpers mit Randleiste an wenigstens einer Seitenrandfläche | |
| CH665133A5 (de) | Filtermembran mit abdichtung und verfahren zu ihrer herstellung. | |
| DE1794235A1 (de) | Praegeblatt und Verfahren zu dessen Herstellung | |
| DE69805425T2 (de) | Stempelvorrichtung | |
| DE69800255T2 (de) | Schablonenblatt und Verfahren zur Herstellung eines Druckschablones, das dieses Druckschablone verwendet | |
| DE2352966A1 (de) | Gemaeldeimitation mit imitierten pinsel- und/oder farbspachtelstrichen und verfahren zur herstellung derselben | |
| DE3741499A1 (de) | Verfahren zur perforation von mit kunststoff-folien versiegelten formteilen | |
| DE19706266A1 (de) | Verfahren zum Herstellen eines Schaumkörpers für eine Tintenpatrone | |
| DE69806081T2 (de) | Schablonendruckvorrichtung | |
| EP1683826B1 (de) | Verfahren zur Herstellung einer definierten dreidimensionalen reliefartigen Struktur auf einer Oberfläche eines bereitgestellten Trägers sowie Verwendung einer mit Hilfe des Verfahrens hergestellten Struktur | |
| DE3401839C1 (de) | Verfahren und Vorrichtung zum Verkleben von Substraten | |
| DE3445715A1 (de) | Verfahren zum erstellen einer dichtung auf einer dichtflaeche eines bauteils | |
| DE69205414T2 (de) | Verfahren zur Herstellung eines verfilzten, porösen Polychloroprenlatex-Schaums. | |
| DE2618741C2 (de) | ||
| DE20320658U1 (de) | Werkzeug zum Stanzen und/oder Rillen | |
| WO1985001339A1 (fr) | Procede de fabrication d'un echangeur de chaleur | |
| DE202004011038U1 (de) | Elektrisches Handstempelgerät | |
| EP0012849B1 (de) | Verfahren zum Überziehen von porösen Schaumstoffkörpern mit einer Haut aus Polyurethan | |
| DE2840386C2 (de) | Verfahren zum Herstellen abriebfester Lochplattensiebe | |
| DE3140292A1 (de) | Verfahren zur herstellung eines farbigen reliefs auf einem plattenfoermigen, faserverstaerkten, kunststoffhaltigen traeger |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): CH DE FR GB IT LI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| 17P | Request for examination filed |
Effective date: 19991029 |
|
| AKX | Designation fees paid |
Free format text: CH DE FR GB IT LI |
|
| 17Q | First examination report despatched |
Effective date: 20001019 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: NU-KOTE INTERNATIONAL, INC. Owner name: PELIKAN PRODUKTIONS AG |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: NU-KOTE INTERNATIONAL, INC. Owner name: PELIKAN HARDCOPY PRODUCTION AG |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): CH DE FR GB IT LI |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: ING. HANS LUDESCHER, PATENTABTEILUNG DER SFS GRUPP |
|
| REF | Corresponds to: |
Ref document number: 59710495 Country of ref document: DE Date of ref document: 20030904 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040120 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040504 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PCAR Free format text: ISLER & PEDRAZZINI AG;POSTFACH 1772;8027 ZUERICH (CH) |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20100626 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PFA Owner name: NU-KOTE INTERNATIONAL, INC. Free format text: NU-KOTE INTERNATIONAL, INC.#200 BEASLEY DRIVE#FRANKLIN, TENNESSEE 37064 (US) $ PELIKAN HARDCOPY PRODUCTION AG#LEESTRASSE 1#8132 EGG (CH) -TRANSFER TO- NU-KOTE INTERNATIONAL, INC.#200 BEASLEY DRIVE#FRANKLIN, TENNESSEE 37064 (US) $ PELIKAN HARDCOPY PRODUCTION AG#HALDENSTRASSE 30#8620 WETZIKON (CH) |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 59710495 Country of ref document: DE Representative=s name: MEISSNER, BOLTE & PARTNER GBR, DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110624 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 59710495 Country of ref document: DE Representative=s name: MEISSNER, BOLTE & PARTNER GBR, DE Effective date: 20120116 Ref country code: DE Ref legal event code: R081 Ref document number: 59710495 Country of ref document: DE Owner name: PELIKAN HARDCOPY PRODUCTION AG, CH Free format text: FORMER OWNERS: PELIKAN HARDCOPY PRODUCTION AG, EGG, CH; NU-KOTE INTERNATIONAL INC., FRANKLIN, TENN., US Effective date: 20120116 Ref country code: DE Ref legal event code: R081 Ref document number: 59710495 Country of ref document: DE Owner name: NU-KOTE INTERNATIONAL INC., FRANKLIN, US Free format text: FORMER OWNERS: PELIKAN HARDCOPY PRODUCTION AG, EGG, CH; NU-KOTE INTERNATIONAL INC., FRANKLIN, TENN., US Effective date: 20120116 Ref country code: DE Ref legal event code: R081 Ref document number: 59710495 Country of ref document: DE Owner name: PELIKAN HARDCOPY PRODUCTION AG, CH Free format text: FORMER OWNER: PELIKAN HARDCOPY PRODUCTION AG, NU-KOTE INTERNATIONAL INC., , US Effective date: 20120116 Ref country code: DE Ref legal event code: R081 Ref document number: 59710495 Country of ref document: DE Owner name: NU-KOTE INTERNATIONAL INC., FRANKLIN, US Free format text: FORMER OWNER: PELIKAN HARDCOPY PRODUCTION AG, NU-KOTE INTERNATIONAL INC., , US Effective date: 20120116 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20120622 Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R084 Ref document number: 59710495 Country of ref document: DE Effective date: 20120703 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20120705 Year of fee payment: 16 Ref country code: GB Payment date: 20120621 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20130621 Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20130624 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20140228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130630 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130630 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130701 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59710495 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59710495 Country of ref document: DE Effective date: 20150101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150101 |