EP0854232B1 - Machine pour la fabrication d'une bande fibreuse - Google Patents
Machine pour la fabrication d'une bande fibreuse Download PDFInfo
- Publication number
- EP0854232B1 EP0854232B1 EP97119333A EP97119333A EP0854232B1 EP 0854232 B1 EP0854232 B1 EP 0854232B1 EP 97119333 A EP97119333 A EP 97119333A EP 97119333 A EP97119333 A EP 97119333A EP 0854232 B1 EP0854232 B1 EP 0854232B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- press
- nip
- shoe
- machine according
- unit
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004519 manufacturing process Methods 0.000 title description 8
- 238000001035 drying Methods 0.000 claims description 8
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 7
- 230000000750 progressive effect Effects 0.000 claims description 4
- 238000007493 shaping process Methods 0.000 claims 1
- 238000011144 upstream manufacturing Methods 0.000 claims 1
- 238000010586 diagram Methods 0.000 description 5
- 229920000034 Plastomer Polymers 0.000 description 1
- 230000002745 absorbent Effects 0.000 description 1
- 239000002250 absorbent Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 238000009950 felting Methods 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
Images
Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F3/00—Press section of machines for making continuous webs of paper
- D21F3/02—Wet presses
- D21F3/0209—Wet presses with extended press nip
- D21F3/0218—Shoe presses
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F11/00—Processes for making continuous lengths of paper, or of cardboard, or of wet web for fibre board production, on paper-making machines
- D21F11/14—Making cellulose wadding, filter or blotting paper
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F3/00—Press section of machines for making continuous webs of paper
- D21F3/02—Wet presses
- D21F3/0281—Wet presses in combination with a dryer roll
Definitions
- the invention relates to a machine for producing a Tissue or tissue paper web with a pressure unit and a drying cylinder comprising Main press.
- DE-A-42 24 730 different embodiments are one Hygiene paper machine of the type mentioned above.
- One of these known embodiments includes a total of three press stations, namely two pre-presses between two upper rollers and two lower shoe press rollers with flexible Roller jacket and a main press with a pressure roller and a drying cylinder.
- the paper web is on a Roller former between a drainage screen and an upper one Tape created.
- Lower permeable felts Ribbons come together with the paper web and the top ribbon passed through the two pre-presses.
- an upper one Tape the paper web from a former to it afterwards through a pre-press between a top roller and a Bottom roller with bottom felt through to a main press between a pressure roller and a drying cylinder.
- the pressure roller a shoe press roll.
- the top felt is very dense and the bottom felt is very water absorbent.
- the lower roller is designed as a suction roller.
- the blind holes or grooves in the surface of the press jacket may be limited due to their manufacturing constraints Do not absorb the entire amount of water. This should be a reason why most of the people in the Embodiments described in DE-A-42 24 730 two pre-presses and in one case additionally a suction pressure roller in the Main press are provided.
- WO-A-9100389 is a machine for producing a fibrous web known with a shoe press unit, which is designed so that one in one Press gap of the shoe press unit over the gap length creates a progressive pressure profile Has pressure increase that begins in the area of the beginning of the gap and extends over at least a third of the gap length.
- the aim of the invention is a machine of the type mentioned kind of creating the disadvantages mentioned above are eliminated and the generated, by the sum of all line forces divided by the web speed defined Press pulse as optimally as possible in a high paper quality, a high production output and low operating costs implemented and with the use of any suction press rolls becomes dispensable.
- the special pressure distribution through a special Shape of the respective press shoe taking into account the radius of the counter roll, the press jacket and felt thickness as well as the dynamic compressibility of the used Press felts reached. Since the felt compressibility with the Operating time reduced, it is the selected one Shape of the press shoe around a compromise.
- the Values previously given for the pressure profile should in particular for a new or for two new ones as upper and lower felt intended press felts at the beginning of their operating time in apply for the first two to four days of operation.
- the respective shoe press unit is advantageous formed by a shoe press roll.
- the machine according to the invention is behind in the direction of web travel the first shoe press provided a second shoe press, the length of the press nip of the first shoe press being greater or is equal to 100 mm and the length of the press nip second shoe press in a range from about 60 to about 130 mm lies.
- the main press is the first viewed in the direction of web travel Press is in the direction of web travel in front of this first press preferably a preheating and / or predrying device provided to pre-dry or preheat the fibrous web, which significantly drains the fibrous web is improved.
- the preheating and / or predrying device advantageously comprises at least one heat radiator and / or at least a steam box.
- this preheating and / or predrying device also at least comprise a suction unit.
- This suction unit in turn can, for example, by at least one suction box and / or at least one suction roll can be formed.
- the Length of the press nip of the pre-press in a range of about 100 to about 250 mm and the length of the press nip of the main press in a range from about 50 to about 100 mm.
- the pressure roller can Main press a conventional with blind holes Press roll with a soft rubber cover with a hardness of preferably about shore A 89 to 80 (25 to 45 P&J).
- a soft rubber cover with a hardness of preferably about shore A 89 to 80 (25 to 45 P&J).
- P&J Precision Engineering Laboratory
- the Pussey & Jones device with 1/8 "ball measured plastomer points.
- the line force is limited to around 90 kN / m. Higher line forces are the longest possible Soft rubber covers of the pressure rollers not available or not to recommend.
- the pressure unit of the main press is a shoe press unit, preferably a shoe press roll.
- Both presses can vary over a wide line force range Need to be set. For example, the line force one or both presses are withdrawn to the Softness of the product at the expense of production performance increase. Conversely, for maximum production of Mass products high line forces can be set. moreover can old, already heavily compacted felts to the next planned standstill of the machine can continue to be used if the line force is somewhat reduced.
- the pressing unit of the main press is a shoe pressing unit, preferably a shoe press roll, is formed that generated in the nip of the main press maximum line force less than 250 kN / m and that in the range of the pressure rise gradient present at the beginning of the gap is lower than 50 kPa / mm.
- the pressure rise gradient in the first shoe press for new felt in the field of The beginning of the gap is less than or equal to 30 kPa / mm.
- the falling average gradient at the end of the press nip should preferably so steep that no significant rewetting the fibrous web through the separating from it Felt is done. According to a preferred embodiment in practice is accordingly provided that in the press nip the average gradient of the pressure drop of the respective shoe press at the end of the column in a range from about 400 to about 1000 kPa / mm.
- At least the press nip of the main press zone is simply felted.
- On Felt belt can both through the nip of a pre-press also be guided through the press nip of the main press.
- the press nip at least one pre-press is double felted.
- this Case is advantageously an upper felt band both through the press nip of the pre-press as well as through the press nip Main press and additionally a lower felt belt through the Press nip of the pre-press performed.
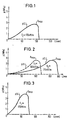
- Figure 1 shows the pressure profile in a press nip Embodiment of a 1-felt tissue machine with new Felt.
- the press nip in question is between a drying cylinder and a pressure roller.
- the pressure shown in MPa is shown in the diagram p plotted over the length L of the press nip, the is given here in mm.
- the line force generated in the press nip is about 170 kN / m.
- a soft suction press felt with a basis weight of 1,350 g / m 2 was used as the felt.
- the old felt still had about a third of the compressibility of the new felt.
- the press jacket was 6.2 mm thick and provided with blind holes.
- the maximum pressure p max is approximately 2.5 MPa.
- Figure 2 shows the pressure profile in the press nip one Prepress of an embodiment of a 2-felt tissue machine with new felts.
- the pressing pressure given in MPa is plotted over the length L of the press nip, which is given here in mm.
- the line force F L generated in the press nip is approximately 175 kN / m in the embodiment shown with a solid curve. In a further embodiment shown in broken lines, this line force F L is approximately 120 kN / m.
- the gap length is smaller in the second case than in the first case.
- Figure 3 shows the pressure profile in a press nip Main press of the 2-felt tissue machine again through this Main press guided top felt.
- the pressing pressure p given in MPa is plotted over the length L of the press nip, which is again given here in mm.
- the line force F L generated in the press nip is approximately 170 kN / m.
- the press nip of the main press is shorter than that Prepress nip.
- the maximum pressure in the main press higher than that in the pre-press.
Landscapes
- Paper (AREA)
- Sanitary Thin Papers (AREA)
Claims (19)
- Machine pour la fabrication d'une bande de tissu ouaté ou de papier hygiénique, avec au moins une unité de patin de pressage, dans laquelle il est prévu une presse principale comprenant une unité de pressage et un cylindre de séchage et au moins l'unité de pressage de la presse principale est formée par une unité de patin de pressage pour former un patin de pressage avec une fente de pressage allongée dans le sens de circulation de la bande et le premier patin de pressage, en considérant le sens de circulation de la bande, est conçu de telle façon qu'un profil de pression p(L), produit sur la longueur (L) de la fente dans la fente de pressage de celui-ci par un formage spécial du patin de pressage respectif en tenant compte du rayon d'un contre-cylindre, d'une épaisseur d'enveloppe de pressage et d'une épaisseur de feutre ainsi que d'une compressibilité dynamique des feutres de pressage utilisés, présente une hausse de pression progressive, qui commence dans la région du début de la fente et qui s'étend sur au moins un tiers, de préférence au moins la moitié, de la longueur (L) de la fente, dans lequel une force linéique maximale (FL) produite dans la fente de pressage de la presse principale est inférieure à 250 kN/m et un gradient de hausse de pression existant dans la région du début de la fente est inférieur à 50 kPa/mm.
- Machine suivant la revendication 1, caractérisée en ce que l'unité de patin de pressage est un rouleau de presse à patin.
- Machine suivant la revendication 1 ou 2, caractérisée en ce qu'il est prévu un deuxième patin de pressage après le premier patin de pressage, en considérant le sens de circulation de la bande, en ce que la longueur (L) de la fente de pressage du premier patin de pressage est supérieure ou égale à 100 mm et en ce que la longueur (L) de la fente de pressage du deuxième patin de pressage se situe dans une plage d'environ 60 à environ 130 mm.
- Machine suivant l'une quelconque des revendications précédentes, caractérisée en ce que la presse principale est la première presse en considérant le sens de circulation de la bande et en ce qu'il est prévu, avant cette première presse en considérant le sens de circulation de la bande, un dispositif de préchauffage et/ou de préséchage pour présécher, respectivement préchauffer la bande fibreuse.
- Machine suivant la revendication 4, caractérisée en ce que le dispositif de préséchage et/ou de préchauffage comprend au moins un radiateur de chaleur et/ou au moins un caisson de soufflage de vapeur.
- Machine suivant la revendication 4 ou 5, caractérisée en ce que le dispositif de préchauffage et/ou de préséchage comprend au moins une unité d'aspiration.
- Machine suivant la revendication 6, caractérisée en ce que l'unité d'aspiration comprend au moins un caisson d'aspiration et/ou au moins un rouleau aspirant.
- Machine suivant l'une quelconque des revendications précédentes, caractérisée en ce qu'une unité de pressage associée à une presse préliminaire est formée par une unité de patin de pressage et le premier patin de pressage est formé par cette presse préliminaire, en ce que l'unité de pressage de la presse principale est également formée par une unité de patin de pressage et en ce que la longueur (L) de la fente de pressage de la presse principale se situe dans une plage d'environ un tiers à environ deux tiers de la longueur (L) de la fente de pressage de la presse préliminaire.
- Machine suivant la revendication 8, caractérisée en ce que l'unité de pressage associée à la presse préliminaire est formée par une unité de patin de pressage et le premier patin de pressage est formé par cette presse préliminaire, en ce que l'unité de pressage de la presse principale est également formée par une unité de patin de pressage et en ce que la longueur (L) de la fente de pressage de la presse préliminaire se situe dans une plage d'environ 100 à environ 250 mm et la longueur (L) de la fente de pressage de la presse principale se situe dans une plage d'environ 50 à environ 100 mm.
- Machine suivant l'une quelconque des revendications précédentes, caractérisée en ce que le gradient de hausse de pression dans le premier patin de pressage avec des nouveaux feutres est inférieur ou égal à 30 kPa/mm dans la région du début de la fente.
- Machine suivant l'une quelconque des revendications précédentes, caractérisée en ce que l'unité de pressage de la presse principale est formée par une unité de patin de pressage, de préférence un rouleau de presse à patin, et en ce que, dans la fente de pressage de celle-ci, le gradient moyen de chute de pression à la fin de la fente se situe dans une plage d'environ 500 à 1000 kPa/mm.
- Machine suivant l'une quelconque des revendications 8 à 11, caractérisée en ce que l'unité de pressage de la presse préliminaire est formée par une unité de patin de pressage, de préférence par un rouleau de presse à patin, et en ce que, dans la fente de pressage de celle-ci, le gradient moyen de chute de pression à la fin de la fente se situe dans une plage d'environ 500 à 1000 kPa/mm.
- Machine suivant l'une quelconque des revendications 8 à 12, caractérisée en ce que la force linéique (FL) dans la première presse formée par la presse préliminaire est supérieure à celle produite dans la deuxième presse formée par la presse principale et en ce que la pression maximale (pmax) dans la deuxième presse est supérieure à celle produite dans la première presse.
- Machine suivant l'une quelconque des revendications précédentes, caractérisée en ce qu'au moins la fente de pressage de la zone de pressage principale est garnie d'un feutre simple.
- Machine suivant l'une quelconque des revendications 8 à 14, caractérisée en ce qu'une bande de feutre est menée à travers la fente de pressage de la presse préliminaire comme aussi à travers la fente de pressage de la presse principale.
- Machine suivant l'une quelconque des revendications 8 à 15, caractérisée en ce que la fente de pressage au moins de la presse préliminaire est garnie d'un feutre double.
- Machine suivant la revendication 16, caractérisée en ce qu'une bande de feutre supérieure est menée aussi bien à travers la fente de pressage de la presse préliminaire qu'à travers la fente de pressage de la presse principale et en plus une bande de feutre inférieure est menée à travers la fente de pressage de la presse préliminaire.
- Machine suivant l'une quelconque des revendications 1 à 17, caractérisée en ce que l'enveloppe de pressage du rouleau de pressage possède dans sa surface de pressage des cavités destinées à recueillir l'eau extraite par le pressage.
- Machine suivant l'une quelconque des revendications 8 à 18, caractérisée en ce que l'enveloppe du rouleau de presse à patin de la presse préliminaire ne possède dans sa surface extérieure aucune cavité destinée à recueillir de l'eau.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19654197 | 1996-12-23 | ||
| DE19654197A DE19654197A1 (de) | 1996-12-23 | 1996-12-23 | Maschine zur Herstellung einer Faserstoffbahn |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0854232A2 EP0854232A2 (fr) | 1998-07-22 |
| EP0854232A3 EP0854232A3 (fr) | 1999-07-28 |
| EP0854232B1 true EP0854232B1 (fr) | 2003-04-09 |
Family
ID=7816125
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP97119333A Expired - Lifetime EP0854232B1 (fr) | 1996-12-23 | 1997-11-05 | Machine pour la fabrication d'une bande fibreuse |
Country Status (3)
| Country | Link |
|---|---|
| US (1) | US6083349A (fr) |
| EP (1) | EP0854232B1 (fr) |
| DE (2) | DE19654197A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6669821B2 (en) | 1998-11-13 | 2003-12-30 | Fort James Corporation | Apparatus for maximizing water removal in a press nip |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19860687A1 (de) | 1998-12-29 | 2000-07-06 | Voith Sulzer Papiermasch Gmbh | Maschine sowie Verfahren zur Herstellung einer Faserstoffbahn |
| DE19902274A1 (de) * | 1999-01-21 | 2000-07-27 | Voith Sulzer Papiertech Patent | Siebpartie sowie Bandführungseinrichtung für eine solche Siebpartie |
| DE10003686A1 (de) * | 2000-01-28 | 2001-08-23 | Voith Paper Patent Gmbh | Maschine sowie Verfahren zur Herstellung einer Tissuebahn |
| JP2003533609A (ja) * | 2000-05-18 | 2003-11-11 | メッツォ ペーパー カルルスタッド アクチボラグ | ソフトクレープ紙の抄紙機および該抄紙機のプレスセクション |
| EP1156153B1 (fr) * | 2000-05-18 | 2007-01-24 | Metso Paper Karlstad Aktiebolag | Machine à papier crêpé souple et sa section de presses |
| DE10032251A1 (de) * | 2000-07-03 | 2002-01-17 | Voith Paper Patent Gmbh | Maschine sowie Verfahren zur Herstellung einer Faserstoffbahn |
| EP1251203B1 (fr) * | 2001-04-18 | 2007-06-13 | Stowe Woodward Aktiengesellschaft | Bande pour presse à patin |
| EP1293601A1 (fr) * | 2001-09-17 | 2003-03-19 | Stowe Woodward Aktiengesellschaft | Bande pour presse à patin |
| DE102004033751A1 (de) * | 2004-07-13 | 2006-02-02 | Voith Paper Patent Gmbh | Walzenmantel |
| EP2896743B1 (fr) | 2014-01-20 | 2016-06-29 | Valmet S.p.A. | Procédé et machine de fabrication d'une bande de papier de soie |
| SE542214C2 (en) * | 2018-10-12 | 2020-03-10 | Valmet Oy | A tissue paper making machine and a method of operating a tissue paper making machine |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FI65103C (fi) * | 1982-05-05 | 1984-03-12 | Tampella Oy Ab | Laongzonspress foer en pappersmaskin |
| FI842115A7 (fi) * | 1984-05-25 | 1985-11-26 | Valmet Oy | Pressparti med separata pressnyp i en pappersmaskin. |
| DE3705241A1 (de) * | 1986-12-24 | 1988-07-07 | Escher Wyss Gmbh | Verfahren zur mechanisch-thermischen entwaesserung einer faserstoffbahn |
| US5230776A (en) * | 1988-10-25 | 1993-07-27 | Valmet Paper Machinery, Inc. | Paper machine for manufacturing a soft crepe paper web |
| US4973384A (en) * | 1989-06-23 | 1990-11-27 | Beloit Corporation | Heated extended nip press apparatus |
| US5047122A (en) * | 1989-06-23 | 1991-09-10 | Beloit Corporation | Method for heated extended nip pressing |
| DE4102356C1 (fr) * | 1991-01-26 | 1992-01-23 | J.M. Voith Gmbh, 7920 Heidenheim, De | |
| US5167768A (en) * | 1991-11-07 | 1992-12-01 | Beloit Corporation | Wide nip web press and method using a press shoe with two pivots |
| DE4224730C1 (en) * | 1992-07-27 | 1993-09-02 | J.M. Voith Gmbh, 89522 Heidenheim, De | Tissue paper mfg. machine preventing moisture return - comprises shoe press for press unit(s) for drying tissue web, for min. press units |
| US5868904A (en) * | 1993-12-08 | 1999-02-09 | Valmet Corporation | Press section employing an extended nip press with suction counter roll |
| FI955014A7 (fi) * | 1995-10-20 | 1997-04-21 | Valmet Corp | Paperikoneen puristinosa, jossa käytetään pitkänippipuristinta |
-
1996
- 1996-12-23 DE DE19654197A patent/DE19654197A1/de not_active Withdrawn
-
1997
- 1997-11-05 EP EP97119333A patent/EP0854232B1/fr not_active Expired - Lifetime
- 1997-11-05 DE DE59709775T patent/DE59709775D1/de not_active Expired - Lifetime
- 1997-12-23 US US08/997,689 patent/US6083349A/en not_active Expired - Lifetime
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6669821B2 (en) | 1998-11-13 | 2003-12-30 | Fort James Corporation | Apparatus for maximizing water removal in a press nip |
| US7300552B2 (en) | 1998-11-13 | 2007-11-27 | Georgia-Pacific Consumer Products Lp | Method for maximizing water removal in a press nip |
| US7754049B2 (en) | 1998-11-13 | 2010-07-13 | Georgia-Pacific Consumer Products Lp | Method for maximizing water removal in a press nip |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0854232A2 (fr) | 1998-07-22 |
| US6083349A (en) | 2000-07-04 |
| DE19654197A1 (de) | 1998-06-25 |
| EP0854232A3 (fr) | 1999-07-28 |
| DE59709775D1 (de) | 2003-05-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1749934B1 (fr) | Machine pour la fabrication du papier tissu | |
| DE4224730C1 (en) | Tissue paper mfg. machine preventing moisture return - comprises shoe press for press unit(s) for drying tissue web, for min. press units | |
| EP0496965B1 (fr) | Section de presse | |
| EP0988417B1 (fr) | Secherie | |
| EP0309530B1 (fr) | Machine pour produire des bandes de materiaux fibreux | |
| EP0848106B1 (fr) | Section de pressage | |
| EP0854232A2 (fr) | Machine pour la fabrication d'une bande fibreuse | |
| EP1016754B1 (fr) | Machine et procédé pour la fabrication d'une bande fibreuse | |
| EP0708858B1 (fr) | Train de sechage d'une machine a papier | |
| EP1316641B1 (fr) | Section de pressage | |
| DE1696176B2 (de) | Verfahren zum herstellen von kompressiv verdichtetem papier | |
| EP1111126B1 (fr) | Section de presse | |
| EP0857818B1 (fr) | Machine pour la fabrication d'une bande fibreuse | |
| EP0837181B1 (fr) | Section de pressage | |
| EP0854230B1 (fr) | Press humide | |
| DE19633958A1 (de) | Saugpreßwalze | |
| DE29712682U1 (de) | Preßeinheit | |
| DE29624464U1 (de) | Maschine zur Herstellung einer Faserstoffbahn | |
| DE19912226A1 (de) | Verfahren und Vorrichtung zum Herstellen von Tissue-Papier sowie das damit erhältliche Tissue-Papier | |
| DE19801417A1 (de) | Pressenpartie | |
| DE19708966A1 (de) | Pressenanordnung | |
| DE19645408B4 (de) | Verfahren zur Herstellung einer Faserstoffbahn | |
| EP1026314A2 (fr) | Dispositif de pressage | |
| DE10132652A1 (de) | Pressenanordnung | |
| DE29923284U1 (de) | Papiermaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: VOITH SULZER PAPIERTECHNIK PATENT GMBH |
|
| AKX | Designation fees paid | ||
| 17P | Request for examination filed |
Effective date: 20000128 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): DE FI SE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: VOITH PAPER PATENT GMBH |
|
| 17Q | First examination report despatched |
Effective date: 20010824 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): DE FI SE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLBQ | Unpublished change to opponent data |
Free format text: ORIGINAL CODE: EPIDOS OPPO |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: PMT ITALIA S.P.A. Effective date: 20040109 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 20050531 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20151111 Year of fee payment: 19 Ref country code: DE Payment date: 20151119 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20151118 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59709775 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161106 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170601 |