EP0857529A1 - Metallrohre und Verfahren und Anlage zu deren Herstellung - Google Patents
Metallrohre und Verfahren und Anlage zu deren Herstellung Download PDFInfo
- Publication number
- EP0857529A1 EP0857529A1 EP98400079A EP98400079A EP0857529A1 EP 0857529 A1 EP0857529 A1 EP 0857529A1 EP 98400079 A EP98400079 A EP 98400079A EP 98400079 A EP98400079 A EP 98400079A EP 0857529 A1 EP0857529 A1 EP 0857529A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tubes
- casting
- metal
- blank
- mandrel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 12
- 238000000034 method Methods 0.000 title description 4
- 238000005266 casting Methods 0.000 claims abstract description 15
- 229910052751 metal Inorganic materials 0.000 claims abstract description 14
- 239000002184 metal Substances 0.000 claims abstract description 14
- 238000010622 cold drawing Methods 0.000 claims abstract description 9
- 238000009434 installation Methods 0.000 claims abstract description 8
- 238000010438 heat treatment Methods 0.000 claims abstract description 7
- 229910001338 liquidmetal Inorganic materials 0.000 claims abstract description 6
- 229910000881 Cu alloy Inorganic materials 0.000 claims abstract description 4
- 238000001816 cooling Methods 0.000 claims abstract description 4
- 238000003756 stirring Methods 0.000 claims abstract description 4
- 238000000605 extraction Methods 0.000 claims abstract description 3
- 230000005484 gravity Effects 0.000 claims abstract 2
- 230000007704 transition Effects 0.000 claims description 6
- 238000000137 annealing Methods 0.000 claims description 5
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims description 4
- 229910045601 alloy Inorganic materials 0.000 claims description 4
- 239000000956 alloy Substances 0.000 claims description 4
- 229910052802 copper Inorganic materials 0.000 claims description 3
- 239000010949 copper Substances 0.000 claims description 3
- 239000007787 solid Substances 0.000 claims description 3
- 239000007788 liquid Substances 0.000 claims description 2
- 238000003760 magnetic stirring Methods 0.000 claims 1
- 238000003303 reheating Methods 0.000 abstract 1
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 description 4
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 3
- 229910000570 Cupronickel Inorganic materials 0.000 description 3
- 230000007547 defect Effects 0.000 description 3
- 229910002804 graphite Inorganic materials 0.000 description 2
- 239000010439 graphite Substances 0.000 description 2
- 238000002844 melting Methods 0.000 description 2
- 230000008018 melting Effects 0.000 description 2
- ATJFFYVFTNAWJD-UHFFFAOYSA-N Tin Chemical compound [Sn] ATJFFYVFTNAWJD-UHFFFAOYSA-N 0.000 description 1
- 229910052790 beryllium Inorganic materials 0.000 description 1
- ATBAMAFKBVZNFJ-UHFFFAOYSA-N beryllium atom Chemical compound [Be] ATBAMAFKBVZNFJ-UHFFFAOYSA-N 0.000 description 1
- 229910017052 cobalt Inorganic materials 0.000 description 1
- 239000010941 cobalt Substances 0.000 description 1
- 238000009749 continuous casting Methods 0.000 description 1
- 239000012535 impurity Substances 0.000 description 1
- 230000006698 induction Effects 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 229910052759 nickel Inorganic materials 0.000 description 1
- 238000001953 recrystallisation Methods 0.000 description 1
- 238000009987 spinning Methods 0.000 description 1
- 238000011282 treatment Methods 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/006—Continuous casting of metals, i.e. casting in indefinite lengths of tubes
Definitions
- the present invention relates to metal tubes and their manufacturing processes and facilities.
- the eccentricity i.e. the variation of the thickness measured in different points of a tube circumference, is large and commonly reached 20%.
- the invention overcomes this drawback by making it possible to obtain a batch of metal tubes in which, for all the tubes in the batch and at some point of a tube whatsoever, the ratio of the difference between the thickness of the wall of the tube at this point and the average wall thickness of the tubes at the thickness average tube wall is less than 7% and commonly attains only 5%.
- tubes made of copper alloy use may in particular be made of tubes made of copper alloy.
- copper alloy mention may be made of cupro-nickel with nickel content varying from 5 to 35%, cupro-tin with tin content varying from 5 to 9%, special alloys such as cupro-nickel silicon, cuproberyllium and cupro-cobalt beryllium. The percentages are expressed by weight.
- the invention also relates to an installation for manufacturing tubes metallic as defined in claim 3.
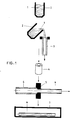
- the process illustrated in Figure 1 consists in melting, in a first stage, metal 1 in a tank 2.
- metal 1 in a tank 2.
- this metal 1 in a casting machine 3 so as to obtain a blank 4 tubular in the form of a hollow billet.
- we stretch the hollow bill 4 in a drawing bench 5 so as to stretch the tube 6 Cold.
- the tube 6 can then be treated if desired in an oven 7 of heat treatment.
- FIG. 2 The installation according to the invention is shown in Figures 2 and 3. It consists of a casting tool, shown in Figure 2, and a set of cold drawing and heat treatment, shown in Figure 3.
- a graphite core called mandrel 14 which is engaged in the opening of the bottom of the reservoir 12.
- the liquid metal is gradually solidified between the mold 13 and the mandrel 14 in the transition zone T.
- An extraction system 18 ensures the draft 17 is drawn through casting tools.
- An electronic assembly allows the adjustment of the draft parameters.
- the entire cold draft and heat treatment consists, on the one hand, a shrinking machine which allows a reduction of one end of the blank, on the other hand, of a bench or drawing press.
- the blank 17 is mounted on an internal shape 21 called a ball or mandrel.
- the constricted end of the blank extended by an extension 23 or faux-silk is introduced into a die 22, the false silk 23 protruding is hooked by a jaw system 24 on a carriage 25.
- the carriage 25 driven by a chain or a piston 26 pulls the blank between the die 22 and the ball 21.
- An annealing furnace or cell allows annealing after the drawing operation recrystallization of the blank 17.
- the shrinking machine - cold drawing - annealing cycle is repeated from two to n times, depending on the dimensions to be achieved.
- the blanks obtained have a temperature at the outlet of the ingot mold from 990 ° C. Their length is 2200 mm. They are free from defects, their ovalization is ⁇ 0.5%.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Metal Extraction Processes (AREA)
- Forging (AREA)
- Continuous Casting (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9701440 | 1997-02-07 | ||
| FR9701440A FR2759309B1 (fr) | 1997-02-07 | 1997-02-07 | Tubes metalliques et procede et installation pour les fabriquer |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0857529A1 true EP0857529A1 (de) | 1998-08-12 |
Family
ID=9503467
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98400079A Withdrawn EP0857529A1 (de) | 1997-02-07 | 1998-01-16 | Metallrohre und Verfahren und Anlage zu deren Herstellung |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0857529A1 (de) |
| FR (1) | FR2759309B1 (de) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2008072787A3 (en) * | 2006-12-14 | 2008-12-04 | Cta Technology Proprietary Ltd | Manufacturing method for a multi-channel copper tube, and manufacturing apparatus for the tube |
| WO2013020241A1 (es) * | 2011-08-10 | 2013-02-14 | Madeco S.A. | Producción de tubos a través de colada continua |
| CN109127772A (zh) * | 2018-10-31 | 2019-01-04 | 哈尔滨工业大学 | 一种减少内表面擦伤的铝基复合材料热挤压管材制造方法 |
| US11179771B2 (en) * | 2019-09-20 | 2021-11-23 | Harbin Institute Of Technology | Equipment and method of semi-continuous casting optimized by synergistic action of traveling magnetic field and ultrasound wave for thin-walled alloy casting with equal outer diameter |
| CN116571701A (zh) * | 2023-06-08 | 2023-08-11 | 邢台鑫晖铜业特种线材有限公司 | 一种多元铜合金熔炼双轴向回转流槽、配料密封组件 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4000773A (en) * | 1976-02-09 | 1977-01-04 | Gus Sevastakis | Die assembly for continuous vertical casting of tubular metallic products |
| JPS59212146A (ja) * | 1983-05-16 | 1984-12-01 | Chuetsu Gokin Chuko Kk | 横型連続鋳造装置 |
| US4616500A (en) * | 1985-02-25 | 1986-10-14 | George A. Mitchell Company | Method for producing tubing of varying wall thickness |
| US5279353A (en) * | 1992-06-04 | 1994-01-18 | Nielsen Sr William D | Method and apparatus to effect a fine grain size in continuous cast metals |
| EP0615794A1 (de) * | 1993-02-27 | 1994-09-21 | KM Europa Metal Aktiengesellschaft | Verfahren zur Herstellung einer Stopfenkammer beim Kaskadenziehen von Rohren und Vorrichtung zur Durchführung des Verfahrens |
-
1997
- 1997-02-07 FR FR9701440A patent/FR2759309B1/fr not_active Expired - Fee Related
-
1998
- 1998-01-16 EP EP98400079A patent/EP0857529A1/de not_active Withdrawn
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4000773A (en) * | 1976-02-09 | 1977-01-04 | Gus Sevastakis | Die assembly for continuous vertical casting of tubular metallic products |
| JPS59212146A (ja) * | 1983-05-16 | 1984-12-01 | Chuetsu Gokin Chuko Kk | 横型連続鋳造装置 |
| US4616500A (en) * | 1985-02-25 | 1986-10-14 | George A. Mitchell Company | Method for producing tubing of varying wall thickness |
| US5279353A (en) * | 1992-06-04 | 1994-01-18 | Nielsen Sr William D | Method and apparatus to effect a fine grain size in continuous cast metals |
| EP0615794A1 (de) * | 1993-02-27 | 1994-09-21 | KM Europa Metal Aktiengesellschaft | Verfahren zur Herstellung einer Stopfenkammer beim Kaskadenziehen von Rohren und Vorrichtung zur Durchführung des Verfahrens |
Non-Patent Citations (1)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 009, no. 084 (M - 371) 13 April 1985 (1985-04-13) * |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2008072787A3 (en) * | 2006-12-14 | 2008-12-04 | Cta Technology Proprietary Ltd | Manufacturing method for a multi-channel copper tube, and manufacturing apparatus for the tube |
| EP2202015A1 (de) * | 2006-12-14 | 2010-06-30 | Cta Technology (Proprietary) Limited | Vorrichtung zur Herstellung eines Mehrkanalkupferrohres |
| US8336604B2 (en) | 2006-12-14 | 2012-12-25 | Cta Technology (Proprietary) Limited | Manufacturing method for a multi-channel copper tube, and manufacturing apparatus for the tube |
| US8869874B2 (en) | 2006-12-14 | 2014-10-28 | Cta Technology (Proprietary) Limited | Manufacturing method for a multi-channel copper tube, and manufacturing apparatus for the tube |
| WO2013020241A1 (es) * | 2011-08-10 | 2013-02-14 | Madeco S.A. | Producción de tubos a través de colada continua |
| CN109127772A (zh) * | 2018-10-31 | 2019-01-04 | 哈尔滨工业大学 | 一种减少内表面擦伤的铝基复合材料热挤压管材制造方法 |
| CN109127772B (zh) * | 2018-10-31 | 2019-10-15 | 哈尔滨工业大学 | 一种减少内表面擦伤的铝基复合材料热挤压管材制造方法 |
| US11179771B2 (en) * | 2019-09-20 | 2021-11-23 | Harbin Institute Of Technology | Equipment and method of semi-continuous casting optimized by synergistic action of traveling magnetic field and ultrasound wave for thin-walled alloy casting with equal outer diameter |
| CN116571701A (zh) * | 2023-06-08 | 2023-08-11 | 邢台鑫晖铜业特种线材有限公司 | 一种多元铜合金熔炼双轴向回转流槽、配料密封组件 |
Also Published As
| Publication number | Publication date |
|---|---|
| FR2759309A1 (fr) | 1998-08-14 |
| FR2759309B1 (fr) | 1999-03-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5575325A (en) | Semi-molten metal molding method and apparatus | |
| FR2537897A1 (fr) | Procede de coulee continue de metal | |
| EP0103220B1 (de) | Induktiv beheizter Giesskanal | |
| EP0092477B1 (de) | Verfahren und Vorrichtung zur Herstellung von Hohlblöcken aus Stahl | |
| FR2543461A1 (fr) | Procede pour fabriquer des tubes d'acier sans soudure | |
| FR2759309A1 (fr) | Tubes metalliques et procede et installation pour les fabriquer | |
| US3259975A (en) | Tube manufacture | |
| RU2201311C2 (ru) | Способ изготовления контактных проводов из меди и ее сплавов | |
| FR2568153A1 (fr) | Procede et dispositif ameliores pour le coulage horizontal et continu du metal | |
| EP0215874B1 (de) | Mäntel für stranggiessrollen | |
| US2086135A (en) | Method of making a metal-clad rod | |
| FR2511038A1 (fr) | Procede de fabrication de produits semi-finis siderurgiques en aciers durs mettant en oeuvre une operation de coulee continue | |
| FR2570304A1 (fr) | Procede de reglage du niveau de la ligne de contact de la surface libre du metal avec la lingotiere dans une coulee verticale | |
| CH664310A5 (fr) | Procede et appareil de fabrication de moules pour le moulage en continu de metaux. | |
| CA1121570A (fr) | Anneau pour roue de machine de coulee | |
| FI114901B (fi) | Menetelmä ja laitteisto putkien valmistamiseksi valssaamalla | |
| EP0038275B1 (de) | Vorrichtung zum Stranggiessen von Rohrluppen | |
| EP0588128B1 (de) | Verfahren zum Warmschmieden bei Ultrahoch -Temperatur | |
| JP3671868B2 (ja) | 高Cr含有鋼の鋳造方法 | |
| RU2230625C1 (ru) | Способ изготовления тонкостенных труб из меди и ее сплавов | |
| Dong et al. | Super-high strength 7 A 60 Al alloy by low frequency electromagnetic cast (I)- as-cast structures of billets with diameter of 0. 2 m. | |
| FR2816858A1 (fr) | Procede de fabrication de pieces en alliages metalliques, avec un refroidissement avant pressage | |
| EP0856368B1 (de) | Walzenring zum Stranggiessen von Metallen oder metallischen Legierungen, insbesondere für Aluminium | |
| RU2230623C1 (ru) | Способ изготовления тонкостенных труб из меди и ее сплавов | |
| EP0452294B1 (de) | Verfahren und Vorrichtung zum Stranggiessen eines Metalls |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE ES FI FR GB IT LI SE |
|
| AX | Request for extension of the european patent |
Free format text: SI |
|
| 17P | Request for examination filed |
Effective date: 19981105 |
|
| AKX | Designation fees paid |
Free format text: AT BE CH DE ES FI FR GB IT LI SE |
|
| AXX | Extension fees paid |
Free format text: SI PAYMENT 19981105 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AT BE CH DE ES FI FR GB IT LI SE |
|
| 17Q | First examination report despatched |
Effective date: 20010706 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN WITHDRAWN |
|
| 18W | Application withdrawn |
Withdrawal date: 20020104 |