EP0915014A1 - Verfahren und Vorrichtung zum Drucken von Zeichen auf tablettenförmige pharmazeutische Artikel und zum Ausrichten derselben in einer Blisterpackung - Google Patents
Verfahren und Vorrichtung zum Drucken von Zeichen auf tablettenförmige pharmazeutische Artikel und zum Ausrichten derselben in einer Blisterpackung Download PDFInfo
- Publication number
- EP0915014A1 EP0915014A1 EP98120926A EP98120926A EP0915014A1 EP 0915014 A1 EP0915014 A1 EP 0915014A1 EP 98120926 A EP98120926 A EP 98120926A EP 98120926 A EP98120926 A EP 98120926A EP 0915014 A1 EP0915014 A1 EP 0915014A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- articles
- station
- packaging
- blistered
- printing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000004806 packaging method and process Methods 0.000 title claims abstract description 51
- 239000008188 pellet Substances 0.000 title claims abstract description 10
- 238000000034 method Methods 0.000 title claims description 20
- 239000005022 packaging material Substances 0.000 claims abstract description 19
- 238000007789 sealing Methods 0.000 claims abstract description 10
- 238000005520 cutting process Methods 0.000 claims abstract description 7
- 239000002775 capsule Substances 0.000 claims description 36
- 239000007894 caplet Substances 0.000 claims description 8
- 238000005553 drilling Methods 0.000 claims description 7
- 238000000151 deposition Methods 0.000 claims description 3
- 230000001360 synchronised effect Effects 0.000 claims description 3
- 239000003826 tablet Substances 0.000 description 21
- 239000003814 drug Substances 0.000 description 12
- 229940079593 drug Drugs 0.000 description 12
- 239000000463 material Substances 0.000 description 9
- 239000000825 pharmaceutical preparation Substances 0.000 description 8
- 229940127557 pharmaceutical product Drugs 0.000 description 8
- 239000004033 plastic Substances 0.000 description 4
- 239000003086 colorant Substances 0.000 description 3
- 238000009826 distribution Methods 0.000 description 3
- 230000009977 dual effect Effects 0.000 description 3
- 230000005484 gravity Effects 0.000 description 3
- 239000000047 product Substances 0.000 description 3
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 2
- 229910052782 aluminium Inorganic materials 0.000 description 2
- 239000011888 foil Substances 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 239000011148 porous material Substances 0.000 description 2
- 239000002253 acid Substances 0.000 description 1
- 150000007513 acids Chemical class 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 239000012467 final product Substances 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 239000011159 matrix material Substances 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- 239000002985 plastic film Substances 0.000 description 1
- 229920006255 plastic film Polymers 0.000 description 1
- 238000003908 quality control method Methods 0.000 description 1
- 210000003296 saliva Anatomy 0.000 description 1
- 239000003566 sealing material Substances 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 210000002784 stomach Anatomy 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 238000011144 upstream manufacturing Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B63/00—Auxiliary devices, not otherwise provided for, for operating on articles or materials to be packaged
- B65B63/005—Auxiliary devices, not otherwise provided for, for operating on articles or materials to be packaged for marking or coding articles prior to packaging
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F7/00—Rotary lithographic machines
- B41F7/20—Details
- B41F7/24—Damping devices
- B41F7/36—Inking-rollers serving also to apply ink repellants
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/02—Enclosing successive articles, or quantities of material between opposed webs
- B65B9/04—Enclosing successive articles, or quantities of material between opposed webs one or both webs being formed with pockets for the reception of the articles, or of the quantities of material
- B65B9/045—Enclosing successive articles, or quantities of material between opposed webs one or both webs being formed with pockets for the reception of the articles, or of the quantities of material for single articles, e.g. tablets
Definitions
- This invention relates to a method and apparatus for printing indicia on pharmaceutical pellet-shaped articles and placing them in a moving blistered receptacle.
- the invention relates to an apparatus using a transporting device to place a pellet-shaped article in a blistered receptacle such that the articles are uniformly oriented with respect to color and/or indicia as they appear through the clear portion of the blister.
- the present invention has special applicability towards two types of pellet shaped articles.
- substantially round tablets having first and second differently colored sides can be oriented within the blister package such that the same color is visible through the clear portion of the blister package.
- a predetermined (colored) side of the tablet will be selected to receive indicia, which will face the clear portion of the blister package.
- substantially oblong capsules or caplets having differently colored ends can be oriented within the blister package such that ends having the same color will face the same direction.
- the concept of providing solid medication in unit doses for oral consumption is well known and commercially available wherever pharmaceutical products are sold.
- the medication is packaged for distribution and sale in a blistered or bottled package.
- the present invention is primarily concerned with the blistered package and the orientation of a pellet-shaped article bearing printed indicia and/or dual colors so the orientation of the indicia and/or the dual colors remains visible to the consumer through the clear portion of the blistered recess.
- the blistered package is known as a package composed of a thermoformed plastic film having a plurality of recesses or blisters arranged in a symmetrical pattern for receiving a dose of medication.
- the blistered package is typically covered by heat sealing a film of usually opaque material, such as aluminum foil, to the face of the package with the product contained in the blisters.
- a film of usually opaque material such as aluminum foil
- a package contains a trademark, logo and/or dosage indicator printed on the article prior to the article being placed in the recess or blister.
- arbitrary placement of the articles in a blistered package often obscures the printed information, thereby requiring additional effort to determine the type of medication, and possibly exposing the user to mistakenly ingesting the wrong medication, which may lead to catastrophic or fatal results.
- tablets may be placed within the blister such that the indicia (printed on only one side) cannot be viewed through the blister.
- the differently colored ends may be oppositely oriented from one article to the next thus giving a disorganized appearance. In each case, such packaging gives the impression that the medication placed in the blistered package was not subjected to quality control during manufacturing.
- the tablets or capsules initially have indicia printed upon them, then they are forwarded to be packaged, yet the capsules are not color organized and/or the tablets are not oriented for the user to read the indicia.
- One method to obviate the indicia orientation problem is to place indicia on two or more sides of the capsule or tablet so the printed indicia will be visible regardless of the article's orientation.
- this method results in increased costs due to the multiple apparatuses necessary to carry out the process, as well as the additional printing.
- This method may also have drawback that, although the indicia is visible on the tablets, the background base color of the tablets facing the clear portion of the blister package are different.
- USP 3,933,239 discloses a capsule positioning machine.
- the machine includes a hopper supplying radially ordered capsules to transporting and inverting drums where the capsules are oriented to be positioned on a moving conveyor system.
- the capsules are positioned in the conveyor in a uniform manner, no printed indicia is placed on the capsules, thereby requiring the capsules to be printed at another station, or even worse, the capsules have no printing placed upon them leaving the user uninformed as to the contents of the capsules.
- the capsules are placed on a conveyor, indicating a necessity of having to be packaged at another station or machine thereby adding cost to packaging the pharmaceutical products.
- Yoshida does not provide a mechanism for color based orientation of caplets having differently colored ends because caplets cannot be gravity oriented due to their uniform cross-sections and weight.
- USP 5,415,321 discloses a apparatus for feeding a plurality of tablets simultaneously onto a matrix of blister packaging.
- the apparatus comprises a feeder having a rectangular housing including a product bin with a plurality of openings through which capsules fall when the feeder is vibrated.
- the capsules are placed in blistered packaging, however, the capsules are not marked with printed indicia, as well as being randomly positioned within the blistered packaging thereby making it unsure whether consumers will be able to read any information printed or indicated on the capsule, and know the nature or type of medication they are ingesting.
- USP 3,545,164 discloses a apparatus and method for filling packaging receptacles.
- the apparatus has a top plate for supporting a number of randomly grouped capsules.
- the capsules are then agitated by a vibrator and separated from the supply.
- the capsules pass through guide mouths and are deposited in blistered packaging where the packages are closed and sealed once they are filled. Again, no device is provided to mark the capsules with printed indicia and no tool is until to uniformly align the positioning of the capsules within the packaging.
- USP 4,790,118 discloses a medication packaging and dispensing machine for packaging medication specific to a patient.
- the unit dose package includes the patient name, day, and hours of administration prescribed for the patient.
- the tablets or medication is not labeled, and thus the orientation of the capsule in the packaging system is of little importance.
- USP 4,999,979 discloses a machine for continuously packing pharmaceutical products in plastic material containers.
- the machine comprises a station for receiving and unwinding reels of the plastic material, heating stations, a thermaforming station, a dosing station, a sealing station and a cutting station.
- the system does not have a station for printing indicia upon the pharmaceutical products.
- the produets are not oriented in a predetermined manner within the plastic container.
- a packaging apparatus includes a transporting device capable of placing capsules or tablets in blistered packaging with the uniform color orientation of dual-colored capsules and/or the printed indicia of the tablets visible through the clear portion of the packaging.
- the transporting device can be a drum having a plurality of peripherally spaced cavities adapted to receive and maintain pellet shaped articles.
- the drum is in rotary arrangement to the feeding, printing, and packaging stations. The cavities receive the articles from the feeding station and transport the articles to the printing station.
- trademark or logo information and/or dosage strength are marked on a face of the articles.
- the drum and the packaging station are synchronized so that the cavities of the drum and the blistered receptacles of the packaging station are aligned, so that when the drum delivers the printed articles to the packaging station, the articles are placed in blistered receptacles such that the uniform color orientation of dual-colored capsules/caplets or the indicia of tablets is visible to the consumer through the clear portion of the blister.
- the feeding station comprises, for example, a gravity feed hopper located above the transporting device.
- the hopper is designed to frictionally feed the randomly ordered articles into the cavities of the drum in a controlled manner.
- the articles are then transported to the printing station where a printer marks indicia upon the articles.
- the printer can be an ink jet or contact printer.
- the drum of the transporting device will contain a vacuum for maintaining the articles in their respective cavities.
- the orientation of the articles will be maintained through the printing station.
- air drawn into the cavities is stopped, thereby forcing the articles to drop into the receptacles with the uniform color orientation or the indicia visible through the clear portion of the blister.
- other devices such as amp feed, maybe used to sport the articles through the various stations.
- the packaging station has a conveyor system that continuously supplies packaging material.
- the packaging material comprises blistered receptacles having a clear portion capable of receiving and retaining a tablet or pellet. Because the conveyor and drum are operatively associated with each other, the blistered receptacles are aligned with the cavities. Therefore, once the articles pass the back guide they drop directly into the blistered receptacles with the uniform color orientation or the printed indicia facing through the clear portion.
- a sealing station Downstream on the conveyor system is a sealing station where a seal is applied to the blistered receptacles.
- a film of material typically opaque, such as aluminum foil, is heat sealed to the receptacles, alter which the packaged material is fed to a cutting station where it is separated by a blade in packages of four, six, eight, or such doses per packet for use by a consumer.
- the drum may have an arcuate back guide provided having curvature substantially similar as the drum to maintain the orientation of the articles.
- the guide is adjustably positioned with respect to the drum to allow different sized articles to be transported.
- the novel method accurately and automatically controls the movement of the articles from the feeding station, through the printing station and deposits them at the packaging station into the blistered package with the proper orientation.
- the resulting apparatus and method for packaging printed pharmaceutical capsules or tablets places the articles with dual colors or printed indicia in blistered receptacles in a predetermined manner.
- the articles need only be printed on one side, saving time and money.
- the visibility of the indicia provides the consumer with the required information to help prevent improper administration of dosages.
- the need for less procedures to package the articles results in a more efficient apparatus wherein the manufacturing to process additional articles fester, resulting in a more economical apparatus that also provides a better informed consumer. Consequently, the present apparatus and method for packaging pellet-sped pharmaceutical articles can be used so consumers can take doses of medication more easily, safely, and with less dangerous consequences.
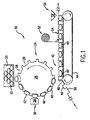
- FIG. 1 is a perspective view of one example of an apparatus 10 for printing indicia on pellet shaped pharmaceutical articles 12 and orienting the articles 12 within blistered packaging according to a preferred embodiment of the present invention.
- Apparatus 10 includes a transporting device 24 that coopates with a feeding station 20, printing station 36, and packaging station 42.
- the feeding station 20 is designed to distribute a plurality of randomly ordered pellet shaped pharmaceutical articles 12 to the transporting device 24.
- the transporting device 24 is synchronized with the feeding station 20 and packaging station 42. Therefore, the transporting device 24 is able to continuously receive the articles 12 from the feeding station 20, guide the articles 12 through the printing station 36, deposit the articles in the packaging station 42, and repeat the cycle uninterrupted.
- the printing station 36 can be upstream of the transporting device 24, especially if the articles are preoriented such that a desired portion (e.g. end or side) of the articles will be visible in a proper orientation within the clear portion of the blister package.
- the transporting device 24 is depicted as comprising a drum 26.
- the transporting device 24 is not restricted to this design and may be comprised of any number of transporting apparatus, such as a ramp-feed type device, for example.
- the drum 26 has cavities 28 adapted to receive the articles 12 from the feeding station 20. Once in their respective cavities 28, the articles 12 are taken to a printing station 36 having a printer 38 for marking the article 12 with printed indicia 40.
- the cavities 28 may be specially shaped to maintain the positioning of the articles 12 until forwarding the articles 12 to packaging station 42.
- the data is marked by a printer 38 such as an ink jet or contact printer, located tangentially to the transporting device 24 and between the feeding station 20 and packaging station 42 along the transporting path of the drum 26.
- the indicia 40 may provide information such as the manufacturer's trademark, a logo, and/or the dosage strength as well. From the printing station 36, the articles 12 are taken to the packaging station 42.
- the packaging station 42 has a conveyor 44 for continuously supplying packaging material 46 defining blistered receptacles 48.
- Each blistered receptacle 48 has a clear portion 50 capable of receiving and retaining the articles 12. Since the drum 26 and the blistered receptacles 48 are aligned, the drum 26 is able to deposit the articles 12 into the blistered receptacles 48 with the article 12 oriented so the proper color and/or printed indicia 40 on the article 12 is visible (in proper orientation) through each clear portion 50.
- a sealing station 52 Downstream of where the drum 26 deposits the articles 12 into the blistered receptacles 48, there may be a sealing station 52 where a seal 54 is applied to the open side of the packaging material 46. Ideally, the sealing material comprises opaque material.
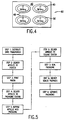
- downstream of the sending station 52 there may be a cutting station 56 where the filled packaging material 46 is separated by a blade 58. As shown in Fig. 4, the marerial 46 is separated into multiple packages 60 of articles 12 with the indicia 40 visible through the clear portion 50 of the blistered receptacles 48 and ready for sale or distribution.
- the feeding station 20 may provide a hopper 22 designed to contain and distribute the articles 12 to the transporting device 24.
- the articles 12 for example, will be gravity fed to the cavities 28 in the device 24 as the cavities 28 pass underneath the opening (not shown) of the hopper 22.
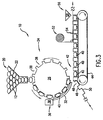
- FIG. 2 depicts a alternative embodiment of the present invention where a vacuum 34 is placed inside the drum 26.
- the drum in this case may include a shell 26A having pores that communicate the cavities and the vacuum.
- the shell 26A is guided about a non-porous stationary guide 27 such that the vacuum 34 is maintained along the path between the hopper and the conveyor 44.
- the vacuum helps the drum 26 maintain the orientation of the articles 12 within the cavities 28 along the path.
- the vacuum 34 maintains the orientation by drawing air into the cavities 28 through the pores, creating a negative air pressure, thereby keeping the articles 12 secured in the cavities 28.
- the negative air pressure is only applied along the section of the drum 26 between the feeding station 20 and the packaging station 42.
- the negative air pressure is cut off when the cavities 28 are aligned with the blistered receptacles 48 on the conveyor 44. Consequently, the articles 12 drop or are guided into the receptacles 48 with the indicia 40 being visible to the consumer through the clear portion 50 of the receptacles 48.
- Figure 3 depicts a optional apparatus for maintaining the orientation of the articles 12 in the transporting device 24.
- a back guide 32 having a curvature similar to that of the drum 26 is provided.
- the back guide 32 prevents the articles from losing their orientation within the cavities 38 and from falling out of the drum 26.
- the drum deposits the articles 12 into the blistered receptacles 48 so that the printed indicia 40 on the articles 12 is visible to the consumer through the clear portion 50.
- the vacated cavity 28 continues around to the feeding station 20 to pick up another article 12.
- the position of the back guide 32 is adjustable in relation to the drum 26 so that articles 12 of different dimensions may be printed and packaged.
- Step 1 of the method entails distributing the articles 12 onto a transporting device 24.
- Step 2 involves delivering the articles 12 on the transporting device 24 to a printing station 36 having a printer 38.
- Step 3 includes printing of indicia 40 onto the articles 12.
- Step 4 includes delivering the printed articles 12 to a packaging station.
- Step 5 entails depositing the printed articles 12 from the transporting device 24 onto a packaging station 42 having a conveyor 44 for continuously supplying packaging material 46 containing blistered receptacles 48, each having a clear portion 50 and capable of receiving and retaining an article, wherein the printed indicia 40 on the articles 12 is visible to the consumer through the clear portion 50.
- Figure 5 also includes step 6, delivering the packaged articles 12 to a sealing station 52.
- Step 7 involves sealing the open side of the packaging material 46.
- Step 8 entails delivering the scaled packages to a cutting station 56.
- Step 9 requires separating the packaged material 46 with a blade 58 resulting in multiple packages of articles 60 ready for sale or distribution.
- the articles 12 may be arranged in a predetermined order prior to being fed to the transporting device 24. See Figure 1A.
- the articles 12 may first pass through a drilling station 62 where a mechanical time-release mechanism 64 is created.
- the time-release mechanism 64 is formed by creating a depression or hole in the coating of the article 12 with a laser or other drilling device 66 so saliva and assorted body acids interact with the chemical composition within the article 12. This allows certain portions of the interior of the articles 12 to be immediately exposed to the stomach and absorbed into the bloodstream when ingested.
- the articles 12 are transported to the feeding station 20 and/or the transporting device 24 as indicated by arrow 67.
- the drilling station 62 may be located between the feeding station 20 and the printing station 36. See Figure 3.
- the portion of the article 12 that will have the indicia 40 placed on it and exposed through the clear portion 50 of the blister receptacle 48 will also have the time-release mechanism 64, thereby resulting in the indicia 40 camouflaging the depression or hole.
- the drilling station can be located downstream of the printing station 36 ( Figure 2) depending on the desired appearance of the final product.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US96460997A | 1997-11-05 | 1997-11-05 | |
| US964609 | 1997-11-05 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0915014A1 true EP0915014A1 (de) | 1999-05-12 |
Family
ID=25508765
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98120926A Withdrawn EP0915014A1 (de) | 1997-11-05 | 1998-11-04 | Verfahren und Vorrichtung zum Drucken von Zeichen auf tablettenförmige pharmazeutische Artikel und zum Ausrichten derselben in einer Blisterpackung |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP0915014A1 (de) |
Cited By (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2368830A (en) * | 2000-11-11 | 2002-05-15 | P J Contractors Ltd | Pack feeding |
| US6851874B2 (en) * | 2002-06-18 | 2005-02-08 | Hewlett-Packard Development Company, L.P. | Methods and systems of producing blister packaging |
| US7156308B2 (en) | 2001-12-17 | 2007-01-02 | International Barcode Corporation | Double-sided bar code doubling as a single bar code |
| US7182259B2 (en) | 2001-10-26 | 2007-02-27 | International Barcode Corporation | Method and apparatus for applying bar code information to products during production |
| EP2088867A4 (de) * | 2006-10-19 | 2010-12-01 | Wrigley W M Jun Co | Esswaren, die kontaktfrei bedruckt wurden, sowie gerät und verfahren zu ihrer herstellung |
| US20120052118A1 (en) * | 2010-07-19 | 2012-03-01 | Carlos Salazar Altamar | Apparatus and process for encapsulating capsules or other solid dosage forms within capsules |
| US8371216B2 (en) | 2009-12-03 | 2013-02-12 | Mars, Incorporated | Conveying and marking apparatus and method |
| WO2013040599A3 (en) * | 2011-09-16 | 2013-05-10 | Tri-Star Technologies | Laser capsule marking system and method |
| US20150174008A1 (en) * | 2010-07-19 | 2015-06-25 | Procaps SAS | Apparatus and process for encapsulating microparticles with liquid in soft gel capsules |
| CN104828271A (zh) * | 2015-04-30 | 2015-08-12 | 瑞安市安泰制药机械有限公司 | 高速双铝包装机 |
| CN106112270A (zh) * | 2016-07-26 | 2016-11-16 | 中核(天津)机械有限公司 | 管件的自动打标装置 |
| CN107031882A (zh) * | 2016-02-04 | 2017-08-11 | Ckd株式会社 | 拾取装置和泡罩包装机 |
| JP2018114041A (ja) * | 2017-01-17 | 2018-07-26 | フロイント産業株式会社 | 錠剤印刷包装装置及び錠剤印刷包装方法 |
| CN108706335A (zh) * | 2018-06-11 | 2018-10-26 | 上海松川远亿机械设备有限公司 | 用于散装颗粒物料包装的进料整理装置 |
| CN108860744A (zh) * | 2018-06-11 | 2018-11-23 | 上海松川远亿机械设备有限公司 | 散装颗粒物料的进料整理工艺 |
| CN109677670A (zh) * | 2019-01-15 | 2019-04-26 | 苏波 | 一种槟榔自动包装设备 |
| JP7083719B2 (ja) | 2018-07-25 | 2022-06-13 | Ckd株式会社 | Ptpシートの製造方法 |
| JP7142521B2 (ja) | 2018-09-03 | 2022-09-27 | Ckd株式会社 | Ptp包装機 |
| CN116829463A (zh) * | 2020-12-11 | 2023-09-29 | 皇家戴维艾格伯茨有限公司 | 饮料粉囊包和饮料粉囊包制造设备 |
| CN117864510A (zh) * | 2024-03-11 | 2024-04-12 | 新华制药(高密)有限公司 | 一种药片泡罩包装机 |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3545164A (en) | 1968-08-22 | 1970-12-08 | Warnaco Inc | Apparatus and method for filling packaging receptacles |
| DE2031896A1 (de) * | 1970-06-27 | 1972-01-05 | Hassia Verpackungsmaschinen GmbH, 6479 Ranstadt | Verfahren und Vorrichtung zum Herstellen, Füllen, Abdeckein und Vereinzeln von tiefgezogenen Tabletten packungen |
| US3933239A (en) | 1973-11-15 | 1976-01-20 | Takeda Chemical Industries, Ltd. | Capsule positioning machine |
| WO1982003842A1 (en) * | 1981-05-04 | 1982-11-11 | Michael E Ackley | Material orientation and printing apparatus and method |
| US4790118A (en) | 1987-04-13 | 1988-12-13 | Econodose, Inc. | Medication packaging and dispensing system |
| US4999979A (en) | 1988-07-13 | 1991-03-19 | A.R.C.I.L. | Machine for continuously packing in particular food or pharmaceutical products in plastic material containers |
| JPH03148430A (ja) * | 1989-10-23 | 1991-06-25 | Fujisawa Pharmaceut Co Ltd | 錠剤印刷包装機 |
| JPH0776305A (ja) * | 1993-09-10 | 1995-03-20 | Ckd Corp | 錠剤包装機 |
| US5415321A (en) | 1993-10-19 | 1995-05-16 | Gemel Precision Tool Co., Inc. | Feeder for pharmaceutical thermoform packaging machines |
| WO1996018539A1 (en) * | 1994-12-16 | 1996-06-20 | I.M.A. Industria Macchine Automatiche S.P.A. | System for feeding articles to blisters of a blister band |
-
1998
- 1998-11-04 EP EP98120926A patent/EP0915014A1/de not_active Withdrawn
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3545164A (en) | 1968-08-22 | 1970-12-08 | Warnaco Inc | Apparatus and method for filling packaging receptacles |
| DE2031896A1 (de) * | 1970-06-27 | 1972-01-05 | Hassia Verpackungsmaschinen GmbH, 6479 Ranstadt | Verfahren und Vorrichtung zum Herstellen, Füllen, Abdeckein und Vereinzeln von tiefgezogenen Tabletten packungen |
| US3933239A (en) | 1973-11-15 | 1976-01-20 | Takeda Chemical Industries, Ltd. | Capsule positioning machine |
| WO1982003842A1 (en) * | 1981-05-04 | 1982-11-11 | Michael E Ackley | Material orientation and printing apparatus and method |
| US4790118A (en) | 1987-04-13 | 1988-12-13 | Econodose, Inc. | Medication packaging and dispensing system |
| US4999979A (en) | 1988-07-13 | 1991-03-19 | A.R.C.I.L. | Machine for continuously packing in particular food or pharmaceutical products in plastic material containers |
| JPH03148430A (ja) * | 1989-10-23 | 1991-06-25 | Fujisawa Pharmaceut Co Ltd | 錠剤印刷包装機 |
| JPH0776305A (ja) * | 1993-09-10 | 1995-03-20 | Ckd Corp | 錠剤包装機 |
| US5415321A (en) | 1993-10-19 | 1995-05-16 | Gemel Precision Tool Co., Inc. | Feeder for pharmaceutical thermoform packaging machines |
| WO1996018539A1 (en) * | 1994-12-16 | 1996-06-20 | I.M.A. Industria Macchine Automatiche S.P.A. | System for feeding articles to blisters of a blister band |
Non-Patent Citations (2)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 015, no. 370 (M - 1159) 18 September 1991 (1991-09-18) * |
| PATENT ABSTRACTS OF JAPAN vol. 095, no. 006 31 July 1995 (1995-07-31) * |
Cited By (26)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2368830A (en) * | 2000-11-11 | 2002-05-15 | P J Contractors Ltd | Pack feeding |
| US7182259B2 (en) | 2001-10-26 | 2007-02-27 | International Barcode Corporation | Method and apparatus for applying bar code information to products during production |
| US7156308B2 (en) | 2001-12-17 | 2007-01-02 | International Barcode Corporation | Double-sided bar code doubling as a single bar code |
| US6851874B2 (en) * | 2002-06-18 | 2005-02-08 | Hewlett-Packard Development Company, L.P. | Methods and systems of producing blister packaging |
| EP2088867A4 (de) * | 2006-10-19 | 2010-12-01 | Wrigley W M Jun Co | Esswaren, die kontaktfrei bedruckt wurden, sowie gerät und verfahren zu ihrer herstellung |
| US8091319B2 (en) * | 2006-10-19 | 2012-01-10 | Wm. Wrigley Jr. Company | Apparatus for packaging non-contact printed comestible products |
| US8371216B2 (en) | 2009-12-03 | 2013-02-12 | Mars, Incorporated | Conveying and marking apparatus and method |
| US20120052118A1 (en) * | 2010-07-19 | 2012-03-01 | Carlos Salazar Altamar | Apparatus and process for encapsulating capsules or other solid dosage forms within capsules |
| US8967989B2 (en) * | 2010-07-19 | 2015-03-03 | Procaps SAS | Apparatus and process for encapsulating capsules or other solid dosage forms within capsules |
| US20150174008A1 (en) * | 2010-07-19 | 2015-06-25 | Procaps SAS | Apparatus and process for encapsulating microparticles with liquid in soft gel capsules |
| WO2013040599A3 (en) * | 2011-09-16 | 2013-05-10 | Tri-Star Technologies | Laser capsule marking system and method |
| US9517855B2 (en) | 2011-09-16 | 2016-12-13 | Tri-Star Technologies | Laser capsule marking system and method |
| US10492994B2 (en) | 2011-09-16 | 2019-12-03 | Tri-Star Technologies | Laser capsule marking system and method |
| CN104828271A (zh) * | 2015-04-30 | 2015-08-12 | 瑞安市安泰制药机械有限公司 | 高速双铝包装机 |
| CN107031882B (zh) * | 2016-02-04 | 2019-06-04 | Ckd株式会社 | 拾取装置和泡罩包装机 |
| CN107031882A (zh) * | 2016-02-04 | 2017-08-11 | Ckd株式会社 | 拾取装置和泡罩包装机 |
| CN106112270A (zh) * | 2016-07-26 | 2016-11-16 | 中核(天津)机械有限公司 | 管件的自动打标装置 |
| JP2018114041A (ja) * | 2017-01-17 | 2018-07-26 | フロイント産業株式会社 | 錠剤印刷包装装置及び錠剤印刷包装方法 |
| CN108860744A (zh) * | 2018-06-11 | 2018-11-23 | 上海松川远亿机械设备有限公司 | 散装颗粒物料的进料整理工艺 |
| CN108706335A (zh) * | 2018-06-11 | 2018-10-26 | 上海松川远亿机械设备有限公司 | 用于散装颗粒物料包装的进料整理装置 |
| JP7083719B2 (ja) | 2018-07-25 | 2022-06-13 | Ckd株式会社 | Ptpシートの製造方法 |
| JP7142521B2 (ja) | 2018-09-03 | 2022-09-27 | Ckd株式会社 | Ptp包装機 |
| CN109677670A (zh) * | 2019-01-15 | 2019-04-26 | 苏波 | 一种槟榔自动包装设备 |
| CN116829463A (zh) * | 2020-12-11 | 2023-09-29 | 皇家戴维艾格伯茨有限公司 | 饮料粉囊包和饮料粉囊包制造设备 |
| US12503298B2 (en) | 2020-12-11 | 2025-12-23 | Koninklijke Douwe Egberts B.V. | Beverage pad and apparatus for making beverage pads |
| CN117864510A (zh) * | 2024-03-11 | 2024-04-12 | 新华制药(高密)有限公司 | 一种药片泡罩包装机 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US3933239A (en) | Capsule positioning machine | |
| CA2417103C (en) | Variable size pill dispenser | |
| EP0077576B1 (de) | Verfahren und Vorrichtung zum Ausrichten von Kapseln | |
| RU2279379C2 (ru) | Способ и установка для нанесения маркировки на элементы упаковки | |
| JP6914604B2 (ja) | Ptpシート及びptp包装機 | |
| US3628694A (en) | Apparatus for packaging medicinal tablets or the like | |
| JPS61174023A (ja) | 物品の方位付け装置 | |
| CA2642064C (en) | Method for blister packing | |
| US5157896A (en) | Modularly constructed automatic packaging machine | |
| ES2329817T3 (es) | Unidad para alimentar productos a una maquina de fabricacion de blisters. | |
| US6494022B1 (en) | Orbital motion pill packaging device and associated method | |
| JP2000142602A (ja) | 薬剤分包機、薬剤分包機の制御方法及び薬包 | |
| AUPP656498A0 (en) | An apparatus for filling containers with discrete articles | |
| JP2001294204A5 (de) | ||
| WO2016050775A1 (en) | Method and apparatus for making a pack with a printed insert | |
| AU2008291795B9 (en) | System and method for matching colored lids to cartons | |
| EP0329054B1 (de) | Verfahren und Vorrichtung zum Einrahmen von photographischen Filmen | |
| JPH06135401A (ja) | 散薬分包機 | |
| TW304183B (de) | ||
| JPH07285523A (ja) | 帯状体への小袋の添着装置 | |
| GB2635196A (en) | Apparatus for the preparation of a unit dose of a medicine | |
| JP2004059034A5 (de) | ||
| JP2011036444A (ja) | 薬袋袋詰機 | |
| HK1125605B (en) | Method for blister packing | |
| JP2005225504A (ja) | 袋詰め包装機用製品搬出装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT CH DE ES FR GB IE IT LI |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Free format text: AT CH DE ES FR GB IE IT LI |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19991113 |