EP0943372A2 - Régulateur commandé de débit de poudre - Google Patents
Régulateur commandé de débit de poudre Download PDFInfo
- Publication number
- EP0943372A2 EP0943372A2 EP99105303A EP99105303A EP0943372A2 EP 0943372 A2 EP0943372 A2 EP 0943372A2 EP 99105303 A EP99105303 A EP 99105303A EP 99105303 A EP99105303 A EP 99105303A EP 0943372 A2 EP0943372 A2 EP 0943372A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- powder
- coating
- air
- objects
- coated
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/14—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas designed for spraying particulate materials
- B05B7/1404—Arrangements for supplying particulate material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B12/00—Arrangements for controlling delivery; Arrangements for controlling the spray area
- B05B12/08—Arrangements for controlling delivery; Arrangements for controlling the spray area responsive to condition of liquid or other fluent material to be discharged, of ambient medium or of target ; responsive to condition of spray devices or of supply means, e.g. pipes, pumps or their drive means
- B05B12/084—Arrangements for controlling delivery; Arrangements for controlling the spray area responsive to condition of liquid or other fluent material to be discharged, of ambient medium or of target ; responsive to condition of spray devices or of supply means, e.g. pipes, pumps or their drive means responsive to condition of liquid or other fluent material already sprayed on the target, e.g. coating thickness, weight or pattern
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B12/00—Arrangements for controlling delivery; Arrangements for controlling the spray area
- B05B12/08—Arrangements for controlling delivery; Arrangements for controlling the spray area responsive to condition of liquid or other fluent material to be discharged, of ambient medium or of target ; responsive to condition of spray devices or of supply means, e.g. pipes, pumps or their drive means
- B05B12/12—Arrangements for controlling delivery; Arrangements for controlling the spray area responsive to condition of liquid or other fluent material to be discharged, of ambient medium or of target ; responsive to condition of spray devices or of supply means, e.g. pipes, pumps or their drive means responsive to conditions of ambient medium or target, e.g. humidity, temperature position or movement of the target relative to the spray apparatus
- B05B12/122—Arrangements for controlling delivery; Arrangements for controlling the spray area responsive to condition of liquid or other fluent material to be discharged, of ambient medium or of target ; responsive to condition of spray devices or of supply means, e.g. pipes, pumps or their drive means responsive to conditions of ambient medium or target, e.g. humidity, temperature position or movement of the target relative to the spray apparatus responsive to presence or shape of target
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B13/00—Machines or plants for applying liquids or other fluent materials to surfaces of objects or other work by spraying, not covered by groups B05B1/00 - B05B11/00
- B05B13/02—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work
- B05B13/0221—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work characterised by the means for moving or conveying the objects or other work, e.g. conveyor belts
- B05B13/0264—Overhead conveying means, i.e. the object or other work being suspended from the conveying means; Details thereof, e.g. hanging hooks
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B13/00—Machines or plants for applying liquids or other fluent materials to surfaces of objects or other work by spraying, not covered by groups B05B1/00 - B05B11/00
- B05B13/02—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work
- B05B13/04—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work the spray heads being moved during spraying operation
- B05B13/0405—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work the spray heads being moved during spraying operation with reciprocating or oscillating spray heads
- B05B13/041—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work the spray heads being moved during spraying operation with reciprocating or oscillating spray heads with spray heads reciprocating along a straight line
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B13/00—Machines or plants for applying liquids or other fluent materials to surfaces of objects or other work by spraying, not covered by groups B05B1/00 - B05B11/00
- B05B13/02—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work
- B05B13/04—Means for supporting work; Arrangement or mounting of spray heads; Adaptation or arrangement of means for feeding work the spray heads being moved during spraying operation
- B05B13/0447—Installation or apparatus for applying liquid or other fluent material to conveyed separate articles
Definitions
- the present invention relates to a method according to the The preamble of claim 1 and a device for carrying it out of the procedure.
- a metering device is known to the Regulate the amount of powder in a powder coating facility, in such a way that the conveying speed of the to applying powder even with different amounts of powder remains at least almost the same. That proposed in DE-44 09 493 Air divider, by means of which the air supply in Dosing air and conveying air is divided in front of one Coating campaign stopped and constant during the campaign leave. If necessary during a coating campaign influences or changes in coating parameters, such as climate fluctuations, powder composition and the like, are not taken into account and can differ Lead coating results.
- the method according to the invention is based on DE-44 09 493, in which a powder coating device an air part organ has for the division of an air supply into dosing air and conveying air, such that with different settings the amount of powder conveyed differently in the air division can be applied at a constant conveying speed can.
- a powder coating device coated objects in the area of the coating member, such as a powder gun, and / or in the area of the objects to be coated and / or the coated objects measured at least one coating-relevant parameter is and based on the measurement, the setting of the air divider being affected.
- the layer thickness of an already coated object by means of a sensor is determined, the measured value with a Setpoint is compared and then the actuator of the Air divider is controlled or changed such that at least the layer thickness of objects to be subsequently coated almost corresponds to the setpoint.
- the Layer thickness of the object just coated is too small Value
- the air divider is to be controlled in such a way that the air supply is divided into more conveying air and less dosing air is conveyed, whereby a larger amount of powder is conveyed and is applied.
- This optimization of the coating can also be combined with the previously described recognition of a code for certain Objects by first storing the air divider organ according to the Data is set and then a Coating is optimized using the values which are determined on the initially coated objects. Finally, whether these newly determined, optimal parameters can be saved, or the originally saved Data for coating further object campaigns can be used depending on which external influences have led to the fact that not the originally saved optimized data for the desired Have succeeded.
- the vertical or longitudinal extent of the objects to be coated to determine before the coating process and the measured height to forward to a lifting device by means of which Coating member, such as a coating gun, performed in height during the coating process or changed. Due to the measured object height, the Lifting height of the lifting device to the one to be coated effectively Height of the object can be limited, which in turn increases the the amount of powder applied can be optimized. At the same time it is possible for objects with large heights to occur to avoid different coating thicknesses because usually more powder is to be applied at height than in the depth, because part of the material to be applied due to gravity Powder falls down. Experience has shown that an object with height expansion per meter above approx. 3 to 6% to apply more powder than at depth. The different The amount of powder to be applied can in turn be varied Adjustment of the air divider can be effected which can be controlled by the measuring device, by means of which measuring device the height of the object to be coated is determined.
- Coating member such as a coating gun
- the fact Taking into account that, for example, when using Tribo pistols charge the powder to friction charge based, the charge depending on the composition of the powder and depending on the climatic conditions during a coating process Is subject to fluctuations.
- the coating result depends largely on the friction charge of the powder from, the layer thickness in the remains essentially constant.
- the charge is suggested of the powder to be applied and in the event of fluctuations the charges to control the air divider again, such that the conveying air is changed to a constant To ensure powder loading. So is falling Charge to increase the amount of powder to be conveyed accordingly or to reduce the amount of powder when there is an increased load.
- the control of the air divider or an associated Actuator can be done both analog and digital, and also the regulation by comparing a measured actual value with a preset setpoint can be analog or done electronically.
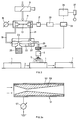
- objects 1 are arranged on a conveyor belt 2, which are to be coated or are already coated.
- the Coating is carried out by means of a coating member, such as for example a powder gun 3, by means of which the powder 5 is applied to the object.
- the feed, for example the gun 3 is carried out by means of a powder coating device, described in DE-44 09 493.
- this coating device for a better understanding be briefly this coating device at this point described and how they work.
- the Air is fed, for example, via an inlet pressure regulator 9, by means of which the supplied air is adjusted can be.
- the air is supplied to an air divider 11 in which a double valve 13 is provided, which by means of for example, a rotary control 17 is adjustable.
- the Display 15 can be read how the distribution of the from Inlet pressure regulator 9 supplied air in conveying air 19 and dosing air 21 is divided.
- the conveying air 19 is in an injector 22, for example, by arranging a venturi tube-like one Zone 15 sucked 25 powder from a powder supply and a second venturi tube-like zone 27. In the latter zone is also fed the metering air 21 and mixed with the conveying air and the powder. Then will the powder via the connecting line of the coating gun 3 fed.
- the coating zone is now connected a measuring sensor 31 is arranged, by means of which the layer thickness measured on the already coated object 1 or can be determined.
- the measured layer thickness becomes one Record 33 supplied, in which the measured value is compared with a target value 35, which by means of a Setting 37 can be set or changed.
- a controller 39 influenced in such a way that the control dial 17 is actuated becomes. Of course, this only applies if the actual value from Setpoint deviates.
- the Rotary control set in such a way that the conveying air 19 increases and more powder is conveyed accordingly. Is the Layer thickness too large, the rotary control 17 is actuated in such a way that the double valve 13 is moved in the direction of conveying air 19, respectively more dosing air of the venturi-like device 27 is supplied and correspondingly less powder promoted becomes.
- objects 1 which are about Suspension devices 43 connected to a conveyor 41 or attached to it, coated, initially in front of a coating device by means of a measuring device 45 whose height or longitudinal extent is detected or ascertained becomes.
- the signal measured by the measuring device 45 47 is connected to the coating arrangement via a control device forwarded, which for example on a mobile Device 51 is arranged.
- This coating arrangement includes on the one hand the coating gun 3, on the other hand is arranged on a lifting device 49 to be in height to be operated adjustable.
- the measurement signal 47 now the stroke of the powder gun is controlled so that the detected Object 1 in its entire vertical or longitudinal extent is sprayed, but the stroke movement is limited such that the pistol does not cross the object's longitudinal or Height direction is moved or operated. Thereby ensures that powder is not sprayed unnecessarily, which is not deposited on the surface of the object.
- the measured Signal 47 is also used to air divider 11 from Fig. 1 and the amount of powder, which by means the gun 3 is applied to control accordingly.
- the control takes place in such a way that in the upper area of the object 1 more powder is sprayed than in the lower area, whereby Experience has shown that approx. 3 to per meter in the upward direction 6% more powder is to be applied than at the lower end to make one to achieve a uniform layer thickness when coating the object.
- FIG. 3 Another example is shown in the diagram of FIG. 3, which with the scheme shown in Fig. 1 largely is identical.
- the exception is that in the 3 not primarily the layer thickness on one already coated object is measured or determined, but, that here the charge of the powder to be applied in one Sensor 51 is measured or detected.
- the charge of the powder to be applied in one Sensor 51 is measured or detected.
- using more new Powder or more recycled powder leads to different ones Charges in the powder to be applied, so that different Coatings can be achieved. This is especially true when using of so-called tribo pistols, where the powder is charged by means of friction. The charge is usually approx.
- the measured signal is not merely is used regardless of the selected conveyor speed of the powder when applying the amount of powder to vary, but that the variation in the amount of powder at least almost constant conveying speed of the Powder takes place, which for example by means of a coating device, described in DE-44 09 493, enables becomes.
Landscapes
- Electrostatic Spraying Apparatus (AREA)
- Coating Apparatus (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CH66298 | 1998-03-19 | ||
| CH66298 | 1998-03-19 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0943372A2 true EP0943372A2 (fr) | 1999-09-22 |
| EP0943372A3 EP0943372A3 (fr) | 2002-05-15 |
Family
ID=4192219
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99105303A Withdrawn EP0943372A3 (fr) | 1998-03-19 | 1999-03-15 | Régulateur commandé de débit de poudre |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP0943372A3 (fr) |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1124088A1 (fr) * | 2000-02-11 | 2001-08-16 | Cryospace l'air liquide aerospatiale | Procédé d'isolation thermique d'une structure metallique a usage cryogenique |
| CN102188858A (zh) * | 2010-03-18 | 2011-09-21 | 日本碍子株式会社 | 蜂窝过滤器制造装置 |
| CN102989611A (zh) * | 2012-10-18 | 2013-03-27 | 吴江市元通纺织品有限公司 | 一种均匀涂布机 |
| US8534221B2 (en) | 2010-03-18 | 2013-09-17 | Ngk Insulators, Ltd. | Honeycomb filter production apparatus |
| WO2015166374A1 (fr) * | 2014-04-28 | 2015-11-05 | Marangoni S.P.A. | Unité de distribution pour un matériau particulaire |
| US10071482B2 (en) * | 2015-08-19 | 2018-09-11 | Ford Global Technologies, Llc | Robotic vehicle painting instrument including a terahertz radiation device |
| US10323932B1 (en) | 2017-12-28 | 2019-06-18 | Ford Motor Company | System for inspecting vehicle bodies |
| EP3439792B1 (fr) * | 2016-04-05 | 2022-10-05 | Sat (Surface Aluminium Technologies) S.R.L. In Short "Sat S.R.L." | Système et procédé de revêtement de profilés |
| EP4190454A1 (fr) * | 2021-12-06 | 2023-06-07 | coatingAI AG | Système de ligne de production de revêtement |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4409493A1 (de) | 1993-03-26 | 1994-09-29 | Peter Ribnitz | Luftteilerventil |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3594211A (en) * | 1966-10-20 | 1971-07-20 | Ransburg Electro Coating Corp | Automatic coating system |
| DE4443859A1 (de) * | 1994-12-09 | 1996-06-13 | Friedrich Lothar | Verfahren und Vorrichtung zum Messen der Lackierpulverdurchflußmengen bei der elektrostatischen Pulverbeschichtung |
| DE19548607A1 (de) * | 1995-12-23 | 1997-06-26 | Gema Volstatic Ag | Pulver-Sprühbeschichtungsvorrichtung |
| DE19623121C2 (de) * | 1996-06-10 | 2000-05-11 | Wagner International Ag Altsta | Verfahren und Vorrichtung zum photothermischen Prüfen von Werkstückoberflächen |
-
1999
- 1999-03-15 EP EP99105303A patent/EP0943372A3/fr not_active Withdrawn
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4409493A1 (de) | 1993-03-26 | 1994-09-29 | Peter Ribnitz | Luftteilerventil |
Cited By (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2805023A1 (fr) * | 2000-02-11 | 2001-08-17 | Cryospace L Air Liquide Aerosp | Procede d'isolation thermique d'une structure metallique a usage cryogenique |
| EP1124088A1 (fr) * | 2000-02-11 | 2001-08-16 | Cryospace l'air liquide aerospatiale | Procédé d'isolation thermique d'une structure metallique a usage cryogenique |
| CN102188858B (zh) * | 2010-03-18 | 2014-11-05 | 日本碍子株式会社 | 蜂窝过滤器制造装置 |
| CN102188858A (zh) * | 2010-03-18 | 2011-09-21 | 日本碍子株式会社 | 蜂窝过滤器制造装置 |
| EP2371452A1 (fr) * | 2010-03-18 | 2011-10-05 | NGK Insulators, Ltd. | Appareil de production de filtre en nid d'abeille |
| US8495968B2 (en) | 2010-03-18 | 2013-07-30 | Ngk Insulators, Ltd. | Honeycomb filter production apparatus |
| US8534221B2 (en) | 2010-03-18 | 2013-09-17 | Ngk Insulators, Ltd. | Honeycomb filter production apparatus |
| US8632852B2 (en) | 2010-03-18 | 2014-01-21 | Ngk Insulators, Ltd. | Method for producing a honeycomb filter |
| CN102989611A (zh) * | 2012-10-18 | 2013-03-27 | 吴江市元通纺织品有限公司 | 一种均匀涂布机 |
| WO2015166374A1 (fr) * | 2014-04-28 | 2015-11-05 | Marangoni S.P.A. | Unité de distribution pour un matériau particulaire |
| US20170050397A1 (en) * | 2014-04-28 | 2017-02-23 | Marangoni S.P.A. | Distribution Unit for a Particulate Material |
| US9873235B2 (en) * | 2014-04-28 | 2018-01-23 | Marangoni S.P.A. | Distribution unit for a particulate material |
| US10071482B2 (en) * | 2015-08-19 | 2018-09-11 | Ford Global Technologies, Llc | Robotic vehicle painting instrument including a terahertz radiation device |
| EP3439792B1 (fr) * | 2016-04-05 | 2022-10-05 | Sat (Surface Aluminium Technologies) S.R.L. In Short "Sat S.R.L." | Système et procédé de revêtement de profilés |
| US10323932B1 (en) | 2017-12-28 | 2019-06-18 | Ford Motor Company | System for inspecting vehicle bodies |
| EP4190454A1 (fr) * | 2021-12-06 | 2023-06-07 | coatingAI AG | Système de ligne de production de revêtement |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0943372A3 (fr) | 2002-05-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0576498B2 (fr) | Procede et dispositif d'application d'une matiere pateuse | |
| EP3185680B1 (fr) | Pulvérisateur agricole comprenant un système pour le control automatique des profiles de pulvérisation | |
| DE69021136T2 (de) | Vorrichtung zur Regelung des Materialflusses bei einem Prozess mit Abgabe eines fliessfähigen Mediums. | |
| EP1445031A2 (fr) | Appareil pour l'application de colle sur une pièce | |
| DE102014225516B3 (de) | Verfahren und Vorrichtung zum Beschichten eines Metallbandes | |
| DE69429163T2 (de) | Verfahren und gerät zum beschichten dreidimensionaler artikel | |
| DE2224833C3 (de) | Vorrichtung zur Messung des Spaltes eines Arbeitswalzenpaares für ein Walzgerüst | |
| DE102014005077A1 (de) | Selbstfahrende Baumaschine und Verfahren zum Steuern einer selbstfahrenden Baumaschine | |
| DE19803240A1 (de) | Farbvorhang-Auftragsvorrichtung | |
| DE3434904C1 (de) | Verfahren und Anlage zum UEberwachen der Abmessungen eines aus einer oder mehreren Mischungen bestehenden,kontinuierlich extrudierten Profilbandes aus Kautschuk oder thermoplastischem Kunststoff | |
| DE102019203394A1 (de) | Verfahren zum Einstellen eines Parameters einer landwirtschaftlichen Spritzvorrichtung | |
| DE102014100829A1 (de) | Verfahren zum gesteuerten und/oder geregelten Ausbringen von Pflanzenschutzmittel sowie landwirtschaftliche Verteilmaschine zur Anwendung des Verfahrens | |
| EP0690932A1 (fr) | Dispositif de soufflage | |
| DE3135721C3 (de) | Verfahren und anlage zum verspruehen von farben | |
| DE3824908A1 (de) | Verfahren und vorrichtung zum elektrostatischen spruehbeschichten | |
| DE19854675A1 (de) | Vorrichtung zum Kühlen eines Metallbandes, insbesondere eies Warmbreitbandes | |
| DE3309210A1 (de) | Verfahren und vorrichtung zur pneumatischen foerderung von feingut | |
| EP0102937B1 (fr) | Dispositif pour commander l'épaisseur dans un laminoir à froid | |
| DE9112257U1 (de) | Konusschärmaschine | |
| DE10111383B4 (de) | Verfahren zur Förderung von Beschichtungspulver zu einer Beschichtungseinheit und zugehörige Pulverfördervorrichtung | |
| DE112005000426T5 (de) | Verfahren zum Streichen einer Papier-/Kartonbahn mit einer Vorhangstreicheinrichtung | |
| DE4300868C1 (de) | Beschichtungsvorrichtung | |
| DE3047857A1 (de) | Filterstrangfertigung | |
| EP1298504B1 (fr) | Procédé et dispositif pour améliorer la réponse d'une installation contrôlée par commandes | |
| DE69101977T2 (de) | Vorrichtung zur Ausstreuung eines körnigen Materials. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid | ||
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20021001 |