EP0952896B1 - Vorrichtung zum biegen von rohren mit kleinen durchmesser - Google Patents
Vorrichtung zum biegen von rohren mit kleinen durchmesser Download PDFInfo
- Publication number
- EP0952896B1 EP0952896B1 EP98902049A EP98902049A EP0952896B1 EP 0952896 B1 EP0952896 B1 EP 0952896B1 EP 98902049 A EP98902049 A EP 98902049A EP 98902049 A EP98902049 A EP 98902049A EP 0952896 B1 EP0952896 B1 EP 0952896B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- axis
- tube
- bending
- rollers
- bending machine
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000005452 bending Methods 0.000 title claims description 96
- 238000006073 displacement reaction Methods 0.000 claims description 26
- 230000015572 biosynthetic process Effects 0.000 claims description 25
- 238000011144 upstream manufacturing Methods 0.000 claims description 19
- 230000000694 effects Effects 0.000 claims description 4
- 210000003739 neck Anatomy 0.000 claims description 4
- 238000001514 detection method Methods 0.000 claims description 2
- 230000002093 peripheral effect Effects 0.000 claims description 2
- 229920000297 Rayon Polymers 0.000 description 7
- 239000002964 rayon Substances 0.000 description 7
- 238000004519 manufacturing process Methods 0.000 description 6
- 210000000056 organ Anatomy 0.000 description 4
- WWYNJERNGUHSAO-XUDSTZEESA-N (+)-Norgestrel Chemical compound O=C1CC[C@@H]2[C@H]3CC[C@](CC)([C@](CC4)(O)C#C)[C@@H]4[C@@H]3CCC2=C1 WWYNJERNGUHSAO-XUDSTZEESA-N 0.000 description 1
- 241001080024 Telles Species 0.000 description 1
- 239000003638 chemical reducing agent Substances 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 230000014759 maintenance of location Effects 0.000 description 1
- 238000005457 optimization Methods 0.000 description 1
- 230000000284 resting effect Effects 0.000 description 1
- -1 à échelle agrandie Chemical compound 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D11/00—Bending not restricted to forms of material mentioned in only one of groups B21D5/00, B21D7/00, B21D9/00; Bending not provided for in groups B21D5/00 - B21D9/00; Twisting
- B21D11/06—Bending into helical or spiral form; Forming a succession of return bends, e.g. serpentine form
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D7/00—Bending rods, profiles, or tubes
- B21D7/02—Bending rods, profiles, or tubes over a stationary forming member; by use of a swinging forming member or abutment
- B21D7/021—Construction of forming members having more than one groove
Definitions
- the invention relates to a bending head according to the preamble of claim 1. It also relates to a bending machine small diameter tubes, in particular less than 10 mm, pre-cut and with connection systems to each of their ends equipped with at least one such head bending.
- Current bending machines used for bending such tubes conventionally include a frame on which are mounted bending means provided with bearing surfaces between which passes, is clamped then wound the tube to be bent, said bending means being mounted on a folding head capable of pivoting around a axis coaxial with the axis of the bending shape.
- these bending machines usually include a guide strip arranged upstream of the clamping jaw and possibly a wrinkle-removing element arranged upstream of the bending shape.
- they include means longitudinal displacement of the tube relative to the frame.
- a first solution consists in providing the bending machines with a clamp digitally controlled suitable for rotating the tube around its axis in order to change the direction of bending.
- bending machines have a first drawback resulting from the fact that, during changes in bending direction, tube movements generate so-called "whiplash" phenomena likely to alter the shape of the part carried out.
- a second solution consists in carrying out bending machines with drive means in rotation of the folding head capable of rotating this last around the tube.
- this solution is to currently only used with tubes packaged as a coil and not with tubes pre-cut and fitted with fittings beforehand. But he turns out that the fitting of these fittings is more complex and longer when performed on initially bent products.
- a third solution finally consists in make bending machines with a double head folding associated with rotary drive means and / or in translation allowing the second head to be brought folding in working position.
- this solution leads to the production of relatively bending machines complex and bulky, and therefore cost important.
- the change in bending direction forces the folding heads to be moved, an operation which requires a relatively long time which leads to penalize machine productivity.
- the present invention aims to overcome all of the aforementioned drawbacks of bend current and main objective is to provide a machine of very simple design therefore of a cost of returns relatively small and space-saving, allowing to achieve with a very high rate the production of parts of complex geometry, not achievable with current machines as described above, from straight tubes of small diameter, pre-cut and equipped with systems of fittings at each of their ends.
- Another object of the invention is to produce parts with high speed turns.
- Another object of the invention is to produce parts with high speed sheathed portions.
- Another object of the invention is to produce parts with high speed a final portion of very short straight end.
- a bending machine equipped with at least one bending head according to the invention is defined in claim 2.
- such a machine bending is designed to allow bending of tubes pre-cut with connection systems to each of their extremities.
- the gripping means are adapted to maintain the end rear of the tube with its connection system and other part, the "opening" faculty of the guide rollers, allows you to thread the straight pre-cut tube with its connection systems, either manually or by means of a loading system.
- the bending machine according to the invention has also as an advantage to allow very easily to bend the tubes in both directions, the only ones operations to be carried out for the change of bending consisting in combining displacements in translation, and a displacement along its circular path, of the finger folding.
- this bending machine allows very high folding rates, and moreover due to its simple design (only the folding finger is brought to be moved) leads to obtaining a bending head of small footprint.
- the forming rollers comprise two superimposed grooves of sections adapted to form two guide conduits having necks of different diameters.
- means for translational movement of the forming rollers respectively along an axis (Y 2 ), (Y 3 ) parallel to (Y) are adapted to position the latter so that either of their grooves is oriented relative to the longitudinal axis (X).
- This provision allows, without requiring any adjustment, to bend a tube with two different diameters, such as for example a tube whose certain length portions are sheathed, and / or bend a tube with different bending radii.
- the bending machine comprises means for translational movement of the folding finger capable of move radially with respect to the axis (Y).
- the fact of ability to move bending pin relative to forming rollers allows the length of the straight tube portions between two bending operations, and in particular to produce straight tube portions of very short length.
- the bending machine further comprises preferably, a strip arranged upstream of the forming rollers in contact with them, and having a bearing face forming a support for the tube, said strip being associated with displacement means adapted for bring it into a retracted position allowing to move forward the gripping means in contact with the forming rollers.
- This strip is to maintain the tube immediately upstream of the rollers and therefore provides the right bending angle.
- his character retractable allows the gripping means to be moved until the latter come into contact with the rollers, where they replace said strip to ensure the tube retention.
- this strip has the shape of a U, the means of displacement of said strip consisting of means of pivot able to tilt it around an axis orthogonal to the axes (X) and (Y).
- the means for relative displacement of the forming rollers comprise means for driving in rotation each of these rollers around the axes (Y 2 ), (Y 3 ), said rollers having a shape that is not circular adapted to free up a space during their rotation from their adjoining position.
- This mode of relative movement of the rollers has the advantage of leading to an optimization of the size of the bending head because the translation of said rollers aiming to use one or the other of their grooves, as well as their relative movement are operated around single axes (Y 2 ), (Y 3 ).
- rollers of different sizes allowing to make bends of different radii and / or bending of tubes of different diameters.
- each forming roller is mounted on a shaft extending respectively along the axis (Y 2 ), (Y 3 ), the means for rotating said rollers comprising two pinions each mounted on a trees, a rack with two toothed lateral faces arranged to mesh each with a pinion, and means for driving the rack along a longitudinal axis (X 1 ) parallel to the axis (X).
- each roller is advantageously constituted by a rod of a jack arranged so as to cause the translational displacements of said roller respectively along the axis (Y 2 ), (Y3).
- the bending machine comprises a member laterally retractable support relative to the axis (X) arranged to come and position itself in contact with a tube generator diametrically opposite to that resting on the support face of the strip, upstream and near forming rollers.
- This support body has the function, for bending machines conventionally allowing rotate the bending head around the tube to perform multidirectional bends, ensure holding the tube in position when, when opening rollers, the bending head is arranged so that said tube is located under the strip.
- this support member is advantageously consisting of a cable extending to the inside of a sheath, one end of this cable being secured to a cylinder rod arranged to bring said cable to slide inside said sheath, and the other end of this cable extending along a plane orthogonal to planes (X) and (Y) so as to come position in contact with the tube when moving the cylinder.
- the bending machine comprises two plates bearing having a convex bearing face, arranged orthogonally to the axis (X), on both sides of the latter, upstream of the forming rollers, said support plates being offset with respect to said rollers forming along an axis parallel to the axis (Y), and arranged so that during the formation of turns, the tube is caused after bending to move on the bearing face one of the support plates.
- Such support plates have the advantage to allow the formation of turns having a pitch determined.
- means adjust the position of the plates along an axis parallel to the axis (Y), and so allow to modify the pitch of the turns.
- the guide members of the tube are preferably arranged each on the end of an arm pivotally mounted relative to the frame and associated with elastic means capable of holding it in a position tilted backwards with respect to the direction of displacement of said tube.
- This design provides a self-locking of the guide members when moving the tube, while allowing the retraction, by pivoting, of the latter under the effect of the effort exerted by the means gripping.
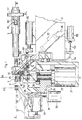
- the bending machine shown example in Figures 1 to 3 is adapted to ensure the bending of tubes 1 of small diameter, such as by example with a diameter of 4.75 mm, pre-cut to a predetermined length, with fittings 2, 3 each of their ends.
- This bending machine includes, in first, a frame 4 on which is mounted a head of bending described below, and a clamp 5 capable of clamping the rear end of the tube 1 downstream of the connector 3, said clamp being housed inside a cylindrical conduit 6 and associated with conventional training means (not shown) able to move it longitudinally in a axis (X) relative to the frame 4.
- this bending machine can be provided with either means for driving in rotation the clamp 5 around the axis (X), either of drive means in rotation of the frame 4 around the clamp 5, and this in the goal of making multidirectional bends. Heads below described bending can also equip a bending machine as described in the patent FR 2 554 021.
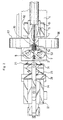
- the bending head comprises two forming rollers 7, 8 of general shape semicircular (as shown in the figures) or semi-elliptical, each with two superimposed grooves 9, 10, of semi-circular sections, making it possible to guide tubes of different diameters, such as for example a tube 1 of given diameter and the same tube 1 covered with a sheath.
- Each of these forming rollers 7, 8 is mounted on the upper end of a rotation shaft vertical 12, 13 to which it is secured by means of a screw 11, each of said shafts being housed and rotatably mounted at the interior of bores made in a housing 14.
- the means for rotating these shafts 12, 13 around their respective axes of revolution (Y 2 ), (Y 3 ) comprise, for each of said shafts, a pinion 15, 16 mounted around and integral with the latter. They also include a rack 17 extending horizontally and provided with two toothed lateral faces arranged to mesh each with one of the pinions 15, 16.
- the means for rotating the shafts 12, 13 finally comprise a jack 70 arranged horizontally, the body of which is secured to the frame 4, and the rod of which is secured to the rack 17 so as to cause the displacements of the latter along a horizontal axis (X 1 ).
- rollers 7, 8 allow the use of rollers larger than those shown in the figures in view to obtain different forming radii. To this end, it it is enough for the axis of rotation of these rollers to be adequately offset from the axis of symmetry of these.
- the forming rollers 7, 8 are also associated with means for driving in translation respectively along the axes (Y 2 ), (Y 3 ), capable of bringing either one or the other groove 9, 10 into the axis of the plane of movement of the tube 1.
- These means of translational training include, for each shaft 12, 13, a piston 18, 19 secured under the lower end of said tree by means a screw such as 20, each of said pistons extending in a cylinder chamber 21, 22 formed in the housing 14, and conventionally provided with fluid inlets suitable for allow the movements of the pistons to be generated.
- the bending machine comprises, first, a rotary block 24 secured to a shaft motor 25 extending along the axis (Y) and located under the housing 14, said shaft being rotatably mounted relative to the frame 4 by means of bearings such as 26, and being rotated by a coaxial motor-reducer 27 with the latter.
- the bending machine comprises a first carriage 28 mounted on the rotary block 24 by means of a translational guidance system 29 in the form of a tail dovetail, and secured to the rod of a jack 30 arranged vertically, the body of which is carried by a horizontal plate 31 fixed to the rotary block 24.
- the bending machine comprises a second carriage 32 mounted on the first carriage 28 via a system dovetail-shaped guide, and secured to the rod of a jack 33 arranged horizontally, the body of which is carried by the first carriage 28.
- the folding finger 23 is worn by this second carriage 32 and is disposed at the right of the end of an inclined arm 34 extending above said second carriage in the direction of the forming rollers 7.8.
- the bending machine includes, for elsewhere, first and second means for guiding the tube 1 arranged to prevent any deformation of said tube upstream forming rollers 7, 8.
- the first guiding means consist in a strip 35 disposed immediately upstream of the forming rollers 7, 8 and having a bearing face forming a support for the tube 1.
- This strip 35 consists into a U-shaped jumper centered on the axis (X), and is mounted on a part 36 strip holder articulated by relation to the frame 4 around a horizontal axis orthogonal to the axis (X), so as to allow the strip 35 to be retracted by pivoting the latter, and bringing the clamp 6 to contact of the forming rollers 7, 8.
- the means of pivoting this strip 35 consist, in turn, of a cylinder 37 extending along an axis inclined substantially by 45 ° relative to the axis (X), whose rod is articulated on said strip, and whose body is articulated inside a clevis 38 integral of the frame 4.
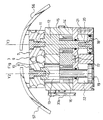
- the second guide means include, as shown in Figure 4, two rollers 39, 40 each carried by an arm such as 50 extending through a light in the conduit 6 for guiding the clamp 5, said arms being pivotally mounted, each on a leg such as 41 secured to a flange 51 mounted on the duct 6.
- spiral springs such as 52 arranged around the rotation shaft of the arms 50 and integral with the legs 41 and the said arms, are adapted for maintain these, in the absence of solicitation, in a position where they are tilted backwards by relative to the direction of movement of the tube 1.
- rollers 39, 40 ensure the holding and guiding the tube 1 during movement longitudinal of the latter, but retract transversely under the effect of the pressure exerted by the clamp 5 when the latter comes into contact with said casters.
- the bending machine includes, for elsewhere, a support member adapted to provide support of tube 1 when frame 4 is rotated 180 ° relative to at the position shown in the figures, and when the "opening" of the forming rollers 7, 8.
- This support member consists of a cable 53 extending inside a sheath 54, one of the ends of this cable being secured to the rod of a jack 55 arranged to cause said cable to slide inside said sheath, and the other end being arranged so to be positioned transversely under the tube 1 (in the aforementioned position of the frame 4) during deployment jack 55.
- the bending machine further comprises two support plates 56, 57 intended to allow determine the pitch of the turns when forming these past. ''
- these two support plates 56, 57 consist of two curved plates with one side upper convex, arranged orthogonally to the axis (X) on either side of the latter, upstream of the forming rollers 7, 8 and offset upwards relative to said axis (X).
- these support plates 56, 57 are carried by vertical legs such as 59 drilled an oblong hole with a large vertical axis and secured to the frame 4 by means of screws such as 60 for adjusting the position in height of said support plates and therefore of change the pitch of the turns.
- the bending machine finally comprises two cells 61, 62 arranged upstream of the support plates 56, 57 symmetrically on either side of the axis (X) so that the beam of one of said cells is cut by the end strand of tube 1 during the formation of turns.
- These two cells 61, 62 associated with a CNC bending machine aim to allow, during the production of a series of products identical, to consume a fixed developed length for the formation of turns, and to form turns whose the angle of the output strand and the angle of the input strand are always the same.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
Claims (16)
- Biegekopf für eine Biegemaschine zum Biegen von Rohren (1) mit kleinen Durchmessern, die vorgeschnitten und mit Verbindungssystemen (2, 3) an jeder von ihren Enden versehen sind, dadurch gekennzeichnet, daß sie umfaßt :zwei Verformungsrollen (7, 8) jeweils mit mindestens einer halbrunden Umfangskehle (9, 10), angepaßt bei einer aneinander gesetzten Stellung der genannten Rollen an das Ausführen einer in die Richtung einer Achse (X) gerichteten Führungsleitung mit einem Hals, dessen Durchmesser im wesentlichen größer als dieser des Rohres (1) ist,Bewegungsmittel (12-17) zum relativen Bewegen der Verformungsrollen (7, 8), geeignet für das Positionieren der genannten Rollen entweder in ihre aneinander gesetzte Stellung oder in eine sogenannte Öffnungsstellung, in der der Durchgang des Rohres (1) in die senkrechte zur Achse (X) Richtung ermöglicht ist,einen Biegefinger (23), angeordnet unterhalb und in der Nähe der Verformungsrollen (7, 8),Bewegungsmittel (24-27) zum Bewegen des Biegefingers (23) nach einem um eine senkrechte zur Achse (X) Achse (Y) angeordneten Kreisbahn,Verschiebungsmittel (30) zum Verschieben des Biegefingers (23) in die Richtung einer parallelen zu (Y) Achse (Y1),Führungselemente (39, 40) zum Führen des Rohres (1), die von beiden Seiten der Achse (X) angeordnet sind, so daß sie das genannte Rohr oberhalb und in der Nähe der Verformungsrollen (7, 8) berühren, wobei die genannte Führungselemente daran angepaßt sind, sich quer unter der Wirkung von einer von der Griffmitteln (5) ausgeübten Längsspannung einzuziehen.
- Biegemaschine zum Biegen von Rohren (1) mit kleinen Durchmessern, insbesondere mit kleineren als 10 mm Durchmessern, die vorgeschnitten sind, so daß sie eine vorbestimmte Länge haben, und die mit Verbindungssystemen (2, 3) an jeder ihrer Enden versehen sind, wobei die genannte Biegemaschine ein Gestell (4), auf dem mindestens einen Biegekopf (7, 8, 23) montiert ist, und Längsbewegungsmittel für die Längsbewegung des Rohres (1) relativ zum Gestell (4) in die Richtung einer Achse (X) umfaßt, und wobei sie dadurch gekennzeichnet ist, daß :die Längsbewegungsmittel Griffmittel (5) zum Greifen der Hinterende des Rohres (1), und Antriebsmittel zum Antreiben der genannten Griffmittel in die Richtung der Längsachse (X) umfassen, und daßjeder Biegekopf ein gemäßer dem Anspruch 1 Biegekopf ist.
- Biegemaschine nach Anspruch 2, dadurch gekennzeichnet, daß :die Verformungsrollen (7, 8) zwei übereinanderliegenden Kehlen (9, 10) umfassen, deren Schnitte daran angepaßt sind, zwei Führungsleitungen mit Hälsen mit verschiedenen Durchmessern zu bilden, und daßVerschiebungsmittel (18, 19) zum Verschieben der Verformungsrollen (7, 8) in die Richtung einer parallelen zu (Y) Achse (Y2), (Y3) daran angepaßt sind, diese Rollen zu positionieren, so daß die Achse der einen oder der anderen ihrer Kehlen (9, 10) auf der Längsachse (X) ausgerichtet ist.
- Biegemaschine nach einem der Ansprüche 2 oder 3, dadurch gekennzeichnet, daß sie Verschiebungsmittel (33) zum Verschieben des Biegefingers (23) umfaßt, welche sich dafür eignen, radial bezüglich der Achse (Y) ihn zu verschieben.
- Biegemaschine nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß sie ein Lineal (35) umfaßt, das oberhalb der Verformungsrollen (7, 8) in Berührung mit ihnen angeordnet ist, und das eine als Träger für das Rohr (1) ausgestalte Auflagefläche aufweist, wobei das genannte Lineal Bewegungsmitteln (37) zugeordnet ist, die daran angepaßt sind, in eine eingezogen Stellung ihn zu bringen, in der der Vorschub der Griffmittel (5) an die Verformungsrollen (7, 8) erlaubt ist.
- Biegemaschine nach Anspruch 5, dadurch gekennzeichnet, daß das Lineal (35) U-förmig ist, wobei die Bewegungsmittel zum Bewegen des genannten Lineals aus Schwenkmitteln (37) bestehen, die sich dafür eignen, um eine senkrechte zu den Achsen (X) und (Y) Achse ihn zu schwenken.
- Biegemaschine nach Anspruch 3, dadurch gekennzeichnet, daß die Bewegungsmittel zum relativen Bewegen der Verformungsrollen (7, 8) Drehantriebsmittel (12-17) für den Drehantrieb jeder Rolle um die Achsen (Y2), (Y3) umfassen, wobei die Form der genannten Rollen nicht rund ist, und daran angepaßt ist, einen Freiraum bei ihrer Drehung ab ihrer aneinander gesetzten Stellung zu machen.
- Biegemaschine nach Anspruch 7, dadurch gekennzeichnet, daß jede Verformungsrolle (7, 8) eine allgemein halbkreisförmige oder halbelliptische Form aufweist.
- Biegemaschine nach einem der Ansprüche 7 oder 8, dadurch gekennzeichnet, daß jede Verformungsrolle (7, 8) an einer Welle (12, 13) montiert ist, die sich jeweils in die Richtung der Achse (Y2), (Y3) erstreckt, wobei die Drehantriebsmittel für den Drehantrieb der genannten Rollen zwei jeweils an der Wellen (12, 13) montierte Zahnräder (15, 16), eine Zahnstange (17) mit zwei gezahnten Seitenflächen, die sich jeweils mit den Zahnrädern (15, 16) eingreifen, und Antriebsmittel (70) zum Antreiben der Zahnstange (17) in die Richtung einer parallelen zur Achse (X) Längsachse (X1) umfassen.
- Biegemaschine nach den zusammen in Betracht gezogenen Ansprüchen 3 und 9, dadurch gekennzeichnet, daß die Welle (12, 13) jeder Verformungsrolle (7, 8) aus einer Stange eines Zylinders (18, 19, 21, 22) besteht, der angeordnet ist, so daß die Verschiebungen der genannten Rolle jeweils in die Richtung der Achse (Y2), (Y3) erzeugt werden.
- Biegemaschine nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß sie ein Auflageelement (53) umfaßt, das bezüglich der Achse (X) seitlich einschiebbar ist, die angeordnet ist, um sich in Berührung mit einer Generatrix des Rohres (1) zu positionieren, welche genau gegenüber derjenigen ist, die auf der Auflagefläche des Lineals (35) oberhalb und in der Nähe der Verformungsrollen (7, 8) liegt.
- Biegemaschine nach Anspruch 11, dadurch gekennzeichnet, daß das Auflageelement aus einem sich innerhalb einer Umhüllung (54) erstreckenden Kabel (53) besteht, wobei eine der Enden dieses Kabels (53) an einer Kolbenstange (55) befestigt ist, die angeordnet ist, um die Gleitführung des genannten Kabels innerhalb der genannte Umhüllung zu steuern, und die andere Ende dieses Kabels (53) sich in einer senkrechten zu den Ebenen (X) und (Y) Ebene erstreckt, so daß sie sich in Berührung mit dem Rohr (1) bei der Bewegung des Zylinders (55) positioniert.
- Biegemaschine nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß sie zwei Auflageplatten (56, 57) mit einer konvexen Auflagefläche umfaßt, die senkrecht zu, und von beiden Seiten, der Achse (X) oberhalb der Verformungsrollen (7, 8) angeordnet sind, wobei die genannte Auflageplatten bezüglich den genannten Verformungsrollen in der Richtung einer parallelen zur Achse (Y) Achse versetzt, und angeordnet sind, so daß beim Ausführen von Windungen das Rohr (1) auf die Auflagefläche einer der Auflageplatten (56, 57) nach dem Biegen sich bewegen muß.
- Biegemaschine nach Anspruch 13, dadurch gekennzeichnet, daß sie Einstellmittel zum Einstellen der Stellung der Auflageplatten (56, 57) entlang einer parallelen zur Achse (Y) Achse umfaßt.
- Biegemaschine nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß die Führungselemente (39, 40) zum Führen des Rohres (1) jeweils an der Ende eines Arms (50) angeordnet sind, welcher bezüglich dem Gestell (4) drehbar montiert, und elastischen Mitteln (52) zugeordnet ist, die sich dafür eignen, in einer Rückwärts geneigten Stellung bezüglich der Bewegungsrichtung des genannten Rohres ihn zu halten.
- Biegemaschine nach einem der vorhergehenden Ansprüche, dadurch gekennzeichnet, daß sie umfaßt :zwei Erfassungszellen (61, 62), die symmetrisch von beiden Seiten der Achse (X) oberhalb der Verformungsrollen (7, 8) angeordnet sind, so daß gemäß der Biegerichtung der Strahl einer der genannten Zellen von der Ende des Rohres (1) beim Ausführen von Windungen geschnitten wird,numerische Steuerungsmittel, die programmiert sind, um die abgewickelte Länge für die Ausführung jeder Windung zu kalkulieren, diesen Wert mit einem gespeicherten Wert, repräsentativ der theoretischen abgewickelten Länge, erforderlich für die Ausführung einer Windung, zu vergleichen, und abhängig von dem Ergebnis dieser Vergleichung eine Bewegung des Biegefingers (23) entlang seinem Kreisbahn zum Ausführen der nächsten Windung zu steuern, so daß die gesamte abgewickelte Länge zum Ausführen einer Windung streng immer die gleiche für eine Reihe von identischen Artikeln ist.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9700437A FR2758281B1 (fr) | 1997-01-14 | 1997-01-14 | Machine a cintrer des tubes de faible diametre, notamment inferieurs a 10mm, predecoupes et presentant des systemes de raccord a chacune de leurs extremites, et tete de cintrage pour une telle machine |
| FR9700437 | 1997-01-14 | ||
| PCT/FR1998/000033 WO1998031484A1 (fr) | 1997-01-14 | 1998-01-09 | Machine a cintrer des tubes de faible diametre |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0952896A1 EP0952896A1 (de) | 1999-11-03 |
| EP0952896B1 true EP0952896B1 (de) | 2001-05-16 |
Family
ID=9502679
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98902049A Expired - Lifetime EP0952896B1 (de) | 1997-01-14 | 1998-01-09 | Vorrichtung zum biegen von rohren mit kleinen durchmesser |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6185969B1 (de) |
| EP (1) | EP0952896B1 (de) |
| CA (1) | CA2275946A1 (de) |
| DE (1) | DE69800795T2 (de) |
| FR (1) | FR2758281B1 (de) |
| WO (1) | WO1998031484A1 (de) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| TW311945B (de) * | 1994-11-23 | 1997-08-01 | Barmag Barmer Maschf | |
| US7213152B1 (en) * | 2000-02-14 | 2007-05-01 | Intel Corporation | Modular bios update mechanism |
| FR2922127B1 (fr) * | 2007-10-15 | 2010-03-05 | Jaubjaub Consulting | Machine a cintrer un profile et outillage de cintrage pour une telle machine |
| EP3255510B1 (de) * | 2016-06-10 | 2019-06-05 | Nivarox-FAR S.A. | Kalander und kalandrierverfahren einer schliesszylinderfeder einer uhr |
| US11635073B2 (en) * | 2017-12-18 | 2023-04-25 | Flex Ltd. | Linear peristaltic pump |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1047612A (en) * | 1911-09-16 | 1912-12-17 | Frederick Brantigam | Machine for bending tubes. |
| US1567107A (en) * | 1922-08-04 | 1925-12-29 | Bonn Carl Robert Hugo | Machine for bending tubes and the like |
| US3373587A (en) * | 1966-12-08 | 1968-03-19 | Shubin Vladimir Nikolaevich | Automatic tube bending machines |
| US3430474A (en) * | 1967-01-10 | 1969-03-04 | Morley Mann | Apparatus for forming coils |
| FR2554021B1 (fr) | 1983-11-02 | 1987-09-04 | Autocoussin Sa | Machine automatique perfectionnee pour cambrer selon une configuration speciale des elements minces et rectilignes, et notamment des fils metalliques |
| IT8453880V0 (it) * | 1984-10-02 | 1984-10-02 | Mauro Meliga | Macchina curvatrice per tubi profilati e simili |
| FR2624038A1 (fr) * | 1987-12-02 | 1989-06-09 | Snecma | Outillage de cintrage de canalisations et procede de fabrication d'une canalisation a embout soude |
| US5197320A (en) * | 1990-07-26 | 1993-03-30 | Usui Kokusai Sangyo Kaisha Ltd. | Method of and apparatus for bending a metal tube of a small diameter |
| JPH04127919A (ja) * | 1990-09-17 | 1992-04-28 | Opton Co Ltd | 曲げ装置 |
| IT1251934B (it) * | 1991-10-16 | 1995-05-27 | Macchine Curvatubi Crippa Agos | Macchina curvatubi polifunzionale |
-
1997
- 1997-01-14 FR FR9700437A patent/FR2758281B1/fr not_active Expired - Fee Related
-
1998
- 1998-01-09 EP EP98902049A patent/EP0952896B1/de not_active Expired - Lifetime
- 1998-01-09 DE DE69800795T patent/DE69800795T2/de not_active Expired - Fee Related
- 1998-01-09 CA CA002275946A patent/CA2275946A1/fr not_active Abandoned
- 1998-01-09 WO PCT/FR1998/000033 patent/WO1998031484A1/fr not_active Ceased
- 1998-01-09 US US09/341,512 patent/US6185969B1/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| DE69800795T2 (de) | 2002-05-29 |
| FR2758281A1 (fr) | 1998-07-17 |
| EP0952896A1 (de) | 1999-11-03 |
| US6185969B1 (en) | 2001-02-13 |
| WO1998031484A1 (fr) | 1998-07-23 |
| DE69800795D1 (de) | 2001-06-21 |
| FR2758281B1 (fr) | 1999-04-02 |
| CA2275946A1 (fr) | 1998-07-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0892686B1 (de) | Maschine zum biegen oder wölben von profilen und biegekopf für solche maschine | |
| FR2513926A1 (fr) | Mecanisme de commande du bras de prehension d'un manipulateur robot | |
| EP0168331B1 (de) | Maschine zum Biegen von Rohren, Stangen oder Profilen | |
| CA1252030A (fr) | Machine automatique perfectionnee pour cambrer selon une configuration spatiale des elements minces et rectilignes, et notamment des fils metalliques | |
| WO2008142252A2 (fr) | Unite de cintrage d'un tub | |
| FR2479039A1 (fr) | Groupe de blocage et de rotation de fils, tubes et barres et son utilisation dans les machines a cintrer ou cintreuses | |
| CA2275946A1 (fr) | Machine a cintrer des tubes de faible diametre | |
| EP2274117B1 (de) | Versorgungsstation | |
| CA1260737A (fr) | Procede de reglage d'un laminoir a cylindres obliques et laminoir pour la mise en oeuvre de ce procede | |
| FR2795006A1 (fr) | Dispositif de cintrage d'elements metalliques allonges tels que des tubes | |
| EP2035310B1 (de) | Spuler mit expandierbarem dorn für eine rolle | |
| EP0281488B1 (de) | Drehender Biegekopf für Rohrbiegemaschine | |
| BE1010497A6 (fr) | Dispositif pour l'alimentation, la reception et le dechargement de pieces telles que des tubes ou des barres qui doivent etre traites dans une machine de coupe travaillant avec un rayon laser. | |
| FR2541603A1 (fr) | Appareil a cintrer | |
| FR2531649A1 (fr) | Appareil pour faire avancer une lame de scie dans une machine servant a faconner des lames de scie | |
| EP0092462B1 (de) | Herstellungs- und Transportvorrichtung von bearbeiteten Drahtstücken | |
| CA2244440C (fr) | Tete de travail pour machine de faconnage d'objets | |
| FR2462959A1 (fr) | Machine pour l'usinage fin, par exemple le rasage du flanc des dents de roues dentees | |
| EP0043750A1 (de) | Vorrichtung zum Formen von Rohren mit kleinem Durchmesser | |
| WO2002078155A1 (fr) | Pince motorisée pour plier des barres d'enroulements | |
| FR2659879A1 (fr) | Dispositif de dressage d'un fil metallique. | |
| EP0517637A1 (de) | Biegekopf mit Mehrfachwerkzeugen für eine Drahtbiegemaschine | |
| WO2008142305A2 (fr) | Machine a cintrer un profile selon deux sens de cintrage | |
| FR2685228A1 (fr) | Machine a cintrer un element du type tige, barre, tube, fil ou analogue. | |
| EP1097761A1 (de) | Vorrichtung zur Bearbeitung von Rohrenden |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19990615 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB IT |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| 17Q | First examination report despatched |
Effective date: 20000922 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20010516 |
|
| REF | Corresponds to: |
Ref document number: 69800795 Country of ref document: DE Date of ref document: 20010621 |
|
| ITF | It: translation for a ep patent filed | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20010516 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20011130 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020930 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20040121 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050802 |