EP1013360A1 - Verfahren zur Herstellung dünner keramischer Kerne für die Giesserei - Google Patents
Verfahren zur Herstellung dünner keramischer Kerne für die Giesserei Download PDFInfo
- Publication number
- EP1013360A1 EP1013360A1 EP99402794A EP99402794A EP1013360A1 EP 1013360 A1 EP1013360 A1 EP 1013360A1 EP 99402794 A EP99402794 A EP 99402794A EP 99402794 A EP99402794 A EP 99402794A EP 1013360 A1 EP1013360 A1 EP 1013360A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- ceramic
- manufacturing
- core
- strip
- thin
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/10—Cores; Manufacture or installation of cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C1/00—Compositions of refractory mould or core materials; Grain structures thereof; Chemical or physical features in the formation or manufacture of moulds
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C1/00—Compositions of refractory mould or core materials; Grain structures thereof; Chemical or physical features in the formation or manufacture of moulds
- B22C1/16—Compositions of refractory mould or core materials; Grain structures thereof; Chemical or physical features in the formation or manufacture of moulds characterised by the use of binding agents; Mixtures of binding agents
- B22C1/20—Compositions of refractory mould or core materials; Grain structures thereof; Chemical or physical features in the formation or manufacture of moulds characterised by the use of binding agents; Mixtures of binding agents of organic agents
- B22C1/22—Compositions of refractory mould or core materials; Grain structures thereof; Chemical or physical features in the formation or manufacture of moulds characterised by the use of binding agents; Mixtures of binding agents of organic agents of resins or rosins
Definitions
- the present invention relates to a method for manufacturing thin ceramic cores for precision foundry and its application to the production of turbine blades.
- foundry cores ceramics
- foundry cores ceramics
- aeronautical applications and by example, obtaining turbine blades in the foundry for turbojets.
- Improvement of foundry processes evolving from the equiax foundry to the foundry by directed or monocrystalline solidification, further increased these kernel requirements, the use and complexity are imposed by the search for high performance for parts to be obtained, as is the case for example for hollow blades with internal cooling.
- These fields of application are related to the precision foundry, in particular to the process known under the lost wax foundry designation. In all cases the use of the nucleus intervenes for the manufacture of hollow parts.
- compositions intended for the preparation of such nuclei are given by FR-A 2,371,257 and mainly contain fused silica, flour zircon and cristobalite which is a form of silica crystallized, a silicone resin being used as binder and additional elements in small quantities such that lubricant and catalyst being added.
- FR-A 2,371,257 mainly contain fused silica, flour zircon and cristobalite which is a form of silica crystallized, a silicone resin being used as binder and additional elements in small quantities such that lubricant and catalyst being added.
- FR-A 2,371,257 examples of known compositions intended for the preparation of such nuclei are given by FR-A 2,371,257 and mainly contain fused silica, flour zircon and cristobalite which is a form of silica crystallized, a silicone resin being used as binder and additional elements in small quantities such that lubricant and catalyst being added. The process of preparation
- the cores used to cast the parts and blades are made of ceramic with a generally porous structure: these cores are made from a mixture consisting of a refractory fraction (in the form of particles) and an organic fraction more or less complex.
- a refractory fraction in the form of particles
- an organic fraction more or less complex is described by EP-A 0 328 452.
- the shaping of the foundry cores in particular from thermoplastic pastes, can be done by molding using for example a press injection. This shaping is followed by a debinding operation during which the organic fraction of the nucleus is eliminated by various known means such as sublimation or thermal degradation, depending on the materials used.
- a porous structure results.
- a heat treatment for baking the core to consolidate the porous structure is then applied to the refractory fraction.
- This treatment introduces a dimensional modification, in the form of a withdrawal which is often non-isotropic in the volume of the nucleus, compared to the initial form. At this stage, it may be necessary to strengthen the core so that it is not damaged in the next cycle of use. It is known in this case in particular to carry out an impregnation by means of an organic resin.
- one or more thin cores as well obtained are assembled either together or on a core thick central.
- the core assembly obtained can then be used in foundry at lost wax according to current operations known per se wax injection, clustering, quenching and casting of metal parts to be obtained such as blades turbine.
- the preparation is rotated at low speed, of the order of 1 to 2 revolutions per minute during minus 48 hours.
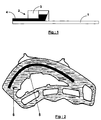
- the solution obtained is spread on a support 1 forming the casting bench.
- a shoe 2 provided a strip 3 makes it possible to obtain a strip 4 of thickness constant.
- the strip is preheated in the mold at 100 ° C for 30 minutes.
- the form mold used is preferably metallic.
- the strip is then pressed in the next step (f).
- a 40MPa pressure is applied for 3 minutes, the tape remaining in the mold.
- the part obtained can then, at the stage (g) next, be placed in a ceramic preform and undergo a standard cooking cycle including, in the example of realization whose compositions have been indicated previously maintained at 1250 ° C for 4 hours.
- the thin core obtained is then impregnated with an organic resin or polymer.
- the core thus obtained has sufficient mechanical strength to allow its use in its application in foundry where it will be subjected to pressure forces especially during the injection of wax in the known process in itself a lost wax foundry.
- Figure 2 shows a thin core 5 used for the manufacture of a blade of turbine 6.
- the thin core obtained and in order to ensure the geometries of required foundry piece can then be assembled with other thin nuclei or on a thick central nucleus obtained for example according to a conventional method of manufacture of foundry cores.
- various techniques can be used.
- the thin core can be assembled by gluing, in using, for example, a ceramic glue based on silica colloidal and a mullite mineral filler in mass proportions of 30 to 70 for example.
- a relationship mechanical by mortise-tenon system can also allow assembly.
- the link can be ensured by a quartz tube passing through the cores and the tube is held in its cavity by glue ceramic.
- the multi-core obtained after assembly can then be used as a standard foundry core and undergo the foundry cycle operations: wax injection, setting bunch, hardened, pouring of the part to be obtained, cooling, elimination of the nucleus.
- One of the advantages of using conformal thin cores to the invention is to facilitate the operations of setting cooling point of the cavity parts obtained such than turbine blades. Indeed, the modifications are facilitated because the cores obtained are machinable.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Mold Materials And Core Materials (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9814168A FR2785836B1 (fr) | 1998-11-12 | 1998-11-12 | Procede de fabrication de noyaux ceramiques minces pour fonderie |
| FR9814168 | 1998-11-12 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1013360A1 true EP1013360A1 (de) | 2000-06-28 |
| EP1013360B1 EP1013360B1 (de) | 2004-01-21 |
Family
ID=9532605
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99402794A Expired - Lifetime EP1013360B1 (de) | 1998-11-12 | 1999-11-10 | Verfahren zur Herstellung dünner keramischer Kerne für die Giesserei |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US6286582B1 (de) |
| EP (1) | EP1013360B1 (de) |
| DE (1) | DE69914299T2 (de) |
| FR (1) | FR2785836B1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2373747A (en) * | 2001-03-27 | 2002-10-02 | Howmet Res Corp | Impregnating a fired, porous ceramic core with a polymer |
Families Citing this family (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7343960B1 (en) | 1998-11-20 | 2008-03-18 | Rolls-Royce Corporation | Method and apparatus for production of a cast component |
| US6932145B2 (en) | 1998-11-20 | 2005-08-23 | Rolls-Royce Corporation | Method and apparatus for production of a cast component |
| US20040159985A1 (en) * | 2003-02-18 | 2004-08-19 | Altoonian Mark A. | Method for making ceramic setter |
| FR2875425B1 (fr) * | 2004-09-21 | 2007-03-30 | Snecma Moteurs Sa | Procede de fabrication d'une aube de turbomachine, assemblage de noyaux pour la mise en oeuvre du procede. |
| FR2878458B1 (fr) | 2004-11-26 | 2008-07-11 | Snecma Moteurs Sa | Procede de fabrication de noyaux ceramiques de fonderie pour aubes de turbomachines, outil pour la mise en oeuvre du procede |
| US7093645B2 (en) | 2004-12-20 | 2006-08-22 | Howmet Research Corporation | Ceramic casting core and method |
| WO2007040236A1 (ja) * | 2005-10-06 | 2007-04-12 | Mitsubishi Electric Corporation | ターボファン、空気調和機 |
| US20070221359A1 (en) * | 2006-03-21 | 2007-09-27 | United Technologies Corporation | Methods and materials for attaching casting cores |
| FR2914871B1 (fr) | 2007-04-11 | 2009-07-10 | Snecma Sa | Outillage pour la fabrication de noyaux ceramiques de fonderie pour aubes de turbomachines |
| CN102079653B (zh) * | 2010-12-06 | 2013-05-08 | 北京航空航天大学 | 航空发动机叶片用硅基陶瓷型芯的制备方法 |
| FR3022810B1 (fr) | 2014-06-30 | 2019-09-20 | Safran Aircraft Engines | Procede de fabrication d'un noyau pour le moulage d'une aube |
| CN104384452A (zh) * | 2014-10-24 | 2015-03-04 | 沈阳黎明航空发动机(集团)有限责任公司 | 一种薄壁硅基陶瓷型芯制备工艺 |
| US10507515B2 (en) | 2014-12-15 | 2019-12-17 | United Technologies Corporation | Ceramic core for component casting |
| DE102015111418A1 (de) | 2015-07-14 | 2017-01-19 | Nemak, S.A.B. De C.V. | Verfahren zum Herstellen eines Gießkerns und Gießkern |
| US20190060982A1 (en) | 2017-08-29 | 2019-02-28 | General Electric Company | Carbon fibers in ceramic cores for investment casting |
| KR20200045095A (ko) | 2018-10-22 | 2020-05-04 | 한국기계연구원 | 세라믹 판의 제조 방법 및 이를 제조하기 위한 성형부재 |
| CN110439627B (zh) * | 2019-08-30 | 2022-02-11 | 中国航发动力股份有限公司 | 一种叶片的气膜孔及尾劈缝孔防护方法 |
| FR3113255B1 (fr) | 2020-08-06 | 2022-10-07 | Safran | Protection contre l’oxydation ou la corrosion d’une pièce creuse en superalliage |
| FR3113254B1 (fr) | 2020-08-06 | 2022-11-25 | Safran | Protection contre l’oxydation ou la corrosion d’une pièce creuse en superalliage |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2241921A (en) * | 1990-03-17 | 1991-09-18 | Toshiba Ceramics Co | Moulding a refractory nozzle for the casting of molten metal |
| EP0648560A1 (de) * | 1993-10-13 | 1995-04-19 | Societe Nationale D'etude Et De Construction De Moteurs D'aviation "Snecma" | Verfahren zur Herstellung keramischer Kerne für die Giesserei |
| US5711833A (en) * | 1995-07-25 | 1998-01-27 | Thermicedge Corporation | Process for the production of thin walled ceramic structures |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4093017A (en) * | 1975-12-29 | 1978-06-06 | Sherwood Refractories, Inc. | Cores for investment casting process |
| US4190450A (en) | 1976-11-17 | 1980-02-26 | Howmet Turbine Components Corporation | Ceramic cores for manufacturing hollow metal castings |
| US4532974A (en) * | 1981-07-03 | 1985-08-06 | Rolls-Royce Limited | Component casting |
| FR2626794B1 (fr) | 1988-02-10 | 1993-07-02 | Snecma | Pate thermoplastique pour la preparation de noyaux de fonderie et procede de preparation desdits noyaux |
| US4989664A (en) * | 1988-07-07 | 1991-02-05 | United Technologies Corporation | Core molding composition |
| US5273104A (en) * | 1991-09-20 | 1993-12-28 | United Technologies Corporation | Process for making cores used in investment casting |
| US5394932A (en) * | 1992-01-17 | 1995-03-07 | Howmet Corporation | Multiple part cores for investment casting |
-
1998
- 1998-11-12 FR FR9814168A patent/FR2785836B1/fr not_active Expired - Fee Related
-
1999
- 1999-11-09 US US09/436,770 patent/US6286582B1/en not_active Expired - Lifetime
- 1999-11-10 DE DE69914299T patent/DE69914299T2/de not_active Expired - Lifetime
- 1999-11-10 EP EP99402794A patent/EP1013360B1/de not_active Expired - Lifetime
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2241921A (en) * | 1990-03-17 | 1991-09-18 | Toshiba Ceramics Co | Moulding a refractory nozzle for the casting of molten metal |
| EP0648560A1 (de) * | 1993-10-13 | 1995-04-19 | Societe Nationale D'etude Et De Construction De Moteurs D'aviation "Snecma" | Verfahren zur Herstellung keramischer Kerne für die Giesserei |
| US5711833A (en) * | 1995-07-25 | 1998-01-27 | Thermicedge Corporation | Process for the production of thin walled ceramic structures |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2373747A (en) * | 2001-03-27 | 2002-10-02 | Howmet Res Corp | Impregnating a fired, porous ceramic core with a polymer |
| GB2373747B (en) * | 2001-03-27 | 2005-02-23 | Howmet Res Corp | Impregnated ceramic core and method of making |
Also Published As
| Publication number | Publication date |
|---|---|
| FR2785836B1 (fr) | 2000-12-15 |
| FR2785836A1 (fr) | 2000-05-19 |
| DE69914299D1 (de) | 2004-02-26 |
| US6286582B1 (en) | 2001-09-11 |
| DE69914299T2 (de) | 2004-11-25 |
| EP1013360B1 (de) | 2004-01-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1013360B1 (de) | Verfahren zur Herstellung dünner keramischer Kerne für die Giesserei | |
| JP6097307B2 (ja) | 可動ブレード用セラミックコアの製造方法、セラミックコアおよび可動ブレード | |
| JP2005028455A (ja) | インベストメント鋳造法並びにそれに用いるコア及びダイ | |
| EP3630399B1 (de) | Verbessertes herstellungsverfahren eines bauteils mit einer dualen mikrostruktur | |
| EP0328452B1 (de) | Verfahren zur Herstellung von keramischen Gusskernen | |
| EP0648560B1 (de) | Verfahren zur Herstellung keramischer Kerne für die Giesserei | |
| FR3069179A1 (fr) | Procede de fabrication de pieces de forme complexe par moulage par injection de poudres metalliques. | |
| CA2759647C (fr) | Procede de fabrication d'un ensemble comprenant une pluralite d'aubes montees dans une plateforme | |
| EP4370260A1 (de) | Verbesserter formkern zur herstellung eines hohlen omc-teils | |
| EP4010135A1 (de) | Verfahren zur herstellung eines metallteils | |
| JPH0627482B2 (ja) | ラジアル型セラミックタービンローターの製法 | |
| FR3125237A1 (fr) | Noyau de fonderie amélioré pour la fabrication de pièce aéronautique métallique creuse | |
| JP2016514054A (ja) | セラミックコアの補修方法 | |
| WO2016071619A1 (fr) | Procédé pour fabriquer une pale de turbine en céramique. | |
| WO2016001564A1 (fr) | Procédé de fabrication d'un noyau pour le moulage d'une aube | |
| EP0478413B1 (de) | Verfahren zur Herstellung einer Geissform aus einem Schaumstoff und keramischem Kitt | |
| EP0112146B1 (de) | Keramischer Rotor und Verfahren zur Herstellung | |
| JP2019076954A (ja) | インベストメント鋳造用セラミックコア内の炭素繊維 | |
| FR3098740A1 (fr) | Procede de fabrication d’une piece metallique | |
| FR3125446A1 (fr) | Procédé de réalisation d’une préparation réfractaire pour la fabrication d’un moule en céramique, préparation obtenue par ce procédé, procédé de fabrication d’un moule en céramique et moule pour aube de turbomachine obtenu par ce procédé | |
| EP3980207B1 (de) | Verfahren zur herstellung eines turbomaschinenteils durch mim-formen | |
| EP3487649B1 (de) | Verfahren zur herstellung einer schalenform | |
| FR3098747A1 (fr) | Procede de fabrication d’une piece metallique | |
| CA2960059C (fr) | Procede de production d'un noyau ceramique | |
| EP4382226B1 (de) | Verfahren zur herstellung eines werkzeugs mit eutektischem material |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19991119 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Free format text: DE FR GB |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SNECMA MOTEURS |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 69914299 Country of ref document: DE Date of ref document: 20040226 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040317 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20041022 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD Owner name: SAFRAN AIRCRAFT ENGINES Effective date: 20170717 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20181023 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20181024 Year of fee payment: 20 Ref country code: GB Payment date: 20181024 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 69914299 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20191109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20191109 |