EP1016356A1 - Element ornemental et sa méthode de production - Google Patents
Element ornemental et sa méthode de production Download PDFInfo
- Publication number
- EP1016356A1 EP1016356A1 EP99830787A EP99830787A EP1016356A1 EP 1016356 A1 EP1016356 A1 EP 1016356A1 EP 99830787 A EP99830787 A EP 99830787A EP 99830787 A EP99830787 A EP 99830787A EP 1016356 A1 EP1016356 A1 EP 1016356A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- coils
- mandrel
- wire
- workpiece
- precious metal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- A—HUMAN NECESSITIES
- A44—HABERDASHERY; JEWELLERY
- A44C—PERSONAL ADORNMENTS, e.g. JEWELLERY; COINS
- A44C27/00—Making jewellery or other personal adornments
- A44C27/001—Materials for manufacturing jewellery
- A44C27/002—Metallic materials
-
- A—HUMAN NECESSITIES
- A44—HABERDASHERY; JEWELLERY
- A44C—PERSONAL ADORNMENTS, e.g. JEWELLERY; COINS
- A44C15/00—Other forms of jewellery
- A44C15/0045—Jewellery specially adapted to be worn on a specific part of the body not fully provided for in groups A44C1/00 - A44C9/00
- A44C15/005—Necklaces
-
- A—HUMAN NECESSITIES
- A44—HABERDASHERY; JEWELLERY
- A44C—PERSONAL ADORNMENTS, e.g. JEWELLERY; COINS
- A44C5/00—Bracelets; Wrist-watch straps; Fastenings for bracelets or wrist-watch straps
- A44C5/0053—Flexible straps
- A44C5/0061—Flexible straps essentially made from metal
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C37/00—Manufacture of metal sheets, rods, wire, tubes, profiles or like semi-manufactured products, not otherwise provided for; Manufacture of tubes of special shape
- B21C37/04—Manufacture of metal sheets, rods, wire, tubes, profiles or like semi-manufactured products, not otherwise provided for; Manufacture of tubes of special shape of rods or wire
- B21C37/045—Manufacture of wire or rods with particular section or properties
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21F—WORKING OR PROCESSING OF METAL WIRE
- B21F45/00—Wire-working in the manufacture of other particular articles
Definitions
- the present invention relates to the field of jewellery and costume jewellery and in particular relates to a tubular ornamental element for use in the above field.
- the invention also relates to a method for producing the tubular ornamental element as well as the jewellery and costume jewellery articles, typically necklaces and earrings, which can be made from the above mentioned ornamental element.
- An ornamental chain of the known type in the above mentioned field comprises a tubular structure, known as "gas-tube” according to a term familiar to any person skilled in the art.
- This chain is used in particular for the production of necklaces and bracelets and is formed by the connection of two helicoidal strip-shaped members with longitudinal edges bent in opposite sides.
- the coils of the helicoidal members are coaxially alternated in a continuous sequence, each of the two longitudinal bent edges of a coil of one member engaging with one of the opposedly bent edges of a pair of adjacent coils of the other one. Therefore, the structure of the "gas-tube” chain exhibit a nearly negligible axial and transverse play.
- the structure of the tubular ornamental element according to the present invention is characterized in that a precious or non-precious hollow wire with a substantially quadrilateral section, which is helicoidally bent according to adjacent coils about a longitudinal axis, the ends of the wire being connected by a substantially filiform tie rod extending along the longitudinal axis within the wire coils.
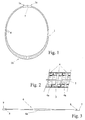
- a necklace is formed by a ornamental element according to the invention generally indicated at 1, with a closure 2 schematically shown in figure 1, connected at the ends la thereof in a conventional way and fit for engaging chain ends la with one another.
- Element 1 is formed by a hollow wire 3 of a substantially C-shaped quadrilateral cross section, of the known type, typically of precious metal, such as gold.
- Wire 3 is bent in the shape of a helic with side-by-side adjacent coils, of substantially circular cross section in the embodiment shown in figure 2, according to a substantially tubular arrangement.
- each coil 4 is shown as having a box-like section with a circumferential cut 4a on its inner side resulting form the wire production process, as will be described here below.
- the diameter of coils 4 is constant for a given length from ends la and symmetrically and continuously increases at an intermediate portion 1b of element 1 and, in such a way that the overall shape of element 1 and, consequently, of the necklace formed therewith is of the variable link size type.
- a substantial filiform tie rod 5 extends between ends la of element 1 inside coils 4, in a substantially axial direction with respect to the tubular development of element 1. More precisely, tie rod 5 connects the ends of hollow wire 3 threbetween, to ensure the axial alignment of coils 4, due to the traction force exerted by it , and consequently, to ensure the compactness of element 1, without hindering the mutual movement between adjacent coils.
- Tie rod 5, schematically shown in figure 2 may be constituted by a thin chain made of gold or other precious, metallic material, or, particularly for less valuable products, by a wire made of non-precious metal or other material such as nylon.
- the ornamental element 1 is made through a specific production process.
- a bimetallic wire must be prepared.
- the wire is formed by a non-precious metal core, such as copper, iron or an alloy fit for being solubilized by chemical attack with a suitable solvent, and an external layer of precious metal such as gold.
- the wire may be produced by known techniques such as plating or seaming.
- a bimetallic workpiece of quadrilateral section, in particular rectangular section has been used.
- Mandrel 6 is especially made in metallic or plastic material, for instance by known moulding or turning processes.
- the mandrel material is iron or an alloy thereof which, according to what will be described herebelow, also the above mentioned core can be made of.
- mandrel 6 comprises an enlarged central portion 6a for generating coils 4 of larger diameter and therefore the above mentioned variable size shape of element 1.
- Mandrel 6 also comprises end blocks 7 having respective through holes 8, within which the ends of the bimetallic wire are engaged as wounding is completed.
- the two or three coils forming the end portions of the workpiece are soldered together.
- the method further comprises a step of radial hammering of the workpiece with press or vibrating hammer means of known type to stabilize the helicoidal shape of coils 4 and eliminate, as far as possible, any discontinuity, in the form of small steps or gaps unavoidably formed between adjacent coils during wounding operation, with the aim of obtaining an essentially uniform and smooth external surface.
- coils 4 After emptying, even if lacking of the support provided by mandrel 6, coils 4 maintain an helical configuration due to their compression. On the other hand they are substantially free to mutually slide in the radial direction and, therefore, need a suitable locking capable of forming a stable tubular configuration of element 1.
- tie rod 5 To this end tie rod 5 is inserted axially within coils 4 and is connected to the ends of hollow wire 3.
- element 1 can have also a tubular development of a substantially constant diameter.
- coils 4 can have an elliptical or generally curved development, formed by means of a mandrel 6 with a correspondingly profiled cross section.
- Tie rod 5 can be formed by two or more chains or wires optionally intertwined to each other.
- the ornamental element according to the invention is particularly suited for the production of necklaces and earrings, but it can be used for the production of other jewellery goods as well, such as bracelets and pendants. Even if the ornamental effect of the element of the invention is somewhat similar to that of a "gas-tube" chain, it is made of only one piece with important advantages as far as the functionality and the aesthetic value of the product as well as the productivity of the process are concerned, the process being also relatively easy and inexpensive to carry out.
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Adornments (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT1998FI000282A IT1305067B1 (it) | 1998-12-29 | 1998-12-29 | Elemento ornamentale a sviluppo tubolare di impiego nel settore orafoe della bigiotteria, in particolare per la realizzazione di collane ed |
| ITFI980282 | 1998-12-29 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1016356A1 true EP1016356A1 (fr) | 2000-07-05 |
Family
ID=11352740
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99830787A Withdrawn EP1016356A1 (fr) | 1998-12-29 | 1999-12-21 | Element ornemental et sa méthode de production |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP1016356A1 (fr) |
| IT (1) | IT1305067B1 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2003022091A1 (fr) * | 2001-09-11 | 2003-03-20 | Rancangelo De Rancan Dario E Pietro S.N.C. | Procede relatif a l'elaboration d'elements metalliques allonges |
| EP1245168A3 (fr) * | 2001-03-26 | 2003-12-10 | Roana Antonio E Figli S.N.C. | Un produit manufacturé d'ornement de type "dégradé" |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2099285A (en) * | 1981-05-28 | 1982-12-08 | Vieri Spa | Method for making necklaces, bracelets and the like by chains wound upon a supporting core |
| GB2161695A (en) * | 1984-07-21 | 1986-01-22 | Shikiseimitsu Kabushikikaisha | Metal wristwatch strap |
| EP0214363A1 (fr) * | 1985-07-30 | 1987-03-18 | Gebr. Niessing GmbH & Co. | Objet d'ornement |
| EP0441138A1 (fr) * | 1990-02-08 | 1991-08-14 | Georg Bunz | Chaîne ornementale |
| EP0638256A1 (fr) * | 1993-08-11 | 1995-02-15 | Comptoir Lyon-Alemand - Louyot | Procédé pour la fabrication d'un fil composite destiné à la réalisation de bijoux creux |
-
1998
- 1998-12-29 IT IT1998FI000282A patent/IT1305067B1/it active
-
1999
- 1999-12-21 EP EP99830787A patent/EP1016356A1/fr not_active Withdrawn
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2099285A (en) * | 1981-05-28 | 1982-12-08 | Vieri Spa | Method for making necklaces, bracelets and the like by chains wound upon a supporting core |
| GB2161695A (en) * | 1984-07-21 | 1986-01-22 | Shikiseimitsu Kabushikikaisha | Metal wristwatch strap |
| EP0214363A1 (fr) * | 1985-07-30 | 1987-03-18 | Gebr. Niessing GmbH & Co. | Objet d'ornement |
| EP0441138A1 (fr) * | 1990-02-08 | 1991-08-14 | Georg Bunz | Chaîne ornementale |
| EP0638256A1 (fr) * | 1993-08-11 | 1995-02-15 | Comptoir Lyon-Alemand - Louyot | Procédé pour la fabrication d'un fil composite destiné à la réalisation de bijoux creux |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1245168A3 (fr) * | 2001-03-26 | 2003-12-10 | Roana Antonio E Figli S.N.C. | Un produit manufacturé d'ornement de type "dégradé" |
| WO2003022091A1 (fr) * | 2001-09-11 | 2003-03-20 | Rancangelo De Rancan Dario E Pietro S.N.C. | Procede relatif a l'elaboration d'elements metalliques allonges |
Also Published As
| Publication number | Publication date |
|---|---|
| ITFI980282A1 (it) | 2000-06-29 |
| IT1305067B1 (it) | 2001-04-10 |
| ITFI980282A0 (it) | 1998-12-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US20030233845A1 (en) | Flexible piece of jewelry | |
| US6895737B2 (en) | Lightweight omega chain and improved method of manufacture | |
| US6860097B2 (en) | Lightweight omega chain and improved method of manufacture | |
| US6381942B1 (en) | Thin walled attached silver filled gold jewelry | |
| GB2042943A (en) | Composite Material of Precious Metals | |
| US6092358A (en) | Thin walled silver filled gold jewelry | |
| EP1245168A2 (fr) | Un produit manufacturé d'ornement de type "dégradé" | |
| US20010039792A1 (en) | Thin walled attached silver filled gold jewelry | |
| US20090241598A1 (en) | Method of forming hollow and solid jewelry chains and chains formed therefrom | |
| JP4072567B2 (ja) | 装身具用ワイヤの製造方法 | |
| US20060042222A1 (en) | Method for the production of elongated elements afor jewels | |
| US6274250B1 (en) | Process for manufacture of jewelry and jewelry made thereby | |
| JP3030775B1 (ja) | 装身具 | |
| JP2001509409A (ja) | ファッション・アクセサリの製造法、該法実施のための装置およびかくして得られたファッション・アクセサリ | |
| EP1679015A1 (fr) | Procédé pour fabriquer des articles de bijouterie | |
| ITFI980282A1 (it) | Elemento ornamentale a sviluppo tubolare di impiego nel settore orafoe della bigiotteria, in particolare per la realizzazione di collane ed | |
| KR100463458B1 (ko) | 액세서리용 체인 및 그 제조방법 | |
| WO2003022091A1 (fr) | Procede relatif a l'elaboration d'elements metalliques allonges | |
| KR100490282B1 (ko) | 장신용 체인의 제조방법 | |
| RU2147823C1 (ru) | Способ изготовления полых тонкостенных ювелирных изделий или их элементов из золотых или серебряных сплавов | |
| EA002943B1 (ru) | Способ изготовления цепочки и цепочка, изготовленная таким способом | |
| JP3072328U (ja) | 装飾具用ワイヤ | |
| NL1000789C2 (nl) | Sieraad gemaakt van stafvormig materiaal dat is opgebouwd uit twee edelmetalen. | |
| JPH03258209A (ja) | 宝飾用貴金属品の製造方法 | |
| KR100392883B1 (ko) | 파이프를 이용한 신변장신구의 제조방법 및 그 신변장신구 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE DE ES FR GB IT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20010102 |
|
| AKX | Designation fees paid |
Free format text: BE DE ES FR GB IT |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20020702 |