EP1059233A1 - Procédé et dispositif pour emballer des objets dans une housse en feuille - Google Patents
Procédé et dispositif pour emballer des objets dans une housse en feuille Download PDFInfo
- Publication number
- EP1059233A1 EP1059233A1 EP99107666A EP99107666A EP1059233A1 EP 1059233 A1 EP1059233 A1 EP 1059233A1 EP 99107666 A EP99107666 A EP 99107666A EP 99107666 A EP99107666 A EP 99107666A EP 1059233 A1 EP1059233 A1 EP 1059233A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- film
- gap
- hood
- bow
- frame
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000000034 method Methods 0.000 title claims description 17
- 238000004806 packaging method and process Methods 0.000 title claims description 15
- 229920006302 stretch film Polymers 0.000 claims description 4
- 239000011248 coating agent Substances 0.000 claims description 3
- 238000000576 coating method Methods 0.000 claims description 3
- 239000000463 material Substances 0.000 claims description 2
- 239000004033 plastic Substances 0.000 claims 1
- 229920003023 plastic Polymers 0.000 claims 1
- 239000011888 foil Substances 0.000 abstract description 15
- 238000007373 indentation Methods 0.000 abstract 2
- 238000004519 manufacturing process Methods 0.000 description 5
- 238000005520 cutting process Methods 0.000 description 4
- 230000003068 static effect Effects 0.000 description 4
- 230000000694 effects Effects 0.000 description 3
- 238000003466 welding Methods 0.000 description 3
- 238000010276 construction Methods 0.000 description 2
- 238000003825 pressing Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 230000035515 penetration Effects 0.000 description 1
- 239000002985 plastic film Substances 0.000 description 1
- 229920006255 plastic film Polymers 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 230000037303 wrinkles Effects 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/10—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs
- B65B9/13—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs the preformed tubular webs being supplied in a flattened state
- B65B9/135—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs the preformed tubular webs being supplied in a flattened state for palletised loads
Definitions
- the invention relates to a method for packaging objects according to the The preamble of claim 1 and a device for packaging objects according to the preamble of claim 6.
- Methods and devices of the generic type are used in particular for Packaging of stacks of goods arranged on pallets is used to pack the goods against slipping on the pallet by those occurring during transport
- the film hood is pulled in Stretched crosswise and lengthways. That is, it becomes elastic before covering stretched in the transverse direction and elastic in the longitudinal direction during the covering stretched. After covering, the film hood is elastic on all sides resiliently against the stack of goods and the gripped pallet. It takes hold of it Palette.
- the film hood presses the often consisting of individual bags or boxes Stack of goods in themselves and as a whole against the pallet.
- the plastic films used for such packaging are extremely elastic stretchy. However, they also have high internal friction. That is, the Elastic stretched film does not return completely in one after relief "rushing movement” back to their relieved position. Rather, the Return to the relieved state at least partially in a continuous, movement requiring a certain period of time.
- EP-A-0 633 186 discloses a method and a device for wrapping of general cargo, in which a stretch film is drawn over a stack of goods becomes. To do this, first a film tube of the desired length is closed welded to a film hood and cut off above the weld. The the film hood formed in this way is made up of four rectangles by means of reefing rollers Gripping devices raised and stretched across in a shape that something is larger than the cross section of the stack of goods to be packed. Then will the film hood by a downward movement of the gripping devices over the Good stack pulled and stretched in the longitudinal direction by the film under Considerable sliding friction is deducted from the gripping devices. To increase the friction of the film when peeling it off, i. H.
- DE 90 01 319 U1 describes a further device for packaging objects known to be used in the movable jaws to the film hood to press against the stack of goods in a lower area. This too The procedure prevents the film hood from sliding up until the understretch is completed, however, can easily cause unwanted damage of the film hood or the packaged goods and also brings one unwanted additional construction effort.
- the film over at least one recess of the sliding surface, i.e. least a section in the sliding surface that is opposite to it in the sliding direction immediately preceding and immediately following sliding surfaces the resistance the film offers to its peeling optimized. Because the film pulls in its under tension currently the area bridging the depression together. It penetrates through it into the recess. When leaving the recess, the film is redirected again and stretched again due to the positive connection with the surface deflecting it. An intensified frictional engagement occurs here. It’s not absolutely necessary that the bow-like frame sections in a particular degree compared to the adjacent Project the contour of the frame support.
- the recess over which the film is guided as Gap formed between the bracket-like frame section and the bracket support is.
- the bow-like frame section and the bow support usually anyway Two separate components can be represented by enlarging them Simply create a gap in the parting line.
- the gap in before or during the removal of the film its depth T or / and its length L is changed or changed can. Due to the general adjustability, the gap can be adjusted for each individual case relevant parameters such as film material, film thickness, pulling speed, Preloading the film, profile of the stack of goods to be packed, etc. be adjusted.
- By adjusting the gap during the pulling movement can, it becomes possible, for example, to change in the course of the coating Friction conditions, a charge contour that changes in the pulling direction, but also other parameters that change in the course of the coating To take into account.
- the fact that the depth T of the gap (i.e. the distance from the lowest point of the gap up to the highest point in the pulling direction of the Foil immediately following sliding surface) and the length L of the gap independently will be a particularly sensitive adjustment to the respective conditions possible.
- the film is guided so that the lower edge of the film hood in the Overdrawn phase snaps into the gap and contracts, so that Film end during the movement of the gripping device in relation to the overlay contour internally to form a substretch, at least temporarily is held.
- the wrapping of those still in contact with the film The sliding surface is intensified by guiding the film in this way, the friction enlarged.
- the film is passed over the gap so that it is only partially in contact faces the surfaces delimiting the gap. This can cause wrinkles pull apart in the film before the film over the bow-like frame sections running.
- the at least one depression of the sliding surface is as close as possible to the end of the Arranged gripping device on which the film runs from the gripping device. This means that a very short section of film is sufficient to place the film on the gripping devices to hold while opposing this to forming a substretch the overlay contour can be moved inwards. Foil is saved.
- the sliding surface seen in the sliding direction of the film, almost jumps into the recess. This is especially for holding the film important snapping of the film end in the manufacture of the Unterstretches the recess favors the end of the film when it reaches the recess is suddenly relieved.
- the inventive device is designed so that the Gap on each gripping device extends over its entire outer circumference. This means that the entire circumference occurs when the film is pulled off in the pull-over phase the bow-like frame section has increased resistance, which is the vertical stretch improved. In addition, this design can keep the film in the Improve the phase of making the bottom stretch.
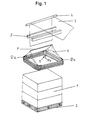
- the device for packaging objects 1 shown in FIG. 1 has one Supply roll, not shown, for a folded film tube 3, of unwound the supply roll and fed to a central packaging unit becomes.
- the packaging unit has a frame in which to be packed Objects are transported, and a packaging facility guided on this frame on. From this packaging facility are for the better Illustration only shows the components relevant to the invention.
- the film tube 3 is connected via a deflecting rod 4 led vertically down to a welding and cutting device 5. Below the welding and cutting device 5, the film tube 3 is opened and gripped from the inside by four movable gripping devices 8.
- the gripping devices 8 consist of the bracket-like frame sections 8 a and the bracket supports 8 b.
- the bracket-like frame sections 8 a and the bracket supports are L-shaped or C-shaped and thus define the corners of the film hood.
- a predetermined length of the film tube 3 on the gripping devices Following the gripping of the film tube 3 is a predetermined length of the film tube 3 on the gripping devices. This is done by a reefing roller 10 on each outside of each gripping device 8, the film tube 3 pulls on the gripping device, which causes the film tube on the discharge side the reef roll merges into a folded supply 6 a. (Hitting the slide not shown in the drawing using the reef rollers).
- the film tube 3 is then welded and cut to a desired length so that a Foil hood 6 is formed, which by the four gripping devices 8 into a rectangle is spanned.
- the film hood 6 stretched in this way is in a next one Step stretched in the horizontal direction so that the lower opening of the film hood 6 is somewhat larger than the cross section of the stack of goods 1 to be packed.
- the film takes on its "covering contour". Then will the film hood 6 is moved down and pulled onto the stack of goods 1. The the welded end of the film hood lies on the top of the stack of goods 1 on. The film is now, braked by the gripping devices 8, pulled off. Here it is stretched in the vertical direction.
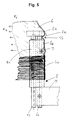
- FIGS. 2 and 3 Associated detail enlargement Fig. 5.
- the film hood 6 is in when pulling in deducted in the vertical direction continuously from the dormant stock 6 a. It passes the freely rotating roller 9, which acts as a counter roller when the film hits it serves for the reef roller 10. From the main sliding surface 8 a of the bow-like Frame section 8 is the film over the gap representing a recess 15 pulled.
- a different design of the depression (not shown here), for example as a local trough that is rounded on all sides is possible. At only local extension of the depression, it is particularly advantageous if the depression extends over the outer corner, i.e. the intersection of the two legs the gripping device extends.
- the film in the area of the gap 15 no longer has bow-like frame sections is supported, it pulls due to its bias during the Passage across the gap together, d. H. it pulls into the gap. Because of that the film, due to its internal friction, does not is suddenly able to contract completely, it depends on the dimensions L and T of the gap (dimensions: see Fig. 9), with what intensity the film in the Gap.
- the wrapping of the bow-like frame section 8 is increased by the penetration of the film into the gap 15.
- the film lies to an increased extent on the area 8 e of the bow-like frame section 8 a facing away from the sliding side of the film.
- the film lying against the bow-like frame section in this area can only be pulled off the bow-like frame section 8 a by being further expanded, viewed in the circumferential direction. This leads to a significant increase in the frictional forces effective when pulling off. Because now the film is no longer pulled essentially only by the horizontal forces of the film indicated as F H on the film cutting line (resulting from the film tension in the horizontal direction) against the bow-like frame section 8 a.
- the vertical stretch i. H. the one that occurs when you pull it off Sliding friction force, influenced in a wide range by the fact that the length, on which the film 6 wraps around the bow-like frame section 8 a, by a Variation of the gap dimensions L and / or T (Fig. 9) to the given requirements is adjusted.
- Fig. 6 shows the situation when a fold 6 e from when pulling the hood withdrawn stock 6 a is withdrawn.
- the fold slides the sliding surface 8 c of the Bow support 8 b along.
- the foil sections are folded through the strong horizontal bias of the film is pressed tightly together. Between static friction occurs in the folds of film. If under unfavorable circumstances this static friction is greater than the sliding friction between the film and the sliding surface of the gripping device, the fold can no longer pull apart as long as they are under tension over the gripping device slides. This is undesirable. Because especially if there is a crease in the area of the bow-like frame sections, the film becomes impermissible loads exposed.
- the gap 15 prevents this. As soon as the fold 6 e in the area of the gap 15 glides, the fold is temporarily relieved of horizontal forces. The wrinkled one on top of the other placed film sections are no longer pressed against each other. The The fold can open and the film can align itself.
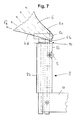
- Fig. 7 shows the situation immediately upon completion of the covering of the hood.
- the vertical movement of the gripping device 8 has ended.
- the slide is complete from the sliding surface 8 c of the stirrup support 8 d has been deducted.
- the slide end is just slid into the gap 15.
- FIG. 7 represents a snapshot insofar as it shows an outer end 6 b of the film hood that currently projects freely into the gap. However, this end, in particular depending on the internal friction of the film, is immediately caused by the film forces F R ( resulting from the film horizontal forces F H and the film vertical forces F V , see FIG. 5) on the cut surface of the film Because of the gap 15 or, preferably, applied to the area of the bow-like frame section 8 a facing away from the sliding side of the film.
- the situation shown in FIG. 8 thus occurs.
- the bow-like frame section 8 a engages behind the film opening.
- a kind of "bag” is pulled into the film.
- This "bag” loops around the bow-like frame section 8 a.
- the wrap angle W i.e. the angle at which the film faces the area facing away from the slide side of the film of the bow-like frame section 8a wrapped around the horizontal
- the opening 6 d of the film hood has a smaller extent than the areas of the Foil hood, as these are stretched by the bow-like frame section 8 a.
- the film hood can be used for the manufacture of the substretches the static friction between the film and bracket-like frame section 8 a held securely become.
- the film hood in the region of its opening 6 d should continue in the circumferential direction be stretched.
- the forces required for this are due the extensive wrap of the holding portion 8 b and accordingly high frictional forces are no longer available.
- the related self-reinforcing effect described with FIGS. 2 and 5 now comes here good for stiction. With suitable dimensioning of the gap, self-locking occurs on.
- the following effect can be used.
- the film As long as the film is in the covering phase of the hood bridging the gap, it pulls with appropriate dimensioning of the The gap is not completely in the gap. This can cause the film the bow-like frame section 8 a wraps only to such an extent that the sliding friction is increased, but there is no self-locking.
- the slide end in contrast, can penetrate deeper into the gap and thus settles in to a greater extent on the bow-like frame section 8 a. So that the friction be increased further in the overdraft phase. Under certain circumstances the self-locking phase of the film can be achieved.
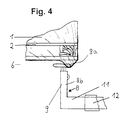
- Fig. 4 shows the situation when the Unterstretches is completed.
- the foil has frictionally applied to the side edge of the pallet.
- the tension of the film in the vertical direction this has almost broken down.
- the bow-like frame section 8 a can therefore easily by moving the gripping devices further inwards 8 be released from engagement with the film.
- Fig. 9 shows a bow-like frame section 8, in which an alternative design of the gap is executed.
- the rounding in the bottom of the gap can advantageously partially support the film when crossing the gap. Farther the rounding can be beneficial when holding the film shown in FIG. 8 impact by the end of the film also in this phase up to runs into the area of the curve.
- the dimension L shown in FIG. 9 can be changed in a simple manner by the bracket-like frame section attached to the guide rods 13 and 14 8 a in the vertical direction more or less pulled out of the bracket supports 8 d becomes. If the rods 13 and 14 in the corresponding guides run, all that needs to be done is the clamping (not shown in FIG. 9) between the Rods 13 and 14 and their guides are lifted. If necessary, it can Dimension L can also be changed during stalling if possible is provided to move the rods 13 and 14 motor-driven.
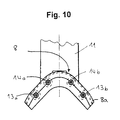
- Fig. 10 shows a view of a bracket-like frame section 8 a, of seen above.
- the rods 13 a and 14 a are indicated in dashed lines Gap 15 profiled and thus make it possible to find the one located in the area of the gap 15 To guide or support the film locally. These rods match of the rod 14 shown in Fig. 9.
- the rods 13b and 14b provide an alternative Execution. They are circular cylindrical throughout and offer none specially defined support or guidance.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Basic Packing Technique (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP99107666A EP1059233A1 (fr) | 1999-04-16 | 1999-04-16 | Procédé et dispositif pour emballer des objets dans une housse en feuille |
| US09/549,225 US6470654B1 (en) | 1999-04-16 | 2000-04-13 | Method and apparatus for packaging objects |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP99107666A EP1059233A1 (fr) | 1999-04-16 | 1999-04-16 | Procédé et dispositif pour emballer des objets dans une housse en feuille |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1059233A1 true EP1059233A1 (fr) | 2000-12-13 |
Family
ID=8237982
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99107666A Withdrawn EP1059233A1 (fr) | 1999-04-16 | 1999-04-16 | Procédé et dispositif pour emballer des objets dans une housse en feuille |
Country Status (2)
| Country | Link |
|---|---|
| US (1) | US6470654B1 (fr) |
| EP (1) | EP1059233A1 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2003062062A1 (fr) | 2002-01-24 | 2003-07-31 | Lachenmeier A/S | Procede et dispositif pour l'emballage de marchandises de detail |
| WO2009131449A1 (fr) * | 2008-04-23 | 2009-10-29 | Gerarda Maria Van Der Stam | Dispositif permettant d’emballer des produits |
Families Citing this family (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10103261A1 (de) * | 2001-01-25 | 2002-08-14 | Msk Verpackung Syst Gmbh | Verfahren zum Überziehen eines Flachschlauches |
| DK1497176T3 (da) * | 2002-04-19 | 2008-03-25 | Msk Verpackung Syst Gmbh | Anordning og fremgangsmåde til emballering af styk- eller pakkegods |
| FR2846943B1 (fr) * | 2002-11-12 | 2005-02-18 | Thimon | Procede et dispositif de mise en place d'une housse d'emballage de film plastique etirable sur une charge palettisee |
| US20050204709A1 (en) * | 2004-03-16 | 2005-09-22 | Regis Berger | Bagging of compressible bulk material |
| DE102004029132A1 (de) * | 2004-06-17 | 2005-12-29 | Basf Ag | Blends aus Styrol-Butadien-Blockcopolymeren und Polyolefinen für transparente, elastische Folien |
| DE102004029138A1 (de) * | 2004-06-17 | 2005-12-29 | Basf Ag | Blends aus Styrol-Butadien-Blockcopolymeren und Polyolefinen für transparente, elastische Folien |
| US20070220830A1 (en) * | 2006-03-27 | 2007-09-27 | Macleod Richard F J | Methods and apparatus for preserving pallet units of fresh perishables in modified atmosphere-containing bags |
| EP2060492B1 (fr) * | 2007-11-16 | 2011-11-30 | Msk-Verpackungs-Systeme Gesellschaft Mit Beschränkter Haftung | Dispositif destiné à recouvrir une feuille tubulaire ou une enveloppe de feuille sur une pile de marchandises |
| ES2670427T3 (es) | 2008-06-05 | 2018-05-30 | Kellogg Company | Procedimientos de producir un recipiente transportable |
| US8104520B2 (en) | 2008-06-11 | 2012-01-31 | Kellogg Company | Gentle handling hopper and scrunched bag for filling and forming a transportable container |
| US7861500B2 (en) * | 2008-07-14 | 2011-01-04 | Bradley Arthur Bennett | Automatic cart bagger |
| AU2009288034B2 (en) | 2008-09-03 | 2013-08-22 | Kellanova | A method of producing a transportable container for flowable bulk goods |
| EP2371716B1 (fr) * | 2008-12-19 | 2012-06-13 | MSK - Verpackungs-Systeme GmbH | Procédé et dispositif destinés à recouvrir une feuille tubulaire ou une enveloppe de feuille sur une pile de marchandises |
| US8225584B2 (en) * | 2009-08-21 | 2012-07-24 | Exxonmobil Chemical Patents Inc. | Film for stretch hood applications and method for using same |
| SG190181A1 (en) | 2010-12-01 | 2013-06-28 | Kellog Co | Transportable container for bulk goods and method for forming the same |
| DE102011000205B4 (de) | 2011-01-18 | 2014-07-17 | Illinois Tool Works Inc. | Vorrichtung und Verfahren zum Reffen eines Schlauchfolienabschnitts |
| DE102011075451B4 (de) * | 2011-05-06 | 2014-05-08 | Illinois Tool Works Inc. | Verfahren und Vorrichtung zum Aufreffen eines Schlauchfolienabschnitts auf die Refffinger einer Verpackungsanlage |
| FI124180B (fi) | 2011-09-30 | 2014-04-15 | Illinois Tool Works | Menetelmä käärintäkoneen kuljetustilaan saattamiseksi sekä käärintäkone |
| FI125661B (en) | 2012-09-07 | 2015-12-31 | Signode Int Ip Holdings Llc | Method and apparatus for positioning corner guards on a load |
| FI125411B (en) | 2013-10-31 | 2015-10-15 | Signode Internat Ip Holdings Llc | Method and Attachment Device for Attaching the End of a Wrapping Film Web to a Wrapping Machine, and a Wrapping Machine |
| DE102014106365B4 (de) | 2014-05-07 | 2017-06-14 | Lachenmeier Aps | Verpackungsverfahren zum Verpacken eines Gutes |
| DK178374B1 (en) * | 2014-11-04 | 2016-01-18 | Frank Bruhn Aps | HORIZONTALLY ARRANGED WRAP PACKAGING SYSTEM |
| DE102015101489A1 (de) * | 2015-02-02 | 2016-08-04 | Signode Industrial Group Llc | Verpackungsvorrichtung und Verfahren zum Betrieb derselben |
| DE102016212436B4 (de) * | 2016-07-07 | 2018-07-26 | Signode Industrial Group Llc | Verpackungsverfahren und Haubenstretchanlage |
| DE102019216346A1 (de) * | 2019-10-23 | 2021-04-29 | Signode Industrial Group Llc | Verfahren und Vorrichtung zum Verpacken eines Stapels von Gütern in einem schlauchförmigen Stretchfilm |
| US11492155B2 (en) | 2020-05-14 | 2022-11-08 | Signode Industrial Group Llc | Stretch-hood machine |
| JP7572912B2 (ja) * | 2021-05-27 | 2024-10-24 | 日立グローバルライフソリューションズ株式会社 | 冷蔵庫 |
| US20260070690A1 (en) * | 2024-09-09 | 2026-03-12 | Border Valley LLC | Bale packing assembly and method |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE9001319U1 (de) | 1990-02-06 | 1990-04-12 | MSK-Verpackungs-Systeme GmbH, 47533 Kleve | Vorrichtung zum Überziehen von Stretchfolienhauben über einen Gutstapel |
| EP0633186A1 (fr) | 1990-06-15 | 1995-01-11 | Bernhard Beumer Maschinenfabrik KG | Procédé et dispositif pour envelopper des marchandises |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE633186C (de) * | 1931-04-29 | 1936-07-21 | Jenaer Glaswerk Schott & Gen | Direkt geheizte Gluehkathode fuer gasgefuellte Entladungsgefaesse |
| DE8513892U1 (de) * | 1985-05-10 | 1985-09-05 | MSK - Verpackungs-Systeme GmbH, 4190 Kleve | Vorrichtung zum Überziehen und Einschrumpfen von Gutstapeln mit Schrumpfhauben |
| DE3621297A1 (de) * | 1986-06-25 | 1988-01-14 | Moellers Maschf Gmbh | Vorrichtung zum ueberziehen und anschrumpfen einer schrumpffolienhaube ueber bzw. an einen stapel. |
| DE4019041C1 (fr) | 1990-06-14 | 1991-10-17 | Bernhard Beumer Maschinenfabrik Kg, 4720 Beckum, De | |
| DE59106276D1 (de) * | 1990-09-13 | 1995-09-21 | Hannen Reiner Develog | Verfahren zum Überziehen von Stretchfolienhauben über einen Gutstapel und Vorrichtung zur Durchführung des Verfahrens. |
| US5398487A (en) * | 1993-11-26 | 1995-03-21 | Ag-Bag Corporation | Bale bagging machine |
| DE59811838D1 (de) * | 1998-11-05 | 2004-09-23 | Lachenmeier Kurt Aps | Verfahren und Vorrichtung zum Anbringen und Schrumpfen einer Verpackungshaube auf einem Gegenstand |
-
1999
- 1999-04-16 EP EP99107666A patent/EP1059233A1/fr not_active Withdrawn
-
2000
- 2000-04-13 US US09/549,225 patent/US6470654B1/en not_active Expired - Fee Related
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE9001319U1 (de) | 1990-02-06 | 1990-04-12 | MSK-Verpackungs-Systeme GmbH, 47533 Kleve | Vorrichtung zum Überziehen von Stretchfolienhauben über einen Gutstapel |
| EP0633186A1 (fr) | 1990-06-15 | 1995-01-11 | Bernhard Beumer Maschinenfabrik KG | Procédé et dispositif pour envelopper des marchandises |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2003062062A1 (fr) | 2002-01-24 | 2003-07-31 | Lachenmeier A/S | Procede et dispositif pour l'emballage de marchandises de detail |
| WO2009131449A1 (fr) * | 2008-04-23 | 2009-10-29 | Gerarda Maria Van Der Stam | Dispositif permettant d’emballer des produits |
Also Published As
| Publication number | Publication date |
|---|---|
| US6470654B1 (en) | 2002-10-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3918311C2 (de) | Verfahren und Vorrichtung zum Umhüllen von Stückgut, insbesondere Stückgutstapeln, mit einer Stretchfolienhaube | |
| EP2251267B1 (fr) | Dispositif et procédé d'emballage d'une unité de chargement dotée d'une feuille | |
| DE19732298C1 (de) | Vorrichtung und Verfahren zum Umhüllen eines Stapels | |
| DE69015497T2 (de) | Verfahren und Maschine zum Banderolieren einer palettisierten Ladung. | |
| EP2371716B1 (fr) | Procédé et dispositif destinés à recouvrir une feuille tubulaire ou une enveloppe de feuille sur une pile de marchandises | |
| EP1184281B1 (fr) | Procédé et dispositif pour emballer des objets | |
| EP1266828A1 (fr) | Procédé et appareil pour envelopper des piles de marchandises avec une housse ou un manchon de film étirable | |
| EP1963187B1 (fr) | Installation d'emballage par bache avec dispositif de realisation de plis lateraux | |
| EP0727353A2 (fr) | Emballeuse sous pellicule | |
| EP0399540B1 (fr) | Procédé et dispositif pour envelopper des marchandises avec une housse de film étirable et ensemble d'emballage formé avec ceux-ci | |
| DE102020106025A1 (de) | Verpackungsmaschine und Verfahren zum Verpacken eines Packguts mit einer aus einer oberen Papierbahn und einer unteren Papierbahn erzeugten Umverpackung | |
| EP0564971B1 (fr) | Dispositif et procédé pour fabriquer une pile d'articles | |
| DE3908957A1 (de) | Verfahren und vorrichtung zum umhuellen von stueckgut mit kunststoffolie | |
| WO2003062062A1 (fr) | Procede et dispositif pour l'emballage de marchandises de detail | |
| DE4307287C2 (de) | Verfahren zum Umhüllung eines Stapels | |
| EP1275581B1 (fr) | Procédé et appareil pour envelopper une pile de marchandises avec une housse de film étirable | |
| DE60311050T2 (de) | Verfahren und Vorrichtung zum Umhüllen einer palettisierten Ladung mit einer Stretchfolienhaube | |
| DE60302588T2 (de) | Verfahren und Vorrichtung zum Überziehen einer Stretchfolienhaube über eine palettesierte Ladung | |
| DE102009059049A1 (de) | Längstrennschweißvorrichtung für eine Folienverpackungsmaschine | |
| EP2130771B1 (fr) | Dispositif et procédé de recouvrement d'une feuille tubulaire sur une pile de marchandises | |
| EP1048565B1 (fr) | Procédé et dispositif pour emballer des objets dans une housse en feuille | |
| EP1048566A1 (fr) | Procédé et dispositif pour emballer des objets dans une housse en feuille | |
| EP1050459A2 (fr) | Procédé et dispositif pour envelopper un objet avec une feuille thermoplastique | |
| DE19824044A1 (de) | Schlauchbeutelverpackungsmaschine | |
| EP0445443B1 (fr) | Gaine à replis intérieurs en feuille étirable destinée à l'emballage d'articles |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20000323 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB IT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Free format text: DE ES FR GB IT |
|
| 17Q | First examination report despatched |
Effective date: 20030326 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20050510 |