EP1076103B1 - Verfahren und Vorrichtung zum Waermebehandeln von Blechen - Google Patents
Verfahren und Vorrichtung zum Waermebehandeln von Blechen Download PDFInfo
- Publication number
- EP1076103B1 EP1076103B1 EP00116544A EP00116544A EP1076103B1 EP 1076103 B1 EP1076103 B1 EP 1076103B1 EP 00116544 A EP00116544 A EP 00116544A EP 00116544 A EP00116544 A EP 00116544A EP 1076103 B1 EP1076103 B1 EP 1076103B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- zones
- sheets
- nozzle
- zone
- quench
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 30
- 238000010438 heat treatment Methods 0.000 title claims abstract description 10
- 238000010791 quenching Methods 0.000 claims abstract description 42
- 230000000171 quenching effect Effects 0.000 claims abstract description 30
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 22
- 238000005507 spraying Methods 0.000 claims abstract description 10
- 239000007921 spray Substances 0.000 claims description 4
- 238000011144 upstream manufacturing Methods 0.000 claims 1
- 239000002184 metal Substances 0.000 abstract description 9
- 238000001816 cooling Methods 0.000 description 10
- 239000000498 cooling water Substances 0.000 description 7
- 238000011161 development Methods 0.000 description 4
- 230000018109 developmental process Effects 0.000 description 4
- 229910000831 Steel Inorganic materials 0.000 description 3
- 210000000078 claw Anatomy 0.000 description 3
- 230000033001 locomotion Effects 0.000 description 3
- 239000010959 steel Substances 0.000 description 3
- 238000004364 calculation method Methods 0.000 description 2
- 238000010276 construction Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 238000005496 tempering Methods 0.000 description 2
- 238000004458 analytical method Methods 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 229910000734 martensite Inorganic materials 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 238000004886 process control Methods 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/62—Quenching devices
- C21D1/667—Quenching devices for spray quenching
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2221/00—Treating localised areas of an article
Definitions
- the sheets at a thickness of less than 10 mm completely have considerable dimensions, for example, 14 m x 3.5 m. Are such sheets in the middle cooled faster than at the edge, so the material in the middle waves; at faster edge cooling results in edge waves.
- Each batch can consist of a single sheet metal strip or else of secondary and / or consecutively arranged individual sheets.
- the treatment parameters bear the respective sheet geometry and occupancy calculation.
- the parameters are in stored on a computer and can be accessed as needed.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
- Heat Treatments In General, Especially Conveying And Cooling (AREA)
- Tunnel Furnaces (AREA)
Description
- in einem Ofen erwärmt,
- aus dem Ofen in eine Standquette transportiert,
- in der Standquette durch Besprühen ihrer Ober- und Unterseite mit Wasser abgeschreckt werden,
- zwei Zonen vorne/außen und zwei Zonen hinten/außen,
- zwei Zonen Mitte/außen,
- eine Zone vorne/Mitte und eine Zone hinten/Mitte,
- eine Zone Mitte und
wobei die oberhalb und unterhalb des Rollenganges angeordneten Düsen je zu neun Düsenzonen zusammengefasst sind, die ihrerseits je vier Düsenzonengruppen bilden, nämlich
- zwei Düsenzonen vorne/außen und zwei Düsenzonen hintenlaußen,
- zwei Düsenzonen Mitte/außen,
- eine Düsenzone vorne/Mitte und eine Düsenzone hinten/Mitte,
- eine Düsenzone Mitte
und wobei mittels der Steuermittel die Zonen der Bleche mit unterschiedlicher Abschreckgeschwindigkeit durch Einstellen der Wassermenge pro Fläche und Zeiteinheit oder durch Einstellen der Wassertemperatur und/oder unterschiedlicher Abschreckdauer und/oder zeitlich versetzt zueinander abgeschreckt werden.
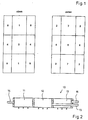
- Figur 1
- die Ober- und die Unterseite eines Blechs;
- Figur 2
- einen schematischen Schnitt durch ein Düsenrohr.
Claims (12)
- Verfahren zum Wärmebehandeln von Blechen, wobei die Bleche chargenweisewobei die Ober- und Unterseite der Bleche je in neun Zonen unterteilt wird, die zu vier Zonengruppen zusammengefasst werden, nämlichin einem Ofen erwärmt,aus dem Ofen in eine Standquette transportiert,in der Standquette durch Besprühen ihrer Ober- und Unterseite mit Wasser abgeschreckt werden,wobei die Zonen der Bleche mit unterschiedlicher Abschreckgeschwindigkeit durch Einstellen der Wassermenge pro Fläche und Zeiteinheit oder durch Einstellen der Wassertemperatur und/oder unterschiedlicher Abschreckdauer und/oder zeitlich versetzt zueinander abgeschreckt werden.zwei Zonen vorne/außen und zwei Zonen hinten/außen,zwei Zonen Mitte/außen,eine Zone vorne/Mitte und eine Zone hinten/Mitte,eine Zone Mitte und
- Verfahren nach Anspruch 1,
dadurch gekennzeichnet, dass die Zonen mit unterschiedlicher Abschreckintensität abgeschreckt werden, wobei die Abschreckintensität jeweils durch den Sprühabstand eingestellt wird. - Verfahren nach einem der Ansprüche 1 oder 2,
dadurch gekennzeichnet, dass die Zonen jeder Zonengruppe nach gemeinsamen Parametern abgeschreckt werden. - Verfahren nach einem der Ansprüche 1 bis 3,
dadurch gekennzeichnet, dass die Zonen im Ofen unterschiedlich erwärmt werden. - Verfahren nach Anspruch 4,
dadurch gekennzeichnet, dass die Temperatur im Ofen in Transportrichtung zunimmt. - Standquette zum chargenweisen Abschrecken von erwärmten Blechen, mit einem Rollengang und einer Mehrzahl von Düsen, die oberhalb und unterhalb des Rollengangs angeordnet und unter Zwischenschaltung von Steuermitteln an eine Wasserversorgung angeschlossen sind,
wobei die oberhalb und unterhalb des Rollenganges angeordneten Düsen je zu neun Düsenzonen zusammengefasst sind, die ihrerseits je vier Düsenzonengruppen bilden, nämlichwobei die Düsen jeder Düsenzone in Parallelschaltung an die Steuermittel angeschlossen sindzwei Düsenzonen vorne/außen und zwei Düsenzonen hinten/außen,zwei Düsenzonen Mitte/außen,eine Düsenzone vorne/Mitte und eine Düsenzone hinten/Mitte,eine Düsenzone Mitte
und wobei mittels der Steuermittel die Zonen der Bleche mit unterschiedlicher Abschreckgeschwindigkeit durch Einstellen der Wassermenge pro Fläche und Zeiteinheit oder durch Einstellen der Wassertemperatur und/oder unterschiedlicher Abschreckdauer und/oder zeitlich versetzt zueinander abgeschreckt werden. - Standquette nach Anspruch 6,
dadurch gekennzeichnet, dass die Düsenzonen jeder Düsenzonengruppe in Parallelschaltung an die Steuermittel angeschlossen sind. - Standquette nach Anspruch 6 oder 7,
dadurch gekennzeichnet, dass die Düsen von Düsenrohren (10) gebildet werden, die sich quer zur Transportrichtung des Rollengangs erstrecken und in gegeneinander abgedichtete, gesondert an die Steuermittel angeschlossene Rohrabschnitte (11 bis 13) unterteilt sind. - Standquette nach Anspruch 8,
dadurch gekennzeichnet, dass drei Rohrabschnitte (11 bis 13) vorgesehen sind und dass der mittlere Rohrabschnitt (12) über eine durch einen der seitlichen Rohrabschnitte (13) führende Leitung (15) an die Steuermittel angeschlossen ist. - Standquette nach einem der Ansprüche 6 bis 9,
dadurch gekennzeichnet, dass die oberhalb des Rollenganges vorgesehenen Düsen an einem vertikal verfahrbaren Quettenrahmen angeordnet sind, dessen Hubhöhe in Abhängigkeit von der Dicke der abzuschreckenden Bleche gesteuert wird. - Standquette nach einem der Ansprüche 6 bis 11,
gekennzeichnet durch eine vorgeschaltete Einrichtung zum definierten Ausrichten der Bleche. - Kammer-Pendelrollenherd-Erwärmungsanlage mit einer Standquette nach einem der Ansprüche 6 bis 11.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19937764A DE19937764A1 (de) | 1999-08-10 | 1999-08-10 | Verfahren und Vorrichtung zum Wärmebehandeln von Blechen |
| DE19937764 | 1999-08-10 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1076103A2 EP1076103A2 (de) | 2001-02-14 |
| EP1076103A3 EP1076103A3 (de) | 2003-04-02 |
| EP1076103B1 true EP1076103B1 (de) | 2005-12-28 |
Family
ID=7917870
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00116544A Expired - Lifetime EP1076103B1 (de) | 1999-08-10 | 2000-08-01 | Verfahren und Vorrichtung zum Waermebehandeln von Blechen |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1076103B1 (de) |
| AT (1) | ATE314491T1 (de) |
| DE (2) | DE19937764A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015115049A1 (de) * | 2015-09-08 | 2017-03-09 | Thyssenkrupp Ag | Verfahren und Vorrichtung zum Einstellen einer mechanischen Eigenschaft eines Werkstücks aus Stahl |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE886002C (de) * | 1942-10-09 | 1953-08-10 | Hoerder Huettenunion Ag | Verfahren zum Haerten von Blechen |
| JPS5848019B2 (ja) * | 1979-11-09 | 1983-10-26 | 石川島播磨重工業株式会社 | 鋼板の噴霧冷却方法及びその装置 |
| JPS60174833A (ja) * | 1984-02-20 | 1985-09-09 | Nippon Steel Corp | 熱鋼板の冷却方法 |
| JPS60197825A (ja) * | 1984-03-19 | 1985-10-07 | Yokogawa Hokushin Electric Corp | 冷却制御方法 |
| BE1010419A3 (fr) * | 1996-07-11 | 1998-07-07 | Ti Consult | Procede et dispositif de trempe de produits metalliques plats. |
-
1999
- 1999-08-10 DE DE19937764A patent/DE19937764A1/de not_active Withdrawn
-
2000
- 2000-08-01 DE DE50011947T patent/DE50011947D1/de not_active Expired - Lifetime
- 2000-08-01 EP EP00116544A patent/EP1076103B1/de not_active Expired - Lifetime
- 2000-08-01 AT AT00116544T patent/ATE314491T1/de active
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102015115049A1 (de) * | 2015-09-08 | 2017-03-09 | Thyssenkrupp Ag | Verfahren und Vorrichtung zum Einstellen einer mechanischen Eigenschaft eines Werkstücks aus Stahl |
| EP3141619A1 (de) * | 2015-09-08 | 2017-03-15 | ThyssenKrupp Steel Europe AG | Verfahren und vorrichtung zum einstellen einer mechanischen eigenschaft eines werkstücks aus stahl |
| DE102015115049B4 (de) * | 2015-09-08 | 2018-04-26 | Thyssenkrupp Ag | Verfahren und Vorrichtung zum Einstellen einer mechanischen Eigenschaft eines Werkstücks aus Stahl |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE314491T1 (de) | 2006-01-15 |
| EP1076103A2 (de) | 2001-02-14 |
| DE50011947D1 (de) | 2006-02-02 |
| DE19937764A1 (de) | 2001-02-15 |
| EP1076103A3 (de) | 2003-04-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3405244C1 (de) | Industrieofen,insbesondere Mehrkammer-Vakuumofen zur Waermebehandlung von Chargen metallischer Werkstuecke | |
| EP2233593B1 (de) | Verfahren und Warmumformanlage zur Herstellung von pressgehärteten Formbauteilen aus Stahlblech | |
| DE69314275T2 (de) | Wasser verwendende Entzunderungsvorrichtung | |
| DE3027846A1 (de) | Verfahren und einrichtung zum abkuehlen von blech, insbesondere stahlblech, mittels wasser | |
| EP3099829B1 (de) | Einrichtung zum kühlen von platten- oder bahnförmigem blech aus metall und verfahren zur wärmebehandlung | |
| EP3262202B1 (de) | Anlage für die serienfertigung pressgehärteter und korrosionsgeschützter blechformteile, mit einer kühleinrichtung zur zwischenkühlung der platinen | |
| EP3350352A1 (de) | Durchlaufkühlvorrichtung und verfahren zum abkühlen eines metallbandes | |
| EP0236666B1 (de) | Arbeitsverfahren zum Aufheizen von in Stranggusseinrichtungen gegossenen oder in Umformeinrichtungen umgeformten Halbzeugen für deren Einbringen in Umform- und/oder Weiterverarbeitungseinrichtungen | |
| EP3074150B1 (de) | Verfahren zum wärmebehandeln und abschreckeinrichtung zum kühlen von platten- oder bahnförmigem blech aus metall | |
| EP3862710B1 (de) | Ofen zur partiellen erwärmung von metallbauteilen | |
| EP3420111B1 (de) | Verfahren zur gezielten bauteilzonenindividuellen wärmebehandlung | |
| DE1558020A1 (de) | Durchlaufofen | |
| DE202015104565U1 (de) | Kühl- und Spritzwassersystem für mitteldickes Blech nach dem Walzen | |
| WO2019101486A1 (de) | Kühlbalken und kühlprozess mit variabler abkühlrate für stahlbleche | |
| DE2230401C3 (de) | Verfahren und Vorrichtung zur Steuerung der Gestalt von geformten, erhitzten Glasscheiben während des Kühlens | |
| EP3757496A1 (de) | Rollenherd-durchlauf-ofenanlage und verfahren zur erwärmung von mit aluminium, silizium und/oder zink beschichteten stahlplatinen auf härte- und presstemperatur | |
| EP1300484B1 (de) | Verfahren zur Wärmebehandlung von metallischen Pressbolzen | |
| DE2548116C3 (de) | Vorrichtung zum Abschrecken eines erwärmten Metallrohres | |
| DE19757485A1 (de) | Vorrichtung zum kontrollierten Abkühlen von warmgewalzten Profilen, insbesondere Trägern, direkt aus der Walzhitze | |
| EP1076103A2 (de) | Verfahren und Vorrichtung zum Waermebehandeln von Blechen | |
| WO2015155136A1 (de) | Vorrichtung und verfahren zum kühlen von stahlblechplatinen | |
| WO1994009164A1 (de) | Verfahren zur wärmebehandlung von metallischem gut | |
| EP4015657B1 (de) | Thermisches behandeln von bauteilen | |
| DE2129704A1 (de) | Verfahren zum Haerten von Tafelglas und Anlage zur Durchfuehrung des Verfahrens | |
| DE3234299C2 (de) | Verfahren zum Oberflächenhärten von Werkstücken und Vorrichtung zum Durchführen des Verfahrens |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SALZGITTER AG Owner name: LOI THERMPROCESS GMBH |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| 17P | Request for examination filed |
Effective date: 20030408 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| 17Q | First examination report despatched |
Effective date: 20041004 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051228 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051228 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50011947 Country of ref document: DE Date of ref document: 20060202 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060328 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060328 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060408 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20060405 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060529 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| ET | Fr: translation filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060831 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060831 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060831 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20060929 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051228 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20120813 Year of fee payment: 13 Ref country code: GB Payment date: 20120821 Year of fee payment: 13 Ref country code: SE Payment date: 20120821 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120823 Year of fee payment: 13 Ref country code: FR Payment date: 20120906 Year of fee payment: 13 Ref country code: DE Payment date: 20120822 Year of fee payment: 13 Ref country code: BE Payment date: 20120824 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20120813 Year of fee payment: 13 |
|
| BERE | Be: lapsed |
Owner name: *SALZGITTER A.G. Effective date: 20130831 Owner name: *LOI THERMPROCESS G.M.B.H. Effective date: 20130831 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 314491 Country of ref document: AT Kind code of ref document: T Effective date: 20130801 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20130801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130801 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130802 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140301 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50011947 Country of ref document: DE Effective date: 20140301 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20140430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130831 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130801 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130902 |