EP1122058B1 - Station d'encollage pour enveloppe à fenêtre - Google Patents
Station d'encollage pour enveloppe à fenêtre Download PDFInfo
- Publication number
- EP1122058B1 EP1122058B1 EP01100804A EP01100804A EP1122058B1 EP 1122058 B1 EP1122058 B1 EP 1122058B1 EP 01100804 A EP01100804 A EP 01100804A EP 01100804 A EP01100804 A EP 01100804A EP 1122058 B1 EP1122058 B1 EP 1122058B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- window
- blanks
- envelope
- suction
- suction roller
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000003292 glue Substances 0.000 title claims description 15
- 239000000463 material Substances 0.000 claims description 23
- 239000000853 adhesive Substances 0.000 claims description 17
- 230000001070 adhesive effect Effects 0.000 claims description 17
- 238000004026 adhesive bonding Methods 0.000 claims description 16
- 238000000034 method Methods 0.000 claims description 4
- 238000010586 diagram Methods 0.000 description 3
- 230000001154 acute effect Effects 0.000 description 1
- 230000000994 depressogenic effect Effects 0.000 description 1
- 230000035622 drinking Effects 0.000 description 1
- 230000002093 peripheral effect Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
- B31B70/74—Auxiliary operations
- B31B70/81—Forming or attaching accessories, e.g. opening devices, closures or tear strings
- B31B70/82—Forming or attaching windows
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2150/00—Flexible containers made from sheets or blanks, e.g. from flattened tubes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2160/00—Shape of flexible containers
- B31B2160/10—Shape of flexible containers rectangular and flat, i.e. without structural provision for thickness of contents
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2160/00—Shape of flexible containers
- B31B2160/10—Shape of flexible containers rectangular and flat, i.e. without structural provision for thickness of contents
- B31B2160/102—Shape of flexible containers rectangular and flat, i.e. without structural provision for thickness of contents obtained from essentially rectangular sheets
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
- B31B70/60—Uniting opposed surfaces or edges; Taping
- B31B70/62—Uniting opposed surfaces or edges; Taping by adhesives
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
- B31B70/74—Auxiliary operations
- B31B70/81—Forming or attaching accessories, e.g. opening devices, closures or tear strings
- B31B70/82—Forming or attaching windows
- B31B70/826—Forming or attaching windows involving applying window patches
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10S—TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10S493/00—Manufacturing container or tube from paper; or other manufacturing from a sheet or web
- Y10S493/916—Pliable container
- Y10S493/917—Envelope
- Y10S493/919—Envelope having window
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/10—Methods of surface bonding and/or assembly therefor
- Y10T156/1089—Methods of surface bonding and/or assembly therefor of discrete laminae to single face of additional lamina
- Y10T156/1092—All laminae planar and face to face
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1702—For plural parts or plural areas of single part
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1702—For plural parts or plural areas of single part
- Y10T156/1744—Means bringing discrete articles into assembled relationship
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T156/00—Adhesive bonding and miscellaneous chemical manufacture
- Y10T156/17—Surface bonding means and/or assemblymeans with work feeding or handling means
- Y10T156/1702—For plural parts or plural areas of single part
- Y10T156/1744—Means bringing discrete articles into assembled relationship
- Y10T156/1768—Means simultaneously conveying plural articles from a single source and serially presenting them to an assembly station
Definitions
- the invention relates to a window sticking station for an envelope machine, d. H. according to the features of the preamble of claim 1 a device for gluing prefabricated, from transparent Window material existing window cuts on window cutouts having blank envelopes.
- the window cuts are separated from a sheet made of window material and bonded to the envelope blanks with the help of glue.
- the glue can either on the envelope blanks or applied to the untrimmed window blank from which the window cuts are then separated.
- the parts provided with adhesive are then one as Suction roller trained adhesive cylinder supplied and there with the no adhesive parts connected (US 2 880 656 A).
- the sheet made of transparent window material runs basically slower than the paper web for the envelope blanks.
- the Window cuts are smaller and shorter than that in the direction of transport Blanks for the envelope blanks so that the window blanks before joining to the speed of the envelope blanks need to be accelerated.
- the invention is therefore based on the object of providing measures with the help of which said difficulties become easier than before let dominate.
- a compact design for the Device aimed.
- the invention provides with the features of Claim 1 before that a suction belt transport device at least in the area of the connection point as a carrier for the envelope blanks as a counter tool for the suction roll as a stick-on cylinder is provided.
- a suction belt transport device with one or more suction belts forms an essential counter tool for the sticker cylinder larger contact area than, for example, a counter roller.
- conveyor belts can adhere to a cylindrical contour of a sticker cylinder basically adapt and are therefore able to create a contact area to generate, which is much larger than a line-shaped connection point.
- the or Transport belts in the area of the suction roll serving as a sticker cylinder be moved in an arc.
- the transport belt or belts at least partially deflected into a trough at the contact point. This ensures that the window material Window cuts and the envelope blanks a safe one Make adhesive bond with each other.
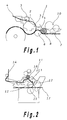
- a known device 1 for gluing prefabricated, from see-through window material existing window cuts 2 comprises a knife roller 3, by means of which the window blanks 2 of a material web 4 consisting of window material can be separated.
- Suction roller 5 the one rotating at the same peripheral speed Deflection roller 6 is assigned.
- the deflection roller 6 leads as Adhesive cylinder serving suction roller 5 envelope blanks wetted with adhesive 7 to.
- a glue roller 8 is also assigned to the deflection roller 6, which carries at least one glue element 9, with the aid of which glue applied to each envelope blank 7 from a gluing unit 10 becomes.
- the state of the Technique-related device 11 is first glue using a belonging to a gluing unit, not shown, glue roller 18 on the Material web 14 applied for the window blanks. Only in the direction of transport The knife roller 13 is arranged behind the glue roller 18 and acts with a counter roller 20 when cutting the window blanks 12 together.
- the counter roll 20 also includes one with the same Circumferential speed of the pressure roller 21. The nip between the counter roller 20 and the pressure roller 21 not just the isolated window cuts and wetted with adhesive 12, but also envelope blanks 17 fed and between the Counter roller 20 and the pressure roller 21 connected to each other.
- the device 31 for gluing prefabricated, from transparent Window material existing window blanks 32 on the edges of window cutouts in envelope blanks 37 according to FIG. 3 is much simpler and has fewer components than that for Prior art devices 1 and 11. It includes how 1 a knife roller 33 and a counter tool 34 for the window cuts 32.
- the knife roller 33 and that Counter tool 34 are immediately in front of one serving as a sticker cylinder Suction roller 35 arranged and cut through the window material - Material web 36 in the individual window blanks 32.
- the suction roller 35 are the glue roller 38 with at least one glue element 39 and the gluing unit 40, so that the glue roller 38 applies the adhesive to the window blanks 32 when they open of the suction roller 35 serving as a sticker cylinder.
- the ones that have already been isolated are also Envelope blanks 37 guided such that a window blank 32 when meeting over the window cutout in the envelope blank 37 comes to rest and with this with the help of the adhesive is connectable.
- FIG. 3 also shows that the Window blank 32 when applying glue on the suction roller 35 in one position A is located less than 180 ° before position B, in the the window blank 32 and the envelope blank 37 together get connected.
- the transport of the envelope blanks 37 to that as a sticker cylinder serving suction roller 35 is carried out with the aid of a suction belt transport device 41.
- This suction belt transport device 41 is used, however not only as a carrier for the envelope blanks 37, but at the same time also as a counter tool for those intended as stick-on cylinders Suction roller 35.
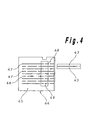
- the suction belt transport device 41 comprises at least one or according to the embodiment several, at a distance and parallel to each other arranged conveyor belts 43 and at least one suction box 44, which serves as a carrier for the upper run of the conveyor belts 43.
- the or the transport belts 43 can also have drinking openings and lie directly on the top 45 of the suction box 44 and slide over its cover plate 46 during operation.
- the cover plate 46 of the suction box 44 has the position of the Transport belts 43 a plurality of openings extending in the transport direction or slots 47, which are interrupted by webs 48.
- the Slots 47 each lie between the conveyor belts 43.
- the Window blanks 32 after the adhesive application until they rest on the Envelope blanks 37 arcuate.
- the immediate Contact of the window blanks 32 with the envelope blanks 37 both move briefly along an arcuate path accordingly the contour of the suction roller 35.
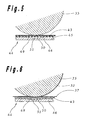
- the envelope blanks 37 meet at an acute angle and not tangential to the window blanks held by the suction roller 35 32 (Fig. 6). Immediately in the contact area of the window cuts 32 and the envelope blanks 37 is a trough 49 in the top 45 of the cover plate 46 of the suction box 44.
- This trough 49 is flat. It is in the form of a circular segment or in cross section approximately segment of a circle (Fig. 6). Envelope blanks 37 and the window blanks 32 move parallel in the contact area to the contour of the suction roller 35. The or the conveyor belts 43 give way dodge something in the trough 49 in the contact area, as shown in FIG. 6 is shown.
- the transport belts 43 In the idle state according to FIG. 5 when there is neither a window cut 32 another envelope blank 37 between the suction roller 35 and the transport belts 43, the transport belts 43 extend straight on the top 45 of the cover plate 46 of the suction box 44 and touch the suction roller 35 tangentially. The transport belts 43 dive not in the recess 49 so that their teeth 50 in one clear distance above the trough base 51. If the Suction roller 35, however, a window blank 32 in the contact area transported with the trough 49 and the conveyor belts 43 an envelope blank 37 of the contact and liaison point, see above are the conveyor belts 43 according to the material thickness of Window cut 32 and envelope blank 37 somewhat into the trough 49 depressed, as shown in Fig. 6. Touch even in this situation the teeth 50 of the conveyor belts 43 not the trough base 51.
- window panels 32 and envelope blank 37 are not used at the contact point directly supported transport belts 43 as a counter tool for the Adhesive cylinder or the suction roller 35.
- Adhesive cylinder or the suction roller 35 Along a short piece of sheet as well as briefly loop around the conveyor belts 43 together with the window cuts 32 and the envelope blanks 37 die Suction roller 35. This ultimately has the consequence that the window cuts 32 and the envelope blanks in the contact area during of bringing together and connecting together along an arc move.
- the greatest depth of the trough 49 can be about 1.5 to 2 millimeters opposite the level formed by the top 45 of the suction box 44.
- the conveyor belts 43 are constant during operation Force biased. This also applies if there is something in the trough 49 dodge. Due to the belt tension, the window cuts 32 and the envelope blanks 37 when connecting at the same time with constant Force pressed together.
- the suction belt transport device 41 accordingly the contour of the cover plate 45 both in front of the trough 49 and behind the trough 49 lies in a straight line in one plane.
- the transport belt or belts 43 are therefore only briefly at the contact and liaison point slightly deflected into the trough 49.
- the transport belt or belts 43 therefore wrap around the brewing roller serving as a sticker cylinder 35 not spacious, but only significantly more than linear. Therefore, there are almost no strains on the belt and none at all Shifts like a belt that is cylindrical Contour lays.
- the transport belt or belts meet at the connection point 43 tangential to the suction roller 35 and run in the same plane again tangentially from the suction roll 35 if there is no material between the suction roller 35 and the conveyor belts 43.
- the deflection of the transport belt (s) 43 therefore only takes place in the Scope and due to the parts to be connected.
- the suction belt transport device can 41 with a single, wide suction belt Suction holes and possibly one or more each have narrow, only carrying straps.
Landscapes
- Making Paper Articles (AREA)
Claims (15)
- Dispositif pour coller des pièces découpées de fenêtre préfabriquées, en matériau de fenêtre transparent, sur des ébauches d'enveloppe présentant des découpures de fenêtre, où les pièces découpées de fenêtre séparées d'une bande de matériau constituée de matériau de fenêtre, d'une part, et des ébauches d'enveloppe, d'autre part, peuvent être réunies à l'aide d'un rouleau d'aspiration servant de cylindre de collage et peuvent être assemblées avec de la colle, où est prévu et disposé un mécanisme d'application de colle (40) pour appliquer la colle sur les pièces découpées de fenêtre (32) de telle sorte que la pièce découpée de fenêtre (32), pendant l'application de la colle, se trouve déjà sur le rouleau d'aspiration (35) servant de cylindre de collage, à l'aide duquel la pièce découpée de fenêtre (32) peut être assemblée directement ensuite avec l'ébauche d'enveloppe (37), caractérisé en ce qu'il est prévu une installation de transport à courroie d'aspiration (41) au moins dans la zone de l'emplacement d'assemblage comme support pour les ébauches d'enveloppe (37) et comme contre-outil pour le rouleau d'aspiration (35) servant de cylindre de collage.
- Dispositif selon la revendication 1, caractérisé en ce que la pièce découpée de fenêtre (32), lors de l'application de la colle, se trouve sur le rouleau d'aspiration (35) servant de cylindre de collage dans une position (A) qui, dans la direction de rotation, se situe à un décalage inférieur à 180° en amont de la position (B) dans laquelle la pièce découpée de fenêtre (3) et l'ébauche d'enveloppe (37) peuvent être assemblées.
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que l'installation de transport à courroie d'aspiration (41) présente au moins une courroie de transport (43) et au moins un caisson d'aspiration (44) avec des ouvertures respectivement fentes (47) dans sa plaque de recouvrement (46) supportant les courroies de transport (43).
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que la respectivement les courroies de transport (43), dans la zone du rouleau d'aspiration (35) servant de cylindre de collage, sont déplaçables en forme d'arc.
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que les courroies de transport (43), dans la zone du rouleau d'aspiration (35) servant de cylindre de collage, sont déplaçables d'une manière légèrement concave au rouleau d'aspiration (35).
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que le caisson d'aspiration (44) présente dans son côté supérieur (45) orienté vers le rouleau d'aspiration (35) un creux (49).
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que la/les courroies de transport (43) sont déplaçables dans la zone du rouleau d'aspiration (35) sur le creux (49).
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que le creux (49), en section transversale, est réalisé en forme de segment de cercle.
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que le creux (49) est plat.
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que le creux (49) présente une profondeur maximale d'environ 1,5 à 2 mm relativement au côté supérieur (45) du caisson d'aspiration (44) portant les courroies de transport (43).
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que le rouleau d'aspiration (35), la/les courroies de transport (43) et le creux (49) sont dimensionnés de façon que la/les courroies de transport (43) sans pièce découpée de fenêtre (32) et sans ébauche d'enveloppe (37) s'appliquent tangentiellement au rouleau d'aspiration (35), sans plonger dans le creux (49).
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que les courroies de transport (43) et le creux (49) sont dimensionnés de façon que les courroies de transport (43), dans un état de fonctionnement avec une pièce découpée de fenêtre (32) et une ébauche d'enveloppe (37) entre le rouleau d'aspiration (35) et les courroies de transport (43), ne viennent pas en contact avec le fond (51) du creux.
- Dispositif selon au moins l'une des revendications précédentes, caractérisé en ce que les courroies de transport précontraintes (43) servent de contre-outil lors de la réunion et de l'assemblage des pièces découpées de fenêtre (32) avec les ébauches d'enveloppe (37).
- Procédé pour coller des pièces découpées de fenêtre préfabriquées, réalisées en matériau de fenêtre transparent, sur des ébauches d'enveloppe présentant des découpures de fenêtre, où les pièces découpées de fenêtre sont séparées d'une bande de matériau constituée de matériau de fenêtre et sont réunies au moyen d'un rouleau d'aspiration (35) avec les ébauches d'enveloppe et sont assemblées à l'aide d'une colle, où la colle est appliquée sur les pièces découpées de fenêtre (32) après que celles-ci ont été séparées de la bande de matériau (37), et où les pièces découpées de fenêtre (32), après l'application de la colle, jusqu'à l'application aux ébauches d'enveloppe (37), continuent à se déplacer en forme d'arc, caractérisé en ce que les pièces découpées de fenêtre (32) et les ébauches d'enveloppe (37) sont placées pendant un mouvement en forme d'arc les unes sur les autres et sont assemblées, où est utilisée une installation de transport à courroie d'aspiration précontrainte (41), servant de support aux ébauches d'enveloppe (37), comme contre-outil pour le rouleau d'aspiration (35) servant de cylindre de collage.
- Procédé selon la revendication 14, caractérisé en ce que les ébauches d'enveloppe (37) se déplacent en ligne droite vers l'emplacement de contact et d'assemblage avec les pièces découpées de fenêtre (32) et se déplacent en ligne droite au loin de l'emplacement de contact et d'assemblage, et en ce qu'elles sont déviées à l'emplacement de contact et d'assemblage en raison de l'épaisseur du matériau de la direction de déplacement rectiligne.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10002544 | 2000-01-21 | ||
| DE10002544A DE10002544A1 (de) | 2000-01-21 | 2000-01-21 | Fensteraufklebestation |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1122058A2 EP1122058A2 (fr) | 2001-08-08 |
| EP1122058A3 EP1122058A3 (fr) | 2002-07-10 |
| EP1122058B1 true EP1122058B1 (fr) | 2004-08-11 |
Family
ID=7628298
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01100804A Expired - Lifetime EP1122058B1 (fr) | 2000-01-21 | 2001-01-15 | Station d'encollage pour enveloppe à fenêtre |
Country Status (3)
| Country | Link |
|---|---|
| US (1) | US6634403B1 (fr) |
| EP (1) | EP1122058B1 (fr) |
| DE (2) | DE10002544A1 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105150593B (zh) * | 2015-08-31 | 2017-12-01 | 中山市正茂机械设备有限公司 | 一种贴窗机的定位贴膜装置 |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1001581B (de) | 1957-01-24 | Rengsdorf Richard Winkler (Kr Neuwied) und Kurt Dunnebier, Wollendorf (Kr Neuwied) | Verfahren und Vorrichtung zum Aufbringen einer Profilgummierung aus Latex auf Flachbeuteln, Brief umschlagen od dgl | |
| US2096789A (en) * | 1934-09-15 | 1937-10-26 | Coty Thomas Earl | Apparatus for making bags |
| GB495228A (en) * | 1936-10-20 | 1938-11-09 | Smithe Machine Co Inc F L | Mechanism for applying patches to envelope blanks and the like |
| US2880656A (en) * | 1954-06-25 | 1959-04-07 | Parten Machinery Company | Window envelope machine |
| DE1218274B (de) * | 1963-11-13 | 1966-06-02 | Winkler Richard | Vorrichtung zum Aufbringen des Fensterwerkstoffs auf Fensterausschnitte in gleichfoermig bewegten Bahnen oder Einzelzuschnitten aus Papier od. dgl. |
| US3618935A (en) * | 1969-06-23 | 1971-11-09 | New England Envelope Mfg Co | Transfer apparatus for a small piece of sheet material |
| US4108710A (en) * | 1972-02-14 | 1978-08-22 | B & H Manufacturing Company, Inc. | Apparatus for applying labels to containers |
| US4029537A (en) * | 1975-12-08 | 1977-06-14 | Pitney-Bowes, Inc. | Label applicator |
| DE3365835D1 (en) * | 1982-05-28 | 1986-10-09 | Smithe Machine Co Inc F L | Apparatus for making window patches |
| DE3905469A1 (de) * | 1989-02-22 | 1990-08-23 | Windmoeller & Hoelscher | Vorrichtung zum aufbringen von mit einem leimauftrag versehenen verstaerkungszetteln auf eine mit querperforationen versehene bahn |
| US5429576A (en) * | 1994-04-08 | 1995-07-04 | Winkler & Dunnebier | Apparatus for making reusable adhesive envelopes |
| DE10002543A1 (de) * | 2000-01-21 | 2001-07-26 | Winkler & Duennebier Ag | Verfahren und Vorrichtung zum Herstellen von Versandbeuteln einschließlich von Briefumschlägen |
-
2000
- 2000-01-21 DE DE10002544A patent/DE10002544A1/de not_active Withdrawn
-
2001
- 2001-01-15 EP EP01100804A patent/EP1122058B1/fr not_active Expired - Lifetime
- 2001-01-15 DE DE50103168T patent/DE50103168D1/de not_active Expired - Fee Related
- 2001-01-22 US US09/767,371 patent/US6634403B1/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| DE50103168D1 (de) | 2004-09-16 |
| US6634403B1 (en) | 2003-10-21 |
| EP1122058A2 (fr) | 2001-08-08 |
| EP1122058A3 (fr) | 2002-07-10 |
| DE10002544A1 (de) | 2001-07-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69212348T2 (de) | Seitenfaltvorrichtung mit Unterdruck für Umschlagfaltapparat | |
| EP1120238A2 (fr) | Méthode et dispositif pour alimenter un matériau en bande pendant la fabrication d'emballages | |
| WO1996014204A1 (fr) | Dispositif de façonnage d'une ebauche transportee le long d'une voie de transport a une vitesse predeterminee de transport | |
| DE69702667T2 (de) | Vorrichtung zum montieren von sägezahnschneidestreifen | |
| EP0031515A1 (fr) | Appareil pour découper des feuilles d'emballage d'une bande en mouvement | |
| DE2530992C3 (de) | Vorrichtung zum Herstellen von Verpackungszuschnitten | |
| EP2423137B1 (fr) | Dispositif de transport | |
| EP1105333B1 (fr) | Procede et dispositif de perforation de bandes de matiere | |
| EP0087724A1 (fr) | Appareil pour appliquer une bande de colle sur une feuille continue mobile | |
| EP1166977A1 (fr) | Machine pour la coupe automatisée d'imprimés | |
| EP0071229B1 (fr) | Procédé et dispositif pour la fabrication en continu de boîtes pliantes | |
| EP2130772B1 (fr) | Procédé et dispositif de fabrication de sections pour emballages de cigarettes | |
| WO2010091771A1 (fr) | Dispositif de coupe et de séparation | |
| DE2755625A1 (de) | Schneidvorrichtung | |
| DE102015011399B4 (de) | Vorrichtung und Verfahren zum Rillen, Perforieren, Schneiden und Ritzen von flächigen Elementen | |
| DE3504536C2 (fr) | ||
| EP1122058A2 (fr) | Station d'encollage pour enveloppe à fenêtre | |
| EP1112952B1 (fr) | Dispositif pour plier en continu de matériau plat | |
| EP0384221B1 (fr) | Dispositif pour appliquer des morceaux de papier de renforcement pourvus de colle sur une bande pourvue de perforations transversales | |
| EP0105191B1 (fr) | Dispositif de découpe pour des bandes flexibles | |
| EP1120239B1 (fr) | Méthode et dispositif de fabrication de sachets d'expédition | |
| DE102013113289A1 (de) | Vorrichtung sowie Verfahren zum Schneiden eines Bahnmaterials in Teilbahnen und Spreizen der Teilbahnen | |
| DE69001061T2 (de) | Schervorrichtung mit rotierendem messer. | |
| DE19546697A1 (de) | Fördereinrichtung für zu beleimende Zuschnitte aus Verpackungsmaterial zu einer Zigarettenverpackungsmaschine | |
| DE3744107A1 (de) | Einrichtung zur herstellung von querlinien an materialbahnen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20021029 |
|
| AKX | Designation fees paid |
Designated state(s): DE ES FR GB IT |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20040811 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040811 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040811 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50103168 Country of ref document: DE Date of ref document: 20040916 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041122 |
|
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20040811 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20050512 |
|
| EN | Fr: translation not filed | ||
| EN | Fr: translation not filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20070322 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080801 |