EP1266973B1 - Verfahren zur Herstellung eines leichtgewichtigen Formkörpers und Formkörper aus Metallschaum - Google Patents
Verfahren zur Herstellung eines leichtgewichtigen Formkörpers und Formkörper aus Metallschaum Download PDFInfo
- Publication number
- EP1266973B1 EP1266973B1 EP02450137.1A EP02450137A EP1266973B1 EP 1266973 B1 EP1266973 B1 EP 1266973B1 EP 02450137 A EP02450137 A EP 02450137A EP 1266973 B1 EP1266973 B1 EP 1266973B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- moulded body
- body according
- cavities
- metal
- particles
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 229910052751 metal Inorganic materials 0.000 title claims description 22
- 239000002184 metal Substances 0.000 title claims description 22
- 238000004519 manufacturing process Methods 0.000 title description 7
- 239000006262 metallic foam Substances 0.000 claims description 24
- 238000009826 distribution Methods 0.000 claims description 18
- 239000002245 particle Substances 0.000 claims description 15
- 239000011159 matrix material Substances 0.000 claims description 13
- 229910052782 aluminium Inorganic materials 0.000 claims description 5
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 5
- 229910000838 Al alloy Inorganic materials 0.000 claims description 2
- 239000013528 metallic particle Substances 0.000 claims description 2
- 239000004411 aluminium Substances 0.000 claims 1
- PNEYBMLMFCGWSK-UHFFFAOYSA-N aluminium oxide Inorganic materials [O-2].[O-2].[O-2].[Al+3].[Al+3] PNEYBMLMFCGWSK-UHFFFAOYSA-N 0.000 claims 1
- 229910052593 corundum Inorganic materials 0.000 claims 1
- 238000009827 uniform distribution Methods 0.000 claims 1
- 229910001845 yogo sapphire Inorganic materials 0.000 claims 1
- 230000006835 compression Effects 0.000 description 16
- 238000007906 compression Methods 0.000 description 16
- 239000006260 foam Substances 0.000 description 15
- 239000000463 material Substances 0.000 description 13
- 238000000465 moulding Methods 0.000 description 11
- 239000007789 gas Substances 0.000 description 7
- 239000000155 melt Substances 0.000 description 6
- 230000015572 biosynthetic process Effects 0.000 description 5
- 230000008901 benefit Effects 0.000 description 4
- 230000002902 bimodal effect Effects 0.000 description 4
- 230000002349 favourable effect Effects 0.000 description 4
- 230000009969 flowable effect Effects 0.000 description 4
- 238000000034 method Methods 0.000 description 4
- 239000011148 porous material Substances 0.000 description 4
- 230000002787 reinforcement Effects 0.000 description 4
- 238000007711 solidification Methods 0.000 description 4
- 230000008023 solidification Effects 0.000 description 4
- 238000012935 Averaging Methods 0.000 description 2
- 239000010953 base metal Substances 0.000 description 2
- 238000002591 computed tomography Methods 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 239000006261 foam material Substances 0.000 description 2
- 230000005484 gravity Effects 0.000 description 2
- 239000000203 mixture Substances 0.000 description 2
- 229910018072 Al 2 O 3 Inorganic materials 0.000 description 1
- UFHFLCQGNIYNRP-UHFFFAOYSA-N Hydrogen Chemical compound [H][H] UFHFLCQGNIYNRP-UHFFFAOYSA-N 0.000 description 1
- 239000006096 absorbing agent Substances 0.000 description 1
- 238000010521 absorption reaction Methods 0.000 description 1
- 230000009471 action Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000000052 comparative effect Effects 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000005489 elastic deformation Effects 0.000 description 1
- 238000005187 foaming Methods 0.000 description 1
- 239000001257 hydrogen Substances 0.000 description 1
- 229910052739 hydrogen Inorganic materials 0.000 description 1
- 238000011835 investigation Methods 0.000 description 1
- 239000007791 liquid phase Substances 0.000 description 1
- 229910001338 liquidmetal Inorganic materials 0.000 description 1
- 238000013507 mapping Methods 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 239000002905 metal composite material Substances 0.000 description 1
- 239000012768 molten material Substances 0.000 description 1
- 239000012071 phase Substances 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 239000012744 reinforcing agent Substances 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 239000011343 solid material Substances 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
- 238000004154 testing of material Methods 0.000 description 1
- 238000005979 thermal decomposition reaction Methods 0.000 description 1
- 230000008719 thickening Effects 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C1/00—Making non-ferrous alloys
- C22C1/08—Alloys with open or closed pores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D25/00—Special casting characterised by the nature of the product
- B22D25/005—Casting metal foams
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C1/00—Making non-ferrous alloys
- C22C1/08—Alloys with open or closed pores
- C22C1/083—Foaming process in molten metal other than by powder metallurgy
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C1/00—Making non-ferrous alloys
- C22C1/08—Alloys with open or closed pores
- C22C1/083—Foaming process in molten metal other than by powder metallurgy
- C22C1/086—Gas foaming process
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F3/00—Manufacture of workpieces or articles from metallic powder characterised by the manner of compacting or sintering; Apparatus specially adapted therefor ; Presses and furnaces
- B22F3/10—Sintering only
- B22F3/11—Making porous workpieces or articles
- B22F3/1103—Making porous workpieces or articles with particular physical characteristics
- B22F2003/1106—Product comprising closed porosity
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2998/00—Supplementary information concerning processes or compositions relating to powder metallurgy
Definitions
- the invention relates to a lightweight molded body of metal foam consisting of a metal matrix, in which particles are embedded and which encloses a plurality of substantially spherical and / or substantially ellipsoidal cavities.
- Molded metal foam naturally have a low density and, due to the structure, have special mechanical material properties.
- such bodies can be given large deformations with upsetting degrees of up to 70% and more when applying two- or three-dimensional compressive stresses.
- These materials with special properties are in the technological application, for example as an energy absorber in automotive technology and the like, can be used with advantage.
- Another lightweight metal body according to EP 545 957 B1 and US 5,221,234 a plurality of closed and isolated, generally spherical pores having sizes in the range of 10 to 500 microns. Although such small pores with large differences in diameter can lend a metal body formed with aluminum in comparison with the solid material lower specific gravity, a density of less than 1.0 g / cm 3 and degree of compression of over 60% of the material under defined conditions are usually not achievable ,
- This object of the invention in particular with regard to a desired material behavior under mechanical stress, is achieved in that the metal foam of the molding has a monomodal distribution of the maximum longitudinal extent of the cavities in the range between 1.0 and 30.0 mm when viewed spatially.
- the ratio of the maximum longitudinal extents of two different cavities on average at least 20 pairs is less than 45, are largely narrow load ranges, in which a collapse of the foam cavities begins to reach ,
- the accuracy of the transition from an elastic deformation in a plastic deformation of the material as a function of the compressive stress can be further increased if, viewed spatially of the metal foam, the ratio of the maximum longitudinal extent of two different cavities on average over at least 20 pairs less than 30, preferably less than 15 and in particular less than 5, is. These values refer to created cavities, ignoring solidification voids in the molding.
- Equally important for a metal foam production and for the behavior of the molded article under mechanical stress is the composition and structure of the liquid metal and that or those of the boundary walls of the cavities.
- the particles are embedded uniformly distributed in the metal matrix for reinforcement, there is a high and isotropic reinforcement of the base metal with regard to the mechanical stress. It is also advantageous if adjoining cavities are completely separated from one another by the metal matrix. Individual cracks, which can be caused by mechanical stress during cooling, are not effective for compression loads.
- the metal matrix consists of a light metal, preferably of aluminum or an aluminum alloy.
- the particles incorporated in the metal matrix have a size of 1 to 50 ⁇ m, preferably 3 to 20 ⁇ m, a particularly advantageous weight / property ratio can be achieved.
- reinforcement or reinforcement of the base metal for a foaming and solidification of the same or for a structure of kinkungsver prisonen bladder walls have inclusions of non-metallic particles, preferably SiC particles and / or Al 2 O 3 - particles and / or those of intermetallic phases as unexpected proved favorable.
- the volume fraction of the incorporated particles in the metal matrix is between 10% by volume and 30% by volume, preferably between 15% by volume and 30% by volume.
- the favorable weight / property ratio of a lightweight molded article of the type according to the invention can be increased if the density of the metal foam is less than 1.05 g / cm 3 , preferably less than 0.7 g / cm 3 , in particular less than 0.3 g / cm 3 , is.
- a lightweight molded article according to the invention is produced by a method in which a molten metal having a particle formed by introducing gas or gas mixtures into this, at least partially introduced into a mold and its liquid phase is solidified in this and a flowable metal foam with a monomodal distribution of the dimension of the cavities and a proportionately maximum longitudinal extent of the same in the range between 1.0 and 30.0 mm made, placed in a G dematforrn or mold and compacted therein in substantially under all-round pressure, wherein the cavities enclosing particles containing Metal melt boundary walls at least partially planar areas are granted and the solidification heat of the melt is dissipated.
- the inner body structure is formed such that the material has substantially accurate mechanical characteristics.
- the monomodal distribution of the dimensions of the cavities in the metal foam provides a prerequisite for a material behavior at certain stress states.
- the proportional maximum diameter of the cavities is important for the height the elastic limit of the material and the tolerable specific surface load at a Druckthesesbeaufschlagung of the part.
- a substantially all-sided, optionally low pressure load of the flowable foam is required, resulting in several advantages.
- the boundary walls and their node areas in the foam material for a mechanical support or buckling load are set or formed low.
- a cavitation formation in an Al molding according to the invention is shown in each case on the basis of a sectional image.
- the largest longitudinal extents of cavities in the range between 20 and 12 mm were found in the body of image A, with the proportional maximum extent being 17.2 mm.
- a compression of the flowable metal foam of only about 3.2% was made, significantly planar area are formed in the cavities enclosing boundary walls.
- Out Fig. 2 is the dependence of the compression stress of a shaped body of the
- a monomodal distribution of the largest longitudinal extension of the cavities and an increasing equality of the same affects narrowing the range of dependency.
- the beginning of the deformation or collapse is an exact material value when the pressure is applied to the same.
- the behavior of a foam component can be calculated precisely or, for certain functions, the design and construction of the foam part can be defined.
- the stress as a function of the compression deformation is in Fig. 3 compared with test results of three moldings.
- the structure of the lightweight moldings 1 and 2 with a density of 0.091 gcm -3 and 0.114 gcm -3 was according to the invention, the comparison body 3 had a bimodal distribution of the dimension of the cavities with material concentrations in the nodes of the foam walls.
- an extremely low hardening of the same is noted up to a degree of compression of about 70%.
- the comparison body 3 shows up to a compression ratio of about 45% a significant hardening of the material, which increases even further from this value. This indicates an effect of the bimodal distribution of the cavity dimensions.
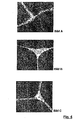
- Fig. 4 shows nodule shapes in the foam wall of lightweight bodies based on sectional images.
- Figure A shows a sharp-edged node formation of the wall between three cavities. Such knots are prone early to cracks and breaks in the connection area.
- Picture B shows a thickened wall node. This node formation leads to an increased specific weight and an unfavorable formation of the force components in a compression load of the body.
- Figure C shows a node with wall parts, where both the thickness of the walls and the node mass with a view to a high compression set with less Solidification of the body are designed low at high compression ratios.
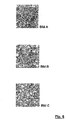
- Fig. 5 represented formed metal foam body without compression in plan view, wherein the gas was introduced in each case with different separation parameters for the bubbles durach projecting into the melt projecting entry pipes. A monomodal distribution of the respective dimensions of the gas bubbles can be seen.
- the body has a specific weight of 0.1 gcm -3 according to image A, those according to image B and image C have one of 0.2 gcm -3 and 0.4 gcm -3 .
- Computer tomography data sets can be used to calculate local density values (density mapping).
- An averaging process for calculating the local density makes it possible to determine the material distribution between the averaging volumes.
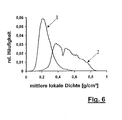
- Diagrams of the calculated density values of investigations can give information about the homogeneity of a lightweight molded article.
- the relative frequency of the mean local density in a molded body according to the invention determined by a computed tomography method is designated 1 and can be taken from a comparison body 2.
- the mean local density of the body 1 has a narrow frequency maximum at about 0.22 gcm -3 , demonstrating a monomodal distribution of the dimension of the cavities and a narrow range of the proportionately maximum longitudinal extent thereof.
- the multimodal comparison body is characterized by a marked decline of the broad mean local density values.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Manufacture Of Alloys Or Alloy Compounds (AREA)
- Powder Metallurgy (AREA)
- Manufacture Of Porous Articles, And Recovery And Treatment Of Waste Products (AREA)
- Continuous Casting (AREA)
- Porous Artificial Stone Or Porous Ceramic Products (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| SI200231055T SI1266973T1 (sl) | 2001-06-15 | 2002-06-14 | Postopek izdelave lahkega ulitka in ulitek iz penjene kovine |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT0093501A AT410103B (de) | 2001-06-15 | 2001-06-15 | Verfahren zur herstellung eines leichtgewichtigen formkörpers und formkörper aus metallschaum |
| AT9352001 | 2001-06-15 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1266973A2 EP1266973A2 (de) | 2002-12-18 |
| EP1266973A3 EP1266973A3 (de) | 2004-08-18 |
| EP1266973B1 true EP1266973B1 (de) | 2015-03-04 |
Family
ID=3683236
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02450137.1A Expired - Lifetime EP1266973B1 (de) | 2001-06-15 | 2002-06-14 | Verfahren zur Herstellung eines leichtgewichtigen Formkörpers und Formkörper aus Metallschaum |
Country Status (9)
| Country | Link |
|---|---|
| EP (1) | EP1266973B1 (cs) |
| JP (1) | JP4158170B2 (cs) |
| AT (1) | AT410103B (cs) |
| CA (1) | CA2390766C (cs) |
| CZ (1) | CZ304437B6 (cs) |
| ES (1) | ES2533772T3 (cs) |
| NO (1) | NO20022756L (cs) |
| PT (1) | PT1266973E (cs) |
| SI (1) | SI1266973T1 (cs) |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AT411768B (de) | 2002-09-09 | 2004-05-25 | Huette Klein Reichenbach Gmbh | Verfahren und vorrichtung zur herstellung von fliessfähigem metallschaum |
| DE50304053D1 (de) * | 2003-05-28 | 2006-08-10 | Univ Hannover | Schaumgiessverfahren sowie eine druckdicht verschliessbare Giessform zur Herstellung von Formteilen |
| DE10325819B4 (de) * | 2003-06-07 | 2005-06-23 | Friedrich-Alexander-Universität Erlangen-Nürnberg | Verfahren zur Herstellung eines Metallschaumkörpers |
| AT503824B1 (de) | 2006-07-13 | 2009-07-15 | Huette Klein Reichenbach Gmbh | Metallformkörper und verfahren zu dessen herstellung |
| DE102008000100B4 (de) | 2008-01-18 | 2013-10-17 | Fraunhofer-Gesellschaft zur Förderung der angewandten Forschung e.V. | Verfahren zur Herstellung eines leichtgewichtigen Grünkörpers, danach hergestellter leichtgewichtiger Grünkörper und Verfahren zur Herstellung eines leichtgewichtigen Formkörpers |
| JP5482658B2 (ja) * | 2008-09-12 | 2014-05-07 | 国立大学法人群馬大学 | 発泡金属用前駆体および発泡金属の製造方法、並びに前記製造方法で製造された発泡金属用前駆体および発泡金属 |
| WO2019070487A1 (en) * | 2017-10-04 | 2019-04-11 | Ih Holdings Limited | PROCESS FOR PRODUCING CHARGED METAL FOAMS |
| CN110438360B (zh) * | 2019-08-20 | 2021-05-25 | 北京康普锡威科技有限公司 | 泡沫铝或铝合金材料的制备方法 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NO172697C (no) * | 1989-07-17 | 1993-08-25 | Norsk Hydro As | Fremgangsmaate ved fremstilling av partikkelforsterket metallskum og resulterende produkt |
| US5112697A (en) * | 1989-09-06 | 1992-05-12 | Alcan International Limited | Stabilized metal foam body |
| US4973358A (en) * | 1989-09-06 | 1990-11-27 | Alcan International Limited | Method of producing lightweight foamed metal |
| DE69212157T2 (de) * | 1991-05-31 | 1996-11-21 | Alcan Int Ltd | Verfahren und vorrichtung zum herstellen profilierter platten aus teilchenstabilisiertem metallschaum |
| US5281251A (en) * | 1992-11-04 | 1994-01-25 | Alcan International Limited | Process for shape casting of particle stabilized metal foam |
-
2001
- 2001-06-15 AT AT0093501A patent/AT410103B/de not_active IP Right Cessation
-
2002
- 2002-06-10 NO NO20022756A patent/NO20022756L/no not_active Application Discontinuation
- 2002-06-11 JP JP2002204813A patent/JP4158170B2/ja not_active Expired - Fee Related
- 2002-06-11 CZ CZ2002-2035A patent/CZ304437B6/cs not_active IP Right Cessation
- 2002-06-14 SI SI200231055T patent/SI1266973T1/sl unknown
- 2002-06-14 EP EP02450137.1A patent/EP1266973B1/de not_active Expired - Lifetime
- 2002-06-14 CA CA002390766A patent/CA2390766C/en not_active Expired - Fee Related
- 2002-06-14 ES ES02450137.1T patent/ES2533772T3/es not_active Expired - Lifetime
- 2002-06-14 PT PT2450137T patent/PT1266973E/pt unknown
Also Published As
| Publication number | Publication date |
|---|---|
| SI1266973T1 (sl) | 2015-08-31 |
| CZ20022035A3 (cs) | 2003-02-12 |
| EP1266973A3 (de) | 2004-08-18 |
| CA2390766C (en) | 2007-06-12 |
| NO20022756L (no) | 2002-12-16 |
| JP4158170B2 (ja) | 2008-10-01 |
| PT1266973E (pt) | 2015-04-28 |
| EP1266973A2 (de) | 2002-12-18 |
| NO20022756D0 (no) | 2002-06-10 |
| CA2390766A1 (en) | 2002-12-15 |
| ES2533772T3 (es) | 2015-04-15 |
| AT410103B (de) | 2003-02-25 |
| JP2003119526A (ja) | 2003-04-23 |
| ATA9352001A (de) | 2002-06-15 |
| CZ304437B6 (cs) | 2014-05-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2301743B1 (de) | Verfahren und vorrichtung zum herstellen eines formkörpers durch schichtweisen aufbau | |
| EP1472026B1 (de) | Verfahren zur herstellung von metallformteilen | |
| DE102007039035B3 (de) | Verfahren zum Herstellen eines Bauteils sowie Verwendung des nach dem Verfahren hergestellten Bauteils | |
| EP2046519B1 (de) | Metallformkörper und verfahren zu dessen herstellung | |
| DE3503763C2 (de) | Maschinenteil, insbesondere für eine Werkzeugmaschine aus Polymerbeton und Verfahren zu dessen Herstellung | |
| EP1354651B1 (de) | Metallschaum enthaltender Leichtbauteil, sowie Verfahren und Vorrichtung zu dessen Herstellung | |
| AT410103B (de) | Verfahren zur herstellung eines leichtgewichtigen formkörpers und formkörper aus metallschaum | |
| DE102011120988A1 (de) | Flächiges Halbzeug aus einer Aluminiummatrixverbundlegierung mit Borcarbid-Partikeln zur Herstellung einer mit Borcarbid-Partikeln angereicherten Platte und Herstellungsverfahren | |
| DE69200219T2 (de) | Entfernbare Kerne zum Metallgiessen. | |
| DE68916515T2 (de) | Verfahren zur Herstellung von Verbundmaterial mit einer Metallmatrix mit kontrollierter Verstärkungsphase. | |
| EP3141362A1 (de) | Verfahren zur herstellung einer struktur aus mörtel oder beton und dazu geeignete anordnung | |
| DE20209294U1 (de) | Leichtgewichtiger Formkörper aus Metallschaum | |
| EP1288320B1 (de) | Vorrichtung und Verfahren zur Herstellung von Metallschaum | |
| DE102007042513A1 (de) | Verfahren zur und Formwerkzeug für die Herstellung von Bauteilen, insbesondere aus Faserverbundwerkstoffen | |
| DE102009024182B3 (de) | Verfahren zur Bildung und zum Entformen einer Form und/oder eines Kerns beim Formguss | |
| DE60212822T2 (de) | Verfahren zur herstellung einer mikrostruktur | |
| DE19703175C2 (de) | Verfahren zur Herstellung von keramischen oder pulvermetallurgischen Bauteilen mit einer schraubenförmigen Außenkontur | |
| DE102016219968A1 (de) | Verfahren zur Bestimmung einer relativen Pulverbettdichte in einer Vorrichtung zum generativen Herstellen eines dreidimensionalen Objekts | |
| DE69122339T2 (de) | Verfahren zur Herstellung eines Pulverformkörpers | |
| EP0842130B1 (de) | Verfahren zur herstellung von keramischen oder pulvermetallurgischen bauteilen mit einer schraubenförmigen aussenkontur und keramisches oder pulvermetallurgisches bauteil mit schraubenförmiger aussenkontur | |
| DE69503979T2 (de) | Zementmörtelzusammensetzung und daraus hergestellte Gegenstände | |
| DE102004013146A1 (de) | Verfahren zur Verstärkung von Kernstrukturen zur Bildung von beidseitig mit Deckschichten versehenen Kernverbunden sowie lokal verstärkter Kernverbund | |
| DE102022131971A1 (de) | Gießform zum Gießen von Metallen | |
| DE102023003731A1 (de) | Strangpressrohling und Verfahren zu dessen Herstellung sowie Verfahren zur Herstellung eines Strangpressteils | |
| DE69119392T2 (de) | Poröses Material mit einstellbarer Dichte für die Dämpfung von Stosswellen oder Schallwellen und Verfahren zu dessen Herstellung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| 17P | Request for examination filed |
Effective date: 20040925 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AXX | Extension fees paid |
Extension state: SI Payment date: 20040925 Extension state: RO Payment date: 20040925 |
|
| 17Q | First examination report despatched |
Effective date: 20091002 |
|
| APBK | Appeal reference recorded |
Free format text: ORIGINAL CODE: EPIDOSNREFNE |
|
| APBN | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2E |
|
| APBR | Date of receipt of statement of grounds of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA3E |
|
| APAF | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNE |
|
| APBT | Appeal procedure closed |
Free format text: ORIGINAL CODE: EPIDOSNNOA9E |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20141028 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: RO SI |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: ISLER AND PEDRAZZINI AG, CH |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 713978 Country of ref document: AT Kind code of ref document: T Effective date: 20150415 Ref country code: ES Ref legal event code: FG2A Ref document number: 2533772 Country of ref document: ES Kind code of ref document: T3 Effective date: 20150415 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 50216022 Country of ref document: DE Effective date: 20150416 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20150406 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20150401018 Country of ref document: GR Effective date: 20150618 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 50216022 Country of ref document: DE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| 26N | No opposition filed |
Effective date: 20151207 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150304 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20170621 Year of fee payment: 16 Ref country code: IE Payment date: 20170628 Year of fee payment: 16 Ref country code: GB Payment date: 20170620 Year of fee payment: 16 Ref country code: GR Payment date: 20170614 Year of fee payment: 16 Ref country code: FR Payment date: 20170621 Year of fee payment: 16 Ref country code: CH Payment date: 20170620 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20170620 Year of fee payment: 16 Ref country code: FI Payment date: 20170621 Year of fee payment: 16 Ref country code: PT Payment date: 20170609 Year of fee payment: 16 Ref country code: LU Payment date: 20170620 Year of fee payment: 16 Ref country code: IT Payment date: 20170622 Year of fee payment: 16 Ref country code: NL Payment date: 20170620 Year of fee payment: 16 Ref country code: BE Payment date: 20170620 Year of fee payment: 16 Ref country code: AT Payment date: 20170623 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20170608 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20170724 Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50216022 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20181214 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180615 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20180701 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 713978 Country of ref document: AT Kind code of ref document: T Effective date: 20180614 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20180614 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20180630 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180701 |
|
| REG | Reference to a national code |
Ref country code: SI Ref legal event code: KO00 Effective date: 20190218 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180630 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180630 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180630 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190107 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180630 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20190916 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180615 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180614 |