EP1321382B1 - Grossgebinde aus mehreren jeweils zu einer Rolle gewickelten, folienverpackten Dämmstoffbahnen aus Mineralwolle - Google Patents
Grossgebinde aus mehreren jeweils zu einer Rolle gewickelten, folienverpackten Dämmstoffbahnen aus Mineralwolle Download PDFInfo
- Publication number
- EP1321382B1 EP1321382B1 EP02023601A EP02023601A EP1321382B1 EP 1321382 B1 EP1321382 B1 EP 1321382B1 EP 02023601 A EP02023601 A EP 02023601A EP 02023601 A EP02023601 A EP 02023601A EP 1321382 B1 EP1321382 B1 EP 1321382B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rolls
- package
- compression
- module
- insulation material
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Revoked
Links
- 239000012774 insulation material Substances 0.000 title claims description 9
- 239000011490 mineral wool Substances 0.000 title claims description 5
- 239000004033 plastic Substances 0.000 title description 2
- 239000011810 insulating material Substances 0.000 claims abstract description 36
- 239000000835 fiber Substances 0.000 claims abstract description 20
- 238000007906 compression Methods 0.000 claims description 59
- 230000006835 compression Effects 0.000 claims description 54
- 238000000034 method Methods 0.000 claims description 15
- 239000000156 glass melt Substances 0.000 claims description 2
- 239000002985 plastic film Substances 0.000 claims 8
- 229920006255 plastic film Polymers 0.000 claims 8
- 239000011152 fibreglass Substances 0.000 claims 1
- 239000000203 mixture Substances 0.000 claims 1
- 238000009413 insulation Methods 0.000 abstract description 49
- 239000011888 foil Substances 0.000 abstract description 8
- 238000004804 winding Methods 0.000 description 14
- 238000004519 manufacturing process Methods 0.000 description 5
- 238000003860 storage Methods 0.000 description 4
- 230000008901 benefit Effects 0.000 description 3
- 238000004806 packaging method and process Methods 0.000 description 3
- 238000003466 welding Methods 0.000 description 3
- 230000015572 biosynthetic process Effects 0.000 description 2
- 229920006300 shrink film Polymers 0.000 description 2
- 239000011230 binding agent Substances 0.000 description 1
- 238000005056 compaction Methods 0.000 description 1
- 238000007796 conventional method Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 230000006735 deficit Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000011491 glass wool Substances 0.000 description 1
- 230000001771 impaired effect Effects 0.000 description 1
- 239000005022 packaging material Substances 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000009418 renovation Methods 0.000 description 1
- 238000010008 shearing Methods 0.000 description 1
- 229920006302 stretch film Polymers 0.000 description 1
- 238000012549 training Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D71/00—Bundles of articles held together by packaging elements for convenience of storage or transport, e.g. portable segregating carrier for plural receptacles such as beer cans or pop bottles; Bales of material
- B65D71/0088—Palletisable loads, i.e. loads intended to be transported by means of a fork-lift truck
- B65D71/0092—Palletisable loads, i.e. loads intended to be transported by means of a fork-lift truck provided with one or more rigid supports, at least one dimension of the supports corresponding to a dimension of the load, e.g. skids
- B65D71/0096—Palletisable loads, i.e. loads intended to be transported by means of a fork-lift truck provided with one or more rigid supports, at least one dimension of the supports corresponding to a dimension of the load, e.g. skids the dimensions of the supports corresponding to the periphery of the load, e.g. pallets
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B27/00—Bundling particular articles presenting special problems using string, wire, or narrow tape or band; Baling fibrous material, e.g. peat, not otherwise provided for
- B65B27/12—Baling or bundling compressible fibrous material, e.g. peat
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B63/00—Auxiliary devices, not otherwise provided for, for operating on articles or materials to be packaged
- B65B63/02—Auxiliary devices, not otherwise provided for, for operating on articles or materials to be packaged for compressing or compacting articles or materials prior to wrapping or insertion in containers or receptacles
- B65B63/026—Auxiliary devices, not otherwise provided for, for operating on articles or materials to be packaged for compressing or compacting articles or materials prior to wrapping or insertion in containers or receptacles for compressing by feeding articles through a narrowing space
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D85/00—Containers, packaging elements or packages, specially adapted for particular articles or materials
- B65D85/07—Containers, packaging elements or packages, specially adapted for particular articles or materials for compressible or flexible articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2571/00—Bundles of articles held together by packaging elements for convenience of storage or transport, e.g. portable segregating carrier for plural receptacles such as beer cans, pop bottles; Bales of material
- B65D2571/00006—Palletisable loads, i.e. loads intended to be transported by means of a fork-lift truck
- B65D2571/00012—Bundles surrounded by a film
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D85/00—Containers, packaging elements or packages, specially adapted for particular articles or materials
- B65D85/30—Containers, packaging elements or packages, specially adapted for particular articles or materials for articles particularly sensitive to damage by shock or pressure
- B65D85/46—Containers, packaging elements or packages, specially adapted for particular articles or materials for articles particularly sensitive to damage by shock or pressure for bricks, tiles or building blocks
Definitions
- the invention relates to a bulk container according to the preamble of claim 1 and a method for producing such a large package.
- Mineral wool insulation sheets are used in a variety of ways for thermal insulation purposes.
- a main field of application is the insulation of roofs, in particular the insulation of pitched roofs.
- the insulating material webs are fixed between the rafters, which are usually used for both the thermal insulation of new buildings as well as for the thermal insulation of old buildings in the course of renovations so-called Klemmfilze.
- Klemmfilzen is insulating material webs, which are provided transversely to the longitudinal direction of the insulating material web with markings, so that according to the distance of the rafters to be introduced between the insulating material, a corresponding section of an insulation web using the transverse markers cut as cutting guides and then it is inserted with a press fit between the rafters.
- Such Klemmfilze are known from DE 36 12 875 C 3.
- the insulating material is wound here in each case to form a roll.
- markings separating cuts are made, whereby in each case a section is separated from the insulation web whose length corresponds to the distance of the rafters.
- the severed section is rotated 90 ° and then laid between the rafters, where it is then held with a press fit.
- Such pinch felts have an increased binder content in the range of 6 to 7 wt .-% and are characterized by a higher rigidity .
- the insulation webs for the clamping felt are usually kept in a width range of 1000 to 1250 mm, preferably 1200 mm, and may have thicknesses in the range of 60 to 240 mm and more.
- This insulating material webs are wound for transport and storage to insulation rolls and it is obvious that such insulation rolls with the aforementioned dimensions require a considerable amount of space.
- large packages For transport and storage, more and more so-called large packages have been established here, which are formed from a number of insulation rolls packed in a film envelope.
- Such bulk containers are mainly composed of 18 Dämmstoffrollen which are arranged standing and packed in two layers of nine insulation rolls for bulk packaging.
- each layer of the large package three rows of juxtaposed modules, each consisting of three insulation rolls, are used, with the insulation rolls, which are each packaged under compression in a film envelope, also undergoing compression within the module.
- the bulk of two layers of insulating material rolls arranged one above the other is also packed in a film wrapping, often including the range on which the lower layer of insulation rolls of large containers is included in the film packaging.
- Corresponding large containers are known (cf., DE 40 05 541 A1) in which, in order to save packaging material, a number of plates or rolls are layered above or next to one another and the stack formed thereby is subjected to a compression process and wrapped with a film.
- the foil-wrapped modules of plates or rolls are stacked in layers, side by side, to form a transport unit, re-compressed and edged to maintain the compression of the transport unit.
- the object of the invention is the necessary for transport and storage of such large containers To reduce space requirements, considering the required quantities Insulating material leads to very significant cost advantages. Here is this task be accomplished by simple measures without the suitability of the insulating material webs is lost or impaired for thermal insulation.
- a large package which consists of several each consists of a roll wound, foil-wrapped insulation webs, in two layers one above the other and in any position in several parallel rows of several to einnem Module summarized roles are arranged, both the role as well as that Module compressed so gentle on the fiber that at a height of the large package between 2.30 m and 2.50 m, in particular 2.40 m, and a thickness of the insulating material in the area from 60 to 240 mm the ratio of insulating surface to standing surface of the large container is equal to 50: 1 to 115: 1.
- the fiber-sparing compression is composed of two compression processes.
- the first compression process takes place before the actual winding of the insulating material web.
- the insulating material web is expediently guided through a tapered gap between a precompression belt and a lower belt, the actual transport belt, where a gentler compression, in which no harmful shearing forces occur, in particular in the range from 1: 3 to 1: 6.
- a practicable preferred precompression value is in the range of 1: 3.5 to 1: 5.5.
- Vorkomprim ist is very important because here, unlike compression during the winding process in consequence of the implementation of the insulating material by a gradually tapering gap between Vorkomprim michmaschinesband and lower conveyor belt a very gentle compression or compression takes place, the high compression levels without damaging impairment of the fiber structure allows, so that a sufficient residue capacity of the fibers is ensured.
- the Vorkomprimierband expediently has an inclination between 5 ° and 10 ° and in particular 8 °.
- the shear forces which can not be completely suppressed are negligible with respect to the shear forces which occur during compression of the insulating material during the conventional winding process.
- fibers of increased quality are used to form the large package used by the fibers using known spin baskets or centrifuges with a lower hole throughput per hole compared to conventional practices or opening of the centrifuge or the spin basket are thrown or pressed.
- Preferred perforation capacities here are 0.7 to 1.1 kg glass melt / hole and day, preferably 0.9 kg / hole and day.
- the invention is applicable to insulation webs with a density in the range of 10-22 kg / m 3 , in particular 12-15 kg / m 3 , in currently practiced embodiments, very good results at a Rohêtwert of 13, 5 and 14 kg / m 3 for mineral wool have shown. Even with increased compression no damage to the fiber structure was observed and there was a perfect return spring insulation webs to the original initial thickness after opening the large package and indeed after long residence times of the mineral wool within the package.
- the compression within the module is made up of several insulating rolls 28 to 32%, preferably about 30%.
- thermal conductivity class 035 is a ratio from insulating surface to standing surface of about 112: 1 preferred.
- a thickness of the insulation sheet of 120 mm and a thermal conductivity class 035 preferably results in the ratio of insulating surface to floor space with about 96: 1.
- the preferred ratio of insulation area to floor space is about 80: 1 or 100: 1.
- a thickness of the insulating material of 160 mm and a thermal conductivity class 035 or 040 is the preferred ratio of insulating surface to floor space about 70: 1 or 89: 1.
- a thickness of the insulation sheet of 180 mm and a thermal conductivity class 035 or 040 is preferably the ratio insulating surface to floor space about 64: 1 or 80: 1.
- the ratio of insulation surface to surface area is approximately 56: 1 or 70: 1.
- a thickness of the insulation web of 220 mm and a thermal conductivity class 035 or 040 is preferably the ratio of insulating surface to floor space about 66: 1.
- the measures according to the invention result in considerable cost advantages by a correspondingly large reduction in space requirements and by simple Measures with the conventional methods for the production of large containers can be executed.
- the large container conventional design of 18 roles result in the same Transport volume considerably larger amounts of thermal insulation material, which processes can be.
- the large container from 24 rolls at a thickness of insulation rolls of 400 mm for use on standard pallets a size of 1200 x 1200 mm, since on the pallet three modules each consisting of four insulating rolls can be accommodated flush. In two layers, this results in a Large container with 24 insulating rolls.
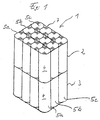
- FIG. 1 shows a bulk container for transporting and storing a plurality of insulating material rolls, in which a total of 24 insulating rolls are packed into a large package.
- the general 1 denoted large package is in this case of two superimposed layers 2 and 3, wherein in each layer 2.3 each 12 Dämmstoffrollen are packed.
- the designated 4 Dämmstoffrollen are arranged standing in any position and each layer 2,3 is made formed three adjacent modules 5a to 5c, wherein in each module four Dämmstoffrollen are arranged in a straight line.
- the combined into a module and arranged in a straight line next to each other Dämmstoffrollen are, as clearly apparent from Figure 5, by a film wrapping 6 packed to module 5.
- the film wrapping 6 covers in the embodiment according to Figure 5, the exposed lateral surface of the Dämmstoffrollen 4, but leaves the end faces the insulation rolls free. If necessary, but also a closed film wrapping be used.
- the film envelope 6 according to FIG. 5 is only schematic here represented, because in practice, it is desirable that the film wrapping in use a shrink film also extends over part of the end face, so that the film wrapping 6 slightly longer than the designated in Figure 5 with 1 length of Dämmstoffrollen. 4 is and thus protrudes on both sides over the successively arranged Dämmstoffrollen, so that during the shrinking process, the protruding portions of the film are slightly Pull over the front sides of the insulation rolls.
- the film cover 7 can also over the pallet, not shown in Figure 1 may be drawn, so that the pallet in the package of the large package is involved.
- the height of the large container from two layers of insulating rubber rolls arranged one above the other is preferably between 2.30 m and 2.50 m, measured without pallet, what a width of the insulation web or a height of each insulation roll from 1.15 m to 1.25 m.
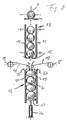
- the insulating material web 9 conveyed up on a lower belt 8 is subjected to a first compression in front of the winding device, specifically in that the insulating material web 9 is guided between the narrowing gap between an upper pre-compression belt 10 and the lower belt 8.
- the insulation web 9 brought up in a thickness of d is compressed to a reduced thickness d 'and then in this condition; as can be seen from Figure 2, wound, with 11, the so-called Ausd Wegwalze and with 12 of the winding arm 12 formed by a conveyor belt is designated.
- there is a substantial pre-compression of the insulating material web before the actual winding process which is advantageously slippery and therefore gentle on the fibers.
- the wrapping arm 12 which rests from above on the insulating roll formed in the winding device, it is ensured that the winding process takes place under the compression generated by the Vorkomprimierband, so the compression is maintained in the winding.
- the insulation roll formed in the winding device is then packaged in a conventional manner in a shrink film, so that the compression is maintained.
- the degree of compression when pre-compressing the insulating material web over the Vorkomprimierband 10 is in the range of 1: 3.5 to 1: 5.5, in particular in the range of 4.5 to 5.4, wherein in a practical embodiment, starting from a bulk density of the insulating material ago Introduced into the gap between Vorkomprimierband 10 and Subband 8 of 14 kg / m 3, a compression of the insulating tape to a density of 76 kg / m 3 takes place. This results in a compression of 1: 5.4, wherein in practice a maximum degree of compression can be driven to about 6, so the insulating material can be vorkomprimiert to one sixth in thickness.
- the following table shows compression values of practicable embodiments of insulation webs of the thermal conductivity group WLG 040 and WLG 035.
- FIG. 3 shows a conventional stacking device for forming a module, wherein the vertically arranged stacking device 13 from above the wrapped in a foil insulation rolls 4 are supplied.
- the stacking device 13 two at a distance mutually arranged walls 14, which between them a gap for receiving a Series of four successively arranged Dämmstoffrollen limited.
- the in the stacking device 13 received between the opposite walls 14 four Dämmstoffrollen 4 are held by a holding device 15.
- Under the holding device 15 is a sheath means 16, which in turn similar to the stacking device 13 from opposite arranged walls 17 is formed. Above the sheath device 16 two films 18 are fed from two opposite sides of the reels 19 be handled.
- These films 18 are represented by a turn only schematically Welding device 20 together before entering the gap between the walls 17 welded into a foil. If the holding device 15 is opened, the four arrive in the stacking device 13 superposed Dämmstoffrollen 4 under entrainment the welded film of the two films 18 between the walls 17 and lie on the punch 21 of a hydraulic piston cylinder 22. After the four insulation rolls are inserted between the walls 17, there is a pressing of the row of four superimposed insulating rolls 4 by raising the punch 21, wherein above the two walls 17 through the rollers of the welding device 20 a stop is formed, so that compressing the four insulating rolls in the module longitudinal direction takes place.
- the four insulating rolls are arranged under compression in the module longitudinal direction, wherein the foils 18 are reinforced, d. H. with a thickness between 40 and 100 ⁇ m, preferably 70 ⁇ m
- the insulating rolls become rolls with a Diameter of 400 mm wound, which means that the length a of the series of four successively arranged Dämmstoffrollen 4 before the formation of the module is 1600 mm.
- the compression of the module takes place in MödullCodescardi to a length a of 1200 mm, making three modules flush with four insulating rolls fit on a standard pallet measuring 1200 x 1200 mm.
- the fibers are made of particular quality.
- the spin basket here has a diameter from 400 to 600 mm.
- the spin basket also has a hole number of 27,000. This data of the spin basket are however changeable and serve only as an example. Essential is the hole performance, the is reduced compared to conventional manufacturing process. This results in glass wool fibers with a mean fiber diameter of 3 to 4, in particular 3.5 microns.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Packages (AREA)
- Basic Packing Technique (AREA)
- Packaging Of Annular Or Rod-Shaped Articles, Wearing Apparel, Cassettes, Or The Like (AREA)
- Laminated Bodies (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10152385A DE10152385B4 (de) | 2001-10-24 | 2001-10-24 | Großgebinde aus mehreren jeweils zu einer Rolle gewickelten, folienverpackten Dämmstoffbahnen aus Mineralwolle, insbesondere Glaswolle |
| DE10152385 | 2001-10-24 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1321382A1 EP1321382A1 (de) | 2003-06-25 |
| EP1321382B1 true EP1321382B1 (de) | 2005-06-29 |
Family
ID=7703516
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02023601A Revoked EP1321382B1 (de) | 2001-10-24 | 2002-10-17 | Grossgebinde aus mehreren jeweils zu einer Rolle gewickelten, folienverpackten Dämmstoffbahnen aus Mineralwolle |
Country Status (6)
| Country | Link |
|---|---|
| EP (1) | EP1321382B1 (da) |
| AT (1) | ATE298713T1 (da) |
| DE (3) | DE10152385B4 (da) |
| DK (1) | DK1321382T3 (da) |
| ES (1) | ES2244713T3 (da) |
| PT (1) | PT1321382E (da) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102009035104A1 (de) * | 2009-07-29 | 2011-02-03 | Saint-Gobain Isover G+H Ag | Dämmstoffbahn aus Mineralwolle sowie Großgebinde aus derartigen zu Rollen gewickelten Dämmstoffbahnen |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1777170A1 (en) * | 2005-10-18 | 2007-04-25 | Knauf Insulation SA | Assembly of stacked rolls or slabs of compressible insulation material |
| PL2206656T3 (pl) | 2009-01-13 | 2011-05-31 | Ursa Insulation Sa | Paczka dla produktów w postaci wełny mineralnej, moduły dla utworzenia takiej paczki i sposób wytwarzania takiej paczki |
| DE202009006441U1 (de) * | 2009-05-02 | 2009-07-09 | Nies, Klaus-Dieter | Verpackungseinheit eines Dämmstoffproduktes |
| GB201412350D0 (en) | 2014-07-11 | 2014-08-27 | Knauf Insulation | Insulating package |
| FR3055322B1 (fr) * | 2016-08-30 | 2021-06-18 | Saint Gobain Isover | Module comprenant des produits isolants et procede de fabrication d'un tel module |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3546846A (en) * | 1965-12-29 | 1970-12-15 | Owens Corning Fiberglass Corp | Method and apparatus for packaging fibrous material |
| US4018337A (en) * | 1973-10-23 | 1977-04-19 | Cadillac Products, Inc. | Heat shrink packaging |
| CA1080110A (en) * | 1975-06-09 | 1980-06-24 | Lawrence R. Finn | Method and apparatus for packaging compressible fibrous batts and package of same |
| SE395529C (sv) * | 1975-11-18 | 1985-09-30 | Eskadern Ab | Forfarande for forbehandling, forpackning och efterbehandling av en ljud- eller vermeisolerande produkt av oorganiska fibrer |
| FR2460862A1 (fr) * | 1979-07-09 | 1981-01-30 | Saint Gobain | Fardeau de rouleaux de materiaux compressibles |
| US4602471A (en) * | 1985-05-28 | 1986-07-29 | Owens-Corning Fiberglas Corporation | Roll-up method and apparatus for mineral fiber pack |
| FR2587682B1 (fr) * | 1985-09-25 | 1987-12-18 | Saint Gobain Isover | Constitution de fardeaux d'isolants thermiques fibreux |
| DE4005541A1 (de) * | 1990-02-22 | 1991-08-29 | Rockwool Int | Verfahren und vorrichtung zum komprimieren und verpacken von platten oder rollen aus mineralwolle |
| FR2685904A1 (fr) * | 1992-01-07 | 1993-07-09 | Saint Gobain Isover | Rouleau de matelas fibreux comprime, methode et dispositif pour l'obtenir. |
| US5350063A (en) * | 1993-07-13 | 1994-09-27 | Owens-Corning Fiberglas Technology Inc. | Cartwheelable shipping package for insulation |
| EP0908400A1 (en) * | 1997-10-13 | 1999-04-14 | Rockwool International A/S | Packaged mineral wool products |
| DE10026269B4 (de) * | 2000-05-26 | 2013-04-18 | Saint-Gobain Isover G+H Ag | Großgebinde für Transport und Lagerung von Dämmstoffrollen und dergleichen Produkte |
| DE10100640A1 (de) * | 2001-01-09 | 2002-07-11 | Saint Gobain Isover G & H Ag | Dämmstoffelement aus Mineralwolle, insbesondere zu einer Dämmstoffrolle wickelbare Dämmstoffbahn |
-
2001
- 2001-10-24 DE DE10152385A patent/DE10152385B4/de not_active Revoked
-
2002
- 2002-10-17 DE DE20221898U patent/DE20221898U1/de not_active Expired - Lifetime
- 2002-10-17 ES ES02023601T patent/ES2244713T3/es not_active Expired - Lifetime
- 2002-10-17 AT AT02023601T patent/ATE298713T1/de active
- 2002-10-17 DK DK02023601T patent/DK1321382T3/da active
- 2002-10-17 EP EP02023601A patent/EP1321382B1/de not_active Revoked
- 2002-10-17 DE DE50203491T patent/DE50203491D1/de not_active Revoked
- 2002-10-17 PT PT02023601T patent/PT1321382E/pt unknown
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102009035104A1 (de) * | 2009-07-29 | 2011-02-03 | Saint-Gobain Isover G+H Ag | Dämmstoffbahn aus Mineralwolle sowie Großgebinde aus derartigen zu Rollen gewickelten Dämmstoffbahnen |
| DE102009035104B4 (de) | 2009-07-29 | 2020-06-25 | Saint-Gobain Isover G+H Ag | Dämmstoffbahn aus Mineralwolle sowie Großgebinde aus derartigen zu Rollen gewickelten Dämmstoffbahnen |
Also Published As
| Publication number | Publication date |
|---|---|
| ES2244713T3 (es) | 2005-12-16 |
| DE20221898U1 (de) | 2008-11-27 |
| ATE298713T1 (de) | 2005-07-15 |
| DE10152385A1 (de) | 2003-05-08 |
| DK1321382T3 (da) | 2005-10-10 |
| PT1321382E (pt) | 2005-11-30 |
| DE10152385B4 (de) | 2012-11-22 |
| EP1321382A1 (de) | 2003-06-25 |
| DE50203491D1 (de) | 2005-08-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE602004002303T2 (de) | Rollenpackungen und ihr herstellungsverfahren | |
| DE3789113T2 (de) | Packung mit einer banderolenartigen hülle sowie verfahren und anordnung zum herstellen einer derartigen packung. | |
| EP0544704B2 (de) | Vorrichtung zum umhüllen einer verpackungseinheit | |
| EP3431399B1 (de) | Vorrichtung und verfahren zum verpacken gestapelter länglicher gegenstände sowie verwendung einer derartigen vorrichtung | |
| EP0347729B1 (de) | Verfahren und Vorrichtung zur Herstellung eines endlosen Wabenbandes | |
| DE10152385B4 (de) | Großgebinde aus mehreren jeweils zu einer Rolle gewickelten, folienverpackten Dämmstoffbahnen aus Mineralwolle, insbesondere Glaswolle | |
| EP3757046B1 (de) | Vorrichtung und verfahren zum verbinden von zwei jeweils von einer bobine ablaufenden materialbahnen | |
| DE10026269B4 (de) | Großgebinde für Transport und Lagerung von Dämmstoffrollen und dergleichen Produkte | |
| DE7920480U1 (de) | Halbzeug aus mineralfasern | |
| CH688890A5 (de) | Verfahren zum Herstellen von Palettenstuetzen. | |
| DE3444897A1 (de) | Mineralwollegebinde und verfahren zu dessen herstellung | |
| EP1017597A1 (de) | Verpackungssystem für stückgut | |
| DE10146921B4 (de) | Gebinde aus Dämmstoffpaketen sowie dessen Verwendung | |
| DE4005541A1 (de) | Verfahren und vorrichtung zum komprimieren und verpacken von platten oder rollen aus mineralwolle | |
| DE10111829A1 (de) | Vorrichtung und Verfahren zum Pressen von mindestens einem Fasermaterialkörper, Presskörper, Pressplatte | |
| DE29608864U1 (de) | Transporteinheit, bestehend aus einer Anzahl Mineralwolleplatten | |
| WO2021032560A1 (de) | Verwendung einer verpackungseinheit für umreifungsbänder | |
| EP2424790B1 (de) | Verpackungseinheit eines dämmstoffproduktes | |
| DE69206506T3 (de) | Verfahren zur Herstellung einer Ladung von Rollen aus zusammendrückbarem Material. | |
| EP1447350A1 (de) | Palettiersystem | |
| WO2012031699A1 (de) | Verpackungseinheit sowie verfahren und verpackungsvorrichtung zum herstellen von verpackungseinheiten | |
| DE102005055803B4 (de) | Vorrichtung zum Entfernen eines Sicherungselements | |
| WO2008009456A1 (de) | Verfahren und vorrichtung zur herstellung eines gebindes aus einer mehrzahl von einzelpaketen sowie derartiges gebinde | |
| DE1004992B (de) | Verfahren und Einrichtung zum Buendeln und Verpacken streifenfoermiger Wellpappe-Zuschnitte | |
| DE202015104606U1 (de) | Paket aus Mehrschichtisolierstoff und Einrichtung zurHerstellung eines solchen Pakets |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20030403 |
|
| AK | Designated contracting states |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR IE IT LI LU MC NL PT SE SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| 17Q | First examination report despatched |
Effective date: 20040123 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR IE IT LI LU MC NL PT SE SK TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RTI1 | Title (correction) |
Free format text: PACKAGE COMPRISING A PLURALITY OF PLASTIC WRAPPED ROLLS OF MINERAL WOOL INSULATION MATERIAL |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR IE IT LI LU MC NL PT SE SK TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050629 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 50203491 Country of ref document: DE Date of ref document: 20050804 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050929 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20051017 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20050922 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20051031 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: URS WEGMANN DIPL.-ING. |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2244713 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| ET | Fr: translation filed | ||
| 26 | Opposition filed |
Opponent name: KNAUF INSULATION SA Effective date: 20060318 |
|
| 26 | Opposition filed |
Opponent name: ROCKWOOL INTERNATIONAL A/S Effective date: 20060327 Opponent name: KNAUF INSULATION SA Effective date: 20060318 Opponent name: URSA INTERNARIONAL GMBH Effective date: 20060329 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| NLR1 | Nl: opposition has been filed with the epo |
Opponent name: ROCKWOOL INTERNATIONAL A/S Opponent name: URSA INTERNARIONAL GMBH Opponent name: KNAUF INSULATION SA |
|
| PLAF | Information modified related to communication of a notice of opposition and request to file observations + time limit |
Free format text: ORIGINAL CODE: EPIDOSCOBS2 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| RDAF | Communication despatched that patent is revoked |
Free format text: ORIGINAL CODE: EPIDOSNREV1 |
|
| APBP | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2O |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |
|
| APBQ | Date of receipt of statement of grounds of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA3O |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: URSA INTERNARIONAL GMBH Effective date: 20060329 Opponent name: ROCKWOOL INTERNATIONAL A/S Effective date: 20060327 Opponent name: KNAUF INSULATION SA Effective date: 20060318 |
|
| NLR1 | Nl: opposition has been filed with the epo |
Opponent name: ROCKWOOL INTERNATIONAL A/S Opponent name: URSA INTERNARIONAL GMBH Opponent name: KNAUF INSULATION SA |
|
| APBU | Appeal procedure closed |
Free format text: ORIGINAL CODE: EPIDOSNNOA9O |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20090921 Year of fee payment: 8 Ref country code: PT Payment date: 20090925 Year of fee payment: 8 Ref country code: SK Payment date: 20090921 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20091026 Year of fee payment: 8 Ref country code: CH Payment date: 20091027 Year of fee payment: 8 Ref country code: DE Payment date: 20091029 Year of fee payment: 8 Ref country code: DK Payment date: 20091026 Year of fee payment: 8 Ref country code: ES Payment date: 20091015 Year of fee payment: 8 Ref country code: FI Payment date: 20091027 Year of fee payment: 8 Ref country code: IE Payment date: 20091028 Year of fee payment: 8 Ref country code: LU Payment date: 20091026 Year of fee payment: 8 Ref country code: SE Payment date: 20091027 Year of fee payment: 8 Ref country code: TR Payment date: 20091019 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20091028 Year of fee payment: 8 |
|
| RDAG | Patent revoked |
Free format text: ORIGINAL CODE: 0009271 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT REVOKED |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BG Payment date: 20091029 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MP4A Effective date: 20100415 |
|
| 27W | Patent revoked |
Effective date: 20091111 |
|
| GBPR | Gb: patent revoked under art. 102 of the ep convention designating the uk as contracting state |
Effective date: 20091111 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF THE APPLICANT RENOUNCES Effective date: 20050629 Ref country code: LI Free format text: LAPSE BECAUSE OF THE APPLICANT RENOUNCES Effective date: 20050629 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20091117 Year of fee payment: 8 Ref country code: GB Payment date: 20091026 Year of fee payment: 8 Ref country code: IT Payment date: 20091023 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20091027 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: ECNC |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: MM4A Ref document number: E 236 Country of ref document: SK Effective date: 20101017 |