EP1331047A2 - Machine automatique pour le pliage de panneaux - Google Patents
Machine automatique pour le pliage de panneaux Download PDFInfo
- Publication number
- EP1331047A2 EP1331047A2 EP03290220A EP03290220A EP1331047A2 EP 1331047 A2 EP1331047 A2 EP 1331047A2 EP 03290220 A EP03290220 A EP 03290220A EP 03290220 A EP03290220 A EP 03290220A EP 1331047 A2 EP1331047 A2 EP 1331047A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- sheets
- automatic
- blade holder
- carriage
- holder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D5/00—Bending sheet metal along straight lines, e.g. to form simple curves
- B21D5/006—Bending sheet metal along straight lines, e.g. to form simple curves combined with measuring of bends
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D5/00—Bending sheet metal along straight lines, e.g. to form simple curves
- B21D5/04—Bending sheet metal along straight lines, e.g. to form simple curves on brakes making use of clamping means on one side of the work
- B21D5/045—With a wiping movement of the bending blade
Definitions
- the present invention relates to a machine intended for the formation of sheet metal panels and, more particularly, to carry out the necessary folds to the application plates using means which effectively make the work of this function.
- machines that realize automatically bending sheets, at angles predetermined, said machines comprising a punch and a matrix, between which the forming of sheets by folding, this operation being carried out by progressive folding, to compensate for the capacity of recovery of folded sheets which varies depending on various factors, such as the nature of the material, the size, etc.
- Folding precision also requires exact control of the angle obtained and, for this purpose, uses measurement systems associated with the folding, consisting of a laser measuring instrument, in complex devices integrated into the folding punch or in independent portable devices, the systems in question proving complicated and expensive.
- the subject of the present invention is a machine which includes means for folding and a device for measuring the angle of the folded sheet, different in their design of known systems and offering certain advantages for the practical function of the folding of the application sheets.
- the machine which is the subject of the present invention includes a folding mechanism consisting of a blade holder mobile located in front of a holding device and immobilization of the sheets to be folded, the device immobilizer comprising a fixed lower part or counter blade and an actuated upper sheet clamp vertically using a push cylinder, while the blade holder is fitted with a probe arranged on a cylinder displacement which leads it towards the device sheet immobilization.
- the blade holder is incorporated in a device for translation which ensures its movement towards the device sheet immobilization and an articulated device tilting which allows to vertically vary its position relative to the immobilizer sheets, the two movements being provided by the two drive cylinders.
- the sheet clamps of the device for immobilizing sheets is arranged on a carriage driven by the cylinder pusher, the blank holder in question consisting of a assembly formed by two end blocks and a block central which determine a continuous longitudinal shape, the central block can be replaced to modulate the longitudinal dimension of the assembly as a function of the width of the application sheets.
- the blade holder includes a cart capable of automatically transport the central block of the blank holder from the mounting position to a magazine containing several blocks of different lengths, to allow selective replacement of the block in question in the longitudinal adaptation of the blank holder, the carriage replacement being driven by an independent cylinder or associated with that of the probe also incorporated in the blade holder.
- a functional group is thus obtained which makes it possible to quickly and precisely bend sheets at predetermined angles, controlling with automatic measurement of the folding angle for determine the corrections necessary for the operation.
- the functional assembly can be adapted to sheets of different widths, thanks to the change automatic selection of the length of the blank holder of immobilization, which makes it possible to obtain a large speed in the operational operating arrangement compared to the application sheets.
- the machine subject to present invention actually has features very advantageous, by acquiring a clean life and a reference character for the function to which it is intended.
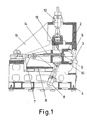
- Figure 1 shows a sectioned side view of the panel maker recommended.
- FIG. 2 is a sectioned view of the machine, in upper shot.
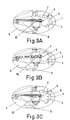
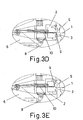
- Figures 3A to 3E show a sequence of successive positions of the bending operation of a sheet and control of the folding angle.
- the subject of the invention is a paneling machine intended for automatically bend sheets (1), according to the folds necessary for the formation of door panels, partitions or similar applications.
- the machine has a folding mechanism which comprises a blade holder (2) arranged, in mobile mounting, facing a sheet immobilization device (1) at to fold.
- the immobilizer comprises a part lower (3) or counter blade fixed on the structural frame (4) of the machine and an upper hold-down (5) likely to be driven vertically against the lower part (3) mentioned above in order to immobilize between one and the other part the application sheets (1) to be able to perform the folding operations.
- the blade holder (2) is arranged in articulation of vertical tilting on carrier trolleys (6) mounted on slides that lead them to the device sheet immobilization (1).
- the carriages (6) are joined to the respective cylinders (7) which allow them to move forward and backward while the blade holder (2) is joined to one or more cylinders (8) which ensure the vertical tilting of the blade holder (2) in relation to the articulation provided on the carriages carriers (6).
- the blade holder (2) is equipped with a probe (9) arranged on a jack (10) which leads it to the part front where the immobilizer of the sheets (1).
- the sheet (1) to be folded is retained using the immobilization device between the blank holder (5) and the fixed part (3), as illustrated in FIG. 3A, of so that when the sheet ends up in this position, the movement of the blade holder (2) driven by the jacks (7 and 8) cause the end of the the sheet (1) immobilized, as shown in the figure 3B.
- the blade holder is automatically driven by the cylinders (7 and 8) depending on the programmed folding angle in the control of the machine, the bending of the sheet performed during a first operation according to the angle programmed, without exceeding this angle, after which the blade holder (2) returns to the starting position, as as illustrated in Figure 3C.
- the cylinder (10) then drives the probe (9) and the leads to the bending zone of the sheet (1), as as illustrated in Figure 3D; then, by tilting blade holder (2) required, the probe (9) is set to contact of the extreme zone of the folded part of the sheet (1), as shown in Figure 3E.
- the blank holder (5) is arranged on a carriage (11) articulated on the structural frame (4) of the machine, the carriage (11) in question being driven in tilting by the jack (12), this same jack exerts pressure against the sheets (1) to immobilize them by bringing the blank holder (5) against the fixed lower part (3).
- the blank holder (5) consists of two blocks end and a central block which determine the length of the body of the blank holder (5), the central block can be replaced by blocks of different lengths, which allows you to adjust the length of the whole blank holder (5) depending on the width application sheets (1) so that the operation of the machine is as precise as possible in each case.
- the blade holder (2) is equipped with a carriage (13) which automatically replaces the central block of the blank holder (5) depending on the width sheets (1) to be folded with the machine in each case, so that the carriage (13) moves and grips pass the central block of the blank holder (5) for the lead to a store (not shown) containing several similar blocks, of different lengths, where the carriage (13) in question takes the appropriate length block, then take it to the blank holder (5) and place it in the center of it.
- the carriage (13) is driven by a jack (14) controlled by the machine control, said cylinder (14) can be an independent cylinder, used only for move the carriage (13); but we also planned the possibility of using the jack (10) for this function of the probe (9), in which case the carriage (13) would be associated said cylinder (10) relative to the corresponding control to perform this central block change function blank holder (5).
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Measurement Of The Respiration, Hearing Ability, Form, And Blood Characteristics Of Living Organisms (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
- Investigating Strength Of Materials By Application Of Mechanical Stress (AREA)
Abstract
Description
- Pliage correct depuis la première opération.
- Economie de temps à la mise au point, lors de la reconfiguration durant la production et lors des corrections du pliage.
- Augmentation de la précision d'obtention de l'angle de pliage.
- Permet d'éviter des pertes inutiles de matériaux suite à des erreurs dans l'angle de pliage.
- Permet de travailler avec des matériaux possédant n'importe quel type de caractéristiques d'épaisseur, dureté, sens de laminage, etc.. et donc d'éviter des déchets de matériaux possédant ce type de caractéristiques en dehors de la marge standard.
- La plieuse se caractérise par une grande flexibilité du processus de production en ce sens qu'elle permet de réaliser des pliages sans avoir à manipuler ou à reconfigurer le machine ou le capteur de contrôle de l'angle de pliage.
Claims (6)
- Panneauteuse automatique destinée à former des pliages d'angles déterminés sur des tôles (1) d'application, caractérisée en ce qu'elle comprend un mécanisme de pliage composé d'un porte-lames (2) disposé en face d'un dispositif d'immobilisation des tôles (1) à plier, le porte-lames (2) étant incorporé à un dispositif de translation qui assure son déplacement vers le dispositif d'immobilisation des tôles (1) et à un dispositif articulé de basculement qui lui permettent de réaliser le pliage des tôles (1), tandis que le porte-lames (2) est équipé d'un palpeur (9) disposé sur un vérin (10) destiné à l'amener au contact des tôles (1) pliées, pour mesurer l'angle du pliage.
- Panneauteuse automatique, en tout conforme à la première revendication, caractérisée en ce que le dispositif d'immobilisation des tôles (1) comprend une partie inférieure fixe (3) et un serre-flans supérieur (5) qui se déplace verticalement contre la partie inférieure fixe (3) de telle sorte que les tôles (1) à plier soient immobilisées entre les deux.
- Panneauteuse automatique, en tout conforme à la première et deuxième revendications, caractérisée en ce que le serre-flans (5) se compose de deux blocs d'extrémité et d'un bloc central, le bloc central pouvant être remplacé par des blocs de différentes longueurs pour ajuster la dimension longitudinale du serre-flans (5) en fonction de la largeur des tôles (1) d'application.
- Panneauteuse automatique, en tout conforme aux trois revendications précédentes, caractérisée en ce que le porte-lames (2) est équipé d'un chariot (13) qui permet de remplacer automatiquement le bloc central du serre-flans (5), ledit chariot conduisant le bloc à changer jusqu'à un magasin de logement et ramenant du même magasin un autre bloc de longueur appropriée pour l'incorporer au serre-flans (5).
- Panneauteuse automatique, en tout conforme aux quatre revendications précédentes, caractérisée en ce que le chariot (13) de changement du bloc central du serre-flans (5) est associé à un vérin d'entraínement (14) indépendant ou associé au propre vérin (10) du palpeur (9) pour que le vérin(10) entraíne également le chariot (13) susmentionné.
- Panneauteuse automatique, en tout conforme à la première revendication, caractérisée en ce que le porte-lames (2) est articulé sur un chariot (6) entraíné par un vérin(7), le porte-lames (2) étant, par ailleurs, uni à un second vérin (8) qui le fait basculer.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ES200200193A ES2209594B1 (es) | 2002-01-29 | 2002-01-29 | Maquina paneladora automatica. |
| ES200200193 | 2002-01-29 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1331047A2 true EP1331047A2 (fr) | 2003-07-30 |
| EP1331047A3 EP1331047A3 (fr) | 2004-10-13 |
| EP1331047B1 EP1331047B1 (fr) | 2008-06-18 |
Family
ID=8500311
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP03290220A Expired - Lifetime EP1331047B1 (fr) | 2002-01-29 | 2003-01-29 | Machine automatique pour le pliage de panneaux |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1331047B1 (fr) |
| DE (1) | DE60321610D1 (fr) |
| ES (1) | ES2209594B1 (fr) |
| PT (1) | PT1331047E (fr) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1797973A1 (fr) * | 2005-12-16 | 2007-06-20 | CREA S.r.l. | Cintreuse et presse plieuse pour panneaux combinées |
| EP2127771A1 (fr) * | 2008-05-30 | 2009-12-02 | Goiti S. Coop. | Plieuse |
| CN108746268A (zh) * | 2018-05-29 | 2018-11-06 | 郑文豪 | 一种电力母线槽自动生产机器人 |
| CN109530626A (zh) * | 2018-12-07 | 2019-03-29 | 中国航发南方工业有限公司 | 一种涡轮叶片底座制备方法 |
| CN112207168A (zh) * | 2020-10-23 | 2021-01-12 | 南京邮电大学 | 一种折边机折边梁驱动机构 |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3216053A1 (de) * | 1982-04-29 | 1983-11-03 | Karl Mengele & Söhne Maschinenfabrik und Eisengießerei GmbH & Co, 8870 Günzburg | Optoelektronisches messverfahren und vorrichtung zur durchfuehrung des verfahrens |
| DE3441113A1 (de) * | 1984-11-10 | 1986-05-15 | Klöckner-Moeller Elektrizitäts GmbH, 5300 Bonn | Biegemaschine mit nummerischer steuerung |
| JPH0688084B2 (ja) * | 1985-04-05 | 1994-11-09 | 株式会社日立製作所 | 折曲げ装置 |
| IT1201126B (it) * | 1987-01-09 | 1989-01-27 | Salvagnini Transferica Spa | Macchina piegatrice per la produzione di pannelli in lamiera rettangolari a partire da fogli piani di lamiera |
| DE3739173A1 (de) * | 1987-11-19 | 1989-06-01 | Feintool Int Holding | Verfahren und vorrichtung zum biegen von werkstuecken |
| IT1237750B (it) * | 1989-12-29 | 1993-06-15 | Prima Ind Spa | Procedimento di piegatura di una lamiera |
| FI96008C (fi) * | 1994-02-10 | 1996-04-25 | Balaxman Oy | Menetelmä ja laitteisto taivutuskoneessa |
| IT1273326B (it) * | 1994-02-23 | 1997-07-08 | Salvagnini Italia Spa | Macchina piegatrice per fogli di lamiera |
| JP3459460B2 (ja) * | 1994-04-07 | 2003-10-20 | 株式会社アマダ | 折曲げ加工装置 |
| US5934134A (en) * | 1994-11-14 | 1999-08-10 | Amada Company, Ltd. | Bending press |
| IT1292331B1 (it) * | 1997-05-29 | 1999-01-29 | Antonio Codatto | Pressa piegatrice per l'esecuzione di pieghe a c sui bordi di un pannello di lamiera |
| NL1007290C1 (nl) * | 1997-10-16 | 1999-04-19 | Cornelis Hendricus Liet | Inrichting voor het meten van de hoek tussen twee oppervlakken van een te buigen werkstuk. |
| NZ503297A (en) * | 1999-03-22 | 2000-10-27 | Fisher & Paykel | Sheet metal folder with two consecutive bends with second movement of fold bar determined from first bend position and position at which fold bar leaves contact with sheet on retreat |
| ES2190298B1 (es) * | 2000-01-31 | 2004-10-16 | Goiti, S.Coop | Maquina plegadora de chapas metalicas. |
-
2002
- 2002-01-29 ES ES200200193A patent/ES2209594B1/es not_active Expired - Fee Related
-
2003
- 2003-01-29 PT PT03290220T patent/PT1331047E/pt unknown
- 2003-01-29 EP EP03290220A patent/EP1331047B1/fr not_active Expired - Lifetime
- 2003-01-29 DE DE60321610T patent/DE60321610D1/de not_active Expired - Lifetime
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1797973A1 (fr) * | 2005-12-16 | 2007-06-20 | CREA S.r.l. | Cintreuse et presse plieuse pour panneaux combinées |
| EP2127771A1 (fr) * | 2008-05-30 | 2009-12-02 | Goiti S. Coop. | Plieuse |
| CN108746268A (zh) * | 2018-05-29 | 2018-11-06 | 郑文豪 | 一种电力母线槽自动生产机器人 |
| CN109530626A (zh) * | 2018-12-07 | 2019-03-29 | 中国航发南方工业有限公司 | 一种涡轮叶片底座制备方法 |
| CN112207168A (zh) * | 2020-10-23 | 2021-01-12 | 南京邮电大学 | 一种折边机折边梁驱动机构 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE60321610D1 (de) | 2008-07-31 |
| EP1331047B1 (fr) | 2008-06-18 |
| ES2209594A1 (es) | 2004-06-16 |
| PT1331047E (pt) | 2008-09-30 |
| EP1331047A3 (fr) | 2004-10-13 |
| ES2209594B1 (es) | 2005-06-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| FR3001906A1 (fr) | Procede de decoupage de pieces dans une bande de matiere et machine de decoupage mettant en oeuvre ledit procede | |
| FR2733709A1 (fr) | Ameliorations concernant le calibrage du diametre de parties cylindriques excentrees de pieces a usiner | |
| EP0439975A1 (fr) | Système mécanique de guidage automatique d'une ou plusieurs torches d'une unité de soudage à l'arc | |
| FR2582974A1 (fr) | Dispositif pour effectuer un changement automatique d'outils de mesure dans un robot ou une machine de mesure | |
| WO2007012739A1 (fr) | Dispositif de coupe longitudinale d'une laize de materiau defilant en continu pour former une bande a profil longitudinal variable | |
| EP2945758A1 (fr) | Dispositif de cintrage de profilés tels que des tubes | |
| EP0892686A1 (fr) | Machine a cintrer ou a cambrer un profile, et tete de cintrage pour une telle machine | |
| WO2007122346A1 (fr) | Dispositif de cintrage de tubes ou profiles a structure symetrique pour double sens de cintrage et machine equipee du dispositif | |
| WO2010116052A1 (fr) | Machine à cintrer pour la réalisation de profilés coudés, notamment de tubes d'échangeurs | |
| FR2866255A1 (fr) | Systeme de compemsation d'usure d'electrodes | |
| EP0168331B1 (fr) | Machine pour le cintrage de tubes, barres ou profilés | |
| EP1331047B1 (fr) | Machine automatique pour le pliage de panneaux | |
| FR2988309A1 (fr) | Machine de cintrage a tete de pliage mobile autour d'un nez de pliage fixe | |
| EP2029322B1 (fr) | Procédé et machine d'usinage pour objet optique | |
| EP0055648A2 (fr) | Machine pour réaliser des pièces ayant des surfaces gauches de configuration déterminée | |
| FR2460167A1 (fr) | Procede et dispositif d'estampage et de pliage d'un materiau en bande et/ou en fil | |
| EP0281488B1 (fr) | Tête de cintrage tournante, pour machine à cintrer les tubes | |
| FR2606307A1 (fr) | Machine a tailler les engrenages par fraise-mere, pourvue de dispositif de controle des dents de la piece en cours de travail | |
| FR2947802A1 (fr) | Outil et procede de montage d'un demi-coussinet, ensemble comportant cet outil | |
| FR2538344A1 (fr) | Dispositif de comptage de billets de banque et de pose d'une bande de scellement | |
| FR2554747A1 (fr) | Outil pour le tronconnage de tubes | |
| CH677835A5 (en) | Alignment of optical fibres during parameter measurement | |
| CH624595A5 (fr) | ||
| FR2662105A1 (fr) | Procede et dispositif d'equerrage pour le cisaillage de toles. | |
| FR2575955A1 (fr) | Procede et installation pour la rectification et le controle du diametre d'une meule |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO |
|
| 17P | Request for examination filed |
Effective date: 20050412 |
|
| AKX | Designation fees paid |
Designated state(s): AT DK FR GB IT PT |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): DE DK FR GB IT PT |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| 17Q | First examination report despatched |
Effective date: 20070202 |
|
| RTI1 | Title (correction) |
Free format text: AUTOMATIC SHEET BENDING MACHINE |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE DK FR GB IT PT |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: GOITI, S.COOP |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: AIZPURUA ZENDOIA, INAKI XABIER |
|
| REF | Corresponds to: |
Ref document number: 60321610 Country of ref document: DE Date of ref document: 20080731 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20080918 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20080618 |
|
| 26N | No opposition filed |
Effective date: 20090319 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20120116 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20120118 Year of fee payment: 10 Ref country code: PT Payment date: 20120109 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120131 Year of fee payment: 10 Ref country code: GB Payment date: 20120116 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Free format text: LAPSE DUE TO NON-PAYMENT OF FEES Effective date: 20130729 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20130129 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20130930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130729 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130801 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 60321610 Country of ref document: DE Effective date: 20130801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130129 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130129 |