EP1533571B1 - Procédé de fabrication de bougies de préchauffage en céramique - Google Patents
Procédé de fabrication de bougies de préchauffage en céramique Download PDFInfo
- Publication number
- EP1533571B1 EP1533571B1 EP04023484.1A EP04023484A EP1533571B1 EP 1533571 B1 EP1533571 B1 EP 1533571B1 EP 04023484 A EP04023484 A EP 04023484A EP 1533571 B1 EP1533571 B1 EP 1533571B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- layer
- glow pin
- conductive layer
- layer structure
- pin axis
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 30
- 239000000919 ceramic Substances 0.000 title claims description 11
- 238000004519 manufacturing process Methods 0.000 claims description 8
- 238000005245 sintering Methods 0.000 claims description 8
- 238000001125 extrusion Methods 0.000 claims description 5
- 238000001746 injection moulding Methods 0.000 claims description 5
- 238000003466 welding Methods 0.000 claims description 5
- 238000007598 dipping method Methods 0.000 claims description 4
- 238000007751 thermal spraying Methods 0.000 claims description 4
- 238000003754 machining Methods 0.000 claims description 3
- 238000005520 cutting process Methods 0.000 claims description 2
- 238000004544 sputter deposition Methods 0.000 claims 1
- 238000010438 heat treatment Methods 0.000 description 7
- 238000010276 construction Methods 0.000 description 4
- 238000005507 spraying Methods 0.000 description 4
- 238000005516 engineering process Methods 0.000 description 3
- 238000002347 injection Methods 0.000 description 3
- 239000007924 injection Substances 0.000 description 3
- 239000012212 insulator Substances 0.000 description 3
- 239000004033 plastic Substances 0.000 description 3
- 229920003023 plastic Polymers 0.000 description 3
- 239000002002 slurry Substances 0.000 description 3
- 238000000137 annealing Methods 0.000 description 2
- 238000002485 combustion reaction Methods 0.000 description 2
- 238000000227 grinding Methods 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000004020 conductor Substances 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 230000007797 corrosion Effects 0.000 description 1
- 229910003460 diamond Inorganic materials 0.000 description 1
- 239000010432 diamond Substances 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 238000001035 drying Methods 0.000 description 1
- 238000005538 encapsulation Methods 0.000 description 1
- 238000007765 extrusion coating Methods 0.000 description 1
- 238000007731 hot pressing Methods 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000007650 screen-printing Methods 0.000 description 1
- 239000011343 solid material Substances 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B3/00—Producing shaped articles from the material by using presses; Presses specially adapted therefor
- B28B3/20—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein the material is extruded
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F23—COMBUSTION APPARATUS; COMBUSTION PROCESSES
- F23Q—IGNITION; EXTINGUISHING-DEVICES
- F23Q7/00—Incandescent ignition; Igniters using electrically-produced heat, e.g. lighters for cigarettes; Electrically-heated glowing plugs
- F23Q7/001—Glowing plugs for internal-combustion engines
- F23Q2007/004—Manufacturing or assembling methods
Definitions
- the invention relates to a method for producing a ceramic glow plug having more than two layers.
- Ceramic glow plugs which come prefabricated as glow plugs in the field of internal combustion engines are characterized by the fact that they can be heated faster than previously used steel glow plugs and have a much longer life.
- the object underlying the invention is therefore to provide a method of the type mentioned, which is inexpensive and suitable for mass production.
- the desired for the optimal function of the glow plug layer structure can be formed in a simple manner, namely by simultaneous extrusion of multiple layers in the form of a tube or a rod.
- the method according to the invention is in particular one by coextrusion, that is, by simultaneous extrusion of all required Layers prepared raw cylinder of the ceramic glow plug after calibration of the diameter and lengths of the blank by cutting processes tapered at one end and provided at the other end with a Greticiansbohrung.
- the cylinder machined in this way is then debinded and presintered to ensure sufficient strength for the subsequent process steps.
- the above-mentioned taper of the raw cylinder at one end and the formation of the contacting hole at the other end can be done by white machining by means of diamond tools even after debinding and pre-sintering.
- the green body After drying, the green body is fired and ground to its final geometry by a simple and inexpensive pass-through grinding process.
- an additionally conductive or non-conductive layer can be applied, which protects the actual heating layer from corrosion or even serves as a heating layer and Stromumlenkungs Mrs or the layer structure can be completed.
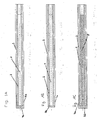
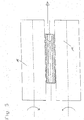
- a glow plug for a ceramic glow plug comprises a rotationally symmetrical structure of an electrically conductive inner cylinder 1, a coaxial with the inner cylinder 1 provided on the cylinder outer surface insulating layer 2, a coaxial thereto provided conductive layer 3 and the actual heating layer 4, the coaxial layer 4a and is formed as a perpendicular to the Glühuxachse layer 4b at the end of the arrangement of inner cylinder 1 and layers 2, 3.
- the cross sections may be asymmetrical, square or rectangular.
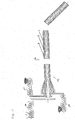
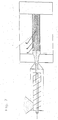
- Fig. 2 shows this in the manufacture of a glow plug after Fig. 1A related principle of coextrusion.
- the layer structure is formed by extruders 10, 11 and 12 in a coextrusion head 13.
- the extruder 10 produces the conductive core 1, the extruder 11 applies the insulating layer 2, and the extruder 12 completes the layer structure with the outer conductive layer 3.
- the coextrusion head 13 for forming three layers may be, for example, a tool used in plastics technology with quill and spiral distributor.
- the outer heating and redirecting layer 4 is applied, which can be done by spraying a slurry before sintering, but also by dipping, overspraying or thermal spraying.
- the usual in the field of plastics technology welding process such as ultrasonic, friction welding, etc. be used.
- This layer 4 is formed as a coaxial layer 4a and perpendicular to the glow plug layer 4b at the end of the arrangement and establishes the connection between the inner and the outer conductor.
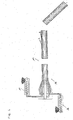
- Fig. 1D shows from top to bottom the annealing zone and the contacting zone.
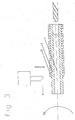
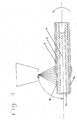
- the necessary for the diversion of the electric current layer on the face can in turn be formed by spraying a slurry before sintering but also by dipping, overspraying or thermal spraying.
- the welding methods customary in the field of plastics technology e.g. Ultrasonic, friction welding and the like be used.
- the inventive method can be carried out in a variety of different variations, so that it can be easily adapted to different layer thicknesses and types of layers.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Combustion & Propulsion (AREA)
- General Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Ceramic Engineering (AREA)
- Resistance Heating (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
Claims (9)
- Procédé de fabrication d'une bougie de préchauffage en céramique avec un cylindre conducteur électrique intérieur (1) et au moins deux couches extérieures (2, 3) d'une structure stratifiée, le cylindre conducteur électrique intérieur (1) et les deux couches extérieures (2, 3) ou plus de la structure stratifiée étant formées simultanément par co-extrusion, et une couche conductrice (4a, 4b) étant appliquée à une extrémité du co-extrudat constitué du cylindre conducteur électrique intérieur (1) et de la structure stratifiée, la couche conductrice (4a, 4b) comportant une partie (4b) à extension radiale par rapport à l'axe de la bougie de préchauffage, et une partie (4a) à extension axiale par rapport à l'axe de la bougie de préchauffage, si bien que la couche conductrice (4a, 4b) assure une liaison électrique entre le cylindre conducteur électrique intérieur (1) et la couche extérieure conductrice (3) de la structure stratifiée.
- Procédé selon la revendication 1, caractérisé en ce que les couches extérieures (2, 3) sont formées symétriquement par rapport à l'axe de la bougie de préchauffage.
- Procédé selon la revendication 2, caractérisé en ce que les couches extérieures (2, 3) sont formées coaxialement.
- Procédé selon la revendication 1, 2 ou 3, caractérisé en ce que la structure stratifiée est à symétrie de révolution et est contactée par un pôle extérieur et un pôle intérieur.
- Procédé selon la revendication 1, caractérisé en ce que la partie (4a) de la couche conductrice à extension axiale par rapport à l'axe de la bougie de préchauffage, et/ou la partie (4b) de la couche conductrice à extension radiale par rapport à l'axe de la bougie de préchauffage, sont appliquées à l'extrémité du co-extrudat par pulvérisation, projection, compression, ou par soudage.
- Procédé selon la revendication 1, Caractérisé en ce que le co-extrudat est confectionné en état non cuit par usinage à enlèvement de copeaux ou par découpage au jet d'eau.
- Procédé selon la revendication 1, caractérisé en ce que la structure stratifiée du co-extrudat est complétée par injection enrobante, couvrante et/ou intérieure dans une presse d'injection.
- Procédé selon la revendication 1, caractérisé
en ce que la partie (4a) de la couche conductrice à extension axiale par rapport à l'axe de la bougie de
préchauffage, et/ou la partie (4b) de la couche conductrice à extension radiale par rapport à l'axe de la bougie de préchauffage, sont formées à l'extrémité du co-extrudat par pulvérisation thermique après frittage de la structure stratifiée formée par co-extrusion. - Procédé selon l'une des revendications précédentes, caractérisé en ce que la bougie de préchauffage est frittée avant d'être partiellement ou complètement rectifiée ou surrectifiée.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10353972A DE10353972B4 (de) | 2003-11-19 | 2003-11-19 | Verfahren zum Herstellen von keramischen Glühkerzen |
| DE10353972 | 2003-11-19 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1533571A2 EP1533571A2 (fr) | 2005-05-25 |
| EP1533571A3 EP1533571A3 (fr) | 2008-01-02 |
| EP1533571B1 true EP1533571B1 (fr) | 2014-03-19 |
Family
ID=34428795
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP04023484.1A Expired - Lifetime EP1533571B1 (fr) | 2003-11-19 | 2004-10-01 | Procédé de fabrication de bougies de préchauffage en céramique |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US7160584B2 (fr) |
| EP (1) | EP1533571B1 (fr) |
| JP (1) | JP2005147654A (fr) |
| KR (1) | KR101169216B1 (fr) |
| DE (1) | DE10353972B4 (fr) |
Families Citing this family (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10353973B4 (de) * | 2003-11-19 | 2006-08-17 | Beru Ag | Verfahren zum Herstellen eines keramischen Glühstiftes für eine keramische Glühkerze |
| EP1815185A2 (fr) * | 2004-10-28 | 2007-08-08 | Saint-Gobain Corporation | Allumeurs ceramiques |
| BRPI0607345A2 (pt) * | 2005-02-05 | 2009-09-01 | Saint Gobain Ceramics | acendedores cerámicos |
| DE102005024623B4 (de) * | 2005-05-30 | 2007-08-23 | Beru Ag | Verfahren zum Herstellen eines keramischen Glühstiftes für eine Glühkerze |
| DE102006016566B4 (de) * | 2005-09-22 | 2008-06-12 | Beru Ag | Zusammengesetzter Leiter, insbesondere für Glühkerzen für Dieselmotoren |
| US7607206B2 (en) * | 2005-12-29 | 2009-10-27 | Federal Mogul World Wide, Inc. | Method for forming layered heating element for glow plug |
| DE102006018606B4 (de) * | 2006-01-04 | 2008-05-08 | Beru Ag | Messglühkerze |
| US20070221647A1 (en) * | 2006-03-23 | 2007-09-27 | Federal-Mogul World Wide, Inc. | Multi-layer heating element |
| JP4794338B2 (ja) * | 2006-03-29 | 2011-10-19 | 京セラ株式会社 | セラミックヒータ |
| DE102007027319A1 (de) * | 2007-06-14 | 2008-12-18 | Beru Ag | Zündkerze und Verfahren zur Herstellung einer Zündkerze |
| US8183501B2 (en) * | 2007-12-13 | 2012-05-22 | Delphi Technologies, Inc. | Method for controlling glow plug ignition in a preheater of a hydrocarbon reformer |
| MX2010007140A (es) * | 2007-12-29 | 2010-08-12 | Saint Gobain Ceramics | Encendedor de ceramica coaxial y metodos de fabricacion. |
| US8820133B2 (en) * | 2008-02-01 | 2014-09-02 | Apple Inc. | Co-extruded materials and methods |
| DE102008040339A1 (de) * | 2008-07-11 | 2010-01-14 | Robert Bosch Gmbh | Glührohr, insbesondere für eine Glühstiftkerze |
| DE102008035036B3 (de) * | 2008-07-26 | 2010-04-15 | Beru Ag | Keramische Glühkerze |
| DE102010045780A1 (de) * | 2010-09-17 | 2012-03-22 | Rohde & Schwarz Gmbh & Co. Kg | Kalibriereinheit für ein Messgerät |
| EA201391073A1 (ru) | 2011-01-25 | 2013-12-30 | Оксан Материалз, Инк. | Экструзионный способ получения расклинивающего агента |
| DE102011055283B4 (de) | 2011-11-11 | 2016-06-23 | Borgwarner Ludwigsburg Gmbh | Glühkerze und Verfahren zum Herstellen eines Glühstifts |
| CN110759730A (zh) * | 2018-07-25 | 2020-02-07 | 比亚迪股份有限公司 | 一种复合陶瓷的制备方法及复合陶瓷 |
| CN112571583A (zh) * | 2020-11-27 | 2021-03-30 | 珠海读书郎网络教育有限公司 | 一种导电陶瓷的挤出装置及挤出方法 |
Family Cites Families (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1534467A (fr) * | 1967-08-21 | 1968-07-26 | Texas Instruments Inc | Conducteur électrique isolé et son procédé de fabrication |
| US4418661A (en) * | 1981-02-07 | 1983-12-06 | Robert Bosch Gmbh | Glow plug, particularly for diesel engine |
| JPS5866720A (ja) * | 1981-10-15 | 1983-04-21 | Ngk Spark Plug Co Ltd | セラミツクグロ−プラグ |
| JPS59153027A (ja) * | 1983-02-18 | 1984-08-31 | Nippon Soken Inc | グロ−プラグ |
| JPS61217626A (ja) * | 1985-03-22 | 1986-09-27 | Jidosha Kiki Co Ltd | 自己温度制御型グロ−プラグ |
| JPS62731A (ja) | 1985-06-27 | 1987-01-06 | Jidosha Kiki Co Ltd | デイ−ゼルエンジン用グロ−プラグ |
| JPS62141424A (ja) * | 1985-12-13 | 1987-06-24 | Jidosha Kiki Co Ltd | デイ−ゼルエンジン用グロ−プラグ |
| JPS62221536A (ja) * | 1986-03-24 | 1987-09-29 | 株式会社神戸製鋼所 | 複合部材及びその製造方法 |
| JPH02251013A (ja) * | 1989-03-24 | 1990-10-08 | Hitachi Metals Ltd | ディーゼルエンジン用グロープラグ |
| US5304778A (en) * | 1992-11-23 | 1994-04-19 | Electrofuel Manufacturing Co. | Glow plug with improved composite sintered silicon nitride ceramic heater |
| US5338716A (en) * | 1992-12-01 | 1994-08-16 | Akzo Nobel Nv | Non-oxide metal ceramic catalysts comprising metal oxide support and intermediate ceramic passivating layer |
| AU1669695A (en) * | 1994-02-18 | 1995-09-04 | Morgan Matroc S.A. | Hot surface igniter |
| JPH09159170A (ja) * | 1995-12-04 | 1997-06-20 | Tokyo Gas Co Ltd | セラミックグロープラグ |
| JPH09191350A (ja) * | 1996-01-10 | 1997-07-22 | Canon Inc | マルチメディア通信装置 |
| JPH1154246A (ja) * | 1997-07-30 | 1999-02-26 | Kyocera Corp | セラミック発熱体 |
| DE19844347A1 (de) * | 1998-09-28 | 2000-03-30 | Bosch Gmbh Robert | Keramische Glühstiftkerze |
| DE19857958A1 (de) * | 1998-12-16 | 2000-06-21 | Bosch Gmbh Robert | Verfahren zur Herstellung eines Stiftheizer |
| US6184497B1 (en) * | 1999-06-16 | 2001-02-06 | Le-Mark International Ltd. | Multi-layer ceramic heater element and method of making same |
| US6084212A (en) | 1999-06-16 | 2000-07-04 | Le-Mark International Ltd | Multi-layer ceramic heater element and method of making same |
| DE19930334C2 (de) * | 1999-07-02 | 2003-07-31 | Beru Ag | Keramischer Heizstab und diesen enthaltende Glühkerze und Verfahren zu dessen Herstellung |
| DE10053327C2 (de) * | 2000-10-27 | 2003-04-10 | Bosch Gmbh Robert | Stiftheizer |
| DE10055082A1 (de) * | 2000-11-07 | 2002-05-16 | Bosch Gmbh Robert | Keramischer Verbundwerkstoff |
| US6610964B2 (en) * | 2001-03-08 | 2003-08-26 | Stephen J. Radmacher | Multi-layer ceramic heater |
| US6396028B1 (en) * | 2001-03-08 | 2002-05-28 | Stephen J. Radmacher | Multi-layer ceramic heater |
| DE10155230C5 (de) * | 2001-11-09 | 2006-07-13 | Robert Bosch Gmbh | Stiftheizer in einer Glühstiftkerze und Glühstiftkerze |
| DE10155203A1 (de) * | 2001-11-09 | 2003-06-18 | Bosch Gmbh Robert | Laserbearbeitungsvorrichtung |
| DE10310155B4 (de) | 2003-03-07 | 2008-07-31 | Siemens Ag | Zugangskontrollsystem für ein Objekt, insbesondere für ein Kraftfahrzeug und Verfahren zum Betreiben eines Zugangskontrollsystems |
| DE10353973B4 (de) * | 2003-11-19 | 2006-08-17 | Beru Ag | Verfahren zum Herstellen eines keramischen Glühstiftes für eine keramische Glühkerze |
-
2003
- 2003-11-19 DE DE10353972A patent/DE10353972B4/de not_active Expired - Lifetime
-
2004
- 2004-10-01 EP EP04023484.1A patent/EP1533571B1/fr not_active Expired - Lifetime
- 2004-11-10 US US10/984,881 patent/US7160584B2/en not_active Expired - Lifetime
- 2004-11-11 KR KR1020040092059A patent/KR101169216B1/ko not_active Expired - Lifetime
- 2004-11-15 JP JP2004330065A patent/JP2005147654A/ja active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| US7160584B2 (en) | 2007-01-09 |
| DE10353972B4 (de) | 2006-03-16 |
| KR20050048473A (ko) | 2005-05-24 |
| KR101169216B1 (ko) | 2012-07-30 |
| EP1533571A2 (fr) | 2005-05-25 |
| EP1533571A3 (fr) | 2008-01-02 |
| JP2005147654A (ja) | 2005-06-09 |
| US20050145613A1 (en) | 2005-07-07 |
| DE10353972A1 (de) | 2005-06-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE10353972B4 (de) | Verfahren zum Herstellen von keramischen Glühkerzen | |
| EP2357704A1 (fr) | Procédé de fabrication d'une cellule de combustible SOFC | |
| DE102018101512B4 (de) | Verfahren zum Herstellen einer Elektrodenanordnung, Elektrodenanordnung und Zündkerze | |
| DE10115601C1 (de) | Trommelkommutator sowie Verfahren zu seiner Herstellung | |
| DE102012110098A1 (de) | Verfahren zur Herstellung elektrischer Durchführungen | |
| EP1065446A2 (fr) | Barre chauffante en céramique, bougie à incandescence la comprenant et procédé de production | |
| DE19956844A1 (de) | Plankommutator, Verfahren zu seiner Herstellung sowie Leiterrohling und Kohlenstoffscheibe zur Verwendung bei seiner Herstellung | |
| EP2003753B1 (fr) | Bougie d'allumage et procédé de fabrication d'une bougie d'allumage | |
| EP4118717A1 (fr) | Connecteur à soudure de friction et son procédé de production | |
| EP1235285B1 (fr) | Méthode de fabrication des actionneurs piézocéramiques multicouche | |
| DE2059179B2 (de) | Verfahren zur Herstellung eines faserverstärkten Formkörpers sowie Anwendung des Verfahrens zur Herstellung spezieller Formkörper | |
| EP2180967B1 (fr) | Procédé pour fabriquer un corps de machine comportant une chambre de fluide à surface durcie | |
| DE20212918U1 (de) | Elektrische Heizeinrichtung für zylindrische Körper | |
| DE102015200778A1 (de) | Glühstiftkerze | |
| WO2005104256A2 (fr) | Unite fonctionnelle electrique et procede pour sa production | |
| DE10353973B4 (de) | Verfahren zum Herstellen eines keramischen Glühstiftes für eine keramische Glühkerze | |
| DE602004012002T2 (de) | Herstellungsverfahren eines metallischen Gehäuses für eine Zündkerze, Herstellungsverfahren einer Zündkerze mit einem metallischen Gehäuse und Zündkerze hiermit hergestellt | |
| DE102020111654A1 (de) | Zündkerze für eine Verbrennungskraftmaschine sowie Verfahren zum Herstellen einer Elektrode für eine solche Zündkerze | |
| EP3552273B1 (fr) | Procédé de fabrication d'un contact femelle | |
| WO2009087038A2 (fr) | Dispositif de fixation de boîtiers en plastique | |
| DE10229894A1 (de) | Herstellungsverfahren einer Metallhülle einer Zündkerze | |
| DE102008007769A1 (de) | Verfahren zur Herstellung eines Maschinengehäuses mit oberflächengehärteter Fluidkammer | |
| EP1048375B1 (fr) | Procédé de formage d'une ebauche en cuivre par extrusion à froid | |
| DE102019127689B4 (de) | Elektrischer Rohrheizkörper mit Anschlussbolzen und Herstellungsverfahren für elektrische Rohrheizkörper mit Anschlussbolzen | |
| DE102021128646B3 (de) | Verfahren zur Herstellung einer mineralisolierten Buchse |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL HR LT LV MK |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: WEISSENBACHER, JOHANN Inventor name: ALLGAIER, MARTIN Inventor name: VON WATZDORF, HENNING Inventor name: FRASSEK, LUTZ Inventor name: HOUBEN, HANS Inventor name: GOEB, OLIVER |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL HR LT LV MK |
|
| 17P | Request for examination filed |
Effective date: 20080117 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20110825 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20130826 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 657918 Country of ref document: AT Kind code of ref document: T Effective date: 20140415 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502004014555 Country of ref document: DE Effective date: 20140424 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20140319 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502004014555 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140721 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20141028 Year of fee payment: 11 |
|
| 26N | No opposition filed |
Effective date: 20141222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502004014555 Country of ref document: DE Effective date: 20141222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141001 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20141001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141001 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20150630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141001 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 657918 Country of ref document: AT Kind code of ref document: T Effective date: 20141001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141001 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502004014555 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140620 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20041001 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140319 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160503 |