EP1968794B1 - Procede pour commander une machine de traitement de matiere en forme de feuilles - Google Patents
Procede pour commander une machine de traitement de matiere en forme de feuilles Download PDFInfo
- Publication number
- EP1968794B1 EP1968794B1 EP06829469.3A EP06829469A EP1968794B1 EP 1968794 B1 EP1968794 B1 EP 1968794B1 EP 06829469 A EP06829469 A EP 06829469A EP 1968794 B1 EP1968794 B1 EP 1968794B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- inking unit
- cleaning
- cylinder
- driven
- rollers
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000000034 method Methods 0.000 title claims description 19
- 238000012545 processing Methods 0.000 title claims description 8
- 239000000463 material Substances 0.000 title claims description 7
- 238000004140 cleaning Methods 0.000 claims description 39
- 238000007639 printing Methods 0.000 claims description 36
- 239000011248 coating agent Substances 0.000 claims description 13
- 238000000576 coating method Methods 0.000 claims description 13
- 239000012459 cleaning agent Substances 0.000 claims description 11
- 239000000839 emulsion Substances 0.000 claims description 8
- 238000007645 offset printing Methods 0.000 claims description 8
- 238000005406 washing Methods 0.000 claims description 7
- 230000008878 coupling Effects 0.000 claims description 6
- 238000010168 coupling process Methods 0.000 claims description 6
- 238000005859 coupling reaction Methods 0.000 claims description 6
- 230000009969 flowable effect Effects 0.000 claims description 2
- 238000005507 spraying Methods 0.000 claims description 2
- 238000013016 damping Methods 0.000 claims 5
- 238000011161 development Methods 0.000 description 6
- 230000018109 developmental process Effects 0.000 description 6
- 239000003599 detergent Substances 0.000 description 3
- 239000003973 paint Substances 0.000 description 3
- 230000001360 synchronised effect Effects 0.000 description 2
- 239000002966 varnish Substances 0.000 description 2
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Chemical compound O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 2
- 238000012937 correction Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 239000004744 fabric Substances 0.000 description 1
- 238000010422 painting Methods 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 238000012549 training Methods 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
- 238000011144 upstream manufacturing Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F33/00—Indicating, counting, warning, control or safety devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F13/00—Common details of rotary presses or machines
- B41F13/004—Electric or hydraulic features of drives
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F13/00—Common details of rotary presses or machines
- B41F13/008—Mechanical features of drives, e.g. gears, clutches
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F31/00—Inking arrangements or devices
- B41F31/004—Driving means for ink rollers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F35/00—Cleaning arrangements or devices
Definitions
- the invention relates to a method for controlling a processing machine for sheet material with at least one printing and / or coating unit according to the preamble of independent claim 1.
- a processing machine is according to EP 0 812 683 A1 with a controllable direct drive for a single driven cylinder known.
- gear train of a sheetfed offset printing machine decoupled a plate cylinder or a blanket cylinder at least one printing unit by means of individual drive in a predeterminable manner directly. Due to the individual and independent of other cylinders directly driven plate cylinder plate pressure correction options and other operations such as plate replacement or cleaning of cylinders can be realized.
- the inking unit associated with the plate cylinder has at least one roller which can be driven by a direct motor drive. Alternatively, certain inking rollers are coupled on the drive side with the gear train for the sheet transport via the main drive.
- DE 100 00 903 and WO 2006/018106 are also part of the state of the art.
- the invention has for its object to provide a method of the type mentioned above, which reduces the cleaning effort in an inking unit or a metering device on a processing machine for sheet material with at least one individually driven, a printing plate bearing cylinder.
- a first advantage of the invention is that a significant reduction of the cleaning effort by the individual cleaning time and the individual speeds of the rollers or cylinders to be cleaned, in particular when cleaning an inking unit and / or a metering device, is realized on a processing machine.
- each inking unit or each metering device can be cleaned with driven in a selection menu cleaning program over an individual cleaning time period with individual speeds.
- the cleaning program also specifies that the printing ink or varnish used in the respective printing or coating unit (color-specific or varnish-specific) is taken into account during the cleaning period or the rotational speed.
- the respective printing / painting job related criteria can be deposited.
- a third advantage is given by the fact that by individual cleaning time and individual speeds of the roller wear can be significantly reduced. Thus, for example, only slightly contaminated paint / coating plants can be cleaned in less time than could previously be done when cleaning the rollers together on the main drive and gear train.
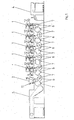
- the sheet-fed rotary printing machine is shown for example with a feeder 4, five offset printing units 1, a coating unit 2 and a boom 5.
- Each offset printing unit 1 has in a known manner an inking unit 12 with inking rollers, a cylinder 10 carrying a printing plate, here as a plate cylinder 10, and a blanket cylinder 8. If necessary, each plate cylinder 10 is associated with a dampening unit.
- the coating unit 2 comprises, in a known manner, a metering device 11 for the medium to be processed (paint, ink), preferably a chambered doctor blade with associated screened applicator roller or a roller system with an applicator roller, and a cylinder 9 carrying a printing plate, here as a forme cylinder 9. on.
- the coating unit 2 is downstream of the offset printing units 1 in the conveying direction 3 for the sheet material.
- Plate cylinder 10 and forme cylinder 9 each carry at least one printing plate and the inking rollers of the inking unit 12 and the applicator roller of the metering device 11 can be brought into contact with the respective plate / forme cylinder 10, 9.
- at least one dampening roller of the dampening unit can be brought into contact with the plate cylinder 10.
- each printing or coating unit 1, 2 is designed as a printing cylinder sheet guiding cylinder 6 with the respective Gumrnituchzylinder 8 or form cylinder 9 in functional connection, wherein in the first printing unit 1 formed as a printing cylinder sheet guiding cylinder 6 a plant drum is arranged upstream as a sheet guiding cylinder 6.
- a transfer cylinder for the sheet transport between the printing cylinder 2 designed as a pressure cylinder sheet of the printing or coating units 1, 2 more sheet guiding cylinder 6 are arranged as a transfer cylinder.
- Each blanket cylinder 8, each forme cylinder 9 and each preferably designed as a printing cylinder sheet guiding cylinder 6 is a cleaning device 7 (cloth or brush washing device or a non-contact Klischeecurisvorraum assigned).
- Each inking unit 12 has an inking unit washing device, for example, a directed onto the compactor detergent spraying system and a engageable doctor device on a last in the direction of rotation of the plate cylinder inking roller. If necessary, the applicator roller is assigned a further cleaning device or the application roller can be cleaned by means of chamber doctor blade.
- At least all sheet guiding cylinders 6 are coupled to each other via a main drive (not shown in detail) (at least one feeding drive motor) and a gear train on the drive side.
- a main drive (at least one feeding drive motor) and a gear train on the drive side.
- Each plate cylinder 10 and preferably each forme cylinder 9 is - mechanically decoupled from the main drive and gear train - by a respective direct drive M, i. a separate drive motor, self-propelled.
- These direct drives M are coupled to a machine control and can be driven individually in a predeterminable manner, at least in relation to the sheet guiding cylinders 6 (main drive and gear train).
- a printing plate carrying cylinder 10 here a plate cylinder 10 coupled to a direct drive M and from one to the gear train of the sheet guiding cylinder 6 mechanically acting for the main transport acting on the sheet transport and can be driven in a predeterminable manner at least with respect to the sheet guiding cylinders 6.
- the directly driven plate cylinder 10 is assigned an inking unit 12 with at least one drivable by the main drive and gear train inking roller.
- the inking roller is preferably a rotary and axially iridescent drivable ink roller. If necessary, a drive-side coupling with other inking rollers can be realized.
- the cleaning preferably takes place via a known inking unit washing device. Thereafter, the temporary drive coupling between the directly driven plate cylinder 10 and the inking rollers of the inking unit 12 is separated and the inking rollers of the inking unit 12 are coupled to the main drive and gear train of the sheet guiding cylinder 6 and the pressure contact between the plate cylinder 10 and the blanket cylinder 8 is generated again.
- the inking rollers to be cleaned are employed on the directly driven plate cylinder 10 and the inking rollers of the inking unit 12 and the plate cylinder 10 are synchronized according to a stored in a selection menu cleaning program over an individual cleaning period with individual speeds be ground.
- the inking rollers to be cleaned in particular the applicator rollers of the inking unit 12 are turned off by the directly driven plate cylinder 10 and only the inking rollers of the inking unit 12 are driven by a stored in a selection menu cleaning program over an individual cleaning period with individual speeds.
- the blanket cylinder 8 and / or the adjacent sheet guiding cylinder 6 are driven by main drive and gear train for a cleaning program stored in a selection menu over an individual cleaning period with a different speed to the inking unit 12 and the directly driven plate cylinder 10. This can be done simultaneously to clean the inking rollers.
- the inking rollers and the plate cylinder 10 are driven synchronously by direct drive M to the machine speed generated by the main drive and then the temporary drive coupling between the directly driven plate cylinder 10 and the inking rollers of the inking unit 12 and then the inking rollers of the inking unit 12 are coupled to the main drive and gear train of the sheet guiding cylinder 6 during cleaning of the blanket cylinder 8 at machine speed.
- this procedure is carried out at a time at which the blanket cylinder 8 has already been substantially cleaned.
- At least one dampening roller to be cleaned a dampening unit can be employed on the directly driven plate cylinder 10 and the dampening rollers of the dampening unit and the plate cylinder 10 are driven synchronously according to a stored in a selection menu cleaning program over an individual cleaning period with individual speeds.
- At least one dampening roller of a dampening unit to be cleaned to an inking roller of the inking unit 12 are employed and the dampening rollers and the inking rollers are driven synchronously according to a stored in a selection menu cleaning program over an individual cleaning period with individual speeds.
- a coupling of the dampening roller with the inking rollers is realized by means of a bridge rollers. The dampening rollers and the inking rollers are separated from the plate cylinder 10 (no contact).
- the emulsion of printing ink and cleaning agent additionally scraps a defined amount of cleaning agent are sprayed onto the compactor.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Inking, Control Or Cleaning Of Printing Machines (AREA)
Claims (10)
- Procédé de commande d'une machine de transformation pour feuilles de matériau, comportant au moins un groupe d'impression et/ou de vernissage, dans lequel un cylindre (10) s'appuyant dans des bâtis latéraux, supportant un cliché d'impression et réalisé sous forme de cylindre porte-plaque (10) est couplé à une commande directe et découplé mécaniquement d'une commande principale agissant sur un train de roues de cylindres porte-cliché (8) et de tambours (6) (cylindre guide-feuilles (6)) pour le transport de feuilles et peut être entraîné de manière prescriptible au moins par rapport aux cylindres guide-feuilles (6), étant associé au cylindre porte-plaque (10) entraîné directement un groupe d'encrage comportant au moins un rouleau de groupe d'encrage (12) pouvant être entraîné par la commande principale et le train de roues, caractérisé en ce que,
dans une zone de contact du cylindre supportant le cliché d'impression, réalisé sous forme de cylindre porte-plaque (10) d'un groupe d'impression offset (1), un contact d'impression avec un cylindre porte-blanche voisin (8) est suspendu,
que, pour le nettoyage, les rouleaux de groupe d'encrage du groupe d'encrage (12) sont séparés du côté moteur des cylindres guide-feuilles (6) entraînés au moyen de la commande principale et du train de roues et couplés temporairement du côté moteur au cylindre porte-plaque (10) entraîné directement et supportant le cliché d'impression et qu'ensuite, les rouleaux de groupe d'encrage du groupe d'encrage (12) sont entraînés suivant un programme de nettoyage enregistré dans un menu de sélection pendant une durée de nettoyage individualisée à des vitesses de rotation individualisées au moyen d'une commande directe (M), puis
que le couplage moteur temporaire entre le cylindre porte-plaque entraîné directement (10) et les rouleaux de groupe d'encrage du groupe d'encrage (12) sont couplés à la commande principale et au train de roues du cylindre guide-feuilles (6) et que le contact d'impression entre le cylindre porte-plaque (10) et le cylindre porte-blanchet (8) est rétabli. - Procédé selon la revendication 1,
caractérisé en ce que
les rouleaux de groupe d'encrage du groupe d'encrage (12) à nettoyer sont approchés du cylindre porte-plaque (10) entraîné directement et que les rouleaux de groupe d'encrage du groupe d'encrage (12) et le cylindre porte-plaque (10) sont entraînés de manière synchrone suivant un programme de nettoyage enregistré dans un menu de sélection pendant une durée de nettoyage individualisée à des vitesses de rotation individualisées. - Procédé selon la revendication 1,
caractérisé en ce que
les rouleaux de groupe d'encrage du groupe d'encrage (12) à nettoyer sont écartés du cylindre porte-plaque (10) entraîné directement et que seuls les rouleaux de groupe d'encrage du groupe d'encrage (12) sont entraînés suivant un programme de nettoyage enregistré dans un menu de sélection pendant une durée de nettoyage individualisée à des vitesses de rotation individualisées. - Procédé selon la revendication 1 ou 2,
caractérisé en ce que le programme de nettoyage englobe au moins une séquence de lavage comprenant les étapes opératoires suivantes :- une quantité définie de produit nettoyant est pulvérisée au moyen d'un dispositif de pulvérisation sur le train de roues du groupe d'encrage (12),- le produit nettoyant est ensuite réparti au moyen du rouleau de groupe d'encrage entraîné et l'encre d'impression est dissoute jusqu'à ce qu'on obtienne une émulsion fluide d'encre d'impression et de produit nettoyant sur les surfaces des rouleaux, puis- un dispositif de raclage est approché d'un cylindre de groupe d'encrage et l'émulsion d'encre d'impression et de produit nettoyant est raclée. - Procédé selon la revendication 1 ou 2,
caractérisé en ce que,
au moins pour nettoyer le cylindre porte-blanchet (8) et/ou le cylindre guide-feuilles voisin (6), ces cylindres (8, 6) sont entraînés au moyen de la commande principale et du train de roues suivant un programme de nettoyage enregistré dans un menu de sélection pendant une durée de nettoyage individualisée à une vitesse de rotation différente de celle du groupe d'encrage (12) et du cylindre porte-plaque (10) entraîné directement. - Procédé selon la revendication 1 ou 2 et 5,
caractérisé en ce que,
après le nettoyage des rouleaux de groupe d'encrage du groupe d'encrage ou des rouleaux de groupe d'encrage du groupe d'encrage et du cylindre porte-plaque (10), pendant le nettoyage du cylindre porte-blanchet (8) entraîné au moyen de la commande principale et du train de roues, les rouleaux du groupe d'encrage et le cylindre porte-plaque (10) sont entraînés de manière synchrone par commande directe (M) à la vitesse de machine générée par la commande principale et le couplage moteur temporaire entre le cylindre porte-plaque (10) entraîné directement et les rouleaux de groupe d'encrage du groupe d'encrage (12) est dissocié et les rouleaux de groupe d'encrage du groupe d'encrage (12) sont couplés à la commande principale et au train de roues des cylindres guide-feuilles (6) pendant le nettoyage du cylindre porte-blanchet (8) à la vitesse de la machine. - Procédé selon la revendication 1 ou 2,
caractérisé en ce
qu'au moins un rouleau de groupe de mouillage à nettoyer d'un groupe de mouillage est approché du cylindre porte-plaque (10) entraîné directement et que les rouleaux de groupe de mouillage du groupe de mouillage et le cylindre porte-plaque (10) sont entraînés de manière synchrone suivant un programme de nettoyage enregistré dans un menu de sélection pendant une durée de nettoyage individualisée à des vitesses de rotation individualisées. - Procédé selon la revendication 1 ou 2,
caractérisé en ce
qu'au moins un rouleau de groupe de mouillage à nettoyer d'un groupe de mouillage est approché d'un rouleau de groupe d'encrage du groupe d'encrage (12) et que les rouleaux de groupe de mouillage et les rouleaux de groupe d'encrage sont entraînés de manière synchrone suivant un programme de nettoyage enregistré dans un menu de sélection pendant une durée de nettoyage individualisée à des vitesses de rotation individualisées. - Procédé selon la revendication 3,
caractérisé en ce que
le dispositif de raclage est approché périodiquement d'un rouleau de groupe d'encrage pendant une séquence de lavage. - Procédé selon la revendication 3,
caractérisé en ce que,
pendant que le dispositif de raclage approché d'un rouleau de groupe d'encrage racle l'émulsion d'encre d'impression et de produit nettoyant, une quantité définie de produit nettoyant est pulvérisée en plus sur le train de roues.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102005062373A DE102005062373A1 (de) | 2005-12-24 | 2005-12-24 | Verfahren zum Steuern einer Verarbeitungsmaschine für Bogenmaterial |
| PCT/EP2006/011877 WO2007073851A1 (fr) | 2005-12-24 | 2006-12-09 | Procede pour commander une machine de traitement de matiere en forme de feuilles |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1968794A1 EP1968794A1 (fr) | 2008-09-17 |
| EP1968794B1 true EP1968794B1 (fr) | 2015-09-23 |
Family
ID=37986796
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP06829469.3A Active EP1968794B1 (fr) | 2005-12-24 | 2006-12-09 | Procede pour commander une machine de traitement de matiere en forme de feuilles |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US8100056B2 (fr) |
| EP (1) | EP1968794B1 (fr) |
| JP (1) | JP2009521339A (fr) |
| CN (1) | CN101346229B (fr) |
| DE (1) | DE102005062373A1 (fr) |
| WO (1) | WO2007073851A1 (fr) |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102007039220B4 (de) * | 2007-06-02 | 2022-05-19 | Koenig & Bauer Ag | Antriebe für eine Bogendruckmaschine |
| DE102008029998A1 (de) * | 2007-07-11 | 2009-01-15 | Manroland Ag | Abfördern von Druckfarbe |
| DE102007044012A1 (de) * | 2007-09-14 | 2009-03-19 | Manroland Ag | Verfahren zum Betreiben einer Bogendruckmaschine |
| DE102009006268B4 (de) | 2008-02-26 | 2017-12-14 | Heidelberger Druckmaschinen Ag | Verfahren zum Reinigen einer Mantelfläche eines Gummituchzylinders einer Nassoffsetdruckmaschine |
| DE102008000866B4 (de) * | 2008-03-27 | 2022-05-25 | manroland sheetfed GmbH | Verarbeitungsmaschine für Bogenmaterial |
| DE102008001923A1 (de) * | 2008-05-21 | 2009-11-26 | Manroland Ag | Verfahren zum Betreiben einer Bogendruckmaschine |
| DE102008045421A1 (de) | 2008-09-02 | 2010-03-04 | Technotrans Ag | Waschanlage für Druckmaschinen |
| DE102010022365B4 (de) * | 2009-06-26 | 2024-08-14 | Heidelberger Druckmaschinen Ag | Erhaltung des Farbprofils im Farbwerk bei Druckunterbrechungen |
| EP2338682A1 (fr) * | 2009-12-22 | 2011-06-29 | KBA-NotaSys SA | Presse d'impression intaglio dotée d'un chariot mobile supportant un cylindre Orlof |
| DE102011118904A1 (de) * | 2010-12-20 | 2012-06-21 | Heidelberger Druckmaschinen Ag | Produktionswerk mit Einzelantrieb |
Family Cites Families (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4000691A (en) * | 1973-02-28 | 1977-01-04 | Maschinenfabrik Augsburg-Nurnberg Ag | Rotary printing press with improved inking system |
| US4270450A (en) * | 1979-09-10 | 1981-06-02 | M.A.N.-Roland Druckmaschinen Aktiengesellschaft | Arrangement for washing cylinders on printing presses |
| JP3406060B2 (ja) * | 1994-05-25 | 2003-05-12 | 東芝機械株式会社 | 切換式連続運転用印刷機の運転方法 |
| DE19623224C1 (de) | 1996-06-11 | 1997-09-11 | Roland Man Druckmasch | Antrieb für eine Druckmaschine |
| DE19640649A1 (de) | 1996-10-02 | 1998-04-16 | Roland Man Druckmasch | Antrieb für eine Bogendruckmaschine |
| DE19650075A1 (de) * | 1996-12-03 | 1998-06-04 | Roland Man Druckmasch | Antrieb für eine Druckmaschine |
| DE19705632A1 (de) | 1997-02-14 | 1998-09-03 | Roland Man Druckmasch | Verfahren und Anordnung zur Reinigung eines Teiles eines Druckwerkes einer Offsetdruckmaschine |
| DE10000903A1 (de) * | 1999-02-05 | 2000-08-10 | Heidelberger Druckmasch Ag | Verfahren zum Betrieb einer Druckmaschine und Druckmaschine zur Durchführung des Verfahrens |
| US6672211B2 (en) | 1999-03-03 | 2004-01-06 | James F. Price | Inking systems for printing presses |
| US6588337B1 (en) * | 2000-04-28 | 2003-07-08 | Baldwin Graphic Systems, Inc. | Method and apparatus for automatically cleaning both the blanket cylinder and the ink rollers of a printing press |
| US6545869B2 (en) * | 2001-01-17 | 2003-04-08 | International Business Machines Corporation | Adjusting fillet geometry to couple a heat spreader to a chip carrier |
| US6796239B2 (en) * | 2001-03-22 | 2004-09-28 | Heidelberger Druckmaschinen Ag | Method and device for driving a printing press |
| WO2002076744A1 (fr) * | 2001-03-26 | 2002-10-03 | Koenig & Bauer Aktiengesellschaft | Entrainement d'un groupe d'impression |
| US20030172818A1 (en) * | 2002-03-13 | 2003-09-18 | Marcel Motard | Dampening system for a printing press |
| DE102004039588B4 (de) * | 2004-08-13 | 2007-11-22 | Man Roland Druckmaschinen Ag | Verfahren und Vorrichtung zum Steuern einer Verarbeitungsmaschine für Bogenmaterial |
| DE102004039536A1 (de) | 2004-08-13 | 2006-02-23 | Man Roland Druckmaschinen Ag | Verfahren zum Steuern einer Verarbeitungsmaschine für Bogenmaterial |
| JP5375484B2 (ja) * | 2009-09-24 | 2013-12-25 | ブラザー工業株式会社 | インクジェット記録装置 |
-
2005
- 2005-12-24 DE DE102005062373A patent/DE102005062373A1/de not_active Withdrawn
-
2006
- 2006-12-09 CN CN200680048976XA patent/CN101346229B/zh not_active Expired - Fee Related
- 2006-12-09 JP JP2008546194A patent/JP2009521339A/ja active Pending
- 2006-12-09 WO PCT/EP2006/011877 patent/WO2007073851A1/fr not_active Ceased
- 2006-12-09 EP EP06829469.3A patent/EP1968794B1/fr active Active
- 2006-12-09 US US12/158,864 patent/US8100056B2/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| EP1968794A1 (fr) | 2008-09-17 |
| JP2009521339A (ja) | 2009-06-04 |
| DE102005062373A1 (de) | 2007-06-28 |
| CN101346229B (zh) | 2011-08-03 |
| WO2007073851A1 (fr) | 2007-07-05 |
| CN101346229A (zh) | 2009-01-14 |
| US8100056B2 (en) | 2012-01-24 |
| US20090071360A1 (en) | 2009-03-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2815388B2 (de) | Vorrichtung zum Waschen von Zylindern an Druckmaschinen, insbesondere Offsetdruckmaschinen | |
| EP1778488B1 (fr) | Procede et dispositif pour commander une machine de transformation pour un materiau en feuilles | |
| EP2703162B1 (fr) | Procédé et dispositif d'impression de matériau d'impression | |
| EP1952987B1 (fr) | Procédé pour contrôler une machine de traitement de feuilles | |
| EP0858891B1 (fr) | Méthode et dispositif de nettoyage d'une partie d'une unité d'impression d'une machine à imprimer offset | |
| DE19729985A1 (de) | Vorrichtung zum Lackieren von Bedruckstoffen in einem Offsetdruckwerk einer Rotationsdruckmaschine | |
| EP1968794A1 (fr) | Procede pour commander une machine de traitement de matiere en forme de feuilles | |
| EP0754552A1 (fr) | Procédé et dispositif de lavage d'un cylindre de plaque et d'un rouleau d'application dans une machine d'impression | |
| DE4324631A1 (de) | Verfahren und Einrichtung zum Aufbringen eines flüssigen Mediums auf einen Bedruckstoff in Offsetdruckmaschinen | |
| EP0692381B1 (fr) | Dispositif pour enlever de l'encre d'un encrier | |
| DE4424590C2 (de) | Einrichtung zur Reinigung eines Farbwerkes einer Offsetdruckmaschine | |
| DE19921628A1 (de) | Verfahren zum Dosieren von Feuchtmittel beim Drucken mit einer Druckform für Offsetdruck | |
| DE102010024011A1 (de) | Traversierende Farbkastenreinigung | |
| EP1040922B1 (fr) | Procédé et dispositif pour enlever d'encre d'un bac ouvert d'un côté | |
| EP0839652B1 (fr) | Méthode de nettoyage des cylindres et des rouleaux dans une machine à imprimer | |
| WO2012123097A1 (fr) | Machine de traitement d'éléments en feuilles comportant au moins une unité de vernissage, et procédé permettant de changer la matière appliquée | |
| DE102007015595B3 (de) | Vorrichtung zum Druckplattenwechsel an einer Verarbeitungsmaschine | |
| DE102022100518A1 (de) | Verfahren zur Reinigung eines Farbwerkes und Farbwerk | |
| EP1567343B1 (fr) | Nettoyage de cylindres dans des machines a imprimer | |
| DE102008031860B4 (de) | Verfahren zum Betreiben einer Bogendruckmaschine | |
| DE102007049453A1 (de) | Verfahren und Vorrichtung zum Druckplattenwechsel an einer Verarbeitungsmaschine | |
| DE102011080699A1 (de) | Verfahren zum Betreiben einer Rotationsdruckmaschine | |
| EP1442884B1 (fr) | Procédé pour le guidage stable d'une bande de largeur moyenne dans des unités d'impression d'une machine à imprimer | |
| DE3705067C1 (en) | Device for improving the ink separation in an inking and damping unit | |
| DE102016210191B4 (de) | Verfahren zum Reinigen eines Gummituches auf einem Gummituchzylinder in einem Werk einer Bogenverarbeitungsmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20080724 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: WIESE, HOLGER Inventor name: MARNETH, BERND Inventor name: SCHUNK, JUERGEN Inventor name: KUEHLMEYER, LOTHAR Inventor name: LINDNER, BERND |
|
| 17Q | First examination report despatched |
Effective date: 20090528 |
|
| 19U | Interruption of proceedings before grant |
Effective date: 20120201 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| 19W | Proceedings resumed before grant after interruption of proceedings |
Effective date: 20121203 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: MANROLAND SHEETFED GMBH |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20150618 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 751003 Country of ref document: AT Kind code of ref document: T Effective date: 20151015 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502006014552 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20150923 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20151224 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160123 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20151231 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160125 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502006014552 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20151209 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20160624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20151209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20061209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150923 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20181203 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20181218 Year of fee payment: 13 Ref country code: CH Payment date: 20181218 Year of fee payment: 13 Ref country code: FR Payment date: 20181220 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 751003 Country of ref document: AT Kind code of ref document: T Effective date: 20191209 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20191209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191209 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191231 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191209 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191231 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230530 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20241210 Year of fee payment: 19 |