EP2077166A1 - Dispositif de traitement de bord longitudinal pour tôles - Google Patents
Dispositif de traitement de bord longitudinal pour tôles Download PDFInfo
- Publication number
- EP2077166A1 EP2077166A1 EP08022540A EP08022540A EP2077166A1 EP 2077166 A1 EP2077166 A1 EP 2077166A1 EP 08022540 A EP08022540 A EP 08022540A EP 08022540 A EP08022540 A EP 08022540A EP 2077166 A1 EP2077166 A1 EP 2077166A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- longitudinal edge
- bending
- processing device
- sheet
- edge processing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000002184 metal Substances 0.000 title claims abstract description 46
- 229910052751 metal Inorganic materials 0.000 title claims abstract description 46
- 238000003754 machining Methods 0.000 title claims description 17
- 238000005452 bending Methods 0.000 claims description 79
- 238000003801 milling Methods 0.000 claims description 8
- 238000005520 cutting process Methods 0.000 claims description 6
- 238000004519 manufacturing process Methods 0.000 claims description 6
- 238000000465 moulding Methods 0.000 claims description 5
- 230000000694 effects Effects 0.000 claims description 2
- 238000000034 method Methods 0.000 description 10
- 239000000463 material Substances 0.000 description 4
- 230000006978 adaptation Effects 0.000 description 2
- 238000010276 construction Methods 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 230000000284 resting effect Effects 0.000 description 1
- 238000005096 rolling process Methods 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D5/00—Bending sheet metal along straight lines, e.g. to form simple curves
- B21D5/01—Bending sheet metal along straight lines, e.g. to form simple curves between rams and anvils or abutments
- B21D5/015—Bending sheet metal along straight lines, e.g. to form simple curves between rams and anvils or abutments for making tubes
Definitions
- the invention relates to a longitudinal edge processing device for sheets, in particular in the production of pipes, with a clamping device, an edge processing device and a bending device with lower and upper mold assembly, which are designed for bending the longitudinal edge.
- Such a longitudinal edge processing device for sheets, in particular in the pipe production is in the DE 23 65 515 A1 specified.
- both straight and oblique cuts can be performed, for. B. a V or X-shaping for a longitudinal weld of the finished bent pipe, and bending operations are carried out on a common table.
- To edit the longitudinal edge of the table is guided with a clamped sheet metal plate on a planing device over. After that, the longitudinal edges of the sheet pass into the area of a pre-bending unit and then into a finish-bending unit.
- the desired bending is carried out by means of pairs of rolls. Due to the contact pressure of the rollers may be in the edge zone
- a plurality of rows directed towards the lower or upper outer surface of the sheet metal stamps are arranged on the upper side and the underside of a metal sheet plate supplied over a support surface, which are adjustable at different distances from the sheet outer surface.
- the stamps on the top and bottom of the sheet are each arranged in at least three rows, each row on the top opposite a row on the bottom and the distances between the rows are adjustable. In particular, thick sheets are to be bent in this way only with considerable effort.
- Another pipe bending machine is in the DE 42 15 807 A1 as well as in the EP 0 051 554 A2 shown.
- the EP 0 051 554 A2 and the DE 24 55 521 A1 show examples of hydraulic sheet metal bending presses.
- the present invention has for its object to provide a longitudinal edge processing device of the type mentioned, which simplifies the processing of metal plates, for example, for the production of pipes.
- the advantage of the longitudinal edge machining device formed in this way is that the bending and machining of the edges in the same installation can be carried out reliably with relatively little effort, even if thick sheets are present, such as are used for pipes of large diameter (for example greater than 50 cm) ,
- An advantageous for the control of the bending process construction is that the lower and / or the upper mold assembly is connected for adjusting to a hydraulic adjusting device / are.
- the features of the structure and the function are advantageous in that the lower and / or the upper die arrangement is / are constructed in a direction parallel to the longitudinal edge of the metal sheet from a plurality of segments.
- a good adaptation to different plates and bending radii results from the fact that the segments of the lower mold assembly each have a control cylinder and a mold punch with press shoe and the segments of the upper mold assembly each have a further actuating cylinder and another Have mold with another press shoe.
- the training may be such that the press shoes are interchangeable.
- the bending of the sheet edge or a subsequent further bending of the sheet is facilitated by the fact that the upper and / or the lower mold assembly with respect to the longitudinal edge has a plurality of parallel rows of segments which are controlled separately.
- An advantageous construction for the processing operations is that for receiving the plate-shaped sheet a support is provided and that a feeding device is provided, by means of which the sheet over the support in the direction transverse to the sheet longitudinal edge can be guided to the arranged next to the support bending device.
- the sheet metal processing is further facilitated by the fact that the edge processing device is arranged outside the bending device with respect to the longitudinal edge of the sheet to be processed, wherein a processing tool can be moved along the longitudinal edge.
- machining tool is a milling tool.
- wave-shaped sheets can be prepared in the same system for further processing.
- the straightening may be effected by the bending device extending longitudinally over the sheet, or an additional arrangement of straightening means may be provided.
- An automatic implementation of the bending process is achieved reliably in that the clamping device and the bending device are connected to a common control device, which is designed for coordinated clamping and bending control.
- the measures that also the feeding device and the edge processing device are connected to the control device contribute to a simplified automatic processing.
- An advantageous further embodiment for the machining is that the bending device is designed for bending, and that the clamping device has an abutment device, which is designed to effect the counterforces to be applied for the bending, wherein the sheet clamping device is dimensioned with pressing cylinders and press shoes so that a fixing of the sheet both during milling, planing or cutting and when bending and / or straightening is ensured.
- a planing tool or another cutting tool may also be provided.
- Fig. 1 shows a longitudinal edge processing device for sheets B, as used in particular for the production of pipes for processing of longitudinal edges before a final bending process.
- a flat, plate-shaped sheet B is fed via a support 14 by means of a feed device 20 in the transverse direction to its one longitudinal edge of a processing station.
- the longitudinal edge portion is located in the region of a bending device with a lower mold unit 7 and an upper mold unit 8, the lower mold unit 7 on its upper side facing the sheet metal side in question a mold cavity 7.1 and the upper mold unit 8 in their respective flat sheet side facing end portion receives a recorded on a molded part 8.2 8.2 convex molded part 8.1.
- the molding units 7 and 8 which may be continuous or segmented in the longitudinal direction, extend parallel to the longitudinal edge of the sheet and are adjustably mounted on a respective adjusting unit 9, 9 ', with which they can be adjusted perpendicular to the sheet metal plane to a bend of the Sheet edge to make.
- an edge processing device 30 is further arranged, which can be moved to the sheet edge or the sheet B by means of the feeder 20 can be fed.
- the machining tool of the edge processing device 30 is shaped accordingly to z. B. to prepare a weld preparation in V, Y or X form.
- the machining tool is preferably a milling tool, but may also be a planing tool or other cutting tool.
- the structure may be designed so that the machining tool along the sheet longitudinal edge is moved at resting sheet B or the sheet B is moved along the stationary machining tool.
- a clamping device 10 is provided with which the plate-shaped sheet B against the support 14 or another support 11 (see. Fig. 2 and 3 ) is clamped to perform the longitudinal edge machining stable and accurate.
- the clamping device is z. B. equipped with pneumatically or hydraulically operated Presszylindem and press shoes and dimensioned so that a fixing of the sheet B is ensured both when working with the milling, planing or cutting tool and when bending.
- the control of the feeding device 20, the clamping device 10 and the bending device is carried out by means of a common control device 5 coordinated with each other, wherein the control of the edge processing device 30 may be included in the control by the control device 5.
- the sheet B is guided by means of the feeding device to the processing point of the edge processing device 30 and then the clamping device 10 is actuated. Then, the control of the bending device takes place. Subsequently, the metal plate thus processed at its edge can be rotated and processed along its other longitudinal edge with the same bending device and edge processing device accordingly.
- a corresponding edge processing device can be provided along the other sheet longitudinal edge, so that a parallel corresponding processing of the two longitudinal edges can be performed simultaneously or with a time delay. After the longitudinal edge machining, the sheet B can then be supplied to the further bending process, for example in a separate plant.
- a further embodiment of a longitudinal edge processing device is shown.
- an edge processing device 30 for example with a milling tool, a planing tool or other cutting tool according to the previous embodiment.
- a feeder 20 may be formed and connected to a control device 5 accordingly.
- the clamping device 10 and a bending device, with which a bending can also take place, are modified in comparison to the first exemplary embodiment.
- the Fig. 2 shows a arranged in a plate bending machine sheet metal plate B, above the top of a plurality of rows of dies 1 and under the bottom of a series of dies 3 are arranged.
- the metal plate B which is supplied via a support 14, is fixed stably in the clamping device 10 with a support 11 on the underside and a clamping arrangement 12 on the upper side, wherein the clamping arrangement 12 by means of a preferably hydraulic or pneumatic actuator 13 against the top of Sheet metal B is pressed against the support 11.
- the top of the metal plate B facing end portions of the die 1 are provided with press shoes 1.1, the ends of which are tapered conical or convex rounded to the outside, so that they favor the bending operation according to the set curvature.
- a further press shoe 4 which directed to the lower surface of the metal plate B towards end face is also tapered or convex rounded to the outside, so that at the beginning of the bending work the flat Sheet metal B rests only point-like or line-like on the press shoe 4 and during bending a change in inclination of the lower sheet surface relative to the end face of the press shoe 4 can proceed unhindered, whereby the bending process is additionally favored.
- the forming dies 1 and the forming dies 3 are preferably operated by means of hydraulically driven actuators, in particular actuating cylinder 2 or 6, for setting to the predetermined curvature on the one hand and for the bending operation on the other hand, wherein the control or regulation of the actuation by means of the control device 5 takes place.
- a hydraulic drive in particular for the forming dies 3, a pneumatic drive can be provided.
- press shoes 1.1 and / or further press shoes 4 are exchangeably attached to the end sections of the forming dies 1 or the forming dies 3 in one embodiment, press shoes 1.1, 4 with differently shaped end faces can easily be exchanged for one another, or they can be easily replaced when worn , Also, an adaptation to different materials to be bent metal plates B is made possible by the exchange of press shoes 1.1 and 4 respectively.
- tuning the material combination press shoes / sheet metal plate it is advantageous to choose the coefficient of friction so that a slip resistance is achieved or a good lubricity depending on the bending contour or sheet material, plate thickness or the like.
- the row of forming dies 3 is arranged for the bending operation with the associated drive means on top of the sheet metal plate B, while the rows of mold punches 1 are arranged for setting the curvature under the underside of the sheet metal plate B.
- the control device 5 By means of the control device 5, the adjustment of the die 1 to the predetermined curvature and the control of the forming dies 3 for the bending process in coordination with each other, for which purpose the controller has a computer unit suitable for programming.
- the sheet metal bending machine has a measuring system with a measuring sensor which picks up the contour of the sheet during bending and optionally further bending in and feeds its data to the control unit and processes it to adjust the bending data.
- the control device 5 advantageously comprises a memory device, are stored in the default values for the processing of certain types of products and are easily retrievable for the operator.
- the clamping device 10 may also be coupled to the control device 5 in order to release the clamping arrangement 12 during the feeding or removal of the metal sheet B and to clamp it during machining during the bending process and the edge processing.
- the feeding device 20 for the metal plate B is also connected to the control device 5 and controlled by it.
- the clamping device 10 results in an unambiguous definition of the metal plate B, so that the bending over the rows of provided with the press shoes 1.1 mold punch 1 can be performed with stable alignment and high accuracy.
- the support 11 with its front side provides a clear reference position for the setting of the die 1 and the above predetermined curvature of the metal plate B, wherein the respective thickness of the metal plate B is taken into account in the control device 5 for the required application of force.
- the bending and, with appropriate training, the desired shape of the sheet such as a cylindrical tube shape, easily and accurately on the means of the control or regulation predetermined adjustment of the hydraulic or pneumatic actuating cylinder by means of a segment bending processing and end position of the rows of mold punches 1, whereby different settings are easily and accurately made possible.
- the rows of mold punches 1 are set with their end faces at the same height or the same distance from the respective surface of the metal sheet B, while the distance from row to row to the edge of the machined Sheet increasingly towards along a straight line or convex curved outward curve can increase.
- the individual rows of the forming dies 1 with their end faces or press shoes 1.1 come into contact with the sheet metal edge in succession with the relevant surface of the sheet, with the lever arm between the relevant row of the forming dies 1 and the row the forming punch 3 increasingly shortened and thus increase the applied bending forces.
- the forming dies 3 are designed for higher forces than the mold punches 1, since they are also stressed more dynamically.
- a press shoe 4 can be assigned a plurality of forming dies 3 with hydraulic or pneumatic drives, so that the number of further press shoes 4 in this case is less than the number of forming dies 3.
- the total number of forming dies 3 in a row can be less than the number of mold dies 1 in a row, whereby the dynamic control of the forming dies 3 favors and wear parts are reduced.
- the row of forming dies 3 is at most as far away from the sheet edge as the row of forming dies 1 lying closest thereto.
- control device 5 By means of the control device 5, the control or regulation during bending or bending on the properties of different materials of the tool of the metal plate B can be suitably adjusted.
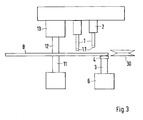
- FIG. 3 A similar embodiment of a longitudinal edge processing device as in Fig. 2 is in Fig. 3 shown.
- the bending device is equipped with only two rows of upper adjusting cylinders 2 and mold dies 1 with press shoes 1.1, while the lower mold assembly accordingly Fig. 2 is executed.
- the lower mold assembly with its press shoes 4 is opposite the edge next upper mold assembly to the longitudinal edge of the sheet B out to perform the bending and optionally further bending of the sheet B.
- the control device 5 and the feeding device 20 and the support 14, which in Fig. 3 not shown, can be done accordingly Fig. 2 be executed.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
- Electrical Discharge Machining, Electrochemical Machining, And Combined Machining (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Grinding And Polishing Of Tertiary Curved Surfaces And Surfaces With Complex Shapes (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL08022540T PL2077166T3 (pl) | 2008-01-03 | 2008-12-31 | Urządzenie do obróbki wzdłużnych krawędzi blach |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE202008000121U DE202008000121U1 (de) | 2008-01-03 | 2008-01-03 | Blechbiegemaschine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2077166A1 true EP2077166A1 (fr) | 2009-07-08 |
| EP2077166B1 EP2077166B1 (fr) | 2013-11-20 |
Family
ID=39311650
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08022322A Not-in-force EP2077165B1 (fr) | 2008-01-03 | 2008-12-23 | Plieuse de tôle |
| EP08022540.2A Not-in-force EP2077166B1 (fr) | 2008-01-03 | 2008-12-31 | Dispositif de traitement de bord longitudinal pour tôles |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08022322A Not-in-force EP2077165B1 (fr) | 2008-01-03 | 2008-12-23 | Plieuse de tôle |
Country Status (9)
| Country | Link |
|---|---|
| EP (2) | EP2077165B1 (fr) |
| AT (1) | ATE457838T1 (fr) |
| DE (2) | DE202008000121U1 (fr) |
| DK (1) | DK2077165T3 (fr) |
| ES (2) | ES2341503T3 (fr) |
| PL (2) | PL2077165T3 (fr) |
| PT (1) | PT2077165E (fr) |
| RS (1) | RS51337B (fr) |
| SI (1) | SI2077165T1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2018114156A1 (fr) * | 2016-12-22 | 2018-06-28 | Bayerische Motoren Werke Aktiengesellschaft | Dispositif et procédé de façonnage d'une tôle |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US7506531B1 (en) * | 2007-12-20 | 2009-03-24 | Gm Global Technology Operations, Inc. | Dimple-forming tool for projection welding |
| EP2419227B1 (fr) * | 2009-04-16 | 2013-02-13 | Bergrohr GmbH Siegen | Presse à cintrer pour feuilles de tôle |
| DE102011053676B4 (de) | 2011-09-16 | 2016-09-08 | EISENBAU KRäMER GMBH | Rohrbiegemaschine |
| CN112404164A (zh) * | 2020-11-10 | 2021-02-26 | 上海宝冶集团有限公司 | 方管压制成形的工艺方法 |
| CN116099952B (zh) * | 2023-01-10 | 2024-03-29 | 连云港市东堡旋耕机械有限公司 | 农业旋耕机多工位同时进行的金属加工冲压设备 |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2365515A1 (de) | 1973-02-14 | 1975-07-03 | Ferndorf Eisen Metall | Vorrichtung zum anbiegen der enden von blechen |
| DE2402190A1 (de) | 1974-01-17 | 1975-07-24 | Mitsubishi Heavy Ind Ltd | Verfahren und vorrichtung zum biegen von stahlblechen bzw. -platten |
| DE2455521A1 (de) | 1974-11-23 | 1976-05-26 | Siempelkamp Gmbh & Co | Hydraulische blechbiegepresse |
| DE2510488A1 (de) | 1975-03-11 | 1976-09-23 | Siempelkamp Gmbh & Co | Hydraulische blechbiegepresse |
| EP0051554A2 (fr) | 1980-11-03 | 1982-05-12 | Kaiser Steel Corporation | Presse à tuyaux |
| EP0056376A1 (fr) | 1980-06-17 | 1982-07-28 | Kaiser Steel Corp | Procede et dispositif de preformage des bords d'une plaque metallique avant sa mise en forme d'un tuyau. |
| US4430872A (en) | 1980-02-14 | 1984-02-14 | Nippon Kokan Kabushiki Kaisha | Method and apparatus for plate edge preparation for UOE pipe making process |
| EP0109031A2 (fr) | 1982-11-12 | 1984-05-23 | Asea Ab | Procédé et outil pour cintrer les sections marginales d'une tôle |
| DE4215807A1 (de) | 1992-05-15 | 1993-11-18 | Mannesmann Ag | Rohrbiegepresse in geschlossener Rahmenbauart |
| EP0906161B1 (fr) | 1996-05-30 | 2000-07-12 | EHT Werkzeugmaschinen GmbH | Machine d'usinage pour pieces sous forme de plaques, notamment pour produire des bords plies sur des pieces en tole |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS6044050B2 (ja) | 1976-09-10 | 1985-10-01 | 新日本製鐵株式会社 | 長尺郭状体の多段成形法 |
| US4043165A (en) | 1976-09-15 | 1977-08-23 | The Boeing Company | Three-point, air-bending sheet metal bender |
| DE4410105A1 (de) * | 1994-03-21 | 1995-09-28 | Mannesmann Ag | Rohrbiegepresse zur Herstellung von Schlitzrohren aus Blechtafeln |
| DE10232098B4 (de) * | 2002-07-15 | 2004-05-06 | Sms Meer Gmbh | Vorrichtung zum Herstellen von Rohren aus Blechtafeln |
-
2008
- 2008-01-03 DE DE202008000121U patent/DE202008000121U1/de not_active Expired - Lifetime
- 2008-12-23 ES ES08022322T patent/ES2341503T3/es active Active
- 2008-12-23 PL PL08022322T patent/PL2077165T3/pl unknown
- 2008-12-23 SI SI200830034T patent/SI2077165T1/sl unknown
- 2008-12-23 DK DK08022322.5T patent/DK2077165T3/da active
- 2008-12-23 AT AT08022322T patent/ATE457838T1/de active
- 2008-12-23 PT PT08022322T patent/PT2077165E/pt unknown
- 2008-12-23 RS RSP-2010/0208A patent/RS51337B/sr unknown
- 2008-12-23 DE DE502008000379T patent/DE502008000379D1/de active Active
- 2008-12-23 EP EP08022322A patent/EP2077165B1/fr not_active Not-in-force
- 2008-12-31 EP EP08022540.2A patent/EP2077166B1/fr not_active Not-in-force
- 2008-12-31 PL PL08022540T patent/PL2077166T3/pl unknown
- 2008-12-31 ES ES08022540.2T patent/ES2447495T3/es active Active
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2365515A1 (de) | 1973-02-14 | 1975-07-03 | Ferndorf Eisen Metall | Vorrichtung zum anbiegen der enden von blechen |
| DE2402190A1 (de) | 1974-01-17 | 1975-07-24 | Mitsubishi Heavy Ind Ltd | Verfahren und vorrichtung zum biegen von stahlblechen bzw. -platten |
| DE2455521A1 (de) | 1974-11-23 | 1976-05-26 | Siempelkamp Gmbh & Co | Hydraulische blechbiegepresse |
| DE2510488A1 (de) | 1975-03-11 | 1976-09-23 | Siempelkamp Gmbh & Co | Hydraulische blechbiegepresse |
| US4430872A (en) | 1980-02-14 | 1984-02-14 | Nippon Kokan Kabushiki Kaisha | Method and apparatus for plate edge preparation for UOE pipe making process |
| EP0056376A1 (fr) | 1980-06-17 | 1982-07-28 | Kaiser Steel Corp | Procede et dispositif de preformage des bords d'une plaque metallique avant sa mise en forme d'un tuyau. |
| EP0056376B1 (fr) * | 1980-06-17 | 1985-02-20 | Kaiser Steel Corporation | Procede et dispositif de preformage des bords d'une plaque metallique avant sa mise en forme d'un tuyau |
| EP0051554A2 (fr) | 1980-11-03 | 1982-05-12 | Kaiser Steel Corporation | Presse à tuyaux |
| EP0109031A2 (fr) | 1982-11-12 | 1984-05-23 | Asea Ab | Procédé et outil pour cintrer les sections marginales d'une tôle |
| DE4215807A1 (de) | 1992-05-15 | 1993-11-18 | Mannesmann Ag | Rohrbiegepresse in geschlossener Rahmenbauart |
| EP0906161B1 (fr) | 1996-05-30 | 2000-07-12 | EHT Werkzeugmaschinen GmbH | Machine d'usinage pour pieces sous forme de plaques, notamment pour produire des bords plies sur des pieces en tole |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2018114156A1 (fr) * | 2016-12-22 | 2018-06-28 | Bayerische Motoren Werke Aktiengesellschaft | Dispositif et procédé de façonnage d'une tôle |
| CN109789463A (zh) * | 2016-12-22 | 2019-05-21 | 宝马股份公司 | 用于板材成形的设备和方法 |
| CN109789463B (zh) * | 2016-12-22 | 2021-08-03 | 宝马股份公司 | 用于板材成形的设备和方法 |
| US12090540B2 (en) | 2016-12-22 | 2024-09-17 | Bayerische Motoren Werke Aktiengesellschaft | Device and method for shaping sheet metal |
Also Published As
| Publication number | Publication date |
|---|---|
| PL2077166T3 (pl) | 2014-05-30 |
| EP2077165B1 (fr) | 2010-02-17 |
| DK2077165T3 (da) | 2010-06-07 |
| PT2077165E (pt) | 2010-05-17 |
| ATE457838T1 (de) | 2010-03-15 |
| SI2077165T1 (sl) | 2010-07-30 |
| EP2077166B1 (fr) | 2013-11-20 |
| RS51337B (sr) | 2011-02-28 |
| ES2341503T3 (es) | 2010-06-21 |
| ES2447495T3 (es) | 2014-03-12 |
| PL2077165T3 (pl) | 2010-07-30 |
| DE502008000379D1 (de) | 2010-04-01 |
| DE202008000121U1 (de) | 2008-04-17 |
| EP2077165A1 (fr) | 2009-07-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0418779A1 (fr) | Méthode pour manufacture de pièces d'oeuvre par découpage, en particulier dans un outil à contre découpage à précision | |
| EP2077166B1 (fr) | Dispositif de traitement de bord longitudinal pour tôles | |
| DE2627972C2 (de) | Schwenkbiegemaschine | |
| DE1652618A1 (de) | Streck-Biege-Vorrichtung | |
| EP0454619A1 (fr) | Machine de cintrage d'une tôle en forme de cylindre | |
| DE102011053676B4 (de) | Rohrbiegemaschine | |
| EP3820631B1 (fr) | Presse à former à jco à réglage élargi | |
| EP0967041B1 (fr) | Procédé et dispositif pour le guidage d'une lame de scie à ruban | |
| DE69223137T2 (de) | Schneidvorrichtung zum automatischen schneiden von messerklingen | |
| EP3325186B1 (fr) | Installation et procédé destinés à l'élimination de défauts de planéité d'un produit plat métallique | |
| EP1731237B1 (fr) | Machine pour travailler de la tôle | |
| DE1602064A1 (de) | Verfahren zur Herstellung sich allmaehlich verjuengender Walzprofile und Maschine zu seiner Durchfuehrung | |
| EP3834976B1 (fr) | Unité de traitement de pièces, en particulier unité de découpe de panneaux, ainsi que procédé d'exploitation d'une unité de traitement de pièces | |
| DE102014116192B4 (de) | Rohrbiegepresse | |
| DE2242314C3 (de) | Bandmesserspaltmaschine | |
| DE68915247T2 (de) | Automatisierbare Rundwalzeneinrichtung mit verzahnten Walzen. | |
| EP1345715B1 (fr) | Presse a forger dotee d'un dispositif de reglage situe cote matrice | |
| CH689689A5 (de) | Verfahren zur programmgesteuerten Dünnblech-Bearbeitung sowie Dünnblech-Bearbeitungsmaschine. | |
| EP2419227B1 (fr) | Presse à cintrer pour feuilles de tôle | |
| EP1638711B1 (fr) | Machine et procede d'estampage de pieces | |
| DE2203913A1 (de) | Verfahren und vorrichtung zum ankuppen von drahtpinnen | |
| EP4395948B1 (fr) | Guide de fil longitudinal pour faire avancer un certain nombre de fils d'acier parallèles | |
| EP1862234A2 (fr) | Dispositif de formage de profilés creux | |
| DE2434217A1 (de) | Verfahren zum formen eines bogenfoermigen steges fuer eine bremsbacke und vorrichtung zur durchfuehrung des verfahrens | |
| EP1609544B1 (fr) | Dispositif et procédé de préparation de plaques pour la disposition sur un cylindre d'impression |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA MK RS |
|
| 17P | Request for examination filed |
Effective date: 20100108 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20130522 |
|
| GRAJ | Information related to disapproval of communication of intention to grant by the applicant or resumption of examination proceedings by the epo deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR1 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| INTG | Intention to grant announced |
Effective date: 20130923 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 641264 Country of ref document: AT Kind code of ref document: T Effective date: 20131215 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502008010970 Country of ref document: DE Effective date: 20140116 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2447495 Country of ref document: ES Kind code of ref document: T3 Effective date: 20140312 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: T2 Effective date: 20131120 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140320 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140320 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502008010970 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| 26N | No opposition filed |
Effective date: 20140821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131231 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502008010970 Country of ref document: DE Effective date: 20140821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131231 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20081231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131120 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131120 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140221 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20161213 Year of fee payment: 9 Ref country code: NL Payment date: 20161221 Year of fee payment: 9 Ref country code: CH Payment date: 20161221 Year of fee payment: 9 Ref country code: DE Payment date: 20161213 Year of fee payment: 9 Ref country code: CZ Payment date: 20161227 Year of fee payment: 9 Ref country code: GB Payment date: 20161222 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20161221 Year of fee payment: 9 Ref country code: FR Payment date: 20161222 Year of fee payment: 9 Ref country code: AT Payment date: 20161222 Year of fee payment: 9 Ref country code: SE Payment date: 20161221 Year of fee payment: 9 Ref country code: PL Payment date: 20161220 Year of fee payment: 10 Ref country code: ES Payment date: 20161213 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NO Payment date: 20161227 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20161223 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20151231 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502008010970 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: MMEP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20180101 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 641264 Country of ref document: AT Kind code of ref document: T Effective date: 20171231 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20171231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180101 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20180831 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20171231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180101 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180102 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180703 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20190704 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171231 |