EP2310152B1 - Procédé permettant le guidage longitudinal d'un produit laminé, en particulier d'une bande d'acier laminée à chaud, et laminoir à chaud pour la mise en oeuvre de ce procédé - Google Patents
Procédé permettant le guidage longitudinal d'un produit laminé, en particulier d'une bande d'acier laminée à chaud, et laminoir à chaud pour la mise en oeuvre de ce procédé Download PDFInfo
- Publication number
- EP2310152B1 EP2310152B1 EP09777151.3A EP09777151A EP2310152B1 EP 2310152 B1 EP2310152 B1 EP 2310152B1 EP 09777151 A EP09777151 A EP 09777151A EP 2310152 B1 EP2310152 B1 EP 2310152B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rolling stock
- rolling
- hot
- stock
- rolling mill
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
- B21B45/0203—Cooling
- B21B45/0209—Cooling devices, e.g. using gaseous coolants
- B21B45/0215—Cooling devices, e.g. using gaseous coolants using liquid coolants, e.g. for sections, for tubes
- B21B45/0218—Cooling devices, e.g. using gaseous coolants using liquid coolants, e.g. for sections, for tubes for strips, sheets, or plates
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B39/00—Arrangements for moving, supporting, or positioning work, or controlling its movement, combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B39/14—Guiding, positioning or aligning work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/62—Quenching devices
- C21D1/667—Quenching devices for spray quenching
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/0221—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips characterised by the working steps
- C21D8/0226—Hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/02—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips
- C21D8/04—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing
- C21D8/0421—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of plates or strips to produce plates or strips for drawing, e.g. for deep-drawing characterised by the working steps
- C21D8/0426—Hot rolling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B37/00—Control devices or methods specially adapted for metal-rolling mills or the work produced thereby
- B21B37/74—Temperature control, e.g. by cooling or heating the rolls or the product
- B21B37/76—Cooling control on the run-out table
Definitions
- the invention relates to a method for longitudinally guiding a rolling stock, in particular a hot-rolled steel strip according to the features of the preamble of claim 1 and a hot rolling mill for carrying out the method according to the features of the preamble of claim. 8
- the rolling stock in a hot rolling mill as it leaves the finishing train, passes through a laminar refrigerating section to a reel section via a roller table.
- the rolling stock In the laminar cooling area, the rolling stock is cooled to a required reel temperature by means of water, in order to achieve a structure structure which is as uniform as possible over the width of the rolling stock and uniform strength properties.
- This temperature profile can be influenced in the sense of a homogenization by preferably one along the rolling stock and over the width of the rolling stock arranged device with shielding elements for cooling the rolling stock.
- Such a device is from the DE 3230866 C2 and from the DE 199 25 535 A1 known.
- the rolling stock is transported after leaving the finishing train of a hot rolling mill via a roller table in the direction of a reel and it passes through lying between the finishing train and the reel laminar -Kühl Symposium.
- the rolling stock is guided longitudinally and on both sides of the laminar cooling area through at least one lateral guide, which consists of parallel guide bars spaced apart from one another, in such a way that it preferably comprises a cooling device with shielding elements for a liquid cooling medium arranged above the rolling stock. is essentially exposed over the entire surface of the cooling medium.
- a uniform temperature profile is achieved with the formation of a uniform microstructure and uniform strength properties.
- the rolling stock can be guided along the laminar cooling area through a plurality of side guides.
- the side guides are, as mentioned, from both sides of the rolling stock, arranged parallel to each other and relatively movable guide rails.
- Setting the at least one side guide to the width of the rolling stock takes place in an embodiment of the invention automatically, by the fact that after leaving the finishing train, the width of the rolling stock is detected by measurement. This is followed by a coarse adjustment of the at least one side guide to the width of the rolling stock and after the head of the rolling stock has passed the side guide, the setting is made to the detected width of the rolling stock.
- the adjustment of the lateral guide transversely to the transport path of the rolling stock can be effected according to the invention as a function of the position of the cooling device preferably arranged above the rolling stock with the shielding elements for a liquid cooling medium.
- the mentioned cooling device can be aligned to the position of the side guide, always under the aspect of achieving a nearly over the width of the rolling stock constant temperature profile.
- the hot rolling mill comprises a arranged after the finishing mill of the hot rolling mill laminar cooling area with roller conveyor for transporting the rolling stock, arranged at the end of the roller table reel for winding the rolling stock and preferably arranged above the rolling stock cooling device with shielding elements for a liquid cooling medium.
- At least one lateral guide is arranged along the laminar cooling area.
- a plurality of such lateral guides may be present along the laminar cooling area.
- a wide range of the rolling stock detecting measuring device is arranged in a further embodiment of the invention, which communicates signal-transmitting with an electronic control of the hot rolling mill.
- the electronic control signal transmitting for example, hydraulic control means for acting on hydraulic piston-cylinder units in combination.
- the piston-cylinder units are the drive means for adjusting the guide rulers to about the width of the rolling stock.
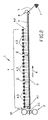
- Hot rolling mill 1 On the output side of the finishing train 2 is a roller table 3 of a laminar cooling area 4 of a plurality of cooling sections 4.3 Hot rolling mill 1 is formed.
- the rolling stock 5 On the roller table 3, the rolling stock 5 is transported in the form of a hot-rolled steel strip in the direction 6 of the arrow to a reel 7 and wound thereon. Before winding, the rolling stock 5 is deflected from its preferably horizontal transport direction 6 by means of a driver 8.
- a known side guide 9 is arranged for the rolling stock 5, which, however, serves only the edge flush reels of the rolling stock 5.
- the laminar cooling region 4 can, as shown here, consist over its longitudinal extent of a plurality of laminar cooling sections 4.3, wherein each laminar cooling section 4.3 a known cooling device 10 with deflecting elements 10.1, sa Figure 3 , may have.
- Fig.2 is the well-known from the prior art laminar cooling section 4 shown, but with the difference that between two successive laminar cooling sections 4.3 consisting of guide rulers 11.1 and 11.2 side guide 11, see also Figure 3 , Is arranged and that between the output 2.1 of the finishing train 2 and the input 4.1 of the laminar cooling area 4, a measuring device 12 for detecting the width of the rolling stock 4 is arranged.
- the measuring device 12 is, following the logic, signal-transmitting connected to an electronic control of the hot rolling mill, not shown here for processing the detected measurement result.
- signal transmitting connected to the electronic control are further, for example, not shown here control means for hydraulic piston-cylinder units, which are assigned as adjustment of existing from a first and second guide ruler 11.1 and 11.2 side guide 11.
- a cooling device 10 known per se is positioned vertically above the rolling stock 5 guided on the roller table 3.
- the cooling device 10 has shielding elements 10. 1 for a liquid cooling medium 13.
- a guide ruler 11.1 and 11.2 is respectively positioned on both sides of the rolling stock 5. Both guide rulers form the side guide 11, which, as in the Fig.2 shown, between each two consecutive laminar cooling sections 4.3 is arranged.
- Each of the guide rulers is connected to the free end of the piston rod 14.1 or 15.1 of a preferably hydraulic piston-cylinder unit 14 or 15 in conjunction to be adjusted according to the width of the rolling stock 5 to about this.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Metal Rolling (AREA)
Claims (14)
- Procédé pour le guidage longitudinal d'un produit de laminage, en particulier d'un ruban d'acier laminé à chaud sur une voie à rouleaux (3) d'un laminoir à chaud (1), qui est transporté après avoir quitté le train finisseur (2) via la voie à rouleaux en direction d'une bobineuse (7) et qui traverse une zone de refroidissement laminaire (4) s'étendant entre le train finisseur et la bobineuse, caractérisé en ce que le produit de laminage (5) est guidé en direction longitudinale et des deux côtés de la zone de refroidissement laminaire (4) par au moins un guidage latéral (11).
- Procédé selon la revendication 1, caractérisé en ce que le produit de laminage (5) est guidé en direction longitudinale et des deux côtés de la zone de refroidissement laminaire (4) par plusieurs guidages latéraux (11).
- Procédé selon la revendication 1, caractérisé en ce que la largeur du produit de laminage (5) est enregistrée de manière automatique après le passage du produit de laminage par le train finisseur (2).
- Procédé selon l'une quelconque des revendications précédentes, caractérisé en ce que les guidages latéraux correspondants (11) sont réglés à la largeur déterminée du produit de laminage, après le passage de la tête du produit de laminage (5) par le guidage latéral respectif.
- Procédé selon la revendication 4, caractérisé en ce que le réglage des guidages latéraux (11) a lieu en fonction de la largeur du produit de laminage.
- Procédé selon l'une quelconque des revendications précédentes, caractérisé en ce que la position des guidages latéraux (11) est réglée en fonction de la position d'un dispositif de refroidissement (10) agencé par-dessus le produit de laminage (5), comportant des éléments de protection (10.1) pour un milieu de refroidissement liquide.
- Procédé selon l'une quelconque des revendications précédentes, caractérisé en ce que la position d'un dispositif de refroidissement (10) agencé par-dessus le produit de laminage (5), comportant des éléments de protection (10.1) pour un milieu de refroidissement liquide est réglée en fonction de la position des guidages latéraux (11).
- Laminoir à chaud équipé d'un train finisseur, comprenant une zone de refroidissement laminaire (4) disposée après le train finisseur (2), équipée d'une voie à rouleaux (3) pour le transport du produit de laminage (5), une bobineuse (7) disposée à l'extrémité de la voie à rouleaux (3) pour l'enroulement du produit de laminage (5) et un dispositif de refroidissement (10) agencé par-dessus le produit de laminage (5) comportant des éléments de protection (10.1) pour un milieu de refroidissement liquide, caractérisé en ce qu'on dispose au moins un guidage latéral (11) le long de la zone de refroidissement laminaire (4).
- Laminoir à chaud selon la revendication 8, caractérisé en ce qu'on dispose plusieurs guidages latéraux (11) le long de la zone de refroidissement laminaire (4).
- Laminoir à chaud selon la revendication 8, caractérisé en ce qu'on dispose entre la sortie (2.1) du train finisseur (2) et l'entrée (4.1) de la zone de refroidissement laminaire (4), un mécanisme de mesure (12) qui enregistre la largeur du produit de laminage (5).
- Laminoir à chaud selon la revendication 8, caractérisé en ce que, dans le but d'obtenir une structure uniforme et des propriétés de résistance uniformes du produit de laminage (5), ledit au moins un guidage latéral (11) peut être réglé en fonction de la position du dispositif de refroidissement (10) agencé par-dessus le produit de laminage (5) comportant des éléments de protection (10.1) pour un milieu de refroidissement liquide.
- Laminoir à chaud selon la revendication 8, caractérisé en ce que, dans le but d'obtenir une structure uniforme et des propriétés de résistance uniformes du produit de laminage (5), la position du dispositif de refroidissement (10) agencé par-dessus le produit de laminage (5), comportant des éléments de protection (10.1) pour un milieu de refroidissement liquide peut être réglée en fonction de la position des guidages latéraux (11).
- Laminoir à chaud selon l'une quelconque des revendications précédentes 8 à 12, caractérisé en ce que ledit au moins un guidage latéral (11) comprend des règles de guidage (11.1, 11.2) présentes des deux côtés du produit de laminage (5), disposées parallèlement l'une à l'autre et aptes à se déplacer l'une par rapport à l'autre.
- Laminoir à chaud selon la revendication 13, caractérisé en ce que chacune des règles de guidage (11.1, 11.2) est mise en relation de travail avec un dispositif d'entraînement réalisé sous la forme d'une unité à piston/cylindre (13) qui active le déplacement parallèle des règles de guidage.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102008032932A DE102008032932A1 (de) | 2008-07-12 | 2008-07-12 | Verfahren zum Längsführen eines Walzgutes, insbesondere eines warmgewalzten Stahlbandes und Warmwalzwerk zur Durchführung des Verfahrens |
| PCT/EP2009/005074 WO2010006750A2 (fr) | 2008-07-12 | 2009-07-13 | Procédé permettant le guidage longitudinal d'un produit laminé, en particulier d'une bande d'acier laminée à chaud, et laminoir à chaud pour la mise en oeuvre de ce procédé |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2310152A2 EP2310152A2 (fr) | 2011-04-20 |
| EP2310152B1 true EP2310152B1 (fr) | 2013-06-26 |
Family
ID=41412820
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP09777151.3A Not-in-force EP2310152B1 (fr) | 2008-07-12 | 2009-07-13 | Procédé permettant le guidage longitudinal d'un produit laminé, en particulier d'une bande d'acier laminée à chaud, et laminoir à chaud pour la mise en oeuvre de ce procédé |
Country Status (9)
| Country | Link |
|---|---|
| US (1) | US20110132054A1 (fr) |
| EP (1) | EP2310152B1 (fr) |
| JP (1) | JP2011527634A (fr) |
| KR (1) | KR101332198B1 (fr) |
| CN (1) | CN102089092A (fr) |
| DE (1) | DE102008032932A1 (fr) |
| RU (1) | RU2466810C2 (fr) |
| UA (1) | UA98061C2 (fr) |
| WO (1) | WO2010006750A2 (fr) |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101879531A (zh) * | 2010-05-31 | 2010-11-10 | 北京科技大学 | 一种冷却板形可控制的热轧带钢层流冷却装置 |
| WO2012148069A1 (fr) * | 2011-04-27 | 2012-11-01 | 현대제철 주식회사 | Appareil de blocage de la vapeur |
| CN102636160B (zh) * | 2012-04-28 | 2013-11-13 | 天津二十冶建设有限公司 | 冶金工业超长距离轧线辊道螺栓整体放样方法 |
| EP2666558A1 (fr) * | 2012-05-21 | 2013-11-27 | Siemens Aktiengesellschaft | Guidage latéral pour une voie de laminage |
| EP2853315A1 (fr) * | 2013-09-26 | 2015-04-01 | Siemens VAI Metals Technologies GmbH | Dispositif de guidage de bandes métalliques avec des corps d'usure |
| CN112845619B (zh) * | 2020-11-19 | 2023-02-17 | 邯郸钢铁集团有限责任公司 | 一种减小热轧高强带钢尾部残余应力的方法 |
| CN115121632B (zh) * | 2022-07-21 | 2023-03-10 | 东北大学 | 一种热轧带钢层流冷却过程横向温度均匀化控制方法 |
| CN119926984B (zh) * | 2025-03-20 | 2026-03-03 | 常熟市龙腾特种钢有限公司 | 一种交替冷却的轧钢生产用的脱头辊道结构 |
Family Cites Families (24)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5423060A (en) * | 1977-07-23 | 1979-02-21 | Kawasaki Steel Co | Control device for roll crown while rolling |
| JPS57156830A (en) * | 1981-03-24 | 1982-09-28 | Kawasaki Steel Corp | Cooling method for rolling material |
| JPS5832511A (ja) | 1981-08-21 | 1983-02-25 | Nippon Kokan Kk <Nkk> | 厚鋼板の冷却方法 |
| JPS5924511A (ja) * | 1982-08-03 | 1984-02-08 | Kawasaki Steel Corp | 圧延材の冷却方法 |
| AT377712B (de) * | 1983-09-08 | 1985-04-25 | Voest Alpine Ag | Anlage zum warmwalzen von band- oder tafelfoermigem walzgut |
| JPH06247B2 (ja) * | 1984-10-02 | 1994-01-05 | 石川島播磨重工業株式会社 | サイドガイド装置 |
| JPS6261713A (ja) * | 1985-09-09 | 1987-03-18 | Nippon Kokan Kk <Nkk> | 熱間圧延鋼板の冷却方法 |
| SU1715461A1 (ru) * | 1989-04-14 | 1992-02-28 | Центральный научно-исследовательский институт черной металлургии им.И.П.Бардина | Отвод щий рольганг полосового прокатного стана дл транспортировани гор чекатаных полос к моталке |
| JPH0669582B2 (ja) * | 1990-10-23 | 1994-09-07 | 石川島播磨重工業株式会社 | サイドガイドの制御方法 |
| US5560236A (en) * | 1993-10-07 | 1996-10-01 | Kawasaki Steel Corporation | Method of rolling and cutting endless hot-rolled steel strip |
| JPH0810821A (ja) * | 1994-06-28 | 1996-01-16 | Nippon Steel Corp | 熱板冷却装置 |
| DE19540978A1 (de) * | 1995-11-03 | 1997-05-07 | Schloemann Siemag Ag | Produktionsanlage zum kontinuierlichen- oder diskontinuierlichen Auswalzen von Warmband |
| TW340067B (en) * | 1996-11-13 | 1998-09-11 | Ishikawajima Harima Heavy Ind | Rolled strip joining device and a hot strip mill having such a device |
| DE19718530B4 (de) * | 1997-05-02 | 2005-02-03 | Sms Demag Ag | Verfahren zum Kühlen von walzwarmem Walzgut und Vorrichtung zur Durchführung des Verfahrens und Verwendung der Vorrichtung |
| KR200288285Y1 (ko) * | 1998-12-09 | 2002-11-18 | 재단법인 포항산업과학연구원 | 강판 연속라인의 측면 가이드장치 |
| JP4337157B2 (ja) * | 1998-12-22 | 2009-09-30 | 住友金属工業株式会社 | 鋼板の冷却方法およびその装置 |
| DE19925535A1 (de) | 1999-06-04 | 2000-12-07 | Sms Demag Ag | Verstellverfahren für zwei über einem Metallband angeordnete Abschirmelemente und hiermit korrespondierende Verstellvorrichtung |
| DE19943288A1 (de) * | 1999-09-10 | 2001-03-15 | Sms Demag Ag | Verstellverfahren für zwei Abschirmelemente und zugehöriger Rollgang |
| DE10038292A1 (de) * | 2000-08-05 | 2002-02-14 | Sms Demag Ag | Produktionsverfahren und -anlage zur Erzeugung von dünnen Flachprodukten |
| DE10215229A1 (de) * | 2002-04-06 | 2003-10-16 | Sms Demag Ag | Vorrichtung zum Kühlen von Walzgut innerhalb der Kühlstrecke einer Walzanlage |
| ITBO20030076A1 (it) * | 2003-02-20 | 2004-08-21 | Packservice Srl | Macchina per la realizzazione di confezioni strip. |
| JP2005238304A (ja) * | 2004-02-27 | 2005-09-08 | Jfe Steel Kk | 熱延鋼板の製造方法 |
| DE102006024761A1 (de) * | 2006-05-27 | 2007-11-29 | Sms Demag Ag | Vorrichtung zum Messen der Breite und/oder der Bandlage eines Metallbandes oder einer Bramme |
| DE102007053523A1 (de) * | 2007-05-30 | 2008-12-04 | Sms Demag Ag | Vorrichtung zur Beeinflussung der Temperaturverteilung über der Breite |
-
2008
- 2008-07-12 DE DE102008032932A patent/DE102008032932A1/de not_active Withdrawn
-
2009
- 2009-07-13 EP EP09777151.3A patent/EP2310152B1/fr not_active Not-in-force
- 2009-07-13 JP JP2011517042A patent/JP2011527634A/ja active Pending
- 2009-07-13 KR KR1020117000789A patent/KR101332198B1/ko not_active Expired - Fee Related
- 2009-07-13 RU RU2011105132/02A patent/RU2466810C2/ru not_active IP Right Cessation
- 2009-07-13 UA UAA201101625A patent/UA98061C2/uk unknown
- 2009-07-13 CN CN2009801273183A patent/CN102089092A/zh active Pending
- 2009-07-13 WO PCT/EP2009/005074 patent/WO2010006750A2/fr not_active Ceased
- 2009-07-13 US US12/737,437 patent/US20110132054A1/en not_active Abandoned
Also Published As
| Publication number | Publication date |
|---|---|
| WO2010006750A2 (fr) | 2010-01-21 |
| KR20110019423A (ko) | 2011-02-25 |
| DE102008032932A1 (de) | 2010-01-14 |
| RU2011105132A (ru) | 2012-08-20 |
| CN102089092A (zh) | 2011-06-08 |
| UA98061C2 (uk) | 2012-04-10 |
| EP2310152A2 (fr) | 2011-04-20 |
| RU2466810C2 (ru) | 2012-11-20 |
| US20110132054A1 (en) | 2011-06-09 |
| WO2010006750A3 (fr) | 2010-03-25 |
| JP2011527634A (ja) | 2011-11-04 |
| KR101332198B1 (ko) | 2013-11-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3541564B1 (fr) | Procédé et dispositif de fabrication d'un matériau complexe sous forme de bande continue | |
| DE69102280T2 (de) | Verfahren und anlage zum herstellen von direkt einer warmwalzstrasse erzeugter stahlbandcoils mit kaltwalzeigenschaften. | |
| EP3246102B1 (fr) | Procédé et dispositif de refroidissement d'une tôle dans une section de refroidissement | |
| EP2310152A2 (fr) | Procédé permettant le guidage longitudinal d'un produit laminé, en particulier d'une bande d'acier laminée à chaud, et laminoir à chaud pour la mise en oeuvre de ce procédé | |
| EP3535069B1 (fr) | Procede permettant de faire fonctionner une installation mixte de laminage en coulee continue | |
| DE2805172A1 (de) | Vorrichtung und verfahren zum abkuehlen von metallerzeugnissen | |
| EP2651578B1 (fr) | Train de laminoir pour la production d'acier tubulaire et de bandes minces | |
| EP3234204B1 (fr) | Dispositif et procédé de traitement en continu d'une bande métallique | |
| EP2982453A1 (fr) | Réglage d'un profil de température ciblé sur une tête de bande et pied de bande devant la partie transversale d'une bande métallique | |
| DE60224211T2 (de) | Verfahren und vorrichtung zur kühlung von stahlplatten | |
| EP2344287B1 (fr) | Procédé et dispositif pour le refroidissement d'une bande préliminaire ou d'une bande d'une ligne continue métallique dans un laminoir à chaud | |
| DE112007000641B4 (de) | Kontinuierliche Kaltwalzanlage | |
| EP2445664B1 (fr) | Système et procédé pour la coulée horizontale d'une bande métallique | |
| WO2019101486A1 (fr) | Barre de refroidissement et processus de refroidissement avec taux de refroidissement variable pour tôles d'acier | |
| WO2018192968A1 (fr) | Dispositif et procédé pour le refroidissement de bandes ou de tôles métalliques | |
| EP1781428B1 (fr) | Procede et dispositif pour produire des bandes de metal | |
| DE19524729A1 (de) | Verfahren und Vorrichtung zum Walzen von Bändern mit über ihrer Breite ungleichförmige Dicken- und/oder Längenverteilung | |
| EP3941655B1 (fr) | Installation et procédé pour fabriquer un feuillard à chaud métallique | |
| WO2018158420A1 (fr) | Procédé et dispositif permettant la fabrication en continu d'un feuillard d'acier | |
| DE102018220386A1 (de) | Verfahren und Vorrichtung zum Einstellen der Solltemperaturen von Kühlsegmenten einer Stranggießanlage | |
| EP1294502B1 (fr) | Dispositif de traitement de bande | |
| DE102008063547A1 (de) | Verfahren und Vorrichtung zur Entzunderung eines Metallbandes | |
| WO2022058152A1 (fr) | Procédé et appareil de pulvérisation pour le traitement thermique de surface d'un produit métallique | |
| DE102008047029A1 (de) | Entzunderungsvorrichtung | |
| DE102020117682A1 (de) | Richtmaschine und Verfahren zum Richten eines Metallbandes oder eines flächigen Metallteils |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20110214 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA RS |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 618458 Country of ref document: AT Kind code of ref document: T Effective date: 20130715 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502009007440 Country of ref document: DE Effective date: 20130822 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130927 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130926 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130926 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20130626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 |
|
| BERE | Be: lapsed |
Owner name: SMS SIEMAG AG Effective date: 20130731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130717 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131028 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131026 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131007 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130731 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130731 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130731 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20140327 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502009007440 Country of ref document: DE Effective date: 20140327 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130713 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130713 Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130626 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20090713 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502009007440 Country of ref document: DE Representative=s name: HEMMERICH & KOLLEGEN, DE Ref country code: DE Ref legal event code: R081 Ref document number: 502009007440 Country of ref document: DE Owner name: SMS GROUP GMBH, DE Free format text: FORMER OWNER: SMS SIEMAG AG, 40237 DUESSELDORF, DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20160623 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20160722 Year of fee payment: 8 Ref country code: IT Payment date: 20160725 Year of fee payment: 8 Ref country code: GB Payment date: 20160721 Year of fee payment: 8 Ref country code: FI Payment date: 20160713 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20160721 Year of fee payment: 8 Ref country code: FR Payment date: 20160721 Year of fee payment: 8 Ref country code: SE Payment date: 20160720 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502009007440 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 618458 Country of ref document: AT Kind code of ref document: T Effective date: 20170713 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20170713 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20180330 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170713 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180201 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170714 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170713 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170713 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170713 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170713 |