EP2412501A1 - Dispositif destiné au revêtement de pièces à usiner - Google Patents
Dispositif destiné au revêtement de pièces à usiner Download PDFInfo
- Publication number
- EP2412501A1 EP2412501A1 EP11005025A EP11005025A EP2412501A1 EP 2412501 A1 EP2412501 A1 EP 2412501A1 EP 11005025 A EP11005025 A EP 11005025A EP 11005025 A EP11005025 A EP 11005025A EP 2412501 A1 EP2412501 A1 EP 2412501A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- plasma
- coating
- nozzles
- feed direction
- nozzle
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000576 coating method Methods 0.000 title claims abstract description 28
- 239000011248 coating agent Substances 0.000 title claims abstract description 24
- 239000002346 layers by function Substances 0.000 claims abstract description 14
- 238000007688 edging Methods 0.000 claims 2
- 239000002023 wood Substances 0.000 claims 2
- 239000002983 wood substitute Substances 0.000 claims 2
- 230000005855 radiation Effects 0.000 description 6
- 238000002844 melting Methods 0.000 description 5
- 230000008018 melting Effects 0.000 description 5
- 239000000463 material Substances 0.000 description 4
- 238000010438 heat treatment Methods 0.000 description 2
- 230000004913 activation Effects 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 230000006866 deterioration Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 239000012943 hotmelt Substances 0.000 description 1
- 230000001678 irradiating effect Effects 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
- 230000010355 oscillation Effects 0.000 description 1
- 238000009877 rendering Methods 0.000 description 1
- 230000002123 temporal effect Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27D—WORKING VENEER OR PLYWOOD
- B27D5/00—Other working of veneer or plywood specially adapted to veneer or plywood
- B27D5/003—Other working of veneer or plywood specially adapted to veneer or plywood securing a veneer strip to a panel edge
Definitions
- the invention relates to a device for coating workpieces.
- edge band and plate are brought together to form a joint gap in a joint zone and firmly connected to each other, wherein edge band and workpiece are thereby moved relative to each other.
- edge band is transferred to an adhesive state.
- plasma radiation has recently also been used to melt the functional layer.
- the functional layer of the edge band is heated with a radiation or flame emerging from a plasma nozzle.
- the distance between edge band and plasma nozzle is important in order to achieve an optimal melting result.
- edge band In relative movement between edge band and workpiece, therefore, the edge band is guided past the plasma nozzle, so that in the longitudinal direction of the edge band, a homogeneous irradiation is realized.
- the nozzles can not be placed arbitrarily close to each other due to space constraints, so that in the exiting rays or flames adjacent nozzles usually remains too low radiation intensity left to sufficiently melt the functional layer , Consequently, one makes do with a diagonal arrangement of the nozzles, as they are in the FIG. 2 is shown.
- the edge band 2 is guided in the direction X, the nozzles 3a are arranged at an angle to the edge band 2 in a row, which is indicated by the dashed line D.
- the individual nozzles 3a or their effective regions on the edge band 2 in the transverse direction Z of the edge strip 2 move closer to one another than would be the case with a perpendicular to the longitudinal or feed direction X of the edge band 2.
- this configuration also has shortcomings on.
- the improvement of the homogeneity in the direction Z leads to a deterioration in the homogeneity in the direction X, since the material sections of the edge band 2 melted by the individual nozzles 3a on the way to the point P, at which it comes into contact with the workpiece, have different distances have covered.
- the portion of material (in the region of the upper edge 2a) heated by the front nozzle 3a in series D travels a lesser distance to P and is warmer than the portion of material heated by the nozzle D in the row D (in the region of the lower nozzle) Edge 2b).
- the resulting temperature gradient is disadvantageous.
- the object of the present invention is therefore to provide a device for coating workpieces, in which the mentioned disadvantages are at least reduced.
- nozzles can be arranged in two parallel or inclined in each case in the same direction rows.
- the at least two rows can also be inclined in opposite directions, resulting in, for example, a V-shaped arrangement of the plasma nozzles. It is important in every case that so many nozzles are provided, that in each case the coating material lies over its full width in the effective range of the plasma nozzles.
- the openings of at least one plasma nozzle to be slit-shaped or slot-shaped, with an opening longitudinal extent, which takes place substantially transversely to the feed direction such that the coating lies completely within the effective range of the plasma nozzle. It can be provided in succession in the feed direction a plurality of nozzles with different sized or long nozzle openings in order to work with the effective range of the plasma nozzles different width coatings can.
- the plasma nozzles of all embodiments can be turned on or off individually in order to be able to use in particular coatings such as edge bands or the like with different widths transversely to the feed direction.
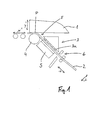
- FIG. 1 the coating process or the device used for this purpose is shown.
- the plate 1, whose narrow side is to be coated with the edge band 2 is fed in a direction X '.
- From a magazine is transported via a feeder 6 usually stored on a roll edge band 2 in the direction X towards the plate 1 and added in the region of a joining zone F to the narrow plate side and pressed against the plate 1 by means of printing tools such as the pinch roller 4, wherein the pressure primarily perpendicular to the direction X 'of the plate 1 in a direction Y' is exercised.
- P describes the area at which the edge band 2 contacts the panel 1 at the end of the joining zone F. To connect plate 1 and edge band 2, these are moved relative to each other.
- a functional layer (not shown) provided on the edge band is activated. This is done by irradiating the same with a plasma source 3 which generates plasma jets and / or a flame which emerges through plasma jets (referred to below as nozzles) 3a in the direction of the edge band 2 (essentially in the direction Y transverse to the direction X) and to strike at the same thing.
- a plasma source 3 which generates plasma jets and / or a flame which emerges through plasma jets (referred to below as nozzles) 3a in the direction of the edge band 2 (essentially in the direction Y transverse to the direction X) and to strike at the same thing.
- the distance between the edge band 2 and the plasma source 3 can optionally be varied, either by moving the source 3 or by moving the guide 5 of the edge band 2 opposite the plasma source 3 by the irradiation
- the edge band 2 is melted up or melted in the region of its functional layer as a result of the heat development, thereby rendering it "sticky” or liable.
- the so-melted edge band 2 is pressed against the narrow side of the plate 1 as described above.
- the functional layer solidifies and melts with the plate 1.
- FIG. 3 are two (not necessarily parallel) nozzle rows D with the nozzles 3a and D 'shown with the nozzles 3a', which are angled or inclined to the running direction X of the edge strip 2 and to its transverse direction Z and in particular with the direction X about the angle form ⁇ or ⁇ '.
- this arrangement is opposite to in FIG. 2
- a larger area of the edge band 2 in the effective region of the plasma nozzles 3a, 3a ' so that the melting is more effective.
- this arrangement achieves an overlap of the effective range of the nozzles of the row D and those of the row D ', which are not available in the prior art.
- banding in the longitudinal direction X on the edge band 2 can be reduced by varying the heat input over the width of the edge band.
- This can also be done by moving the rows of nozzles, such as the row D 'opposite to in FIG. 3 shown Configuration is offset by half the distance A (Z component of the distance between two nozzles 3a) in the Z direction.
- the entire nozzle assembly which is preferably provided on a block to vibrate in the Z direction, move or swing to achieve the spaces between "stripes" on the edge band 2.
- FIG. 4 An alternative is in the FIG. 4 where also combinations with the in FIG. 3 embodiment shown are conceivable.
- the nozzles are activatable such that the edge band lies in the effective range of the plasma nozzles 3a, 3a "over its entire width, which is defined by the distance in the Z direction between its upper edge 2a and its lower edge 2b (this applies to all embodiments discussed here).
- FIG. 2 well-known single-row form, that thereby the The distance between the first and the last nozzle in the running or feed direction X can be reduced, whereby the initially mentioned temporal offset between the heating of the edge region located in the effective region of the frontmost nozzle and the heating of the regions located further behind can be reduced and a more homogeneous melting result can be achieved.
- FIG. 4 shown arrangement much more flexible, especially if wider edge bands 2 are to be used.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Wood Science & Technology (AREA)
- Forests & Forestry (AREA)
- Coating Apparatus (AREA)
- Plasma Technology (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE201010032845 DE102010032845A1 (de) | 2010-07-30 | 2010-07-30 | Vorrichtung zur Beschichtung von Werkstücken |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2412501A1 true EP2412501A1 (fr) | 2012-02-01 |
| EP2412501B1 EP2412501B1 (fr) | 2013-07-24 |
Family
ID=44512493
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20110005025 Not-in-force EP2412501B1 (fr) | 2010-07-30 | 2011-06-21 | Dispositif destiné au revêtement de pièces à usiner |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP2412501B1 (fr) |
| DE (1) | DE102010032845A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2017123101A1 (fr) | 2016-01-15 | 2017-07-20 | Hyfuse Limited | Appareil et procédé d'encollage de bords |
| EP3653353A1 (fr) * | 2018-11-13 | 2020-05-20 | HOMAG GmbH | Dispositif et procédé de revêtement d'une pièce |
| US10807121B2 (en) | 2012-08-03 | 2020-10-20 | Homag Gmbh | Method and device for coating workpieces |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102017114970A1 (de) * | 2017-07-05 | 2019-01-10 | Homag Gmbh | Vorrichtung und Verfahren zum Veredeln von Werkstücken |
| EP4086052B1 (fr) * | 2021-05-07 | 2025-06-11 | Riepe GmbH & Co. KG | Agencement et procédé d'usinage d'un bord d'un panneau de meuble |
| DE102022119457A1 (de) | 2022-08-03 | 2024-02-08 | Homag Gmbh | Vorrichtung zum Beschichten eines Werkstücks |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19810680A1 (de) * | 1998-03-12 | 1999-09-16 | Kuesters Eduard Maschf | Verfahren zur Herstellung einer mehrschichtigen Folienbahn |
| DE20308202U1 (de) * | 2003-05-22 | 2003-11-27 | Dietz, Roland | Düsenaufsatz für Atmosphärenplasmaerzeuger |
| DE102006060942A1 (de) * | 2006-12-20 | 2008-06-26 | Plasma Treat Gmbh | Vorrichtung und Verfahren zur Erzeugung eines Plasmastrahls |
| DE202009009253U1 (de) * | 2008-07-21 | 2009-11-12 | Karl W. Niemann Gmbh & Co.Kg | Mit einem Kantenband versehene plattenförmige Werkstücke |
-
2010
- 2010-07-30 DE DE201010032845 patent/DE102010032845A1/de not_active Withdrawn
-
2011
- 2011-06-21 EP EP20110005025 patent/EP2412501B1/fr not_active Not-in-force
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19810680A1 (de) * | 1998-03-12 | 1999-09-16 | Kuesters Eduard Maschf | Verfahren zur Herstellung einer mehrschichtigen Folienbahn |
| DE20308202U1 (de) * | 2003-05-22 | 2003-11-27 | Dietz, Roland | Düsenaufsatz für Atmosphärenplasmaerzeuger |
| DE102006060942A1 (de) * | 2006-12-20 | 2008-06-26 | Plasma Treat Gmbh | Vorrichtung und Verfahren zur Erzeugung eines Plasmastrahls |
| DE202009009253U1 (de) * | 2008-07-21 | 2009-11-12 | Karl W. Niemann Gmbh & Co.Kg | Mit einem Kantenband versehene plattenförmige Werkstücke |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10807121B2 (en) | 2012-08-03 | 2020-10-20 | Homag Gmbh | Method and device for coating workpieces |
| WO2017123101A1 (fr) | 2016-01-15 | 2017-07-20 | Hyfuse Limited | Appareil et procédé d'encollage de bords |
| CN109070380A (zh) * | 2016-01-15 | 2018-12-21 | 希菲斯有限公司 | 封边设备和方法 |
| EP3402640A4 (fr) * | 2016-01-15 | 2019-08-14 | Hyfuse Limited | Appareil et procédé d'encollage de bords |
| EP3653353A1 (fr) * | 2018-11-13 | 2020-05-20 | HOMAG GmbH | Dispositif et procédé de revêtement d'une pièce |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2412501B1 (fr) | 2013-07-24 |
| DE102010032845A1 (de) | 2012-02-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2412501B1 (fr) | Dispositif destiné au revêtement de pièces à usiner | |
| EP1900500B1 (fr) | Buse d'air chaud | |
| EP2782725B1 (fr) | Arrangement de tuyères pour un dispositif de revetêment latéral par bandes pour alimentation d'air chaud sur les bandes couvertes d'un revetement activable par chaleur ou de thermocolle ou sur la piece et dispositif de collage de bandes comprenant un tel arrangement | |
| EP0743133B1 (fr) | Procédé et dispositif pour joindre deux pièces métalliques | |
| EP3676079B1 (fr) | Composant chauffant de soudage par contact et automate de soudage | |
| DE10214010A1 (de) | Vorrichtung und Verfahren zur Herstellung von Verbundwerkstoffen | |
| DE2812415A1 (de) | Verfahren zur herstellung verschweisster blechprofile sowie vorrichtung zur durchfuehrung dieses verfahrens | |
| DE19810680A1 (de) | Verfahren zur Herstellung einer mehrschichtigen Folienbahn | |
| DE202015106488U1 (de) | Vorrichtung zur Nachbearbeitung mindestens eines plattenförmigen Werkstücks | |
| EP2020195B1 (fr) | Procédé de fabrication d'un panneau pliable | |
| DE2414262B2 (de) | Verfahren und Vorrichtung zum Herstellen eines Nagelstreifens | |
| WO2017114792A1 (fr) | Ensemble buse et procédé de fabrication d'un ensemble buse | |
| EP3790715B1 (fr) | Dispositif et méthode de placage de chant | |
| EP2522437A1 (fr) | Dispositif et procédé de revêtement dans la zone des bords de parois fines de pièces à usiner | |
| EP1905912B1 (fr) | Procédé pour marquer des matériaux isolants en fibres de bois | |
| DE102019122423A1 (de) | Vorrichtung zur Bearbeitung eines plattenförmigen Werkstücks im Durchlauf | |
| DE102012109817A1 (de) | Beschichtungsvorrichtung für Solarmodule | |
| DE102005054351B3 (de) | Remote-Laserschweißverfahren | |
| DE102022106444A1 (de) | Verfahren und Vorrichtung zur Bestückung eines Riemens mit Bauelementen | |
| DE2552854A1 (de) | Verfahren und vorrichtung zum warmpressen von platten aus spaenen oder fasern aus holz oder anderem lignozellulosehaltigem material | |
| EP4610008A1 (fr) | Dispositif de pose d'une bande de chant et procédé de traitement d'un tel dispositif | |
| EP1877351B1 (fr) | Procede et dispositif pour usiner des surfaces de plaques de verre, de maniere a supprimer des bandes de matiere et des zones de forme differente | |
| DE102016108583B4 (de) | Vorrichtung und Verfahren zum Besprühen einer Materialbahn | |
| DE102006017063A1 (de) | Vorrichtung und Methode zum Schutz | |
| DE19542328A1 (de) | Verfahren und Einrichtung zum Herstellen eines dreidimensionalen Schichtkörpers |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20120731 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20130506 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 623132 Country of ref document: AT Kind code of ref document: T Effective date: 20130815 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502011001068 Country of ref document: DE Effective date: 20130919 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20130724 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131024 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131125 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130807 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131124 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131025 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20140425 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011001068 Country of ref document: DE Effective date: 20140425 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140621 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20150227 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140630 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140621 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140630 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20150621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140630 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20110621 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 623132 Country of ref document: AT Kind code of ref document: T Effective date: 20160621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130724 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502011001068 Country of ref document: DE Representative=s name: THIELKING & ELBERTZHAGEN PATENTANWAELTE, DE Ref country code: DE Ref legal event code: R081 Ref document number: 502011001068 Country of ref document: DE Owner name: IMA SCHELLING DEUTSCHLAND GMBH, DE Free format text: FORMER OWNER: IMA KLESSMANN GMBH HOLZBEARBEITUNGSSYSTEME, 32312 LUEBBECKE, DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20210625 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20210828 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502011001068 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220621 |