EP2845653A1 - Installation de tri de bouteilles et procédé de tri de bouteilles - Google Patents
Installation de tri de bouteilles et procédé de tri de bouteilles Download PDFInfo
- Publication number
- EP2845653A1 EP2845653A1 EP20140179720 EP14179720A EP2845653A1 EP 2845653 A1 EP2845653 A1 EP 2845653A1 EP 20140179720 EP20140179720 EP 20140179720 EP 14179720 A EP14179720 A EP 14179720A EP 2845653 A1 EP2845653 A1 EP 2845653A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- bottle
- bottles
- conveyor line
- crate
- conveying
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07C—POSTAL SORTING; SORTING INDIVIDUAL ARTICLES, OR BULK MATERIAL FIT TO BE SORTED PIECE-MEAL, e.g. BY PICKING
- B07C5/00—Sorting according to a characteristic or feature of the articles or material being sorted, e.g. by control effected by devices which detect or measure such characteristic or feature; Sorting by manually actuated devices, e.g. switches
- B07C5/04—Sorting according to size
- B07C5/12—Sorting according to size characterised by the application to particular articles, not otherwise provided for
- B07C5/122—Sorting according to size characterised by the application to particular articles, not otherwise provided for for bottles, ampoules, jars and other glassware
Definitions
- bottles which are indefinitely, i. arbitrarily populated crates are delivered, first automatically categorized according to different criteria, such as bottle geometry, bottle color, labels, etc. and then sorted, so as a result, each bottle crate as completely as possible with only one sort of bottles, usually each box type one or a few Bottle types are assigned.
- Bottles of one sort, associated with a type of box are referred to in the context of this description as boxes for boxes of this type.
- Bottles of other types of bottles are referred to herein as false bottles for boxes of this type of box.
- a gripper head which has a plurality of ordered individual gripper.
- the order of the single gripper corresponds to the order of bottle positions in the bottle crate, i. of positions in the bottle crate where bottles can be positioned.
- the gripper head moves specifically over the provided on the conveyor line bottle crate, takes with its individually controllable single grippers the respective associated false bottles, drives to a provided next to the conveyor line bottle memory and sets the faulty bottles there. He then takes according to the pattern of defects now present in the box the bottle memory a corresponding number of bottles of good, goes back to the bottle crate and fills the gaps in the bottle crate with bottles of good.
- the transfer device a plurality of functionally similar, includes independently controllable and arranged in the conveying direction of the conveyor line one behind the other gripper heads, each having exactly two individually controllable single gripper and each associated with a arranged outside the conveyor line bottle memory.
- the basic idea of the present invention is to split the large box-shaped gripper head comprising a plurality of individual grippers into a series of gripper heads with the smallest possible design.
- Each of these minimalist gripper heads has exactly two individually controllable single grippers.
- Each gripper head is suitable and in the context of the method according to the invention also intended to make only a minimal contribution to the entire sorting process. It may be a pure false bottle removal, a pure good bottle filling or an exchange of a false bottle against a good bottle in the bottle crate. When pure removal or filling process can be handled according to the number of individual gripper per rapier head, two or even a single bottle. During a replacement process, exactly one wrong bottle is exchanged for exactly one good bottle.
- Each of these three alternative elementary sorting steps can be carried out in a single cyclic movement of the gripper head, ie during one Drive from the bottle store to the bottle crate on the conveyor line and back or from the bottle crate on the conveyor line to the bottle store and back.
- An essential advantage of the invention is that the comparatively simple movement which the comparatively small and light gripper heads execute in the context of an elementary process have only a few braking and acceleration phases, where only small forces are required due to the small masses to be accelerated. As a result, considerable amounts of energy can be saved; In addition, the structural design of bearings, carriers, etc. may be smaller and thus cheaper.
- Another advantage of the invention is that a variety of crates can be sorted on a plant according to the invention.
- bottle crates vary considerably both in the number and shape and size of their bottle positions.
- a box-shaped gripper head is extremely inflexible in this respect and can only cope with a fraction of the possibly resulting empties.
- a sorting system according to the invention works completely independent of the specific box shape and can handle boxes of any box shape in any order, as long as only the respective stocking pattern is transmitted from an upstream placement detection device to the control unit.
- the conveyor line is designed as a clamping conveyor. This has the advantage that in their bottle position jammed bottles can be solved by increased force of the respective single gripper, without changing the position of the crate on the conveyor line.
- the continuous operation of the conveyor blocks avoids acceleration and deceleration processes, which in turn can lead to energy savings and smaller, ie cheaper design of bearings and carriers.
- the aforementioned synchronized movability of the gripper heads is used for this purpose.
- the conveying path is equipped with a barrier sensor which detects a starting time of each bottle crate and a clock synchronized with the conveying movement of the conveying path, both of which are connected to the control unit in an information-transmitting manner.
- the start time of each bottle crate can be detected by means of the cabinet sensor and transmitted as well as a clock signal synchronized with the conveying movement of the conveyor line clock to the control unit, which calculates the trajectories of the bottle positions of the bottle crate and the movement of the bottle crate from the stored stocking pattern of the bottle crate Gripper heads controls accordingly.
- each gripper head with an imaging sensor system and to let the control unit calculate the respective bottle positions by image processing from the sensor material obtained.
- this variant is - at least according to the current state of the art - more expensive and more prone than the preferred intended non-imaging sensor.
- the time is determined by means of a light barrier, at which the bottle crate passes a defined position on the conveyor line.
- tactile barrier sensors can be used here.
- the true position of the bottle crate on the conveyor line can be calculated at any time.
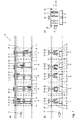
- FIG. 1 shows a highly schematic representation of a section of a bottle sorting system 10 according to the invention.
- the detail shown extends along a section of a conveying path 12, which may be formed, for example, as a conveyor belt or, preferably, as a clamping conveyor.
- the conveying direction of the conveyor line is indicated by the directional arrow 14.
- the conveyor line 12 serves the preferably continuous promotion of crates 16, which are determined by a basically undetermined assembly pattern, which, however, determined by an upstream, not shown Be Publishedungsmustererkennungs worn and transmitted to a control unit, also not shown, in the conveying path.
- the assembly pattern of each bottle crate 16 and its exact position on the conveyor line 12, which is detected with suitable sensors, can therefore be assumed to be known in the control unit. It follows that the coordinates of each individual bottle position of each bottle crate 16 on the conveyor line can be assumed to be known at virtually any time.
- Each sorting elementary station includes a side of the conveyor line 12 arranged bottle memory 20 and a gripper head 22, which is mounted along a transverse to the conveying direction and the conveyor line 12 and the bottle memory 20 spanning traverse 24 linearly movable and driven by a motor.
- the mobility of the gripper head 22 is indicated by the movement arrow 26.
- the traverse 24 is in turn displaceable parallel to the conveying direction and driven by a motor mounted on a rail system 28. The mobility of the traverse 24 is symbolized by the movement arrow 30.
- each sorting elementary station 18 is assigned a conveyor section which does not overlap with the conveyor section of the adjacent sorting elementary station.
- Each gripper head 22 has exactly two individual grippers 221, 222, which are arranged side by side in the conveying direction in the embodiment shown for better visibility. In fact, however, an arrangement is preferred transversely to the conveying direction, since this the required space in the longitudinal direction relative to the in FIG. 1 reduced variant shown. In any case, the individual grippers 221, 222 of each gripper head 22 are individually controllable, as symbolized by the vertical movement arrows 321, 322nd
- each of the sorting elementary stations with a single cyclic movement of its gripper head 22 between the currently located in the associated conveyor section section bottle box 16 and the associated bottle memory 20 change the assembly pattern of the bottle crate by either a bottle in the bottle crate 16 with a material bottle in the bottle memory 20 is replaced or by one or two false bottles removed from the bottle case 16 and converted into the bottle memory 20 or by one or two bottles of good removed from the bottle memory 20 and converted into the bottle crate 16.
- the five sorting elementary stations shown can be changed the assembly of up to ten bottle positions in a bottle crate 16. This corresponds to a change rate of approx.
- More complex tasks ie the sorting of boxes with a higher misfit quota, can be solved in different ways.
- this can be accomplished by prolonging the life of the bottle crates 16 in the individual sorting elementary stations 18.
- the conveying speed would have to be reduced, so that the traverse 24, which overlaps the working movement of the gripper head 22 synchronized with the conveying speed linear motion in the conveying direction, not outside the limits of her assigned conveyor section.
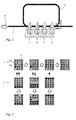
- FIG. 4 shows an embodiment of the sorting method according to the invention using the example of a bottle crate 16 with 20 bottle positions and a loading pattern as in FIG FIG. 3 shown at the top left, namely with 16 bottles of good 161, a false bottle 162 and 3 empty positions 163. This corresponds to a Fehlbe Publishedungsquote of 20%.
- the bottle storage 20 of the first sorting elementary station 18 which is also preferably designed as a bottle crate, more preferably as a bottle crate of the same type as the bottle crate 16 to be sorted, sixteen goods bottles 161 (relative to the bottle crate 16 to be sorted) and four false bottles 162 according to the in FIG. 3 (Line 2 first field) shown mounting pattern are arranged.
- the bottle memory 20 is thus full, so that no pure implementation of bottles from the bottle case 16 in the bottle memory 20 is possible.
- the bottle memory 20 has an excess of good bottles 161, which is negative in terms of flexible responsiveness to different sorting tasks.
- Cheaper would be an approximate equal distribution of good and false bottles and the presence of at least some empty positions in the bottle memory 20.
- the control unit controls the sorting elementary station therefore so that a maximum number of good bottles 161, ie two pieces, converted from the bottle memory 20 in the bottle crate 16 become.
- the bottle stores 20 are preferably taken from the two food bottles in the same spatial relation as there are adjacent empty positions 163 in the bottle box 16 to be sorted.
- the resulting population pattern of the bottle crate 20 is in FIG. 3 shown in the bottom line on the far left.
- the resulting assembly pattern of the bottle crate 16 to be sorted is in FIG. 3 in line 1 shown as a second partial image.
- the gripper head 22 With a slight position correction, the gripper head 22 then brings its first single gripper 221 over the resulting empty position 163 and sets the first gripper 221 located on the material bottle 161 there. Finally, the gripper head 22 moves back to the bottle memory 20 and sets with his second single gripper 222 from this held false bottle to an empty position in the bottle memory 20 from. It can basically be any empty position; Preferably, spatially contiguous clusters of bottles of the same type are formed.
- the resulting pop-up pattern of the bottle memory 20 is shown in FIG FIG. 3 in line 3, second partial image shown.
- the resulting assembly pattern of the bottle crate 16 to be sorted is in FIG. 3 shown in line 1 third field.
- control unit determines the order of the individual sorting steps and distributes them to the different sorting elementary stations.
- criteria according to which the control unit determines the order of the individual sorting steps and distributes them to the different sorting elementary stations can be adapted by the person skilled in the art to the requirements of the individual case.
- different strategies can be advantageous.
- the number of actually used sorting elementary stations is not limited in principle.
Landscapes
- Sorting Of Articles (AREA)
- Branching, Merging, And Special Transfer Between Conveyors (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
- Specific Conveyance Elements (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE201310109839 DE102013109839B4 (de) | 2013-09-09 | 2013-09-09 | Flaschensortieranlage und Verfahren zum Sortieren von Flaschen |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2845653A1 true EP2845653A1 (fr) | 2015-03-11 |
| EP2845653B1 EP2845653B1 (fr) | 2016-03-02 |
Family
ID=51302636
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP14179720.9A Active EP2845653B1 (fr) | 2013-09-09 | 2014-08-04 | Installation de tri de bouteilles et procédé de tri de bouteilles |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP2845653B1 (fr) |
| DE (1) | DE102013109839B4 (fr) |
| ES (1) | ES2573455T3 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102018212254A1 (de) * | 2018-07-24 | 2020-01-30 | Krones Aktiengesellschaft | Handhabungs- und/oder Verpackungsvorrichtung und Verfahren zum Verpacken von Artikeln |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0569689A2 (fr) | 1992-04-15 | 1993-11-18 | Hermann Kronseder | Procédé et dispositif de tri de bouteilles |
| DE10244804B3 (de) | 2002-09-26 | 2004-01-15 | Recop Elektronic Gmbh | Verfahren zum Aussortieren von Fehlflaschen aus einem ersten auf einer Kastenbahn geförderten Flaschenkasten und Entnahmevorrichtung zur Durchführung des Verfahrens |
| EP1445038A2 (fr) * | 2003-02-07 | 2004-08-11 | Recop Electronic GmbH | Procédé de tri de bouteilles à partir de caisses transportées sur un premier convoyeur et dispositif d'extraction pour la réalisation du procédé |
| DE102005014300A1 (de) * | 2005-03-24 | 2006-09-28 | Recop Electronic Gmbh | Erkennungseinrichtung zum Erkennen von Leerflaschen und Verfahren zur Erkennung von Leerflaschen |
-
2013
- 2013-09-09 DE DE201310109839 patent/DE102013109839B4/de not_active Expired - Fee Related
-
2014
- 2014-08-04 ES ES14179720.9T patent/ES2573455T3/es active Active
- 2014-08-04 EP EP14179720.9A patent/EP2845653B1/fr active Active
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0569689A2 (fr) | 1992-04-15 | 1993-11-18 | Hermann Kronseder | Procédé et dispositif de tri de bouteilles |
| DE10244804B3 (de) | 2002-09-26 | 2004-01-15 | Recop Elektronic Gmbh | Verfahren zum Aussortieren von Fehlflaschen aus einem ersten auf einer Kastenbahn geförderten Flaschenkasten und Entnahmevorrichtung zur Durchführung des Verfahrens |
| EP1445038A2 (fr) * | 2003-02-07 | 2004-08-11 | Recop Electronic GmbH | Procédé de tri de bouteilles à partir de caisses transportées sur un premier convoyeur et dispositif d'extraction pour la réalisation du procédé |
| DE10305072B3 (de) | 2003-02-07 | 2004-08-19 | Recop Elektronic Gmbh | Verfahren zum Aussortieren von Fehlflaschen aus einem auf einer Kastenbahn beförderten Flaschenkasten und Entnahmevorrichtung |
| DE102005014300A1 (de) * | 2005-03-24 | 2006-09-28 | Recop Electronic Gmbh | Erkennungseinrichtung zum Erkennen von Leerflaschen und Verfahren zur Erkennung von Leerflaschen |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2845653B1 (fr) | 2016-03-02 |
| DE102013109839B4 (de) | 2015-03-19 |
| ES2573455T3 (es) | 2016-06-08 |
| DE102013109839A1 (de) | 2015-03-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2822883B1 (fr) | Installation et procédé permettant d'usiner des lentilles optiques | |
| EP2792626B1 (fr) | Procédé et dispositif de regroupement | |
| EP3853156B1 (fr) | Procédé et dispositif d'acheminement de produits d'un premier processus vers un second processus dans une installation d'emballage | |
| EP3374170B1 (fr) | Procédé, installation et système pour le traitement de lentilles optiques | |
| EP1522508B1 (fr) | Dispositif de séparation, de synchronisation et d'accumulation | |
| EP3877306B1 (fr) | Dispositif pour regrouper des contenants | |
| DE102008020622A1 (de) | Vorrichtung und Verfahren zum Umsortieren von Stückgutzusammenstellungen | |
| DE102009003845A1 (de) | Vorrichtung und Verfahren zum definierten Zusammenführen von Gebinden und/oder Gebindegruppen | |
| EP3437745B1 (fr) | Trieur matriciel | |
| EP2586712A1 (fr) | Procédé et dispositif d'insertion de produits dans des récipients dans une suite de robots | |
| AT524109A1 (de) | Vorrichtung und ein Verfahren zur Kommissionierung von Artikeln | |
| WO2020200716A1 (fr) | Dispositif de stockage temporaire et procédé de stockage temporaire de récipients | |
| EP4313810A1 (fr) | Appareil et procédé de création d'espacements entre des groupes individuels de marchandises transportées pendant le transport simultané des groupes de marchandises transportées | |
| DE102017118928A1 (de) | Lagenbildungs- und Palettiermodul und Verfahren zum Gruppieren und Palettieren von Stückgütern | |
| EP3770086A1 (fr) | Procédé et dispositif de manipulation des marchandises déplacées les unes après les autres dans au moins une rangée | |
| EP3770085A1 (fr) | Procédé et dispositif de manipulation de marchandises déplacées les unes après les autres dans au moins une rangée | |
| EP2845653B1 (fr) | Installation de tri de bouteilles et procédé de tri de bouteilles | |
| EP2021982A1 (fr) | Dispositif et procede pour le transport successif d'une pluralite de cartes a puces gsm | |
| WO2019076708A1 (fr) | Procédé et dispositif de manipulation et/ou de regroupement de marchandises de détail | |
| EP3677396A1 (fr) | Dispositif et procédé d'usinage de bords de pièces tavulaires | |
| EP3623323A1 (fr) | Procédé et dispositif de manipulation des marchandises, des articles et / ou des emballages | |
| DE102021107087A1 (de) | Vorrichtung und Verfahren zur Erzeugung von Abständen zwischen einzelnen Förderguteinheiten bei gleichzeitigem Transport der Förderguteinheiten | |
| EP0646055A1 (fr) | Procede et dispositif permettant de transferer des pieces | |
| AT514673B1 (de) | Verfahren zum Steuern einer Fertigungsanlage | |
| EP3999455A1 (fr) | Dispositif de palettisation et procédé de palettisation de charges isolées |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 17P | Request for examination filed |
Effective date: 20141205 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20150610 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20151002 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 777631 Country of ref document: AT Kind code of ref document: T Effective date: 20160315 Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502014000412 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: ROSENICH PAUL; KUENSCH JOACHIM PATENTBUERO PAU, LI |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2573455 Country of ref document: ES Kind code of ref document: T3 Effective date: 20160608 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160603 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160602 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160702 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160704 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502014000412 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160831 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| 26N | No opposition filed |
Effective date: 20161205 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160602 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20170428 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160804 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160804 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502014000412 Country of ref document: DE Representative=s name: FIEDLER, OSTERMANN & SCHNEIDER - PATENTANWAELT, DE Ref country code: DE Ref legal event code: R082 Ref document number: 502014000412 Country of ref document: DE Representative=s name: FIEDLER, OSTERMANN & SCHNEIDER, DE Ref country code: DE Ref legal event code: R081 Ref document number: 502014000412 Country of ref document: DE Owner name: VISION-TEC PATENT GMBH, DE Free format text: FORMER OWNER: VISION-TEC GMBH, 34277 FULDABRUECK, DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20140804 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PUE Owner name: VISION-TEC PATENT GMBH, DE Free format text: FORMER OWNER: VISION-TEC GMBH, DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| REG | Reference to a national code |
Ref legal event code: PC2A Effective date: 20180723 Ref country code: ES Ref legal event code: PC2A Owner name: VISION-TEC PATENT GMBH Effective date: 20180723 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: PD Owner name: VISION-TEC PATENT GMBH; DE Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), ASSIGNMENT; FORMER OWNER NAME: VISION-TEC GMBH Effective date: 20180611 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 777631 Country of ref document: AT Kind code of ref document: T Owner name: VISION-TEC PATENT GMBH, DE Effective date: 20180719 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160302 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20180804 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180804 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PCAR Free format text: NEW ADDRESS: ROTENBODENSTRASSE 12, 9497 TRIESENBERG (LI) |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20250821 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20250917 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250625 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250829 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20250819 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20250901 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20250722 Year of fee payment: 12 |