EP3936808A1 - Tube ailettes et son procédé de fabrication - Google Patents
Tube ailettes et son procédé de fabrication Download PDFInfo
- Publication number
- EP3936808A1 EP3936808A1 EP21183932.9A EP21183932A EP3936808A1 EP 3936808 A1 EP3936808 A1 EP 3936808A1 EP 21183932 A EP21183932 A EP 21183932A EP 3936808 A1 EP3936808 A1 EP 3936808A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- section
- cross
- band
- strip
- finned tube
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images


Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F1/00—Tubular elements; Assemblies of tubular elements
- F28F1/10—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses
- F28F1/12—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses the means being only outside the tubular element
- F28F1/34—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses the means being only outside the tubular element and extending obliquely
- F28F1/36—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses the means being only outside the tubular element and extending obliquely the means being helically wound fins or wire spirals
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C37/00—Manufacture of metal sheets, rods, wire, tubes, profiles or like semi-manufactured products, not otherwise provided for; Manufacture of tubes of special shape
- B21C37/06—Manufacture of metal sheets, rods, wire, tubes, profiles or like semi-manufactured products, not otherwise provided for; Manufacture of tubes of special shape of tubes or metal hoses; Combined procedures for making tubes, e.g. for making multi-wall tubes
- B21C37/15—Making tubes of special shape; Making tube fittings
- B21C37/22—Making finned or ribbed tubes by fixing strip or like material to tubes
- B21C37/26—Making finned or ribbed tubes by fixing strip or like material to tubes helically-ribbed tubes
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F2275/00—Fastening; Joining
- F28F2275/06—Fastening; Joining by welding
- F28F2275/067—Fastening; Joining by welding by laser welding
Definitions
- the invention initially relates to a finned tube with a tube body.
- finned tubes are used in heat exchangers and typically have fluid, for example heated water, running through them for this purpose.
- the tubes have ribs to improve the thermal conductivity.
- the ribs are rolled out of the walls of the tubular body by being acted upon by packs of disks, this having the disadvantage that the ribs cannot be particularly high, which is fundamentally desirable.
- the second type of finned tube generic to the present invention consists of tube bodies to which a separate band of the same material as the tube body or of a different material is fed, the band being fixed to the outside of the tube body, typically with the aid of welded by a laser.
- the strip normally protrudes from the surface of the pipe base body at a 90° angle, at least in cross section (which is usually completely homogeneous).
- the invention solves the problem with the features of claim 1, in particular with those of the characterizing part, and is accordingly characterized in that the fixed band has a cross-section that tapers, at least in sections.
- the idea of the invention is to provide a band with a more stable cross-sectional shape, in particular a wider foot area.
- the band in contrast to a conventional band with a point-symmetrical cross section having a deformed cross section.
- the cross section of the strip can be trapezoidal, for example, but no longer point-symmetrical.
- the band can be acted on before it is attached to the tubular body in such a way that the sides of the band are deformed towards one another (wedge-shaped).
- the strip can be moved through two roller bodies, for example, in order to achieve a corresponding deformation.
- the band can then have a wider base area than the apex area.
- the band is widened in the foot area and made narrower in the crown area. This leads to the already mentioned trapezoidal shape.
- the tape has a particularly wide contact area, in particular in the foot area of the tape, due to the tapering, a more stable attachment to the pipe base body can take place.
- Another advantageous effect of a broadened foot area or a cross section that tapers outwards is that during a welding process (for attaching the strip to the pipe body), a molten pool is created that, compared to the molten pool of a strip with a conventional, undeformed Cross-section is flatter, so it does not extend as far into the wall of the tubular body as with a conventional band.
- the molten pool is deeper and penetrates further into the wall of the pipe body.
- a tapering rib is used for a tubular body with a predetermined wall thickness
- the advantage of the design according to the invention can be seen in the fact that the wider foot area makes it possible to achieve an overall more stable design, in particular such that the tubular body is protected during the process of attaching the band is faster to rotate, since the tape with a widened foot area is more tolerant of high rotational speeds of the tubular body. Overall, this saves time when attaching the tape to the tubular body.
- a band designed according to the invention is also more tolerant of subsequent reshaping of the finned tube.
- a finned tube is typically produced by ribbing an essentially straight tube body, with the finished, i.e. also essentially straight, finned tube then—at least in some applications—being formed, e.g. into a helical shape, in which it is installed in a heat exchanger will.
- the strip should have a cross section that tapers, at least in sections.
- the meant cross-section is in particular orthogonal to Longitudinal direction of the belt aligned (substantially orthogonal to the conveying direction).
- Conventional belts typically have a substantially rectangular (possibly rounded at the edges) cross-section, with two opposite sides and two opposite, shorter edges. In particular, the opposite sides are aligned parallel to one another.
- a tapering cross section means first of all that the sides no longer run parallel (at least not over the entire width of the strip).
- the tapering cross section means that the band is now wider at one edge, which can also be designated in particular as the foot area, than at the opposite edge, which can also be designated in particular as the apex area.
- a finned tube with a band is also to be understood that, although it tapers from its base area to its apex area, either overall or in sections, it becomes wider in an area in between, for example (in particular if the apex area is narrower than the foot area of the band).
- the fixed band preferably tapers radially outwards with respect to the basic pipe body, in particular so that the connection area of the basic pipe body is particularly wide.
- the band is fixed to the pipe body, which means that the rib is not rolled out of the pipe body.
- the band is welded, in particular a laser is used for this purpose, for example a fiber laser (or any other laser suitable for the application). Which laser is used can depend, in particular, on the materials selected for the strip and the pipe body.
- the basic pipe body and the band can in principle consist of different materials or, in special cases, of the same material.
- Band and/or finned tube are typically made of metal.
- the tape can be made of copper or aluminum, whose thermal conductivity is particularly suitable for use in heat exchangers.
- the band can also consist of a different material, for example stainless steel, aluminum, titanium or carbon steel.
- the pipe body can typically be made of copper, since this is considered a material that is particularly well suited for harmless contacting or conducting process water.
- the tubular body can be made of another suitable material, such as stainless steel or aluminum.
- This can, for example, be wound helically around the main pipe body.
- the bands can in particular be bands of the same type (ie the same material, the same cross section, etc.) or also different bands (e.g. different material and/or different cross section).
- a laser beam is typically radiated into the contact area between the tube body and the strip. It irradiates both parts of the pipe body and the strip (namely to partially melt both bodies to produce a fastening welding plasma or a weld pool).
- the strip in particular already has a (at least in sections) tapering cross-section before it is welded to the pipe base body.
- the tapering cross section should therefore be detectable independently of the solidified melt.
- the strip material is initially in an endless form (e.g. as a coil or similar) and is fed to the pipe base body, which is typically suspended in a rotating manner.
- the pipe base can therefore take the band with it during the ribbing process, such that the band, in particular under tension, is placed essentially helically on the pipe base and welded there by the laser.
- the entire finned tube can be cut to the desired length and/or then converted into a different, final shape, for example a helical shape or an ⁇ shape, if desired.
- the tubular body is typically in a straight, linear, rod-like shape during the fining process.
- it can in particular be rotated during the ribbing process, for which purpose it can be clamped at its ends or applied to a mandrel.
- the tape is typically brought up to the basic tubular body transversely to the direction of the longitudinal extent of the basic tubular body (that is to say tangentially).
- pipe bodies can have completely different diameters of between 5 and 150 mm, for example.
- the wall thickness of the pipe body can also vary accordingly (from fractions of a millimeter to several millimeters).
- the height of the ribs or band is normally between 1 and 40 mm.
- the ribs of the fixed bands protrude approximately vertically, ie at an angle of 90°, from the (still straight) pipe body surface.
- this essentially means that the central perpendicular or central axis (relative to the cross section) protrudes approximately radially from the pipe base body.
- the finned tube according to the invention can in particular also provide a twist structure on the inside of its tube. This can be before or after the ribbing process or during the ribbing process be produced (e.g. by pressing through from the outside).
- the finished finned tubes can in particular be installed in heat exchangers or assembled into such or the like.
- the band is fixed in its foot area to the tubular body.
- the cross-section of the band tapers with increasing distance from the foot area.
- the cross section tapers radially away from the pipe body.
- the cross section is wider in the area of the tubular body than at a distance from it.
- the cross section tapers essentially monotonically. This means that the cross-section never increases in width from its wider area to its narrower area. It may well remain the same over a range.
- the cross-section narrows strictly monotonically, which then means that the cross-section exclusively decreases (without staying the same in sections or becoming larger).
- This monotonous tapering preferably takes place outwards, ie with increasing distance from the foot area.
- the cross section of the band does not change over the entire length of the pipe or band but remains constant.
- the cross section is essentially trapezoidal. So he knows in particular two sides which are not parallel but tilted to one another at a certain angle. The upper and lower edges can also be essentially parallel.
- the wording “substantially” means in particular that a trapezoidal shape is recognizable. Very small deviations from a trapezoidal shape are of course acceptable. It's about the overall impression.
- the cross section can be essentially wedge-shaped.
- a wedge shape is described by the two sides or flanks of a rib or band that are tilted relative to one another.
- the wedge shape can correspond to the cross section of a cone or a truncated cone.
- the band is fixed to the pipe body by means of a fastening melt.
- the tapering cross section described in the main claim then does not relate to this melting range, which can be present in any conventional, welded pipe.
- the idea is to be understood in such a way that the strip also has a tapering cross-section apart from or independent of the melt (a strip with a rectangular cross-section, which is simply widened by a melt, is not meant).
- the cross section is essentially mirror-symmetrical.
- the cross-section of the strip means that cross-section in which the height clearly exceeds the width, in particular by at least twice or three times (only to prevent a misinterpretation, according to which the cross-section is parallel would put to the side of the tape).
- the cross section tapers by a maximum of 50 percent. This means in particular that the rib or band cross-section in its apex area is at most half as wide as in its base area.
- the cross section tapers by a maximum of 35 percent, so that the width of the apex area is at least 65 percent of the width or more compared to the base area.
- the strip has rolled flanks that are tilted relative to one another.
- the flanks can therefore be machined, namely rolled, in such a way that they no longer run parallel but are arranged tilted relative to one another, ie have a smaller spacing in the area of one edge than in the area of the opposite edge.
- the invention also achieves the stated object with a method according to patent claim 9 and is accordingly characterized in particular by the steps of fixing a band to a tubular base body, the band to be fixed having a cross-section that tapers, at least in sections. All the advantages and explanations presented so far in connection with the finned tube according to the invention should not be repeated explicitly for claim 9 at this point, but apply to it as well.
- the band can be fixed, for example, in its foot area to the pipe base body, with the cross section narrowing as the distance from the foot area increases.
- this comprises a method step, after which the strip undergoes a cross-sectional deformation towards a tapering cross-section before it is fixed (on the pipe base body).
- the band that has been deformed in cross section in this way can then be fixed to the tubular body in a conventional manner.
- a rolling process or a rolling tool can be used.
- the tool used can advantageously have two contact, rolling or pressing surfaces, each acting on an opposite side of the strip to achieve the deformation.
- the two said surfaces can advantageously assume an angle of attack relative to one another, which later essentially corresponds to the tilting angle of the two sides of the belt relative to one another.
- the surfaces can, for example, be provided by rollers or presses or the like.
- a rolling tool is used in which two rolls are arranged tilted with respect to their axis relative to one another.
- FIG. 2 1 shows a finned tube 10 that has already been completed and which has basically been manufactured from two separate pieces: First of all, a tube base body 12 is provided, which is designed as a straight round tube. A (copper) strip 13 (alternatively an aluminum strip) is wound helically around the base body 12 and welded to the tubular base body 12 . The band 13 thus forms an endless rib 13' (the rib 13' of course actually having a finite, fixed length; in other words, the rib 13' is designed to be continuous).
- Volume 13 can be proven 1 the ends 14 and 15 of the tubular body 12 are free and is welded to the surface 16 of the tubular body 12. As already mentioned and particularly visible at the left-hand end 15 of the tubular body in the partially transparent illustration, this is hollow with a wall thickness d and a diameter D.
- the rib 13′ here has a rib height h.
- the average distance a between two adjacent rib sections can - vary - depending on the application.
- the rib 13 ′ or the band 13 has a cross-sectional shape that tapers with increasing distance from the pipe base body 12 . Consequently, the cross-section of the band 13 according to 3 designed essentially trapezoidal.
- band 13 has undergone a forming process with regard to its cross section before it is attached to the tubular base body 12, which will be described in more detail later.
- the melt 18 can partly consist of material both of the pipe base body 12 and of the strip 13 or the rib 13' (on the underside thereof).
- the section 17 of the rib 13' shown on the right is located further forward in the ribbing direction B (as a section that has already been defined) than in 4 also shown section 17'.
- This section 17' of the rib 13' or band 13 is 3 welded just in the contact area 19 (which is substantially angled due to the straight tube surface 16 and the straight side edge 20 of the rib 13').
- a laser beam 21 strikes an in 3 not shown laser at an angle ⁇ , in particular a small angle ⁇ , onto the contact area 19.
- the laser beam 21 irradiates both material of the band 13 or the rib 13 'or the section 17' as well as material of the tubular body 12, in particular its surface 16.
- the left-hand section according to FIG 4 so to speak, represents the state of welding of a section of the tape and the right side accordingly 4 then the finished, welded state of a section of the band. Further sections of the strip would of course follow, in particular in the ribbing direction B (and thus already welded) with a defined rib pitch.
- figure 5 shows in a view, roughly according to 4 , an enlarged, exemplary detail from a modified finned tube with a rib 13 'of a first band 13 (which rib approximately that of 4 corresponds), and with a second rib 23 of a second, separate, conventional band.
- the rib 13 ′ has the taper or trapezoidal shape according to the invention and tapers in the radial direction R with increasing distance from the pipe base body 12 .
- the rib 23 has a substantially rectangular cross-sectional shape and is not tapered.
- both bands which differ in cross-section, can of course (alternately) be fixed to the same tubular base body 12 .
- the rib 13' has a greater base width f in its base region 22 than the base width f' of the rib 23.
- the crest width s of the rib 13' is smaller than that of the rib 23 with the crest width s'.
- the rib 13' has a wider base region 22 than the rib 23, although exactly the same material is used (quantitatively) to form the rib 13' or the band 13 as to form the rib 23.
- This foot area 22 ensures, in particular, that the rib 13' is held more stably and securely on the wall 24 of the pipe base body 12 and, moreover, also ensures a higher tolerance for material weaknesses, such as signs of corrosion in the foot area 22.
- a material weakening 25 is indicated for both ribs 13' and 23 with a dashed line.
- figure 5 shows that although these material weakenings 25 are essentially the same size in absolute terms, they extend over the base area 22 of the ribs 13' and 23 to different extents in percentage terms. In other words, such a material weakening 25 (percentage) has a much greater influence on the stability of the foot area 22 of the rib 23 than on that of the rib 13'.
- FIG. 5 it can be seen schematically that the wall thickness d of the tube base body 12 for a finned tube which would only have fins 13 ′ from the strip 13 could be selected to be significantly smaller without the melt 18 passing through the wall 24 .
- ribs 23 from conventional strips requires a thicker wall 24, namely, for example, that which is shown in figure 5 is indicated with d.
- the wall thickness d can no longer be reduced or can hardly be reduced when using ribs 23, whereas this would be possible without further ado if only formed strip material 13 was used.
- ribs 13' is still advantageous in contrast to the use of ribs 23, because in this case the pipe base body 12 can be rotated faster during the ribbing with strip material and a faster ribbing done. This has to do in particular with the fact that the rib 13 ′ has a wider foot area 22 and possibly also with the fact that the solidified melt does not extend quite as far into the wall 24 of the basic pipe body 12 .
- a usual rib height can typically assume a value h of between 1 mm and 50 mm, typically between 3 mm and 33 mm.
- Typical, average widths b and b' can have values of 0.1 to 2 mm, for example.
- the ratio of the crest width s to the base width f in figure 5 is not shown to scale.
- the foot width f exceeds the crown width s by a maximum of 50 percent, in particular a maximum of 35 percent.
- a crest width of s ⁇ 0.5 mm and a root width f of approximately 0.6 mm to 0.8 mm may be assumed for the rib 13' and the band 13, respectively.
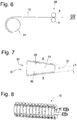
- the strip material can first be stored and made available as endless material from a coil 27 .
- the strip 13 (still with a conventional, typically rectangular cross-section) can be fed from the coil 27 to a rolling device 28, in particular by machine.
- the rolling device 28 can, for example, provide two associated rolling bodies 5 and 6 (in particular in the manner of cylindrical rollers), through which the strip 13 is passed.
- an essentially wedge-shaped gap 31 is formed between the two roller contact surfaces 29 and 30, through which the strip can slide with respect to the figure plane of FIG 7 is passed through orthogonally.
- a rolling process takes place here, which ensures that the width of the strip 13 is reduced at a first strip edge 32 .
- the strip width can increase at an opposite second strip edge 33 (or in an alternative exemplary embodiment also remain the same, for example if the material is compressed). However, this is not decisive for the invention at all.
- the band 13 according to the invention is more tolerant of such deformations of the finned tube 10, in particular since the contact area 19 between the fin and the basic tube body is larger.
- the invention includes all versions in which at least one band with a tapering cross section is fixed to a raw base body (cf. 4 ) or several bands, some with different cross-sections (cf. figure 5 ).
Landscapes
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Mechanical Engineering (AREA)
- Geometry (AREA)
- Thermal Sciences (AREA)
- General Engineering & Computer Science (AREA)
- Heat-Exchange Devices With Radiators And Conduit Assemblies (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102020117930.8A DE102020117930A1 (de) | 2020-07-07 | 2020-07-07 | Rippenrohr und Verfahren zu dessen Herstellung |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP3936808A1 true EP3936808A1 (fr) | 2022-01-12 |
Family
ID=77206918
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP21183932.9A Withdrawn EP3936808A1 (fr) | 2020-07-07 | 2021-07-06 | Tube ailettes et son procédé de fabrication |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP3936808A1 (fr) |
| DE (1) | DE102020117930A1 (fr) |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2667337A (en) * | 1947-08-06 | 1954-01-26 | Chapman Everett | Finned element for thermal or heat transfer purposes |
| US3047712A (en) * | 1961-02-23 | 1962-07-31 | American Mach & Foundry | Method and apparatus for welding striplike material to curved surfaces |
| US4227572A (en) * | 1978-03-27 | 1980-10-14 | Seton-Scherr, Inc. | Finned tubing |
| WO2002033340A2 (fr) * | 2000-10-19 | 2002-04-25 | Ibc Corporation | Ailette effilee et son procede de formation |
| EP1729079A1 (fr) * | 2005-05-30 | 2006-12-06 | Son S.R.L. | Mèthode de production d'une unité d'échange de chaleur pour un générateur de vapeur à récupération de chaleur , une unité d'échange de chaleur, un générateur de vapeur à récupération de chaleur et un tube pour une unité d'échange de chaleur |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19628745A1 (de) | 1996-07-17 | 1998-01-22 | Kme Schmoele Gmbh | Verfahren zur Herstellung eines Rippenrohrs und Rippenrohr |
-
2020
- 2020-07-07 DE DE102020117930.8A patent/DE102020117930A1/de not_active Withdrawn
-
2021
- 2021-07-06 EP EP21183932.9A patent/EP3936808A1/fr not_active Withdrawn
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2667337A (en) * | 1947-08-06 | 1954-01-26 | Chapman Everett | Finned element for thermal or heat transfer purposes |
| US3047712A (en) * | 1961-02-23 | 1962-07-31 | American Mach & Foundry | Method and apparatus for welding striplike material to curved surfaces |
| US4227572A (en) * | 1978-03-27 | 1980-10-14 | Seton-Scherr, Inc. | Finned tubing |
| WO2002033340A2 (fr) * | 2000-10-19 | 2002-04-25 | Ibc Corporation | Ailette effilee et son procede de formation |
| EP1729079A1 (fr) * | 2005-05-30 | 2006-12-06 | Son S.R.L. | Mèthode de production d'une unité d'échange de chaleur pour un générateur de vapeur à récupération de chaleur , une unité d'échange de chaleur, un générateur de vapeur à récupération de chaleur et un tube pour une unité d'échange de chaleur |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102020117930A1 (de) | 2022-01-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE19643137C2 (de) | Wärmeübertragungsrohr mit gerillter Innenfläche und Verfahren zum Herstellen desselben | |
| DE3220029C2 (fr) | ||
| DE2657294A1 (de) | Reibungs-schweissverfahren | |
| DE69312807T2 (de) | Verfahren und Vorrichtung zum Herstellen einer rohrförmigen Zahnstange | |
| DE19861391B4 (de) | Verfahren zum Formen einer Nabenscheibe und Drückrolle zur Verwendung beim Formen einer Nabenscheibe | |
| DE10196332B4 (de) | Fertigungsvorrichtung für ein gekrümmtes Metallrohr mit einem beliebig geformten Querschnitt und Verfahren zur Herstellung eines gekrümmten Metallrohres und einer gekrümmten Metallstange | |
| DE2714485A1 (de) | Verfahren zum walzen von breitflansch- metallprofilen | |
| CH704438B1 (de) | Verfahren zur Herstellung einer Nocke für eine Nockenwelle. | |
| EP2212039B1 (fr) | Procédé de fabrication d'un profilé à partir d'un feuillard métallique plat | |
| DE1940341B2 (de) | Verfahren und Einrichtung zum Herstellen von Metalleisten, insbesondere von rohrförmigen Schweißelektroden, aus einem Stabmaterial | |
| DE2303192A1 (de) | Rippenrohr sowie verfahren und vorrichtung zu seiner herstellung | |
| DE2605236C2 (de) | Verwendung eines Lochdorns und einer Matrize zum Herstellen eines Lochstückes | |
| EP2156870B1 (fr) | Grand huit doté d'éléments de rail développés comme un colombage | |
| DE2803273A1 (de) | Rippenrohr sowie verfahren und vorrichtung zu dessen herstellung | |
| DE2932964C2 (fr) | ||
| DE3019592C2 (de) | Vorrichtung zum Bearbeiten von Stahlrohren | |
| EP3391978A1 (fr) | Procédé de fabrication d'un tube à ailettes et d'un échangeur thermique | |
| EP0014474B1 (fr) | Procédé pour la fabrication d'un tube | |
| DE102020117930A1 (de) | Rippenrohr und Verfahren zu dessen Herstellung | |
| DE2532143A1 (de) | Metallischer waermeuebertrager, insbesondere rohr, und verfahren zu seiner herstellung | |
| DE3873829T2 (de) | Verfahren zur herstellung eines metallrohres mit spiralrippen. | |
| DE102007002450B3 (de) | Verbundlenkerachse für Kraftfahrzeuge und Verfahren zur Herstellung eines Torsionsprofils für eine Verbundlenkerachse | |
| EP3825021B1 (fr) | Procédé ainsi que dispositif de fabrication d'un tube à ailettes | |
| EP0648985A2 (fr) | Absorbeur solaire et méthode pour sa fabrication | |
| DE19832288B4 (de) | Verfahren zur Herstellung eines Verbindungselementes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| B565 | Issuance of search results under rule 164(2) epc |
Effective date: 20211203 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20220609 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20250201 |