JP2012183591A - 閉鎖された中空横断面を有する部材を溶接する方法 - Google Patents
閉鎖された中空横断面を有する部材を溶接する方法 Download PDFInfo
- Publication number
- JP2012183591A JP2012183591A JP2012141399A JP2012141399A JP2012183591A JP 2012183591 A JP2012183591 A JP 2012183591A JP 2012141399 A JP2012141399 A JP 2012141399A JP 2012141399 A JP2012141399 A JP 2012141399A JP 2012183591 A JP2012183591 A JP 2012183591A
- Authority
- JP
- Japan
- Prior art keywords
- housing member
- housing
- welding
- gap
- region
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
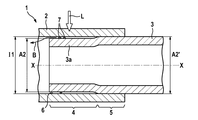
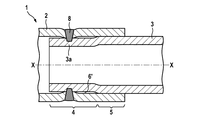
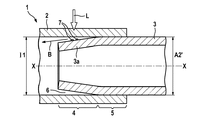
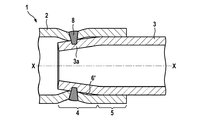
Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F16—ENGINEERING ELEMENTS AND UNITS; GENERAL MEASURES FOR PRODUCING AND MAINTAINING EFFECTIVE FUNCTIONING OF MACHINES OR INSTALLATIONS; THERMAL INSULATION IN GENERAL
- F16K—VALVES; TAPS; COCKS; ACTUATING-FLOATS; DEVICES FOR VENTING OR AERATING
- F16K27/00—Construction of housing; Use of materials therefor
- F16K27/10—Welded housings
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K33/00—Specially-profiled edge portions of workpieces for making soldering or welding connections; Filling the seams formed thereby
- B23K33/004—Filling of continuous seams
- B23K33/006—Filling of continuous seams for cylindrical workpieces
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/20—Bonding
- B23K26/21—Bonding by welding
- B23K26/24—Seam welding
- B23K26/244—Overlap seam welding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K26/00—Working by laser beam, e.g. welding, cutting or boring
- B23K26/20—Bonding
- B23K26/21—Bonding by welding
- B23K26/24—Seam welding
- B23K26/28—Seam welding of curved planar seams
- B23K26/282—Seam welding of curved planar seams of tube sections
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02M—SUPPLYING COMBUSTION ENGINES IN GENERAL WITH COMBUSTIBLE MIXTURES OR CONSTITUENTS THEREOF
- F02M61/00—Fuel-injectors not provided for in groups F02M39/00 - F02M57/00 or F02M67/00
- F02M61/16—Details not provided for in, or of interest apart from, the apparatus of groups F02M61/02 - F02M61/14
- F02M61/168—Assembling; Disassembling; Manufacturing; Adjusting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2101/00—Articles made by soldering, welding or cutting
- B23K2101/006—Vehicles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K2101/00—Articles made by soldering, welding or cutting
- B23K2101/04—Tubular or hollow articles
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02M—SUPPLYING COMBUSTION ENGINES IN GENERAL WITH COMBUSTIBLE MIXTURES OR CONSTITUENTS THEREOF
- F02M2200/00—Details of fuel-injection apparatus, not otherwise provided for
- F02M2200/80—Fuel injection apparatus manufacture, repair or assembly
- F02M2200/8084—Fuel injection apparatus manufacture, repair or assembly involving welding or soldering
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49405—Valve or choke making
- Y10T29/49412—Valve or choke making with assembly, disassembly or composite article making
- Y10T29/49416—Valve or choke making with assembly, disassembly or composite article making with material shaping or cutting
- Y10T29/49421—Valve or choke making with assembly, disassembly or composite article making with material shaping or cutting including metallurgical bonding
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49826—Assembling or joining
- Y10T29/49908—Joining by deforming
- Y10T29/49925—Inward deformation of aperture or hollow body wall
- Y10T29/49927—Hollow body is axially joined cup or tube
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- General Engineering & Computer Science (AREA)
- Plasma & Fusion (AREA)
- Chemical & Material Sciences (AREA)
- Combustion & Propulsion (AREA)
- Manufacturing & Machinery (AREA)
- Laser Beam Processing (AREA)
- Fuel-Injection Apparatus (AREA)
- Standing Axle, Rod, Or Tube Structures Coupled By Welding, Adhesion, Or Deposition (AREA)
- Connection Of Plates (AREA)
Abstract
【解決手段】第1のハウジング部材2と第2のハウジング部材3とを溶接によって接合する方法であって、第1の内寸I1を備えた第1のハウジング部材を準備し、第1のハウジング部材の内寸I1よりも小さな外寸A2を備えた小横断面部分と、第1のハウジング部材との間でプレス結合部を形成する大横断面部分とを有する第2のハウジング部材を準備し、第2のハウジング部材を第1のハウジング部材内に配置して、第1のハウジング部材の内壁と第2のハウジング部材の外壁との間に、環状の間隙6を形成し、第1のハウジング部材と第2のハウジング部材との溶接を、該第1のハウジング部材と第2のハウジング部材との間の間隙の領域において行う、というステップを有している。
【選択図】図1
Description
下記のステップ、すなわち:
第1の内寸を備えた第1のハウジング部材を準備し、
第1のハウジング部材の内寸よりも小さな外寸を備えた小横断面部分と、第1のハウジング部材との間でプレス結合部を形成する大横断面部分とを有する第2のハウジング部材を準備し、
第2のハウジング部材を第1のハウジング部材内に配置して、第1のハウジング部材の内壁と第2のハウジング部材の外壁との間に、環状の間隙を形成し、両ハウジング部材の間に間隙を有する領域が接合領域であり、
第1のハウジング部材と第2のハウジング部材との溶接を、該第1のハウジング部材と第2のハウジング部材との間の間隙の領域において行う、というステップを有しており、
第1のハウジング部材と第2のハウジング部材とを溶接ステップの前に相対的に位置決めするために、第1のハウジング部材と第2のハウジング部材との間にプレス結合領域が形成されていて、該プレス結合領域が接合領域に隣接して配置されているようにした。
Claims (13)
- 第1のハウジング部材(2)と第2のハウジング部材(3)とを溶接によって接合する方法であって、第1のハウジング部材(2)及び第2のハウジング部材(3)がそれぞれ、閉鎖された中空横断面を有する中空体として形成されており、第2のハウジング部材の中空横断面の形状が第1のハウジング部材の中空横断面の形状に相当しており、
下記のステップ、すなわち:
第1の内寸(I1)を備えた第1のハウジング部材(2)を準備し、
第1のハウジング部材(2)の内寸(I1)よりも小さな外寸(A2)を備えた小横断面部分と、第1のハウジング部材(2)との間でプレス結合部を形成する大横断面部分とを有する第2のハウジング部材(3)を準備し、
第2のハウジング部材(3)を第1のハウジング部材(2)内に配置して、第1のハウジング部材(2)の内壁と第2のハウジング部材(3)の外壁との間に、環状の間隙(6)を形成し、両ハウジング部材(2,3)の間に間隙を有する領域が接合領域(4)であり、
第1のハウジング部材(2)と第2のハウジング部材(3)との溶接を、該第1のハウジング部材(2)と第2のハウジング部材(3)との間の間隙(6)の領域において行う、というステップを有しており、
第1のハウジング部材(2)と第2のハウジング部材(3)とを溶接ステップの前に相対的に位置決めするために、第1のハウジング部材(2)と第2のハウジング部材(3)との間にプレス結合領域(5)が形成されていて、該プレス結合領域(5)が接合領域(4)に隣接して配置されていることを特徴とする、閉鎖された中空横断面を有する部材を溶接する方法。 - 環状の間隙(6)がその周方向に沿ってかつ、ハウジング部材の軸線方向(X−X)におけるその長さに沿って、等しいままの厚さを有している、請求項1記載の方法。
- 間隙(6)が、第1のハウジング部材(2)の壁厚の1/100〜50/100の厚さを有している、請求項2記載の方法。
- 間隙(6)が先細に形成されている、請求項1記載の方法。
- 溶接がレーザ溶接である、請求項1から4までのいずれか1項記載の方法。
- 第1のハウジング部材(2)及び第2のハウジング部材(3)がそれぞれ円形の横断面を有している、請求項1から5までのいずれか1項記載の方法。
- 溶接が同時に、両ハウジング部材(2,3)の周囲における複数のポジションにおいて実施される、請求項1から6までのいずれか1項記載の方法。
- 第1のハウジング部材(2)及び第2のハウジング部材(3)が薄い金属薄板材料から製造されている、請求項1から7までのいずれか1項記載の方法。
- 請求項1から8までのいずれか1項記載の方法によって製造された、噴射弁用のハウジング。
- 第1のハウジング部材(2)と第2のハウジング部材(3)とが設けられていて、両ハウジング部材(2,3)が接合領域(4)において、溶接によって互いに接合されており、接合領域(4)において第1のハウジング部材(2)の内寸(I1)が第2のハウジング部材(3)の外寸(A2)よりも大であり、溶接ステップの前に第1のハウジング部材(2)と第2のハウジング部材(3)と間に間隙(6)が形成されている、請求項9記載のハウジング。
- 間隙(6)が溶接の前において、等しいままの厚さを有しているか、又は間隙(6)が先細の形状を有している、請求項9又は10記載のハウジング。
- 第1のハウジング部材(2)及び第2のハウジング部材(3)がそれぞれ真円形又は楕円形の横断面を有している、請求項9から11までのいずれか1項記載のハウジング。
- 第1のハウジング部材(2)と第2のハウジング部材(3)との間にプレス結合領域(5)が設けられている、請求項9から12までのいずれか1項記載のハウジング。
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102006040650A DE102006040650A1 (de) | 2006-08-30 | 2006-08-30 | Verfahren zum Fügen von Bauteilen mit geschlossenem Hohlquerschnitt |
| DE102006040650.8 | 2006-08-30 |
Related Parent Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2009526016A Division JP5156746B2 (ja) | 2006-08-30 | 2007-07-27 | 閉鎖された中空横断面を有する部材を溶接する方法 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2012183591A true JP2012183591A (ja) | 2012-09-27 |
| JP5575186B2 JP5575186B2 (ja) | 2014-08-20 |
Family
ID=38561208
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2009526016A Expired - Fee Related JP5156746B2 (ja) | 2006-08-30 | 2007-07-27 | 閉鎖された中空横断面を有する部材を溶接する方法 |
| JP2012141399A Expired - Fee Related JP5575186B2 (ja) | 2006-08-30 | 2012-06-22 | 閉鎖された中空横断面を有する部材を溶接する方法 |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2009526016A Expired - Fee Related JP5156746B2 (ja) | 2006-08-30 | 2007-07-27 | 閉鎖された中空横断面を有する部材を溶接する方法 |
Country Status (6)
| Country | Link |
|---|---|
| US (2) | US8607457B2 (ja) |
| EP (1) | EP2059366B1 (ja) |
| JP (2) | JP5156746B2 (ja) |
| CN (1) | CN101578156B (ja) |
| DE (1) | DE102006040650A1 (ja) |
| WO (1) | WO2008025623A1 (ja) |
Families Citing this family (22)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102010005873B4 (de) * | 2010-01-27 | 2012-06-06 | Magna Powertrain Ag & Co. Kg | Verfahren zum Verbinden einer Welle und einer Nabe sowie Anordnung aus Welle und Nabe |
| JP5381766B2 (ja) * | 2010-02-09 | 2014-01-08 | 株式会社デンソー | 溶接方法 |
| JP5509901B2 (ja) * | 2010-02-12 | 2014-06-04 | 株式会社デンソー | 燃料噴射弁 |
| DE102010031365A1 (de) * | 2010-07-15 | 2012-01-19 | Robert Bosch Gmbh | Bauelement für ein Einspritzventil mit zwei verbundenen Bauteilen |
| KR101272050B1 (ko) * | 2011-11-11 | 2013-06-07 | 주식회사 성우하이텍 | 레이저 용접방법 |
| JP5921240B2 (ja) * | 2012-02-10 | 2016-05-24 | 日立オートモティブシステムズ株式会社 | 燃料噴射弁 |
| WO2013157269A1 (ja) * | 2012-04-20 | 2013-10-24 | 日本特殊陶業株式会社 | 圧力センサ付きグロープラグ |
| JP5947122B2 (ja) * | 2012-06-27 | 2016-07-06 | 日本特殊陶業株式会社 | グロープラグ |
| EP3006721A4 (en) * | 2013-06-06 | 2016-11-23 | Hitachi Automotive Systems Ltd | ELECTROMAGNETIC FUEL INJECTION VALVE |
| US10794523B2 (en) * | 2015-12-14 | 2020-10-06 | Wilmarc Holdings, Llc | Laser induced sealing of concentrically layered materials |
| DE102015226469A1 (de) * | 2015-12-22 | 2017-06-22 | Robert Bosch Gmbh | Komponente einer Hochdruckanlage, insbesondere einer Hochdruck-Brennstoffeinspritzanlage |
| JP6709638B2 (ja) * | 2016-03-10 | 2020-06-17 | 日立造船株式会社 | 鋼管構造体における鋼管と継手との溶接方法 |
| WO2017168975A1 (ja) * | 2016-03-28 | 2017-10-05 | 日立オートモティブシステムズ株式会社 | 流量制御装置 |
| WO2018154689A1 (ja) * | 2017-02-23 | 2018-08-30 | 三菱電機株式会社 | 圧縮機 |
| DE102017105900A1 (de) * | 2017-03-20 | 2018-09-20 | Kirchhoff Automotive Deutschland Gmbh | Verfahren zum stirnseitigen Laserschweißen |
| EP3466601B1 (en) * | 2017-10-04 | 2024-06-12 | Saint-Gobain Ecophon AB | Method for manufacturing of a profile member |
| US11313336B2 (en) * | 2018-04-20 | 2022-04-26 | Hitachi Astemo, Ltd. | Component for flow rate control device, and fuel injection valve |
| US11883049B2 (en) * | 2019-03-29 | 2024-01-30 | Gyrus Acmi, Inc. | Forceps drive shaft control |
| CN110576261B (zh) * | 2019-08-21 | 2021-06-25 | 中车青岛四方机车车辆股份有限公司 | 激光叠焊装置及其焊接方法 |
| GB202001710D0 (en) * | 2020-02-07 | 2020-03-25 | Delphi Automotive Systems Lux | Fuel injector |
| CN115214149A (zh) * | 2021-04-19 | 2022-10-21 | 财团法人金属工业研究发展中心 | 纤维热塑复材管与铝合金管的接合方法 |
| DE102022203695A1 (de) | 2022-04-12 | 2023-10-12 | Mahle International Gmbh | Verfahren zum Verbinden eines ersten Bauteils mit einem zweiten Bauteil mittels Laserschweißen und Wellenanordnung |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE511461C (de) * | 1926-09-09 | 1930-10-30 | Johann Steinnes | Verfahren zur UEberlappungsschweissung von Rohren |
| JPH02268990A (ja) * | 1989-04-10 | 1990-11-02 | Nissan Motor Co Ltd | 鉄鋼製自動車用ロードホイールの溶接方法 |
| JPH0996264A (ja) * | 1995-10-02 | 1997-04-08 | Nippon Injector Kk | 電磁式燃料噴射弁及びその製造方法 |
| US5626776A (en) * | 1993-10-21 | 1997-05-06 | Morris Holmes & Co. | Flangeless fuel tank |
| US20010015013A1 (en) * | 2000-02-18 | 2001-08-23 | Takayuki Kato | Method of producing swash plate type compressor piston |
| JP2002327660A (ja) * | 2001-04-09 | 2002-11-15 | Siemens Vdo Automotive Corp | モジューラ燃料インジェクタ及びモジューラ燃料インジェクタを組み立てる方法 |
| JP2004095824A (ja) * | 2002-08-30 | 2004-03-25 | Sumitomo Electric Ind Ltd | 発光モジュール |
| JP2005319482A (ja) * | 2004-05-10 | 2005-11-17 | Nisshin Steel Co Ltd | 金属製マフラーシェルの製造方法 |
| WO2006138665A2 (en) * | 2005-06-16 | 2006-12-28 | Siemens Vdo Automotive Corporation | Component geometry and method for blow-out resistant welds |
| WO2006138712A1 (en) * | 2005-06-16 | 2006-12-28 | Siemens Vdo Automotive Corporation | Blowout resistant weld method for laser welds for press fit parts |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2988811A (en) * | 1957-03-08 | 1961-06-20 | Huet Andre | Method of making tube and wall connections |
| US4257155A (en) * | 1976-07-26 | 1981-03-24 | Hunter John J | Method of making pipe coupling joint |
| IT1182277B (it) * | 1984-09-20 | 1987-10-05 | Prima Progetti Spa | Metodo per la saldatura laser di lamiere metalliche protette con materiali a bassa temperatura di vaporizzazione |
| JPH01258886A (ja) | 1988-04-08 | 1989-10-16 | Hitachi Ltd | レーザ溶接方法 |
| JP2839394B2 (ja) | 1991-08-26 | 1998-12-16 | 日鐵溶接工業株式会社 | 金属管の接合方法 |
| CN2379679Y (zh) * | 1999-06-10 | 2000-05-24 | 赵培成 | 搭接缠绕式钢塑复合管 |
| DE19930931A1 (de) * | 1999-07-06 | 2001-01-11 | Sgl Technik Gmbh | Schichtverbund mit geschweißter Metalleinlage |
| US6421913B1 (en) * | 2000-01-19 | 2002-07-23 | Delphi Technologies, Inc. | Retention feature for assembling a pole pieces into a tube of a fuel injector |
| US6403916B1 (en) * | 2000-05-12 | 2002-06-11 | Isostar International, Inc. | System and automated method for producing welded end closures in thin-walled metal tubes |
| ITTO20010185A1 (it) * | 2001-03-02 | 2002-09-02 | Comau Systems Spa | Procedimento e sistema per la saldatura laser di due o piu' lamiere metalliche fra loro sovrappost, e dispositivo di bloccaggio delle lamier |
| ITBO20010375A1 (it) * | 2001-06-13 | 2002-12-13 | Valter Lolli | Metodo per la realizzazione di elementi di testa per radiatori termici, ed elemento di testa realizzato con tale metodo |
| CN2494465Y (zh) * | 2001-06-29 | 2002-06-05 | 广州市自来水制管厂 | 球形承插式焊接钢管 |
| JP4397631B2 (ja) * | 2003-06-27 | 2010-01-13 | 株式会社オーハシテクニカ | 圧入接合構造及びその接合部品 |
| DE112008002206B4 (de) * | 2007-08-17 | 2012-06-21 | Danfoss A/S | Laserschweißen von hochreflektierenden Materialien |
-
2006
- 2006-08-30 DE DE102006040650A patent/DE102006040650A1/de not_active Withdrawn
-
2007
- 2007-07-27 US US12/301,785 patent/US8607457B2/en not_active Expired - Fee Related
- 2007-07-27 EP EP07788002A patent/EP2059366B1/de not_active Ceased
- 2007-07-27 WO PCT/EP2007/057788 patent/WO2008025623A1/de not_active Ceased
- 2007-07-27 CN CN2007800319458A patent/CN101578156B/zh not_active Expired - Fee Related
- 2007-07-27 JP JP2009526016A patent/JP5156746B2/ja not_active Expired - Fee Related
-
2012
- 2012-06-22 JP JP2012141399A patent/JP5575186B2/ja not_active Expired - Fee Related
-
2013
- 2013-11-05 US US14/071,880 patent/US20140131610A1/en not_active Abandoned
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE511461C (de) * | 1926-09-09 | 1930-10-30 | Johann Steinnes | Verfahren zur UEberlappungsschweissung von Rohren |
| JPH02268990A (ja) * | 1989-04-10 | 1990-11-02 | Nissan Motor Co Ltd | 鉄鋼製自動車用ロードホイールの溶接方法 |
| US5626776A (en) * | 1993-10-21 | 1997-05-06 | Morris Holmes & Co. | Flangeless fuel tank |
| JPH0996264A (ja) * | 1995-10-02 | 1997-04-08 | Nippon Injector Kk | 電磁式燃料噴射弁及びその製造方法 |
| US20010015013A1 (en) * | 2000-02-18 | 2001-08-23 | Takayuki Kato | Method of producing swash plate type compressor piston |
| JP2002327660A (ja) * | 2001-04-09 | 2002-11-15 | Siemens Vdo Automotive Corp | モジューラ燃料インジェクタ及びモジューラ燃料インジェクタを組み立てる方法 |
| JP2004095824A (ja) * | 2002-08-30 | 2004-03-25 | Sumitomo Electric Ind Ltd | 発光モジュール |
| JP2005319482A (ja) * | 2004-05-10 | 2005-11-17 | Nisshin Steel Co Ltd | 金属製マフラーシェルの製造方法 |
| WO2006138665A2 (en) * | 2005-06-16 | 2006-12-28 | Siemens Vdo Automotive Corporation | Component geometry and method for blow-out resistant welds |
| WO2006138712A1 (en) * | 2005-06-16 | 2006-12-28 | Siemens Vdo Automotive Corporation | Blowout resistant weld method for laser welds for press fit parts |
Also Published As
| Publication number | Publication date |
|---|---|
| JP5156746B2 (ja) | 2013-03-06 |
| DE102006040650A1 (de) | 2008-03-13 |
| CN101578156A (zh) | 2009-11-11 |
| US8607457B2 (en) | 2013-12-17 |
| JP2010501811A (ja) | 2010-01-21 |
| US20140131610A1 (en) | 2014-05-15 |
| US20110204276A1 (en) | 2011-08-25 |
| WO2008025623A1 (de) | 2008-03-06 |
| EP2059366B1 (de) | 2012-04-11 |
| CN101578156B (zh) | 2012-10-24 |
| JP5575186B2 (ja) | 2014-08-20 |
| EP2059366A1 (de) | 2009-05-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5575186B2 (ja) | 閉鎖された中空横断面を有する部材を溶接する方法 | |
| JP5227154B2 (ja) | 管板と管とを接合する方法およびこの方法を実施する摩擦工具 | |
| JP5609632B2 (ja) | レーザ重ね溶接方法 | |
| JP2010155275A (ja) | 溶接継手及びその製造方法 | |
| CN103038017B (zh) | 通过焊接电流和压入对轴和轮毂进行连接的方法以及轴和轮毂通过这种连接构成的装置 | |
| JP7462392B2 (ja) | プレート式熱交換器 | |
| WO2014119342A1 (ja) | 部材接合方法、部材接合構造、および継手管 | |
| CN102131631A (zh) | 在激光透射方法中连接管状零件的激光头和方法 | |
| CN107073620A (zh) | 焊料和用于通过材料锁合的连接制造组件的方法 | |
| JP5526567B2 (ja) | 溶接接合部材 | |
| JP2006289500A (ja) | 電子ビーム又はレーザ溶接のための溶接プレップジョイント | |
| JP2006233964A (ja) | ディーゼルエンジン用コモンレール | |
| JP5381501B2 (ja) | 溶接接合部品及び溶接接合方法 | |
| JP5378661B2 (ja) | 拡管方法 | |
| CN103206723A (zh) | 燃料喷嘴和制造燃料喷嘴的工艺 | |
| JP6952632B2 (ja) | レーザー重ね溶接の構造および方法 | |
| JP7007251B2 (ja) | 異材接合方法、異材接合継手、異材接合用補助部材付き管状部材及びその製造方法 | |
| JP2008055448A (ja) | 溶接継手構造および重ね隅肉溶接方法 | |
| JP2009291828A (ja) | 配管接合方法 | |
| KR20110003235A (ko) | 마운팅 러그 및 인젝터 홀더를 연료분배관에 용접하는 방법 | |
| JP4578386B2 (ja) | 排気管とフランジの溶接方法 | |
| JP2010253488A (ja) | 管外周突部の形成方法及び管外周突部を有する金属管 | |
| JP7343409B2 (ja) | 接合体の製造方法 | |
| JP4357788B2 (ja) | 閉鎖容器の突合せ溶接方法 | |
| JP2006167768A (ja) | ろう付け方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20120622 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20130830 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20130902 |
|
| A601 | Written request for extension of time |
Free format text: JAPANESE INTERMEDIATE CODE: A601 Effective date: 20131202 |
|
| A602 | Written permission of extension of time |
Free format text: JAPANESE INTERMEDIATE CODE: A602 Effective date: 20131205 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20140228 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20140602 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20140701 |
|
| R150 | Certificate of patent or registration of utility model |
Ref document number: 5575186 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| LAPS | Cancellation because of no payment of annual fees |