JP2017140652A - 金属管の冷間圧延方法および製造方法 - Google Patents
金属管の冷間圧延方法および製造方法 Download PDFInfo
- Publication number
- JP2017140652A JP2017140652A JP2017013827A JP2017013827A JP2017140652A JP 2017140652 A JP2017140652 A JP 2017140652A JP 2017013827 A JP2017013827 A JP 2017013827A JP 2017013827 A JP2017013827 A JP 2017013827A JP 2017140652 A JP2017140652 A JP 2017140652A
- Authority
- JP
- Japan
- Prior art keywords
- rolling
- metal tube
- steel pipe
- temperature
- manufacturing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B19/00—Tube-rolling by rollers arranged outside the work and having their axes not perpendicular to the axis of the work
- B21B19/02—Tube-rolling by rollers arranged outside the work and having their axes not perpendicular to the axis of the work the axes of the rollers being arranged essentially diagonally to the axis of the work, e.g. "cross" tube-rolling ; Diescher mills, Stiefel disc piercers or Stiefel rotary piercers
- B21B19/06—Rolling hollow basic material, e.g. Assel mills
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Heat Treatment Of Steel (AREA)
- Heat Treatment Of Articles (AREA)
Abstract
Description
(1)金属管を冷間圧延する方法であって、回転軸が金属管の圧延パス方向センターラインに対して傾斜して配置した2個以上の圧延ロールを有する傾斜圧延機のロールギャップに前記金属管を通過させて縮径圧延することを特徴とする金属管の冷間圧延方法。
(2)前記金属管が前記ロールギャップを通過する際に、前記金属管の内面を自由表面として縮径圧延することを特徴とする(1)に記載の金属管の冷間圧延方法。
(3)前記金属管の肉厚を減少させないように縮径圧延することを特徴とする(1)または(2)に記載の金属管の冷間圧延方法。
(4)前記圧延ロールの回転軸が圧延出側で45°以下の交叉角をなして交叉するように配置することを特徴とする(1)〜(3)のいずれかに記載の金属管の冷間圧延方法。
(5)前記縮径圧延を複数パスで行うことを特徴とする(1)〜(4)のいずれかに記載の金属管の冷間圧延方法。
(6)(1)〜(5)のいずれかに記載の冷間圧延方法によって縮径圧延を施した後、700℃以下の温度T1で熱処理することを特徴とする金属管の製造方法。
(7)前記金属管が鋼管であり、(1)〜(5)のいずれかに記載の冷間圧延方法によって縮径圧延を施した後、700℃以下の温度T1で熱処理することを特徴とする鋼管の製造方法。
(8)前記熱処理に加えて、さらに700℃以下の温度であって、かつ(T1+150℃)以上あるいは(T1−150℃)以下の温度T2で熱処理することを特徴とする(7)に記載の鋼管の製造方法。
(9)(1)〜(5)のいずれかに記載の冷間圧延方法によって縮径圧延を施した鋼管を再結晶温度域に加熱し、冷却後、再度、前記冷間圧延方法による縮径圧延を1回以上施すことを特徴とする鋼管の製造方法。
(10)前記製造方法の出発素材である素管がフェライト相分率:50%以上の組織を有する鋼管であることを特徴とする(9)に記載の鋼管の製造方法。
(11)前記加熱、冷却後、再度、前記縮径圧延を施した鋼管を、700℃以下の温度T1で熱処理することを特徴とする(9)または(10)に記載の鋼管の製造方法。
(12)前記熱処理に加えて、さらに700℃以下の温度であって、かつ(T1+150℃)以上あるいは(T1−150℃)以下の温度T2で熱処理することを特徴とする(11)に記載の鋼管の製造方法。

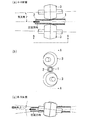
2 冷間圧延管
3 圧延ロール
β 傾斜角
γ 交叉角
Claims (12)
- 金属管を冷間圧延する方法であって、回転軸が金属管の圧延パス方向センターラインに対して傾斜して配置した2個以上の圧延ロールを有する傾斜圧延機のロールギャップに前記金属管を通過させて縮径圧延することを特徴とする金属管の冷間圧延方法。
- 前記金属管が前記ロールギャップを通過する際に、前記金属管の内面を自由表面として縮径圧延することを特徴とする請求項1に記載の金属管の冷間圧延方法。
- 前記金属管の肉厚を減少させないように縮径圧延することを特徴とする請求項1または2に記載の金属管の冷間圧延方法。
- 前記圧延ロールの回転軸が圧延出側で45°以下の交叉角をなして交叉するように配置することを特徴とする請求項1〜3のいずれかに記載の金属管の冷間圧延方法。
- 前記縮径圧延を複数パスで行うことを特徴とする請求項1〜4のいずれかに記載の金属管の冷間圧延方法。
- 請求項1〜5のいずれかに記載の冷間圧延方法によって縮径圧延を施した後、700℃以下の温度T1で熱処理することを特徴とする金属管の製造方法。
- 前記金属管が鋼管であり、請求項1〜5のいずれかに記載の冷間圧延方法によって縮径圧延を施した後、700℃以下の温度T1で熱処理することを特徴とする鋼管の製造方法。
- 前記熱処理に加えて、さらに700℃以下の温度であって、かつ(T1+150℃)以上あるいは(T1−150℃)以下の温度T2で熱処理することを特徴とする請求項7に記載の鋼管の製造方法。
- 請求項1〜5のいずれかに記載の冷間圧延方法によって縮径圧延を施した鋼管を再結晶温度域に加熱し、冷却後、再度、前記冷間圧延方法による縮径圧延を1回以上施すことを特徴とする鋼管の製造方法。
- 前記製造方法の出発素材である素管がフェライト相分率:50%以上の組織を有する鋼管であることを特徴とする請求項9に記載の鋼管の製造方法。
- 前記加熱、冷却後、再度前記縮径圧延を施した鋼管を、700℃以下の温度T1で熱処理することを特徴とする請求項9または10に記載の鋼管の製造方法。
- 前記熱処理に加えて、さらに700℃以下の温度であって、かつ(T1+150℃)以上あるいは(T1−150℃)以下の温度T2で熱処理することを特徴とする請求項11に記載の鋼管の製造方法。
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2016021413 | 2016-02-08 | ||
| JP2016021413 | 2016-02-08 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2017140652A true JP2017140652A (ja) | 2017-08-17 |
| JP6432614B2 JP6432614B2 (ja) | 2018-12-05 |
Family
ID=59626996
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2017013827A Active JP6432614B2 (ja) | 2016-02-08 | 2017-01-30 | 金属管の冷間圧延方法および製造方法 |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP6432614B2 (ja) |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110102575A (zh) * | 2019-04-30 | 2019-08-09 | 北京科技大学 | 一种轴类零件两辊柔性斜轧成形装置及方法 |
| CN111041180A (zh) * | 2019-12-31 | 2020-04-21 | 南京沃尔德特钢有限公司 | 超级耐腐蚀双相钢管的生产工艺 |
| WO2020217725A1 (ja) | 2019-04-23 | 2020-10-29 | Jfeスチール株式会社 | 圧延矯正機、及び該圧延矯正機を用いた管又は棒の製造方法 |
| CN115151353A (zh) * | 2020-02-26 | 2022-10-04 | 杰富意钢铁株式会社 | 无缝管及其制造方法 |
| JP2023134349A (ja) * | 2022-03-14 | 2023-09-27 | Jfeスチール株式会社 | 金属管の圧延方法、金属管の製造方法、圧延設備及び金属管 |
| CN119747439A (zh) * | 2025-01-14 | 2025-04-04 | 山西太钢不锈钢股份有限公司 | 电站过热器用hr3c特厚无缝管加工制造方法 |
| JP2025096160A (ja) * | 2023-12-14 | 2025-06-26 | Jfeスチール株式会社 | 傾斜圧延設備、傾斜圧延方法および金属管の製造方法 |
| CN120460473A (zh) * | 2025-05-26 | 2025-08-12 | 张家港华裕有色金属材料有限公司 | 一种提升钛合金管材延伸率的方法 |
Citations (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5381466A (en) * | 1976-12-27 | 1978-07-18 | Kubota Ltd | Seamless pipe manufacturing by pipe made with centrifugal casting |
| JPS55103208A (en) * | 1979-01-31 | 1980-08-07 | Nippon Steel Corp | Manufacture of seamless metallic pipe with small diameter |
| JPS63210236A (ja) * | 1987-02-25 | 1988-08-31 | Sumitomo Metal Ind Ltd | 耐サワ−用高コラプス油井管の製造法 |
| JPS63268504A (ja) * | 1987-04-24 | 1988-11-07 | Sumitomo Metal Ind Ltd | 管の冷間圧延方法 |
| JPH0199707A (ja) * | 1987-10-09 | 1989-04-18 | Sumitomo Metal Ind Ltd | 管の冷間圧延方法 |
| JPH0371904A (ja) * | 1989-08-10 | 1991-03-27 | Sumitomo Metal Ind Ltd | 金属管の縮径圧延方法 |
| JPH04187319A (ja) * | 1990-11-21 | 1992-07-06 | Nippon Steel Corp | 高強度電縫鋼管の製造方法 |
| JPH07246403A (ja) * | 1994-03-11 | 1995-09-26 | Nkk Corp | 金属管の絞り加工方法及び装置 |
| JPH09271811A (ja) * | 1996-04-10 | 1997-10-21 | Sumitomo Metal Ind Ltd | 二相ステンレス鋼製継目無鋼管の製造方法 |
| JPH1157842A (ja) * | 1997-08-27 | 1999-03-02 | Sumitomo Metal Ind Ltd | 管軸長方向の圧縮強度に優れた鋼管の製造方法 |
| JPH1177116A (ja) * | 1997-09-02 | 1999-03-23 | Kawasaki Steel Corp | 高疲労強度鋼管の製造方法 |
| JP2006326652A (ja) * | 2005-05-27 | 2006-12-07 | Sumitomo Metal Ind Ltd | 超薄肉継目無金属管の冷間製造方法 |
| WO2007091585A1 (ja) * | 2006-02-09 | 2007-08-16 | Sumitomo Metal Industries, Ltd. | エアバッグインフレータ用ボトル部材の製造方法 |
-
2017
- 2017-01-30 JP JP2017013827A patent/JP6432614B2/ja active Active
Patent Citations (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5381466A (en) * | 1976-12-27 | 1978-07-18 | Kubota Ltd | Seamless pipe manufacturing by pipe made with centrifugal casting |
| JPS55103208A (en) * | 1979-01-31 | 1980-08-07 | Nippon Steel Corp | Manufacture of seamless metallic pipe with small diameter |
| JPS63210236A (ja) * | 1987-02-25 | 1988-08-31 | Sumitomo Metal Ind Ltd | 耐サワ−用高コラプス油井管の製造法 |
| JPS63268504A (ja) * | 1987-04-24 | 1988-11-07 | Sumitomo Metal Ind Ltd | 管の冷間圧延方法 |
| JPH0199707A (ja) * | 1987-10-09 | 1989-04-18 | Sumitomo Metal Ind Ltd | 管の冷間圧延方法 |
| JPH0371904A (ja) * | 1989-08-10 | 1991-03-27 | Sumitomo Metal Ind Ltd | 金属管の縮径圧延方法 |
| JPH04187319A (ja) * | 1990-11-21 | 1992-07-06 | Nippon Steel Corp | 高強度電縫鋼管の製造方法 |
| JPH07246403A (ja) * | 1994-03-11 | 1995-09-26 | Nkk Corp | 金属管の絞り加工方法及び装置 |
| JPH09271811A (ja) * | 1996-04-10 | 1997-10-21 | Sumitomo Metal Ind Ltd | 二相ステンレス鋼製継目無鋼管の製造方法 |
| JPH1157842A (ja) * | 1997-08-27 | 1999-03-02 | Sumitomo Metal Ind Ltd | 管軸長方向の圧縮強度に優れた鋼管の製造方法 |
| JPH1177116A (ja) * | 1997-09-02 | 1999-03-23 | Kawasaki Steel Corp | 高疲労強度鋼管の製造方法 |
| JP2006326652A (ja) * | 2005-05-27 | 2006-12-07 | Sumitomo Metal Ind Ltd | 超薄肉継目無金属管の冷間製造方法 |
| WO2007091585A1 (ja) * | 2006-02-09 | 2007-08-16 | Sumitomo Metal Industries, Ltd. | エアバッグインフレータ用ボトル部材の製造方法 |
Cited By (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11731184B2 (en) | 2019-04-23 | 2023-08-22 | Jfe Steel Corporation | Rolling straightening machine and method of manufacturing a pipe or tube or a bar using same |
| WO2020217725A1 (ja) | 2019-04-23 | 2020-10-29 | Jfeスチール株式会社 | 圧延矯正機、及び該圧延矯正機を用いた管又は棒の製造方法 |
| JP6795131B1 (ja) * | 2019-04-23 | 2020-12-02 | Jfeスチール株式会社 | 圧延矯正機、及び該圧延矯正機を用いた管又は棒の製造方法 |
| CN110102575B (zh) * | 2019-04-30 | 2020-07-31 | 北京科技大学 | 一种轴类零件两辊柔性斜轧成形装置及方法 |
| CN110102575A (zh) * | 2019-04-30 | 2019-08-09 | 北京科技大学 | 一种轴类零件两辊柔性斜轧成形装置及方法 |
| CN111041180A (zh) * | 2019-12-31 | 2020-04-21 | 南京沃尔德特钢有限公司 | 超级耐腐蚀双相钢管的生产工艺 |
| US12140265B2 (en) | 2020-02-26 | 2024-11-12 | Jfe Steel Corporation | Seamless pipe and method for manufacturing same |
| CN115151353A (zh) * | 2020-02-26 | 2022-10-04 | 杰富意钢铁株式会社 | 无缝管及其制造方法 |
| EP4094856A4 (en) * | 2020-02-26 | 2023-10-04 | JFE Steel Corporation | SEAMLESS TUBE AND METHOD FOR MANUFACTURING SAME |
| JP7647732B2 (ja) | 2022-03-14 | 2025-03-18 | Jfeスチール株式会社 | 金属管の圧延方法、金属管の製造方法及び圧延設備 |
| JP2023134349A (ja) * | 2022-03-14 | 2023-09-27 | Jfeスチール株式会社 | 金属管の圧延方法、金属管の製造方法、圧延設備及び金属管 |
| JP2025096160A (ja) * | 2023-12-14 | 2025-06-26 | Jfeスチール株式会社 | 傾斜圧延設備、傾斜圧延方法および金属管の製造方法 |
| CN119747439A (zh) * | 2025-01-14 | 2025-04-04 | 山西太钢不锈钢股份有限公司 | 电站过热器用hr3c特厚无缝管加工制造方法 |
| CN120460473A (zh) * | 2025-05-26 | 2025-08-12 | 张家港华裕有色金属材料有限公司 | 一种提升钛合金管材延伸率的方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP6432614B2 (ja) | 2018-12-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6432614B2 (ja) | 金属管の冷間圧延方法および製造方法 | |
| JP4894855B2 (ja) | 継目無管の製造方法 | |
| KR101660601B1 (ko) | 강도와 저온 인성이 우수한 이음매 없는 강관의 제어 압연 방법 | |
| CN114273574B (zh) | 一种控制大规格易偏析奥氏体不锈钢棒材组织均匀性的锻造方法 | |
| US20230151474A1 (en) | Metal rings formed from beryllium-copper alloys | |
| US11313005B2 (en) | Seamless steel pipe and method for producing the seamless steel pipe | |
| CN102581555A (zh) | P91 无缝钢管及其制备方法 | |
| JP7647732B2 (ja) | 金属管の圧延方法、金属管の製造方法及び圧延設備 | |
| CN112044978A (zh) | 高温耐压钛合金小规格厚壁管材的制备方法 | |
| CN109909298B (zh) | 优钢及螺纹钢棒材生产线及优钢及螺纹钢的生产方法 | |
| CN103103329A (zh) | 一种超级双相不锈钢无缝管的冷加工方法 | |
| CN121571941A (zh) | 锚杆杆体连续成型工艺及设备 | |
| CN110860558B (zh) | 一种超宽特厚钢质安全壳核电用钢的轧制方法 | |
| JPS60114517A (ja) | 軟化焼鈍処理の省略可能な鋼線材の製造方法 | |
| JP4182556B2 (ja) | 継目無鋼管の製造方法 | |
| CN116219311B (zh) | 一种Si-Cr系800MPa级抗弯管起皱用热轧钢板及其生产方法 | |
| JPH0547603B2 (ja) | ||
| JP7559728B2 (ja) | 継目無鋼管および鋼管の製造方法 | |
| JPH06285546A (ja) | 延性を向上した冷間引抜鋼管の製造方法 | |
| JP2018075576A (ja) | 継目無鋼管の製造方法および継目無鋼管製造設備 | |
| JP2025095054A (ja) | 傾斜圧延設備、傾斜圧延方法および金属管の製造方法 | |
| JP2026048044A (ja) | 傾斜圧延方法、傾斜圧延設備および金属管の製造方法 | |
| JP2026048043A (ja) | 金属管の傾斜圧延方法、金属管の傾斜圧延設備および金属管の製造方法 | |
| JP2019150875A (ja) | 鋼管およびその製造方法 | |
| JP2025095055A (ja) | 傾斜圧延設備および金属管の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20170922 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20180614 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20180626 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20180820 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20181009 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20181022 |
|
| R150 | Certificate of patent or registration of utility model |
Ref document number: 6432614 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |