JP6091276B2 - 窓を有するケミカルメカニカル研磨層の製造方法 - Google Patents
窓を有するケミカルメカニカル研磨層の製造方法 Download PDFInfo
- Publication number
- JP6091276B2 JP6091276B2 JP2013058848A JP2013058848A JP6091276B2 JP 6091276 B2 JP6091276 B2 JP 6091276B2 JP 2013058848 A JP2013058848 A JP 2013058848A JP 2013058848 A JP2013058848 A JP 2013058848A JP 6091276 B2 JP6091276 B2 JP 6091276B2
- Authority
- JP
- Japan
- Prior art keywords
- mold cavity
- axis
- nozzle opening
- donut
- region
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D7/00—Bonded abrasive wheels, or wheels with inserted abrasive blocks, designed for acting otherwise than only by their periphery, e.g. by the front face; Bushings or mountings therefor
- B24D7/12—Bonded abrasive wheels, or wheels with inserted abrasive blocks, designed for acting otherwise than only by their periphery, e.g. by the front face; Bushings or mountings therefor with apertures for inspecting the surface to be abraded
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D11/00—Constructional features of flexible abrasive materials; Special features in the manufacture of such materials
- B24D11/001—Manufacture of flexible abrasive materials
- B24D11/003—Manufacture of flexible abrasive materials without embedded abrasive particles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B37/00—Lapping machines or devices; Accessories
- B24B37/11—Lapping tools
- B24B37/20—Lapping pads for working plane surfaces
- B24B37/24—Lapping pads for working plane surfaces characterised by the composition or properties of the pad materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D18/00—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for
- B24D18/0009—Manufacture of grinding tools or other grinding devices, e.g. wheels, not otherwise provided for using moulds or presses
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24D—TOOLS FOR GRINDING, BUFFING OR SHARPENING
- B24D3/00—Physical features of abrasive bodies, or sheets, e.g. abrasive surfaces of special nature; Abrasive bodies or sheets characterised by their constituents
- B24D3/02—Physical features of abrasive bodies, or sheets, e.g. abrasive surfaces of special nature; Abrasive bodies or sheets characterised by their constituents the constituent being used as bonding agent
- B24D3/20—Physical features of abrasive bodies, or sheets, e.g. abrasive surfaces of special nature; Abrasive bodies or sheets characterised by their constituents the constituent being used as bonding agent and being essentially organic
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09K—MATERIALS FOR MISCELLANEOUS APPLICATIONS, NOT PROVIDED FOR ELSEWHERE
- C09K3/00—Materials not provided for elsewhere
- C09K3/14—Anti-slip materials; Abrasives
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Chemical & Material Sciences (AREA)
- Materials Engineering (AREA)
- Organic Chemistry (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
- Mechanical Treatment Of Semiconductor (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
Description
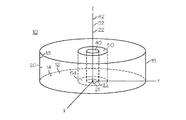
Cx−area=πrC 2
ここで、rCはx−y平面上に投影される金型キャビティの断面積Cx−areaの平均半径であり;ドーナツ穴領域はx−y平面上に円形断面DHx−sectを投影し、対称軸DHaxisを有する、金型キャビティ内の直円柱形状領域であり;ドーナツ穴は以下に定義される断面積DHx−areaを有し:
DHx−area=πrDH 2
ここで、rDHはドーナツ穴領域の円形断面DHx−sectの半径であり;ドーナツ領域はx−y平面上に環状断面Dx−sectを投影し、ドーナツ領域対称軸Daxisを有する、金型キャビティ内のトロイド形状領域であり;環状断面Dx−sectは以下に定義される断面積Dx−areaを有し:
Dx−area=πRD 2−πrD 2
ここで、RDはドーナツ領域の環状断面Dx−sectの長半径であり;rDはドーナツ領域の環状断面Dx−sectの短半径であり;rD≧rDHであり;RD>rDであり;RD<rCであり;Cx−sym、DHaxisおよびDaxisの各々がx−y平面と垂直である方法を提供する。
驚くべきことに、ケミカルメカニカル研磨パッドに使用する、一体化窓を有する研磨層の製造において、硬化性材料を金型キャビティ内に装填しながら、それを通して硬化性材料を金型キャビティに装填するノズル開口部の位置を、金型キャビティの中心軸Caxisに沿っておよびそれを中心としての両方において三次元で移動させることにより、ノズル開口部の位置が金型キャビティの中心軸Caxisに沿って一次元でのみ移動する同様のプロセスによって生成されたものに対して、生成された研磨層における密度欠陥の発生を有意に低減することが見出された。
CRmax≦(1.1*CRavg)
CRmin≧(0.9*CRavg)
ここで、CRmaxは装填時間中に硬化性材料が金型キャビティ内に装填される最大質量流量(kg/sec)であり;CRminは装填時間中に硬化性材料が金型キャビティ内に装填される最小質量流量(kg/sec)であり;CRavgは装填時間の間に金型キャビティに装填された硬化性材料の合計質量(kg)を、装填時間(秒)の長さで割ったものである。
Cx−area=πrC 2
ここで、rCはx−y平面上に投影される金型キャビティの断面積Cx−areaの平均半径であり;rCが20〜100cm(より好ましくは25〜65cm;最も好ましくは40〜60cm)である。
DHx−area=πrDH 2
ここで、rDHはドーナツ穴領域の円形断面DHx−sect(44)の半径(46)である。好ましくは、rDH≧rNOである(より好ましくは、rDHが5〜25mmであり、最も好ましくは、8〜15mmである)。
Dx−area=πRD 2−πrD 2
ここで、RDはドーナツ領域の環状断面Dx−sectの長半径(56)であり;rDはドーナツ領域の環状断面Dx−sectの短半径(58)であり;rD≧rDHであり;RD>rDであり;RD<rCである。好ましくは、rD≧rDHであり、rDが5〜25mmである。より好ましくは、rD≧rDHであり、rDが8〜15mmである。好ましくは、rD≧rDHであり;RD>rDであり;RD≦(K*rC)であり、Kが0.01〜0.2(より好ましくは、0.014〜0.1、最も好ましくは、0.04〜0.086)である。より好ましくは、rD≧rDHであり;RD>rDであり;RDは20〜100mm(より好ましくは、20〜80mm、最も好ましくは、25〜50mm)である。
Claims (9)
- ケミカルメカニカル研磨パッド用の研磨層を形成する方法であって、
金型基部および金型基部に取り付けられた囲壁部を有する金型を準備する工程と、
上面、底面および2〜10cmの平均厚さを持つライナーを準備する工程と、
ライナー接着剤を準備する工程と、
窓用ブロックを準備する工程と、
窓接着剤を準備する工程と、
液状プレポリマー及び複数の微小成分を含む硬化性材料を準備する工程と、
ノズル開口部を有するノズルを準備する工程と、
刃先を持つ薄片化ブレードを準備する工程と、
革砥を準備する工程と、
ストロッピング研磨剤を準備する工程と、
ライナーの上面と囲壁部とが金型キャビティを画定するように、ライナー接着剤を使用してライナーの底面と金型基部とを接着する工程と、
窓接着剤を使用して窓用ブロックとライナーの上面とを接着する工程と、
装填時間CPの間、ノズル開口部を通して金型キャビティに硬化性材料を装填する工程と、
ここで、ライナーの上面が金型キャビティの水平内部境界を画定し、金型の水平内部境界がx−y平面に沿って向いており、金型キャビティがx−y平面と垂直の中心軸Caxisを有し、金型キャビティがドーナツ穴領域およびドーナツ領域を有し、
装填時間CPが初期段階、転移段階および残段階として区別される三つの個別の段階に分割され、ノズル開口部がある位置を有しており、硬化性材料を金型キャビティ内に溜める際にそのノズル開口部の位置が金型キャビティ内の硬化性材料の上面の上方に維持されるように、装填時間CPの間、金型基部に対して金型キャビティの中心軸Caxisに沿って移動し、
初期段階の全体にわたってノズル開口部の位置がドーナツ穴領域内にあり、
転移段階の間、ノズル開口部の位置がドーナツ穴領域内にある状態からドーナツ領域内にある状態へと転移し、
金型キャビティ内の硬化性材料をケーキへと硬化させる工程と、
ここで、ケーキを切り出す間、ノズル開口部の位置がドーナツ領域内にあり、
金型基部およびケーキから囲壁部を分離させる工程と、
ストロッピング研磨剤を刃先に適用する工程と、
薄片化ブレードを革砥で研ぐ工程と、
ケーキを各研磨層が一体化窓を有する複数のケミカルメカニカル研磨層に薄く切り出す工程と、
を含む方法。 - 熱源を準備する工程と、
ケーキを複数のケミカルメカニカル研磨層に薄く切り出す前に、ケーキを熱源にさらす工程とをさらに含む、請求項1記載の方法。 - 残段階の間、ノズル開口部の位置の移動が金型キャビティの中心軸Caxisに対するその動きを一時的に停止する、請求項1記載の方法。
- 装填時間CPの間、硬化性材料が本質的に一定の流量で金型キャビティに装填され、その平均装填流量CRavgが0.015〜2kg/secである、請求項1記載の方法。
- 金型キャビティが金型キャビティの中心軸Caxisを中心に対称である、請求項1記載の方法。
- 金型キャビティが実質的に円形の断面Cx−sectを有する略直円柱形状領域の形状であり、金型キャビティが金型キャビティの中心軸Caxisと一致する対称軸Cx−symを有し、直円柱形状領域が以下に定義される断面積Cx−areaを有し、
Cx−area=πrC 2
ここで、rCはx−y平面上に投影される金型キャビティの断面積Cx−areaの平均半径であり、ドーナツ穴領域はx−y平面上に円形断面DHx−sectを投影し、対称軸DHaxisを有する、金型キャビティ内の直円柱形状領域であり、ドーナツ穴は以下に定義される断面積DHx−areaを有し、
DHx−area=πrDH 2
ここで、rDHはドーナツ穴領域の円形断面DHx−sectの半径であり、ドーナツ領域はx−y平面上に環状断面Dx−sectを投影し、ドーナツ領域対称軸Daxisを有する、金型キャビティ内のトロイド形状領域であり、環状断面Dx−sectは以下に定義される断面積Dx−areaを有し、
Dx−area=πRD 2−πrD 2
ここで、RDはドーナツ領域の環状断面Dx−sectの長半径であり、rDはドーナツ領域の環状断面Dx−sectの短半径であり、rD≧rDHであり、RD>rDであり、RD<rCであり、Cx−sym、DHaxisおよびDaxisの各々がx−y平面と垂直である、請求項5記載の方法。 - RD≦(K*rC)であり、Kが0.01〜0.2である、請求項6記載の方法。
- rD=rDHであり、rDが5〜25mmであり、RDが20〜100mmであり、rCが20〜100cmである、請求項6記載の方法。
- 本発明の方法を使用して生成されたケーキが、装填時間CPの全体にわたってノズル開口部の位置が金型キャビティの中心軸Caxisに沿って一次元でのみ移動する以外は同じプロセスを使用して生成されたもう一つのケーキと比較して、より少ない密度欠陥を含有する、請求項8記載の方法。
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US13/427,408 | 2012-03-22 | ||
| US13/427,408 US8986585B2 (en) | 2012-03-22 | 2012-03-22 | Method of manufacturing chemical mechanical polishing layers having a window |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| JP2013197597A JP2013197597A (ja) | 2013-09-30 |
| JP2013197597A5 JP2013197597A5 (ja) | 2016-04-28 |
| JP6091276B2 true JP6091276B2 (ja) | 2017-03-08 |
Family
ID=49112321
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2013058848A Expired - Fee Related JP6091276B2 (ja) | 2012-03-22 | 2013-03-21 | 窓を有するケミカルメカニカル研磨層の製造方法 |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US8986585B2 (ja) |
| JP (1) | JP6091276B2 (ja) |
| KR (1) | KR102028208B1 (ja) |
| CN (1) | CN103358226B (ja) |
| DE (1) | DE102013004942A1 (ja) |
| FR (1) | FR2988316B1 (ja) |
| TW (1) | TWI551397B (ja) |
Families Citing this family (21)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US9034063B2 (en) * | 2012-09-27 | 2015-05-19 | Rohm And Haas Electronic Materials Cmp Holdings, Inc. | Method of manufacturing grooved chemical mechanical polishing layers |
| US9216489B2 (en) * | 2014-03-28 | 2015-12-22 | Rohm And Haas Electronic Materials Cmp Holdings, Inc. | Chemical mechanical polishing pad with endpoint detection window |
| US9873180B2 (en) | 2014-10-17 | 2018-01-23 | Applied Materials, Inc. | CMP pad construction with composite material properties using additive manufacturing processes |
| SG10202002601QA (en) | 2014-10-17 | 2020-05-28 | Applied Materials Inc | Cmp pad construction with composite material properties using additive manufacturing processes |
| US10875145B2 (en) | 2014-10-17 | 2020-12-29 | Applied Materials, Inc. | Polishing pads produced by an additive manufacturing process |
| US9776361B2 (en) | 2014-10-17 | 2017-10-03 | Applied Materials, Inc. | Polishing articles and integrated system and methods for manufacturing chemical mechanical polishing articles |
| US10875153B2 (en) | 2014-10-17 | 2020-12-29 | Applied Materials, Inc. | Advanced polishing pad materials and formulations |
| US10821573B2 (en) | 2014-10-17 | 2020-11-03 | Applied Materials, Inc. | Polishing pads produced by an additive manufacturing process |
| US10399201B2 (en) | 2014-10-17 | 2019-09-03 | Applied Materials, Inc. | Advanced polishing pads having compositional gradients by use of an additive manufacturing process |
| US11745302B2 (en) | 2014-10-17 | 2023-09-05 | Applied Materials, Inc. | Methods and precursor formulations for forming advanced polishing pads by use of an additive manufacturing process |
| CN113103145B (zh) | 2015-10-30 | 2023-04-11 | 应用材料公司 | 形成具有期望ζ电位的抛光制品的设备与方法 |
| US10593574B2 (en) | 2015-11-06 | 2020-03-17 | Applied Materials, Inc. | Techniques for combining CMP process tracking data with 3D printed CMP consumables |
| US10391605B2 (en) | 2016-01-19 | 2019-08-27 | Applied Materials, Inc. | Method and apparatus for forming porous advanced polishing pads using an additive manufacturing process |
| US20180304539A1 (en) | 2017-04-21 | 2018-10-25 | Applied Materials, Inc. | Energy delivery system with array of energy sources for an additive manufacturing apparatus |
| US11471999B2 (en) | 2017-07-26 | 2022-10-18 | Applied Materials, Inc. | Integrated abrasive polishing pads and manufacturing methods |
| US11072050B2 (en) * | 2017-08-04 | 2021-07-27 | Applied Materials, Inc. | Polishing pad with window and manufacturing methods thereof |
| WO2019032286A1 (en) | 2017-08-07 | 2019-02-14 | Applied Materials, Inc. | ABRASIVE DISTRIBUTION POLISHING PADS AND METHODS OF MAKING SAME |
| WO2020050932A1 (en) | 2018-09-04 | 2020-03-12 | Applied Materials, Inc. | Formulations for advanced polishing pads |
| US11813712B2 (en) | 2019-12-20 | 2023-11-14 | Applied Materials, Inc. | Polishing pads having selectively arranged porosity |
| US11806829B2 (en) | 2020-06-19 | 2023-11-07 | Applied Materials, Inc. | Advanced polishing pads and related polishing pad manufacturing methods |
| US11878389B2 (en) | 2021-02-10 | 2024-01-23 | Applied Materials, Inc. | Structures formed using an additive manufacturing process for regenerating surface texture in situ |
Family Cites Families (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1916330A1 (de) | 1969-03-29 | 1970-10-08 | Richard Zippel & Co Kg Farbspr | Anlage zur Herstellung von grossen oder kompliziert geformten Formteilen aus fluessigen Mehrkomponenten-Kunststoffen |
| US4158535A (en) | 1977-01-25 | 1979-06-19 | Olin Corporation | Generation of polyurethane foam |
| MY114512A (en) | 1992-08-19 | 2002-11-30 | Rodel Inc | Polymeric substrate with polymeric microelements |
| US5762544A (en) * | 1995-10-27 | 1998-06-09 | Applied Materials, Inc. | Carrier head design for a chemical mechanical polishing apparatus |
| US6012971A (en) * | 1997-03-14 | 2000-01-11 | Edgecraft Corporation | Sharpening apparatus |
| US6095905A (en) * | 1998-07-01 | 2000-08-01 | Molecular Optoelectronics Corporation | Polishing fixture and method |
| GB0008553D0 (en) | 2000-04-06 | 2000-05-24 | Unilever Plc | Process and apparatus for the production of a detergent bar |
| JP2002100593A (ja) * | 2000-09-21 | 2002-04-05 | Nikon Corp | 研磨装置、これを用いた半導体デバイスの製造方法及びこの製造方法により製造された半導体デバイス |
| TWI220405B (en) * | 2002-11-19 | 2004-08-21 | Iv Technologies Co Ltd | Method of fabricating a polishing pad having a detection window thereon |
| TW592894B (en) * | 2002-11-19 | 2004-06-21 | Iv Technologies Co Ltd | Method of fabricating a polishing pad |
| TWI385050B (zh) | 2005-02-18 | 2013-02-11 | 奈平科技股份有限公司 | 用於cmp之特製拋光墊及其製造方法及其用途 |
| WO2007089004A1 (ja) * | 2006-02-03 | 2007-08-09 | Jsr Corporation | 化学機械研磨パッド |
| CN101134303A (zh) * | 2006-08-30 | 2008-03-05 | 力晶半导体股份有限公司 | 抛光垫及其制造方法 |
| JP2008238349A (ja) * | 2007-03-28 | 2008-10-09 | Toray Ind Inc | 研磨パッド用材料のスライス方法 |
| US8585790B2 (en) * | 2009-04-23 | 2013-11-19 | Applied Materials, Inc. | Treatment of polishing pad window |
| US8552980B2 (en) | 2009-04-30 | 2013-10-08 | Gregory A. Shaver | Computer input devices and associated computing devices, software, and methods |
| TWI396602B (zh) * | 2009-12-31 | 2013-05-21 | Iv Technologies Co Ltd | 具有偵測窗之研磨墊的製造方法及具有偵測窗之研磨墊 |
| US9017140B2 (en) * | 2010-01-13 | 2015-04-28 | Nexplanar Corporation | CMP pad with local area transparency |
| CN102133734B (zh) * | 2010-01-21 | 2015-02-04 | 智胜科技股份有限公司 | 具有侦测窗的研磨垫及其制造方法 |
-
2012
- 2012-03-22 US US13/427,408 patent/US8986585B2/en not_active Expired - Fee Related
-
2013
- 2013-03-21 TW TW102109983A patent/TWI551397B/zh not_active IP Right Cessation
- 2013-03-21 JP JP2013058848A patent/JP6091276B2/ja not_active Expired - Fee Related
- 2013-03-21 DE DE102013004942A patent/DE102013004942A1/de not_active Withdrawn
- 2013-03-22 CN CN201310262744.6A patent/CN103358226B/zh not_active Expired - Fee Related
- 2013-03-22 KR KR1020130030756A patent/KR102028208B1/ko not_active Expired - Fee Related
- 2013-03-22 FR FR1352614A patent/FR2988316B1/fr not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| US8986585B2 (en) | 2015-03-24 |
| TW201404537A (zh) | 2014-02-01 |
| US20130247477A1 (en) | 2013-09-26 |
| FR2988316A1 (fr) | 2013-09-27 |
| JP2013197597A (ja) | 2013-09-30 |
| TWI551397B (zh) | 2016-10-01 |
| KR102028208B1 (ko) | 2019-10-02 |
| CN103358226A (zh) | 2013-10-23 |
| DE102013004942A1 (de) | 2013-09-26 |
| FR2988316B1 (fr) | 2016-06-10 |
| CN103358226B (zh) | 2016-02-24 |
| KR20130108172A (ko) | 2013-10-02 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6026931B2 (ja) | ケミカルメカニカル研磨層の製造方法 | |
| JP2013197597A (ja) | 窓を有するケミカルメカニカル研磨層の製造方法 | |
| TWI577706B (zh) | 化學機械硏磨墊 | |
| TW201433628A (zh) | 柔軟且可調理之化學機械研磨墊 | |
| JP2015047692A (ja) | 基材を化学機械研磨する方法 | |
| JP2017052079A (ja) | ケミカルメカニカル研磨パッドのための複合研磨層の製造方法 | |
| JP5900227B2 (ja) | ケミカルメカニカルポリッシング層の製造方法 | |
| JP2013039663A5 (ja) | ||
| JP2017013224A (ja) | ケミカルメカニカル研磨パッドのための研磨層の製造方法 | |
| TWI542616B (zh) | 製造化學機械硏磨層之方法 | |
| JP6238664B2 (ja) | 溝付き化学機械研磨層の製造方法 | |
| TWI592256B (zh) | 製造化學機械硏磨層之改良方法 | |
| JP2017052078A (ja) | ケミカルメカニカル研磨パッド及び同研磨パッドの製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| RD04 | Notification of resignation of power of attorney |
Free format text: JAPANESE INTERMEDIATE CODE: A7424 Effective date: 20150303 |
|
| RD04 | Notification of resignation of power of attorney |
Free format text: JAPANESE INTERMEDIATE CODE: A7424 Effective date: 20160222 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20160309 |
|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20160309 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20161013 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20161018 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20161216 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20170124 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20170207 |
|
| R150 | Certificate of patent or registration of utility model |
Ref document number: 6091276 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| S802 | Written request for registration of partial abandonment of right |
Free format text: JAPANESE INTERMEDIATE CODE: R311802 |
|
| R350 | Written notification of registration of transfer |
Free format text: JAPANESE INTERMEDIATE CODE: R350 |
|
| LAPS | Cancellation because of no payment of annual fees |