JP7204184B2 - Vehicle door seal material - Google Patents
Vehicle door seal material Download PDFInfo
- Publication number
- JP7204184B2 JP7204184B2 JP2018214951A JP2018214951A JP7204184B2 JP 7204184 B2 JP7204184 B2 JP 7204184B2 JP 2018214951 A JP2018214951 A JP 2018214951A JP 2018214951 A JP2018214951 A JP 2018214951A JP 7204184 B2 JP7204184 B2 JP 7204184B2
- Authority
- JP
- Japan
- Prior art keywords
- component
- door
- vehicle
- sealing material
- vehicle door
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Landscapes
- Seal Device For Vehicle (AREA)
- Sealing Material Composition (AREA)
Description
本発明は、車両用ドアシール材に関する。更に詳しくは、自動車の各種ドアや車両本体に開口した車両開口部等に沿って取設され、ドアを閉じた際に雨水の車両内部への浸入等を防止するための高シール性を備えた車両用ドアシール材に関する。 The present invention relates to a vehicle door seal material. More specifically, it is installed along various vehicle doors and vehicle openings in the vehicle body, and has high sealing performance to prevent rainwater from entering the vehicle interior when the door is closed. It relates to a vehicle door seal material.
従来、車両用ドアシール材(「車両用ウェザーストリップ」とも呼称される。)は、可動部材としてのドア及び/または固定部材としての車両本体の車両開口部の周縁に沿って取設されている(例えば、特許文献1参照)。例えば、車両用ドアシール材(以下、単に「シール材」と称す。)の取設されたドアを車両開口部に近接させて閉じた状態にすることで、ドア及び車両本体の間に当該シール材が挟まれた状態となる。なお、シール材は、ドア側または車両本体側のいずれか一方または双方に取設されるものであっても構わない。 Conventionally, a vehicle door seal material (also referred to as a "vehicle weather strip") is attached along the periphery of a vehicle opening of a door as a movable member and/or a vehicle body as a fixed member ( For example, see Patent Document 1). For example, by closing a door on which a vehicle door seal material (hereinafter simply referred to as "seal material") is attached to the opening of the vehicle, the seal material is placed between the door and the vehicle body. is sandwiched. The sealing material may be attached to either one or both of the door side and the vehicle body side.
シール材は、応力に対して弾性変形可能なゴム材料から主に構成されている。そのため、ドア及び車両本体の間に挟まれた状態では、少なくとも一部が押し潰されて変形した状態となる。このとき、シール材には応力の負荷されていない元の形状に戻ろうとする復元力(反発力)が働くため、押し潰されたシール材の一部の面がドアまたは車両本体に密着する。その結果、車両外部及び車両内部の間を水等が流通することが規制され、シール材によって車両内部が密閉された状態となる。 The sealing material is mainly made of a rubber material that is elastically deformable against stress. Therefore, when sandwiched between the door and the vehicle body, at least a portion thereof is crushed and deformed. At this time, a restoring force (repulsive force) acts on the sealing material to return it to its original shape where no stress is applied, so that a part of the surface of the crushed sealing material comes into close contact with the door or the vehicle body. As a result, water or the like is restricted from flowing between the vehicle exterior and the vehicle interior, and the interior of the vehicle is sealed by the sealing material.
これにより、車両外部から車両内部への虫や高圧の洗車水等の水の浸入を防いだり、水以外の塵や埃等の細かな夾雑物の侵入、或いは、車両外部の騒音、臭い、または風等の侵入等を防止したりすることができる。すなわち、シール材によって、運転中のドライバーや同乗者を不快にさせることがなく、快適な車内空間を保った状態にすることができる。 This prevents insects and water such as high-pressure car wash water from entering the vehicle from the outside of the vehicle, the entry of fine contaminants such as dust and dirt other than water, or the noise, odor, or noise from the outside of the vehicle. Intrusion of wind or the like can be prevented. In other words, the sealing material does not make the driver and fellow passengers uncomfortable while driving, and a comfortable interior space can be maintained.
更に、シール材は、車両外部及び車両内部の空気の流出入を併せて抑制することができる。そのため、車両内部から車両外部(また、車両外部から車両内部)への暖気または冷気の流出入を抑制することができる。その結果、エアーコンディショニング装置によって調整された車内温度を安定して維持することができる。そのため、ガソリンの消費量等を抑えるなど燃費性能に優れ、かつ高い環境性能の維持を図ることができる。 Furthermore, the sealing material can suppress the inflow and outflow of air both to the outside of the vehicle and to the inside of the vehicle. Therefore, it is possible to suppress the inflow and outflow of warm air or cold air from the inside of the vehicle to the outside of the vehicle (or from the outside of the vehicle to the inside of the vehicle). As a result, the vehicle interior temperature adjusted by the air conditioning device can be stably maintained. Therefore, it is possible to maintain excellent fuel efficiency, such as by suppressing the consumption of gasoline, etc., and to maintain high environmental performance.
上記したように、シール材は、乗用車またはその他各種車両等において重要な機能を発揮するものである。ここで、シール材の基本的な構造について説明すると、シール材は、ドアや車両本体の車両開口部等に周知の固定手段(例えば、クリップ等)を介して固定される略板状のシール基部と、当該シール基部と一体的に成形され、ドアを閉じた状態にした際に一部が押し潰され、変形する中空構造のシール部とを具備して主に構成されている。なお、シール部のシール外面から所定方向に突出した板状のリップ部を備えたシール材も形成されている。 As described above, the sealing material exhibits important functions in passenger cars and various other vehicles. Here, the basic structure of the sealing material will be described. The sealing material is a substantially plate-shaped seal base that is fixed to a door or a vehicle opening of a vehicle body via a known fixing means (for example, a clip or the like). and a seal portion of a hollow structure that is molded integrally with the seal base portion and partially crushed and deformed when the door is closed. A sealing material having a plate-shaped lip portion projecting in a predetermined direction from the seal outer surface of the seal portion is also formed.
上述した通り、シール材は弾性変形可能なゴム材料などの樹脂材料を主原料として形成され、所定の温度に加熱して粘度を調整した主原料を押出成形技術や型成形技術(射出成形技術)等の周知の樹脂成形技術を用いて所望の形状に形成されている。シール材は、ドアの周縁に沿って取設される長尺状のものであるため、主に押出成形技術によって形成されている。ここで、主原料として使用されるゴム材料(樹脂材料)としては、例えば、エチレン・プロピレン・ジエンゴム(EPDM)、或いはその他の熱可塑性エラストマー等が主に用いられることが多い。 As mentioned above, the sealing material is formed mainly from elastically deformable resin materials such as rubber materials, and is heated to a predetermined temperature to adjust the viscosity. It is formed into a desired shape using a well-known resin molding technique such as. Since the sealing material is elongated to be installed along the perimeter of the door, it is mainly formed by an extrusion technique. Here, as the rubber material (resin material) used as the main raw material, for example, ethylene-propylene-diene rubber (EPDM) or other thermoplastic elastomers are mainly used in many cases.
上記に示した通り、シール材は、止水効果等の高いシール性を備えた有用な部材の一つである。更に、シール部の形状や原料として使用する樹脂材料を適宜選択し、より高いシール性を発揮させることが可能であった。しかしながら、高いシール性のみを追求すると、下記に掲げる不具合を生じることがあった。 As described above, the sealing material is one of useful members having high sealing properties such as a water stopping effect. Furthermore, it was possible to appropriately select the shape of the sealing portion and the resin material used as the raw material to exhibit higher sealing performance. However, if only high sealability is pursued, the following problems may occur.
すなわち、高いシール性を獲得するためには、ドアを閉めた状態で、一方(例えば、ドア側)から他方(例えば、車両本体側)に向かって、強い力でシール部を押し付ける必要があった。すなわち、シール部を構成する樹脂材料は、高い反発力(反発性)が求められていた。特に、近年においては車両内部に高性能のスピーカー等のオーディオ機器が搭載され、車内で高音質の音楽を楽しむ人々も増えている。そのため、車両内部の音が車両外部に漏れないようにするために高い遮音性が求められることがある。これにより、高い反発力を備えたシール部が採用されることが多くなっている。 That is, in order to obtain high sealing performance, it was necessary to press the seal portion with a strong force from one side (for example, the door side) toward the other side (for example, the vehicle body side) while the door was closed. . In other words, a high repulsive force (resilience) is required for the resin material forming the seal portion. In particular, in recent years, audio equipment such as high-performance speakers have been mounted inside vehicles, and more and more people are enjoying high-quality music in the vehicles. Therefore, in order to prevent the sound inside the vehicle from leaking to the outside of the vehicle, high sound insulation is sometimes required. As a result, a seal portion having a high repulsive force is often used.
ここで、反発力が弱い場合、シール材と密着した車両本体等との間に隙間が生じる可能性があり、当該隙間から水や塵等が浸入(または侵入)するおそれがあった。そのため、ある程度の反発力の強さは必要であった。 Here, if the repulsive force is weak, there is a possibility that a gap will be formed between the sealing material and the vehicle body or the like that is in close contact, and there is a risk that water, dust, etc. will enter (or enter) through the gap. Therefore, a certain degree of repulsive force was required.
一方、反発力が強すぎると、ドアを確実に閉じるために必要な力(エネルギー)が大きくなる可能性があった。すなわち、ドアを閉めようとする際に、車両開口部等に取設されたシール材が当該ドアを閉める力を弱める可能性があった。そのため、ドアを車両本体に対して規定以上の速さ(ドア閉め速度)で、勢い良く閉めるドア閉め操作が必要となることがあった。これにより、力の弱い高齢者や子供は、ドアを確実に閉めることができず、所謂「半ドア」の状態となったり、何度かドア閉め操作を繰り返したりする必要があった。そのため、運転者等はドア閉まり性に不満を感じることがあった。 On the other hand, if the repulsive force is too strong, the force (energy) required to securely close the door may increase. That is, when trying to close the door, there is a possibility that the sealing material attached to the vehicle opening or the like weakens the force to close the door. For this reason, it has sometimes become necessary to perform a door closing operation in which the door is vigorously closed with respect to the vehicle body at a speed (door closing speed) higher than the regulation. As a result, elderly people and children with weak strength cannot close the door securely, resulting in a so-called "ajar door" state, or they have to repeat the operation of closing the door several times. As a result, drivers and the like may feel dissatisfied with the door closing performance.
上記のような高いシール性とともに、良好なドア閉まり性を確保するために、従来はシール部の形状や厚さを変更したり、樹脂材料の種類自体を変更したりすることが行われていた。シール性及びドア閉まり性は、互いに相反する性質のものであるため、双方が良好な性状を示すシール材を構築することは困難性を有していた。 In addition to the above-mentioned high sealing performance, in order to ensure good door closing performance, conventionally, the shape and thickness of the seal part have been changed, and the type of resin material itself has been changed. . Since sealing properties and door-closing properties contradict each other, it has been difficult to construct a sealing material that exhibits good properties for both.
本願発明者は、上記不具合を解消するために鋭意研究を重ねた結果、シール材の主原料となるゴム材料(樹脂材料)と、当該ゴム材料に加えられる炭素成分(カーボンブラック)のそれぞれの配合部数を調整することで、シール性及びドア閉まり性の双方の性能が良好なシール材を得ることを見出した。更に、シール材の動的粘弾性、速度依存性、及びムーニー粘度に着目し、これらの各パラメータを所定の範囲に規定することで、特にドア閉まり性の向上が図られたシール材を安定的に形成可能であることを見出したものである。 The inventors of the present application, as a result of extensive research in order to solve the above problems, found that the rubber material (resin material), which is the main raw material of the sealing material, and the carbon component (carbon black) added to the rubber material are mixed. It was found that by adjusting the number of copies, a sealing material having both excellent sealing performance and door closing performance can be obtained. Furthermore, by focusing on the dynamic viscoelasticity, velocity dependence, and Mooney viscosity of the sealing material, and by defining each of these parameters within a predetermined range, a sealing material that is particularly improved in door closing performance can be stably obtained. It has been found that it is possible to form
そこで、本発明は、上記実情に鑑み、高いシール性の維持とともに、従来と比較して小さな力(エネルギー)であってもドアを確実に閉めることの可能な良好なドア閉まり性を備えたシール材の提供を課題とするものである。 Therefore, in view of the above-mentioned circumstances, the present invention provides a seal that maintains high sealing performance and has good door closing performance that allows the door to be securely closed even with a smaller force (energy) than conventional seals. The challenge is to provide materials.
本発明によれば、上記課題を解決したドアシール材(車両用ドアシール材)が提供される。 According to the present invention, a door seal material (vehicle door seal material) that solves the above problems is provided.
[1] エチレン・プロピレン・ジエンゴムを含む第一成分、及び、カーボンブラックを含む第二成分を原材料とする車両用ドアシール材であって、前記第一成分の配合部数を前記第二成分の配合部数で除した値が、0.83~1.25の範囲であり、ムーニー粘度が、25~61ML(1+4)125℃であり、前記カーボンブラックのヨウ素吸着量が20~40mg/g、かつ、DBP吸油量が50~112cm 3 /100gの範囲である車両用ドアシール材。 [1] A vehicle door seal material containing a first component containing ethylene/propylene/diene rubber and a second component containing carbon black as raw materials, wherein the number of parts of the first component is equal to the number of parts of the second component. The value divided by 0. 83 to 1.25 , the Mooney viscosity is 25 to 61 ML (1+4) 125° C., the iodine adsorption of the carbon black is 20 to 40 mg/g, and the DBP oil absorption is 50 to 112 cm 3 /. Vehicle door seals in the range of 100 g .
[2] 動的粘弾性を示す損失正接の値が、0.095~0.210の範囲である前記[1]に記載の車両用ドアシール材。 [2] The vehicle door seal material according to [1], wherein the value of loss tangent indicating dynamic viscoelasticity is in the range of 0.095 to 0.210.
[3] 横軸を圧縮速度[m/s]、及び、縦軸を荷重変化率[%]として、圧縮速度試験の結果をプロットし、算出された近似式の傾きによって示される速度依存性[%/(m/s)]の値が、100以下である前記[1]または[2]に記載の車両用ドアシール材。 [3] Plot the results of the compression speed test with the horizontal axis as the compression speed [m / s] and the vertical axis as the load change rate [%], and the speed dependence [ %/(m/s)] value of 100 or less, the vehicle door seal material according to the above [1] or [2].
[4] 前記第一成分のムーニー粘度が、29~80ML(1+4)125℃の範囲であ
る前記[1]~[3]のいずれかに記載の車両用ドアシール材。
[ 4 ] The vehicle door seal material according to any one of [1] to [ 3 ], wherein the Mooney viscosity of the first component is in the range of 29 to 80ML(1+4)125°C.
[5] 前記第一成分及び前記第二成分に加え、軟化剤、加工助剤、充填剤、架橋剤、加硫促進剤、及び発泡剤の少なくともいずれか一種を更に原材料として含む前記[1]~[4]のいずれかに記載の車両用ドアシール材。 [ 5 ] In addition to the first component and the second component, at least one of a softening agent, a processing aid, a filler, a cross-linking agent, a vulcanization accelerator, and a foaming agent is further included as a raw material in the above [1] The vehicle door seal material according to any one of to [ 4 ].
本発明のシール材によれば、従来のシール材と同様の高いシール性を確保しつつ、小さな力で良好なドア閉まり性を発揮することができる。その結果、高齢者や子供であっても確実にドアを閉めることが可能となり、半ドアの状態からドア閉め操作を繰り返したりする必要がない。これにより、ドア閉め操作に対する不具合及び不満を解消することができる。 According to the sealing material of the present invention, it is possible to exhibit good door closing performance with a small force while ensuring high sealing performance similar to that of the conventional sealing material. As a result, even elderly people and children can securely close the door, and there is no need to repeatedly close the door when the door is ajar. As a result, inconvenience and dissatisfaction with the door closing operation can be eliminated.
以下、図面を参照しつつ、本発明のシール材(車両用ドアシール材)の実施の形態について説明する。なお、本発明のシール材は、以下の実施形態に限定されるものではなく、本発明の範囲を逸脱しない限りにおいて、種々の設計の変更、修正、改良等を加え得るものである。 EMBODIMENT OF THE INVENTION Hereinafter, embodiment of the sealing material (vehicle door sealing material) of this invention is described, referring drawings. The sealing material of the present invention is not limited to the following embodiments, and various design changes, modifications, improvements, etc. can be added without departing from the scope of the present invention.
1.シール材
本発明の一実施形態のシール材1は、乗用車等の車両のドア(または車両本体)にクリップ等の周知手段(図示しない)を介して取設されるものである。シール材1は、例えば、図1に示すように、ドア等に接し、固定される略平板状のシール基部2と、当該シール基部2と一体的に成形された断面中空状のシール部3とを主に具備して構成されるものである。ここで、図1は、本発明のシール材の構成を単純化して示したものであり、この断面形状のものに限定されるものではない。
1. Seal Material
ドア等にシール基部2が接し固定された状態で、車両本体等に近接されることにより、シール部3のシール部外表面4が車両本体の一部と接し、中空状のシール部3が押し潰され変形する。これにより、ドア及び車両本体の間に中空状のシール部3が変形した状態で挟まれることなり、シール部外表面4が反発力によって車両本体側に押し付けられる。これにより、車両本体及びシール部3のシール部外表面4の間が密となり、止水性等の高いシール性が確保される。
When the vehicle main body or the like is approached while the
更に具体的に説明すると、シール材1は、応力に対して弾性変形可能な樹脂材料(ゴム材料)を押出成形した長尺状のものである。本実施形態のシール材1は、樹脂材料として、エチレン・プロピレン・ジエンゴム(以下、「EPDM」と称す。)を主原料として用いられている。ここで、EPDMを含む成分が本発明における第一成分に相当する。
More specifically, the sealing
更に、本実施形態のシール材1は、上記第一成分に加え、カーボンブラックを含んでいる。ここで、カーボンブラックが本発明における第二成分に相当する。すなわち、上記の第一成分及び第二成分が本実施形態のシール材1の主原料となる。ここで、第一成分の樹脂成分は、上述したEPDMに限定されるものではなく、他の合成樹脂や天然樹脂等で構成されたゴム材料であっても、その他熱可塑性エラストマー等の周知のポリマー成分であっても構わない。すなわち、応力に対して弾性変形し、高いシール性を有するとともに、後述する要件を具備し、良好なドア閉まり性を備えるものであればよい。
Furthermore, the sealing
なお、シール材1には、EPDMを含む第一成分及びカーボンブラックを含む第二成分の原材料以外に、その他種々の添加剤等を含むものであっても構わない。例えば、軟化剤、加工助剤、充填剤、架橋剤、加硫促進剤、及び発泡剤等の少なくともいずれか一種を、それぞれ添加量を調整して含んでもよい。なお、これらの軟化剤等の添加については、シール材の製造において既に周知のものであるため詳細な説明は省略するものとする。
In addition to the raw materials of the first component containing EPDM and the second component containing carbon black, the sealing
本実施形態のシール材1は、上記の第一成分及び第二成分の配合部数の比率が下記に示す範囲内に規定される。すなわち、EPDMを含む第一成分の配合部数を、カーボンブラックを含む第二成分の配合部数で除した値(以下、「第一成分/第二成分比」と称す。)が、0.60~2.00の範囲であることを特徴とする。第一成分/第二成分比の値が上記範囲内である条件を満たすことにより、ドア閉まり性の良好なシール材とすることができる。第一成分/第二成分比を所定範囲に規定することに着目し、良好なドア閉まり性を備えたシール材を形成可能とすることは本発明に特有の構成である。
In the sealing
更に、本実施形態のシール材1によれば、ゴム材料の動的粘弾性を示す損失正接の値が、0.095~0.210の範囲であることを特徴とするものであっても構わない。上記の範囲内に第一成分/第二成分比の値を調整することで、ゴム材料等の材料の動的粘弾性に係る損失正接(tanδ)の値を上記範囲内にすることができる。
Furthermore, according to the sealing
「動的粘弾性」とは、ドアを閉じる際のドア閉まり性に大きく寄与するゴム材料等の性質の一つである。ゴム材料等の樹脂材料は、単一または複数の分子が多数結合した高分子材料である。高分子材料は、一般的に、「弾性」及び「粘性」のそれぞれの中間の性質である「粘弾性」の性状を呈している。 "Dynamic viscoelasticity" is one of the properties of a rubber material or the like that greatly contributes to the door closing performance when the door is closed. A resin material such as a rubber material is a polymeric material in which a large number of single or multiple molecules are bonded. Polymeric materials generally exhibit “viscoelastic” properties, which are properties intermediate between “elastic” and “viscous” properties.
更に具体的に説明すると、「弾性」とは、“変形に必要な力は、変形の大きさによって主に決定され、変形の速度には依存しない”性質を備えるものであり、一方、「粘性」とは、“変形に必要な力は、変形の速度によって主に決定され、変形の大きさには依存しない”性質を備えるものと一般的に定義される。理想的なゴムは弾性体の一例であり、水飴状のものが粘性体の一例である。 More specifically, "elasticity" has the property that "the force required for deformation is mainly determined by the magnitude of deformation and does not depend on the speed of deformation". is generally defined as having the property that "the force required for deformation is determined primarily by the rate of deformation and is independent of the magnitude of deformation". An ideal rubber is an example of an elastic body, and starch syrup is an example of a viscous body.
粘弾性体としての性状を有する樹脂材料に対し、弾性の性質及び粘性の性質のどちらかが強く寄与しているかを評価するための指標として、損失正接(tanδ)の値が用いられることがある。一般的には、樹脂材料等の材料の力学物性に対する粘性の寄与(E”)を、弾性の寄与(E’)で除した値(E”/E’≒tanδ)が損失正接として求められる。 A value of loss tangent (tan δ) is sometimes used as an index for evaluating whether elastic properties or viscous properties strongly contribute to a resin material having properties as a viscoelastic body. . In general, the value (E″/E′≈tan δ) obtained by dividing the contribution of viscosity (E″) to the mechanical properties of a material such as a resin material by the contribution of elasticity (E′) is obtained as the loss tangent.
すなわち、損失正接の値が0に近似するほど、その材料は弾性体の性質を強く有し、一方、損失正接の値が大きくなるほど粘性体の性質を有する材料となる。本発明のシール材は、損失正接の値が0.095~0.210の範囲内であることを特徴とするものであり、弾性体及び粘性体の双方の性質を有することになる。 That is, the closer the value of the loss tangent to 0, the stronger the material has properties of an elastic body, while the larger the value of the loss tangent, the more the material has the properties of a viscous body. The sealing material of the present invention is characterized by having a loss tangent value within the range of 0.095 to 0.210, and has properties of both an elastic body and a viscous body.
損失正接の値が0.095よりも低い場合は、弾性体としての性質が強くなり、後述するムーニー粘度の値が低くなり加工性が悪化する。一方、損失正接の値が0.210を超える場合、粘性体としての性質が強くなる。そのため、損失性質の値を上記範囲に規定することで、高シール性と良好なドア閉まり性の双方を作用効果を奏するシール材を形成することができる。なお、損失正接の値の測定等についての詳細は後述する。 When the loss tangent value is lower than 0.095, the property as an elastic body becomes strong, the value of the Mooney viscosity described later becomes low, and the processability deteriorates. On the other hand, when the loss tangent value exceeds 0.210, the property as a viscous body becomes strong. Therefore, by defining the value of the loss property within the above range, it is possible to form a sealing material that exhibits both high sealing performance and good door closing performance. The details of the measurement of the loss tangent value will be described later.
更に、本実施形態のシール材1は、横軸を圧縮速度[m/s]、及び、縦軸を荷重変化率[%]として、圧縮速度試験を行い、その試験結果をプロットし、算出された近似式の傾きによって示される速度依存性[%/(m/s)]の値が100以下であることを特徴とするものであっても構わない。すなわち、ドアを閉める際にシール材1に圧力が加わる際の圧縮速度と荷重変化率に基づいて速度依存性が算出され、その値が100以下のシール材1が良好なドア閉まり性を有する。なお、圧縮速度試験の具体例についての詳細は後述する。
Furthermore, the sealing
また、本実施形態のシール材1は、シール材1自体のムーニー粘度が25~69ML(1+4)125℃の範囲であることを特徴するものであってもよい。ここで、ムーニー粘度(M)は、ゴム材料等の塑性を評価するための単位であり、評価対象の試料を所定の温度で加熱した後、当該温度を保ちながら毎分2回転するローターに加わるトルクを求め、当該トルクの値から算出したものである。なお、所定の加熱温度(例えば、125℃)で試料を加熱し、1分間の予備加熱後、L形ローターを回転させ、4分後の値(ムーニー値)を“ML(1+4)125℃”として表示する。なお、ムーニー粘度の測定の詳細は後述する。
Further, the sealing
加えて、シール材1の原料となる第一成分のムーニー粘度が、29~80ML(1+4)125℃の範囲であることを特徴としてもよい。ムーニー粘度については、既に説明をしたため、ここでは詳細な説明は省略する。シール材1の全体のムーニー粘度は、第一成分のムーニー粘度が大きく寄与するためである。
In addition, the mooney viscosity of the first component, which is the raw material of the sealing
以下、本発明のシール材について、下記の実施例に基づいて説明するが、本発明の製造方法は、これらの実施例に限定されるものではない。 The sealing material of the present invention will be described below based on the following examples, but the manufacturing method of the present invention is not limited to these examples.
1.試料(シール材)の作成
エチレン・プロピレン・ジエンゴムを含む第一成分、及び、カーボンブラックを含む第二成分を主たる原材料として混合し、周知の押出成形機によって長尺状に押出成形することで所望の形状(図1等参照)のシール材を作成した。
1. Preparation of sample (sealing material) The first component containing ethylene/propylene/diene rubber and the second component containing carbon black are mixed as the main raw materials, and the mixture is extruded into a long shape using a well-known extruder. A sealing material having a shape (see FIG. 1, etc.) was prepared.
第一成分に含まれるEPDMとして、ムーニー粘度の異なる3種類のエチレン・プロピレン・ジエンゴム(EPDM1、EPDM2、EPDM3)をそれぞれ用いた(下記表1参照)。なお、EPDM3は、油展ポリマーであり、樹脂成分(EPDM):100phr、油展:20phrのものを用いた。そのため、EPDM3については、後述する第一成分/第二成分比については、上記油展率を考慮した上での算出を行っている。すなわち、EPDM3の実配合部数Xに、油展率Yを乗じた値をEPDM3の配合部数としている。ここで、油展率Yは、上記例では、樹脂成分/(樹脂成分+油展)=100/(100+20)であり、約0.83となる。 As the EPDM contained in the first component, three types of ethylene-propylene-diene rubbers (EPDM1, EPDM2, and EPDM3) with different Mooney viscosities were used (see Table 1 below). EPDM3 is an oil-extended polymer, and resin component (EPDM): 100 phr, oil-extended: 20 phr was used. Therefore, for EPDM3, the ratio of the first component/second component, which will be described later, is calculated in consideration of the oil extension ratio. That is, the value obtained by multiplying the actual blending number X of EPDM3 by the oil extension rate Y is the blending number of EPDM3. Here, in the above example, the oil extension rate Y is resin component/(resin component + oil extension)=100/(100+20), which is approximately 0.83.

一方、第二成分に含まれるカーボンブラックとして、粒径、ヨウ素吸着量、及びDBP吸油量のそれぞれ異なる3種類のカーボンブラック(CB1、CB2、CB3)を用いた(下記、表2参照)。 On the other hand, as the carbon black contained in the second component, three types of carbon black (CB1, CB2, CB3) having different particle sizes, iodine adsorption amounts, and DBP oil absorption amounts were used (see Table 2 below).

なお、上記第一成分及び第二成分以外に、その他原料として、軟化剤としてパラフィンオイル、加工助剤としてステアリン酸及び酸化亜鉛、充填剤として炭酸カルシウム、架橋剤として硫黄を加えている。また、加硫促進剤及び発泡剤等も適宜加えている。 In addition to the above first and second components, other raw materials include paraffin oil as a softening agent, stearic acid and zinc oxide as processing aids, calcium carbonate as a filler, and sulfur as a cross-linking agent. In addition, a vulcanization accelerator, a foaming agent, and the like are added as appropriate.
下記表3に示すように、使用する第一成分及び第二成分の種類、及び各成分の配合部数[phr]を変化させることにより、実施例1~7及び比較例1,2のシール材に押出成形する前の原料を調製した。なお、第一成分及び第二成分の種類及び配合部数を変化させる以外、すなわち、軟化剤や加工助剤等の配合部数は実施例1~7及び比較例1,2において同一のものとした。 As shown in Table 3 below, the sealing materials of Examples 1 to 7 and Comparative Examples 1 and 2 were obtained by changing the types of the first and second components used and the number of parts [phr] of each component. A stock was prepared prior to extrusion. In Examples 1 to 7 and Comparative Examples 1 and 2, the same number of softening agents, processing aids, etc. were used, except for changing the types and number of parts of the first and second components.
このようにして得られた原料を周知の押出成形機を用いて所望の形状の押出成形することで、図1に示すような試験形状のシール材を形成した。なお、用いた押出成形機及び押出成形技術は、既存のシール材を形成する際に使用される周知のものであり、ここでは詳細な説明は省略する。更に、第一成分及び第二成分の種類及び配合部数以外に、押出成形を行う原料の加熱温度や押出圧力等の種々の条件についてはいずれも同じものとした。 The raw material thus obtained was extruded into a desired shape using a well-known extruder to form a sealing material having a test shape as shown in FIG. The extruder and extrusion molding technique used are well-known ones used when forming existing sealing materials, and detailed description thereof is omitted here. Furthermore, other than the type and number of parts of the first component and the second component, various conditions such as the heating temperature and extrusion pressure of the raw material for extrusion were the same.
2.第一成分/第二成分比
上記の通り、原料を調製し形成された実施例1~7及び比較例1,2のシール材に係る第一成分/第二成分比の値を下記表3に示す。ここで、前述したように、第一成分のEPDM3については油展ポリマーのため油展率を考慮して算出を行っている。これによると、実施例1~7は、本発明において規定された第一成分/第二成分比の範囲(0.60~2.00)を満たすものであり、比較例1は第一成分/第二成分比の上限値を超えるもの、比較例2は第一成分/第二成分比の下限値を超え、いずれも本発明において規定された第一成分/第二成分比を逸脱するものである。
2. First Component/Second Component Ratio Values of the first component/second component ratio of the sealing materials of Examples 1 to 7 and Comparative Examples 1 and 2 formed by preparing the raw materials as described above are shown in Table 3 below. show. Here, as described above, since EPDM3 as the first component is an oil-extended polymer, the calculation is performed in consideration of the oil extension ratio. According to this, Examples 1 to 7 satisfy the first component / second component ratio range (0.60 to 2.00) specified in the present invention, and Comparative Example 1 is the first component / Those exceeding the upper limit of the second component ratio and Comparative Example 2 exceeded the lower limit of the first component/second component ratio, and both deviated from the first component/second component ratio specified in the present invention. be.

3.シール材の評価
上記の通り、第一成分/第二成分を考慮して形成された実施例1~7及び比較例1,2のシール材についてそれぞれ評価した結果を以下に示す。
3. Evaluation of Seal Material As described above, the evaluation results of the seal materials of Examples 1 to 7 and Comparative Examples 1 and 2, which were formed in consideration of the first component/second component, are shown below.
3-1.損失正接(動的粘弾性)の評価
損失正接(tanδ)の値は、JIS K6394:2007(加硫ゴム及び熱可塑性ゴム-動的性質の求め方-一般指針)に準拠して算出した。更に具体的に説明すると、粘弾性を測定するための測定機器として、粘弾性測定装置RSA-3(TA INSTRUMENTS製)を用い、上記の通り作成された実施例1~7、及び比較例1、2のシール材からそれぞれ直径6mm、高さ2~3mm程度の円柱状の測定用試験片をそれぞれ切り出し、粘弾性測定装置にセットし、計測を行った。
3-1. Evaluation of loss tangent (dynamic viscoelasticity) The value of loss tangent (tan δ) was calculated in accordance with JIS K6394:2007 (vulcanized rubber and thermoplastic rubber-determination of dynamic properties-general guidelines). More specifically, Examples 1 to 7 and Comparative Example 1, which were prepared as described above, using a viscoelasticity measuring device RSA-3 (manufactured by TA INSTRUMENTS) as a measuring instrument for measuring viscoelasticity. A cylindrical test piece for measurement having a diameter of 6 mm and a height of about 2 to 3 mm was cut out from each of the sealing materials No. 2, set in a viscoelasticity measuring device, and measured.
この場合、測定条件は、試験回数:n=3、変形方法:圧縮方法、静的歪み:10%、動的歪み:±0.1%、測定周波数:1Hzに統一して行った。当該測定条件に基づいて動的粘弾性が測定され、算出された損失正接(tanδ)の値を上記表3に示す。これによると、比較例1,2以外は全て本発明において規定された損失正接の値の条件(0.095~0.210)を満たしていることが確認された。 In this case, the measurement conditions were uniform: number of tests: n=3, deformation method: compression method, static strain: 10%, dynamic strain: ±0.1%, measurement frequency: 1 Hz. The dynamic viscoelasticity was measured based on the measurement conditions, and the calculated loss tangent (tan δ) values are shown in Table 3 above. According to this, it was confirmed that all samples other than Comparative Examples 1 and 2 satisfied the loss tangent value condition (0.095 to 0.210) specified in the present invention.
一方、第一成分/第二成分比が規定範囲の上限値を超える場合(比較例1)では、損失正接の値が低くなることが確認された。すなわち、第一成分の比率が多い場合は、弾性体としての性状が強くなることが示された。一方、第一成分/第二成分比が規定範囲の下限値を下まわる場合(比較例2)では、損失正接の値が大きくなることが確認された。すなわち、第一成分の比率が小さい場合は、粘性体としての性状が強くなることが確認された。 On the other hand, it was confirmed that when the first component/second component ratio exceeded the upper limit of the specified range (Comparative Example 1), the value of the loss tangent decreased. That is, it was shown that when the ratio of the first component is large, the property as an elastic body is enhanced. On the other hand, it was confirmed that when the ratio of the first component to the second component was below the lower limit of the specified range (Comparative Example 2), the value of the loss tangent increased. That is, it was confirmed that when the ratio of the first component is small, the property as a viscous body becomes strong.
3-2.圧縮速度試験
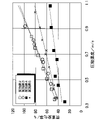
圧縮速度試験用のために、形成されたシール材から長さ100mmの試料をそれぞれ切り出した。その後、ロードセルに荷重治具を固定した後、0.3~1.0m/sの速度で、当該試料を設定基準位置まで圧縮した場合の荷重値を計測し、更に静荷重値(試験速度:20mm/min)からの荷重変化率[%]を算出した。その後、算出された荷重変化率[%]に基づき、横軸に圧縮速度[m/s]、縦軸に荷重変化率[%]をプロットしたグラフを作成した(図2)。
3-2. Compression Speed Test For the compression speed test, a 100 mm long sample was cut from the formed sealing material. After that, after fixing the load jig to the load cell, the load value is measured when the sample is compressed to the set reference position at a speed of 0.3 to 1.0 m / s, and the static load value (test speed: 20 mm/min) was calculated. After that, based on the calculated load change rate [%], a graph was created by plotting the compression speed [m/s] on the horizontal axis and the load change rate [%] on the vertical axis (Fig. 2).
これにより、圧縮速度及び荷重変化率の相関関係を示す近似式を算出し、求められた近似式の傾き[%/(m/s)]によって速度依存性の評価を行った。なお、プロットされたグラフから近似式を求める手法は周知のものを使用可能である。例えば、補間多項式、最小二乗法、テーラー級数、パデ近似、及び連分数展開などの方法がある。これらの方法を任意に選択して求めることができる。図2は、図示の簡略化のため、実施例1~7及び比較例1,2の中の一部の実施例及び比較例についてプロットしたグラフを示している。 An approximation formula showing the correlation between the compression speed and the load change rate was calculated from this, and the velocity dependence was evaluated by the gradient [%/(m/s)] of the obtained approximation formula. A well-known method can be used for obtaining an approximate expression from the plotted graph. For example, there are methods such as interpolating polynomials, least squares, Taylor series, Padé approximation, and continued fraction expansion. Any of these methods can be selected for determination. FIG. 2 shows a graph plotted for some examples and comparative examples among Examples 1 to 7 and Comparative Examples 1 and 2 for simplification of illustration.
本実施例において、グラフより求められた近似式の傾きが、40以下のものを“A(=優)”、41~70の範囲のものを“B(=良)”、71~100の範囲のものを“C(=可)”、及び、100以上のものを“D(=不可)”として圧縮速度試験の評価を行った。得られた速度依存性(≒近似式の傾き)の値及びその評価結果を上記表3に示す。 In this embodiment, the slope of the approximate expression obtained from the graph is "A (=excellent)" when it is 40 or less, "B (=good)" when it is in the range of 41 to 70, and in the range of 71 to 100. Those with a value of 100 or more were evaluated as "C (=acceptable)", and those with a value of 100 or more were evaluated as "D (=impossible)" in the compression speed test. Table 3 shows the obtained speed dependency (≈the slope of the approximation formula) and the evaluation results thereof.
これによると、第一成分/第二成分比の値が1.25であり、かつ損失正接の値が0.097と実施例中で最も低い値を示す実施例4が良好な速度依存性を示すことが確認された。更に、損失正接の値が高くなるに連れて、速度依存性の評価が低くなる傾向が示された。なお、比較例1は速度依存性に関しては良好な評価を得るものの、後述する加工性の評価が低くなっている。すなわち、速度依存性のみを良好なものとしてもシール材全体としては低い評価になる。 According to this, Example 4, which has a first component/second component ratio value of 1.25 and a loss tangent value of 0.097, which is the lowest among the examples, exhibits good speed dependence. It was confirmed that Furthermore, it was shown that the higher the value of the loss tangent, the lower the evaluation of the speed dependence. Although Comparative Example 1 obtained a favorable evaluation with respect to the speed dependence, the evaluation of workability, which will be described later, was low. In other words, even if only the speed dependence is considered to be good, the evaluation of the sealing material as a whole is low.
3-3.加工性(ムーニー粘度)
更に、シール材の加工性の評価のために、ムーニー粘度ML(1+4)125℃の値を測定した。ムーニー粘度の測定は、JIS K6300-1:2001(第1部:ムーニー粘度計による粘度及びスコーチタイムの求め方)に準拠して行った。具体的には、ムーニー粘度計(M&K製)を用い、125℃の温度でL形ローターを用いて1分間予熱した後、当該L形ローターを4分間回転させた際のムーニー粘度ML(1+4)125℃を測定した。なお、既に説明した第一成分のムーニー粘度の値も、上記と同様の条件により行っている(表1参照)。
3-3. Workability (Mooney viscosity)
Furthermore, the Mooney viscosity ML(1+4) at 125° C. was measured to evaluate the workability of the sealing material. Mooney viscosity was measured in accordance with JIS K6300-1:2001 (Part 1: Method for determining viscosity and scorch time by Mooney viscometer). Specifically, using a Mooney viscometer (manufactured by M&K), after preheating for 1 minute using an L-shaped rotor at a temperature of 125 ° C., Mooney viscosity ML (1 + 4) when rotating the L-shaped rotor for 4 minutes 125°C was measured. The values of Mooney viscosity of the first component already explained are also determined under the same conditions as above (see Table 1).
シール部材の加工性の評価は、上記ムーニー粘度ML(1+4)125℃の値が、40~55の範囲のものを“B(=良)”、25~39の範囲、または、56~70の範囲のもの“C(=可)”、及び、24以下若しくは71以上のものを“D(=不可)”として評価した。得られたムーニー粘度の値及び評価結果を上記表3に示す。 The evaluation of the workability of the seal member is as follows: "B (= good)" when the value of the Mooney viscosity ML (1 + 4) 125 ° C. is in the range of 40 to 55, 25 to 39, or 56 to 70. Those within the range were evaluated as "C (=acceptable)", and those of 24 or less or 71 or more were evaluated as "D (=impossible)". The obtained Mooney viscosity values and evaluation results are shown in Table 3 above.
これによると、ムーニー粘度が40~55の範囲に該当する実施例4が最も加工性が良好となることが示された。しかしながら、第一成分/第二成分比、損失正接、及び速度依然性との明確な相関関係は現時点では確認されなかった。 According to this, it was shown that Example 4, whose Mooney viscosity falls within the range of 40 to 55, has the best workability. However, a clear correlation with the first component/second component ratio, loss tangent, and speed dependence was not confirmed at this time.
3-4.実車試験評価
次に、最も評価の高かった実施例4のシール材を実際の車両に装着し、実車に使用されている既存のシール材との間で、ドア閉まり性がどの程度改良されているかの確認を行った。ここで、実車試験は、車両のフロント運転席側のドアの周縁に長尺状のシール材を所定の固定手段で装着し、更に、車両の全てのドア及び窓を閉じた状態で行った。すなわち、試験のためにドア閉め操作を行うドア以外から空気が流出入することを抑制し、最もドア閉まり性が悪くなる条件で実車試験を行った。
3-4. Actual vehicle test evaluation Next, the sealing material of Example 4, which received the highest evaluation, was installed in an actual vehicle, and how much the door closing performance was improved compared to the existing sealing material used in the actual vehicle. was confirmed. Here, the actual vehicle test was conducted with a long sealing material attached to the periphery of the door on the front driver's seat side of the vehicle by a predetermined fixing means, and with all the doors and windows of the vehicle closed. That is, for the purpose of the test, an actual vehicle test was conducted under the conditions in which the inflow and outflow of air from the door other than the door for the door closing operation were suppressed, and the door closing performance was the worst.
ここで、ドア閉まり速度[m/s]は、ドアの把持部の下方に反射板を装着し、ドアを閉める操作の際に当該反射板にレーザーを照射することにより測定した。すなわち、ドアを閉める操作によって、当該ドア(反射板)がレーザー速度計を通過する際の速度を計測し、ドアが完全に閉まった状態になる、換言すれば、「半ドア」にならない最小の速度を本実施例におけるドア閉まり速度とした。実車試験評価の結果を下記表4に示す。 Here, the door closing speed [m/s] was measured by attaching a reflector below the handle of the door and irradiating the reflector with a laser when closing the door. In other words, by closing the door, the speed of the door (reflector) is measured when it passes through the laser speedometer, and the door is completely closed. The speed was taken as the door closing speed in this embodiment. The results of the actual vehicle test evaluation are shown in Table 4 below.

これによると、既存のシール材によって測定されたドア閉まり速度が0.95[m/s]であるのに対し、本発明のシール材は、ドア閉まり速度が0.93[m/s]となった。すなわち、既存のシール材よりもゆっくりした速度でドアを確実に閉めることができる。更に、ドア一枚当たりのエネルギーも-4.2[%]抑えることが示された。その結果、腕の力の弱い高齢者や子供等であってもドアを確実に閉めることができる。すなわち、本発明のシール材は、ドア閉まり性において有効であることが示された。 According to this, the door closing speed measured by the existing sealing material is 0.95 [m/s], whereas the sealing material of the present invention has a door closing speed of 0.93 [m/s]. became. That is, the door can be reliably closed at a slower speed than the existing sealing material. Furthermore, it was shown that the energy per door was reduced by -4.2 [%]. As a result, even elderly people and children with weak arm strength can securely close the door. That is, it was shown that the sealing material of the present invention is effective in closing the door.
本発明のシール材(車両用ドアシール材)は、乗用車や産業用或いは農業等の各種車両のドアまたは車体開口部等に取設可能であり、その他の種々の産業技術分野において利用可能性が期待される。 The sealing material (vehicle door sealing material) of the present invention can be attached to doors or vehicle body openings of various vehicles such as passenger cars, industrial vehicles, and agricultural vehicles, and is expected to be used in various other industrial technology fields. be done.
1:シール材(車両用ドアシール材)、2:シール基部、3:シール部、4:シール部外表面。 1: seal material (vehicle door seal material), 2: seal base, 3: seal portion, 4: outer surface of seal portion.
Claims (5)
前記第一成分の配合部数を前記第二成分の配合部数で除した値が、0.83~1.25の範囲であり、
ムーニー粘度が、25~61ML(1+4)125℃であり、
前記カーボンブラックのヨウ素吸着量が20~40mg/g、かつ、DBP吸油量が50~112cm 3 /100gの範囲である車両用ドアシール材。 A vehicle door seal material comprising a first component containing ethylene/propylene/diene rubber and a second component containing carbon black as raw materials,
The value obtained by dividing the number of parts of the first component by the number of parts of the second component is 0. in the range of 83 to 1.25 ,
Mooney viscosity is 25 to 61 ML (1 + 4) 125 ° C.,
The vehicle door seal material , wherein the carbon black has an iodine adsorption amount of 20 to 40 mg/g and a DBP oil absorption amount of 50 to 112 cm 3 /100 g .
0.095~0.210の範囲である請求項1に記載の車両用ドアシール材。 The value of loss tangent, which indicates dynamic viscoelasticity, is
The vehicle door seal material according to claim 1, which is in the range of 0.095 to 0.210.
29~80ML(1+4)125℃の範囲である請求項1~3のいずれか一項に記載の車両用ドアシール材。 The Mooney viscosity of the first component is
The vehicle door seal material according to any one of claims 1 to 3, which has a temperature range of 2 9 to 80 ML(1+4) 125°C.
軟化剤、加工助剤、充填剤、架橋剤、加硫促進剤、及び発泡剤の少なくともいずれか一種を更に原材料として含む請求項1~4のいずれか一項に記載の車両用ドアシール材。 In addition to the first component and the second component,
The vehicle door seal material according to any one of claims 1 to 4 , further comprising at least one of a softening agent, a processing aid, a filler, a cross-linking agent, a vulcanization accelerator, and a foaming agent as a raw material.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2018214951A JP7204184B2 (en) | 2018-11-15 | 2018-11-15 | Vehicle door seal material |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2018214951A JP7204184B2 (en) | 2018-11-15 | 2018-11-15 | Vehicle door seal material |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2020082763A JP2020082763A (en) | 2020-06-04 |
| JP7204184B2 true JP7204184B2 (en) | 2023-01-16 |
Family
ID=70909550
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2018214951A Active JP7204184B2 (en) | 2018-11-15 | 2018-11-15 | Vehicle door seal material |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP7204184B2 (en) |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002205606A (en) | 2001-01-10 | 2002-07-23 | Nishikawa Rubber Co Ltd | Automotive weather strip |
| JP2003237497A (en) | 2002-02-12 | 2003-08-27 | Toyo Tire & Rubber Co Ltd | Weather strip |
| JP2003237377A (en) | 2002-02-20 | 2003-08-27 | Toyo Tire & Rubber Co Ltd | Weather strip |
| JP2006282887A (en) | 2005-03-31 | 2006-10-19 | Toyoda Gosei Co Ltd | Sealing part for hydraulic cylinder |
| JP2007015321A (en) | 2005-07-11 | 2007-01-25 | Toyo Tire & Rubber Co Ltd | Weatherstrip manufacturing method |
| JP2014111731A (en) | 2012-11-06 | 2014-06-19 | Nishikawa Rubber Co Ltd | Foam rubber material for weather strip |
-
2018
- 2018-11-15 JP JP2018214951A patent/JP7204184B2/en active Active
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002205606A (en) | 2001-01-10 | 2002-07-23 | Nishikawa Rubber Co Ltd | Automotive weather strip |
| JP2003237497A (en) | 2002-02-12 | 2003-08-27 | Toyo Tire & Rubber Co Ltd | Weather strip |
| JP2003237377A (en) | 2002-02-20 | 2003-08-27 | Toyo Tire & Rubber Co Ltd | Weather strip |
| JP2006282887A (en) | 2005-03-31 | 2006-10-19 | Toyoda Gosei Co Ltd | Sealing part for hydraulic cylinder |
| JP2007015321A (en) | 2005-07-11 | 2007-01-25 | Toyo Tire & Rubber Co Ltd | Weatherstrip manufacturing method |
| JP2014111731A (en) | 2012-11-06 | 2014-06-19 | Nishikawa Rubber Co Ltd | Foam rubber material for weather strip |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2020082763A (en) | 2020-06-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5183613A (en) | Process for the preparation of solventless, low friction, abrasion-resistant coatings for elastomeric substrates | |
| US8353130B2 (en) | Door weather strip | |
| EP3246356B1 (en) | Epdm based rubber composition for sponge section in weather strip of passenger car | |
| JPH10324200A (en) | Automotive weather strip | |
| JP2014111731A (en) | Foam rubber material for weather strip | |
| Lee et al. | Multidisciplinary design of door inner belt weatherstrip for simultaneous reduction of wind noise and squeaking in electric vehicles | |
| JP2020082763A (en) | Door seal material for vehicle | |
| KR101491166B1 (en) | Weather strip composition | |
| Lee et al. | Multidisciplinary tailgate guide bumper design for electric vehicles: Overcoming rattle, separation noise and closure effort trade-offs | |
| JP2000191863A (en) | Wind-sealed molded article and method for producing the same | |
| KR101776413B1 (en) | Nano zinc oxide filled weather strip rubber composition and weather strip for car using the same | |
| JP3754940B2 (en) | Rubber composition | |
| US11680126B2 (en) | Thermoplastic elastomer composition and thermoplastic elastomer manufactured by using the same | |
| CN108698496B (en) | Profiled strip for a motor vehicle and method for producing a profiled strip | |
| JP7716378B2 (en) | Extrusions, weather strips | |
| KR102721742B1 (en) | Epdm rubber compounds with surface embossing efect of glass run corner molding using uhmwpp and glass run for vehicle by using the same | |
| KR20260032699A (en) | Rubber composition of automobile parts, manufacturing method of the same, automobile parts produced by using the same | |
| KR101567166B1 (en) | A Rubber Composition with Improved Durability | |
| KR20030091391A (en) | Weatherstrip for automobile | |
| US20230278406A1 (en) | Bonding sheet material for weather strip, weather strip, and method for producing same | |
| KR20250079958A (en) | Rubber Composition for Sealing Appratus and Weather-strip For Vehicle using the same | |
| JP2024093686A (en) | Rubber composition and hose | |
| KR20100007540A (en) | Rubber composition for weather strip joint of automobile | |
| JP2005114141A (en) | Anti-vibration rubber | |
| US20190176764A1 (en) | Rubber wiper blade element with friction reducing agent that continuously migrates to the surface |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20210729 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20220720 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20220726 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20220901 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20221220 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20221221 |
|
| R150 | Certificate of patent or registration of utility model |
Ref document number: 7204184 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |