KR20140103370A - 공작기계 주축 회전정밀도 측정장치 - Google Patents
공작기계 주축 회전정밀도 측정장치 Download PDFInfo
- Publication number
- KR20140103370A KR20140103370A KR1020130016240A KR20130016240A KR20140103370A KR 20140103370 A KR20140103370 A KR 20140103370A KR 1020130016240 A KR1020130016240 A KR 1020130016240A KR 20130016240 A KR20130016240 A KR 20130016240A KR 20140103370 A KR20140103370 A KR 20140103370A
- Authority
- KR
- South Korea
- Prior art keywords
- measuring
- machine tool
- axis
- master ball
- spindle
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
- 238000006073 displacement reaction Methods 0.000 claims abstract description 12
- 238000004891 communication Methods 0.000 claims abstract description 4
- 238000000034 method Methods 0.000 claims description 5
- 238000005259 measurement Methods 0.000 description 5
- 239000000523 sample Substances 0.000 description 5
- 230000000694 effects Effects 0.000 description 3
- 230000015572 biosynthetic process Effects 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 230000000295 complement effect Effects 0.000 description 1
- 238000007796 conventional method Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000011156 evaluation Methods 0.000 description 1
- 230000001788 irregular Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 230000002093 peripheral effect Effects 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 230000004044 response Effects 0.000 description 1
- 230000003068 static effect Effects 0.000 description 1
- 230000003746 surface roughness Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q17/00—Arrangements for observing, indicating or measuring on machine tools
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q5/00—Driving or feeding mechanisms; Control arrangements therefor
- B23Q5/02—Driving main working members
- B23Q5/04—Driving main working members rotary shafts, e.g. working-spindles
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B11/00—Measuring arrangements characterised by the use of optical techniques
- G01B11/14—Measuring arrangements characterised by the use of optical techniques for measuring distance or clearance between spaced objects or spaced apertures
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01L—MEASURING FORCE, STRESS, TORQUE, WORK, MECHANICAL POWER, MECHANICAL EFFICIENCY, OR FLUID PRESSURE
- G01L9/00—Measuring steady of quasi-steady pressure of fluid or fluent solid material by electric or magnetic pressure-sensitive elements; Transmitting or indicating the displacement of mechanical pressure-sensitive elements, used to measure the steady or quasi-steady pressure of a fluid or fluent solid material, by electric or magnetic means
- G01L9/12—Measuring steady of quasi-steady pressure of fluid or fluent solid material by electric or magnetic pressure-sensitive elements; Transmitting or indicating the displacement of mechanical pressure-sensitive elements, used to measure the steady or quasi-steady pressure of a fluid or fluent solid material, by electric or magnetic means by making use of variations in capacitance, i.e. electric circuits therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23Q—DETAILS, COMPONENTS, OR ACCESSORIES FOR MACHINE TOOLS, e.g. ARRANGEMENTS FOR COPYING OR CONTROLLING; MACHINE TOOLS IN GENERAL CHARACTERISED BY THE CONSTRUCTION OF PARTICULAR DETAILS OR COMPONENTS; COMBINATIONS OR ASSOCIATIONS OF METAL-WORKING MACHINES, NOT DIRECTED TO A PARTICULAR RESULT
- B23Q2717/00—Arrangements for indicating or measuring
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Measurement Of Length, Angles, Or The Like Using Electric Or Magnetic Means (AREA)
Abstract
Description
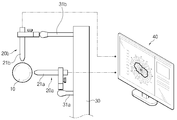
도 2는 본 발명에 따른 공작기계 주축 회전정밀도 측정장치의 실시예를 보인 예시도이다.
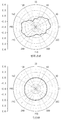
도 3은 본 발명의 실시예에 따라 측정된 주축의 반경방향값과 축방향값의 예시를 보인 그래프이다.
20a,20b: 측정수단
21a: 레이저센서
21b: 정전용량형 근접센서
30: 지그본체
40: 연산출력부
Claims (2)
- 공작기계의 주축 척에 장착되어, 상기 주축이 회전함에 따라 회전되어 측정 대상물이 되는 구형의 마스터볼;
상기 마스터볼 주변의 X축 또는 Y축 선상에 배치되어, 고속 회전하는 상기 마스터볼의 변위를 측정하는 제1,제2측정수단;
상기 공작기계에 설치되고, 상기 제1,제2측정수단이 각각 장착되는 제1,제2부재가 구비되는 지그본체;
상기 제1,제2측정수단과 통신선으로 각각 연결되고, 상기 제1,제2측정수단에서 측정된 값을 토대로 주축의 회전 정밀도를 그래프 또는 임계수치로 출력하는 연산출력부를 포함하는 공작기계 주축 회전정밀도 측정장치.
- 청구항 1에 있어서,
상기 제1,제2측정수단은
상기 지그본체와 연결된 제1부재에 장착되어 상기 마스터볼 주변의 X축 또는 Y축 중 어느 한 축 선상에 배치되고, 조사되는 레이저가 상기 마스터볼에 의해 반사되어 돌아오는 시간값을 측정하여, 측정된 시간값을 실시간으로 출력하는 레이저센서;
상기 지그본체와 연결된 제2부재에 장착되어 상기 마스터볼() 주변의 X축 또는 Y축 중 어느 한 축 선상에 배치되고, 상기 마스터볼과의 거리에 따라 정전용량 값을 측정하며, 측정된 정전용량 값을 실시간으로 출력하는 정전용량형 근접센서로 이루어지는 공작기계 주축 회전정밀도 측정장치.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020130016240A KR20140103370A (ko) | 2013-02-15 | 2013-02-15 | 공작기계 주축 회전정밀도 측정장치 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020130016240A KR20140103370A (ko) | 2013-02-15 | 2013-02-15 | 공작기계 주축 회전정밀도 측정장치 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| KR20140103370A true KR20140103370A (ko) | 2014-08-27 |
Family
ID=51747647
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| KR1020130016240A Ceased KR20140103370A (ko) | 2013-02-15 | 2013-02-15 | 공작기계 주축 회전정밀도 측정장치 |
Country Status (1)
| Country | Link |
|---|---|
| KR (1) | KR20140103370A (ko) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108955534A (zh) * | 2018-05-15 | 2018-12-07 | 天津工业大学 | 一种纱管智能检测与评价方法 |
| CN112355712A (zh) * | 2020-11-23 | 2021-02-12 | 苏州千机智能技术有限公司 | 一种触发式在机测量的精度校准方法及系统 |
| CN116026576A (zh) * | 2023-03-24 | 2023-04-28 | 山东普鲁特机床有限公司 | 一种高精度车铣复合加工中心性能试验台 |
-
2013
- 2013-02-15 KR KR1020130016240A patent/KR20140103370A/ko not_active Ceased
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108955534A (zh) * | 2018-05-15 | 2018-12-07 | 天津工业大学 | 一种纱管智能检测与评价方法 |
| CN108955534B (zh) * | 2018-05-15 | 2020-02-07 | 天津工业大学 | 一种纱管智能检测与评价方法 |
| CN112355712A (zh) * | 2020-11-23 | 2021-02-12 | 苏州千机智能技术有限公司 | 一种触发式在机测量的精度校准方法及系统 |
| CN112355712B (zh) * | 2020-11-23 | 2022-05-03 | 苏州千机智能技术有限公司 | 一种触发式在机测量的精度校准方法及系统 |
| CN116026576A (zh) * | 2023-03-24 | 2023-04-28 | 山东普鲁特机床有限公司 | 一种高精度车铣复合加工中心性能试验台 |
| CN116026576B (zh) * | 2023-03-24 | 2023-06-20 | 山东普鲁特机床有限公司 | 一种高精度车铣复合加工中心性能试验台 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| Castro | A method for evaluating spindle rotation errors of machine tools using a laser interferometer | |
| CN112526924B (zh) | 一种五轴双摇篮结构机床用3d测头的标定方法 | |
| US10591268B2 (en) | Feeler for workpieces being machined | |
| CN104972395A (zh) | 具备加工变质层检测传感器的机床 | |
| JP5069287B2 (ja) | 誤差補正の方法 | |
| CN108020409A (zh) | 一种主轴回转误差的四点动态测量与分离方法 | |
| CN106643576B (zh) | 一种不同心度测量方法及不同心度测量装置 | |
| CN108759694A (zh) | 一种快速大冗余度的轴承尺寸检测系统 | |
| Bohan et al. | Study on pre-travel behaviour of touch trigger probe under actual measuring conditions | |
| CN103363861B (zh) | 一种测量精密小型主轴内锥跳动的检具 | |
| CN103868441A (zh) | 一种用于检测工件平面度的检具 | |
| CN1225345C (zh) | 一种对被加工表面同时进行加工和测量参数的方法 | |
| CN109253710B (zh) | 一种revo测头a轴零位误差标定方法 | |
| KR101501409B1 (ko) | 공작기계의 가공상태 모니터링 장치 | |
| CN101871759A (zh) | 三坐标测量机 | |
| JP2000205854A (ja) | 機械部品の寸法計測方法 | |
| Masashi et al. | Evaluation of linear axis motion error of machine tools using an R-test device | |
| US20160349039A1 (en) | Runout Calibrator for Hydrodynamic Bearing Testing | |
| KR101409199B1 (ko) | 공작기계 주축 회전정밀도 측정장치 | |
| CN204757949U (zh) | 成套回转装备主轴动态回转误差的测量装置 | |
| JPH0810134B2 (ja) | 平面基板と3センサによる回転中心位置の自動検出法及び検出装置 | |
| CN203509927U (zh) | 一种超精密抛光机床坐标原点标定块 | |
| CN102699766A (zh) | 一种数控加工中测量刀具安装端面与回转中心距离的方法 | |
| CN205254688U (zh) | 精密机床主轴回转精度检测装置 | |
| CN116428963A (zh) | 圆度仪用气浮转台装置及其标定方法和测量方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A201 | Request for examination | ||
| PA0109 | Patent application |
Patent event code: PA01091R01D Comment text: Patent Application Patent event date: 20130215 |
|
| PA0201 | Request for examination | ||
| E902 | Notification of reason for refusal | ||
| PE0902 | Notice of grounds for rejection |
Comment text: Notification of reason for refusal Patent event date: 20140403 Patent event code: PE09021S01D |
|
| PG1501 | Laying open of application | ||
| E601 | Decision to refuse application | ||
| PE0601 | Decision on rejection of patent |
Patent event date: 20140912 Comment text: Decision to Refuse Application Patent event code: PE06012S01D Patent event date: 20140403 Comment text: Notification of reason for refusal Patent event code: PE06011S01I |