KR840000006B1 - A manufacturing process of embossing sheet - Google Patents
A manufacturing process of embossing sheet Download PDFInfo
- Publication number
- KR840000006B1 KR840000006B1 KR1019800003072A KR800003072A KR840000006B1 KR 840000006 B1 KR840000006 B1 KR 840000006B1 KR 1019800003072 A KR1019800003072 A KR 1019800003072A KR 800003072 A KR800003072 A KR 800003072A KR 840000006 B1 KR840000006 B1 KR 840000006B1
- Authority
- KR
- South Korea
- Prior art keywords
- sheet
- cosmetic
- heat
- adhesive film
- cosmetic sheet
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
Images

Landscapes
- Laminated Bodies (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
- Adhesive Tapes (AREA)
Abstract
내용 없음.No content.
Description
도면은 본 발명 화장체의 일예와, 이것을 제조하는 본 발명 방법의 일실시 태양과를 설명하기 위한 것으로서,The drawings are for explaining one example of the present invention and one embodiment of the method of the present invention for producing the same,
제1도는 화장체의 일부 확대 단면도.1 is a partially enlarged cross-sectional view of a cosmetic body.
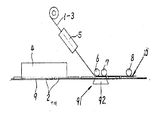
제2도는 화장체 제조방법의 개략 설명도.2 is a schematic explanatory diagram of a method for manufacturing a cosmetic body.
본 발명은 사전에 그 자체에 나무 "결"의 무늬모양, 기타 요철무늬를 부착하기 위한 요철소성가공(압인가공, 엠보싱(Embossing)가공, 기타의 유사한가공)을 실시함에는 적당하지 않은 화장용 시이트 즉, 너무 얇아서 파손되기 쉽기 때문에 요철소성 가공을 실시하는 것이 불가능하거나 곤란한 화장용 시이트, 혹은 요철가공을 실시할수 있다 하더라도 연약하기 때문에 다른 재료 표면에 압압 접착하려고 할때에는 요철이 손상되기 쉬운 화장용 시이트를 기재에 접착하여 이루어진 화장체 등으로서, 그 화장체에 있어서 화장용 시이트가 요철모양 무늬를 보유하는 화장체의 제조방법에 관한 것이다.The present invention is a cosmetic that is not suitable for carrying out uneven plastic processing (pushing, embossing, other similar processing) for attaching a pattern of wood "grain", other irregularities on its own in advance. Sheet, that is, too thin to be easily broken, so that it is impossible to carry out uneven plastic processing, or even if it is difficult to carry out uneven processing or uneven processing, it is fragile. The cosmetic body etc. which adhere | attached the sheet | seat to the base material, It is related with the manufacturing method of the cosmetic body in which the cosmetic sheet has a concave-convex pattern in the cosmetic body.
종래에는 박엽지, 얇은 장식용 종이 등에 나무결 무늬와 같은 모양을 실시한 것, 혹은 이러한 모양을 실시하지 않은 얇은 화장용 시이트를 기재(예컨데 목판)에 접착하여 이루어진 화장체가 있었다.Conventionally, there existed the thing which gave the shape like a wood grain pattern on thin paper, thin decorative paper, etc., or the thin cosmetic sheet which did not give such a shape to the base material (for example, wooden board).
이러한 종래의 화장체는 화장용 시이트에 요철이 부착되어 있지 않기때문에 이것이 접착되는 기재표면이 평탄에 가까울 때에는 접착된 화장용 시이트 표면도 평탄하게되어 단조로우며, 시각이나 촉각 등에 의한 품질 평가가 나쁜 화장체 밖에는 얻을 수가 없었다.Since such a conventional cosmetic body does not have irregularities attached to the cosmetic sheet, when the surface of the substrate to which it is bonded is flat, the surface of the cosmetic sheet adhered to the surface is flat and monotonous, and the quality evaluation due to visual or touch is poor. I could only get the makeup.
이 문제를 해결하기 위하여 이러한 화장용 시이트에 사전 나무결의 무늬 모양등의 요철을 부착하려고해도 그 시이트가 얇아서 파손되기 쉽기 때문에 요철가공이 곤란하며, 또 가령 이러한 화장용 시이트에 사전에 나무결무늬 등의 요철무늬를 부착할수 있었다 하더라도 그 요철무늬는 시이트의 기재에 접착을 할때 눌러서 퍼지기가 쉬우며, 또한 시이트의 요부의 이면이 기재표면에서 위로 뜨는 경향이 있어 접착이 불충분하게 되는것은 명백한 사실이다.In order to solve this problem, even if an unevenness such as a pre-wood pattern is attached to such a cosmetic sheet, it is difficult to process unevenness because the sheet is thin and easily broken. Even if the uneven pattern could be attached, the uneven pattern is easy to press and spread when adhering to the substrate of the sheet, and it is obvious that the backside of the sheet of the sheet tends to float upward from the surface of the substrate, resulting in insufficient adhesion.
본 발명의 목적은 사전에 그 자체에 요철가공을 실시하여서 사용함에는 적당하지 않은 화장용 시이트가 기재에 접착되며, 그 화장용 시이트가 손상되는일 없이 요철모양의 무늬를 보유하고 있으며, 또한 기재에 확실하게 접착되어 있는 화장체의 간편한 제조방법을 제공하는 것이다.An object of the present invention is to adhere to the base material cosmetic sheet which is not suitable for use by applying uneven processing on its own in advance, and retains the uneven pattern without damaging the cosmetic sheet. It is to provide a simple method of manufacturing a cosmetic body that is securely bonded.
본 발명의 이러한 목적은 사전에 그 자체에 요철소성가공을 실시함에는 적당하지 않은 화장용 시이트를 열 접착성막을 (개재하여 기재)위에 재치하고, 전기한 열 접착성막을 열 접착가능한 온도로 가열하면서 전기한 기재에 압압하여서 전기한 화장용 시이트 및 열 접착성 막에 소정의 요철을 형성하고, 그후 전기한 열 접착성막을 냉각하여 전기한 화장용 시이트에 요철을 유지시킴과 아울러, 그 화장용 시이트를 전기한 기재에 접착하는 것을 특징으로하는 화장체의 제조방법에 의하여 달성되는 것이다.It is an object of the present invention to place a cosmetic sheet, which is not suitable for performing uneven plastic processing on its own, on a thermally adhesive film (substrated thereon), and heat the above-mentioned thermally adhesive film to a temperature at which it can be heat-bonded. While forming the predetermined irregularities in the cosmetic sheet and the heat-adhesive film which is pressed by the substrate described above, and then cools the heat-adhesive film, and maintains the irregularities in the cosmetic sheet, It is achieved by the manufacturing method of the cosmetic body characterized by adhering a sheet | seat to the base material mentioned above.
상기한 기재 및 화장용 시이트의 재질은 그 시이트를 열접착성막을 개재하여 기체에 접착함에 필요한 상기한 압압력 및 가열온도에 견딜수 있는 것이라면 족한 것이다.The material of the base material and the cosmetic sheet is sufficient as long as it can withstand the pressure and heating temperature described above necessary for bonding the sheet to a substrate via a heat-adhesive film.
예컨대 기체로서 목판, 금속판, 석고보오드(Gypsum-board)등을 화장용 시이트로 하여서 예컨데 종이, 특히 박엽지(薄葉紙)를 들수가 있다.For example, a wood board, a metal board, a gypsum board, or the like as a cosmetic sheet may be used as a base, for example, paper, in particular thin paper.
상기한 열 접착성막은 폴리아미드계, 폴리우레탄계, 폴리에스텔계, (에치렌-초산비닐 공중합체)계, 또는 폴리오레핀계의 열 접착성 접착제로부터 얻어진다.The heat adhesive film is obtained from a polyamide-based, polyurethane-based, polyester-based, (ethylene-vinyl acetate copolymer) -based, or polyolefin-based heat adhesive adhesive.
이러한 접착제가 사용되는 경우에는 화장용 시이트의 기재예의 압압력은 시이트와 기재와의 충분한 접착을 얻는것과 아울러, 열 접착성막 및 시이트에 소정의 요철부착을 행하기 위하여 대략 2-10㎏/㎠ 보다 더 바람직하게로는 5-10㎏/㎠가 적절하며, 접착하기전의 상기한 막의 두께는 가열압압할때에 있어서 기재 및 시이트 사이로부터의 접착제 유출방지를 위하여 대략 30-150μ, 보다 더 바람직하게로는 대략 50-100μ이 적당하다.When such an adhesive is used, the pressing force of the base material example of the cosmetic sheet is not less than about 2-10 kg / cm 2 in order to obtain sufficient adhesion between the sheet and the base material and to attach predetermined irregularities to the thermal adhesive film and the sheet. More preferably, 5-10 kg / cm 2 is suitable, and the thickness of the film before adhesion is about 30-150 μm, even more preferably, to prevent adhesive leakage from the substrate and the sheet when hot pressing. About 50-100μ is suitable.
또한 필요에 따라 상기한 이외의 열 접착성 접착제를 사용하는 것도 가능하며, 그 접착제의 종류 및 또는 화장용 시이트의 종류, 두께 등에 따라서 상기한 압압력 및 상기한 열 접착성막의 두께를 각각 상기한 범위 외의 것으로 할수가 있다.It is also possible to use other heat-adhesive adhesives other than those described above, and the pressure and the thickness of the heat-adhesive film described above are described in accordance with the type of the adhesive and / or the type and thickness of the cosmetic sheet. Can be out of range.
상기한 열 접착성막은 전기한 기재 및 전기한 화장용 시이트와는 독립한 시이트의 형태로서 제공되는 것으로서 좋으며, 혹은 사전에 전기한 화장용 시이트의 이면에 열 접착성 접착제를 코오팅하여 얻어진 것으로도 좋으며, 혹은 사전에 전기한 기재의 표면에 열 접착성 접착제를 코오팅하여 얻어진 것이라도 좋다.The thermal adhesive film described above may be provided in the form of a sheet independent of the substrate described above and the cosmetic sheet described above, or may be obtained by coating a thermal adhesive on the back surface of the cosmetic sheet previously described. It may be sufficient, or may be obtained by coating a heat-adhesive adhesive on the surface of the substrate previously described.
전기한 열 접착성막을 열접착가능온도에 원할하게 가열할수 있도록 기재와 화장용 시이트와의 접착하기 전에 기재, 화장용 시이트 및 열접착성막중에서 최소한 하나를 적당하게 예열하여 놓는것이 바람직하다.It is preferable that at least one of the substrate, the cosmetic sheet and the thermal adhesive film is appropriately preheated before adhering the substrate to the cosmetic sheet so that the aforementioned thermal adhesive film can be smoothly heated to a heat-adhesive temperature.
그리고 전기한 열 접착성막의 열접착가능 온도에의 최종적 가열은, 그 막을 개재하여 기재위에 재치된 화장용 시이트의 위에서 가열롤(roll) 또는 가열판을 서로 맞닿게하고 혹은 열풍을 불어되는등 하여서 행하여진다.The final heating of the heat-adhesive film to the heat-adhesive temperature is performed by bringing the heating rolls or the heating plates into contact with each other or blowing hot air on the cosmetic sheet placed on the substrate via the film. Lose.
이때 기재쪽에서도 필요에 따라 적당히 가열하는 것은 지장이 없다. 전기한 압압부재는 예컨대 소정된 요철무늬를 둘레표면에 가지고 있는 프레스롤(press-roll)이나 소정의 요철무늬를 가지고 있는 프레스판으로서 좋다.At this time, it is not a problem to properly heat the substrate side as needed. The press member described above may be, for example, a press roll having a predetermined uneven pattern on the circumferential surface or a press plate having a predetermined uneven pattern.
이 프레스롤, 프레스판이 상기한 가열롤, 가열판을 겸하는 구조의 것이여도 좋다.The press roll and the press plate may have a structure serving as the above-described heating roll and the heating plate.
전기한 압압부재에 의한 압압처리가 끝난뒤의 전기한 열 접착성막의 냉각은 냉풍을 불어대는것, 냉각롤 또는 냉각판의 서로 맞닿게하는것 등에 의하여 적당히 행하여진다.Cooling of the heat-adhesive film mentioned above after the press process by the said press member is performed suitably by blowing a cold air, making a cooling roll or a cold plate contact with each other, and the like.
이하 본 발명 화장체의 일예와, 이것을 제조하는 본 발명 방법의 일 실시 태양과를 도면에 따라서 설명한다.EMBODIMENT OF THE INVENTION Hereinafter, one example of the cosmetics body of this invention, and one Embodiment of the method of this invention which manufactures this are demonstrated according to drawing.
제1도에 있어서, 화장체(10)는 화장용 시이트(1), 기재(2) 및 열접착성막(3)을 갖추고 있다.In FIG. 1, the cosmetic body 10 is equipped with the cosmetic sheet 1, the base material 2, and the heat-adhesive film 3. As shown in FIG.
시이트(1)는 표면(11)에 나무결무늬 인쇄를 행한 박엽지(30-50g/㎡) 시이트이다.The sheet 1 is a thin paper (30-50 g / m 2) sheet on which the surface 11 is printed with wood grain pattern.
기재(2)는 베니어판이며, 열접착성막(3)은 폴리오레핀계 접착제로부터 이루어져서 시이트(1)를 기재(2)에 접착하고 있으며, 시이트(1)와의 접착면(31)은 나무결도관(導管) 모양의 요철을 가지고 있고, 시이트(1)는 그 요철에 따라서 요철무늬를 가지고 있다.The base material 2 is a veneer board, and the heat-adhesive film 3 consists of a polyolefin pin adhesive, and the sheet | seat 1 is adhere | attached to the base material 2, and the
이 화장체(10)는 다음과 같이하여 얻어진다.This cosmetic body 10 is obtained as follows.
소정된 칫수로 제단된 베니어판(2)을 콘베이어라인(9)으로서 가공 작업대(91)로 이송하고 그 도중에 예열장치(4)로서 최소한 판(2)의 표면부(21)를 예열하여 놓는다.The veneer plate 2 cut by the predetermined dimension is conveyed to the processing bench 91 as the conveyor line 9, and in the meantime, at least the surface portion 21 of the plate 2 is preheated as the preheater 4.
다른 한편 사전에 열 접착성막(3)을 화장지 시이트(1)의 이면(12)에 두께 약80로서 형성하여서 이루어진 시이트(1-3)를 그 막(3)이 판(2)에 당접하도록 작업대(91)로 이송하고 그 도중에서 예열장치(5)로서 예열하여 놓는다.On the other hand, the worktable is formed so that the film 3 abuts the plate 2 by forming the heat adhesive film 3 in advance on the back surface 12 of the toilet paper sheet 1 with a thickness of about 80. It transfers to 91, and preheats it as the preheater 5 in the middle.
작업대(91)에 도달한 시이트(1-3)의 기재(2)를, 시이트(1-3) 위의 가열롤(6)과 기재(2) 아래의 수납대(92)와의 사이에 협착하여 열 접착성막(3)을 그 융점내지 융점부근의 온도까지 최종 가열한다.The base material 2 of the sheet 1-3 reaching the work table 91 is squeezed between the heating roll 6 on the sheet 1-3 and the storage stand 92 under the base material 2. The thermal adhesive film 3 is finally heated to a temperature near its melting point to its melting point.
그후 즉시 소정의 요철무늬를 보유하는 프레스롤(7)로서 5-6㎏/㎠의 압력하에서 시이트(1-3)를 기재(2)에 압압한다.Thereafter, the sheet 1-3 is pressed against the substrate 2 under a pressure of 5-6 kg / cm 2 as a
그러면 막(3)에 의하여 화장용 시이트(1)가 기재(2)에 접착됨과 아울러 막(3)은 시이트(1)를 개재하여 요철부착되며 따라서 시이트(1)에도 동일한 요철무늬가 형성된다.Then, the cosmetic sheet 1 is adhered to the substrate 2 by the membrane 3, and the membrane 3 is unevenly attached via the sheet 1, so that the same uneven pattern is formed on the sheet 1.
그후 막(3)은 시이트(1)을 개재하여 그 요철무늬를 손상하지 않도록 냉각 롤(roll)로서 냉각되어서 그 결과 요철무늬가 그 상태로 확보된 화장체(10)가 얻어진다.Thereafter, the film 3 is cooled by a cooling roll through the sheet 1 so as not to damage the uneven pattern, and as a result, the cosmetic body 10 in which the uneven pattern is secured is obtained.
그뿐 아니라 이 화장체는 그 화장용 시이트(1)가 요철을 보유함에도 불구하고 전체가 확고하게 기재(2)에 접착되어진다.In addition, this cosmetic body is firmly adhered to the substrate 2 even though the cosmetic sheet 1 retains irregularities.
이와같이 본 발명에 의하면, 사전에 그 자체에 요철가공을 실시하여 사용함에는 적당하지 않는 화장용 시이트가 기재에 접착되며, 그 화장용 시이트가 하등에 손상되는 일없이 요철무늬 모양을 보유하고, 또한 기재에 확실하게 접착되어지는 화장체의 간편한 제조법이 제공되는 것이다.As described above, according to the present invention, the cosmetic sheet which is not suitable for performing the uneven processing on its own in advance is adhered to the substrate, and the cosmetic sheet has a concave-convex pattern shape without being damaged at all. It is to provide a simple method of manufacturing a cosmetic to be securely bonded to.
Claims (1)
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP704 | 1980-05-26 | ||
| JP55-70490 | 1980-05-26 | ||
| JP7049080A JPS5817034B2 (en) | 1980-05-26 | 1980-05-26 | Method for producing a decorative body with an uneven pattern |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| KR830003304A KR830003304A (en) | 1983-06-18 |
| KR840000006B1 true KR840000006B1 (en) | 1984-01-25 |
Family
ID=13433004
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| KR1019800003072A Expired KR840000006B1 (en) | 1980-05-26 | 1980-08-01 | A manufacturing process of embossing sheet |
Country Status (2)
| Country | Link |
|---|---|
| JP (1) | JPS5817034B2 (en) |
| KR (1) | KR840000006B1 (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP4977715B2 (en) * | 2006-12-01 | 2012-07-18 | 株式会社クリエイティブ テクノロジー | Concave and convex pattern forming method |
| KR100768253B1 (en) * | 2007-01-24 | 2007-10-17 | 이기봉 | Wallpaper-type decorative plate with uneven decorative pattern |
-
1980
- 1980-05-26 JP JP7049080A patent/JPS5817034B2/en not_active Expired
- 1980-08-01 KR KR1019800003072A patent/KR840000006B1/en not_active Expired
Also Published As
| Publication number | Publication date |
|---|---|
| JPS56166011A (en) | 1981-12-19 |
| JPS5817034B2 (en) | 1983-04-04 |
| KR830003304A (en) | 1983-06-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2415680C (en) | Flocked transfer and article of manufacture including the flocked transfer | |
| AU614622B2 (en) | A gem compound and a method for making it | |
| AU2001280711A1 (en) | Flocked transfer and article of manufacture including the flocked transfer | |
| US3413168A (en) | Adhesive bonding method permitting precise positioning | |
| US2043809A (en) | Method of making cut-embossing stock sheets and article of manufacture | |
| JPS6036187A (en) | Method of decorating substrate material | |
| AU8325691A (en) | Process and device for dry printing of a workpiece or printed item using a thermographic film | |
| US2039284A (en) | Veneering | |
| CN110722896B (en) | Repeatedly sticking character-carving film and its making method | |
| JP3156701B2 (en) | Thermal transfer foil | |
| JPS5817034B2 (en) | Method for producing a decorative body with an uneven pattern | |
| US5637172A (en) | Method for applying a decal to foam | |
| JPH08197899A (en) | Method for decorating candle | |
| JPS5544806A (en) | Continuous bonding process of vinyl chloride sheets | |
| US6497778B1 (en) | Method for making holographic foil | |
| JPH0396324A (en) | Laminate processing | |
| JPH0239395B2 (en) | ||
| JPH04339652A (en) | Transfer apparatus and method | |
| JPS6467338A (en) | Manufacture of grooved decorative board | |
| JP2558382Y2 (en) | Decorative veneer sheet | |
| JPS6344871B2 (en) | ||
| JP2003147293A (en) | Adhesive sheet and method for producing the adhesive sheet | |
| GB1572789A (en) | Application of motifs to textiles | |
| JPS6233080U (en) | ||
| KR200305638Y1 (en) | The heat transcription film formed with hologram pattern |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PA0109 | Patent application |
St.27 status event code: A-0-1-A10-A12-nap-PA0109 |
|
| P11-X000 | Amendment of application requested |
St.27 status event code: A-2-2-P10-P11-nap-X000 |
|
| P13-X000 | Application amended |
St.27 status event code: A-2-2-P10-P13-nap-X000 |
|
| PG1501 | Laying open of application |
St.27 status event code: A-1-1-Q10-Q12-nap-PG1501 |
|
| PE0902 | Notice of grounds for rejection |
St.27 status event code: A-1-2-D10-D21-exm-PE0902 |
|
| P11-X000 | Amendment of application requested |
St.27 status event code: A-2-2-P10-P11-nap-X000 |
|
| P13-X000 | Application amended |
St.27 status event code: A-2-2-P10-P13-nap-X000 |
|
| PG1605 | Publication of application before grant of patent |
St.27 status event code: A-2-2-Q10-Q13-nap-PG1605 |
|
| PE0701 | Decision of registration |
St.27 status event code: A-1-2-D10-D22-exm-PE0701 |
|
| PR0701 | Registration of establishment |
St.27 status event code: A-2-4-F10-F11-exm-PR0701 |
|
| PR1002 | Payment of registration fee |
St.27 status event code: A-2-2-U10-U11-oth-PR1002 Fee payment year number: 1 |
|
| PC1903 | Unpaid annual fee |
St.27 status event code: A-4-4-U10-U13-oth-PC1903 Not in force date: 19870125 Payment event data comment text: Termination Category : DEFAULT_OF_REGISTRATION_FEE |
|
| PC1903 | Unpaid annual fee |
St.27 status event code: N-4-6-H10-H13-oth-PC1903 Ip right cessation event data comment text: Termination Category : DEFAULT_OF_REGISTRATION_FEE Not in force date: 19870125 |
|
| P22-X000 | Classification modified |
St.27 status event code: A-4-4-P10-P22-nap-X000 |