WO2009037210A2 - Eine thermoplastische zusammensetzung beinhaltend ein formtrennmittel basierend auf einem ester aus di- oder polyglycerinen und mindestens einer carbonsäure - Google Patents
Eine thermoplastische zusammensetzung beinhaltend ein formtrennmittel basierend auf einem ester aus di- oder polyglycerinen und mindestens einer carbonsäure Download PDFInfo
- Publication number
- WO2009037210A2 WO2009037210A2 PCT/EP2008/062198 EP2008062198W WO2009037210A2 WO 2009037210 A2 WO2009037210 A2 WO 2009037210A2 EP 2008062198 W EP2008062198 W EP 2008062198W WO 2009037210 A2 WO2009037210 A2 WO 2009037210A2
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- thermoplastic
- carboxylic acid
- thermoplastic composition
- mold release
- release agent
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K5/00—Use of organic ingredients
- C08K5/04—Oxygen-containing compounds
- C08K5/10—Esters; Ether-esters
- C08K5/101—Esters; Ether-esters of monocarboxylic acids
- C08K5/103—Esters; Ether-esters of monocarboxylic acids with polyalcohols
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K5/00—Use of organic ingredients
- C08K5/04—Oxygen-containing compounds
- C08K5/15—Heterocyclic compounds having oxygen in the ring
- C08K5/156—Heterocyclic compounds having oxygen in the ring having two oxygen atoms in the ring
- C08K5/1575—Six-membered rings
Definitions
- thermoplastic composition comprising a mold release agent based on an ester of di- or polyglycerols and at least one carboxylic acid
- the present invention relates to a thermoplastic composition, a process for producing a thermoplastic composition, the thermoplastic composition obtainable by this process, a process for producing a thermoplastic resin-based molded article, a molded article obtainable by this process, and the use of a mold release agent comprising an ester from di- or polyglycerols and at least one carboxylic acid.
- thermoplastic compositions based on thermoplastic polymers are frequently used for the production of moldings because of their thermoplastic properties.
- the thermoplastic compositions are heated to a temperature above the glass transition temperature of the thermoplastic polymers and then injected, for example by injection molding, in an injection mold, which gives the composition its desired shape.
- Effective mold release behavior is a key property for a thermoplastic composition to enable efficient and economical processing to moldings by, for example, injection molding.
- a mold releasing agent MRA
- the mold release agent may, as far as possible, chemically interact with the polymers and other components of the composition, or the composition, only to the extent that it is stable under processing conditions such that it does not lose its effectiveness and / or discoloration in another way adversely affect that the properties of the thermoplastic composition are not affected, or if unavoidable, only negligibly negatively.
- the mold release agent should not degrade the transparency.
- the mold release agent should not form deposits on the surface of the mold, nor should it migrate into the surface of the part after molding to such an extent that it becomes visible on the surface.
- Such deposition of a mold release agent on the surface of a molded article is referred to as "fogging".
- thermoplastic composition based on aromatic polycarbonates or mixtures of aromatic polycarbonates and polyesters which comprises a mixture of a fatty acid ester of a polyol having 2 to 6 hydroxyl groups and a C 10 -C 36 carboxylic acid and a saturated ⁇ -olefinic oligomer Mold release agent includes.
- the disadvantage of this thermoplastic composition is, inter alia, that the mold release agent contained therein, which consists of two chemically different components (fatty acid ester and ⁇ -olefinic oligomer), in its chemical composition is very complex.
- the transparency of the described in US 2005/0234171 Al, thermoplastic composition is still capable of improvement.
- the mold release agents used in the prior art have a high volatility, with the result that part of the mold release agent escapes due to the high temperatures in the production of moldings. This is not only of concern for toxicological reasons, but also leads to a deterioration of the detachment behavior of the thermoplastic compositions on the O ber vom an injection mold It is an object of the present invention to overcome, at least in part, the disadvantages arising from prior art in connection with thermoplastic molding compositions.
- An object of the invention was to provide a mold release agent that is characterized in addition to cost-effective manufacturability and good mold release properties by good environmental performance and in particular by its good biodegradability for use as a mold release agent in the production of fibers, films, films and moldings from biological degradable thermoplastic compositions.
- the present invention has the object, thermoplastic compositions, in particular, however, mainly or exclusively on thermoplastic polyester-based thermoplastic compositions to specify who, when used for the production of moldings, for example by injection molding, easily from the surface of the injection mold can be replaced, wherein the thermoplastic composition contains as few as possible, chemically different components and therefore can be produced cost-effective with as few process steps.
- thermoplastic composition having improved transparency compared to prior art thermoplastic compositions and also a thermoplastic composition as compared to those known in the art shows improved release behavior from the surface of an injection mold.
- thermoplastic composition in particular in the production of moldings from this thermoplastic composition, as less as possible, if possible, no components of this composition should escape, so that the toxicological burden associated with the Production of moldings concerned persons can be reduced to a minimum.
- a further object of the present invention was to provide a process by means of which the advantageous thermoplastic composition described above can be prepared.
- a further object of the present invention is to provide a process for the production of a shaped body, in which a thermoplastic composition is converted into a shaped body after heating to a temperature in the range of or above the glass transition temperature of the thermoplastic composition, whereby after cooling of the Shaped body of this compared to the known from the prior art moldings, especially in comparison to the from the prior art based on thermoplastic polyesters molded body, even better from the surfaces of the mold used for the production of the molded body detach.
- thermoplastic polyester a molded article based on a thermoplastic polyester, which can be produced in a more cost-effective manner compared to the known from the prior art, based on thermoplastic polyesters moldings and possibly also has improved transparency.
- thermoplastic composition A contribution to the solution of at least one of the objects mentioned at the outset is to provide a thermoplastic composition
- thermoplastic polymer a thermoplastic polymer
- the mold release agent comprises an ester of at least one alcohol component based on two or more glycerol units; and - at least one carboxylic acid or a derivative of a carboxylic acid or both.
- Preferred alcohol components are branched, unbranched or else cyclic alcoholic compounds based in each case on two or more, preferably 2 to 20 and particularly preferably 2 to 10 glycerol units. Also suitable as the alcohol component are mixtures of 2 or 3 or more of the abovementioned alcohol compounds. In this case, it is preferred that the proportion of alcohol compounds consisting of 5 and less glycerol units is at least 50% by weight, preferably at least 70% by weight and particularly preferably at least 80% by weight, based in each case on the alcohol component.
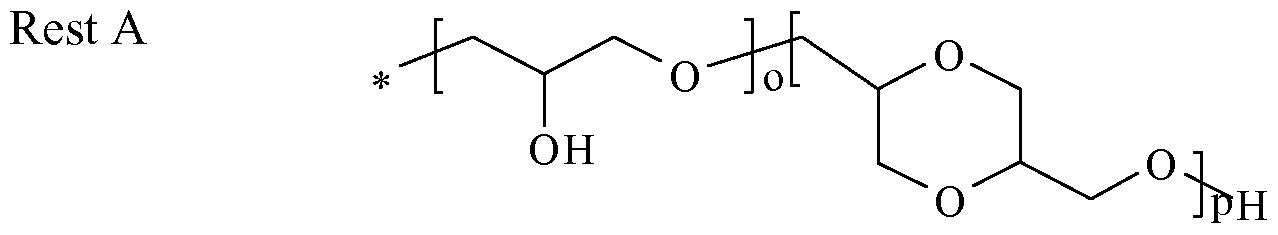
- thermoplastic composition corresponds to the alcohol component of the structure I or the structure II or a mixture of the two, wherein
- n as an integer in the range of 2 to 100, more preferably from 2 to 50, more preferably from 2 to 25, even more preferably from two to 10, more preferably from 2 to 5, and even more preferably from 2 to 4; o as an integer in the range of 0 to 70, more preferably from 1 to 50, more preferably from 1 to 25, even more preferably from 2 to 10, more preferably from 1 to 5 and even more preferably from 1 to 4; p is an integer from the range of 0 to 70, more preferably from 1 to 50, more preferably from 1 to 25, even more preferably from 2 to 10, more preferably from 1 to 5, and still more preferably from 1 to 4;
- one or more compounds of structure I to more than 50 wt .-%, preferably more than 75 wt .-% and particularly preferably more than 85 wt .-% contained in an alcohol component.
- one or more compounds of structure II are more than 50% by weight, preferably more than 75% by weight and more preferably more than 85% by weight in an alcohol component. The above percentages by weight each refer to the alcohol component.
- thermoplastic polymer refers to plastics that can be easily (thermo-plastic) deformed in a certain temperature range.This process is reversible and can be as often as desired by cooling and reheating to the molten state be repeated, as long as the thermal decomposition of the material does not start due to overheating.
- Thermoplastic polymers which may be present in the composition according to the invention are, in particular, thermoplastic polyurethanes, thermoplastic polyesters, thermoplastic polyamides, thermoplastic polyolefins, thermoplastic polyvinyl esters, thermoplastic polyethers, thermoplastic polystyrenes, thermoplastic polyimides, thermoplastic sulfur polymers, thermoplastic polyacetals, thermoplastic fluoroplastics, thermoplastic styrene-olefin copolymers, thermoplastic polyacrylates, thermoplastic ethylene-vinyl acetate copolymers or mixtures of two or more of the above-mentioned thermoplastic polymers in question.
- thermoplastic polyurethanes thermoplastic polyesters, thermoplastic polyamides, thermoplastic polyolefins, thermoplastic polyvinyl esters, thermoplastic polyethers, thermoplastic polystyrenes, thermoplastic polyimides, thermoplastic sulfur polymers, thermoplastic polyacetals, thermoplastic fluoroplastics, thermoplastic styrene-ole
- thermoplastic polymer to more than 90 wt .-%, more preferably more than 95 wt .-%, more preferably at least 99 wt .-% and most preferably to 100 wt. -%, based in each case on the total weight of the thermoplastic polymer, based on thermoplastic polyesters.
- polyester polymers formed by polycondensation reaction between a polycarboxylic acid and a polyol (so-called “4A-BB polyester”) or by polycondensation reaction of a hydroxycarboxylic acid or by ring-opening polymerization of a cyclic ester (so-called called “A5 'polyester”).
- polycarbonates which are obtainable by reaction of phosgene with diols can be excluded from the term "polyester” as used in the invention.
- thermoplastic polyesters and copolyester can be used as component a) in the thermoplastic composition according to the invention.
- polyesters include substantially linear polyesters prepared by a condensation reaction of at least one polycarboxylic acid, preferably a dicarboxylic acid (diacid) or an ester-forming derivative thereof and at least one polyol, preferably a dihydric alcohol (diol) ,
- the preferred dibasic acid and preferably divalent diol may both be either aliphatic or aromatic, but aromatic and partially aromatic polyesters are particularly preferred as thermoplastic molding materials in view of their high softening points and hydrolytic stability.
- substantially all ester linkages are attached to the aromatic rings.
- Partially aromatic polyesters obtained from at least one aromatic dicarboxylic acid or an ester-forming derivative thereof and at least one aliphatic diol are particularly preferably thermoplastic polyesters according to the invention.
- suitable aromatic dicarboxylic acids include terephthalic acid, 1,4-naphthalenedicarboxylic acid or 4,4'-biphenyldicarboxylic acid.
- suitable aliphatic diols include alkylene diols, especially those containing 2 to 6 carbon atoms, preferably 2 to 4 carbon atoms, in particular ethylene glycol, propylene diols and butylene diols.
- thermoplastic polyester as a polyol or diol component ethylene glycol, 1,3-propylene diol or 1,4-butylene diol.
- thermoplastic polyesters obtainable by reaction of a dicarboxylic acid with a diol include, in particular, polyalkylene terephthalates, for example polyethylene terephthalate (PET), polypropylene terephthalate (PPT) or polybutylene terephthalate (PBT), polyalkylene naphthalates, for example polyethylene naphthalate (PEN ) or polybutylene naphthalate (PBN), polyalkylenedibenzoates, for example polyethylene bibenzoate and mixtures of at least two of these thermoplastic polyesters.
- PET polyethylene terephthalate
- PPT polypropylene terephthalate
- PBT polybutylene terephthalate
- polyalkylene naphthalates for example polyethylene naphthalate (PEN ) or polybutylene
- partially aromatic polyesters described above may optionally contain a minor amount of units derived from other dicarboxylic acids, for example isophthalic acid, or other diols such as cyclohexanedimethanol, which generally reduces the melting point of the polyester.
- a specific group of partially aromatic polyesters are so-called segmented or block copolyesters which, in addition to the abovementioned polyester segments (also called “hard segments"), contain so-called “soft segments”. These soft segments are made of a flexible polymer; that is, a substantially amorphous polymer having a low glass transition temperature (T g ) and low rigidity, with reactive end groups, preferably two hydroxyl groups.
- the glass transition temperature of this "soft segments” below 0 C, more preferably below - 20 0 C and most preferably below - 40 0 C.
- several different polymers may be used as a soft segment Suitable Beispie- Ie for "soft. Segments "are aliphatic polyethers, aliphatic polyesters or aliphatic polycarbonates.
- the molecular weight of the soft segments may vary within wide limits, but is preferably between 400 and 6,000 g / mol.
- thermoplastic polymers may also be present in the thermoplastic composition according to the invention. contained by polycondensation reaction of short-chain hydroxycarboxylic acids or by ring-opening reaction of cyclic esters.
- thermoplastic polymers examples include in particular
- Suitable cyclic esters include, in particular, glycolide (a dimer of glycolic acid) and ⁇ -caprolactone (a cyclic ester of 6-hydroxycaproic acid).
- thermoplastic polyesters described above are also described, inter alia, in the "Cyclopedia of Polymer Science and Engineering", Volume 12, pages 1-75 and pages 217-256, John Wiley & Sons (1988) and also in “Ullmann's Encyclopedia of Industrial Chemistry, Vol. A21, pages 227 to 251, VCH Publishers Inc. (1992).
- Thermoplastic polymers preferred according to the invention are polyethylene terephthalate (PET), polybutylene terephthalate (PBT) and polylactic acid (PLA), wherein each of these polymers per se in a preferred embodiment of a thermoplastic composition of the present invention to more than 50 wt .-%, preferably more than 75 wt .-% and particularly preferably more than 90 wt .-%, each based on the thermoplastic composition may be included.
- PET polyethylene terephthalate
- PBT polybutylene terephthalate
- PLA polylactic acid
- the composition according to the invention furthermore comprises, as component b), a mold release agent which preferably comprises an ester of the alcohol component of structure I or structure II or a mixture of compounds of structure I and II and a carboxylic acid.
- a mold release agent which preferably comprises an ester of the alcohol component of structure I or structure II or a mixture of compounds of structure I and II and a carboxylic acid.
- ester of the alcohol component of structure I or II and a carboxylic acid as used herein is meant merely to indicate that the ester, in terms of its chemical composition, is an ester of an alcohol component of the structure. describe I or II and a carboxylic acid. In principle, however, the ester can, in addition to the reaction of the carboxylic acid with the alcohol component of the structure I or II, also by the reaction of the carboxylic acid with glycidol can be obtained.
- carboxylic acid as used herein includes the carboxylic acid in its protonated form, the carboxylic acid in its deprotonated form (ie, especially salts of the carboxylic acid), and mixtures of the carboxylic acid in its protonated form and its deprotonated form
- Term "carboxylic acid” basically all compounds which have at least one carboxylic acid group. It therefore also includes, in particular, compounds which, in addition to the at least one carboxylic acid group, also have other functional groups, such as, for example, hydroxyl groups, keto groups or ether groups. Dicarboxylic acids, tricarboxylic acids or carboxylic acids having more than three carboxyl groups are also encompassed by the term “carboxylic acids", although monocarboxylic acids are particularly preferred.
- derivative (s) of a carboxylic acid includes all derivatives of a carboxylic acid which, when reacted with an alcohol, give a corresponding ester of the carboxylic acid, especially the term “derivative of a carboxylic acid” means the acid chlorides of the carboxylic acid and the acid anhydrides of the carboxylic acid. These derivatives preferably have an increased reactivity of the carboxylic acid group compared to the carboxylic acid, so that ester formation is favored on reaction with an alcohol.
- mold releasing agents comprising esters of an alcohol component of structure I and a carboxylic acid or a derivative of a carboxylic acid are used as the mold release agent contained in the thermoplastic composition of the present invention as component b). It is particularly preferred that the mold release agent to at least 50 wt .-%, more preferably at least 60 wt .-% and most preferably at least 75 wt .-%, each based on the total weight of the mold release agent based on the above-described ester.
- carboxylic acid which is used as the ester component of the mold release agent b there are, in particular, saturated or unsaturated carboxylic acids having a number of carbon atoms in a range of 6 to 26, more preferably in a range of 8 to 24, even more preferably in a range of 10 to 22, moreover preferably in a range of 12 to 20, and most preferably in a range of 14 to 18 into consideration.
- carboxylic acids in particular, are therefore fatty acids.
- carboxylic acids include, in particular, caproic acid, enanthic acid, caprylic acid, pelargonic acid, capric acid, lauric acid, myristic acid, fish oil, palmitic acid, pelagic acid, margaric acid, stearic acid, isostearic acid, arachic acid, behenic acid, lignoceric acid, cerotic acid, undecylenic acid, oleic acid, elaidic acid, vaccenic acid , Icosenoic acid, rapeseed oil, cetoleic acid, erucic acid, nervonic acid, linoleic acid, linolenic acid, arachidonic acid, timnodonic acid, clupanodonic acid or cervonic acid.
- carboxylic acids are hydroxycarboxylic acids, among these hydroxy fatty acids such as ricinoleic acid, 12-hydroxy stearic acid, hydrogenated castor oil fatty acids (fatty acids containing small amounts of stearic acid and palmitic acid, as well as 12-hydroxystearic acid), sabinic acid, 2-hydroxytetradecanoic acid, Ipurolinic acid (3,11-dihydroxytetradecanoic acid, 2-hydroxyhexadecanoic acid, jalapinolic acid, juniperic acid, ambrettolic acid, aleuritic acid, 2-hydroxyoctadecanoic acid, 18-hydroxyoctadecanoic acid, 9,10-dihydroxyoctadecanoic acid, camiolanoic acid, ferric acid, cerebronic acid, 9-hydroxystearic acid and Hydroxystearic acid is most preferred and 12-hydroxystearic acid and ricinoleic acid are most preferred.
- the abovementioned carboxylic acids can be
- alcohol component in principle all known in the art on two or more glycerol units based compounds into consideration.
- Particularly suitable as the alcohol component are one or more compounds of structures I or II or mixtures thereof. In connection with these structures, reference is made to the above statements.
- the alcohol component of the ester accordingly comprises diglycerols, triglycerols, tetraglycerols or else polyglycerols or a mixture thereof. These can be obtained by condensation of more than four glycerol molecules. Such di-, tri-, tetra- or polyglycerols can be obtained by methods known to those skilled in the art, but in particular by base or acid-catalyzed condensation of glycerol.
- esters of a carboxylic acid and an alcohol component of the structure I or II used as mold release agents or as part of the mold release agent can be prepared by any process known to the person skilled in the art for preparing such an ester, but in particular by reacting the carboxylic acid with the alcohol component of the structure I or II or by the reaction of the carboxylic acid with glycidol.
- esters take place by the reaction of the carboxylic acid with the alcohol component of the structure I or II, then both components are initially charged and then catalyzed in the presence of a suitable esterification catalyst.
- esterification catalysts acids such as sulfuric acid or p-toluenesulfonic acid, or metals and their compounds can be used. Suitable examples are tin, titanium, zirconium, which are used as finely divided metals or expediently in the form of their salts, oxides or soluble organic compounds.
- the metal catalysts are in the Unlike protonic acids, high-temperature catalysts that usually reach their full activity only at temperatures above 180 0 C.
- esterification catalysts are one or more divalent tin compounds or tin compounds or elemental tin, which can react with the educts to form divalent tin compounds.
- the catalyst used may be tin, tin (II) chloride, tin (II) sulfate, tin (II) alcoholates or tin (II) salts of organic acids, in particular of mono- and dicarboxylic acids.
- Particularly preferred tin catalysts are tin (II) oxalate and tin (II) benzoate.
- the esterification reaction between the carboxylic acid and the alcohol component of the structure I or II can be carried out by methods known to the person skilled in the art. It may be particularly advantageous to remove the water formed during the reaction from the reaction mixture, wherein this removal of the water is preferably carried out by distillation, optionally by distillation with alcohol used in excess. Also, after carrying out the esterification reaction, unreacted alcohol can be removed from the reaction mixture, and this removal of the alcohol is preferably carried out by means of distillation. Furthermore, after completion of the esterification reaction, in particular after the removal of unreacted alcohol, the catalyst remaining in the reaction mixture, if appropriate after treatment with a base, can be separated off by filtration or by centrifuging.
- Optimum temperatures depend on the feed alcohol (s), reaction progress, the type of catalyst and the catalyst concentration from. They can easily be determined by experiment for each individual case. Higher temperatures increase the reaction rates and promote side reactions, such as dehydration from alcohols or formation of colored by-products.
- the desired temperature or the desired temperature range can be adjusted by the pressure in the reaction vessel (slight overpressure, atmospheric pressure or optionally negative pressure).
- the preparation of the ester is effected by the reaction of a carboxylic acid with glycidol, it is likewise preferred to carry out this esterification in the presence of suitable catalysts, acidic catalysts based in particular on phosphoric acid being preferred in this case.
- suitable catalysts include, in particular, phosphoric acids or esters thereof.
- Suitable catalysts are, in particular, phosphoric acid, phosphoric anhydride, polyphosphoric acid, orthophosphoric acid, metaphosphoric acid, phosphorophosphoric acid, triphosphoric acid and tetraphosphoric acid, and acidic phosphoric esters, such as methyl acid phosphate, ethyl acid phosphate, isopropyl acid phosphate, butyl acid phosphate and 2-ethylhexyl acid phosphate. Also monoester compounds, diester compounds and mixtures can be used.
- mixtures of different esters each of which can be obtained by esterification of a carboxylic acid with an alcohol or a glycidol, or mixtures of at least one ester, by esterification of a carboxylic acid with an alcohol and at least one further ester, the can be obtained by esterification of a carboxylic acid with glycidol, be used as a mold release agent or component of a mold release agent.
- mixtures of different esters, which in terms of their Carboxylic differ can be used as a mold release agent or as part of the mold release agent.
- the mold release agent contained as component b) comprises an ester of a carboxylic acid, preferably of a fatty acid, and diglycerol, triglycerol or tetraglycerol.
- the ester of a carboxylic acid and the alcohol component of the structure I or II used as mold release agent or constituent of the mold release agent (component b) it is preferred that not all hydroxyl groups of the alcohol are esterified, but that part of the hydro - xyl groups remain unesterified.
- the hydroxyl groups of the alcohol are at least 5 mol%, more preferably at least 10 mol%, even more preferably at least 20 mol%, more preferably at least 30 mol% moreover, preferably at least 40 mole% and most preferably at least 50 mole% are not esterified with the carboxylic acid group of the carboxylic acid.
- mold release agent is at least 5 Mo 1% of all for producing the mold release agent of a carboxylic acid and the alcohol component the structure I or II in the alcohol component of the structure I or II originally present hydroxyl groups are not esterified and therefore also present in the final mold release agent as a hydroxyl group.
- thermoplastic composition in addition to the thermoplastic polymer (component a) and the mold release agent (component b), further additives may optionally also be present.
- Other additives include, in particular, modulus modifiers, filler materials, reinforcing agents, flame retardant compounds, heat and UV stabilizers, antioxidants, other processing aids, nucleating agents, dyes and anti-dripping agents. Examples of suitable modulus modifiers, filler materials, reinforcing agents and flame retardant compounds can be found inter alia US 2005/0234171 Al.
- thermoplastic composition according to the invention, it is preferred that the thermoplastic composition
- thermoplastic polymer 60 to 99.99 wt.%, more preferably 80 to 99.8 wt.% and most preferably 90 to 99.6 wt.% of the thermoplastic polymer, bl) 0.01 to 20 wt. %, more preferably 0.1 to 10% by weight and most preferably 0.2 to 5% by weight of the mold release agent, and c1) 0 to 20% by weight, particularly preferably 0.1 to 10% by weight and most preferably from 0.2% to 5% by weight of the further additives,
- thermoplastic composition each based on the total weight of the thermoplastic composition, wherein the sum of the components al) to cl) is 100 wt .-%.
- thermoplastic composition In another embodiment according to the invention, it is preferred that the thermoplastic composition
- thermoplastic polymer 1 to 69.99 wt.%, more preferably 1.5 to 49.8 wt.%, and most preferably 2 to 19.6 wt.% of the thermoplastic polymer, b2) 0.01 to 20 wt %, particularly preferably 0.1 to 10% by weight and most preferably 0.2 to 5% by weight of the mold release agent, c2) at least 10% by weight, preferably at least 20% by weight and particularly preferably at least 30% by weight of a biodegradable filling component and d2) 0 to 20% by weight, particularly preferably 0.1 to 10% by weight and most preferably 0.2 to 5% by weight of the further additives . in each case based on the total weight of the thermoplastic composition, wherein the sum of components a2) to d2) is 100% by weight.
- thermoplastic polymer As a biodegradable filling component, in principle all known and suitable appearing in the art. These include, in particular, single and multiple sugars, such as starch and starch derivatives, cellulose and cellulose derivatives, hemp, jute, bast, reed, reed, in particular, ground-meal, and other substances obtained from plants or a combination of at least two thereof.
- the thermoplastic polymer to at least 10 wt .-%, preferably at least 50 wt .-% and particularly preferably at least 75 wt .-%, each based on the thermoplastic polymer, on a from renewable raw materials can be generated monomer such as lactic acid based.
- This thermoplastic composition is particularly suitable for biodegradable disposable and disposable items such as crockery or cutlery.
- thermoplastic composition according to the invention it is preferred if these are less than 0.001% by weight, more preferably less than 0.0005% by weight and most preferably less than 0.0001% by weight of a saturated, ⁇ -olefinic oligomer of at least one C 6 -CiS ⁇ -Olefm contains.
- thermoplastic composition A contribution to the solution of at least part of the aforementioned object is further provided by a method for producing a thermoplastic composition
- thermoplastic polymer a thermoplastic polymer
- mold release agent a mold release agent
- optionally further additives a thermoplastic polymer
- thermoplastic polymer or a precursor of the thermoplastic polymer including the process steps: i) providing a thermoplastic polymer or a precursor of the thermoplastic polymer; ii) providing the mold release agent comprising an ester based at least on: an alcohol component based on two or more glycerine units; and at least one carboxylic acid or a derivative of a carboxylic acid or both; iii) optionally providing further additives; iv) mixing components i), ii) and optionally iii).
- thermoplastic polymers, mold release agents and other additives are those thermoplastic polymers, mold release agents and other additives which have already been mentioned at the outset in connection with the thermoplastic composition according to the invention as the preferred thermoplastic polymer, mold release agents and other additives.
- blending may be a dry blending operation in which the various components are blended below the melt processing temperature of the thermoplastic polymer, or a melt blending process wherein the components are blended, optionally premixed, and at the melt processing temperatures of the thermoplastic polymer.
- Melt-mixing processes include, in particular, the melt-edge method preferred according to the invention, which is obtained, for example, by continuous melt-kneading using a single-screw kneading machine, a twin-screw kneading machine of Gear-same-direction-rotation-type, gear-different-direction-rotation-type, non-gear-same-direction-rotation-type, non-gear-different-direction-rotation-type, or other types or by batch-melt-kneading using a roll-kneading machine, a Burbury kneader or the like can be realized. Also conceivable is a combination of a dry mixing process and a melt mixing process.
- the order and the manner of adding the individual components i), ii) and optionally iii) into the mixing device is basically not critical.
- initially the thermoplastic polymer and optionally the additives may be introduced into the mixing device and only then the mold release agent may be added.
- the mixing takes place according to at least one of the following measures: Ml) at the glass transition temperature of the thermoplastic polymer or at a temperature above the glass transition temperature of the thermoplastic polymer; M2) wherein the mold release agent is more liquid than the thermoplastic
- the mixing of the components i), ii) and optionally iii) in process step iv) of the process according to the invention is carried out by a melt mixing process.
- the mixing in process step iv) takes place at the glass transition temperature of the thermoplastic polymer or at a temperature above the glass transition temperature of the thermoplastic polymer.
- the mixing at a temperature in a range of 5 degrees below the glass transition temperature (T g ) to 200 0 C above the glass transition temperature of the thermoplastic polymer used, more preferably at a temperature in a range of 1 degree below the glass transition temperature (T g) to 180 0 C above the glass transition temperature of the thermoplastic polymer, and most preferably at a temperature in a range from 1 degree above the glass transition temperature (T g) to 150 0 C above the Glass transition temperature of the thermoplastic polymer used, but the upper limit of the temperature range is essentially limited by the decomposition temperature of the thermoplastic polymer used. Furthermore, it corresponds to embodiments of the invention, when the mixing takes place at temperatures in a range of 10 to 180 0 C and preferably 50 to 150 0 C above the glass transition temperature of the thermoplastic polymer used.
- the mold release agent in which the mold release agent is liquid than the thermoplastic polymer, it is preferred to use the mold release agent at a temperature at which this liquid and the thermoplastic polymer is not yet liquid.
- the temperature of the thermoplastic polymer is below the glass transition temperature of this polymer. That's the way it is preferred when the melting temperature of the mold release agent and the glass transition temperature of the thermoplastic polymer differ by at least 5 ° C, preferably at least 10 0 C and more preferably at least 30 0 C.
- the thermoplastic polymer it is in this embodiment and also generally preferred to use the thermoplastic polymer as granules. In general, all known in the art granular forms with spherical or cylinder-like spatial form in the present case come into consideration.
- the granule size determined by sieve analysis is in a range of 0.01 to 5 cm and preferably in a range of 0.1 to 4 cm for at least 70% by weight of the granule particles.
- the surfaces of the granule particles can be at least partially coated with the mold release agent according to the invention, so that an at least partially coated thermoplastic polymer granules are obtained. This allows the most homogeneous possible distribution of the mold release agent according to the invention in the thermoplastic composition, in particular if it is formulated as a formulation for the subsequent extrusion.
- thermoplastic polymer in which the mold release agent is added to the precursor of the thermoplastic polymer, mold release agents in liquid and also in solid form come into consideration.
- all precursors known to the person skilled in the art prior to obtaining the thermoplastic polymer are considered as precursors of the thermoplastic polymer. These include in particular precursors which have a lower molecular weight than the final thermoplastic polymer. It is preferred here that the molecular weight of the precursor differs from that of the finished thermoplastic polymer by at least 1.1, preferably at least 1.5, and more preferably at least 2-fold.
- thermoplastic polymer which preferably consist of 2 to 100 monomers, especially in the case of polycondensates
- the prepolymer is based on more than 100 monomers as repeat units, the Number of monomers as repeat units and thus the final molecular weight of the finished thermoplastic polymer is not reached.
- inventive mold release agent in each case to the monomers, oligomers or the prepolymer or at least two of these. In this way, in addition to a homogeneous distribution of the mold release agent according to the invention, incorporation of the mold release agent by chemical bonds with the thermoplastic polymer is achieved, usually by the conditions prevailing in the polymerization or polymerization.
- the process may also comprise the further process step v):
- thermoplastic composition preferably to a temperature in a range of 10 to 30 0 C and particularly preferably 15 to 25 ° C.
- thermoplastic composition which was obtained in process step iv) before, during or after carrying out process step v), but optionally also after the process step iv) and without carrying out the process step v) nor granulation.
- the components a) to c) are mixed together in relative amounts such that the thermoplastic composition obtained by mixing the components a) to c)
- thermoplastic polymer 60 to 99.99% by weight, more preferably 80 to 99.8% by weight and most preferably 90 to 99.6% by weight of the thermoplastic polymer, bl) from 0.01 to 20% by weight, more preferably from 0.1 to 10% by weight, and most preferably from 0.2 to 5% by weight of the mold release agent, and from c) from 0 to 20% by weight, particularly preferably 0.1 to 10% by weight and most preferably 0.2 to 5% by weight of the further additives,
- thermoplastic composition each based on the total weight of the thermoplastic composition, wherein the sum of the components al) to cl) is 100 wt .-%.
- the components a2) to d2) are mixed together in such relative amounts that the thermoplastic composition obtained by mixing the components a2) to d2)
- a2) 1 to 69.99 wt.%, more preferably 1.5 to 49.8 wt.%, and most preferably 2 to 19.6 wt.% of the thermoplastic polymer, b2) 0.01 to 20 wt %, more preferably 0.1 to 10% and most preferably 0.2 to 5% by weight of the mold release agent, c2) at least 10%, preferably at least 20%, and most preferably at least 30% by weight of a biodegradable filling component and d2) 0 to 20% by weight, more preferably 0.1 to 10% by weight and most preferably 0.2 to 5% by weight of the further additives .
- thermoplastic composition in each case based on the total weight of the thermoplastic composition, wherein the sum of components a2) to d2) is 100% by weight.
- thermoplastic composition in the course of the process according to the invention for producing a thermoplastic composition a saturated, ⁇ -olefinic oligomer of at least one C 6 -C 20 -alpha-olefin is used in at most such an amount that the mixing of the components al) to cl) or a2) to d2), thermoplastic composition less than 0.001 wt .-%, more preferably less as 0.0005 wt .-% and most preferably less than 0.0001 wt .-% of the saturated, ⁇ -olefinic oligomer.
- thermoplastic composition obtainable by the process described above.
- the thermoplastic composition exhibits a yellowness index of less than 6.64, preferably less than 6, more preferably less than 5, and further preferably less than 4.9 and even more preferably less than 4.7.
- the yellowness index is determined by the yellowness value, which is measured as the b * value according to the L *, a *, b * color system of a sample of the composition to be tested according to DIN 5033. Often the yellowing index is not below 2 or 3.
- a contribution to the solution of at least part of the aforementioned object is also achieved by a process for the production of a molding based on a thermoplastic composition, comprising the process steps:
- thermoplastic composition according to the invention; II) heating the thermoplastic composition to the glass transition temperature of the thermoplastic polymer or at a temperature above the glass transition temperature of the thermoplastic polymer; III) Production of a molded article from the heated, thermoplastic composition prepared in process step II).
- thermoplastic composition according to the invention is first of all provided, this preparation preferably taking place by a process comprising the process steps i), ii), iv) and optionally iii) and / or v) , Then, in process step II), the thermoplastic composition is heated to the glass transition temperature of the thermoplastic polymer or at a temperature above the glass transition temperature of the thermoplastic polymer.
- thermoplastic composition to a temperature in a range of 5 degrees below the glass transition temperature (T g ) to 100 0 C above the glass transition temperature of the thermoplastic polymer used, more preferably to a temperature in a range of 1 degree below the glass transition temperature (T g ) to 50 0 C above the glass transition temperature of the thermoplastic polymer employed, and most preferably to a temperature in the range of 1 degree above the glass transition temperature (T g ) to 20 0 C is above the glass transition temperature of the thermoplastic polymer used, but here too the upper limit of the temperature range is essentially limited by the decomposition temperature of the thermoplastic polymer used.
- the method steps I) and II) can be carried out simultaneously or in succession.
- a simultaneous implementation of process steps I) and II) is useful, for example, if the thermoplastic composition is prepared by means of a melt mixing process. It may optionally be advantageous here to convert the composition produced by the melt-blending method directly into a shaped body.
- Successive carrying out of process steps I) and II) is useful, for example, if the thermoplastic composition is produced by a dry mixing process or if the thermoplastic composition is produced by a melt blending process but is not subjected to the formation of a shaped article immediately after production but rather first according to the method step v) is cooled.
- process step III) of the process according to the invention for the production of a shaped body the heated, heat-treated, produced in process step II) is prepared.
- moplastic composition made a molding.
- injection molding, extrusion molding, compression molding, layer molding, lamination molding, cavity molding, vacuum molding and transfer molding are considered as a method of producing a molded article, with injection molding being particularly preferred.
- the mass cross-section is the cross-section of a region of the shaped body that consists of the thermoplastic molding composition of the invention.
- the mass cross-section represents the thickness of a wall of these containers or containers.
- the mass cross section represents the thickness of these threads or strands.
- the mass cross-section represents the strength of these two-dimensional structures.
- the web running from an extruder can be drawn onto a roll at a speed which is higher than that from the extruder in comparison with the exit speed.
- a container or container are obtained, so in addition to the stretching, pulling and spinning primarily the bubbles in step IV) is used.
- the mass cross-section reduction takes place by applying a gas pressure.
- the gas pressure is generally selected such that the thermoplastic composition, which is usually heated to at least the glass transition temperature, of the shaped body obtained in step III) can be expanded.
- the elongation is limited by the use of a mold having the final shape of the molded article.
- liquid containers such as freezers, trays and packaging for foods such as fruits, vegetables or meat and pharmaceuticals as tablets, capsules, suppositories or powders and containers for liquids produced.
- These liquid containers can be used in addition to liquids of the cosmetic or pharmaceutical industry in the food industry, preferably in the beverage industry as bottles, particularly preferably as reusable containers such as PET or PLA bottles.
- two or more of the method steps I) to IV) to be supplemented by further method steps and / or to run at least overlapping in time. This applies in particular to process steps III) and IV).
- step I) in the production of PET or PLA or PET-PLA bottles in step I) is at least 80 wt .-% PET or a mixture of a multiple sugar such as starch, usually with a proportion based on the mixture in a range of 30 to 70 wt .-%, preferably in a range of 40 to 60 wt .-%, with PLA or PLA with PET-containing inventive thermoplastic composition provided.
- step II) into a shaped body blank in step III) which, in addition to a closure region, usually has a stabilizing collar following the closure region, followed by a sleeve-like bottle region. Gas is fed through the closure area in step IV), which expands the bottle area to a limit through the bottle shape.
- bottles besides bottles, other shaped bodies can also be produced. These include disposable and reusable containers, such as plates, bowls, pots or cups, and cutlery such as knives, forks or spoons.
- the biodegradable thermoplastic compositions according to the invention are particularly suitable for these applications.
- shaped bodies preferably a bottle, particularly preferably a PET bottle, which are obtainable by the above-described process according to the invention for producing a shaped body.
- This shaped body preferably has a yellowing index of less than 6.64, preferably less than 6, more preferably less than 5, and furthermore preferably less than 4.9 and moreover preferably less than 4.7. Often the yellowing index is not below 2 or 3.
- a contribution to the solution of at least part of the abovementioned objects is also provided by the use of a mold release agent comprising at least one alcohol component based on two or more glycerol units; and at least one carboxylic acid or a derivative of a carboxylic acid, or both, in thermoplastic compositions, especially as mold release agents in thermoplastic polyester-based thermoplastic compositions.
- a mold release agent comprising at least one alcohol component based on two or more glycerol units; and at least one carboxylic acid or a derivative of a carboxylic acid, or both, in thermoplastic compositions, especially as mold release agents in thermoplastic polyester-based thermoplastic compositions.
- mold release agents and as thermoplastic polymers those mold release agents and thermoplastic polymers which have already been mentioned at the beginning are also preferred here in connection with the thermoplastic composition according to the invention, have been mentioned as preferred mold release agents and thermoplastic polymers.
- a mold release agent comprising an ester of at least one alcohol component based on two or more glycerine units, and at least one carboxylic acid or a derivative of a carboxylic acid or both, in the manufacture of liquid containers, in particular PET bottles, from thermoplastic polymers a preferred embodiment of the present invention.
- thermoplastic composition Preparation of a thermoplastic composition
- PET SP04 polyethylene terephthalate
- the mixing wall temperature was 40 0 C.
- 0.5 wt .-% of the previously prepared Digly- Cerinstearat added as a mold release agent.
- the material was granulated on a granulator (ZSK 26Mcc) with a screw conveyor.
- thermoplastic composition Production of moldings from the thermoplastic composition
- thermoplastic composition For the production of moldings from the thermoplastic composition, a fully hydraulic injection molding machine with a hydraulic clamping unit type Battenfeld HM800 / 210 was used. The maximum closing force is 800 kN, the screw diameter is 25 mm. As a test tool, a tool with a tapered, rectangular core was used. To determine the demolding force, a load cell with a maximum measuring range of 2 kN was attached to the ejector rod. The pre-drying of the molding compound was carried out at about 225 ° C for about 4 hours.
- thermoplastic additive an ester of diglycerol and stearic acid as a mold release agent in the thermoplastic additive.
- composition leads to a significant improvement in mold release and to a noticeably improved removal behavior from the walls of an injection molding tool.
- moldings with high transparency and smooth and uniform surface structure There were obtained moldings with high transparency and smooth and uniform surface structure.
- a yellowness index according to DIN 5033 averaged 6.64 for PET SP04 and 4.6 for PET SP04 + diglycerin stearate.
Landscapes
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Compositions Of Macromolecular Compounds (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
Abstract
Description


Claims


Priority Applications (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| BRPI0816700 BRPI0816700A2 (pt) | 2007-09-13 | 2008-09-12 | Composição termoplástica, método para produzir uma composição termoplástico, método para produzir um artigo moldado com base na composição termoplástica,artigo moldado, uso de um agente de liberação de molde |
| ES08804159.5T ES2559191T3 (es) | 2007-09-13 | 2008-09-12 | Una composición termoplástica que contiene un agente desmoldeante basado en un éster de di- o poliglicerinas y al menos un ácido carboxílico |
| JP2010524514A JP5334975B2 (ja) | 2007-09-13 | 2008-09-12 | ジグリセロールまたはポリグリセロールおよび少なくとも1つのカルボン酸のエステルに基づく離型剤を含有する熱可塑性組成物 |
| EP08804159.5A EP2203510B1 (de) | 2007-09-13 | 2008-09-12 | Eine thermoplastische zusammensetzung beinhaltend ein formtrennmittel basierend auf einem ester aus di- oder polyglycerinen und mindestens einer carbonsäure |
| US12/677,882 US8796355B2 (en) | 2007-09-13 | 2008-09-12 | Thermoplastic composition containing a mold release agent which is based on an ester of di- or polyglycerols and at least one carboxylic acid |
| CN200880115685.7A CN101855285B (zh) | 2007-09-13 | 2008-09-12 | 包含基于二-或聚甘油与至少一种羧酸的酯的脱模剂的热塑性组合物 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102007043753A DE102007043753A1 (de) | 2007-09-13 | 2007-09-13 | Eine thermoplastische Zusammensetzung beinhaltend ein Formtrennmittel basierend auf einem Ester aus Di- oder Polyglycerinen und mindestens einer Carbonsäure |
| DE102007043753.8 | 2007-09-13 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| WO2009037210A2 true WO2009037210A2 (de) | 2009-03-26 |
| WO2009037210A3 WO2009037210A3 (de) | 2009-05-28 |
Family
ID=40348540
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/EP2008/062198 Ceased WO2009037210A2 (de) | 2007-09-13 | 2008-09-12 | Eine thermoplastische zusammensetzung beinhaltend ein formtrennmittel basierend auf einem ester aus di- oder polyglycerinen und mindestens einer carbonsäure |
Country Status (9)
| Country | Link |
|---|---|
| US (1) | US8796355B2 (de) |
| EP (1) | EP2203510B1 (de) |
| JP (1) | JP5334975B2 (de) |
| CN (1) | CN101855285B (de) |
| BR (1) | BRPI0816700A2 (de) |
| DE (1) | DE102007043753A1 (de) |
| ES (1) | ES2559191T3 (de) |
| MY (1) | MY158814A (de) |
| WO (1) | WO2009037210A2 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2015063145A1 (de) * | 2013-10-31 | 2015-05-07 | Münch Chemie International GmbH | Trennmittel, insbesondere entformungshilfsmittel, verfahren zur herstellung des trennmittels und verwendung des trennmittels |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2009065903A2 (de) * | 2007-11-20 | 2009-05-28 | Cognis Oleochemicals Gmbh | Verfahren zur herstellung einer organischen zusammensetzung beinhaltend einen n-nonylester |
| DE102008026263A1 (de) * | 2008-06-02 | 2009-12-03 | Emery Oleochemicals Gmbh | Antibeschlagmittel auf Basis von Polyglycerin und nativen Ölen |
| DE102008044706A1 (de) * | 2008-08-28 | 2010-03-04 | Emery Oleochemicals Gmbh | Viskositätsreduzierer für Polyetherpolyole |
| TWI534197B (zh) | 2010-12-13 | 2016-05-21 | Wintech Polymer Ltd | Polybutylene terephthalate resin compositions and pellets thereof |
| JP2015527417A (ja) | 2012-06-13 | 2015-09-17 | アムリル アーゲー | 充填剤又は顔料を含む分散剤 |
| PL3167101T3 (pl) | 2014-07-08 | 2020-03-31 | Emery Oleochemicals Gmbh | Spiekalny surowiec do zastosowania w urządzeniach do druku 3d |
| DE102023208909A1 (de) | 2023-09-13 | 2025-03-13 | Volkswagen Aktiengesellschaft | Elektrodenmaterial für die elektrochemische Reduktion von Kohlenstoffdioxid, Elektrode und elektrochemische Zelle umfassend ein solches Elektrodenmaterial |
Family Cites Families (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3643968A1 (de) * | 1986-12-22 | 1988-06-30 | Neynaber Chemie Gmbh | Partialester gesaettigter, geradekettiger c(pfeil abwaerts)2(pfeil abwaerts)(pfeil abwaerts)2(pfeil abwaerts)-c(pfeil abwaerts)3(pfeil abwaerts)(pfeil abwaerts)4(pfeil abwaerts)-monocarbonsaeuren mit polyolen, verfahren zu ihrer herstellung sowie diese enthaltende trennmittel fuer kunststoffe, insbesondere auf basis von pvc oder pvc-copolymerisaten |
| JP2996531B2 (ja) | 1991-05-10 | 2000-01-11 | 昭和電工株式会社 | 包装用積層フィルム |
| JP3144972B2 (ja) * | 1993-12-16 | 2001-03-12 | ポリプラスチックス株式会社 | ポリエステル樹脂組成物 |
| EP0758641B1 (de) | 1995-08-11 | 2000-08-30 | Daicel Chemical Industries, Ltd. | Polyglycerinfettsäureester-Zusammensetzung, ihr Herstellungsverfahren, Verfahren zum Herstellen einer sehr reinen Polyglycerinfettsäureester-Zusammensetzung, eine sehr reine Polyglycerinfettsäureester-Zusammensetzung, ein Zusatzmittel für Lebensmittel, eine Harz-Zusammensetzung und eine Zusammensetzung für Kosmetika oder Waschmittel |
| US5576409B1 (en) * | 1995-08-25 | 1998-09-22 | Ici Plc | Internal mold release compositions |
| JP2000230084A (ja) * | 1999-02-09 | 2000-08-22 | Asahi Denka Kogyo Kk | 樹脂組成物 |
| JP2001279109A (ja) * | 2000-01-25 | 2001-10-10 | Mitsubishi Engineering Plastics Corp | 熱可塑性樹脂組成物 |
| DE10104815A1 (de) * | 2001-02-01 | 2002-08-08 | Cognis Deutschland Gmbh | Verfahren zur Herstellung von epoxidierten Glyceridacetaten |
| KR100952545B1 (ko) * | 2002-04-05 | 2010-04-12 | 디에스엠 아이피 어셋츠 비.브이. | 방향족 폴리카르보네이트 및/또는 폴리에스테르를함유하여 이형 거동을 개선시킨 열가소성 조성물 |
| JP4628649B2 (ja) * | 2003-02-10 | 2011-02-09 | 理研ビタミン株式会社 | 生分解性ポリエステル樹脂組成物の帯電防止法並びにフィルム、シート及び成形品 |
| JP4429835B2 (ja) | 2003-12-19 | 2010-03-10 | 竹本油脂株式会社 | 包装用フィルム |
| DE102004009895B3 (de) * | 2004-02-26 | 2005-07-21 | Cognis Deutschland Gmbh & Co. Kg | Gleitmittelkombinationen |
| DE102004038980A1 (de) * | 2004-08-10 | 2006-02-23 | Cognis Deutschland Gmbh & Co. Kg | Antibeschlagmittel für Kunststoffe |
| JP2006117737A (ja) * | 2004-10-19 | 2006-05-11 | Kaneka Corp | ポリエステル樹脂組成物およびそれから得られる成形体 |
| JP5358864B2 (ja) * | 2004-10-27 | 2013-12-04 | 東洋紡株式会社 | ポリエステル樹脂用改質剤、およびこれを用いた成形品 |
| DE502006006177D1 (de) * | 2006-07-20 | 2010-04-01 | Emery Oleochemicals Gmbh | Verwendung von Polyethylenglykolestern von Fettsäuren als Gleitmittel für thermoplastische Kunststoffe |
| DE102007027371A1 (de) * | 2007-06-11 | 2008-12-18 | Cognis Oleochemicals Gmbh | Verfahren zur Herstellung einer Verbindung aufweisend mindestens eine Ester-Gruppe |
-
2007
- 2007-09-13 DE DE102007043753A patent/DE102007043753A1/de not_active Ceased
-
2008
- 2008-09-12 JP JP2010524514A patent/JP5334975B2/ja not_active Expired - Fee Related
- 2008-09-12 US US12/677,882 patent/US8796355B2/en not_active Expired - Fee Related
- 2008-09-12 EP EP08804159.5A patent/EP2203510B1/de not_active Not-in-force
- 2008-09-12 BR BRPI0816700 patent/BRPI0816700A2/pt not_active Application Discontinuation
- 2008-09-12 WO PCT/EP2008/062198 patent/WO2009037210A2/de not_active Ceased
- 2008-09-12 ES ES08804159.5T patent/ES2559191T3/es active Active
- 2008-09-12 MY MYPI2010001099A patent/MY158814A/en unknown
- 2008-09-12 CN CN200880115685.7A patent/CN101855285B/zh not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2015063145A1 (de) * | 2013-10-31 | 2015-05-07 | Münch Chemie International GmbH | Trennmittel, insbesondere entformungshilfsmittel, verfahren zur herstellung des trennmittels und verwendung des trennmittels |
Also Published As
| Publication number | Publication date |
|---|---|
| US8796355B2 (en) | 2014-08-05 |
| CN101855285A (zh) | 2010-10-06 |
| CN101855285B (zh) | 2015-04-15 |
| JP2010539273A (ja) | 2010-12-16 |
| BRPI0816700A2 (pt) | 2015-03-17 |
| JP5334975B2 (ja) | 2013-11-06 |
| WO2009037210A3 (de) | 2009-05-28 |
| EP2203510A2 (de) | 2010-07-07 |
| US20100267860A1 (en) | 2010-10-21 |
| ES2559191T3 (es) | 2016-02-10 |
| DE102007043753A1 (de) | 2009-03-19 |
| EP2203510B1 (de) | 2015-11-11 |
| MY158814A (en) | 2016-11-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2193164B1 (de) | Eine thermoplastische zusammensetzung beinhaltend ein formtrennmittel basierend auf gehärteten vegetabilen estern | |
| EP2203510B1 (de) | Eine thermoplastische zusammensetzung beinhaltend ein formtrennmittel basierend auf einem ester aus di- oder polyglycerinen und mindestens einer carbonsäure | |
| DE69918233T2 (de) | Polymilchsäure zusammensetzung und daraus hergestellter film | |
| DE69636049T2 (de) | Verfahren zur Herstellung eines Formstückes aus aliphatischem Polyester und nach dem Verfahren hergestelltes Formstück | |
| DE60012381T2 (de) | Aliphatische Polyesterabmischung und daraus erhaltener verstreckter Film | |
| DE60215218T2 (de) | Milchsäurepolymerzusammensetzung und formkörper daraus | |
| DE68928938T2 (de) | Verfahren zur Weichmachung von Lactidpolymerisaten | |
| DE69306874T2 (de) | Durch Wärme formbare Zusammensetzung, Verfahren zu ihrer Herstellung und ihre Anwendung zur Herstellung von thermogeformten Gegenständen | |
| DE60209310T2 (de) | Aliphatishe Polyesterzusammensetzung und biegsame Erzeugnisse | |
| DE69313331T2 (de) | Biodegradierbarer Behälter aus Milchsäurepolymeren | |
| DE102009060851A1 (de) | Esterherstellung mit Nachbehandlung | |
| DE69323320T2 (de) | Mischungen aus stärkeestern und linearen polyestern | |
| DE102009060881A1 (de) | Wärmetauscher in Verfahren und Vorrichtung zur Herstellung eines Esters | |
| WO2015114126A1 (de) | Polymerzusammensetzung enthaltend plla und pdla | |
| DE2913215A1 (de) | Modifiziertes polyaethylenterephthalat, seine herstellung und verwendung | |
| EP1626064B1 (de) | Antibeschlagmittel für Kunststoffe | |
| EP1358267B1 (de) | Umweltfreundliche zusammensetzung | |
| EP1881025B1 (de) | Verwendung von Polyethylenglykolestern von Fettsäuren als Gleitmittel für thermoplastische Kunststoffe | |
| DE60036845T2 (de) | Aliphatische polyesterzusammensetzung für eine grundmischung und verfahren zur herstellung einer aliphatischen polyesterfolie unter verwendung der zusammensetzung | |
| EP2285885B1 (de) | Antibeschlagmittel auf basis von polyglycerin und nativen ölen | |
| DE2359012A1 (de) | Herstellung von polyesterharzen mit verbesserten presseigenschaften | |
| DE102004007429B4 (de) | Granulare Stabilisatorzusammensetzungen für halogenhaltige Polymere, deren Herstellung und Verwendung sowie Polymerzusammensetzungen | |
| DE19513237A1 (de) | Biologisch abbaubare Polymermischung | |
| DE4117308A1 (de) | Verwendung von gemischen aus fettsaeuredialkylendiamiden, fettsaeureestern und gegebenenfalls metallseifen als gleitmittel, insbesondere fuer abs-kunststoffe | |
| DE102007055595A1 (de) | Verfahren zur Herstellung einer organischen Zusammensetzung beinhaltend einen N-Nonylester |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 200880115685.7 Country of ref document: CN |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 08804159 Country of ref document: EP Kind code of ref document: A2 |
|
| DPE1 | Request for preliminary examination filed after expiration of 19th month from priority date (pct application filed from 20040101) | ||
| DPE1 | Request for preliminary examination filed after expiration of 19th month from priority date (pct application filed from 20040101) | ||
| ENP | Entry into the national phase |
Ref document number: 2010524514 Country of ref document: JP Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1761/DELNP/2010 Country of ref document: IN |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2008804159 Country of ref document: EP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: PI 2010001099 Country of ref document: MY |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 12677882 Country of ref document: US |
|
| ENP | Entry into the national phase |
Ref document number: PI0816700 Country of ref document: BR Kind code of ref document: A2 Effective date: 20100312 |