WO2012143263A1 - Procédé et appareil permettant de sertir des récipients et double sertissage obtenu de la sorte - Google Patents
Procédé et appareil permettant de sertir des récipients et double sertissage obtenu de la sorte Download PDFInfo
- Publication number
- WO2012143263A1 WO2012143263A1 PCT/EP2012/056460 EP2012056460W WO2012143263A1 WO 2012143263 A1 WO2012143263 A1 WO 2012143263A1 EP 2012056460 W EP2012056460 W EP 2012056460W WO 2012143263 A1 WO2012143263 A1 WO 2012143263A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- seam
- chuck
- seaming
- double
- double seam
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D51/00—Making hollow objects
- B21D51/16—Making hollow objects characterised by the use of the objects
- B21D51/26—Making hollow objects characterised by the use of the objects cans or tins; Closing same in a permanent manner
- B21D51/30—Folding the circumferential seam
- B21D51/32—Folding the circumferential seam by rolling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D51/00—Making hollow objects
- B21D51/16—Making hollow objects characterised by the use of the objects
- B21D51/26—Making hollow objects characterised by the use of the objects cans or tins; Closing same in a permanent manner
- B21D51/2615—Edge treatment of cans or tins
- B21D51/2623—Curling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D51/00—Making hollow objects
- B21D51/16—Making hollow objects characterised by the use of the objects
- B21D51/26—Making hollow objects characterised by the use of the objects cans or tins; Closing same in a permanent manner
- B21D51/2653—Methods or machines for closing cans by applying caps or bottoms
- B21D51/2661—Sealing or closing means therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D7/00—Containers having bodies formed by interconnecting or uniting two or more rigid, or substantially rigid, components made wholly or mainly of metal
- B65D7/12—Containers having bodies formed by interconnecting or uniting two or more rigid, or substantially rigid, components made wholly or mainly of metal characterised by wall construction or by connections between walls
- B65D7/34—Containers having bodies formed by interconnecting or uniting two or more rigid, or substantially rigid, components made wholly or mainly of metal characterised by wall construction or by connections between walls with permanent connections between walls
- B65D7/36—Containers having bodies formed by interconnecting or uniting two or more rigid, or substantially rigid, components made wholly or mainly of metal characterised by wall construction or by connections between walls with permanent connections between walls formed by rolling, or by rolling and pressing
Definitions
- This invention relates to the seaming of containers, in particular forming a double seam between a container end and a container body.
- the container body is of steel, for example double reduced, and the steel end has a peripheral curl into which a flange on the container body is lifted and the seam is formed in two operations.
- first operation seaming roll With specific radii, permits formation of small seams made of thin starting materials, e.g. less than 0.25 thickness aluminium or aluminium alloy.
- US 5911551 specifies the forming of a double seam of small dimensions with particular relevance to beverage cans and can ends formed from aluminium alloy sheet about 0.25 (0.010”) thick or tinplate or TFS (tin free steel) about 0.23 (0.009”) thick.
- the containers are generally manufactured from steel and the seamed container must often be able to withstand any differential pressures, which result from processing the product within the container.
- One method of minimising the differential pressure and strength requirement is known as an “overpressure” retort where in-can pressure generated, additional to the vapour pressure of the steam (differential pressure) during the sterilisation process, may be balanced by the introduction of air pressure. This method is often used when the container is closed by a peelable end but may also be of use when sterilising specific food products in a container with standard diameter can ends.
- Double seams for joining steel or double reduced (“DR”) steel container (can) bodies and steel ends are well known and are manufactured according to standard criteria.
- the seam which has five layers of metal, must be sealed with lining compound to resist processing and abuse. Any seam, which is not sealed, offers a leakage path, which can allow micro-organisms to enter the can, resulting in product degradation or even food poisoning.
- SEFEL has categorised seam dimensions to ensure interchangeability between food cans and ends from different sources. In addition to these SEFEL categories there are also specified critical seam dimensions required after the two operations for forming the double seam.
- the end is curled into an inter-locking position with the can flange by pressure from a seaming roll.
- the seam is considered to be complete.
- the distance between the top of the seaming chuck lip and seaming roll entrance angle is considered to be critical to prevent metal being pushed over the chuck lip, which can lead to sharp seams and cut-overs, and poor control of countersink depth.
- the five layers of metal, which were loosely interlocked in the first operation, are compressed and the seam is “ironed”.
- the second operation forces sealing compound into any void spaces in the double seam.
- Ends which are used for seaming to a double reduced (“DR”) steel body have standard features but are not generally of DR material since this is very stiff and prone to wrinkling in the seam. Wrinkles are associated with a lack of tightness in the double seam.
- This invention seeks to provide a method and apparatus for downgauging the double seam of a steel container, whilst leaving the end press tooling and seaming roll profiles unchanged, in contrast with the prior art for manufacture of seams with small dimensions.
- the method and apparatus of the present invention is thus intended to be suitable for seaming tighter and smaller seams on a steel container, but without the tooling costs of US 5911551 or WO 9723312 .
- a method of forming a double seam between a flange of a container body formed from steel of from 0.10 to 0.15 gauge and a steel end including a peripheral curl comprising the steps of: supporting the end on a chuck; moving a lifter to lift the flange of the can body into the peripheral curl of the end; applying a first operation tool to the periphery of the end progressively to form the end and to make a first operation seam; applying a second operation tool to flatten the first operation seam to form the complete double seam; wherein pressure is applied to the body throughout at least the first operation to encourage the body flange to become a body hook in the double seam; characterised in that: the end for forming into the double seam is 0.10 to 0.14 gauge, low temper material; and the method is characterised by: increasing the height of a chuck wall lip portion of the chuck, such that, in use, the lip is spaced from a seaming panel of the end by more than 0.1; applying the first operation tool
- Standard practice for the seaming of steel ends considers that space is required within the seaming roll profile for containing the can end seaming panel/curl.
- the Applicant has discovered that when the end material is low temper thin material, it is possible to use a seaming roll profile, which guides the seaming panel by contacting the curl. This is carried out in conjunction with increasing the chuck lip height.
- the present invention also irons the seam in the second operation by applying the face of the second operation roll at an angle, preferably about 4°.
- the lip is spaced from the seaming panel by at least 0.5 , which takes more material out of the standard seaming panel and reduces or avoids wrinkling further.
- an apparatus for forming a double seam between a flange of a container body formed from steel of from 0.10 to 0.15 gauge and a steel end including a peripheral curl comprising: a chuck to support the end; a lifter to lift the flange of the body into the peripheral curl; a first operation tool moveable towards and away from the periphery of the end wall to form the end and to form a first operation seam; a second operation tool moveable towards and away from the periphery of the end wall to flatten the first operation seam and to complete the double seam; and lifting means to apply compressive pressure in an axial direction to the body during at least the first operation of seaming; characterised in that the steel end for forming into the double seam is 0.10 to 0.14 gauge, low temper material; the chuck includes an increased height cylindrical lip portion, the height of the lip portion being such that, in use, the lip is spaced from a seaming panel of the end by more than 0.1; the first operation seaming roll
- the lip is spaced from the seaming panel by at least 0.5 , which takes more material out of the standard seaming panel and reduces or avoids wrinkling further.
- the angle of the second operation roll flat surface preferably matches the angle of the chuck lip, and these may ideally be about 4° so that the surfaces of the roll and chuck lip are substantially parallel.
- the method and apparatus of the present invention involve minor modifications to the seaming chuck but otherwise no first operation tooling or press changes.
- the chuck lip height is increased but the first operation seaming roll is standard, making contact at a higher position.
- the second operation roll has a flat face with tight radii at both ends. It is therefore possible in the present invention to form a seam from thinner low temper material with minimal changes to existing food can end tooling.
- the method and apparatus of the present invention provide a balance between end hook wrinkling, sharp corners and waviness, whilst maintaining the critical seam dimensions noted above.
- a double seam joining a flange of a container body formed from double reduced steel of from 0.10 to 0.15 gauge and a steel end wall including a peripheral curl, in which the end wall is formed from a steel end of 0.10 to 0.14 gauge, low temper material, and has a centre panel within the peripheral curl; the double seam is inclined at an angle of 4° to an axis perpendicular to the centre panel; and the double seam is substantially free of wrinkles.
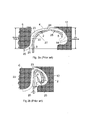
- Figures 1a to 1d are diagrammatic side views of known seam forming apparatus at various stages in the formation of a double seam;
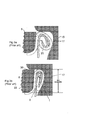
- Figures 2a and 2b are fragmentary sections through a can end and can body during formation of a known first operation seam;
- Figures 3a and 3b are fragmentary sections through a can end and can body during formation of a known second operation seam;
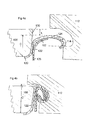
- Figures 4a and 4b are fragmentary sections through a can end and can body during formation of a first operation seam using tooling according to the invention;
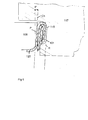
- Figure 5 is a fragmentary section through a can end and can body during formation of a finished seam using second operation tooling according to the invention.
- Fig 1 shows known prior art apparatus for forming a double seam 1 between a flange 2 of a container body 3 and an end wall 4 having a peripheral curl 5.
- This apparatus has a chuck to support the end wall 4, a movable lifter 7 axially aligned with the chuck to lift the flange 2 of the can body into the peripheral curl 5 of the end wall 4.
- seaming apparatus in which the can does not rotate, in this particular example the chuck is driven to rotate in a turret 10 and the lifter 7 is freely mounted for rotation on a spring 8 in a follower 9 mounted in the turret 10. If desired, the lifter may be driven to rotate at the same speed as the chuck.
- the follower 9 is urged to rise and fall by a cam 11 as the turret rotates from positions (a) to (d) in Fig 1.
- a first operation seaming roll 12 is supported for free rotation on a pivotable arm 13 which holds a first operation seaming profile 14 of the roll at a level to receive the peripheral curl 5 of the can end as the first operation roll is swung in to progressively generate the first operation seam of Figs 1b and Fig 2b from the assembled body and can end as shown in Fig 2a.
- the follower has moved from a low portion of the cam 11 at which the can end and body are assembled between the chuck and lifter, to a higher position at which the can end is firmly clamped onto the body flange 2.
- the lifting force on the follower 9 is delivered through spring 8 to the lifter 7 so that the can and end assembly is resiliently clamped under a known pressure imposed by the cam in the axial direction.
- Fig 1c shows the apparatus at commencement of a second operation to complete a double seam.
- the cam 11 has raised the follower 9 from the position shown in Fig 1b and Fig 3(a) to continue to apply a compressive pressure on the body and end.
- a second operation seaming roll 17 is supported for free rotation on a pivotable arm 16 which holds a second operation seam forming profile 15 at a level to receive the first operation seam as the arm is swung-in to progressively flatten the first operation seam and to complete a double seam 1 as shown in Figs 3(b) and 1(d).
- Fig 2a shows a peripheral portion of a can end 4 resting on the flange 2 of a can body 3 at commencement of a first operation of double seaming.
- the can end 4 comprises a centre panel 20, a countersink wall 22 joined to the centre panel by a countersink wall radius 21, a seaming panel 24 joined to the countersink wall by a seaming panel radius 23, and a peripheral curl 5.
- An annulus of lining compound 25 extends around the inside of the curl 5.
- the can body 3 comprises a sidewall portion 26, and t flange 2 joined to the sidewall by a flange radius 27.
- a chuck 6 supports the countersink wall 22 while the first operation seaming roll 12 is moved laterally towards the chuck 6 so that the profile 14 of the first operation roll turns the seaming panel downwards and the curl 5 inwards and upwards to extend between the sidewall portion and the turned down flange or body hook as shown in Fig 2b.
- Fig 2b shows a preferred form of first operation seam in which the turned down flange or body hook 2 is bedded in the annulus of lining compound 25 and the free edge of the end curl (now also referred to as cover hook) 5 reaches well up into the gap between the sidewall portion 26 and the turned-down flange 2.
- This configuration of first operation seam reforms well in the second operation of seaming to achieve adequate overlaps of body flange/hook 2 and end curl/cover hook 5, and subsequent seam tightness in the finished seam.
- the seaming panel radius 23 could be bent to a tighter radius, which would then stand proud of the bent down flange radius. Excess metal in the first operation seam may give rise to a short end hook, excessive seam length or pleating (corrugation) during the second operation. The "slack" metal of panel radius may even be pushed inwards and disturbs the chuck wall fit in the sidewall.
- Fig 2b shows a first operation seam made according to known seaming processes.
- the pressure applied by cam 11 has been passed through the sidewall portion 26 to feed sidewall metal into the first operation seam so tightening the body flange radius 27 to fit the seaming panel radius 23. It is essential that the free edge 29 of the cover hook in the first operation seam is not in contact with the side wall 26 and must be outboard of the arcuate surface 28.
- Fig 3b shows the completed double seam 1 after the second operation roll 17 has cooperated with the chuck 6 (Fig 3a) so as progressively to flatten the arcuate surface of the first operation seam, reducing any wrinkles and generate the double seam 2 by crushing the first operation seam of Fig 2c.
- the can end and body hooks 5, 2 overlap tightly, with lining compound 25 filling any voids and covering “exposed” metal at the ends of both hooks.
- Fig 4a and 4b show fragmentary sections through a can end and can body during formation of a first operation seam using tooling according to the invention.
- a chuck 106 supports the countersink wall 122 while the first operation seaming roll 112 is moved laterally towards the chuck 106.
- the countersink 122 has a depth C from the centre panel 120 to the seaming panel 124.
- the chuck lip 130 of the chuck 106 of the invention has an increased chuck lip height L measured, as shown, from the seaming panel 124 to the top of the chuck lip.
- the position of the first operation seaming roll 112 is raised so that the top of the chuck lip and the top surface of the first operation seaming profile 114 are inter-related, and are approximately at the same level. There are no changes to the first operation seaming roll.
- the widths of the seaming panel 124 and container flange 102 are standard.
- Fig 4b shows the first operation seam after forming with the modified chuck-roll relationship of the invention.
- the countersink 122 has increased depth C’ due to the space available in which the seam has been formed.
- Standard double seaming practice is that the seaming of steel ends requires space between the seaming roll profile and the seaming panel/curl.
- the Applicant has found that when forming a steel end of 0.10 to 0.14 gauge, low temper material, it is not necessary to contain the curl as it is possible to guide the can end by contact between the seaming roll and the end curl and still form satisfactory seams.
- the double seam 101 has been formed using a second operation seaming roll 117 with its profile adapted to give maximum area for seam growth.
- the face 115 of the second operation seaming roll is flat over most of its length and has tight radii at its ends.
- Both the second operation seaming roll surface and the working face of chuck lip (line Ch) are parallel and inclined at an angle, approximately 4° in this example. This angle is measured relative to a line P, which is perpendicular to the top of the chuck 106.
- a double seam developed using 0.13 low temper steel and formed in accordance with the method and apparatus of the present invention has been found to have good integrity and to meet all critical seaming parameters.
- Development samples passed helium leak testing at nominal, loose and tight settings, before and after overpressure processing. Internal end hook appearance was acceptable with a maximum tightness rating of 100%. Visually there was minimal or only slight waviness at the base of the seam but this did not affect seam integrity. Any waviness was considered to be an acceptable feature of seaming 0.13 material, giving substantial cost savings for reducing by over six gauges from standard end thicknesses (i.e. from 0.19 material).
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Rigid Containers With Two Or More Constituent Elements (AREA)
Abstract
La présente invention a trait à un procédé et à un appareil permettant de sertir des récipients, ainsi qu'à un double sertissage joignant le bord d'un corps de récipient et une paroi d'extrémité de récipient. Le procédé et l'appareil utilisent une paroi de cale dotée d'une partie de lèvre (130), qui est augmentée en termes de hauteur, et une seconde molette de sertissage (117) qui est dotée d'une face plate. Les changements mineurs apportés à l'outillage de sertissage (106, 117) permettent la formation de doubles sertissages à partir d'une extrémité comprimée standard d'acier mince et de faible dureté et d'un corps de récipient en acier réduit double, qui est sensiblement sans pli.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP11162769.1 | 2011-04-18 | ||
| EP11162769 | 2011-04-18 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2012143263A1 true WO2012143263A1 (fr) | 2012-10-26 |
Family
ID=45974324
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/EP2012/056460 Ceased WO2012143263A1 (fr) | 2011-04-18 | 2012-04-10 | Procédé et appareil permettant de sertir des récipients et double sertissage obtenu de la sorte |
Country Status (1)
| Country | Link |
|---|---|
| WO (1) | WO2012143263A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106734713A (zh) * | 2017-03-20 | 2017-05-31 | 山东胜宁电器有限公司 | 一种杯体加工方法 |
| CN106807850A (zh) * | 2017-03-20 | 2017-06-09 | 山东胜宁电器有限公司 | 容器口部压合装置及设备 |
| USD1068472S1 (en) | 2023-05-01 | 2025-04-01 | C-Loop Packaging Sweden Ab | Can end |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0664171A1 (fr) * | 1994-01-19 | 1995-07-26 | Schmalbach-Lubeca AG | Outil pour machines de fermeture |
| WO1997023312A1 (fr) | 1995-12-23 | 1997-07-03 | Carnaudmetalbox Plc | Contenants |
| US5911551A (en) | 1994-07-20 | 1999-06-15 | Carnaudmetalbox Plc | Containers |
| US20040074911A1 (en) * | 2001-07-03 | 2004-04-22 | Container Development, Ltd. | Can shell and double-seamed can end |
-
2012
- 2012-04-10 WO PCT/EP2012/056460 patent/WO2012143263A1/fr not_active Ceased
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0664171A1 (fr) * | 1994-01-19 | 1995-07-26 | Schmalbach-Lubeca AG | Outil pour machines de fermeture |
| US5911551A (en) | 1994-07-20 | 1999-06-15 | Carnaudmetalbox Plc | Containers |
| WO1997023312A1 (fr) | 1995-12-23 | 1997-07-03 | Carnaudmetalbox Plc | Contenants |
| US20040074911A1 (en) * | 2001-07-03 | 2004-04-22 | Container Development, Ltd. | Can shell and double-seamed can end |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106734713A (zh) * | 2017-03-20 | 2017-05-31 | 山东胜宁电器有限公司 | 一种杯体加工方法 |
| CN106807850A (zh) * | 2017-03-20 | 2017-06-09 | 山东胜宁电器有限公司 | 容器口部压合装置及设备 |
| CN106734713B (zh) * | 2017-03-20 | 2018-09-18 | 山东胜宁电器有限公司 | 一种杯体加工方法 |
| USD1068472S1 (en) | 2023-05-01 | 2025-04-01 | C-Loop Packaging Sweden Ab | Can end |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA1280701C (fr) | Methode et dispositif de mise en forme de panneaux d'extremite pour contenants, et panneaux ainsi produits | |
| US5911551A (en) | Containers | |
| US5704240A (en) | Method and apparatus for forming threads in metal containers | |
| US3964413A (en) | Methods for necking-in sheet metal can bodies | |
| US9334078B2 (en) | Can manufacture | |
| US5957647A (en) | Containers | |
| EP1603802B1 (fr) | Appareil et procede de sertissage pour boites de conserve | |
| US4991735A (en) | Pressure resistant end shell for a container and method and apparatus for forming the same | |
| US4885924A (en) | Method of forming containers | |
| EP0497346A1 (fr) | Fermeture d'extrémité en tôle résistante à la pression | |
| IE851182L (en) | Sealing canisters | |
| CN101227987A (zh) | 用于在容器端盖中形成加强卷边的方法和装置 | |
| CA2787546C (fr) | Fabrication d'une boite | |
| CA2080972A1 (fr) | Contenant obtenu par emboutissage et etirage, appareil et methode correspondants | |
| US4264017A (en) | Container shape | |
| US20060186127A1 (en) | Reinforced can end - can body joints with laser seaming | |
| JPH0773766B2 (ja) | 缶用シェル | |
| HUE031786T2 (en) | Method for closing metal boxes | |
| JP2020535969A (ja) | ロール縁部を形成する方法 | |
| JPH04220125A (ja) | 缶端板 | |
| US3416476A (en) | Container closure seaming method and apparatus | |
| CN212551195U (zh) | 罐体卷边装置 | |
| US20140197181A1 (en) | Three-piece can | |
| US7454827B2 (en) | Threaded pedestal cup | |
| EP0868234A1 (fr) | Contenants |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 12714672 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 12714672 Country of ref document: EP Kind code of ref document: A1 |