EP0085976A1 - Dauerform für fallende Giessweise mit mindestens zwei nebeneinander angeordneten Formhohlräumen - Google Patents
Dauerform für fallende Giessweise mit mindestens zwei nebeneinander angeordneten Formhohlräumen Download PDFInfo
- Publication number
- EP0085976A1 EP0085976A1 EP83101140A EP83101140A EP0085976A1 EP 0085976 A1 EP0085976 A1 EP 0085976A1 EP 83101140 A EP83101140 A EP 83101140A EP 83101140 A EP83101140 A EP 83101140A EP 0085976 A1 EP0085976 A1 EP 0085976A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- permanent
- mold
- cavities
- mold cavities
- compensating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/06—Permanent moulds for shaped castings
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/20—Stack moulds, i.e. arrangement of multiple moulds or flasks
Definitions
- the present invention relates to a permanent mold with at least two mold cavities arranged side by side.
- This permanent form is particularly suitable for use for direct falling pouring.
- the falling pouring method enables a high liquid metal output to be achieved through controlled solidification.
- the solidification can be further improved up to almost 100%.
- the more favorable temperature gradient in the casting, i.e. the hottest metal in the upper part of the casting supports the desired solidification direction from bottom to top, where the feeder is placed.
- the falling casting method is also used for smaller castings, but with a barrel system and with gates, which results in lower liquid metal output and higher stress on the permanent mold, which inevitably leads to a shorter service life.
- the aim of the present invention is to propose a permanent mold with which, on the one hand, the advantages of the falling casting method can be used for lighter castings, and on the other hand, several castings can be cast at once.
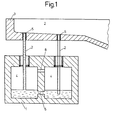
- the single figure shows a multiple permanent form 1, which is filled directly with a liquid metal 2 falling from above.
- the liquid metal 2 flows from a container 3 via several pouring nozzles 5 simultaneously into the mold cavities 4 of the permanent mold 1.
- the container 3 can be a holding furnace or a distributor with pouring nozzles. When using a distributor and a ladle, the amount of liquid metal should be adapted to the casting or castings so that the losses through Metal residues remain minimal.
- the individual cavities are connected by means of compensation channels 6.
- the pouring nozzle cross sections are also graduated. These measures guarantee that the same climbing speed and filling time are achieved in all cavities.
- the connection is provided in the lower part of the mold cavities.
- several compensating connections are necessary, which are preferably arranged one above the other in parallel. Since an irregular filling speed usually occurs at the beginning and at the end of the casting process, it is usually necessary to provide the compensating connections in the lower and in the upper part of the mold cavity.
- the upper compensation connection can also be arranged between the feeders.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Slide Fasteners (AREA)
- Bag Frames (AREA)
- Buckles (AREA)
- Vehicle Interior And Exterior Ornaments, Soundproofing, And Insulation (AREA)
- Blow-Moulding Or Thermoforming Of Plastics Or The Like (AREA)
- Casting Devices For Molds (AREA)
Abstract
Description
- Die vorliegende Erfindung bezieht sich auf eine Dauerfcrm mit mindestens zwei nebeneinander angeordneten Formhohlräumen.
- Diese Dauerform eignet sich insbesondere zur Verwendung für die direkte fallende Giessweise.
- Die fallende Giessweise ermöglicht es ein hohes Flüssigmetallausbringen durch gesteuerte Erstarrung zu erreichen. Durch Optimierung der Giessgeschwindigkeit, im Verhältnis zum Wärmetransport zwischen dem Gussstück und der Formwand kann die Erstarrung weiter bis zu beinahe 100 % verbessert werden. Der günstigere Temperaturgradient im Gussstück, d.h. das heisseste Metall im oberen Teil des Gussstückes, unterstützt die gewünschte Erstarrungsrichtung von unten nach oben, wo der Speiser plaziert ist.
- Dieses Verfahren kann in der Regel nur für genügend schwere Gussstücke eingesetzt werden. Beim mechanisierten Dauerformgiessverfahren liegt die untere wirtschaftliche Grenze bei Gussstückgewichten zwischen 10 und 25 kg.
- Zwar wird die fallende Giessweise auch für kleinere Gussstücke eingesetzt, jedoch mit Laufsystem und mit Anschnitten, was zu einem niedrigeren Flüssigmetallausbringen, sowie zur höheren Belastung der Dauerform, somit zwangsläufig zur kürzeren Lebensdauer führt.
- Ziel der vorliegenden Erfindung ist es eine Dauerform vorzuschlagen mit welcher einerseits die Vorteile der fallenden Giessweise auch für leichtere Gussstücke genutzt werden können, und andererseits mehrere Gussstücke auf einmal gegossen werden können.
- Dieses Ziel wird erfindungsgemäss durch die Lehre des Anspruches 1 gelöst.
- Weitere vorteilhafte Ausgestaltungen ergeben sich aus den abhängigen Ansprüchen.
- Die Erfindung wird anhand der beigelegten Zeichnung beispielsweise näher erläutert.
- Die einzige Figur zeigt eine mehrfache Dauerform 1, die direkt mit einem von oben fallenden flüssigen Metall 2 gefüllt wird. Das flüssige Metall 2 fliesst aus einem Behälter 3 über mehrere Giessdüsen 5 gleichzeitig in die Formhohlräume 4 der Dauerform 1. Der Behälter 3 kann ein Warmhalteofen oder ein Verteiler mit Giessdüsen sein. Bei der Verwendung eines Verteilers und einer Giesspfanne soll die Flüssigmetallmenge dem Gussstück bzw. den Gussstücken so angepasst werden, dass die Verluste durch Metallresten minim bleiben.
- Um die Füllgeschwindigkeit in allen Formhohlräumen 4 auszugleichen sind die einzelnen Hohlräume mittels Ausgleichskanälen 6 verbunden. Zudem sind die Giessdüsenquerschnitte abgestuft. Diese Massnahmen garantieren, dass in allen Hohlräumen die gleiche Steiggeschwindigkeit und die gleiche Füllzeit erreicht werden.
- Bei kleinen Gussstücken ist es möglich, mit nur einer Ausgleichsverbindung den Ausgleich zwischen den Hohlräumen zu erreichen. In diesem Fall wird die Verbindung im unteren Teil der Formhohlräume vorgesehen. Bei grösseren Gussstücken dagegen sind mehrere Ausgleichsverbindungen notwendig, die vorzugsweise parallel übereinander angeordnet werden. Da eine unregelmässige Füllgeschwindigkeit meistens am Anfang und am Ende des Giessvorganges auftritt ist es in der Regel notwendig, die Ausgleichsverbindungen im unteren und im oberen Teil des Formhohlraumes vorzusehen. Als eine weitere Möglichkeit kann die obere Ausgleichsverbindung auch zwischen den Speisern angeordnet sein.
- Bei genug grosser Dimensionierung der Ausgleichsverbindung bei mittelgrossen Gussstücken ist die Anordnung nur einer oberen Verbindung ausreichend.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT83101140T ATE13495T1 (de) | 1982-02-10 | 1983-02-07 | Dauerform fuer fallende giessweise mit mindestens zwei nebeneinander angeordneten formhohlraeumen. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CH811/82A CH654500A5 (de) | 1982-02-10 | 1982-02-10 | Dauerform mit mindestens zwei nebeneinander angeordneten formhohlraeumen. |
| CH811/82 | 1982-02-10 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0085976A1 true EP0085976A1 (de) | 1983-08-17 |
| EP0085976B1 EP0085976B1 (de) | 1985-05-29 |
Family
ID=4195728
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP83101140A Expired EP0085976B1 (de) | 1982-02-10 | 1983-02-07 | Dauerform für fallende Giessweise mit mindestens zwei nebeneinander angeordneten Formhohlräumen |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP0085976B1 (de) |
| JP (1) | JPS58148047A (de) |
| AT (1) | ATE13495T1 (de) |
| AU (1) | AU1123683A (de) |
| CH (1) | CH654500A5 (de) |
| DE (1) | DE3360218D1 (de) |
| ZA (1) | ZA83794B (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4241009C1 (de) * | 1992-12-05 | 1994-02-17 | Pohl Gmbh & Co Kg | Verschluß für eine Medikamentenflasche |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1031981A (fr) * | 1951-02-02 | 1953-06-29 | Procédé de fabrication en série par moulage en mottes à joints verticaux pour tout objet en métal ou matière moulée par gravité | |
| US2799906A (en) * | 1953-01-26 | 1957-07-23 | William M Duncan | Apparatus and method of filling ingot molds |
| DE1932971A1 (de) * | 1969-06-28 | 1971-01-07 | Howmet Corp | Keramische Verbundform und Verfahren zu ihrer Herstellung |
-
1982
- 1982-02-10 CH CH811/82A patent/CH654500A5/de not_active IP Right Cessation
-
1983
- 1983-02-07 JP JP58017568A patent/JPS58148047A/ja active Pending
- 1983-02-07 DE DE8383101140T patent/DE3360218D1/de not_active Expired
- 1983-02-07 AT AT83101140T patent/ATE13495T1/de active
- 1983-02-07 EP EP83101140A patent/EP0085976B1/de not_active Expired
- 1983-02-07 ZA ZA83794A patent/ZA83794B/xx unknown
- 1983-02-08 AU AU11236/83A patent/AU1123683A/en not_active Abandoned
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1031981A (fr) * | 1951-02-02 | 1953-06-29 | Procédé de fabrication en série par moulage en mottes à joints verticaux pour tout objet en métal ou matière moulée par gravité | |
| US2799906A (en) * | 1953-01-26 | 1957-07-23 | William M Duncan | Apparatus and method of filling ingot molds |
| DE1932971A1 (de) * | 1969-06-28 | 1971-01-07 | Howmet Corp | Keramische Verbundform und Verfahren zu ihrer Herstellung |
Also Published As
| Publication number | Publication date |
|---|---|
| AU1123683A (en) | 1983-08-18 |
| DE3360218D1 (en) | 1985-07-04 |
| ZA83794B (en) | 1983-10-26 |
| EP0085976B1 (de) | 1985-05-29 |
| ATE13495T1 (de) | 1985-06-15 |
| CH654500A5 (de) | 1986-02-28 |
| JPS58148047A (ja) | 1983-09-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE7532061U (de) | Einrichtung fuer den mechanisierten niederdruckguss | |
| WO2013164225A1 (de) | VERFAHREN ZUM GIEßEN EINES MIT MINDESTENS EINER DURCHGANGSÖFFNUNG VERSEHENEN GUSSTEILS | |
| CH676094A5 (de) | ||
| DE3151714C1 (de) | Verfahren zur Herstellung von kristallinen Schaufeln | |
| DE2648730C3 (de) | Maschine zum Gießen unter Niederdruck oder unter Gegendruck | |
| DE1963421C3 (de) | Stützkonstruktion für eine Niederdruckgießeinrichtung | |
| EP0085976B1 (de) | Dauerform für fallende Giessweise mit mindestens zwei nebeneinander angeordneten Formhohlräumen | |
| DE102010044606A1 (de) | Das Verfahren der Flüssigmetallbeschickung in der Stranggießanlage und die Vorrichtung für Realisierung des Verfahrens | |
| DE10247751B4 (de) | Verfahren und Vorrichtung zum Verschweißen kopfgehärteter Schienen | |
| EP1050356A1 (de) | Verfahren und Vorrichtung zum Füllen von Giessformen mit flüssigen Metallen | |
| DE69415117T2 (de) | Verfahren und Vorrichtung zum Wiederdruckgiessen | |
| DE3401354A1 (de) | Verfahren zum giessen von graugussteilen | |
| DE2321908A1 (de) | Tragvorrichtung fuer ein gefaess zur aufnahme von metallschmelze | |
| DE4332760A1 (de) | Verfahren zum Betreiben einer Niederdruckmetallgießvorrichtung und Niederdruckmetallgießvorrichtung dafür | |
| EP1685916A1 (de) | Verbundgußplatte | |
| DE2634894C2 (de) | Formenstapel mit Formen aus chemisch gebundenem Formstoff | |
| DE7729772U1 (de) | Niederdruck-giesseinrichtung fuer gussstuecke | |
| DE202006010504U1 (de) | Vorrichtung zum Druckbeaufschlagen von Kernsand in einer Kernschießmaschine und Kernschießmaschine | |
| DE876752C (de) | Form zum Giessen von Zylinderbloecken, Zylinderkoepfen od. dgl. | |
| DE10308208A1 (de) | Gießanlage | |
| DE11840C (de) | Vorrichtungen zum Giefsen des Flufseisens aus der Bessemerbirne | |
| DE69007343T2 (de) | Verfahren und Anlage zum Entgasen und Aufrechterhalten eines niedrigen Wasserstoffgehaltes in legierten Aluminiumschmelzen während des Pfannentransportes. | |
| DE69214067T2 (de) | Steigender Guss mit geregelter Formfüllung und Form für genanntes Verfahren | |
| DE2509688A1 (de) | Vorrichtung zum fuellen von formen mit metallschmelze | |
| DD150341A1 (de) | Einrichtung und verfahren zum stranggiessen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19830207 |
|
| AK | Designated contracting states |
Designated state(s): AT BE DE FR GB IT NL SE |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): AT BE DE FR GB IT NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19850529 |
|
| REF | Corresponds to: |
Ref document number: 13495 Country of ref document: AT Date of ref document: 19850615 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3360218 Country of ref document: DE Date of ref document: 19850704 |
|
| ET | Fr: translation filed | ||
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19860207 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19860208 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Effective date: 19860228 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| BERE | Be: lapsed |
Owner name: GEORG FISCHER A.G. Effective date: 19860228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19861031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19861101 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19881122 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 83101140.8 Effective date: 19861023 |